Category: Quality, NCR, and Continuous Improvement

Quality loop mechanics that connect nonconformance to action and prevention, with defensible evidence trails. Focuses on dispositions, MRB discipline, CAPA closure, and the operational interfaces that stop repeat issues.

  • What is ISO 9001?

    What is ISO 9001?

    ISO 9001 is the international standard that specifies requirements for a quality management system (QMS). The current version, ISO 9001:2015, establishes what an organization’s QMS must achieve to demonstrate the ability to consistently provide products and services that meet customer and applicable statutory and regulatory requirements. Published by the International Organization for Standardization, ISO 9001 belongs to the ISO 9000 family of quality management standards—a set of international standards addressing different aspects of quality management.

    Within that family, ISO 9001 is the requirements standard. It defines what a QMS must accomplish, not how an organization must implement it. The standard does not prescribe specific methods, tools, or software. It sets outcome-oriented requirements across clauses 4 through 10, covering areas from organizational context and leadership to performance evaluation and improvement. These requirements are deliberately generic, making ISO 9001 applicable to organizations of all sizes and sectors, including aerospace manufacturing, maintenance, repair, and overhaul operations.

    This technology-neutral, sector-agnostic design means the same structure applies whether an organization relies on paper-based documentation or integrated digital platforms. ISO 9001 establishes the baseline; sector-specific standards and organizational processes determine how that baseline is met in practice.
    The image depicts an aerospace manufacturing floor featuring precision assembly operations alongside quality inspection stations, emphasizing a quality management system that adheres to ISO 9001 standards. This environment showcases a commitment to customer satisfaction, continual improvement, and effective risk management through structured processes and internal audits.

    The ISO 9000 family and the role of ISO 9001

    The ISO 9000 family originated in 1987, drawing on earlier national standards such as the British Standard BS 5750. Maintained by ISO Technical Committee 176 (ISO/TC 176), these international standards address quality management from multiple angles. The family has evolved through several revisions, with the 2000 version consolidating previously separate standards into a unified process-based framework.

    Three standards define the core of the ISO 9000 family. ISO 9000 establishes fundamentals and vocabulary, providing definitions for terms such as “quality,” “conformity,” “risk,” and “interested parties” that underpin the other standards. ISO 9001 specifies the auditable requirements for a quality management system based on demonstrated capability to meet customer and regulatory requirements. ISO 9004 offers guidance for organizations seeking sustained success beyond basic compliance, addressing performance improvement and organizational maturity.

    ISO 9001 is the only standard in the ISO 9000 series that contains normative requirements suitable for third-party certification. When organizations certified to a quality management standard reference their certification, they are typically referring to ISO 9001. Third party certification bodies, accredited through national accreditation bodies affiliated with the International Accreditation Forum, conduct audits to verify conformity with ISO 9001 requirements. This certification process provides external validation that an organization’s QMS meets the standard’s requirements.

    Sector-specific standards build on ISO 9001 rather than replacing it. In aerospace, AS9100 incorporates all ISO 9001 requirements and adds sector-specific controls for configuration management, product safety, and other stakeholders’ expectations particular to aviation, space, and defense. The same structure applies across industries: IATF 16949 for automotive, ISO 13485 for medical devices, and similar frameworks all use ISO 9001 as their foundation.

    What ISO 9001 specifies at a high level

    ISO 9001:2015 is organized into 10 clauses. Clauses 0 through 3 provide introductory context, scope, normative references, and terms and definitions. Clauses 4 through 10 contain the normative QMS requirements—the sections against which organizations are audited.

    Clause 4 addresses the context of the organization. It requires determination of internal and external issues relevant to the organization’s purpose and strategic direction, identification of interested parties and their requirements, definition of QMS scope, and establishment of processes and their interactions. This includes understanding factors such as market conditions, regulatory environment, and organizational culture that affect the ability to achieve intended results.

    Clause 5 establishes leadership requirements. Top management must demonstrate leadership commitment to the QMS, establish quality policy aligned with organizational direction, assign roles and responsibilities, and promote customer focus throughout the organization. Leadership requirements in ISO 9001 place accountability at the executive level rather than delegating quality to a single department.

    Clause 6 covers planning. Organizations must address risks and opportunities relevant to achieving quality objectives, establish measurable quality objectives consistent with the quality policy, and plan actions to achieve those objectives. Risk based thinking, strengthened in the 2015 revision, replaces earlier prescriptive preventive action requirements with a systematic approach to identifying and addressing effects of uncertainty.

    Clause 7 specifies support requirements. This includes determining and providing necessary resources (people, infrastructure, environment, monitoring and measuring resources, organizational knowledge), ensuring competence through education, training, or experience, maintaining awareness of quality policy and objectives, establishing communication processes, and controlling documented information. The 2015 revision replaced mandatory documents and documented procedures with the more flexible concept of documented information, allowing organizations to determine appropriate formats and media.

    Clause 8 addresses operation—the actual realization of products and services. Requirements cover operational planning and control, requirements determination and review, design and development, control of external providers, production and service provision, release of products and services, and control of nonconforming outputs. For manufacturing organizations, this clause directly addresses production controls, supplier management, and nonconformity handling.

    Clause 9 covers performance evaluation. Organizations must monitor, measure, analyze, and evaluate QMS performance, including customer satisfaction. Internal audits and management reviews are required at planned intervals to assess QMS suitability, adequacy, and effectiveness.

    Clause 10 addresses improvement. Requirements include determining opportunities for improvement, responding to nonconformities through corrective actions, and pursuing continual improvement of QMS suitability, adequacy, and effectiveness.

    The process approach is central to ISO 9001:2015. Organizations must identify their processes, determine inputs and outputs, establish criteria and methods for effective operation and control, and manage process interactions. This approach, combined with the Plan-Do-Check-Act (PDCA) methodology embedded in the standard’s structure, provides a framework for systematic management rather than isolated controls.

    The intent of a Quality Management System under ISO 9001

    The stated purpose of a QMS under ISO 9001 is to enable organizations to consistently provide products and services that meet customer requirements and applicable statutory and regulatory requirements. The standard explicitly connects QMS effectiveness to the objective of enhancing customer satisfaction through system application, including processes for continual improvement and assurance of conformity.

    ISO 9001 frames quality management as a system of interrelated processes, not as a series of isolated inspections or end-of-line checks. Quality objectives link to organizational strategy. Resource allocation, competence development, and operational controls work together to achieve planned results. Customer expectations inform requirements determination, and customer satisfaction data feed back into improvement processes. Evidence based decision making grounds actions in data analysis rather than assumption.

    The seven quality management principles articulated in ISO 9000 inform this approach. Customer focus drives the system’s purpose. Leadership provides direction and creates conditions for achieving quality objectives. Engagement of people ensures competent, empowered personnel at all levels. The process approach enables consistent outcomes through systematic management of activities and resources. Continuous improvement addresses changing conditions and opportunities. Evidence-based decision making relies on data analysis. Relationship management addresses interactions with external providers and other stakeholders. These quality management principles underpin the requirements specified in ISO 9001, though the standard itself does not require formal adoption of each principle as a separate activity.

    The intent, in operational terms, is a management system that produces predictable outputs, responds systematically to deviations, and improves over time. For manufacturing operations, this translates to controlled processes, traceable records, defined authorities, and mechanisms for identifying and correcting problems before they propagate.

    Requirements versus implementation: what ISO 9001 does and does not dictate

    ISO 9001 specifies what an organization’s QMS must achieve. It does not prescribe how those outcomes are realized. This distinction between requirements and implementation is fundamental to understanding the standard’s design.

    The standard requires documented information to be maintained and retained for QMS operation and evidence of conformity. It does not specify document formats, software systems, or file structures. An organization may use paper-based records, electronic document management systems, or integrated digital platforms. The requirement is met when documented information is controlled, accessible, and adequate for its intended purpose.

    Nonconformity management provides another example. Clause 10 requires organizations to react to nonconformities, evaluate the need for action to eliminate root causes, implement corrective actions, and retain documented information of the nature of nonconformities and subsequent actions. The standard does not prescribe nonconformance tracking software, investigation methodologies, or specific forms. Organizations determine the methods appropriate to their operations and the nature of the nonconformities they encounter.

    Control of external providers illustrates the same principle. Clause 8.4 requires organizations to ensure that externally provided processes, products, and services conform to requirements. Organizations must determine and apply criteria for evaluation, selection, monitoring of performance, and re-evaluation of external providers. The standard does not mandate specific supplier audit frequencies, scoring systems, or supply chain visibility platforms. It requires that controls exist and are effective.

    This technology-neutral stance allows ISO 9001 to remain relevant across decades and technological shifts. Organizations in highly regulated sectors such as aerospace, medical devices, or automotive often implement controls that exceed ISO 9001’s basic requirements to meet additional regulatory expectations or customer specifications. In these contexts, ISO 9001 serves as the baseline quality system upon which sector-specific requirements are layered.

    The practical implication is that two organizations, both certified to ISO 9001, may operate very differently. One may rely on manual processes and physical records; another may use fully integrated digital systems with automated workflows. Both can meet the requirements if their respective approaches achieve the intended results: consistent products and services, conformity to requirements, and effective process control.
    An industrial quality control technician is carefully using precision measurement instruments to assess aerospace components, ensuring they meet customer requirements and comply with ISO 9001 quality management standards. This process reflects the commitment to continual improvement and risk management in the quality management system.

    Why ISO 9001 is widely referenced in manufacturing and aerospace

    ISO 9001 certification extends across more than one million organizations certified in over 180 countries. This global adoption reflects the standard’s function as a common baseline for quality expectations in business-to-business relationships.

    Manufacturing organizations work with complex supply chains where consistent quality directly affects production schedules, cost savings, and regulatory compliance. ISO 9001 provides a recognized reference point for supplier quality requirements. Purchasing agreements commonly reference ISO certification as a baseline qualification. Contract language often specifies that suppliers maintain ISO 9001 quality management or equivalent systems. This standardization reduces the burden of supplier qualification by establishing common expectations around documentation, traceability, and process control.

    Several factors contribute to this widespread adoption in manufacturing contexts:

    Factor

    Relevance to Manufacturing

    Process orientation

    Aligns with production systems that depend on repeatable, controlled operations

    Documentation requirements

    Supports traceability and configuration control essential to manufacturing

    Supplier control requirements

    Addresses multi-tier supply chain management common in manufacturing

    Performance evaluation

    Enables data-driven improvements in process efficiency and defect reduction

    Continual improvement focus

    Supports integration with methodologies such as lean manufacturing and Six Sigma

    Global recognition

    Facilitates international trade and supply chain relationships

    For aerospace manufacturing and MRO operations, ISO 9001 serves as the foundation for sector-specific standards. AS9100 incorporates all ISO 9001 requirements while adding controls for product safety, counterfeit part prevention, and configuration management. Regulatory bodies such as the FAA and EASA expect quality systems that address documentation accuracy, traceability, and nonconformance management—areas where ISO 9001’s structure provides an established framework.

    Many organizations in aerospace find that ISO 9001’s process approach aligns with modern production systems. Requirements for documented information, change control, and performance evaluation support integration across ERP, MES, and QMS platforms. The standard’s emphasis on determining and meeting customer requirements maps directly to contract review and requirements flowdown processes common in aerospace programs.

    Industry standards such as AS9100 add aerospace-specific requirements, but the underlying ISO 9001 structure remains. Organizations moving from general manufacturing into aerospace supply chains often find that their existing ISO 9001 certification provides a foundation for AS9100 implementation, though additional controls are invariably required to address sector-specific expectations.

    ISO 9001 in context: links to digital operations and aerospace workflows

    ISO 9001 requirements for documented information, process control, traceability, and change management intersect directly with digital shopfloor and supplier-integration tools in aerospace manufacturing. The standard does not reference specific software, but its requirements describe outcomes that digital operations platforms are designed to support.

    QMS processes for documented information control, for example, require that documents be available at points of use, protected from unintended alterations, and retained as evidence of conformity. Digital work instruction systems address these requirements by providing version-controlled, revision-tracked documents accessible at workstations. Nonconformity logging, corrective actions, and management reviews generate documented information that must be maintained and retained—functions supported by integrated quality management modules within digital platforms.

    Platforms like Connect981 are designed to help aerospace manufacturers and MROs operationalize these requirements within day-to-day workflows. Work instructions, traceability records, defect logs, and audit-ready documentation become part of connected data flows across ERP, MES, QMS, and supplier systems. This integration supports the evidence-based decision making that ISO 9001 requires by making quality data accessible, current, and linked to operational context.

    The standard’s technology-neutral design means ISO 9001 itself does not mandate digital systems. Paper-based approaches remain compliant if they meet requirements for control, accessibility, and retention. In practice, however, aerospace organizations increasingly find that digital operations layers make it easier to demonstrate consistent process control, maintain data integrity across production and supplier networks, and respond to audit inquiries with complete, traceable records.

    ISO 9001 provides a stable reference framework against which aerospace organizations can structure quality governance and digital transformation initiatives. The standard’s requirements define what must be achieved; organizational context, regulatory expectations, and operational complexity determine how those achievements are realized in integrated workflows across factories and suppliers.
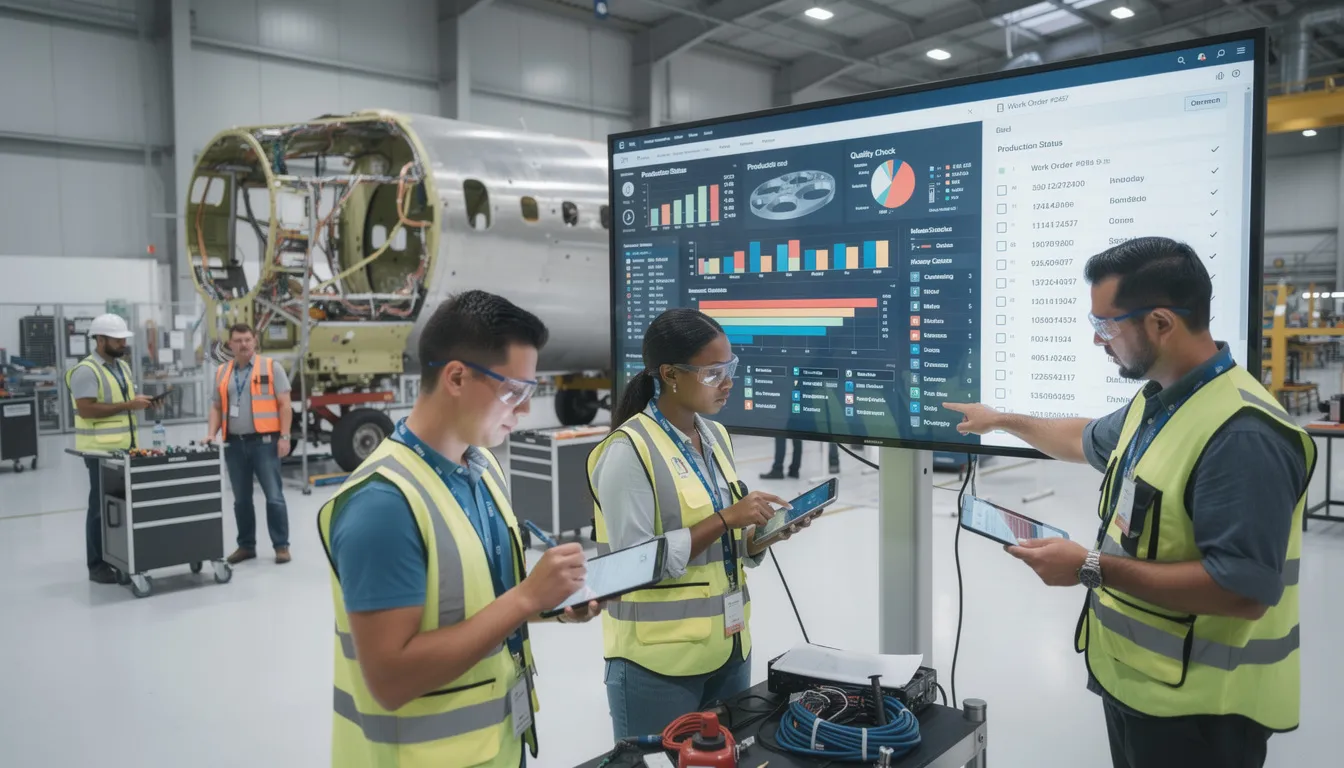
    A group of aerospace workers is actively using digital tablets and screens on the factory floor to track production processes, ensuring adherence to quality management principles and enhancing customer satisfaction. This use of technology supports the implementation of a quality management system aligned with ISO 9001 standards, promoting continual improvement and risk-based thinking in their operations.

    ISO 9001 establishes the baseline for quality management system requirements recognized globally across manufacturing and regulated industries. Understanding what the standard specifies—distinct from the methods organizations use to meet those specifications—enables more effective alignment between quality systems and operational realities. For aerospace manufacturers and MRO operations, ISO 9001 provides the foundation upon which sector-specific requirements, regulatory expectations, and digital transformation strategies are built.

  • IATF 16949 Automotive Quality Standard

    IATF 16949 Automotive Quality Standard

    Overview: What is IATF 16949 and why it matters in 2025

    IATF 16949:2016 is the globally recognized quality management system standard for the automotive industry. As of 2025, it remains the foundational framework that original equipment manufacturers and their suppliers use to ensure consistent quality across passenger cars, commercial vehicles, and other on-road automotive applications. The standard applies to organizations involved in the design, development, production, and servicing of automotive production parts and service parts worldwide.

    The standard was published in October 2016, formally replacing ISO/TS 16949:2009. It is maintained by the International Automotive Task Force, a consortium of major automotive manufacturers and national trade associations, in continuing liaison committee status with the International Organization for Standardization. This strong cooperation between IATF and ISO ensures continued alignment with broader quality management principles while preserving automotive-specific requirements.

    IATF 16949 is not a stand alone document. It must be applied in conjunction with ISO 9001:2015 and follows the same structure established by ISO’s Annex SL framework. Organizations cannot achieve certification to IATF 16949 without simultaneously meeting all ISO 9001 requirements. This relationship means that IATF 16949 functions as an automotive-sector supplement that overlays additional requirements onto the ISO 9001 baseline.

    While Connect981 primarily serves aerospace manufacturing and MRO operations, understanding automotive quality management systems provides valuable context for how structured quality frameworks have developed across safety-critical industries. Many of the themes found in IATF 16949, including traceability, supplier oversight, and rigorous process control, parallel requirements in aerospace standards like AS9100.

    The image depicts an automotive production line showcasing vehicles at various stages of assembly, illustrating the intricate production process within the automotive industry. This scene emphasizes the importance of quality management systems, such as IATF 16949, in ensuring high-quality products and customer satisfaction throughout the automotive supply chain.

    Purpose and intent of the IATF 16949 automotive quality standard

    The central purpose of IATF 16949 is to establish a common, globally harmonized set of quality management system requirements for organizations involved in automotive production and service parts. Before harmonization efforts began, automotive suppliers often faced competing quality requirements from different OEM customers, each with their own certification systems. The IATF standard was originally created to consolidate these expectations into a single framework that serves the entire automotive supply chain.

    The core intent focuses on three interconnected objectives: defect prevention, reduction of variation and waste, and robust process control. Rather than treating quality as an inspection-based activity that catches problems after they occur, IATF 16949 emphasizes preventing defects before they reach the production process. This approach acknowledges that in automotive manufacturing, where a single component failure can cascade into recalls affecting millions of vehicles, prevention is far more cost-effective than correction.

    IATF 16949 aligns with customer specific requirements from major OEMs including General Motors, Ford, Stellantis, Volkswagen Group, BMW, and Daimler Truck, among others. By providing a shared baseline for quality expectations, the standard reduces redundancy for suppliers who would otherwise need to manage multiple competing systems. The standard emphasizes customer satisfaction, risk-based thinking, and continual improvement as foundational principles, while leaving specific implementation approaches to individual organizations based on their context and resources.

    From ISO/TS 16949 to IATF 16949: key changes and replacement history

    IATF 16949:2016 formally replaced the previous technical specification, ISO/TS 16949:2009, with the new standard released in October 2016 and transition deadlines set through 2017 and 2018 by IATF and accreditation bodies. The designation change from “ISO/TS” to “IATF” reflects that the document is now owned and maintained directly by the International Automotive Task Force, though it continues to reference ISO 9001:2015 for its base requirements.

    The transition was driven by several factors. First, ISO 9001:2015 introduced a significantly updated structure based on risk-based thinking, requiring alignment from sector-specific standards. Second, the automotive sector needed to address new technologies, including embedded software in vehicle systems, that were not adequately covered in the previous edition. Third, there was recognition that supplier quality and product safety requirements needed strengthening to reflect the increasing complexity of global automotive supply chains.

    Several high-level areas were strengthened in IATF 16949:2016 compared to its predecessor. Product safety received explicit emphasis, with new requirements for organizations to demonstrate that safety-related products and manufacturing processes are controlled appropriately. Traceability requirements were enhanced to address the need for tracking critical components through complex supply networks. Warranty and field failure analysis expectations were formalized, requiring organizations to establish processes for analyzing field incidents, warranty returns, and customer complaints. The standard also introduced considerations for embedded software in automotive related products, acknowledging that modern vehicles depend increasingly on electronic control systems.

    The first edition of the IATF standard represented an innovative document in how automotive quality requirements would be structured and governed globally. Each subsequent update has reflected changes to the underlying ISO 9001 framework while maintaining the automotive-specific emphasis on defect prevention and waste reduction that defines the IATF approach.

    Relationship between IATF 16949 and ISO 9001

    IATF 16949:2016 is a supplemental automotive QMS standard that must always be used together with ISO 9001:2015. Organizations pursuing certification are evaluated against a combined system, and certificates reflect compliance with both IATF 16949 and the underlying ISO 9001 requirements. There is no option to achieve IATF 16949 certification without meeting ISO 9001 in full.

    The structural relationship follows the ISO 9001:2015 High Level Structure, also known as Annex SL, which organizes management system standards into ten clauses. This same structure appears across multiple ISO standards, enabling organizations to align quality management systems ISO 9001 with environmental management under ISO 14001 and occupational health and safety under ISO 45001. The shared architecture reduces complexity for organizations managing an integrated management system across multiple domains.

    ISO 9001 baseline requirements establish foundational quality management principles including customer focus, leadership engagement, process approach, and evidence-based decision making. The seven quality management principles embedded in ISO 9001 provide the conceptual foundation that IATF 16949 builds upon.

    IATF 16949 automotive additions overlay sector-specific requirements throughout the ten-clause structure. These additions include more detailed control of manufacturing processes, specific requirements for supplier quality management, formalized approaches to product safety, and expectations for automotive-specific tools and methodologies. The automotive requirements do not replace or relax ISO 9001 expectations; they extend them to address the particular risks and operational realities of automotive production.

    This relationship enables straightforward integration with other stakeholders’ management system expectations while maintaining the automotive-specific rigor that OEMs require. Organizations already certified to ISO 9001 have a structural foundation in place, though the automotive-specific additions represent substantial additional requirements that reflect the complexity of the automotive sector.

    Scope and automotive supply chain context

    IATF 16949 applies to organizations involved in manufacturing and servicing automotive production parts, service parts, and accessory parts. This includes direct suppliers to OEMs, as well as organizations throughout the supply chain that provide materials, components, or processing services such as heat treating, plating, or painting. Certification bodies evaluate sites where customer-specified automotive products are manufactured, assembled, or supported.

    The standard focuses specifically on serial production for on-road vehicles, including light vehicles, heavy trucks, and buses. Organizations involved in automotive production at any tier level may pursue certification, though the standard explicitly limits applicability to manufacturers. Contract organizations providing only services, distribution, or activities outside direct production are not eligible for IATF 16949 certification.

    Certification expectations cascade through the automotive supply chain. Major OEMs typically require their Tier 1 suppliers to maintain IATF 16949 certification, and those suppliers in turn expect certification from their Tier 2 and Tier 3 sources. This creates a quality expectation that extends deep into global supplier networks, establishing IATF 16949 as the common language for quality management across geographic and organizational boundaries.

    The global nature of automotive production makes harmonized quality requirements essential. Modern vehicles contain thousands of components sourced from suppliers across North America, Europe, China, Japan, and emerging markets. Just-in-time delivery requirements, distributed manufacturing, and complex logistics create conditions where a quality failure at any point can disrupt production across multiple facilities and geographies. IATF 16949 provides the consistent quality performance expectations necessary to manage these risks across the worldwide automotive supply chain.

    The image depicts a complex scene of global shipping containers stacked at a logistics hub, showcasing the intricacies of the automotive supply chain. This visual representation highlights the importance of quality management systems, such as IATF 16949, in ensuring customer satisfaction and continual improvement in the automotive industry.

    Automotive-specific considerations within IATF 16949

    This section provides a high-level overview of themes where IATF 16949 goes beyond generic ISO 9001 requirements. The focus is on concepts and their significance to the automotive sector, not on methods for achieving compliance.

    IATF 16949 addresses several automotive-relevant topics that reflect the industry’s particular risks and operational demands:

    Theme

    Significance in Automotive Context

    Product Safety

    Vehicles carry passengers; failures create direct safety consequences requiring formalized controls

    Component Traceability

    Recalls may affect millions of units; traceability enables targeted response rather than broad recalls

    Manufacturing Process Change Control

    Process variations directly impact product quality in high-volume production

    Externally Provided Products and Services

    Multi-tier supply chains require consistent quality management across organizational boundaries

    Field Performance Analysis

    Large production volumes generate statistically significant performance data requiring systematic analysis

    The standard acknowledges that automotive organizations commonly use specific tools and practices including Advanced Product Quality Planning, Production Part Approval Process, Failure Mode and Effects Analysis, Measurement Systems Analysis, and Statistical Process Control. While IATF 16949 does not prescribe these specific methodologies, they represent expected practices in most OEM-supplier relationships and support the standard’s emphasis on defect prevention and variation reduction.

    Warranty data and field failure information receive particular attention in IATF 16949. The combination of high production volumes and extended vehicle lifecycles generates substantial performance data that organizations must analyze systematically. Customer feedback loops, including warranty returns and field incidents, provide essential input for continuous improvement and help identify problems that may not appear in manufacturing quality metrics.

    While Connect981 focuses on aerospace and MRO operations, many of these themes parallel requirements in AS9100 and other aerospace standards. Serial-number traceability, supplier oversight, rigorous change control, and systematic nonconformance management appear across both industries, reflecting shared recognition that high quality products in safety-critical applications require structured quality systems.

    High-level structure of IATF 16949:2016

    IATF 16949 follows the ten-clause Annex SL structure established by ISO 9001:2015. This common architecture makes it straightforward for organizations to align multiple management systems and reduces the complexity of maintaining parallel quality, environmental, and safety frameworks.

    The standard’s clause structure provides the organizational framework for automotive QMS requirements:

    Clause 4: Context of the Organization establishes requirements for understanding the organization’s context, including the needs and expectations of customers, suppliers, and other stakeholders. Organizations must define the scope of their quality management system and understand the automotive supply chain context in which they operate.

    Clause 5: Leadership addresses top management responsibility for the quality management system, including establishing quality policy, assigning roles and responsibilities, and demonstrating commitment to customer focus.

    Clause 6: Planning covers quality objectives, actions to address risks and opportunities, and planning for changes. Risk management principles are embedded throughout, reflecting the risk-based thinking introduced in ISO 9001:2015.

    Clause 7: Support addresses resources, competence, awareness, communication, and documented information. This includes requirements for infrastructure, manufacturing environment, and the knowledge necessary for effective quality management.

    Clause 8: Operation contains the most extensive automotive-specific additions, covering operational planning and control, requirements for products and services, design and development, control of externally provided processes, production and service provision, release of products and services, and control of nonconforming outputs.

    Clause 9: Performance Evaluation establishes requirements for monitoring, measurement, analysis, and evaluation, including internal audit and management review. Automotive-specific performance indicators supplement generic ISO 9001 expectations.

    Clause 10: Improvement addresses nonconformity and corrective action, emphasizing defect prevention and continual improvement as ongoing organizational priorities.

    Automotive-specific additions are embedded throughout these clauses rather than appearing in a separate section. This integration means that organizations must understand both the ISO 9001 base requirements and the automotive additions that apply to each clause.

    IATF rules and governance context (including Rules 6th Edition)

    The International Automotive Task Force functions as the consortium responsible for maintaining IATF 16949, associated rules, and oversight of the global certification scheme. The IATF membership includes major automotive manufacturers from North America, Europe, and Asia, along with national trade associations representing automotive suppliers in various regions.

    The IATF Rules documents govern how certification bodies conduct audits, issue certificates, and maintain the impartiality required for credible third-party certification. These rules establish consistent practices across certification bodies worldwide, ensuring that an IATF 16949 certificate represents the same level of demonstrated compliance regardless of which accredited certification body performed the assessment or where in the world the certified site operates.

    The IATF Rules 6th Edition takes effect on January 1, 2025, establishing revised expectations for how IATF 16949 audits and certification processes are managed. These updated rules reflect ongoing refinement of the certification scheme based on experience and feedback from manufacturers, suppliers, and certification bodies. The updates address audit practices, certification requirements, and oversight mechanisms that maintain the integrity of the IATF 16949 certification system.

    These rules are directed primarily at certification bodies and auditors rather than at individual manufacturing sites. The successful implementation of IATF 16949 at a manufacturing organization depends on the organization’s quality management system, while the Rules govern how external parties evaluate and certify that system. A recertification audit follows the same fundamental requirements regardless of Rules edition, though specific procedural details may change.

    Comparing automotive and aerospace quality frameworks

    While IATF 16949 is specific to the automotive sector, aerospace organizations typically follow AS9100, which is also built on ISO 9001’s structure but with aerospace-specific clauses and regulatory considerations. Both standards share the common foundation of ISO 9001 quality management principles, creating conceptual parallels even though the industries face different regulatory environments and customer expectations.

    Quality Theme

    Automotive (IATF 16949)

    Aerospace (AS9100)

    Traceability

    Component-level for recall management

    Serial-number level for airworthiness

    Configuration Management

    Process change control emphasis

    Design and build configuration control

    Supplier Oversight

    Cascading certification expectations

    Flowdown of requirements to supply chain

    Nonconformance Management

    Systematic corrective action

    Root cause analysis and preventive action

    Customer Requirements

    OEM-specific requirements

    Regulatory (FAA, EASA) and customer requirements

    Both frameworks emphasize strong traceability, configuration management, supplier quality oversight, and rigorous management of nonconformities and corrective actions. Advanced change control, production process validation, and field performance feedback loops appear as common themes across both industries, even though the specific standards and regulatory bodies differ.

    Connect981 is built around aerospace use cases, including AS9100 compliance, FAA and EASA regulatory requirements, and the particular demands of MRO operations. The same digital capabilities that support aerospace workflows, such as work instructions, defect logging, serial-number traceability, and supplier collaboration, reflect the maturity seen in highly structured frameworks like IATF 16949. Understanding how automotive quality management has evolved provides useful context for how these principles apply across safety-critical manufacturing sectors.

    The image depicts a precision manufacturing inspection process within a quality-controlled environment, showcasing workers meticulously examining automotive components to ensure compliance with IATF 16949 standards. This scene emphasizes the importance of quality management systems in the automotive industry, highlighting defect prevention and continual improvement for high-quality products.

    Summary: IATF 16949’s role in modern automotive quality management

    IATF 16949:2016 remains the globally recognized automotive quality management standard that supplements ISO 9001:2015 and establishes common expectations across the automotive supply chain. The standard replaced ISO/TS 16949:2009 and brought automotive quality requirements into alignment with modern risk-based thinking while strengthening emphasis on product safety, traceability, and supplier quality management. IATF maintains strong cooperation with ISO through its liaison committee status, ensuring that the automotive framework evolves alongside broader international standard developments.

    The standard’s primary contributions include harmonized quality management system requirements that reduce redundancy for global suppliers, an emphasis on defect prevention rather than detection-based quality approaches, and automotive-specific controls that reflect OEM expectations and applicable customer specific requirements. These elements work together to support customer loyalty by ensuring that vehicles meet quality and safety expectations across the production lifecycle.

    While Connect981 operates primarily in aerospace and MRO environments, understanding IATF 16949 helps frame how advanced quality management and digital traceability have developed across safety-critical manufacturing sectors. The principles of efficiency, waste reduction, and systematic quality control that IATF 16949 embodies are not unique to automotive; they represent baseline concepts for any organization seeking to deliver high quality products in complex production environments.

    Structured standards like IATF 16949 will continue to influence expectations for data integrity, supplier collaboration, and end-to-end quality assurance across industrial value chains. As supply chains become more interconnected and production systems more complex, the harmonized approach that IATF 16949 represents provides a model for how industries can establish common quality language and open new markets while managing the risks inherent in globally distributed manufacturing.

  • Non Conformance in Aerospace: Managing NCRs, Compliance, and Digital Workflows

    Non Conformance in Aerospace: Managing NCRs, Compliance, and Digital Workflows

    Aerospace manufacturing operates under constraints that other industries rarely encounter. When an A320 wing rib arrives machined beyond tolerance limits or a Boeing 777 engine bracket is fabricated from an incorrect alloy, the consequences extend far beyond production delays. These nonconformances directly threaten structural integrity under flight loads, potentially leading to fatigue cracks, certification issues, or catastrophic failure during service.

    Non conformance in aerospace refers to any unplanned deviation where a product, process, or system fails to meet specifications, engineering drawings, regulatory mandates, or contractual obligations. Unlike consumer goods manufacturing, where a nonconforming part might only affect aesthetics or minor functionality, aerospace manufacturing demands absolute precision. Even subtle deviations can cascade into airworthiness certification problems, regulatory groundings, and financial losses measured in billions of dollars.

    Understanding the terminology matters for both operational clarity and audit readiness. Under AS9100D and FAA/EASA frameworks, a nonconformance is an unplanned spec breach, distinct from a defect (an inherent flaw in a part), a deviation (a pre-planned, approved temporary departure from specs), and a concession (formal customer approval to use or release a nonconforming item under controlled conditions). These distinctions shape how aerospace organizations document, disposition, and ultimately close quality issues.

    The Nonconformance Report, or NCR, serves as the primary mechanism for capturing and resolving these issues across aerospace shops, hangars, and supplier facilities. Detection points include First Article Inspection (FAI) under AS9102, in-process checks via coordinate measuring machines (CMM) or non-destructive testing (NDT) on turbine blades, incoming inspection of forgings, and line maintenance during C-checks. This article covers the regulatory framework (AS9100, FAA 14 CFR, EASA Part 21), NCR workflows, root cause analysis, CAPA integration, digital systems, and the cost impact of scrap and rework.

    Aerospace OEMs, Tier 1–3 suppliers, and MROs are increasingly investing in digital nonconformance management platforms like Connect981 to handle the growing complexity of global supply chains, multi-site operations, and regulatory scrutiny. Paper-based systems and fragmented spreadsheets simply cannot keep pace with programs like A350 or F-35, where just-in-time production and remote audits demand real-time visibility and structured documentation.

    The Importance of Non Conformance Management in Aerospace

    The 2018–2020 Boeing 737 MAX crises brought nonconformance management into sharp public focus. Production quality escapes, including nonconforming sensor installations and MCAS software deviations, contributed to two fatal crashes, a 20-month global grounding, over $20 billion in costs, and FAA findings of 178 production-related nonconformances. Similarly, Boeing 787 fuselage nonconformances from 2010–2022, such as shim gaps and fastener issues at Spirit AeroSystems, triggered inventory builds exceeding 500 aircraft and $15 billion in charges.

    Nonconformances occur across the entire product lifecycle:

    • Design phase: Model mismatches in CAD data leading to manufacturing errors
    • Fabrication: Composite porosity in layups, dimensional variations in machined parts
    • Assembly: Misdrilled holes in wing spars, incorrect torque on fasteners
    • Testing: Hydraulic actuator failures, pressure test anomalies
    • Flight line: Pylon fitting mismatches, wiring discrepancies
    • MRO: Corrosion exceeding allowable limits on landing gear during heavy checks

    The risk spectrum ranges from cosmetic issues like paint adhesion problems to critical structural nonconformances affecting airworthiness. A burr on a bracket interior might be classified as minor with no safety impact. A titanium bulkhead crack affecting load paths represents a critical, safety-of-flight issue requiring immediate regulatory notification.

    Operational consequences hit production schedules hard. Line stoppages occur when nonconforming parts cannot be cleared. Aircraft on Ground (AOG) events can cost $10,000–$50,000 per hour for widebody aircraft. Rework bays fill up, drawing resources from planned production. Customer penalties add up, as evidenced by Boeing’s $2.5 billion 737 MAX settlement, including a $243.6 million victim fund.

    Best-in-class aerospace organizations foster a no-blame reporting culture aligned with AS9100 clause 10.2.1. They recognize that every NCR represents an opportunity for continuous improvement. Organizations that encourage reporting every nonconformance, rather than hiding defects, consistently achieve lower defect rates over time. Some suppliers using NCR data for kaizen events have reduced defect rates by 30–50%.

    Effective nonconformance management requires tight integration across functions. Quality logs the NCR. Engineering evaluates disposition options. Production implements containment. Supply chain manages vendor SCARs. MRO provides in-service feedback loops. Siloed responses create gaps where issues recur or escalate.

    An aerospace technician is meticulously inspecting an aircraft wing component, ensuring compliance with quality management systems and safety standards in the aerospace industry. This detailed examination plays a critical role in identifying any non conformances to maintain high product quality and operational excellence.

    Regulatory and Standards Requirements for Aerospace Nonconformance

    Aerospace nonconformance control operates under multiple regulatory layers. International standards, aviation authorities, prime contractor specifications, and customer contracts all impose requirements that quality teams must satisfy simultaneously. Understanding these layers is essential for maintaining compliance across programs and customers.

    AS9100D Requirements

    AS9100D (2016 revision) provides the quality management system foundation for aerospace organizations. Clause 8.7 specifically addresses control of nonconforming outputs, requiring:

    • Identification through tags, labels, or electronic flags
    • Segregation in quarantine areas to prevent unintended use
    • Disposition evaluation with documented rationale
    • Approval authority for use-as-is, rework, or repair decisions
    • Records retention for double the part life or 20 years, whichever is longer

    Clause 10.2 links nonconformity management to corrective action, requiring organizations to react to nonconformances, evaluate the need for action to eliminate root causes, implement actions, review effectiveness, and update risks and opportunities as needed.

    FAA and EASA Expectations

    FAA requirements under 14 CFR Part 21 mandate that design and production organizations identify, document, and disposition nonconforming outputs to prevent unintended use. Part 145 repair stations must ensure airworthy releases via Form 8130-3, with clear processes for handling nonconforming material discovered during maintenance.

    EASA Part 21 Subpart G and Part 145 require equivalent controls, including segregation and Material Review Board (MRB) evaluation. Concessions affecting type design require DOA/DER approvals, adding complexity when dispositioning nonconformances on certified products.

    OEM-Specific Requirements

    Primes layer additional requirements through supplier quality documents:

    • Boeing D6-82479 requires NCRs within 24 hours for Tier 1 suppliers
    • Airbus GRAMS mandates FAI NCRs with 3D scan data
    • Rolls-Royce SABRe uses risk-based classification tied to engine health monitoring

    These requirements flow down through supply chain contracts, creating a web of obligations that suppliers must track and satisfy.

    Documentation and Traceability

    Regulatory compliance demands robust traceability. Serial and lot tracking per AS9100 clause 8.5.4 must connect parts to their manufacturing records. Digital signatures must meet standards equivalent to 21 CFR Part 11. Configuration baselines must align with Illustrated Parts Catalogs (IPCs). Critical structure records like engine disks require retention beyond 10 years.

    Post-2020 FAA and EASA audits flagged paper NCRs in 40% of findings across supply chains. This trend drives digital mandates, as reflected in FAA Order 8120.22 for production approval holders. Primes now audit for integrated QMS/MES/PLM linkages, rejecting siloed Excel tracking as insufficient for regulatory requirements.

    Core Aerospace NCR Workflow: From Detection to Disposition

    A clear, repeatable NCR workflow ensures that nonconformances are captured, evaluated, and resolved with full traceability. The process varies by organization but follows a consistent structure across aerospace manufacturing and MRO operations.

    Detection and Initiation

    Nonconformances surface at multiple points:

    • CMM inspection revealing turbine blade airfoil deviations during FAI
    • NDT ultrasonic testing identifying subsurface indications on landing gear struts
    • Borescope inspection finding erosion beyond limits during heavy maintenance
    • Receiving inspection detecting dimensional nonconformances on incoming forgings
    • Assembly line operators identifying fit issues during installation

    Certified inspectors, operators, or field service representatives can initiate NCRs. The key is ensuring that anyone who identifies a potential nonconformance has a clear path to document it without barriers.

    Documentation Requirements

    An aerospace NCR must capture sufficient detail for evaluation and future reference:

    • Part number, serial number, and lot number
    • Aircraft tail number (for MRO applications)
    • Drawing number and revision level
    • Specification limits and measured results (e.g., “0.005 inch oversize hole”)
    • Photos, NDT reports, and other objective evidence
    • Reference to traveler, route card, or work order step
    • Date, time, and initiator identification

    This structured documentation supports both immediate disposition decisions and long-term trend analysis.

    Containment and Segregation

    Once an NCR is opened, containment prevents the nonconforming item from progressing:

    • Physical red-tags placed on parts
    • Movement to quarantine cages or designated hold areas
    • Electronic holds in ERP blocking MES routing and shipment
    • Notification to downstream operations and MRB members
    • Work order holds preventing installation on other assemblies

    Electronic systems can auto-notify MRB members and trigger containment actions simultaneously, reducing response time compared to paper-based processes.

    Evaluation and Classification

    MRB evaluation classifies the nonconformance based on impact:

    • Minor: Cosmetic issues with no effect on fit, function, or safety
    • Major: Affects fit or function but manageable through disposition, no immediate safety impact
    • Critical: Safety of flight consideration, requires immediate regulatory notification

    Critical nonconformances involving airworthiness must be escalated to FAA or EASA within prescribed timeframes. Classification drives the rigor of the disposition process and the level of approval authority required.

    Disposition Options

    Aerospace MRBs typically select from these disposition categories:

    Disposition

    Description

    When Used

    Scrap

    Destroy and recycle material

    Uneconomic to repair or safety risk precludes rework

    Rework

    Bring part back to drawing requirements

    Feasible within process capability and cost constraints

    Repair

    Accept with approved engineering instruction

    Cannot achieve original spec but meets functional requirements

    Use-as-is

    Accept via concession or deviation

    Customer/DER approved, no safety impact

    Return to vendor

    Send back to supplier

    Supplier-caused defect, warranty claim

    Downgrade

    Use in non-flight application

    Part acceptable for ground support or spares

    Each disposition requires appropriate approval authority. Scrap decisions on critical components often require design authority concurrence. Use-as-is dispositions affecting type design need DER/DOA involvement.

    Verification and Closure

    Final steps ensure the nonconformance is fully resolved:

    • Re-inspection confirms rework or repair meets requirements
    • Updated routing reflects disposition actions
    • Configuration records updated for aircraft or assembly
    • Final digital sign-off with time/date stamps
    • Effectiveness check scheduled if linked to CAPA

    Complete closure creates an audit-ready record demonstrating that the nonconformance was effectively managed.

    Nonconformance vs Deviation, Concession, and Scrap in Aerospace

    Aerospace teams must clearly distinguish between related but distinct terms. Audit findings frequently cite improper classification, and operational confusion can lead to safety risks or regulatory violations.

    Nonconformance Defined

    A nonconformance is an unplanned failure to meet drawing, specification, or contract requirements. Examples include:

    • Holes drilled oversize in a 737 fuselage panel, risking corrosion propagation
    • Surface roughness exceeding callout on a hydraulic cylinder bore
    • Incorrect heat treatment on a landing gear component
    • Missing NDT inspection on a critical weld

    The defining characteristic is that the condition was not planned or anticipated. Something went wrong during production or maintenance.

    Deviation and Concession

    A deviation or concession represents a planned or accepted departure from requirements, approved before use or continued work. For example:

    • Substituting 7075 aluminum for 2024 on a test fixture with OEM waiver limiting cycles
    • Accepting a cosmetic surface condition outside normal limits for a prototype
    • Using an alternative fastener per engineering evaluation

    Concessions typically document the technical rationale, limitations on use, and any follow-up actions required. They represent controlled risk acceptance, not quality escapes.

    Scrap Criteria

    Scrap is the appropriate disposition when a part cannot be economically or safely reworked or repaired. Criteria often include:

    • Rotating engine parts with material inclusions per OEM specifications
    • Structural components with cracks exceeding blend limits
    • Parts where rework would compromise fatigue life or damage tolerance
    • Material contamination that cannot be removed

    Safety-critical components like titanium fan blades with inclusions typically mandate scrap and material recycling. The cost of scrap is significant, but the alternative risks far outweigh material losses.

    Relationship Between NCRs and Concessions

    An NCR typically captures the issue. A separate deviation or concession record documents the decision to use-as-is or repair under specific limits. The NCR remains part of the quality record, linked to the concession that authorized continued use.

    Mislabeling creates risks. Treating a nonconformance as a deviation after the fact bypasses proper root cause analysis and corrective action requirements under AS9100. Using concessions as shortcuts to avoid RCA leads to recurring issues. The Spirit AeroSystems 787 shim problems, which triggered FAA special audits, illustrate how such shortcuts compound over time.

    Root Cause Analysis and CAPA Integration for Aerospace NCRs

    NCR data becomes valuable when it drives improvement. Aerospace quality management systems under AS9100 require rigorous root cause analysis and linkage to corrective and preventive actions. This integration distinguishes mature organizations from those simply processing paperwork.

    Common RCA Tools

    Aerospace organizations deploy several root cause analysis methods depending on the complexity of the nonconformance:

    5 Whys: Sequential questioning to reach underlying factors. For example, peeling rivets trace to operator error, then to training gap, then to absence of refresher training program.

    Ishikawa Diagrams: Fishbone analysis examining man, method, machine, material, measurement, and environment factors for issues like rivet line misalignment.

    Fault Tree Analysis: Logical decomposition for complex failures like avionics intermittents or hydraulic system anomalies.

    FMEA: Failure Mode and Effects Analysis for recurring assembly defects on programs like A220 or Embraer E2, predicting risk priority numbers.

    Cross-Functional Investigation

    Effective RCA requires input beyond the quality control department:

    • Quality engineers lead documentation and process
    • Manufacturing engineering evaluates process capability
    • Design engineering assesses specification adequacy
    • Supply chain investigates vendor-related causes
    • MRO line leads provide in-service failure context
    • Customer representatives participate when required by contract

    This cross-functional approach prevents narrow conclusions that miss systemic issues.

    Translating RCA to CAPA

    RCA outcomes must drive concrete corrective and preventive actions:

    • Process FMEAs revised to reflect new risk understanding
    • Digital work instructions updated in MES with specific guidance
    • Poke-yoke tooling added to prevent recurrence
    • Supplier corrective action requests (SCARs) issued with 30-day closure targets
    • Training modules deployed addressing identified gaps

    The goal is eliminating the root cause, not just addressing the symptom.

    Traceability Requirements

    Auditors expect clear linkage between NCR, RCA, and CAPA records:

    • Unique IDs connecting related documents
    • Hyperlinks in digital systems enabling direct navigation
    • Evidence of effectiveness checks after 3–6 months
    • Closure verification demonstrating sustained improvement

    Example: Composite Layup CAPA

    In 2023, a supplier supporting A220 production experienced repeated nonconformances on composite plies. Using 8D methodology, the cross-functional team traced the issue to cure cycle variations. The CAPA introduced automated ply counters and temperature profiling during cure. The result was a 65% reduction in defect rates per internal metrics.

    Primes and authorities review this NCR-RCA-CAPA chain to assess quality management system maturity. Boeing’s QPM scoring, for instance, evaluates suppliers on their ability to demonstrate this closed-loop process.

    The image depicts a busy manufacturing floor in the aerospace industry, where workers are engaged in quality inspection of composite parts, ensuring adherence to quality management systems and regulatory compliance. The scene highlights the importance of operational excellence and continuous improvement initiatives in maintaining high-quality outcomes and addressing any non-conformance issues.

    Digital Nonconformance Systems and Connected Aerospace Operations

    The shift from paper travelers and email-based MRB logs to integrated digital NCR workflows accelerated dramatically after 2020. Remote audits, global supply disruptions, and increased regulatory scrutiny exposed the limitations of manual processes.

    Core Capabilities of Modern Systems

    Aerospace digital NCR systems must deliver:

    • Electronic forms with validation and required fields
    • Role-based approval workflows matching MRB authority structures
    • Attachment of CMM data, NDT reports, and photos
    • Automatic notifications to stakeholders
    • Integration with ERP for inventory holds
    • Integration with MES for work order routing
    • Integration with PLM for configuration management
    • Audit trail with digital signatures and timestamps

    These capabilities replace fragmented spreadsheets and email chains with structured, auditable workflows.

    Connect981 as a Unified Operations Layer

    Connect981 serves as an aerospace-native platform connecting NCRs to related operational data. The platform links nonconformance management to digital work instructions, supplier data, serial and lot traceability, and shopfloor execution records across OEM and MRO environments.

    This integration means that when an NCR is opened, relevant context is immediately available: the work instruction revision in use, the operator who performed the task, the incoming inspection results for materials, and the configuration baseline for the assembly.

    Multi-Site and Multi-Supplier Visibility

    Large aerospace programs require standardization across facilities and suppliers. Connect981 enables:

    • Standardized NCR templates used across different plants
    • Shared dashboards showing trends by program, part family, or supplier
    • Tier 2 and Tier 3 suppliers using consistent processes
    • Real-time visibility for program quality managers

    This visibility supports early detection of emerging issues before they propagate through the supply chain.

    Zero and Low-Code Workflow Configuration

    Traditional MES implementations require extensive IT involvement to model approval workflows. Connect981’s zero and low-code tools allow quality and manufacturing engineers to configure complex MRB and concession approval routes without heavy IT projects.

    This flexibility matters because NCR workflows vary by program, customer, and part criticality. A concession on a flight-critical structure requires different approvals than a cosmetic deviation on a ground support component.

    AI-Assisted Analytics

    Historical NCR and process data enable predictive capabilities:

    • Identifying likely root causes based on similar past nonconformances
    • Flagging high-risk work orders before issues reach final assembly
    • Suggesting investigation paths for manufacturing engineers
    • Detecting emerging supplier trends before they trigger production impacts

    These capabilities move quality management from reactive to proactive.

    MRO Deployment Example

    A 2025 MRO deployment illustrates the operational impact. The organization used Connect981 to cut NCR processing time from days to hours by automating routing between hangar technicians, engineering disposition, and customer representatives. This speed prevented AOG events on 787 engine maintenance and improved customer satisfaction through faster turnaround.

    Quest Global’s implementation of Connect981’s root cause and corrective action workflows yielded 3x build rates and $10 million in annual savings, demonstrating that digital transformation in quality management delivers measurable operational efficiency gains.

    Supplier NCR Management and Multi-Tier Aerospace Supply Chains

    Large aerospace programs depend on extensive supplier networks. The A320neo program involves over 2,000 vendors. A single supplier nonconformance can ground aircraft or stall final assembly lines. Managing supplier quality issues requires structured processes and clear information flow.

    OEM and Tier 1 Supplier NCR Management

    When nonconformances trace to supplier-provided material or components, OEMs and Tier 1s typically:

    • Raise a supplier NCR documenting the defect
    • Issue a Supplier Corrective Action Request (SCAR)
    • Require stock sweeps to contain suspect material
    • Demand root cause analysis with specified due dates
    • Track cost recovery through chargebacks

    Critical part nonconformances can trigger chargebacks exceeding $100,000, creating significant financial incentive for supplier quality performance.

    Information Flow Requirements

    Effective supplier NCR management requires clear data exchange:

    Information Element

    Direction

    Purpose

    Defect details and photos

    Buyer to supplier

    Define the issue clearly

    Suspected root cause

    Supplier to buyer

    Demonstrate investigation

    Containment actions

    Supplier to buyer

    Show immediate response

    Stock sweep results

    Supplier to buyer

    Confirm scope of problem

    Corrective action plan

    Supplier to buyer

    Define permanent fix

    Effectiveness evidence

    Supplier to buyer

    Prove sustained improvement

    Fragmented Systems Challenge

    The reality across aerospace supply chains is system fragmentation. OEMs use SAP or Oracle ERP with custom QMS modules. Tier 1 suppliers might use different ERP systems. Tier 2 and Tier 3 suppliers often rely on spreadsheets or basic quality databases.

    This fragmentation delays NCR resolution by 2–4x compared to integrated approaches. Data re-entry introduces errors. Audit trails become difficult to reconstruct.

    Connect981 Supplier Integration

    Connect981’s supplier integration capabilities create a shared layer where suppliers can receive, respond to, and close NCR-related actions without needing access to the OEM’s core ERP. This approach:

    • Standardizes NCR and SCAR templates across the supply chain
    • Provides suppliers with clear task lists and due dates
    • Captures responses and evidence in a single system of record
    • Generates audit-ready reports for AS9100 or customer reviews

    A 2024 case demonstrated the impact: a precision machining supplier’s recurring dimensional nonconformances dropped 50% after implementing standardized digital NCR and SCAR workflows. The key was visibility into trends and accountability for closure.

    Audit and Compliance Benefits

    Digital supplier NCR management provides clear trails showing:

    • When suppliers were notified of nonconformances
    • How suppliers responded and what actions they took
    • Evidence that effectiveness checks were completed
    • Trend data supporting supplier performance ratings

    Auditors reviewing the supply chain look for this documentation. Organizations that can demonstrate robust quality management systems for supplier oversight consistently achieve better audit results.

    Cost, Scrap, and Rework Impact of Aerospace Nonconformances

    Nonconformances carry significant financial consequences. Understanding these costs drives investment in prevention and enables informed disposition decisions.

    Direct Cost Categories

    Cost Element

    Typical Range

    Notes

    Scrap (titanium bulkhead)

    $50K–$200K

    Material cost plus machining investment

    Rework labor

    100–500 hours at $150/hr burdened

    Depends on complexity

    MRB evaluation

    20–40 hours per meeting

    Engineering and quality time

    Takt time disruption

    $1M+/day on programs like F-35

    Line stoppages cascade

    AOG events

    $20K/hr for widebodies

    Airline operational impact

    Customer penalties

    1–5% contract value

    Delivery delay liquidated damages

    Industry Examples

    The 2023–2024 fan case supply chain constraints illustrate systemic cost impact. Delivery delays on these critical engine components cost the aerospace industry an estimated $500 million industry-wide, with production rates constrained well below demand.

    Suppliers with high nonconformance rates experience cost of poor quality (COPQ) reaching 15–25% of revenue. This includes not just direct scrap and rework but also expediting costs, inspection overhead, and customer management burden.

    Using NCR Data for COPQ Analysis

    Digital NCR systems enable organizations to calculate COPQ by program and supplier:

    • Aggregate scrap and rework costs by part number
    • Identify suppliers driving disproportionate quality costs
    • Quantify the return on process improvement investments
    • Prioritize where to deploy automation or additional inspection

    Indirect Impacts

    Beyond direct costs, nonconformances create indirect financial exposure:

    • Missed slots on final assembly lines requiring schedule rework
    • Airline AOG events driving MRO nonconformances
    • Reputational damage leading to increased oversight and audit frequency
    • Loss of future contract opportunities

    Digital Platforms Reduce Costs

    Connect981 reduces nonconformance costs through several mechanisms:

    • Shortening NCR cycle time by 50–80%
    • Preventing repeat defects through better RCA visibility
    • Enabling early detection through real-time dashboards
    • Linking NCR trends to WIP data for predictive intervention

    A 2024 deployment demonstrated the impact: an aerospace manufacturer reduced scrap rates on composite panels by 35% after implementing standardized digital NCR workflows and visual dashboards. The visibility enabled manufacturing engineering to identify process drift before it generated scrap.

    The image depicts a modern aerospace manufacturing facility featuring digital displays that showcase production metrics, emphasizing operational efficiency and quality management systems. This environment reflects the aerospace industry's commitment to continuous improvement and regulatory compliance through innovative solutions and robust quality control measures.

    Future of Nonconformance Management in Aerospace

    Through 2030, nonconformance management will evolve significantly as digital transformation reshapes aerospace operations.

    Industry 4.0 Integration

    The “digital thread” connecting design, production, and MRO data will mature. Model-based definition (MBD) will enable simulation of tolerance stack-ups before manufacturing, predicting potential nonconformances during design. Digital twins will track actual versus designed configurations throughout product life. Digital product passports will provide lifecycle configuration visibility for major assemblies.

    Aviation Authority Expectations

    Regulators will continue tightening oversight of digital quality systems. FAA’s 2025+ digital mandates will require production approval holders to demonstrate integrated, auditable NCR workflows. Paper-based systems will increasingly fail to meet regulatory requirements for traceability and configuration control.

    AI and Predictive Analytics

    Machine learning applied to historical NCR, process, and sensor data will flag at-risk operations before visible nonconformances emerge. Early implementations show 80% accuracy in predicting certain defect types like alloy mix-ups. Complex assemblies and engines, where the cost of nonconformance is highest, will see the greatest investment in predictive capabilities.

    Space Technology and Defense Systems

    Emerging programs in space technology and defense systems will demand even more rigorous nonconformance management. These applications combine the quality standards of commercial aerospace with additional security and performance requirements, making integrated digital workflows essential.

    Connect981’s Role

    Connect981 positions aerospace organizations for this future as a configurable, aerospace-specific platform that links NCRs, CAPA, production data, and supplier information into a single operational view. The platform’s zero and low-code flexibility allows organizations to adapt workflows as requirements evolve without waiting for custom development.

    Organizations that invest now in digital nonconformance management build the foundation for continuous improvement and operational excellence as the industry advances toward fully connected operations.

    For quality leaders, operations managers, and MRO directors ready to transform their nonconformance management, Connect981 offers a practical path forward. The platform delivers aerospace-native NCR workflows, supplier integration, and analytics without the complexity of traditional MES replacements.

    Request a Connect981 demo to see digital NCR workflows in action and explore how your organization can reduce cycle time, prevent repeat defects, and satisfy regulatory requirements with a unified operations layer built for aerospace realities.

  • Aerospace NCR Process: From Non Conformance Detection to Verified Closure

    Aerospace NCR Process: From Non Conformance Detection to Verified Closure

    Aerospace teams do not raise an NCR because paperwork is convenient. They raise it because a deviation has appeared in a system where product quality, airworthiness, schedule, and regulatory compliance are tied together. A non conformance report ncr is the controlled mechanism for making that deviation visible, contained, investigated, and effectively resolved.

    This guide explains the aerospace ncr process from detection through containment, MRB, CAPA handoff, root cause analysis, and verified closure. It is written from Connect981’s perspective as an aerospace operations platform that digitizes NCR workflows across factories, MRO lines, and suppliers.

    Overview of the Aerospace NCR Process Workflow

    A Nonconformance Report (NCR) is a controlled quality record used to formally document, investigate, and resolve nonconformities identified during any phase of the product or service lifecycle. In aerospace manufacturing and MRO, the non conformance report is part of the quality management system and is central to meeting AS9100, FAA, EASA, OEM, and customer requirements. The aerospace industry requires strict adherence to quality standards to ensure regulatory compliance and airworthiness certifications.

    The lifecycle of an aerospace NCR includes identification, segregation, documentation, evaluation, and disposition of non-conforming parts. The typical nonconformance report process follows a structured workflow that begins with detection and initiation by QA, production, or inspection teams, followed by documentation, containment measures, assessment, investigation, and closure. Quality standards, such as AS9100 for aerospace, require organizations to manage nonconformities and take corrective actions to ensure compliance and continuous improvement.

    At a practical level, what happens after an NCR is raised is straightforward: the item is controlled, the risk is classified, relevant stakeholders are notified, MRB is involved when required, corrective and preventive actions are assigned, objective evidence is verified, and the audit trail is closed. Immediate containment means physical and digital action on the shopfloor to stop non conforming products from moving forward. MRB gets involved for major non conformance, design deviation, certified configuration, or flight safety concerns. CAPA should start when the issue is major, recurring, customer-facing, or systemic. Closure timing should be governed by severity, due dates, aging reports, and quality manager escalation.

    An aerospace technician is meticulously inspecting a machined aircraft component on a clean shop floor, ensuring it meets established quality standards and regulatory compliance. This inspection is a crucial part of the quality management system, aimed at identifying any non conformances and implementing corrective and preventive actions to maintain high product quality.

    What Is a Non Conformance in Aerospace Operations?

    Aerospace non conformance is any deviation from design data, process specification, regulatory requirement, or customer contract. It can be an Airbus A350 frame misdrill, a missed torque spec on a CFM56 fastener, incomplete maintenance sign-off on a 737 landing gear overhaul, or any condition where the work does not meet specified requirements. NCRs are essential for documenting deviations from approved specifications, procedures, or regulatory requirements, which is critical for maintaining quality standards in aerospace manufacturing.

    Non conformance usually falls into three categories:

    • Product non conformance: dimensional failures, wrong material, incorrect configuration, damaged parts, or nonconforming heat treatment.
    • Process non conformance: unapproved sequence, skipped inspection, expired calibration, missed cure parameter, or unauthorized repair method.
    • Documentation non conformance: missing EASA Form 1, incomplete FAA Form 8130-3, outdated work instruction revision, weak document control, or missing sign-off.

    Organizations should categorize non-conformances as minor or major to prioritize corrective actions effectively, ensuring that minor issues are addressed promptly to prevent them from escalating into major problems.

    • Minor non conformance: paint blemish not affecting corrosion protection, reworkable edge break, label misalignment, or documentation typo with no airworthiness impact.
    • Major non conformance: primary structure out of tolerance, missing required inspection, wrong alloy or heat treat on load-bearing parts, or work performed to the wrong drawing revision.
    • Safety-critical non conformance: crack in flight-critical hardware, unapproved repair on certified structure, or any issue that may compromise quality and safety standards.

    A documented process for identifying non conformance is required under AS9100 expectations. In the aerospace sector, compliance with AS9100 requires organizations to implement non-conformance reporting procedures to address any deviations from established quality standards and regulatory requirements. Regulatory requirements for non-conformance reporting are defined in international standards such as ISO 9001, AS9100 for aerospace, IATF 16949 for automotive, and FDA regulations for healthcare and medical devices. Non-conformance reporting procedures are mandated by various regulations to ensure that organizations consistently identify, document, and resolve deviations from quality standards, thereby maintaining compliance and product safety. In other sectors, including construction projects, NCR terminology is also used, but aerospace risk, traceability, and airworthiness requirements are materially higher.

    Step 1 – Detect and Record the Non Conformance

    The ncr process begins the moment anyone identifies a deviation. That may happen during first article inspection, in-process inspection, supplier receiving, line maintenance, heavy check, customer complaints about delivered hardware, internal audits, or regulator findings from FAA and EASA oversight. Quality assurance and quality control teams need a clear route to document non conformities without waiting for informal approval.

    Typical detection sources include CMM inspection failures, NDT rejects on structural components, torque audits, shopfloor operator observations, reliability program field events, and inspection data from MRO teardown. An effective non conformance report should capture the key elements at creation: date and time, facility, work center, work order or tail number, part number, serial number, batch, drawing or specification reference, detailed description, severity estimate, immediate status, applicable requirements, and an impact assessment to identify all potentially affected items. Effective non-conformance reporting requires clear documentation of the non-conformance, including a description of the issue, the applicable requirements, and the impact assessment to evaluate potentially affected items.

    Operators and inspectors must identify non conformance and open the NCR immediately. Quality engineers validate the finding, confirm proper documentation, and ensure the record enters a controlled NCR log. With Connect981, the NCR can be raised directly from a work order or inspection step using tablets or terminals. The platform pulls live part numbers, revision-controlled instructions, process records, and quality data so teams avoid rekeying errors and maintain instant traceability.

    Step 2 – Immediate Containment and Segregation

    Immediate containment is the set of actions taken within hours of detection to prevent further use of nonconforming parts, processes, or documents while the investigation proceeds. The NCR process is critical to maintaining flight safety and regulatory compliance in the aerospace sector because it ensures defective components never make it onto an aircraft, thereby preventing catastrophic failures.

    Containment includes tagging suspect parts, moving them to a quarantined MRB area, applying electronic holds in MES or ERP, freezing affected serial numbers and lots, and stopping use of an out-of-tolerance fixture or expired adhesive batch. Physical segregation of non-conforming parts prevents contamination of the aircraft assembly line and protects the production process from silent propagation of defects.

    The image shows aerospace parts arranged on a segregated inspection bench, with technicians actively engaged nearby, ensuring compliance with established quality standards and conducting thorough inspections as part of the quality management system. This setting emphasizes the importance of quality assurance and the non conformance reporting process in maintaining high safety and quality standards in aerospace manufacturing.

    Good containment also brackets the impact. Teams check previous and subsequent serial numbers, adjacent lots, recent jobs on the same tooling, and maintenance tasks on the same aircraft system. Production supervisors authorize stop-work, quality ensures physical and digital segregation, planning adjusts routing or schedules, and supply chain is notified if supplier material is involved. Connect981 supports this with real-time status flags, automated alerts to MRB and planners, and an audit trail showing who applied each hold and when.

    Step 3 – Evaluate, Classify, and Decide on MRB Involvement

    Once contained, the non conformance is evaluated for risk, scope, regulatory impact, and customer exposure. This classification drives risk management, resource allocation, and the path to disposition.

    Minor non conformance may include cosmetic paint defects not affecting corrosion protection, reworkable edge breaks, or documentation errors with no airworthiness impact. Major non conformance includes primary structure out of tolerance, missing required inspection, incorrect material, or wrong heat treatment. The phrase major non matters operationally because it usually changes approval authority and timing expectations.

    MRB should get involved when there is any major non conformance, design deviation request, repeated minor issue indicating systemic failure, certified configuration impact, airworthiness exposure, or contract flight safety clause. A Material Review Board (MRB) analyzes issues related to non-conforming parts and decides their fate based on defined paths: scrap, rework, repair, or use as-is. MRB membership typically includes the quality manager, design engineering, stress or structures engineering, manufacturing engineering, operations, and sometimes customer or regulatory representatives.

    A practical example is an A320 wing panel with undersized fastener holes. MRB may decide to scrap the panel, rework with oversized fasteners, repair under an approved engineering scheme, or use as-is with a design authority concession. Connect981 can route NCRs automatically to the correct MRB group by part family, program, supplier, or customer, then enforce electronic signatures for AS9100, FAA, and OEM audit readiness. AS9100D requirements for control of nonconforming outputs are commonly tied to clause 8.7 and corrective action expectations under clause 10.2, as summarized by AS9100 implementation guidance.

    Step 4 – Define Disposition and Handoff to CAPA

    MRB or quality leadership must formally decide disposition. Standard aerospace dispositions are:

    • Scrap: remove the item from usable inventory, update serial trace, and prevent accidental reinstatement.
    • Rework to print: return the part to specified requirements using approved instructions, followed by re-inspection.
    • Repair: apply an engineering-approved repair scheme with stress, design, or airworthiness sign-off where required.
    • Use-as-is: accept the condition with risk justification, concession, and customer approval where required.

    CAPA should start when the issue is a major non conformance, repeated minor non conformance above threshold, tied to customer complaints, linked to field reliability, found by regulator audit, or requiring design concession or notification. The NCR owner, often a quality engineer, retains ownership of the non conformance record. The CAPA owner, often manufacturing engineering, supplier quality, or maintenance engineering, owns systemic corrective and preventive measures.

    The handoff must preserve traceability between the NCR, corrective action, corrective and preventive actions, corrective and preventative actions, and preventive actions. Connect981 links NCR and CAPA workflows through the same data model, shared part and serial identifiers, aircraft identifiers, and dashboards showing which NCRs have open CAPA actions versus those cleared for closure. This prevents premature closure and supports complaint handling when customer-facing issues are involved.

    Step 5 – Root Cause Investigation and Corrective Actions

    For major non conformance and recurring issues, investigation must go beyond “operator error.” Root cause analysis is a structured investigation phase used to determine the underlying cause or combination of causes that led to a nonconformance, ensuring that corrective actions address the root cause to prevent recurrence. RCA may involve cross-functional input from QA, engineering, production, and supply chain, and is performed using validated methodologies like the 5 Whys technique or Ishikawa fishbone diagram.

    Typical aerospace RCA examples include 5 Whys on a mis-routed hose installation, fishbone analysis of repeated NDT failures on titanium forgings, fault tree analysis for a flight control component defect, and review of PFMEA and process control plans. The investigation should collect machine programs, revision history, calibration records, batch and heat numbers, technician training and certification records, environmental conditions, cure oven profiles, humidity data for bonding, and change history for drawings and work instructions.

    Effective corrective actions may include updating work instructions, adding visual aids, tightening inspection at critical control points, revising torque or cure parameters, retraining and requalifying technicians, updating supplier control plans, or modifying fixtures. The objective of root cause analysis is not only to identify the immediate cause of a nonconformance but also to uncover additional preventive actions for similar processes or areas to avoid future occurrences. Teams must implement corrective actions with due dates, owners, and evidence, not just write a corrective action statement. Connect981 can provide AI-assisted root cause suggestions based on historical NCR patterns, then automatically assign tasks so teams implement corrective and preventive measures with due-date tracking.

    Step 6 – Verification, Closure Criteria, and Timing Discipline

    NCR closure in aerospace is not a checkbox. Teams must verify that corrective actions were implemented, validated for effectiveness, and that affected hardware, paperwork, and systems were updated before closure. Best practices for closing a Non-Conformance Report (NCR) include verifying corrective actions, validating their effectiveness, documenting closure details, obtaining necessary approvals, and archiving the report for future reference.

    Closure criteria should include passing re-inspection or re-test data, updated drawings and work instructions released under configuration control, completed training records, relevant documentation attached, customer approvals where required, and confirmation that CAPA is closed or controlled by verified interim action. The NCR owner verifies objective evidence and recommends closure. The quality manager or MRB chair approves closure. Customer or regulatory representatives sign off when required, for example under specific engine or airframe customer MRB controls.

    Closure timing should vary depending on severity and contractual requirements. Many aerospace teams target minor non conformance closure within 30 days and major non closure within 60 to 90 days, with faster containment windows for high-risk events. AS9100 does not prescribe a fixed day count, but it expects action without undue delay. Aging reports, escalation rules, and owner accountability help ensure compliance, verify compliance, and maintain compliance. Connect981 enforces closure discipline with mandatory fields, automated reminders, dashboards by plant, program, and supplier, and exportable audit trail packages.

    Roles and Responsibilities Across the Aerospace NCR Lifecycle

    A repeatable NCR process depends on clearly defined roles, especially when multiple sites and suppliers contribute to the same aircraft program.

    • Operators and technicians identify non conformance, stop affected work when safe, and initiate the NCR.
    • Inspectors validate the defect, capture measurements, and support quality control.
    • Production supervisors apply containment, authorize station holds, and protect schedule realism.
    • Quality engineers own the NCR record, coordinate investigation, and align quality processes with defined procedures.
    • Quality managers approve classification, escalation, closure, and better quality management practices.
    • MRB members decide disposition and ensure the outcome meets applicable requirements.
    • Manufacturing and MRO engineers define rework, repair, and process changes.
    • Supplier quality manages supplier-related non compliance, SCAR linkage, and supplier CAPA.
    • Program managers monitor schedule, customer commitments, service quality, and resource allocation.

    In MRO, maintenance engineers and reliability teams take a larger role because non conformance may be found on in-service aircraft during inspection, teardown, or heavy check. Proper training is essential so each function knows when to raise, route, escalate, and close an NCR.

    Traceability, Documentation, and Audit Trail Requirements

    Aerospace NCR processes live or die on traceability. Each non conformance must link to parts, serial numbers, lots, heat numbers, work orders, aircraft registrations, process parameters, operator IDs, calibration IDs, drawings, and work instruction revisions. NCR processes create a permanent, auditable paper trail that assists with legal traceability and compliance.

    A robust audit trail records the full history of edits and approvals, photos, test reports, MRB minutes, repair schemes, timestamps for creation, containment, MRB, CAPA linkage, verification, and closure. It also cross-references CAPA, SCAR, customer complaint records, process records, and management review inputs. NCRs serve as critical inputs for quality audits, regulatory inspections, and management reviews, ensuring that quality issues are captured, investigated, and resolved in line with defined procedures.

    This level of traceability supports product quality, regulatory review, and future investigations. FAA guidance for production approval holders emphasizes traceability and control of articles through production and delivery, while EASA rules emphasize reliable record keeping and retention for airworthiness data. See the FAA’s AC 21-43A and EASA’s initial airworthiness rules for context.

    Connecting NCRs to Continuous Improvement in Aerospace

    Nonconformance reports are essential for identifying and addressing deviations from quality standards, and they facilitate continuous improvement by documenting issues and corrective actions taken. Continuous improvement in aerospace manufacturing is driven by analyzing trends in NCR logs to identify weak links in supply chains or assembly lines.

    Aggregated NCR data can reveal repeated minor non conformance in one cell, recurring supplier issues on titanium forgings, rising customer complaints on a specific LRU, or increased rework after a design change. Teams can use those insights to update control plans, revisit PFMEA, launch kaizen activity around high-defect manufacturing processes, and renegotiate supplier quality agreements based on evidence.

    The practical objective is not just to close records. It is to drive continuous improvement, improve customer satisfaction, meet customer expectations, and exceed customer expectations where possible. Corrective actions fix the specific event. Preventive measures and preventive actions reduce the likelihood of future events across similar products, suppliers, or processes.

    Digitalizing the Aerospace NCR Process with Connect981

    Paper NCR packs, spreadsheets, and disconnected QMS or MES records make aerospace nonconformance management slower than it needs to be. Data is retyped, holds are missed, attachments live in file shares, and closure depends on chasing signatures. That creates avoidable risk for quality management, schedule control, and audit readiness.

    Connect981 replaces fragmented NCR handling with an aerospace operations platform designed for connected shopfloor execution and supplier collaboration. Capabilities include digital NCR forms embedded in work instructions, automated routing to MRB and CAPA, ERP and PLM integration for part and configuration data, mobile evidence capture, document control, and dashboards for aging NCRs.

    A diverse aerospace manufacturing team is gathered around aircraft components, intently reviewing a digital workflow on their tablets. They are focused on ensuring compliance with quality management systems and addressing any non-conformance issues through effective corrective and preventive actions.

    The platform’s zero and low-code workflow builder lets teams mirror their existing non conformance procedure, including customer-specific rules, without a full MES replacement. In a quality management system qms environment, that matters because local procedures, OEM clauses, ITAR constraints, and customer approvals often differ by program.

    Connect981 also supports cross-factory and supplier visibility with shared NCR views, controlled access for customer representatives, standardized templates, and non conformance reporting software that preserves high quality standards. The result is a clearer workflow from containment through MRB, CAPA handoff, and disciplined closure.

    To see how Connect981 digitizes the full aerospace NCR process across factories, MRO lines, and suppliers, request a demo.

  • NCR Template: Practical Fields, Evidence, and Audit‑Ready Traceability

    NCR Template: Practical Fields, Evidence, and Audit‑Ready Traceability

    In aerospace manufacturing and MRO, a non conformance report is not just a quality form. It is a controlled quality record used to formally document, investigate, and resolve nonconformities identified during any phase of the product or service lifecycle.

    Nonconformance reports are essential for documenting deviations from specifications, procedures, or regulatory requirements, ensuring that quality issues are formally identified and addressed. Manufacturing and production sectors utilize NCRs to flag defective materials, assembly errors, or machinery malfunctions. In aerospace, that same discipline supports AS9100, FAA, EASA, customer, and program requirements.

    This guide explains what belongs in an NCR template, what evidence should be attached, and how an ncr record should be closed so it can withstand external audit review. Examples include nonconforming turbine blade machining in March 2026 and MRO inspection findings on A320 landing gear.

    Connect981, also known as C-981, provides digital NCR templates and workflows that connect shopfloor, engineering, quality control, and suppliers in a single ncr process.

    An inspector is closely examining an aircraft component on a clean maintenance bench, ensuring compliance with regulatory requirements and quality standards. The inspection process is part of a quality management system aimed at identifying any non-conformance and implementing corrective actions to maintain service quality.

    What Is an NCR Template? (Definition and Purpose)

    An NCR template is a standard, controlled layout for capturing every required piece of information about a non conformance in production, MRO, supplier quality, or service quality. An NCR template standardizes how organizations document, track, and resolve deviations from quality standards.

    The template is the data structure. The ncr process is the workflow: detection and reporting, evaluation and classification, root cause analysis, implementation of corrective actions, verification and closure, and follow-up and monitoring. Both must align with the quality management system, defined procedures, customer obligations, and regulatory requirements.

    A good nonconformance report template prevents missing quality data. It forces a clear description, requirement reference, acceptance criteria, immediate containment, disposition, root cause, corrective and preventive actions, closure verification, and sign off.

    There is also an older meaning to NCR. NCR paper is coated with micro-encapsulated dye and a reactive clay that create copies when pressure is applied. In that context, an NCR template is a digital layout used to print multi-part forms that duplicate writing without carbon paper. In this article, ncr template means the quality management form used to control nonconforming material and process deviation records.

    NCRs support compliance with various industry standards and regulations, including ISO 9001, AS9100, and FDA requirements, by providing documented evidence of quality issue resolution. Nonconformance reports are essential for compliance with industry standards and regulations, such as ISO 9001, AS9100, and FDA regulations, which require organizations to manage nonconformities and take corrective action. NCRs also serve as compliance records for government audits and risk mitigation in medical devices and pharmaceuticals. For aerospace, AS9100 clause 8.7 on control of nonconforming outputs is a useful anchor point; see the IAQG 9100 series overview.

    NCRs can be customized and standardized for different organizations, allowing for various templates that fit specific departmental needs, such as simple one-page reports for smaller organizations or extensive reports for larger organizations with compliance requirements.

    Core Sections of an NCR Template (Field-by-Field Guide)

    Every ncr form should contain these core sections, whether it is Word, Excel, paper, eQMS, or a digital workflow:

    • Unique report number, location, work order, date, and ncr status.
    • Problem description and non conformance description.
    • Non conformance type and standard violated.
    • Requirement reference, specifications, and acceptance criteria.
    • Risk, severity, and potential impact.
    • Immediate action, immediate corrections, containment, and affected process.
    • Root cause and root cause analysis.
    • Corrective actions, preventive action, and corrective and preventive actions.
    • Disposition, verification, closure evidence, and closure verification.

    Key sections of an NCR template include unique report number, problem description, standard violated, immediate action, root cause analysis, and corrective/preventive action. A Nonconformance Report includes key components such as a clear description of the nonconformance, the type of nonconformance, a reference to the unmet requirement, associated risk level, immediate containment actions, and disposition decisions.

    The structure of a nonconformance report typically includes sections for identification, location and work description, non-conformance description, requirement references, immediate action or containment, contractor response, engineer disposition, and verification and closure. If any of these fields are missing, the report is easier to challenge during an AS9100 or customer audit.

    1. NCR Identification and Context

    Strong identification is the backbone of traceability and later trend analysis. The template should include:

    • Unique NCR number, such as NCR-A320-MRO-2026-0142.
    • Site, line, cell, station, aircraft tail number, or MRO bay.
    • Manufacturing order, MRO work package, repair order, service bulletin, or PO.
    • Date and time raised.
    • Reporter name, function, department, and role.
    • Internal or supplier origin flag.

    For supplier issues, include supplier name, supplier code, PO number, contract number, delivery note, and supplier certificate reference. These fields link directly to process records and relevant documentation.

    2. Non Conformance Description (Facts, Not Opinions)

    The non conformance description must be factual. It should identify what was observed, where it was found, and how it failed to meet specific requirements. It should not speculate about human error or blame.

    A strong example: “Flap track pin diameter measured 15.94 mm versus specified 16.00 ±0.02 mm on PN FT-23-195, SN 23-981-047, measured on 18 Mar 2026 at Station B using CMM-05.”

    Required fields include part number, serial number, lot or batch, configuration revision, process step, aircraft registration if relevant, and measurement method. NCR documentation must include a clear, objective summary of the defect or deviation and the immediate steps taken to isolate affected products.

    3. Requirement References and Acceptance Criteria

    This is the most important part of turning an observation into a defensible non conformity report. The template must force at least one hard reference:

    • Drawing number and revision.
    • Specification clause.
    • Repair manual task.
    • Work instruction ID.
    • Customer requirement ID.
    • AS9102 first article inspection reference, when applicable.
    • OEM service bulletin or procedure number.

    Examples: “Drawing 981-TRB-110 Rev F, note 7” or “CMM 77-21-01, task 301, allowable corrosion depth 0.25 mm max.” Without a requirement reference, the NCR becomes an opinion rather than objective evidence.

    4. Detection Details and Audit Trail Hooks

    The template should capture when and how the issue was detected:

    • Incoming inspection, in-process inspection, final inspection, MRO inspection, automated vision check, operator observation, audit finding, or customer complaint.
    • Equipment ID, such as CMM-03 or torque wrench TW-12.
    • Last calibration date and calibration certificate number.
    • Linked inspection report, test log, maintenance log, or customer defect report.

    These fields create the early audit trail. In Connect981, several can be auto-populated from ERP, MES, inspection, and work order systems, reducing manual entry errors and protecting data continuity.

    Risk, Severity, and Scope Fields in the NCR Template

    Non-Conformance Reports can be classified into different types based on their severity, including minor and major non-conformance reports, which reflect the impact of the non-conformance on the product, service, or process.

    A strong ncr template includes severity rating, probability or occurrence, risk score if used, and regulatory-impact flag. Severity should consider flight safety, airworthiness, delivery impact, customer escape risk, and compliance exposure.

    Scope fields are equally important. The template must force bracketing: how many units, which lots, which serial numbers, and whether shipped assemblies may be affected. Poor scope definition can turn systemic issues into a false one-off.

    Severity and Classification Fields

    Use a standard dropdown or scale: Minor, Major, Critical. Minor Non-Conformance Reports typically address less severe issues that have a lower impact and can be corrected easily, while Major Non-Conformance Reports involve significant violations that require extensive corrective actions and communication with management.

    Examples:

    • minor non conformance: paint shade variance outside cosmetic requirement.
    • Major: dimensional out-of-tolerance condition on a structural bracket.
    • Critical: suspected unapproved part in a 737NG spoiler repair.

    For MRO, add fields for airworthiness impact, MEL or CDL relevance, and engineering authorization. Consistent classification improves trend analysis and management review.

    Scope and Impacted Items

    Scope fields should include quantity affected, serial numbers, tail numbers, production dates, work order range, and lot genealogy. Add checkboxes for:

    • Confined to single unit.
    • Multiple units affected.
    • Unknown, investigation required.
    • Shipped product potentially affected.

    Example: 50 titanium fasteners received on 02 Feb 2026 fail hardness requirements. The ncr data must show which engine builds used the lot, which units remain in stores, and which assemblies require re inspection.

    A technician is carefully measuring a machined aerospace part using precision equipment, ensuring adherence to quality standards and regulatory compliance. This process is essential for identifying any non conformities and implementing corrective actions to maintain service quality and continuous improvement.

    Containment, Correction, and Disposition Fields

    Containment, correction, and disposition are different decisions. Immediate containment controls risk now. Short-term correction addresses already-touched units. Final disposition determines what happens to each item.

    Auditors expect proof that nonconforming product or work was controlled. The template should show whether the job was stopped, stock was quarantined, ERP or MES holds were applied, and relevant stakeholders were notified.

    In digital systems like Connect981, disposition fields can block production movement until the required authority approves the next process step.

    Immediate Containment and Short-Term Correction

    The template should include:

    • Work stopped? Yes or no.
    • Material quarantined? Yes or no.
    • Hold tag, cage, bin, or location ID.
    • Temporary controls implemented.
    • Authorized by, with date and time.
    • Units already affected and immediate corrections completed.

    Example: a torque wrench is found overdue for calibration. The tool is suspended, all fasteners installed since 01 Apr 2026 are placed under review, and any suspect installation is rechecked against specifications. “Fixed issue” is not enough. The correction must be concrete and verifiable.

    Disposition Options and Approval

    Standard disposition choices include:

    • Rework to meet spec.
    • Repair under approved engineering disposition.
    • Scrap.
    • use as is with documented justification.
    • Return to supplier.
    • Customer-defined concession.

    Each disposition requires named approval, date, technical justification, and reference to any deviation, concession, MRB record, or customer approval. Example: “Accept under MRB concession MRB-2026-078 with revised allowable blend radius per OEM approval.”

    The template must allow split disposition when one lot is divided: some parts reworked, some scrapped, some returned. If a repair or concession changes configuration, the serialized record must not be left unchanged; the build record, markings, or PLM reference must be updated.

    Root Cause, Corrective, and Preventive Actions (CAPA-Ready Fields)

    A strong template separates symptom, root cause, corrective actions, and preventive action. NCR templates are designed to capture essential information such as the nature of the nonconformance, corrective actions taken, and preventive measures to avoid recurrence, ensuring compliance with quality management system requirements.

    For major or recurring issues, the NCR should link to the capa process, corrective action process, CAPA ID, SCAR, or formal risk assessment. Connect981 can initiate CAPA workflows when severity, recurrence, or supplier thresholds are met.

    Nonconformance reports help organizations identify and analyze recurring issues, which can lead to the implementation of preventive actions to avoid future nonconformities.

    Root Cause Analysis Field Design

    The root cause field should be separate from the non conformance description. It should capture contributing factors such as method, machine, material, manpower, environment, and measurement.

    Good example: “Outdated CNC program Rev B used after engineering released Rev D; program control process did not require shopfloor verification of current revision.”

    Add a field for investigation method: informal review, 5 Whys, fishbone, or full investigation. Generic “operator error” should be rejected unless evidence shows why the system allowed the error.

    Corrective and Preventive Action Planning Fields

    Corrective action fields should include action description, owner, target dates, resources, implementation date, and verification method. Preventive action fields should address broader controls that prevent recurrence across similar parts, suppliers, programs, or work centers.

    Examples include updating torque procedures, revising supplier acceptance criteria, adding barcode checks, or changing work instruction revision controls. By documenting nonconformities and their root causes, organizations can implement corrective and preventive actions (CAPA) that address the underlying issues, thereby reducing the likelihood of recurrence.

    Evidence, Attachments, and Traceability Requirements

    An NCR without objective evidence is weak. Typical attachments include photos, dimensional reports, NDT results, material test reports, calibration certificates, MES logs, supplier certificates of conformity, and inspection records.

    The template should list each attachment with filename, ID, revision, storage location, and owner. To ensure complete data collection, an NCR must document details such as evidence of defects and sign-offs for verification.

    Traceability means a reviewer can reconstruct exactly what happened, to which part, when, by whom, and under which requirement. Connect981 supports drag-and-drop uploads, version control, and linked evidence so the ncr record is not split across emails and file shares.

    The image depicts aerospace parts meticulously arranged in a clean industrial workspace, ready for receiving inspection to ensure compliance with quality standards. This setup emphasizes the importance of quality management systems and the need for relevant documentation to verify the acceptance criteria and prevent nonconformance.

    Audit Trail and Revision History Fields

    An audit trail should capture who created, edited, reviewed, dispositioned, verified, and closed the NCR. It should include timestamps for raised, contained, dispositioned, corrective actions completed, verified, and closed.

    Regulated aerospace environments should prevent silent overwrites. Updates need a reason for change, prior value, new value, and user identity. In Connect981, these events are system-generated and exportable for AS9100, customer, FAA, or EASA audit review.

    If the audit history is unreliable, the technical content may still be questioned.

    Internal vs Supplier NCR Templates (What Changes?)

    Internal NCRs apply to shopfloor processes, in-house MRO work, tooling issues, documentation errors, and internal production quality problems. Supplier NCRs apply to incoming material, outsourced special processes, external repair stations, or supplier documentation gaps.

    Both share a common core. Supplier templates add supplier code, PO, contract, delivery note, certificate of conformity, supplier NCR number, 8D reference, and response due date.

    Supplier NCRs may link to SCARs, scorecards, and sourcing decisions. The fields can vary depending on customer requirements, product criticality, and regulatory compliance impact.

    Coordinating Supplier Corrective Actions and Internal Records

    Supplier response fields should include supplier root cause, corrective actions, preventive actions, completion dates, and supplier verification evidence. Internal quality should accept, reject, or return the response with comments.

    Add fields for multi-program impact and impact on other customers when shared suppliers are involved. Keeping supplier answers in the same system reduces email-driven data loss and improves supplier collaboration.

    What Makes an NCR Weak vs Audit-Ready?

    Weak NCRs usually have the same pattern:

    • Vague description such as “dimension wrong.”
    • No requirement reference or acceptance criteria.
    • Missing severity, risk, or scope.
    • No containment record.
    • Disposition not approved.
    • “use as is” without engineering justification.
    • Root cause listed as human error without systemic analysis.
    • No closure evidence or verification.
    • Attachments missing or stored outside the record.

    Strong NCRs include measurable facts, named approvers, linked specifications, objective evidence, complete audit trail, and closure verification that can verify effectiveness.

    Weak example: “Paint peeling on A320 flap track. Repainted.”Audit-ready example: “Paint finish on A320 LT flap track PN FT-23-195, SN 14579, per PS-105 Rev C, found 15 Mar 2026 during final inspection. Delta E measured 4.5 versus required ≤3. Supplier batch 002345 quarantined. Disposition: rework per WP-05. Verification: next 10 parts measured within limit. Closed with QA sign off.”

    The effective use of NCRs can lead to improved product quality, reduced operational costs, and enhanced compliance with regulatory requirements, ultimately preventing customer complaints and operational inefficiencies. NCRs serve as critical inputs for continuous improvement programs, allowing organizations to analyze trends and implement preventive measures that enhance overall quality and compliance.

    Checklist: Quick Review Before Closing an NCR

    Before closure, confirm:

    • Is the unique NCR number, location, date, part, serial, lot, and configuration complete?
    • Is the description factual and measurable?
    • Is the requirement reference documented?
    • Is severity set and justified?
    • Is scope bracketed across affected units and shipped product?
    • Is containment documented with owner and date?
    • Is disposition approved by the authorized role?
    • Are corrective actions assigned with target dates?
    • Is preventive action defined where needed?
    • Are photos, reports, certificates, and process records attached?
    • Did re inspection or test data verify effectiveness?
    • Is closure evidence complete and sign off recorded?

    This checklist should be part of daily quality review, not just audit preparation.

    Designing and Using an NCR Template in Connect981

    A digital NCR template in Connect981 differs from static forms because required fields, routing, approvals, supplier access, and role-based visibility are built into the workflow. Teams can configure internal, supplier, and MRO templates with zero or low-code tools.

    Connect981 links NCRs to work orders, serial numbers, digital work instructions, supplier records, CAPA workflows, and dashboards. Results feed management review, recurrence metrics, time-to-containment, supplier performance, and minor versus major non conformance trends.

    The outcome is practical: better quality, stronger compliance, less manual reporting, and clearer decisions at the point of work. Request a Demo of Connect981 to see NCR templates, supplier workflows, and audit-ready traceability in a live aerospace context.

  • NCR vs MRB vs CAPA: How They Work Together in Aerospace Quality Workflows

    NCR vs MRB vs CAPA: How They Work Together in Aerospace Quality Workflows

    In real aerospace operations, NCR, MRB, and CAPA are not isolated quality terms. They are connected handoffs in the same quality control process, moving from defect detection to product disposition to systemic improvement.

    The practical sequence is simple: Detect → NCR → MRB → sometimes CAPA → closure and learning. The value comes from knowing where each step starts, where it stops, and when the next step becomes necessary.

    1. Overview: NCR vs MRB vs CAPA in One Workflow (Answer the Query Fast)

    In quality management, an NCR documents defects, the MRB evaluates non-conforming materials, and the CAPA addresses underlying causes. That is the cleanest way to understand ncr vs mrb vs capa in aerospace manufacturing and MRO.

    NCR is the first formal record when a nonconforming product, process deviation, or documentation issue fails a requirement. MRB is where a cross functional team determines what to do with that specific material. CAPA is the structured system used to determine root cause, take corrective actions, add preventive action where needed, and prevent recurrence.

    NCR, MRB, and CAPA are interconnected quality management frameworks designed to manage product or process defects. In AS9100, FAA, and EASA environments, this workflow must be well defined, documented, risk based, and supported by objective evidence. Connect981, also known as C-981, supports all three in one system so quality, production, engineering, and suppliers can see the same NCR → MRB → CAPA chain.

    An aerospace technician is carefully inspecting a metallic aircraft component on a clean shop floor, emphasizing the importance of quality control processes and risk management in aerospace manufacturing. This thorough investigation is crucial for ensuring high-quality products and addressing any potential quality issues effectively.

    2. Core Definitions in Service of Workflow Clarity

    Definitions matter only if they clarify the workflow. The question is not “what does each acronym mean?” The better question is: what does each step control, and when does the work move forward?

    2.1 NCR: The Trigger Point in the Quality Workflow

    Nonconformance Reporting (NCR) is a critical process in quality management systems that helps organizations identify and document deviations from expected standards or specifications. NCRs are opened whenever a nonconforming product, process problem, or documentation gap is detected against customer requirements, a drawing, a contract clause, or a quality standard.

    An NCR might capture a mis-drilled hole pattern on a 737 wing rib found on 12 March 2024 during in-process inspection. It might capture incorrect heat-treatment certification from a supplier on a landing gear forging at incoming inspection. It might also come from final inspection, MRO teardown, internal audits, customer complaints, or field returns.

    A useful NCR includes part number, serial or lot number, work order, specification, defect description, immediate actions, containment status, and risk assessment flag. In many organizations, NCRs originate in ERP, MES, QMS, email, or paper. Connect981 can centralize these inputs so quality data is not lost before the next decision point.

    2.2 MRB: Structured Disposition for the Specific Nonconforming Material

    The material review board is the cross-functional decision forum that evaluates the NCR record and the affected product. The MRB is a cross-functional team that decides what to do with non-conforming material that cannot be easily fixed.

    The MRB determines the fate of defective items through actions such as scrapping, reworking, or returning to the vendor. Common mrb decisions include rework to drawing, repair through approved data, use-as-is with documented risk justification, scrap, or return to supplier.

    The MRB question is narrow and practical: what can be safely done with this hardware now? It is not a full systemic investigation. MRB decisions focus on safety, airworthiness, fit, form, function, traceability, and whether customer or OEM approval is required.

    2.3 CAPA: Systemic Corrective and Preventive Actions

    CAPA stands for ‘corrective and preventive action’, which is a systematic approach used in regulated industries to identify, investigate, and address problems or non-conformities in products, processes, and systems. The practical capa meaning is this: CAPA changes the system so the same failure mode is less likely to happen again.

    The capa process is opened when repeat NCRs, serious risk, audit findings, supplier trends, or customer feedback suggest a systemic problem. A robust CAPA process should include steps for creating a CAPA request, reviewing it, initiating it formally, investigating the root cause, and verifying the effectiveness of the actions taken.

    Effective CAPA management requires a cross-functional team to oversee the investigation and resolution of issues, ensuring that all relevant perspectives are considered. That team must approve capa actions, maintain capa records, and confirm capa effectiveness through a verification step, not just implementation evidence.

    The CAPA process is crucial for maintaining compliance with quality management system standards, such as ISO 9001, and is often evaluated during external audits. In aerospace and medical devices, a robust quality management system (QMS) is essential for ensuring compliance with industry standards and regulations, particularly where adherence to standards like AS9100 and ISO 13485 is critical.

    Quality management systems must include clear documentation and control processes to ensure that all procedures are followed and that changes are properly managed throughout the product lifecycle. Continuous improvement is a key principle of quality management systems, which involves regularly assessing and refining processes based on internal audits and customer feedback to enhance product quality and compliance.

    3. The Actual Sequence: From Detection to NCR, MRB, and (Sometimes) CAPA

    The order is operational, not theoretical. An operator, inspector, supplier quality engineer, or MRO technician detects an issue. The immediate issue is contained. The NCR is created. The MRB decides the product disposition. Then the organization determines whether a formal capa is required.

    Sequence diagram logic: Operator → NCR → MRB → CAPA or No CAPA → updated procedures, training, risk files, and closure.

    Key steps:

    1. Detect an issue on the shopfloor, at receiving, during test, in the field, or during MRO.
    2. Contain the affected product and document the NCR.
    3. Route the NCR to MRB for technical evaluation and disposition.
    4. Determine whether the event is isolated or systemic using trends, risk analysis, recurrence, and customer impact.
    5. If needed, open a CAPA investigation with root cause analysis and an action plan.
    6. Close the loop by confirming MRB disposition, verifying CAPA effectiveness, and updating control plans, training, and risk registers.

    Consider an A320 assembly line with repeated torque-out defects on titanium fasteners. The first NCR leads to MRB rework. The second NCR leads to another rework decision. By the third similar event from the same supplier, the pattern points beyond one lot. CAPA becomes necessary because the production process or supplier control process may be unstable.

    A thorough investigation might find improper furnace calibration at the supplier. Corrective and preventive actions could include supplier calibration controls, revised incoming inspection checks, updated work instructions, and tighter supplier scorecards. Connect981 can visualize this chain across programs and suppliers, giving quality and supply chain management one view of NCRs, MRB outcomes, and CAPA status.

    Technicians are gathered around an inspection bench, meticulously reviewing aircraft fasteners and precision tools as part of the quality control process in aerospace manufacturing. This collaborative effort highlights important quality system elements and the commitment to continuous improvement and risk management.

    4. Decision Boundaries: When You Stop at NCR/MRB and When You Escalate to CAPA

    A major source of confusion in ncr vs mrb vs capa is the assumption that every NCR must become CAPA. That is not a robust process. It creates backlog, weak problem solving, and shallow corrective actions.

    You may stop at NCR plus MRB when the cause is obvious, risk is low, impact is local, and recurrence is unlikely. A single handling scratch on a nacelle panel may require containment, repair, documentation, and perhaps localized training. It does not automatically justify a full CAPA.

    Escalate to CAPA when root cause is unclear, recurrence is likely, potential risks extend across other products or suppliers, or the issue affects safety, compliance, delivery, or customer satisfaction. Frequent low-severity NCRs can justify CAPA if they reveal process problems or create cost and schedule impact.

    Effective NCR processes require clear definitions of escalation criteria to ensure consistent decision-making across an organization. NCRs should be used to capture not only isolated incidents but also to identify systemic issues that may require corrective actions to prevent recurrence.

    Good boundaries use risk matrices, FMEA scores, program-specific criteria, and documented risk tolerance set by OEMs or airworthiness authorities. This makes sense in multi-site networks where tribal judgment creates variation. Connect981 helps standardize these thresholds while still allowing site-specific controls.

    5. What Not to Conflate: Common Misunderstandings About NCR, MRB, and CAPA

    Many audit findings and quality escapes happen because organizations collapse these distinct concepts into one informal process. The result is incomplete records, weak root cause determination, and poor closure evidence.

    Common errors include:

    • MRB disposition is not corrective action. Rework or scrap fixes the lot, not necessarily the process.
    • NCR closure is not CAPA closure. “Fixed this part” is not the same as “fixed the cause.”
    • CAPA closure is not complete until effectiveness is verified with objective evidence.
    • Preventive actions are not MRB dispositions. They are changes to process, training, design controls, supplier controls, inspection plans, or environmental conditions.

    The separation is simple. NCR documents and controls the event. MRB documents risk based product disposition. CAPA documents system-level corrective and preventive actions and verifies they were properly addressed.

    Under-escalation is dangerous when repeated NCRs are closed through MRB without recognizing a trend. Over-escalation is also a problem because opening CAPA for every routine defect creates fatigue and delays serious investigations.

    For aerospace manufacturing, AS9100 expects control of nonconforming outputs and effective corrective action. For medical devices, FDA 483 observations and warning letters often cite weak capa procedures, poor complaint handling, and failure to verify effectiveness. A well-designed digital workflow separates the steps while keeping traceability between them.

    6. Risk Management Across NCR → MRB → CAPA

    Risk management in quality assurance involves identifying, assessing, and mitigating potential threats to processes to ensure product safety and reliability. A robust risk management process is essential for maintaining compliance with regulatory standards, as it helps organizations proactively address potential quality issues before they escalate.

    Incorporating risk management into the CAPA process is crucial, as it ensures that corrective and preventive actions are aligned with the severity and likelihood of potential risks.

    At each stage, risk changes shape:

    • NCR stage: screen whether the nonconforming product could have escaped, affected airworthiness, violated customer requirements, or created downstream quality problems.
    • MRB stage: determine whether use-as-is, repair, rework, or scrap is justified. Use-as-is should only occur when risk analysis confirms no safety or performance impact.
    • CAPA stage: determine whether the failure mode can affect the entire organization, other lines, other suppliers, or other programs.

    Risk tools may include FMEA, hazard analysis, severity and occurrence scoring, and program-specific control plans. In medical devices, CAPA actions may also update ISO 14971 risk management files. In Connect981, centralized risk data across NCRs, MRB records, and CAPA cases supports predictive analytics and better prioritization.

    7. How NCR, MRB, and CAPA Interact with Supply Chain Management

    Supplier issues are a major source of NCR volume in aerospace. Effective supplier management involves qualifying, evaluating, and monitoring the performance of suppliers to ensure compliance with industry standards and specifications.

    Establishing stringent criteria for supplier selection and ongoing evaluation is crucial for maintaining quality and compliance in aerospace manufacturing. A robust supplier management process includes issuing nonconformance reports (NCRs) when items purchased from suppliers do not meet established specifications, which can lead to corrective actions if issues are systemic.

    A typical supplier workflow starts with an NCR for composite plies out of tolerance, incorrect material certs, or a machined feature outside drawing limits. MRB then decides whether to rework internally, return to supplier, scrap, or expedite replacement. If the same supplier or commodity repeats the issue, CAPA or supplier corrective action becomes appropriate.

    Supplier corrective action requests (SCARs) may be necessary when suppliers repeatedly fail to provide items that meet specifications, indicating a need for more serious intervention. Supplier PPM, on-time delivery, MRB scrap rates, and customer feedback should all feed capa sources.

    Connect981 supports supplier collaboration by sharing controlled NCR, MRB, and CAPA-related information without relying on disconnected spreadsheets or email threads.

    The image depicts a supplier receiving area filled with inspected aerospace parts stored in clearly labeled containers, highlighting the importance of the quality control process and supply chain management in aerospace manufacturing. This organized setup reflects a robust process for managing quality issues and ensuring compliance with customer requirements.

    8. Industry Examples: Aerospace Manufacturing, MRO, and Medical Devices

    The workflow logic is consistent across regulated industries, but the triggers differ.

    In aerospace manufacturing, repeated paint thickness nonconformities on control surfaces for a 2025 production program may start as final inspection NCRs. MRB may allow rework for affected surfaces. If the pattern continues, CAPA adjusts paint process parameters, operator training, spray booth controls, and inspection frequency.

    In aerospace MRO, multiple repair stations may report the same nonconforming repair outcome on an engine component. Local MRB teams disposition the affected hardware, but the trend should roll into a network-level CAPA. The improvement may include revised repair instructions, validation checks, tooling controls, and technician qualification updates.

    In medical devices, nonconforming product, complaint trends, returns, and customer complaints are common CAPA sources under ISO 13485 and FDA expectations. The same distinction applies: NCR identifies problems, MRB-like review controls product, and CAPA addresses the system.

    In all cases, the value comes from relationship clarity. NCRs detect. MRB controls. CAPA transforms the system so organizations can deliver high quality products with better compliance readiness.

    9. Digitalizing the NCR–MRB–CAPA Chain with Connect981

    Brownfield aerospace environments often spread NCR, MRB, and CAPA work across ERP, MES, legacy QMS, file shares, spreadsheets, paper travelers, and email. That fragmentation creates missed escalations, incomplete thorough documentation, delayed approvals, and weak audit trails.

    Connect981 acts as a unified aerospace operations platform. It ingests NCR data from shopfloor execution, inspection, supplier portals, and existing enterprise systems. It routes MRB decisions through configurable zero-code workflows with the right engineering, quality, manufacturing, and supply chain approvals. It links CAPA records to the originating NCRs, MRB decisions, serial numbers, work orders, and production data.

    The practical capabilities are direct:

    • Digital work instructions update when CAPA actions change the process.
    • Parts traceability and serial number control enforce MRB decisions at point of use.
    • Dashboards show NCR trends, MRB scrap versus rework ratios, CAPA aging, supplier performance, and iso audit readiness.
    • AI-assisted root cause analysis helps identify problems earlier and suggests likely contributing factors for review.
    • Automated alerts help teams address problems before overdue tasks become compliance exposure.

    Technology does not replace quality judgment. It gives the quality system a more reliable operating structure. For teams comparing ncr vs mrb vs capa, the goal is not more terminology. The goal is one connected workflow where product and quality problems are visible, decisions are documented, and improvement is measurable.

    To see an end-to-end digital NCR → MRB → CAPA workflow in action, request a demo of Connect981.

  • ISO 9000 Quality Management Principles: Fundamentals and Vocabulary Reference

    ISO 9000 Quality Management Principles: Fundamentals and Vocabulary Reference

    ISO 9000:2015, titled “Quality management systems — Fundamentals and vocabulary,” is the foundational standard in the iso 9000 family. It defines the terms, concepts, and the seven quality management principles that underpin ISO 9001:2015 and related quality management standards across industries.

    This article is a reference guide to the quality management principles and standardized terminology found in ISO 9000. It is not an implementation handbook, maturity model, or prescriptive guide. The purpose here is definitional clarity.

    Shared definitions matter in cross-functional and multi-site contexts. In aerospace manufacturing and MRO supply chain operations, ambiguity in terminology creates real problems during audits, contract negotiations, and technical documentation reviews. When one team defines “nonconformity” differently than another, or when “corrective action” gets conflated with simple rework, the result is inconsistent records and audit findings that could have been avoided.

    Connect981 works with aerospace and MRO organizations that rely on ISO 9000 terminology to coordinate ERP, MES, QMS, and supplier workflows. Precise language directly affects how digital operations function. When a quality management system maps shopfloor events to ISO-aligned terms, audit readiness improves and data consistency across sites becomes achievable.

    This article covers:

    • The role and history of ISO 9000 in the ISO 9000 family
    • The relationship between ISO 9000 and ISO 9001
    • The seven quality management principles as conceptual foundations
    • Standardized terminology and why it matters
    • Examples of commonly misunderstood terms
    • ISO 9000 vocabulary in aerospace and MRO contexts

    ISO 9000 in the ISO 9000 Family: Role and History

    The iso 9000 family is a set of international standards for quality management first released in 1987 by the international organization for standardization. These standards provide frameworks for organizations to establish, implement, and improve a quality management system qms. The family includes multiple documents, each with a distinct purpose: ISO 9000 defines fundamentals and vocabulary, ISO 9001 specifies requirements for certification, and ISO 9004 provides guidance on achieving sustained success.

    ISO 9000 itself carries the full title “Quality management systems — Fundamentals and vocabulary.” It is not a certification standard. ISO 9001:2015 is the standard that specifies requirements for a QMS that can be audited and certified by accredited certification bodies.

    The revision history of ISO 9000 reflects the evolution of quality management thinking:

    Year

    Milestone

    1987

    Original publication of the ISO 9000 family

    2000

    Major revision introducing process-focused structure

    2008

    Minor update for clarification

    2015

    Alignment with Annex SL high-level structure; seven updated QMPs

    ISO 9000 provides the conceptual baseline that the iso technical committee ISO/TC 176 uses when developing ISO 9001 and sector-specific derivatives. AS9100D for aerospace, published in 2016, aligns with ISO 9001:2015 and therefore inherits ISO 9000’s terminology and principles. The international automotive task force similarly developed IATF 16949:2016 with ISO 9001 as its core, which means ISO 9000 definitions apply there as well.

    ISO 9000 is a normative reference in ISO 9001:2015. This means its definitions and fundamentals are formally invoked by ISO 9001 requirements. When ISO 9001 uses a term like “process,” “documented information,” or “nonconformity,” the precise meaning comes from ISO 9000.

    A technician is performing a quality control inspection on various components in a manufacturing setting, ensuring they meet the quality management standards outlined by ISO 9000. This process is essential for achieving customer satisfaction and maintaining consistent product quality through effective quality management systems.

    Relationship Between ISO 9000 and ISO 9001

    ISO 9000 and ISO 9001 are distinct but interdependent documents within the iso 9000 family. Understanding their relationship is essential for anyone working with quality standards.

    ISO 9000 is the source of agreed vocabulary, key concepts, and the statement of the seven quality management principles. It provides the definitional foundation. ISO 9001:2015 is the standard that specifies auditable QMS requirements used by certification bodies worldwide. Over one million organizations held ISO 9001 certificates in the early 2020s, making it the most widely adopted management system standard globally.

    The structural relationship works as follows:

    Document

    Function

    ISO 9000:2015

    Defines terms, fundamentals, and principles

    ISO 9001:2015

    Specifies requirements for a certifiable QMS

    Sector standards (AS9100, IATF 16949)

    Add sector-specific requirements to ISO 9001

    ISO 9001 clauses—covering context of the organization, leadership, operation, performance evaluation, and improvement—rely on terms defined precisely in ISO 9000. Terms such as “process,” “monitoring,” “nonconformity,” “correction,” and “corrective action” carry specific meanings that auditors and organizations must interpret consistently.

    Sector-specific standards like AS9100D for aerospace and IATF 16949:2016 for automotive adopt ISO 9001 requirements wholesale, then add additional requirements relevant to their industries. Because these sector standards build on ISO 9001, they inherit ISO 9000’s terminology and principles.

    The iso certification process for any of these standards depends on shared understanding of ISO 9000 vocabulary. An external audit conducted against ISO 9001 or AS9100 uses ISO 9000 definitions as the interpretive baseline.

    ISO 9000 Quality Management Principles (QMPs)

    ISO 9000:2015 identifies seven quality management principles that provide the conceptual basis for the iso 9000 family, including ISO 9001. These principles are not listed in priority order; their relative importance varies by organization and context.

    The seven quality management principles are:

    1. Customer focus
    2. Leadership
    3. Engagement of people
    4. Process approach
    5. Improvement
    6. Evidence-based decision making
    7. Relationship management

    Each principle is described below in definitional terms, explaining its role in the structure of ISO 9001.

    Customer Focus

    The customer focus principle recognizes that the primary purpose of a quality management system is to meet customer requirements and strive to exceed customer expectations. Customer satisfaction is the central measure of QMS performance.

    In ISO 9001, this principle is reflected in requirements for determining customer needs, enhancing customer satisfaction through conforming products and services, and monitoring customer perception. Clauses addressing customer requirements, customer communication, and post-delivery activities trace directly to this principle.

    The term “customer” in ISO 9000 encompasses anyone who receives a product or service, including internal customers within an organization. Customer demand and customer expectations shape how organizations define quality objectives.

    Leadership

    The leadership principle is concerned with establishing unity of purpose and direction within an organization. Leaders at all levels create conditions in which people can become fully engaged in achieving the organization’s objectives.

    ISO 9001 clauses on management responsibility, quality policy, and organizational roles reflect this principle. Leadership is not limited to top management; it includes anyone who establishes direction, provides resources related to quality, and maintains accountability for QMS outcomes.

    Engagement of People

    This principle recognizes that competent, empowered, and engaged people at all levels throughout the entire organization are essential to enhance an organization’s ability to create and deliver value.

    ISO 9001 requirements for competence, awareness, and communication reflect engagement of people. The principle aligns with total quality management concepts that emphasize participation across functions and levels.

    Process Approach

    The process approach principle states that consistent and predictable results are achieved more effectively and efficiently when activities are understood and managed as interrelated processes that function as a coherent system.

    This principle shapes the definitions of “process,” “input,” “output,” and “sequence and interaction of processes” in ISO 9000. ISO 9001’s structure—with requirements for process identification, process inputs and outputs, process criteria and controls, and process monitoring—is built on the process approach.

    Manufacturing processes, production processes, and service delivery processes are all understood through this lens. The process approach treats the quality system as an interconnected set of activities rather than isolated functions.

    Improvement

    The improvement principle recognizes that successful organizations have an ongoing focus on improvement. This encompasses continuous improvement of products, services, and processes, as well as continuous quality improvement in the QMS itself.

    ISO 9001 addresses this through requirements for corrective action, continual improvement, and management review. The principle distinguishes between improvement as a permanent organizational objective and specific improvement projects.

    ISO 9000 uses “continual improvement” rather than “continuous improvement” to indicate that improvement occurs in recurring cycles rather than as an unbroken stream. Both terms appear in quality literature, but ISO 9000 formalizes “continual.”

    Evidence-Based Decision Making

    The evidence based decision making principle states that decisions based on the analysis and evaluation of data and information are more likely to produce desired results.

    ISO 9001 reflects this in requirements for monitoring, measurement, analysis, and evaluation. Internal audits, performance indicators, and data analysis requirements all stem from this principle. The expectation is that decisions about quality objectives, process changes, and resource allocation are grounded in evidence rather than assumption.

    Relationship Management

    The relationship management principle recognizes that managing relationships with interested parties—including suppliers, partners, and others in the supply chain—sustains organizational performance.

    ISO 9001 requirements for external providers, supplier evaluation, and stakeholder consideration reflect this principle. In complex manufacturing environments, relationship management affects how organizations coordinate with suppliers, share quality data, and address nonconformities that span organizational boundaries.

    A diverse aerospace manufacturing team is gathered around a table, collaboratively reviewing engineering documentation to ensure compliance with quality management standards and enhance customer satisfaction. Their focus on effective quality management principles reflects a commitment to continuous improvement and meeting customer expectations in their production processes.

    Standardized ISO 9000 Terminology and Why It Matters

    ISO 9000:2015 defines nearly 200 terms related to quality management. These include foundational concepts, QMS-specific vocabulary, and management system terminology aligned with other ISO management system standards.

    Consistent use of ISO 9000 terms supports coherent interpretation of ISO 9001 clauses by:

    • Organizations implementing a QMS
    • Auditors conducting conformity assessment
    • Regulators reviewing compliance
    • Customers evaluating suppliers
    • National standards bodies developing guidance

    In complex environments such as aerospace manufacturing, where Connect981 customers coordinate work packages, MRO events, and supplier data across multiple physical locations and jurisdictions, shared vocabulary reduces ambiguity in contracts, quality agreements, audit reports, and digital records.

    The practical effect of standardized terminology appears when ERP, MES, and QMS systems exchange data using the same terms. If one system logs a “correction” and another system expects a “corrective action,” the mismatch creates confusion and potential audit findings. Standardized definitions prevent this.

    ISO 9000 aligns terminology with other management system standards, including ISO 14001 for environmental management and ISO 45001 for occupational health and safety. This alignment supports integrated management systems and enables organizations to manage quality, environmental, and safety requirements using consistent language.

    Key categories of ISO 9000 terms include:

    Category

    Examples

    Quality concepts

    Quality, requirement, grade, capability

    QMS terms

    Quality management system, quality policy, quality objective

    Process terms

    Process, procedure, input, output, product, service

    Conformity terms

    Conformity, nonconformity, defect, correction, corrective action

    Documentation terms

    Documented information, specification, quality manual, record

    Audit terms

    Audit, audit criteria, audit evidence, audit finding

    Commonly Misunderstood ISO 9000 Terms

    Several ISO 9000 terms are frequently interpreted differently across organizations and industries. Inconsistent interpretation leads to inconsistent application of ISO 9001 requirements, audit findings, and contractual disputes.

    Quality

    ISO 9000 defines “quality” as the degree to which a set of inherent characteristics of an object fulfills requirements. This definition differs from colloquial usage, where “quality” often implies premium grade or superior performance.

    A product with basic specifications that fully meets its stated requirements has quality according to ISO 9000. A premium product that fails to meet requirements does not. Quality managers often encounter confusion when stakeholders equate “quality” with “high-end” rather than “conforming to requirements.”

    Requirement

    A “requirement” in ISO 9000 is a need or expectation that is stated, generally implied, or obligatory. Requirements include customer requirements, statutory and regulatory requirements, and organization-determined requirements.

    The misunderstanding arises when organizations treat only written specifications as requirements. ISO 9000 recognizes that requirements can be implied by custom or practice, even when not explicitly documented.

    Nonconformity

    A “nonconformity” is the non-fulfillment of a requirement. This term is distinct from “defect,” which ISO 9000 defines as non-fulfillment of a requirement related to an intended or specified use.

    In practice, organizations sometimes use these terms interchangeably, which creates problems during audits and when categorizing quality records. Not every nonconformity is a defect, and the distinction affects how issues are logged and addressed.

    Correction vs. Corrective Action

    This distinction causes significant confusion in aerospace and MRO operations.

    A “correction” is an action to eliminate a detected nonconformity. Reworking a turbine blade to bring it into specification is a correction.

    A “corrective action” is an action to eliminate the cause of a nonconformity and to prevent recurrence. Modifying a fixture or revising a work instruction to prevent the same error from happening again is a corrective action.

    Mislabeling a one-off rework as a “corrective action” when ISO 9000 would classify it as a “correction” creates inaccurate quality records and may obscure systemic issues that require root cause analysis.

    Preventive Action

    ISO 9001:2015 removed explicit requirements for “preventive action” as a separate concept, folding it into risk-based thinking. However, ISO 9000 still defines “preventive action” as action to eliminate the cause of a potential nonconformity or other potential undesirable situation.

    Some organizations still reference preventive action in their documented procedures, which can create confusion during audits against current ISO 9001 requirements.

    Monitoring vs. Measurement

    “Monitoring” is determining the status of a system, a process, a product, a service, or an activity. “Measurement” is the process of determining a value.

    Monitoring does not necessarily involve measurement. Visual inspection to confirm that a process step occurred is monitoring. Recording a dimensional value is measurement. The distinction affects how organizations document control activities.

    Documented Information

    ISO 9000:2015 introduced “documented information” to replace the older terms “documents” and “records.” Documented information encompasses both documents (information and the medium on which it is contained) and records (documents stating results achieved or providing evidence of activities performed).

    Organizations transitioning from earlier ISO 9001 versions sometimes struggle with this terminology shift, particularly when updating document control and record-keeping procedures to align with current standards. Quality manuals, while no longer explicitly required by ISO 9001:2015, remain common as documented information.

    Traceability

    “Traceability” is the ability to trace the history, application, or location of an object. In aerospace contexts, traceability requirements extend to materials, components, and production processes.

    Some organizations interpret traceability as simply maintaining records. ISO 9000’s definition emphasizes the ability to trace—meaning the records must be organized and accessible in a way that enables reconstruction of an object’s history when needed.

    ISO 9000 as a Foundational Document for Modern QMS

    ISO 9000 functions as the foundational reference for all iso 9000 family QMS standards and many sector-specific documents. Since the 2015 revisions aligned ISO 9000 with the Annex SL high-level structure used across ISO management system standards, its role as a common vocabulary has become even more significant.

    Technical committees—including ISO/TC 176 for quality management, aerospace standards committees, and industry-specific groups—use ISO 9000’s fundamentals and vocabulary when drafting consistent, interoperable requirements. This consistency enables organizations to integrate multiple management systems without conflicting terminology.

    The structured definitions in ISO 9000 support digitalization of quality data. Platforms like Connect981 map shopfloor events, nonconformities, and traceability records to ISO-aligned terms for audit-ready reporting. When the terminology in digital systems matches ISO 9000 definitions, gap analysis during audits becomes straightforward.

    ISO 9000’s principle-based vocabulary enables organizations, certification bodies, and regulators to discuss QMS performance using a common, globally recognized language. Whether the conversation involves a supplier in one country and a customer in another, or an internal team and an external audit body, ISO 9000 provides the reference point.

    Future revisions of ISO 9000 are expected to preserve its role as a core reference while refining terminology to reflect evolving concepts like risk management and data-driven decision making. The standard’s function as a living vocabulary ensures it remains relevant as quality management practices develop.

    Understanding ISO 9000 is primarily about understanding the language and principles that frame how ISO 9001 and related standards are interpreted. Without this foundation, consistent quality across an organization’s operations and supply chain becomes difficult to achieve.

    The image depicts an aircraft maintenance hangar where technicians are diligently working on a commercial airplane, ensuring adherence to quality management principles and standards. This environment emphasizes customer satisfaction and operational efficiency, reflecting the organization's commitment to continuous improvement and regulatory requirements within the aviation industry.

    ISO 9000 Vocabulary in Aerospace and MRO Contexts

    Aerospace manufacturing and MRO operations rely heavily on ISO 9000 vocabulary to maintain clear communication across OEMs, Tier 1–3 suppliers, and maintenance organizations. The complexity of aerospace supply chains, combined with stringent regulatory requirements from FAA, EASA, and other bodies, makes precise terminology essential.

    Terms from ISO 9000 take on specific interpretations in aerospace standards like AS9100D:

    ISO 9000 Term

    Aerospace Application

    Traceability

    Serial number management, batch tracking, material certifications

    Configuration management

    Revision control of engineering data and as-built records

    Release of product and service

    First article inspection, airworthiness certification

    External provider

    Qualified supplier list, supplier quality agreements

    Nonconformity

    Material review board dispositions, deviation requests

    These terms appear in digital work instructions, inspection points, and defect logging across real-world environments. In airframe assembly or engine overhaul facilities, the distinction between ISO 9000 terms affects how quality events are categorized, reported, and resolved.

    Connect981 uses standardized ISO 9000 definitions when structuring quality checks, nonconformity categories, and audit trails across multiple plants and MRO facilities. When a shopfloor system classifies a discrepancy using the same terminology that appears in AS9100 audit checklists, the path from event detection to audit response becomes direct.

    The alignment of digital systems with ISO 9000 vocabulary also affects how organizations document quality data for customers and regulators. Build packages, routing sheets, and inspection records that use ISO-standard terminology integrate more easily with customer quality systems and reduce rework during contract review.

    Shared definitions influence operational efficiency in specific ways:

    • Work order systems that distinguish “correction” from “corrective action” enable accurate root cause tracking
    • Traceability records structured around ISO 9000 definitions support faster response to customer demand for documentation
    • Nonconformity logs aligned with ISO terminology simplify reporting to certification bodies

    The result is improved customer satisfaction through consistent quality documentation and reduced friction during conformity assessment.

    Summary: ISO 9000 as a Language for Quality Management

    ISO 9000:2015 defines the fundamentals, vocabulary, and quality management principles that underpin ISO 9001 and related international standards. Its primary contribution is a shared language—defining key terms, clarifying the seven quality management principles, and aligning concepts across sectors and geographies.

    The distinction between commonly confused terms like “correction” and “corrective action” matters in practice. When organizations, auditors, and technology providers use these terms consistently, clarity in audits, contracts, and digital records follows.

    The relationship between ISO 9000 and ISO 9001 is foundational:

    • ISO 9000 supplies the definitions and principles
    • ISO 9001 transforms them into specific requirements
    • Sector standards like AS9100 add industry-specific requirements while inheriting ISO 9000’s vocabulary

    For aerospace manufacturing and MRO operations, where compliance with statutory and regulatory requirements intersects with complex supply chain coordination, ISO 9000’s standardized terminology enables an effective quality management system that spans organizational boundaries.

    Organizations that achieve certification to ISO 9001 or AS9100 do so using the vocabulary ISO 9000 defines. Platforms that support quality operations—including Connect981—structure data and workflows around these same terms. The key benefits of grounding quality discussions, documentation, and data models in ISO 9000 terminology include reduced ambiguity, improved operational efficiency, and business opportunities enabled by consistent quality across the enterprise.

    When quality managers, engineers, and operations leaders share a common vocabulary, product quality and process performance become measurable against agreed definitions rather than competing interpretations.