Tag: AS9102 first article inspection

  • First Article Inspection (FAI) in Aerospace Manufacturing

    First Article Inspection (FAI) in Aerospace Manufacturing

    First Article Inspection is the formal verification step that confirms a manufacturing process can consistently produce parts meeting all engineering requirements. In aerospace, this process determines whether a supplier’s production methods, tooling, and materials will deliver conforming hardware before committing to full-rate production or after a major change to design, process, or facility.

    The First Article Inspection Report, commonly called the FAIR, serves as the documented evidence of this validation. It captures material certifications, dimensional measurements, special process approvals, and functional test results in a structured format aligned with AS9100-compliant quality management systems. For aerospace organizations, the FAIR is both a quality gate and a long-term traceability record.

    This pillar guide from Connect981 covers the complete FAI landscape: when first article inspection is required, how to execute the FAI process, what documentation AS9102 demands, how to maintain traceability across the supply chain, and how digital tools reduce FAI cycle time without sacrificing compliance.

    What is First Article Inspection (FAI)?

    First article inspection in aerospace is a formal, documented verification that the manufacturing process, tooling, methods, and suppliers can produce a part that conforms to all engineering, material, and functional requirements. The inspection evaluates a production-representative sample manufactured under normal production conditions, not a hand-finished prototype or engineering sample.

    The critical distinction is that FAI evaluates the manufacturing system, not just a single part. The goal is to prove process capability and consistency before mass production begins. A successful FAI establishes the production baseline and becomes the reference for any future partial FAI or delta FAI activities.

    Aerospace FAI is governed by SAE AS9102, with the latest revision (AS9102D) released in March 2024. This standard defines the documentation structure, required content, and acceptance criteria that suppliers must follow.

    Key terms used throughout this guide:

    • First article inspection: The verification event that validates a manufacturing system’s capability
    • FAIR: The documented report package containing Forms 1, 2, and 3 plus supporting evidence
    • AS9102: The SAE standard governing FAI documentation requirements
    • Ballooned drawing: Engineering drawing with numbered identifiers linking each characteristic to inspection data
    • Characteristic accountability: The systematic verification and recording of all design features
    • Key characteristics: Features with highest risk to product performance or safety requiring special controls

    Unlike routine in-process or final inspection, FAI is event-driven. It occurs at specific triggers such as new part introduction, major design changes, or supplier transitions. The inspection scope is exhaustive, covering 100% of drawing characteristics rather than statistical sampling.

    Regulatory and Standards Context for FAI

    First article inspection matters to aerospace regulators, primes, and certification bodies because it provides documented evidence that production processes meet design intent before hardware enters service. The FAI requirement flows from quality standards through purchase orders into contractual obligations.
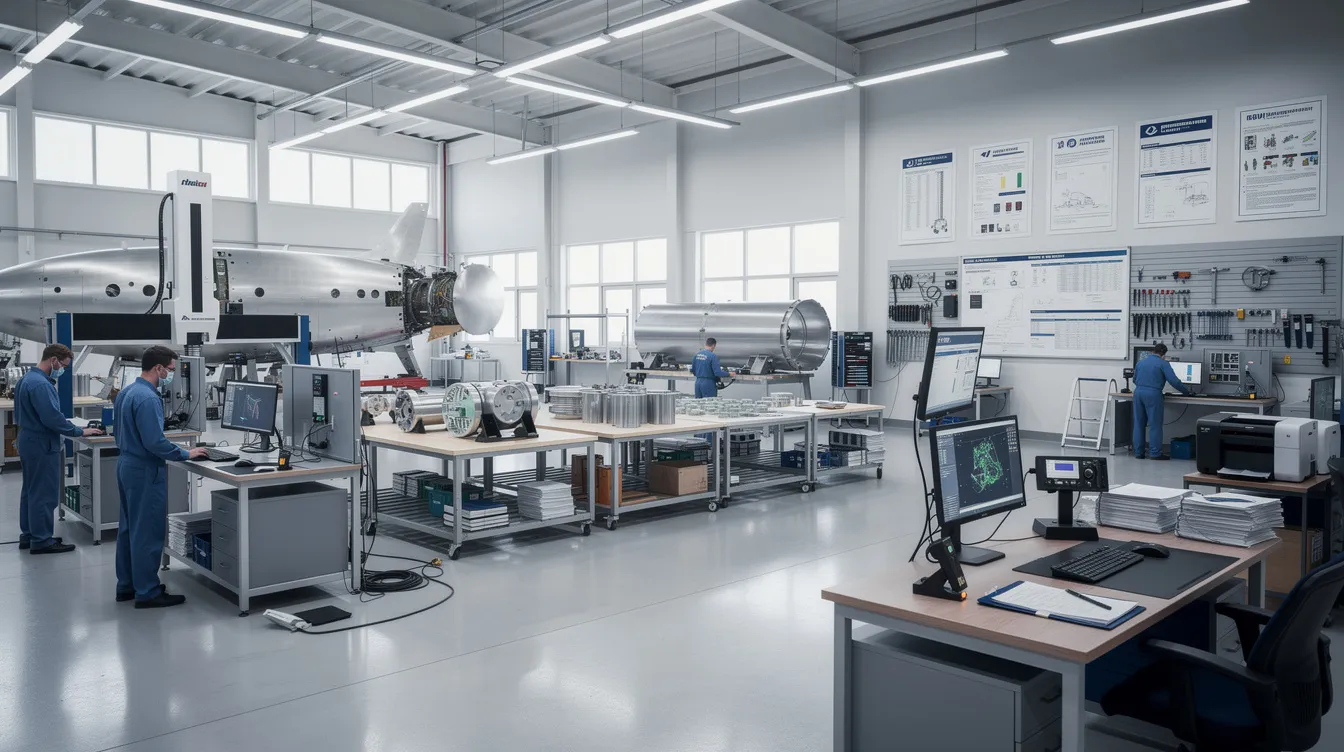
    The image depicts an aerospace manufacturing facility equipped with quality inspection equipment and documentation stations, highlighting the critical aspects of the first article inspection process. Various tools and documentation are present to ensure compliance with stringent quality control and assurance standards in the aerospace industry.

    The regulatory framework includes:

    • AS9100 series: The primary aerospace quality management system standard, with AS9102 referenced in Clause 8.5.1.3 for production process verification
    • EN9100 and JISQ9100: European and Japanese equivalents that align with AS9102 principles
    • SAE AS9102: The specific standard for FAI documentation, developed by the International Aerospace Quality Group (IAQG)

    OEMs like Boeing, Airbus, Lockheed Martin, and Rolls-Royce flow down FAI requirements through purchase orders and quality clauses. These clauses typically reference AS9102 explicitly and may add customer-specific requirements for FAIR format, approval workflows, or delegated representative involvement.

    FAI connects to multiple regulatory environments:

    • FAA and EASA production approvals under 14 CFR Part 21 and European equivalents
    • US Department of Defense contracts subject to DFARS clauses requiring documented first-article verification
    • Export-controlled work under ITAR or EAR regulations

    For organizations pursuing AS9100 certification, FAI records serve as evidence of process control and design understanding during audits. Auditors specifically verify linkage between the first build and ongoing production control plans.

    In aerospace, FAI (AS9102) often integrates with Advanced Product Quality Planning per AS9145. The FAI serves as the production validation step in APQP Phase 4, demonstrating that the production process can meet design specifications and quality requirements.

    When is First Article Inspection Required?

    Timing and triggers for FAI are defined by AS9102 and customer contracts. Understanding these triggers is essential for compliance and for avoiding rework when a FAIR is rejected for scope issues.

    Typical triggers for a full FAI per AS9102 and common OEM practices:

    Trigger

    Description

    New part number

    First production of a new design or purchase from a new supplier

    New supplier

    First production by a supplier, regardless of prior part history

    New facility

    First production at a new manufacturing location

    New methods/tooling

    Adoption of manufacturing methods or tooling differing from approved baseline

    Material changes

    New raw material forms or supplier sources

    Engineering design changes often require FAI. The extent depends on what changed:

    • Full FAI: Required when changes affect multiple characteristics or fundamental process assumptions
    • Partial FAI: Appropriate when only a subset of characteristics changed (e.g., two bore diameters at Rev C)
    • Delta FAI: Used when production transfers between facilities or when tooling relocates with unchanged manufacturing sequence

    Process change triggers include major changes in NC programs, process routing, manufacturing sequence, special processes (heat treat, plating, welding), or raw material specifications.

    Many OEM supplier quality manuals mandate FAI after a production lapse of 24 months or more. This reflects concern that knowledge degradation, personnel turnover, and equipment drift during extended gaps may introduce undetected changes to process capability.

    A separate cluster article on when FAI is required expands on these triggers with specific AS9102D clause references and OEM examples.

    FAI vs PPAP and Other Approval Processes

    Readers often confuse first article inspection FAI with the Production Part Approval Process. Both serve as quality gates, but they differ in scope and origin.

    PPAP originated in the automotive industry as part of the APQP framework. It covers a broad range of deliverables: process capability studies, measurement system analysis, control plans, and long-term production readiness documentation.

    FAI (AS9102) focuses heavily on characteristic verification and traceability for a single build event. It validates that a manufacturing process can produce conforming parts but does not inherently require statistical capability studies or control plan submissions.

    Key distinctions:

    Aspect

    FAI (AS9102)

    PPAP

    Primary focus

    Characteristic verification, material/process traceability

    Broad production readiness

    Documentation

    Three AS9102 forms plus attachments

    Up to 18 elements including capability studies

    Industry origin

    Aerospace (IAQG)

    Automotive (AIAG)

    Scope

    Single build event validation

    Long-term production capability

    FAI can be considered a subset of a full PPAP package. However, aerospace primes may require both AS9102 FAIR and additional PPAP or AS9145 deliverables for complex programs.

    Common aerospace customer requirements include:

    1. AS9102 FAIR only: Standard for many detail parts and lower-tier suppliers
    2. AS9102 plus capability studies: Required for key characteristics on critical assemblies
    3. Full APQP/PPAP evidence: Mandated for new product development programs with extensive design responsibility

    The cluster article FAI vs PPAP compares required documents line-by-line across both approval process frameworks.

    FAI Documentation and AS9102 Forms

    The FAIR is the core deliverable of first article inspection. Unless a customer-specific template is mandated in the purchase order or supplier quality manual, the three AS9102 forms serve as the documentation standard.

    The three forms work together to establish complete traceability:

    Form

    Name

    Purpose

    Form 1

    Part Number Accountability

    Identifies the part, revision, FAI type, and reason

    Form 2

    Product Accountability

    Documents materials, special processes, and tests

    Form 3

    Characteristic Accountability

    Records inspection results for every balloon

    A ballooned drawing or 3D digital product definition identifies every characteristic with unique balloon IDs. These IDs map directly to line items on AS9102 Form 3, creating traceability between visual part definition and inspection results.

    Common supporting documents attached to a FAIR package:

    • Raw material certificates of conformance and mill test reports
    • Special process certifications (NADCAP approvals for heat treat, NDT, welding)
    • Functional test reports (pressure tests, electrical continuity)
    • Process flow diagrams or routing sheets
    • Setup sheets and work instructions
    • Nonconformance reports and corrective actions if applicable
    • Customer-approved concessions or deviations

    Key characteristics and critical-to-quality features must be explicitly identified using designators like “KC,” “CC,” or customer-specific markings. These designations signal which features warrant special controls during production.

    Connect981 can host digital FAIR templates aligned with AS9102D, auto-populate fields from ERP and MES data, capture ballooned drawing links, and enforce mandatory attachments before FAIR submission.

    A dedicated cluster article on FAI documentation requirements walks through each field in AS9102 Forms 1–3 with completed examples.

    AS9102 Form 1 – Part Number Accountability

    Form 1 establishes the identity and context for the FAI. Required content includes:

    • Part number and nomenclature
    • Drawing or model number with revision level
    • FAI type (full, partial, delta)
    • Reason for FAI (new part, design change, facility transfer, production lapse)
    • Date of FAI and effective date of any triggering change

    Form 1 distinguishes between Detail FAI (single-component parts manufactured as a discrete unit) and Assembly FAI (multi-component assemblies with a bill of materials).

    For assemblies, Form 1 must list:

    • Each lower-level part number
    • FAIR reference if an FAI exists for that component
    • Serial or lot numbers to maintain traceability across levels

    This hierarchical approach ensures that if a sub component fails FAI or has a nonconformance, the impact on overall assembly acceptance is transparent and traceable.

    AS9102 Form 2 – Product Accountability (Materials and Processes)

    Form 2 documents raw materials and special processes used to manufacture the first article.

    Raw material entries include:

    • Material designation (e.g., 7075-T6 aluminum plate, Ti-6Al-4V bar stock)
    • Material specification reference (e.g., AMS-QQ-A-250/12 for aluminum)
    • Heat lot or batch numbers for traceability
    • Certificate of conformance reference

    Special process entries include:

    Process Type

    Example Specification

    Required Documentation

    Anodizing

    AMS2469, Type II or III

    Process spec, supplier code, approval status

    Passivation

    AMS2700

    NADCAP certification, lot number

    Heat treatment

    AMS specification with temp/time

    Furnace certification, chart records

    NDT

    Customer or NADCAP spec

    Operator certification, inspection report

    Welding

    AMS or customer spec

    Filler material, heat input, post-weld treatment

    Functional tests such as pressure tests, torque tests, or electrical continuity for harnesses are linked via procedure numbers and test report identifiers.

    Example row for a machined strut fitting:

    Material

    Spec

    Heat Lot

    CoC Reference

    7075-T651 Aluminum Plate

    AMS-QQ-A-250/12

    H-2024-0847

    CoC-2024-0847-A

    AS9102 Form 3 – Characteristic Accountability

    Form 3 is typically the most time-consuming element of FAIR preparation. Each line corresponds to a characteristic from the ballooned drawing.

    Required fields for each characteristic:

    Field

    Description

    Balloon number

    Links to ballooned drawing

    Drawing sheet and zone

    Location reference for multi-sheet drawings

    Characteristic description

    “Bore OD,” “Thread M10x1.5,” “Flatness of seating surface”

    Specification or tolerance

    Nominal dimension with tolerance band

    Key characteristic designator

    KC, CC, or standard feature

    Inspection method

    CMM, micrometer, visual, functional test

    Measured result

    Actual numerical value or attribute result

    Gage ID

    Traceable to calibration records

    Acceptance status

    Accept, reject, or conditional

    Characteristics are recorded as either attribute data (pass/fail for thread presence) or variable data (numerical measurement for bore diameter). Using the correct data type ensures accuracy and supports process control.

    Inspection methods may include CMM, hand tools (micrometers, calipers), optical comparators, calibrated tools, or automated scanning equipment. Gage ID and calibration state must be traceable to ISO 17025 labs where applicable.

    Manual Form 3 population using spreadsheets is error-prone. Connect981 can ingest CMM output files and auto-fill inspection results linked to balloon IDs, reducing transcription errors and preparation time.

    Raw Material and Dimensional Records in FAI

    Material and dimensional integrity together determine whether the first article is acceptable and reliable in service. Both require rigorous documentation.
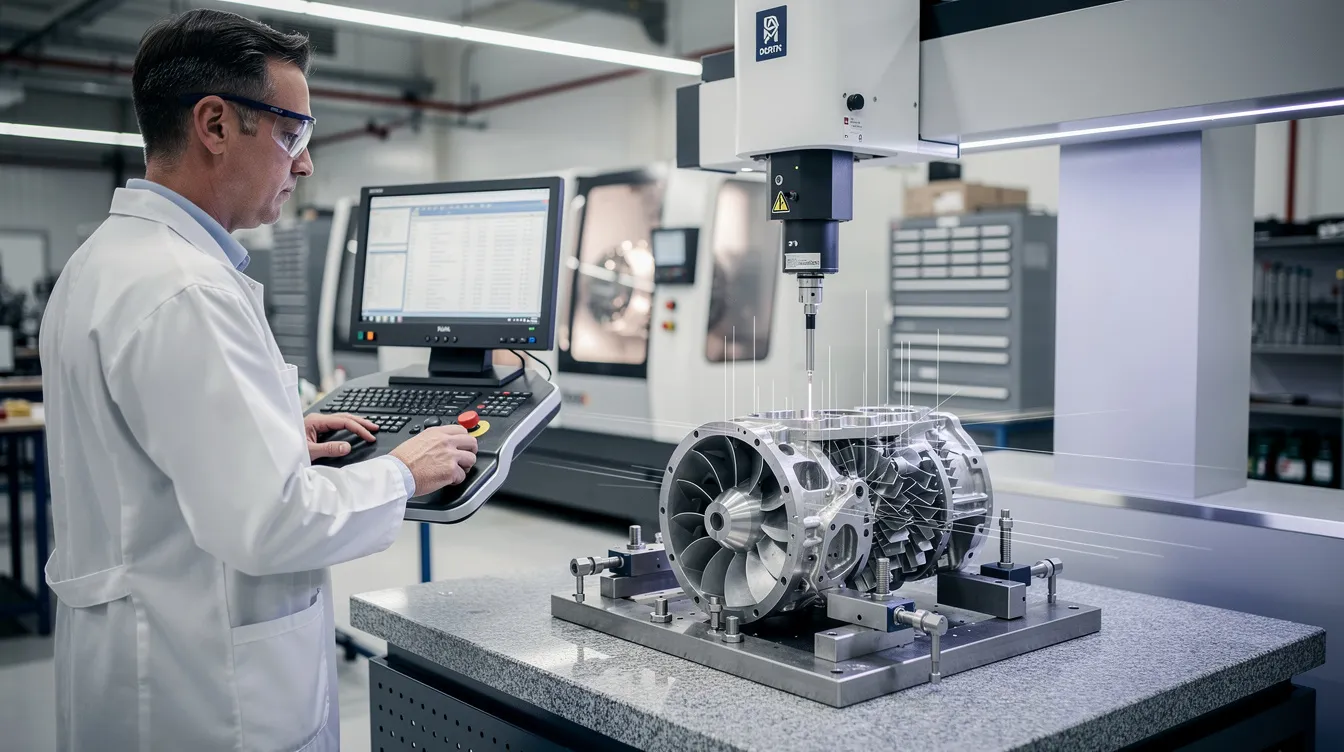
    A quality inspector is using a coordinate measuring machine to perform a first article inspection on an aerospace component, ensuring that it meets the specified design requirements and quality standards. This inspection process is crucial for maintaining product reliability and customer confidence in the aerospace industry.

    Raw material record requirements:

    • Mill test reports documenting chemical composition and mechanical properties
    • Certificates of conformance from material suppliers
    • Traceability to heat lot numbers and purchase orders
    • For critical materials (titanium forgings, composite prepreg), complete mechanical test data

    Aerospace-specific scenarios demand heightened traceability. Titanium forgings for engine mounts require heat lot documentation linking specific material to the first article serial number. Composite prepreg materials have shelf-life limitations requiring lot tracking to ensure out-of-life material is not incorporated.

    Dimensional record requirements:

    • 100% of dimensions on the drawing for FAI
    • GD&T features including flatness, position, runout, and perpendicularity
    • Surface finish measurements where specified
    • Thread verification using appropriate gages

    Common measurement tools in aerospace FAI:

    Tool Type

    Application

    CMM

    Complex geometry, GD&T features, high-precision dimensions

    Portable arms

    Large parts, field measurements

    Laser scanners

    Complex surfaces, rapid data capture

    Pin gages

    Go/no-go verification of holes

    Thread gages

    Pitch and major diameter verification

    Hardness testers

    Material property verification per spec

    Dimensional records must include gage IDs and calibration due dates. Inadequate metrology control is a frequent audit finding. A gage out of calibration at time of measurement can invalidate FAI results for that characteristic.

    The cluster article on FAI traceability explores how raw material, process, and dimensional records tie into serialized part histories over an aircraft’s service life.

    Operational Execution: The FAI Workflow in Aerospace

    The FAI workflow spans multiple functions and requires coordination between quality, manufacturing engineering, supply chain, and the customer. Understanding the operational sequence reduces cycle time and prevents rework.

    Planning phase activities:

    • Review contract and purchase order quality clauses to confirm FAI scope
    • Identify OEM-specific FAIR format or submission portal requirements
    • Hold pre-FAI meeting with quality, manufacturing engineering, and supply chain
    • Confirm latest drawing revision and specifications are available

    Manufacturing engineering planning:

    • Develop process routing and machine/tool selection
    • Identify key characteristics and inspection methods
    • Create digital work instructions or travelers specific to FAI build
    • Verify special process approvals are current (NADCAP certifications)

    The first article must be manufactured under normal production conditions using approved programs, fixtures, materials, and qualified personnel. FAI performed on engineering samples or under special lab conditions does not validate the actual production process.

    Inspection and documentation execution:

    • Balloon the drawing with unique characteristic identifiers
    • Execute dimensional, material, and functional tests per inspection plan
    • Capture results with full traceability: gage IDs, calibration status, inspector identification
    • Document any nonconformances and link to corrective actions

    Review and approval sequence:

    • Internal quality review for accuracy and completeness
    • Customer or delegated representative submission
    • Response to clarification requests within required timeline
    • Final sign-off before rate production release

    Connect981 orchestrates this workflow end-to-end, from digital traveler creation and step-by-step work instructions to automated FAIR compilation and customer portal submission.

    Typical Step-by-Step FAI Process

    This sequential checklist reflects what quality and manufacturing engineers execute during a complete FAI:

    1. Confirm FAI requirement and scope: Review PO quality clauses and determine full, partial, or delta FAI type
    2. Gather latest design data: Obtain current drawing revision, 3D model, specifications, and engineering change notices
    3. Balloon the drawing/model: Assign unique identifiers to every characteristic per customer conventions
    4. Define inspection methods and sampling: Specify gages, CMM programs, and measurement approach for each characteristic
    5. Schedule and build the first article: Execute manufacturing plan using standard production processes and qualified personnel
    6. Perform inspections and tests: Measure all characteristics, conduct functional tests, verify material properties
    7. Compile AS9102 Forms 1–3: Populate all fields with full traceability to gages, materials, and processes
    8. Attach supporting documents: Include CoCs, process certifications, test reports, and any nonconformance records
    9. Internal review and sign-off: Independent verification by quality engineer or supervisor
    10. Customer submission and response: Transmit FAIR via agreed method and respond to questions within timeline
    11. Archive FAIR and link to work orders: Store approved FAIR with connection to serial numbers and purchase orders

    Coordination touchpoints occur at planning (scope agreement), mid-build (observation of critical steps), and review (internal verification before customer submission). Any nonconformances discovered during FAI must be documented with corrective actions, even if the FAIR is approved with concessions.

    Delta FAI and Partial FAI in Practice

    Delta and partial FAIs avoid redoing a full first article inspection when only limited changes have occurred. Both maintain compliance while reducing redundant work.

    Partial FAI focuses only on characteristics affected by a change. For example, if drawing Rev B changes only two bore diameters and a tapped hole position, the partial FAI measures only those three features while referencing the prior full FAIR for unchanged characteristics.

    Delta FAI is a customer- or OEM-defined variation used when:

    • Production transfers between facilities (Wichita to Montreal)
    • Tooling relocates to new equipment
    • Previously approved processes are updated within defined tolerances

    Documentation expectations for both types:

    Requirement

    Partial FAI

    Delta FAI

    FAIR type statement

    “Partial” clearly stated

    “Delta” per OEM definition

    Original FAIR reference

    Required

    Required

    Scope definition

    Changed characteristics only

    Facility/equipment changes

    Supporting evidence

    Process documentation for changes

    Equipment qualification records

    Concrete example: Moving a machining operation from Plant A to Plant B in 2027 would trigger a delta FAI capturing facility-related changes while referencing the original FAIR from the initial production baseline.

    Connect981 versions FAIRs, tracks lineage between full and partial/delta FAIs, and presents a clear audit trail for regulators and customers.

    Common FAI Workflow Challenges and Errors

    FAI failures often stem from preventable documentation and process errors rather than fundamental manufacturing problems. Understanding these risks helps organizations avoid costly errors and customer rejections.

    Documentation issues:

    • Using outdated drawings or engineering documentation (revision mismatch)
    • Inconsistent characteristic numbering between ballooned drawings and Form 3
    • Missing revision updates or engineering change notices
    • Incomplete attachment of required certificates and test reports

    Metrology and data errors:

    • Mis-typed numeric results when transcribing from CMM reports to FAIR forms
    • Incomplete gage ID fields or missing calibration evidence
    • Misuse of attribute versus variable data for critical dimensions
    • Measurement results recorded without units or tolerance context

    Process-related problems:

    • Performing FAI on engineering samples that do not represent actual production process
    • Skipping required special process approvals before FAI build
    • Manufacturing under non-standard conditions (different fixtures, unqualified personnel)

    Communication gaps:

    • Unclear FAI scope communicated between OEM and supplier
    • Customer-specific FAIR formats not shared early in program
    • Late change notices during FAI builds causing scope confusion
    • Delayed responses to customer clarification requests

    The cluster article on common FAI errors presents a detailed checklist of avoidable mistakes and detection methods before customer submission.

    Platforms like Connect981 reduce these errors through enforced templates, automated data import from CMM systems, validation checks before submission, and a single source of truth for drawing revisions.

    Traceability and Record Retention for FAI

    Traceability is central to aerospace safety cases and explains why FAI is so documentation-intensive. The FAIR creates an unbroken chain connecting manufactured parts to their materials, processes, and verification records.

    FAI records connect:

    • Part serial numbers or lot numbers
    • Material lots with heat numbers and mechanical properties
    • Special process lots with vendor identification and approval status
    • Inspection results with gage IDs and inspector identification
    • Responsible parties at each manufacturing and verification step

    This chain enables rapid investigation when field issues occur. If a component fails in service, investigators can trace backward from the serial number to the FAI, then to the specific material heat lot, special process vendor, and dimensional verification records.

    Typical retention expectations:

    Context

    Retention Period

    Commercial aerospace

    10+ years, often through aircraft service life (20-40 years)

    Defense contracts

    Program life or indefinite per contract requirements

    Safety-critical components

    Through product lifecycle plus investigation window

    Rapid retrieval capability matters for regulatory audits, customer investigations, and accident analysis. Older revisions and superseded FAIRs must remain accessible even after design updates.

    The risk of scattered PDFs and spreadsheets across network drives creates compliance exposure. Multi-site operations often struggle with FAIR location and version control, particularly after personnel turnover or facility acquisitions.

    Connect981 centralizes FAIR data, links it to work orders and serial numbers, and provides controlled access to OEMs and tiered suppliers via a shared digital layer.

    The cluster article on FAI traceability deep-dives into serial number management, lot tracking, and integration with ERP, MES, and QMS systems.

    Digital Systems and Automation for FAI

    The aerospace industry is transitioning from paper-based FAIs and standalone spreadsheets toward integrated digital workflows. This shift addresses longstanding pain points while maintaining stringent requirements.
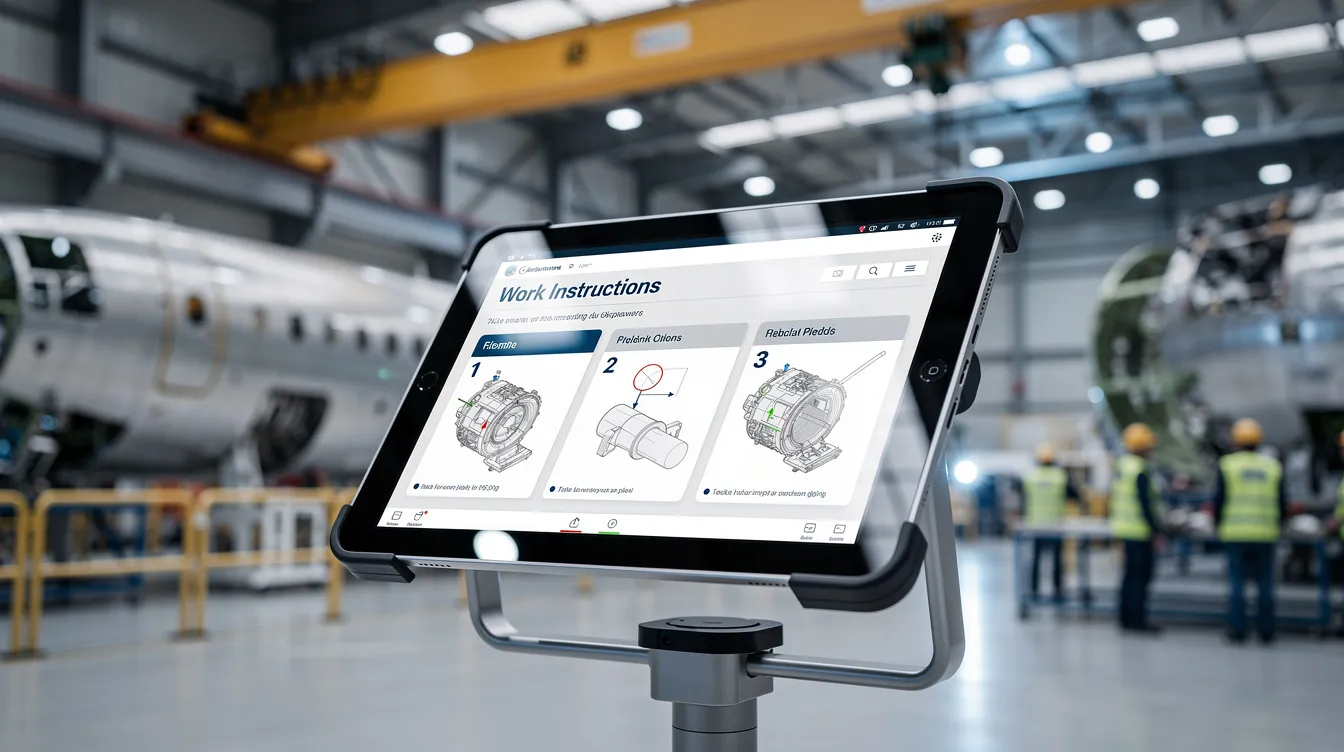
    A digital tablet is positioned on an aerospace manufacturing floor, displaying detailed work instructions related to the first article inspection process. This setup emphasizes the importance of quality control and adherence to specified requirements in the aerospace industry’s production process.

    Common manual pain points:

    • Repeated data entry across inspection logs, spreadsheets, and FAIR forms
    • Inconsistent templates across programs and suppliers
    • Difficulty aggregating CMM output files from different equipment brands
    • Long FAIR cycle times (multiple days per part)
    • High rework rates due to formatting or transcription errors

    Digital FAI capabilities:

    • Automated drawing ballooning and characteristic extraction from CAD/DPD
    • Direct import of CMM and scanner data into Form 3 fields
    • Auto-population of material and process information from MES/ERP
    • Validation checks before submission (missing fields, calibration status)
    • Version control with audit trails

    Integration with MES, ERP, and QMS provides shared part master data, process routings, nonconformance linkage, and document control. This reduces duplication and ensures accuracy between systems.

    Connect981 serves as a unified operations platform that:

    • Provides digital work instructions including FAI-specific steps
    • Captures inspection data at the point of use via mobile devices
    • Links FAIRs to work orders, purchase orders, and supplier records
    • Offers a shared portal for OEM-supplier FAI collaboration with permissioned access

    In aerospace MRO environments, digital FAI systems verify first article repairs or modifications, document new repair procedures, and integrate with maintenance records for product reliability traceability.

    The cluster article on digital travelers and FAI focuses on how digital work instructions and FAIRs work together on a connected shopfloor.

    AI and Analytics in FAI

    Emerging AI and analytics capabilities augment FAI workflows while keeping domain experts in control.

    AI-assisted characteristic extraction from CAD models and engineering drawings reduces manual ballooning time. Machine learning models trained on aerospace drawings can identify features, extract dimensions and tolerances, and propose balloon numbering schemes aligned with customer conventions.

    Advanced analytics on FAIR data across programs and suppliers identifies systemic issues:

    • Recurring nonconformances on specific key characteristics
    • Machines or tooling prone to problems (suggesting calibration drift or wear)
    • Material suppliers with higher nonconformance rates

    Connect981 uses AI-assisted root cause analysis to highlight high-risk features before they fail in FAI or production. Predictive insights flag characteristics similar to historical problem areas for additional review.

    AI augments but does not replace domain experts. Quality engineers, metrologists, and manufacturing engineers retain judgment over design changes, process controls, and supplier qualification decisions.

    Reducing FAI Cycle Time Without Sacrificing Compliance

    FAIs often sit on the critical path for program launches and design changes. A program awaiting FAI approval cannot begin full production run, which delays revenue and may incur customer penalties.

    Typical drivers of long FAI cycle times:

    • Late or unclear requirements from OEMs
    • Fragmented systems (drawings, specs, FAI forms in different locations)
    • Manual data entry and transcription at multiple steps
    • Uncoordinated metrology scheduling
    • Back-and-forth clarifications with customers

    Best practices for acceleration:

    Practice

    Impact

    Early planning and scope confirmation

    Prevents rework from unclear requirements

    Pre-approved templates and conventions

    Reduces formatting questions

    Concurrent inspection planning

    Eliminates metrology scheduling delays

    Digital data capture at point of use

    Eliminates transcription errors

    Integrated FAIR generation

    Cuts preparation time by 75%+

    Digital tools cut FAI turnaround through automated data capture, single-click FAIR generation, integrated approvals, and shared visibility for OEMs and suppliers. Organizations report reducing FAI preparation from 16 hours to 4 hours per part using automated approaches.

    The cluster article on reducing FAI cycle time offers quantitative examples and case scenarios demonstrating specific acceleration strategies.

    FAI in Defense and High-Regulation Contracts

    Defense, space, and safety-critical systems often add requirements beyond standard AS9102 FAI. Understanding these additions prevents compliance gaps on regulated programs.

    Defense-specific FAI requirements:

    • Contract-unique FAI forms replacing or supplementing AS9102 formats
    • Additional review gates with government quality representative involvement
    • DCMA (Defense Contract Management Agency) witness requirements for certain operations
    • Direct linkage between FAI acceptance and payment milestones

    Some defense contracts tie FAI approval to program risk reviews. If the FAI reveals unexpected manufacturing challenges, program risk posture escalates, triggering additional oversight.

    ITAR and export control implications:

    FAI data including drawings, 3D models, and FAIRs may be controlled technical data under ITAR or EAR. This means:

    • FAIRs cannot be freely shared with non-U.S. suppliers
    • Foreign nationals may require export licenses for access
    • Digital systems must incorporate access controls and data segregation
    • Audit trails must document who accessed controlled data

    Connect981’s shared yet permissioned environment supports collaborative FAIs on defense programs while respecting data segregation. Access controls, encryption, and user authentication prevent unauthorized access to controlled FAI data.

    The cluster article on FAI in defense contracts addresses these topics with detailed examples including common clauses and flow-down language.

    The Future of Automated and Connected FAI

    First article inspection will evolve significantly over the next 5–10 years as model-based definition and automated metrology become standard across the aerospace industry.

    The image depicts a modern automated manufacturing cell featuring advanced robotic inspection equipment, designed for the inspection process in the aerospace industry. This setup is crucial for ensuring product reliability and adherence to stringent quality control requirements during the first article inspection process.

    Model-Based Definition (MBD) and Digital Product Definition:

    MBD embeds all design intent, tolerances, and annotations in 3D CAD models. This enables:

    • Direct-to-CAD FAI without reliance on 2D drawings
    • Automatic characteristic extraction for ballooning
    • CMM software reading tolerance data directly from models
    • Reduced manual interpretation and ensure accuracy

    Automated metrology trends:

    • Robotic CMM cells performing hands-off measurement
    • Inline 3D scanners feeding directly into FAIR generation
    • Vision-based inspection capturing attribute data automatically
    • High-volume 100% inspection replacing statistical sampling

    Digital thread integration:

    FAI data will increasingly connect to PLM, ERP, MES, QMS, and fleet maintenance systems. This enables:

    • Closed-loop quality: FAI observations feed directly into control plans
    • Lifecycle traceability: FAI linked to serial numbers and maintenance records
    • Continuous improvement: Aggregate FAI analytics identify systemic issues
    • Predictive intelligence: ML models flag high-risk designs before FAI

    Platforms like Connect981 serve as the connective layer between these systems, enabling standardized FAI workflows across global factories and multi-tier supplier networks. Industry standardization of digital FAIR data exchange will reduce proprietary silos and enable easier OEM-supplier collaboration.

    The future state is a scenario where suppliers receive design specifications, automatically generate FAI plans, manufacture with digital work instructions, compile FAIRs from CMM data and material certifications, submit via digital portal, and receive approval within days rather than weeks.

    Organizations that standardize FAI workflows reduce cycle time, cut costly errors, and maintain customer confidence through audit-ready documentation. The path forward requires evaluating current FAI maturity, identifying manual bottlenecks, and adopting digital tools that integrate with existing systems.

    Connect981 enables aerospace manufacturers and suppliers to modernize their FAI process without replacing ERP or MES infrastructure. Request a demo to see how digital FAI workflows can work for your next project.
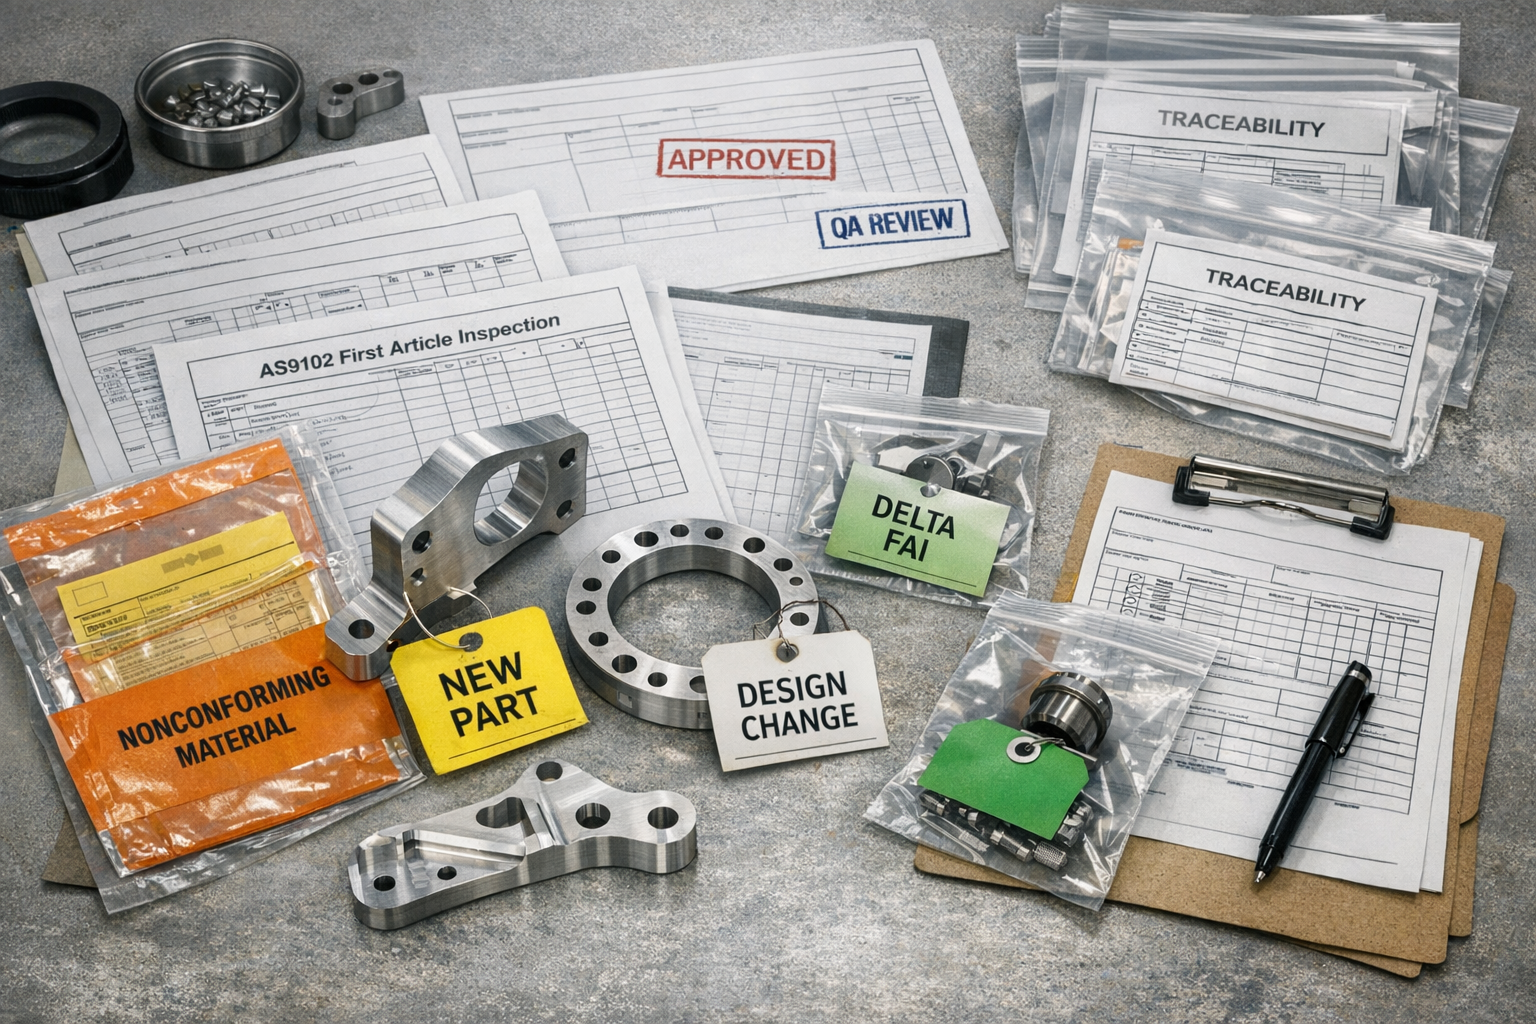
  • AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    In aerospace manufacturing, one of the most common quality questions is not what AS9102 first article inspection is, but when it is actually required. Teams know first article inspection matters. They know customers expect a compliant FAIR. What causes real friction is deciding whether a situation calls for a full FAI, a partial FAI, or no new FAI at all.

    That decision matters because unnecessary first article work slows production, ties up quality resources, and adds documentation overhead. On the other hand, missing a valid trigger can create customer escapes, audit findings, approval delays, and serious traceability problems. In aerospace, where configuration control and product conformity carry real operational and regulatory weight, getting this right is not optional.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains the most important AS9102 FAI triggers, including new part introduction, engineering changes, process changes, production lapses, and the circumstances that justify a partial or delta FAI rather than a full reset. It also looks at how aerospace manufacturers can manage these triggers more consistently using connected digital workflows.

    If you want the broader foundation first, review AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

    What AS9102 FAI Is Designed to Prove

    AS9102 first article inspection is a structured method for verifying that a production process can manufacture a part or assembly that fully conforms to engineering, specification, and purchase order requirements at the released configuration. It is not just a sample inspection. It is not a one-time paperwork exercise. It is a formal record that shows the part definition was interpreted correctly, the process was executed properly, and the evidence of conformity is complete and traceable.

    In practice, an FAI helps answer a straightforward but high-stakes question:

    Can this exact aerospace production process, at this exact released configuration, produce conforming hardware with full documented accountability?

    That is why FAI sits so close to configuration control, traceability, launch readiness, supplier quality, and customer approval. It creates a documented baseline that can later support change management, resubmissions, investigations, and audits.

    Why Knowing the Right Trigger Matters

    Plenty of aerospace organizations understand how to complete Form 1, Form 2, and Form 3. Fewer have a disciplined internal method for deciding when a new or updated FAI is required. That is where problems begin.

    If the trigger logic is weak, teams end up doing one of two things. They either over-trigger, which creates waste and slows down manufacturing, or they under-trigger, which creates risk. Neither outcome is good. The first hurts efficiency. The second hurts compliance, customer trust, and sometimes product integrity.

    A clear trigger model helps quality and manufacturing teams:

    • Apply AS9102 consistently across programs and part families
    • Reduce unnecessary full FAIR rebuilds
    • Identify when partial or delta FAI is appropriate
    • Align change control with customer and contract expectations
    • Protect traceability when production conditions shift

    Here’s the thing. The cost of poor trigger discipline is rarely visible all at once. It shows up as late package corrections, missing evidence, confused resubmissions, duplicated work, and uncomfortable customer conversations.

    New Part Introduction Is the Most Obvious FAI Trigger

    The clearest AS9102 trigger is the first production run of a new part number or assembly. When an aerospace organization introduces a part into production for the first time, it needs objective evidence that the released design can be built and verified correctly using the intended production process.

    This usually calls for a full FAI because there is no prior approved baseline to rely on.

    What counts as a new part introduction

    New part introduction typically includes:

    • A newly released part number entering production for the first time
    • A new assembly requiring first-time product accountability
    • A part transferred from development or prototype status into controlled production
    • A customer program launch where the released configuration has not yet been formally validated

    In these cases, the FAIR establishes the first documented baseline for the product. That baseline matters later when changes occur, because it gives the organization something traceable to compare against.

    Why aerospace treats this carefully

    In aerospace, new part introduction is not just about proving that one part measured correctly on one day. It is about proving that the released configuration, manufacturing route, inspection method, material traceability, and special process chain all support conformity. That is why the first baseline FAIR often becomes an anchor record for the life of the part.

    Design Changes Often Trigger Full or Partial FAI Activity

    Engineering changes are one of the most common reasons organizations revisit FAI. Not every revision change means the entire FAIR must be rebuilt, but changes that affect requirements, form, fit, function, interfaces, or inspection criteria often require at least a partial or delta FAI.

    Examples of design changes that may trigger FAI

    • Dimensional changes to a feature on the drawing
    • Tolerance changes on an existing characteristic
    • Material specification changes
    • Updated notes affecting finish, marking, or identification
    • Changes to critical, key, or safety-related characteristics
    • Revision changes affecting mating or installation conditions

    The real question is not simply whether the drawing revision changed. The better question is whether the released product definition changed in a way that affects conformity or verification. If it did, the FAI baseline likely needs to be updated.

    When a design change justifies a partial or delta FAI

    If the change affects only certain characteristics rather than the entire part, a partial or delta FAI is often the right choice. That allows the organization to revalidate only the impacted features while preserving the unaffected baseline from the original FAIR.

    This approach is especially valuable in aerospace because programs often evolve slowly through controlled revisions, and rebuilding a full FAIR every time can become needlessly expensive. Still, that efficiency only works if the company has strong revision control and can clearly identify which characteristics were affected.

    Process Changes Can Trigger FAI Even When the Drawing Stays the Same

    One of the biggest mistakes organizations make is assuming that if the drawing did not change, the FAIR does not need attention. In aerospace manufacturing, process changes matter because the product may be the same on paper while the route used to build it has changed in a meaningful way.

    If the process changes in a way that could affect part conformity, a new or updated FAI may be required.

    Common process-related FAI triggers

    • New manufacturing equipment or machine replacement
    • New tooling, fixtures, or program changes
    • Method changes in machining, forming, assembly, or inspection
    • Changes to sequence of operations that affect product outcome
    • Transfer of work between facilities or production cells
    • Changes in outside processing sources for controlled operations

    What this really means is that aerospace FAI is not only about the part definition. It is also about the process definition behind that part. If the way the part is made changes enough to alter risk, the FAIR logic needs to catch up.

    Why process changes matter so much in aerospace

    Aerospace production often involves tight tolerances, special processes, controlled materials, complex routings, and customer-specific source requirements. A machine swap, tooling update, supplier change, or move to a different facility can alter process behavior even if the part number and drawing revision remain identical. That is why smart trigger discipline looks at more than engineering release history.

    Material and Special Process Changes Require Careful Review

    In aerospace, traceability to material and special process evidence is central to FAI integrity. Form 2 exists for a reason. If the source or nature of the controlled inputs changes, organizations need to evaluate whether a new or updated FAI is required.

    Typical material and source changes that may trigger FAI

    • A new supplier for a controlled alloy or raw material
    • A change in material specification or condition
    • A new special process source for plating, heat treatment, NDT, coating, or similar operations
    • A change in approval status or scope of a special process provider
    • A change in process parameters that affects product characteristics

    Some of these may require only partial FAI activity. Others may justify a broader review, depending on the criticality of the change and the customer’s expectations. Either way, they should never be treated as invisible background changes. In aerospace, they are often part of the conformity story.

    Production Lapses Are a Real Aerospace Trigger

    Aerospace manufacturing does not always run at a steady cadence. Many parts are made intermittently. Some programs have long pauses. Some part numbers may go quiet for months or years before restarting. That makes production lapse one of the most important and most overlooked FAI triggers.

    If production has been dormant long enough, organizations may need to review whether the baseline process can still be trusted without refreshed validation.

    Why lapse-based triggers exist

    A long production gap can introduce risk even when the part and process documentation appear unchanged. During the lapse, a lot may have shifted:

    • Operators may have changed
    • Tooling may have worn or been replaced
    • Programs may have been updated
    • Equipment may have been serviced or relocated
    • Suppliers may have changed
    • Inspection methods may have evolved

    That is why production lapse should be treated as a process risk issue, not just a scheduling detail.

    How lapse thresholds are handled

    Many organizations use internal thresholds, customer requirements, or contract-specific rules to define what counts as a significant lapse. A common reference point is two years, but the right answer always depends on the customer, the product, and the organization’s quality system. The main point is that lapse-based trigger logic should be defined clearly and applied consistently.

    Full FAI vs Partial FAI vs Delta FAI

    One reason AS9102 remains practical in real aerospace operations is that it does not force a full restart every time something changes. Instead, it allows manufacturers to scale the response to the actual scope of impact.

    When a full FAI is usually appropriate

    • First production of a new part number or assembly
    • Major design change affecting broad portions of the part definition
    • Major process change with wide conformity impact
    • No reliable baseline FAIR exists
    • Customer or contract explicitly requires a complete new FAIR

    When a partial or delta FAI is often the better choice

    • Only selected characteristics changed
    • A limited process change affected a defined subset of features
    • Material or source changes affected traceability but not the full configuration
    • The baseline FAIR remains valid for unaffected requirements

    The discipline here is simple to say but harder to execute: revalidate what changed, preserve what did not, and document the logic clearly.

    Why organizations struggle with delta FAI

    Delta FAI sounds efficient, and it is, but only when the underlying data is structured well enough to support it. If characteristics are trapped in static spreadsheets, traceability is fragmented, or revision history is unclear, teams often end up redoing far more than necessary. In those environments, delta FAI becomes confusing because nobody can cleanly separate affected from unaffected requirements.

    Customer-Specific Requirements Still Matter

    AS9102 gives aerospace manufacturers a standard framework, but it does not erase customer-specific expectations. Many primes and upper-tier suppliers apply additional rules around when FAI is required, what counts as a significant change, how lapse thresholds are handled, and what submission format is acceptable.

    That means the right internal question is never only:

    What does the standard allow?

    It also needs to be:

    What did the customer contract, purchase order, or program requirement actually ask for?

    This matters because a technically defensible partial FAI may still be rejected if the customer expects a full resubmission package, specific portal workflow, or extra supporting documentation.

    Common Mistakes Aerospace Teams Make with FAI Triggers

    Most FAI trigger failures come from poor process visibility rather than bad intent. Teams are busy, systems are disconnected, and changes are sometimes managed in silos.

    Typical mistakes include

    • Treating revision changes as administrative without checking affected characteristics
    • Ignoring process changes because the drawing stayed the same
    • Missing lapse-based triggers on low-volume or intermittent parts
    • Failing to assess source changes for material or special processes
    • Overusing full FAI because delta logic is too hard to manage manually
    • Assuming one customer’s interpretation applies to every program

    The result is usually one of two ugly outcomes. Either the organization creates a lot of unnecessary quality work, or it ships with weaker evidence than the customer expects. Neither is a good place to be.

    How Digital Systems Make FAI Trigger Decisions Easier

    Digital FAI platforms are at their best when they do more than produce forms. They should help aerospace manufacturers manage trigger logic as part of a connected quality and manufacturing workflow.

    What a strong digital workflow can do

    • Maintain a traceable baseline FAIR by part number and revision
    • Track changes to characteristics, materials, and process routes
    • Highlight which features were affected by a revision or process update
    • Support partial or delta FAI generation without recreating everything
    • Connect Form 1, Form 2, Form 3, ballooned drawings, and certifications in one record set
    • Preserve audit history around why a given trigger decision was made

    That last point matters more than people think. In aerospace, it is not enough to make the right trigger decision. You often need to show later why that decision was reasonable.

    Why this matters for Connect 981-style operations

    Connected platforms are especially useful in regulated manufacturing because they reduce the gap between engineering changes, manufacturing process shifts, and quality documentation. Instead of waiting for someone to notice a trigger manually, the system can support earlier visibility into what changed and what evidence may need to be refreshed.

    That does not replace engineering judgment. It makes that judgment more consistent, more traceable, and less dependent on memory.

    How to Build a Better Internal FAI Trigger Policy

    Every aerospace manufacturer should define a practical internal trigger policy that aligns with AS9102, customer requirements, and real production conditions. The best policies are not vague. They are specific enough that quality, manufacturing, and engineering teams can use them without guesswork.

    A strong internal policy should define

    • What counts as a new part or first production run
    • What kinds of design changes trigger full, partial, or delta FAI
    • What kinds of process changes require review
    • How material and special process source changes are evaluated
    • What lapse threshold applies by default
    • How customer-specific rules override standard internal logic
    • Who has authority to approve the trigger decision
    • How that decision is documented for future audit or customer review

    Without this, organizations tend to rely too heavily on tribal knowledge. That works until the key person is out, the program changes hands, or the customer starts asking harder questions.

    Final Takeaway

    AS9102 FAI triggers are not just a compliance detail. They are part of how aerospace manufacturers control change, preserve traceability, and protect confidence in the production process. New parts, engineering changes, process shifts, material source changes, and production lapses can all justify a new or updated FAIR. The real challenge is knowing when a full FAI is necessary and when a partial or delta FAI is the smarter, defensible path.

    The organizations that handle this well do not treat FAI as a last-minute quality document. They treat it as part of a connected operational system that links engineering, production, inspection, and customer requirements. That is where the real efficiency shows up, and it is also where the strongest compliance posture comes from.

    To go deeper into digital workflows, FAIR structure, and connected aerospace quality execution, read AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

  • The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    First article inspection (FAI) is no longer just a stack of AS9102 forms checked before releasing a new aerospace part to production. Over the next few years, FAI will sit at the intersection of model-based definition (MBD), AI-assisted analytics, and the broader aerospace digital thread that connects design, planning, execution, and in-service data. Teams that still treat FAI as an isolated paperwork exercise will struggle to keep pace with program complexity and customer expectations.

    This article explores how digital FAI is evolving, and what quality, manufacturing, and engineering leaders should expect from the next generation of AS9102 software. It builds on foundational concepts from AS9102 software for digital first article inspection, and looks ahead to how MBD, AI, and connected factory systems will reshape day-to-day workflows.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    From 2D Drawings to Model-Based Definition (MBD)

    Most aerospace organizations still anchor FAI on 2D drawings and PDF packages, even when design authority already maintains a full 3D model. That gap creates redundant work: engineers translate 3D intent back into 2D, then FAI teams balloon the drawing and re-enter characteristic data into AS9102 forms.

    What MBD and PMI Mean for FAI

    Model-based definition (MBD) moves the authoritative product definition into the 3D model itself. Dimensions, geometric tolerancing (GD&T), surface finishes, and notes are captured as product manufacturing information (PMI) attached directly to model features. For FAI, that means:

    • The 3D model becomes the primary source for characteristic extraction, not a downstream 2D derivative.
    • Balloon numbers and Form 3 rows can be generated from PMI tags rather than from optical character recognition on a PDF.
    • Design changes propagate through PLM-managed models in a controlled way, reducing the risk of using the wrong revision during FAI.

    In a mature digital thread, AS9102 software consumes PMI-rich models via PLM or CAD integrations, creating structured characteristic records without manual re-interpretation of 2D views.

    Extracting Characteristics Directly from 3D Models

    As MBD adoption increases, the logical next step is for FAI tools to extract measurable requirements directly from 3D geometry and PMI. In practice, this looks like:

    • Loading a native CAD or neutral MBD format, then parsing PMI to identify all verifiable dimensions, GD&T frames, and notes.
    • Assigning unique characteristic IDs that map one-to-one to Form 3 rows and can be reused across builds, delta FAI, and future programs.
    • Providing 3D navigation from each characteristic to its associated feature, making it easier for inspectors and CMM programmers to understand intent.

    Compared with PDF-based ballooning, 3D extraction improves consistency and reduces interpretation errors, especially for complex structures and tight GD&T schemes. It also aligns FAI more closely with how CMM and metrology software already operate in many aerospace factories.

    Challenges in Transitioning from 2D-Centric Processes

    Moving FAI workflows from 2D drawings to MBD is not just a tooling change; it is an organizational shift. Common challenges include:

    • Mixed-revision environments: Some parts are fully MBD, others remain drawing-centric, and FAI teams must support both simultaneously.
    • Standards and customer expectations: Customers may still specify 2D drawing deliverables or have not formally approved model-based FAIRs as a primary reference.
    • Skills and training: Inspectors and quality engineers may be less comfortable navigating 3D PMI than reading traditional blueprints.

    A pragmatic approach is to run hybrid pilots: use MBD-derived characteristics as the internal source of truth but still generate AS9102-compliant forms and, where needed, drawing-based views for customer submission. Over time, as standards and customer practices evolve, organizations can phase out redundant 2D work.

    AI and Automation in FAI Data Analysis

    AI is often oversold as a push-button solution that will replace engineering judgment. In regulated aerospace manufacturing environments, that is neither realistic nor desirable. The more practical direction is AI and analytics augmenting human decision-making: guiding where to focus attention, checking FAIRs for inconsistencies, and surfacing patterns that would be hard to see manually.

    AI-Assisted Risk-Based Sampling Approaches

    Risk-based inspection is already established in aerospace quality systems; what changes is the data and tooling that inform those decisions. Emerging AS9102 software capabilities include:

    • Using historical FAIRs and in-process inspection results to estimate process capability for families of parts and operations.
    • Suggesting when 100% measurement is warranted (e.g., new suppliers, unstable processes, safety-critical characteristics) versus when statistically justified sampling is appropriate.
    • Highlighting characteristics with marginal capability or frequent near-miss conditions so engineers can tighten sampling or adjust control plans.

    Importantly, these AI-assisted recommendations should be transparent and overrideable. Quality leaders remain responsible for approving inspection strategies; the system provides context, not commands.

    Anomaly Detection in Measurement Data

    FAI results often sit in a repository until an audit or customer issue forces a review. Anomaly detection changes that by scanning results as they are recorded. Typical use cases include:

    • Flagging unusual distributions, such as one dimension consistently trending toward a tolerance limit across multiple builds.
    • Identifying inconsistent units, extreme outliers, or patterns that suggest transcription errors.
    • Surfacing systematic offsets that hint at fixture, probe, or program issues, before they propagate across a fleet of parts.

    Because AI models can misinterpret rare yet valid data, anomaly alerts should be reviewed by engineers who can confirm whether the pattern reflects a true process issue or expected variation. The value lies in earlier visibility, not automatic disposition.

    Automated Validation of FAIR Completeness and Consistency

    One of the most immediate AI-adjacent wins is rule-based and statistical validation of FAIRs before submission. Advanced AS9102 tools can:

    • Check that every ballooned or PMI-derived characteristic appears exactly once on Form 3.
    • Verify that material certs and special process records are attached for all relevant Form 2 entries.
    • Confirm unit consistency, tolerance format, and revision alignment across Forms 1, 2, and 3.

    Much of this can be implemented today with deterministic rules, complemented by AI models that learn typical patterns for a program or supplier and highlight deviations. The result is fewer customer rejections and less manual rework on incomplete FAIRs.

    FAI as a Node in the Aerospace Digital Thread

    Historically, FAI data stayed within the quality function. In a digital thread architecture, first article inspection becomes a key node linking design, process planning, production execution, and in-service performance. That shift turns FAIRs from static evidence into a rich source of engineering, sourcing, and operations intelligence.

    Connecting Design, Planning, Production, and In-Service Data

    In a connected aerospace manufacturing environment, AS9102 software does not operate alone. It exchanges data with PLM, MES, ERP, and maintenance information systems:

    • Design: PLM supplies the authoritative model or drawing, change history, and configuration rules.
    • Planning: Process plans and operation sequences flow from manufacturing engineering tools into the FAI context.
    • Production: MES links FAIRs to specific work orders, machines, tools, and operators.
    • In service: Maintenance and reliability systems can reference original FAI data when investigating recurring issues.

    When these connections are in place, the FAIR becomes a snapshot of how a particular configuration was realized at a moment in time, fully traceable back to design intent and forward to field performance.

    Using FAI Results to Refine Tolerances and Manufacturability

    First article results often reveal whether a design is realistically manufacturable with the intended processes and suppliers. By aggregating FAI data across parts and programs, engineering teams can:

    • Identify features that repeatedly push process capability limits or require excessive rework.
    • Highlight tolerances that are unnecessarily tight relative to functional needs.
    • Feed evidence-based feedback into design for manufacturability (DFM) guidelines and design standards.

    This turns FAI from a compliance gate into a feedback loop: design decisions are informed by past production reality, reducing ramp-up friction on future programs.

    Linking Certifications and Process Data to Maintenance Records

    For long-life aerospace platforms, the ability to trace from an in-service serial number back to its initial FAI and associated certifications is increasingly important. In a robust digital thread:

    • Each FAIR is indexed by part number, serial, lot, and configuration.
    • Material and special process records attached to Forms 1 and 2 are stored as structured data, not just PDFs on a shared drive.
    • Maintenance events in fleet management systems can link back to the original FAIR to investigate whether initial variability correlates with field performance.

    This level of linkage requires disciplined configuration management and common identifiers across systems, but it pays off in faster root-cause analysis and more targeted corrective actions.

    Supplier Collaboration and Real-Time Portals

    Aerospace primes are increasingly pushing digital requirements into their supply base: structured FAIRs, standard templates, and near-real-time visibility into inspection status. The future of digital FAI will depend as much on supplier collaboration as on internal factory systems.

    Shared FAIR Templates and Live Status Visibility

    Instead of each supplier maintaining its own spreadsheet templates, modern platforms provide shared, controlled AS9102 formats via secure portals. Capabilities typically include:

    • Prime-defined templates that enforce mandatory fields, revision usage, and customer-specific clauses.
    • Real-time visibility into FAIR status across suppliers: not started, in progress, submitted, under review, or approved.
    • Standardized data structures that make downstream analytics (e.g., across suppliers or commodity groups) feasible.

    This reduces interpretation errors and ensures that when data reaches the OEM, it is already compatible with their systems and reporting needs.

    Reducing Rework and Clarification Cycles with Primes

    Much of the delay and friction around FAI comes from back-and-forth clarification: missing attachments, ambiguous dimension coverage, or questions about process changes. Digital collaboration environments help by:

    • Embedding validation rules and checklists that suppliers must pass before submission.
    • Providing structured comment threads tied to specific characteristics or documents.
    • Maintaining a single source of truth for each FAIR, rather than multiple email chains and file versions.

    The outcome is fewer rejected FAIRs, more predictable lead times, and better use of both supplier and OEM engineering capacity.

    Security, IP Protection, and Access Control Considerations

    As more design and inspection data flows through shared portals, protecting intellectual property and regulated information becomes critical. Future-ready FAI platforms must support:

    • Granular access control down to part families, programs, or specific FAIRs.
    • Encryption in transit and at rest, with clear segregation between customers and suppliers.
    • Audit trails showing who accessed or modified data, when, and from where.

    Aerospace organizations should evaluate not only functional capabilities but also how FAI tools align with IT security policies, export control requirements, and customer data handling clauses.

    Preparing Your Organization for the Next Generation of FAI

    Transitioning to AI-enabled, MBD-driven FAI will not happen overnight. Organizations need to understand their current maturity, set realistic priorities, and align technology decisions with standards evolution and customer roadmaps.

    Assessing Current Digital Readiness

    A practical first step is a structured assessment of how FAI is executed today:

    • What proportion of FAIRs are created manually in spreadsheets versus via dedicated AS9102 software?
    • How frequently are 3D models with PMI available, and how are they used today?
    • Which systems hold critical FAI-related data (PLM, MES, ERP, QMS), and how well are they integrated?

    Documenting this baseline helps identify where digital upgrades will have the most immediate impact: reducing rework, shortening lead time, or improving audit readiness.

    Prioritizing Capabilities to Invest in First

    Not every organization needs cutting-edge AI on day one. For many aerospace manufacturers, the highest-value early investments are:

    • Reliable digital ballooning and characteristic extraction from drawings or models.
    • Structured AS9102 forms with built-in validation and revision control.
    • Centralized storage and search for FAIRs, certs, and supporting documents.

    Once those foundations are in place, teams can layer on analytics, anomaly detection, and deeper integration with MES and PLM. Attempting advanced capabilities without a stable data foundation usually leads to frustration.

    Building a Roadmap That Aligns with Standards Evolution

    AS9102, AS9100, and customer-specific requirements will continue to evolve as digital practices mature. A useful roadmap:

    • Maps target capabilities (e.g., MBD-based FAI, supplier portals, AI-assisted checks) against planned system upgrades and program milestones.
    • Identifies standards or customer guidance that may affect when certain practices are accepted (for example, model-based submissions).
    • Includes governance for how FAI processes are updated as standards or internal procedures change.

    The goal is to avoid one-off tool deployments and instead build a coherent, long-term path toward connected, data-centric FAI.

    Practical Steps to Experiment with Advanced FAI Capabilities

    Many aerospace teams want to explore advanced digital FAI but are constrained by active programs, existing contracts, and limited engineering bandwidth. Small, well-scoped pilots can prove value without disrupting ongoing delivery.

    Pilot Projects Using MBD-Derived Characteristics

    For programs where the design authority already maintains MBD, consider a pilot that:

    • Uses a limited set of parts to trial PMI-based characteristic extraction into the FAI system.
    • Compares time and error rates against traditional 2D ballooning.
    • Engages both design and quality teams to refine how PMI is structured for inspection use.

    Lessons from this pilot can inform modeling practices, internal standards, and supplier training before rolling out model-based FAI more broadly.

    Using Analytics on Existing FAIR Data

    Even without new measurement equipment or AI models, most organizations have years of FAIRs that are underutilized. A straightforward analytics initiative might:

    • Normalize existing FAIR data into a common structure, even if it began as spreadsheets.
    • Visualize where FAI rejections, late approvals, or near-miss dimensions cluster by part family, supplier, or process.
    • Feed those insights into process improvement projects or design guidelines.

    This kind of work builds the data literacy and governance needed before deploying more advanced anomaly detection or risk-based sampling algorithms.

    Partnering with Software Providers on Roadmap Features

    Given the pace of change around the digital thread and AI, no single vendor will have every capability fully mature today. Aerospace manufacturers can shape solutions by:

    • Participating in customer advisory boards focused on MBD, AS9102 Rev C interpretation, and supplier collaboration.
    • Co-designing pilot features such as AI-assisted FAIR checks or new integration points with PLM and MES.
    • Aligning contracts and deployment plans with clear milestones for advanced capabilities rather than generic promises.

    For platforms like Connect 981 that already embed FAI within a broader aerospace operations environment, this collaboration ensures that future enhancements match real engineering and production needs, not abstract technology trends.

    The trajectory is clear: FAI is moving from static documentation toward an integrated, data-rich capability that supports faster new part introduction, tighter process control, and more effective collaboration across the aerospace supply chain. Organizations that invest now in solid digital foundations—structured AS9102 data, integration with core systems, and disciplined configuration management—will be best positioned to take advantage of MBD and AI as they mature.