Tag: Cost of poor quality

  • Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Aerospace manufacturers and suppliers rarely question whether they must comply with AS9102. The real question is whether they can continue to absorb the time, risk, and opportunity cost of manual first article inspection (FAI) processes.

    Digital AS9102 software promises shorter cycle times, fewer errors, and cleaner audits. To win budget and executive support, those promises must be translated into a clear, defensible business case with tangible financial impact.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This guide provides a structured way to quantify the return on investment (ROI) of AS9102 software. You will learn which metrics to track, how to model savings, and how to align your case with quality, operations, and IT stakeholders. For a broader view of capabilities and architecture, see our unified AS9102 and digital FAI platform overview.

    Why AS9102 FAI Is a High-Leverage Improvement Area

    FAI sits at the intersection of engineering, quality, operations, and customer delivery. That makes it one of the highest-leverage processes to digitize: small improvements compound across programs, plants, and suppliers.

    Engineering time consumed by manual FAIRs

    In many aerospace organizations, quality and manufacturing engineers spend a surprising portion of their time on manual first article inspection reports (FAIRs):

    • Hand-ballooning multi-sheet drawings with hundreds of characteristics
    • Copying data into spreadsheet-based Forms 1, 2, and 3
    • Chasing material certs, special process documentation, and signatures
    • Reworking rejected FAIRs from customers or internal approvers

    For complex parts, a single full FAIR frequently consumes 8–24 hours of engineering time. If you produce dozens or hundreds of FAIRs per year, the labor cost and capacity impact become substantial.

    Impact of FAI delays on deliveries and cash flow

    FAI is often on the critical path for first deliveries and engineering changes. When FAIRs run late or are rejected, the impact includes:

    • Delayed shipment of first production lots
    • Slippage in new program milestones and entry into service
    • Deferred revenue recognition and slower cash collection
    • Premium freight or overtime to recover schedule

    Even if the direct cost of an engineer’s time appears modest, the downstream schedule risk can be far more expensive. A credible business case should connect FAI performance to late deliveries and the cost of schedule recovery.

    Hidden costs of rejections and audit findings

    Manual FAIRs are error-prone. Common issues include missed or duplicated balloons, mismatched drawing revisions, incomplete Form 2 documentation, and incorrect tolerance interpretation. These lead to:

    • Customer rejections and resubmissions
    • Internal quality holds while documentation is corrected
    • AS9100 or customer audit findings tied to FAI and traceability
    • Reduced customer confidence and increased oversight

    Digital AS9102 software cannot eliminate all issues, but it can dramatically reduce documentation-related nonconformances. That reduction is a core component of AS9102 software ROI.

    Key Metrics for Evaluating AS9102 Performance

    Before you model ROI, you need a baseline. The following metrics create a clear, quantifiable picture of current performance and provide a way to measure improvement after implementing digital FAI.

    Average time to complete full and delta FAIRs

    Track both engineering and overall calendar time:

    • Engineering effort per FAIR (hours of quality/manufacturing engineering)
    • Elapsed cycle time from trigger to approved FAIR (days)
    • Separate values for full vs. delta FAI

    Suggested approach:

    1. Select a representative sample (e.g., last 20–50 FAIRs across key programs).
    2. Capture effort from time sheets, issue trackers, or quick engineer estimates.
    3. Record dates for FAI trigger, initial submission, rejection (if any), and final approval.

    This baseline is essential for modeling time savings from automated ballooning, form population, and streamlined approvals.

    FAIR rejection and rework rates

    Next, examine quality and completeness of your FAIRs:

    • Percentage of FAIRs rejected by customers or internal approvers
    • Average number of resubmission cycles per FAIR
    • Primary reasons for rejection (documentation vs. product nonconformance)

    Digital FAI primarily affects documentation-related rejections: missed characteristics, mismatched revisions, missing certs, or inconsistent use of AS9102 Forms 1, 2, and 3. Categorizing issues lets you estimate how much rework digital tools can realistically reduce.

    Late deliveries attributable to FAI

    Where possible, identify how often FAI is a direct or contributing cause of late delivery:

    • Number of shipments delayed due to incomplete or rejected FAIRs
    • Average days of delay when FAI is the primary cause
    • Estimated cost of delay (expedite costs, penalties, or internal recovery spend)

    This data is often spread across ERP notes, program reviews, and customer complaints. Even directional estimates (e.g., 5–10 orders per year delayed primarily due to FAIRs) can materially strengthen your business case.

    Estimating the ROI of AS9102 Software

    Once you have baseline metrics, you can model ROI using a combination of time savings, quality risk reduction, and audit efficiency. Avoid promising a single precise number; instead, build a conservative, realistic range.

    Modeling time savings per FAIR and annual volume

    A practical way to estimate time savings is to compare current effort with benchmark reductions from digital FAI:

    • Manual baseline: 8–24 engineering hours per full FAIR is common for complex aerospace parts.
    • Digital target range: Many organizations see full FAIR effort drop to 2–6 hours once ballooning and form population are automated.

    Define variables for your model, for example:

    • H_manual_full = average manual hours per full FAIR
    • H_digital_full = expected digital hours per full FAIR
    • H_manual_delta = average manual hours per delta FAIR
    • H_digital_delta = expected digital hours per delta FAIR
    • N_full = number of full FAIRs per year
    • N_delta = number of delta FAIRs per year
    • Blended_rate = loaded hourly cost for engineers (salary + benefits + overhead)

    Then compute annual labor savings:

    Labor_savings = ((H_manual_full - H_digital_full) × N_full
                     + (H_manual_delta - H_digital_delta) × N_delta)
                     × Blended_rate
    

    For example, if you save 6 hours on 150 FAIRs per year at a blended rate of $80/hour, labor savings alone is roughly $72,000 annually.

    Quantifying reduction in customer escapes and audit issues

    Digital AS9102 software helps enforce complete characteristic accountability, correct use of Rev C forms, and traceability to materials and special processes. The impact shows up as:

    • Fewer documentation-related customer rejections
    • Reduced nonconformance costs linked to incorrect or missing FAIRs
    • Lower likelihood of audit findings tied to FAI records

    To model this conservatively:

    1. Estimate your current annual cost of documentation-related FAI issues (extra engineering time, expedited shipments, minor concessions, or penalties).
    2. Apply an improvement factor based on target rejection reduction (e.g., 20–40% reduction in documentation-related rejections).
    3. Include the value of avoided audit findings (e.g., time for root cause analysis, corrective actions, follow-up audits).

    The formula can be framed as:

    Quality_savings = (Baseline_FAIR_issue_cost × Expected_reduction_percentage)
    

    Because these numbers can be sensitive, use ranges and anonymized examples rather than suggesting guaranteed outcomes.

    Factoring in training and implementation costs

    To present a credible ROI, you must subtract real implementation costs:

    • Software license and subscription: annual or multi-year
    • Implementation services: configuration, integrations, data migration
    • Training time: hours spent by engineers and inspectors learning the system
    • Change management: internal project management and process updates

    Define total annualized cost:

    Total_cost = Software_fees + (Implementation_services / Amortization_years)
                 + Training_cost + Internal_project_cost
    

    Then calculate ROI over a chosen period (often 3 years):

    Annual_benefit = Labor_savings + Quality_savings + Audit_savings + Schedule_risk_impact
    ROI = (Annual_benefit - Total_cost) / Total_cost
    Payback_period = Total_cost / Annual_benefit
    

    Present ROI as a range (e.g., 40–120% over three years) to reflect uncertainty in assumptions and acknowledge that actual results depend on baseline maturity and implementation quality.

    Example Before-and-After Scenarios

    Different organizations start from different levels of digital maturity. The business case for AS9102 software looks a bit different if you are transitioning from paper and spreadsheets versus upgrading from a stand-alone ballooning tool.

    Manual spreadsheets vs. stand-alone ballooning tools

    For teams working primarily with paper drawings and Excel forms, moving to a stand-alone FAI tool typically delivers:

    • Time savings: Auto-ballooning and automatic Form 3 population can cut FAIR creation time by more than half.
    • Error reduction: Fewer missed characteristics and better revision control.
    • Documentation consistency: Standard templates aligned with AS9102 Rev C.

    A high-level scenario:

    • Baseline: 10 hours per full FAIR; 100 FAIRs/year.
    • After stand-alone tool: 4–5 hours per full FAIR.
    • Labor savings: 5–6 hours × 100 FAIRs × blended rate.

    This is often the first step for single-site suppliers with limited integration needs.

    Stand-alone tools vs. integrated operations platforms

    Organizations already using point tools may still struggle with disconnected data and duplicate work across ERP, MES, PLM, and QMS. Moving to an integrated aerospace operations platform that embeds AS9102 FAI alongside work instructions and in-process inspections can add:

    • Reduced re-keying of part, revision, and routing data
    • Direct import of CMM and measurement data into Form 3
    • Unified workflows for FAIR approvals, nonconformance management, and change control
    • Analytics spanning FAI, in-process, and final inspection data

    Here, savings come not just from FAI creation time, but also from fewer discrepancies between systems, faster approvals, and better reuse of data for audits and continuous improvement.

    Multi-site standardization and supplier collaboration gains

    For OEMs and large Tier 1 suppliers, the largest ROI often appears when standardizing AS9102 processes across plants and suppliers:

    • Common FAIR templates and workflows across internal sites
    • Supplier portals for submitting FAIRs in a consistent structure
    • Global visibility into FAI status across programs and tiers
    • Centralized management of prime- or customer-specific AS9102 requirements

    Benefits include:

    • Higher throughput per engineer because tools, templates, and expectations are standardized.
    • Lower training overhead for transfers and new hires.
    • Better supplier performance through clear expectations and shared data.
    • Improved audit readiness at both central and site levels.

    While this level of deployment takes more upfront investment, multi-site standardization typically yields compounding benefits over time.

    Aligning the Business Case with Stakeholder Priorities

    A strong AS9102 software business case speaks different languages to different stakeholders. The core ROI model may be the same, but emphasis and messaging should vary.

    Quality and compliance leadership perspectives

    Quality leaders and compliance managers focus on:

    • AS9102 Rev C conformity and correct use of Forms 1, 2, and 3
    • Reduction in customer rejections and concessions due to FAIR issues
    • Audit readiness for AS9100, customer, and regulatory reviews
    • Traceability from ballooned drawing to measurement, material, and process records

    For this audience, highlight:

    • Lower documentation-related nonconformance rates
    • Faster and more confident responses during audits
    • Reusable FAI data for trend analysis and corrective actions

    Operations and program management concerns

    Operations, plant managers, and program leaders care about:

    • On-time delivery and schedule adherence
    • Engineering capacity to support new product introduction and changes
    • Impact of FAI bottlenecks on throughput and WIP
    • Cost of recovery when FAI issues delay shipments

    For them, emphasize:

    • Reduced cycle time for FAIR approvals
    • Fewer late deliveries attributable to FAI
    • More engineering hours available for process improvement and problem-solving
    • Clear dashboards showing FAI status across programs

    IT and digital transformation alignment

    IT and digital transformation teams look for:

    • Alignment with the broader digital thread and data strategy
    • Integration with ERP, MES, PLM, and QMS
    • Security, access control, and audit logging
    • Scalability across sites and suppliers

    Key talking points include:

    • Standards-based data structures for AS9102 FAIRs
    • Available APIs or connectors to existing systems
    • Cloud and on-premises deployment options, as applicable
    • Support for future capabilities like model-based definition and AI-assisted analytics

    Position digital FAI as a building block in a broader smart manufacturing roadmap, not an isolated point solution.

    Practical Steps to Pilot and Scale Digital FAI

    Even with a compelling ROI model, many organizations benefit from a pilot to validate assumptions, build internal champions, and refine processes before full rollout.

    Selecting candidate parts and suppliers

    A good pilot scope is big enough to be meaningful but small enough to manage. Consider:

    • Parts with medium-to-high complexity (100–300 characteristics) where time savings will be visible
    • Programs with active customer engagement and upcoming engineering changes
    • Sites or suppliers that experience repeated FAIR rejections or long cycle times
    • Internal teams that are open to change and willing to provide detailed feedback

    Include both full and delta FAI cases so you can evaluate how the software handles engineering change scenarios.

    Defining success criteria and measurement plans

    Before the pilot starts, agree on success metrics and how they will be measured. Common criteria include:

    • Reduction in average engineering hours per FAIR
    • Reduction in FAIR cycle time from trigger to approval
    • Decrease in documentation-related rejections
    • User adoption and satisfaction (surveys or interviews)

    Set realistic targets (e.g., 30–50% time reduction in the first phase, improving further as teams gain proficiency) rather than assuming best-case numbers from day one.

    Planning phased rollout across plants and programs

    After a successful pilot, expand in phases:

    1. Stabilize the pilot: Address lessons learned, refine templates, and finalize integrations for the initial site.
    2. Extend to similar parts and programs: Roll out to adjacent product families where requirements and workflows are similar.
    3. Expand to additional sites: Standardize governance, training, and configuration management so each new site ramps faster.
    4. Onboard key suppliers: Provide training and support for tiered suppliers to submit FAIRs using your preferred digital process.

    Each phase should have clear objectives, timelines, and owners. Use early phases to build internal case studies and testimonials that support broader adoption.

    Using a Unified Digital FAI Platform as a Strategic Lever

    While any move away from manual spreadsheets will improve FAI efficiency, a unified operations platform that embeds AS9102 within broader aerospace workflows can unlock additional strategic benefits:

    • Consistent application of AS9102 Rev C across programs, plants, and suppliers
    • Centralized control over templates, customer-specific requirements, and change histories
    • Integrated nonconformance and corrective action management tied to specific FAIRs and characteristics
    • Real-time dashboards for FAI throughput, bottlenecks, and audit readiness

    As described in the AS9102 software: digital first article inspection for aerospace manufacturing overview, platforms like Connect 981 treat FAI as one element of a connected aerospace operations environment. That broader context can strengthen your business case, especially for multi-site and prime-level stakeholders.

    Building a Credible, Actionable Business Case

    To summarize, a strong business case for AS9102 software should include:

    • Current-state baseline for FAIR time, rejection rates, and FAI-driven delays
    • Projected time savings based on realistic efficiency ranges
    • Quality and audit impacts framed as risk and cost reductions, not guarantees
    • Implementation and operating costs with transparent assumptions
    • ROI range and payback period, ideally under 18–24 months
    • Stakeholder-specific benefits for quality, operations, and IT
    • Pilot plan with clear success criteria and a phased rollout strategy

    By grounding your proposal in concrete metrics and openly acknowledging assumptions, you can move AS9102 software from a “nice to have” tool to a strategic investment in capacity, compliance, and customer performance.

    The next step is to gather your baseline data, model a conservative ROI scenario, and design a pilot that tests both the technology and the process changes needed for sustainable improvement.
  • Aerospace Scrap Reduction Strategy

    Aerospace Scrap Reduction Strategy

    Scrap in aerospace manufacturing is not a quality problem. It is a margin stability problem. This distinction matters because it determines how organizations respond. Quality problems get assigned to the quality department. Margin stability problems get executive attention.

    In fixed-price and risk-sharing contract structures that have dominated aerospace programs since 2015, every scrapped titanium fitting, every rejected composite panel, and every rework cycle on an engine component comes directly out of program margin. There is no recovery mechanism. The economics are unforgiving: high-value materials, long cycle times, and multi-year build programs like the A320neo, 737 MAX, and F-35 mean that scrap accumulates into substantial financial exposure before leadership recognizes the pattern.

    This article is written from the perspective of someone who has owned scrap numbers at the cell, value stream, and site level. It is not a software pitch. Connect981 appears in this discussion because it serves as an enabling layer for execution and traceability, but the strategy itself is primarily about leadership discipline and systemic prevention. Technology cannot fix governance failures. It can only make good governance faster and more visible.

    The aerospace industry in 2024–2030 faces unprecedented challenges: capacity ramps, supply chain complexity, workforce transitions, and regulatory scrutiny. Organizations that treat scrap reduction as a strategic discipline will protect margin and schedule. Those that treat it as a quality metric will continue to absorb losses they cannot recover.

    Why Scrap Reduction in Aerospace Is Different from Other Industries

    A 1–2% scrap rate in consumer goods manufacturing is a rounding error. In aerospace, that same rate can destroy the economics of a fixed-price contract. A single scrapped part—a machined titanium bulkhead worth $120,000, or a composite wing skin layup after 20+ hours of touch labor—represents capital that cannot be recovered under most contract structures.

    The aerospace sector operates under constraints that make scrap economically devastating in ways other industries do not experience. Regulatory compliance is mandatory, not optional. ITAR and EAR controls govern material handling and documentation. AS9100D and NADCAP accreditation set baseline quality standards for processes like heat treating, chemical processing, and non destructive testing. Federal Aviation Administration and EASA oversight adds another layer. Customer DCMA representatives and prime audits verify adherence. Every scrapped part generates documentation burden in addition to material cost.

    The differentiators that separate aerospace from automotive or consumer goods manufacturing include:

    • Part value: Aerospace components use exotic materials—titanium alloys, Inconel, advanced composite materials—where raw materials alone can exceed $10,000–$50,000 per part before any machining or processing labor.
    • Low volume, high mix: Production runs are measured in hundreds or low thousands, not millions. Learning curve benefits are limited, and every scrapped unit matters.
    • Long qualification cycles: Requalifying a process or supplier after a change can take 12–24 months, making rapid corrections impossible.
    • Configuration-driven builds: Every aircraft and engine has serialized part histories and traceability requirements that mandate precise configuration management.
    • Schedule compounding: A scrapped part does not just cost material. It costs schedule. Missed delivery slots to Boeing or Airbus cascade into line stoppages and contractual penalties across multi-tier suppliers.

    In MRO operations, the stakes are equally high. Engine module rework during a 30–45 day TAT commitment leaves no room for unplanned scrap. Scrapping a high-value rotable asset—a fan blade, a gear, an actuator—during teardown inspection triggers immediate cost exposure and potential AOG situations for the customer.

    Mapping the Economic Impact of Scrap and Rework Across the Value Stream

    The first step in any aerospace scrap reduction strategy is to quantify scrap and rework as economic leakage, not just as PPM or percentage of pieces. Traditional quality metrics obscure the true impact. A part family with 2% scrap looks acceptable until leadership learns that 2% represents $1.8 million in annual material cost plus another $600,000 in touch labor and MRB processing.

    Building a scrap heat map requires pulling 12–24 months of historical data from ERP, MES, and manual logs. The goal is visibility by cell, part family, program, and supplier. Most aerospace organizations discover that 60–70% of their scrap cost concentrates in 15–20% of part numbers. This concentration creates leverage for targeted intervention.

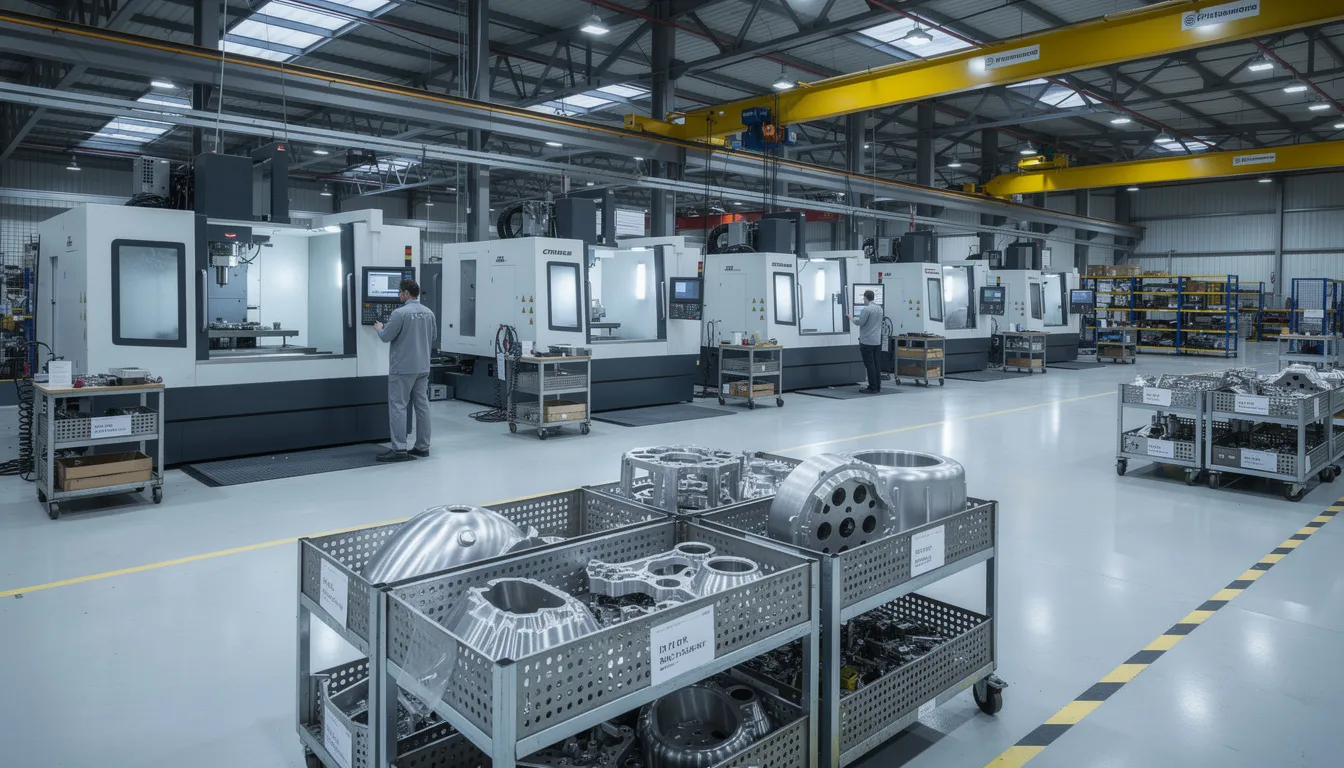
    The image depicts an aerospace manufacturing factory floor featuring multiple CNC machining centers surrounded by organized parts bins, illustrating the operational efficiency and advanced quality management systems essential in the aerospace industry. This setting highlights the importance of standardized processes and regulatory compliance in producing high-quality aerospace components.

    The cost components that must be captured include:

    • Material cost: The value of scrapped raw materials and semi-finished goods, including any special processing already completed.
    • Touch labor: Direct labor hours invested in the scrapped part, valued at fully-burdened rates.
    • Indirect support: MRB hours, engineering disposition time, and quality documentation labor.
    • Expedite and replacement costs: Freight premiums, expedited supplier processing, and overtime to recover schedule.
    • Customer penalties: Contractual damages for late delivery or concession processing fees.

    Connect981 can centralize nonconformance data, rework routing, and cost tags from multiple plants and suppliers into a single view without replacing ERP or existing MES infrastructure. This creates the visibility foundation that governance requires.

    One aerospace supplier manufacturing composite spoilers reduced scrap cost by 25% over 18 months by mapping economic impact at this level of detail. The reduction did not require new capital equipment. It required understanding which operations, which shifts, and which material lots drove the highest-value scrap events—then addressing those specific sources.

    Root Causes of Aerospace Scrap: Systemic Patterns, Not Operator Mistakes

    Aerospace scrap rarely originates in dramatic single events. It accumulates through systemic patterns: engineering ambiguity, late design changes, tolerance stacking, uncontrolled process drift, supplier inconsistency, and weak configuration management. The operator who produces the defect is usually the last person in a chain of decisions that made the defect inevitable.

    Concrete sources of variation that drive scrap include:

    • Model-based definition interpretation errors: PMI and GD&T on complex parts can be misread or inconsistently applied across stations and shifts.
    • Out-of-date work instructions: Engineering changes release but work instructions lag by days or weeks, creating misbuilds.
    • Tribal knowledge on setups: Critical setup parameters live in experienced operators’ heads, not in controlled documents.
    • Missing special process parameters: Routed operations reference NADCAP-controlled processes but omit the specific parameters required for the part configuration.
    • Tolerance stacking: Individual features are in-spec but the assembly fails because tolerance stack-ups were not analyzed at design.

    The cultural normalization of rework has become embedded in aerospace manufacturing since the 1990s. The phrase “we’ll fix it in MRB” signals a system that tolerates chronic instability. MRB becomes a permanent fixture rather than an exception. Rework becomes budgeted rather than reduced. This masks the underlying process capability gaps that continue generating scrap.

    Tangible examples from operating facilities:

    • Recurring hole location issues on 5-axis titanium brackets: The same hole pattern drifts out of position on the same part family, traced to fixture wear that inspection catches late in the routing.
    • Porosity-related scrap in NADCAP-approved weld cells: Shielding gas flow rates drift within acceptable ranges but interact with humidity variations to produce borderline porosity.
    • MRO teardown inspection findings: Certain engine module configurations repeatedly trigger the same unplanned repairs, but the pattern is invisible because teardown data lives in disconnected systems.

    Fragmented systems—paper packets, spreadsheets, disconnected quality tools—make true root cause analysis slow, inconsistent, and heavily dependent on individual expertise. Connect981 addresses this through standardized defect taxonomies, AI-assisted pattern detection across NC records, and shared visibility between plant and supplier engineering teams. The platform does not replace engineering judgment. It makes patterns visible faster so that judgment can be applied.

    Designing a Cross-Functional Aerospace Scrap Reduction Strategy

    Functional silos kill scrap reduction initiatives. Quality-led projects that ignore engineering release schedules fail. Plant initiatives isolated from Tier-1 and Tier-2 suppliers hit walls. Engineering changes that do not flow to the shopfloor in real time generate misbuilds. Effective scrap reduction requires a cross-functional strategy that aligns engineering, supply chain management, operations, quality, and program management around shared objectives.

    The following strategic pillars form the backbone of a sustainable aerospace scrap reduction strategy:

    Governance and ownership: Appoint a scrap reduction leader at the site or program level with clear authority and accountability. Establish a cross-functional steering team that meets monthly with quarterly targets tied to program economics. Without named ownership, scrap reduction becomes everyone’s second priority.

    Data and visibility: Define one source of truth for scrap events, rework, and associated cost. Standardize defect codes and traceability fields across 2024+ programs. Most aerospace organizations have three to five systems that each hold partial scrap data. Consolidation is mandatory for pattern detection.

    Engineering and configuration control: Mandate change management discipline. Require design-for-manufacturability reviews using historical NC and scrap data. Ensure digital work instructions update with every ECN/ECR. The connection between PLM and shopfloor execution must be real-time, not weekly batch updates.

    Supplier integration: Embed suppliers into the same NC, SCAR, and scrap visibility flow. Share dashboards. Conduct quarterly performance reviews that include supplier process owners, not just sales representatives. Scrap often materializes at your site but originates upstream.

    Process capability and stability: Focus on Cp/Cpk, process windows, and special process control instead of adding inspection steps. Statistical process control is not a 1990s relic—it is the foundation of stable aerospace manufacturing processes.

    Cultural shift: Move from “MRB will fix it” to “design and process prevent it.” Leadership messaging must align with incentives. If throughput is rewarded and prevention is ignored, operators and engineers will optimize for throughput.

    Governance, Metrics, and Target Setting for Scrap Reduction

    Leadership discipline separates organizations that achieve sustained scrap reduction from those that run temporary Kaizens. Without clear governance, scrap programs devolve into PowerPoint updates that do not change operations.

    Governance elements that must be defined:

    Element

    Description

    Steering cadence

    Monthly plant review, quarterly executive review

    Roles

    Ops VP, Quality Director, Chief Engineer, Supply Chain Lead

    Decision rights

    Who approves investments, who owns root cause closure, who escalates

    Escalation criteria

    Thresholds that trigger immediate leadership attention

    Metrics must move beyond traditional scrap percentage to capture economic impact:

    • Scrap cost as % of sales by program: This ties scrap directly to margin, making it visible at executive level.
    • Rework hours per airframe or engine: Normalizes rework burden across production volumes.
    • First-pass yield by key operation: Identifies where process instability concentrates.
    • MRB cycle time in days: Long MRB cycles compound schedule impact.

    Target-setting example: A wide-body nacelle program targeting reduction from 3.8% scrap cost to 2.2% of revenue over 12 months (2025), with leading indicators tracked weekly. Weekly tracking allows same-week reaction instead of quarter-end surprises.

    Connect981 provides real-time dashboards tied to work orders, serialized components, and supplier POs. This enables performance monitoring at the cadence governance requires. When a steering team meets monthly, they need data from yesterday, not from the last quarter close.

    Upstream Levers: Engineering, Configuration, and Design-for-Manufacture

    Most scrap originates in decisions made months or years before the part hits the machine. Tolerance decisions, GD&T selections, stack-up assumptions, and manufacturing process selections create the conditions for downstream scrap. By the time a part reaches final assembly, the probability of scrap is largely determined.

    Engineering practices that reduce scrap upstream include:

    • Design reviews using historical scrap data: For complex aerospace products like blisks, structural fittings, and composite spars, review historical NC and scrap records from similar part families before releasing design.
    • PLM-to-shopfloor alignment: Tight integration between PLM systems (CATIA, Teamcenter, 3DEXPERIENCE) and downstream work instructions ensures the latest configuration reaches operators. Configuration drift between released design and floor documentation is a primary scrap driver.
    • Elimination of unapproved shop drawings: Digital work instructions become the controlled, versioned reference. Handwritten notes and informal drawings are eliminated from production.

    A titanium engine mount bracket program experienced recurring dimensional issues traced to tolerance decisions that did not account for manufacturing sequence. Tolerance relaxation on non-critical features and process sequencing changes reduced scrap by 40% without compromising safety margins or product safety requirements.

    Connect981 can trigger mandatory engineering review workflows when NC patterns cross defined thresholds—for example, three similar events in 30 days on the same part family. This closes the loop between production data and engineering action, enabling corrective actions before scrap accumulates.

    Shopfloor Execution: Standardization, Digital Work Instructions, and Error-Proofing

    Scrap reduction on the shopfloor is about a stable system, not about pressuring operators to work harder. Operators who have clear instructions, current revisions, and usable tools produce fewer defects. Operators working from outdated paper packets, tribal knowledge, and ambiguous specifications will generate scrap regardless of effort.

    An aerospace technician is focused on a tablet device at their workstation, which is equipped with various tools and components essential for aerospace manufacturing. This scene highlights the importance of quality management systems and operational efficiency in the aerospace industry.

    Concrete execution levers that minimize defects:

    • Digital work instructions with embedded parameters: Step-by-step visuals, torque values, process parameters, and inspection checkpoints for complex assemblies like flight control surfaces and landing gear subassemblies.
    • Real-time revision access: Automated alerts when a new revision goes live for an active work order. No operator should work from yesterday’s instruction when engineering released a change this morning.
    • In-process quality checks: Embedded signoffs for hole size gauges, ply orientation checks, and dimensional verifications logged directly against the serialized part.

    Replacing paper routers and tribal notes with Connect981 on tablets and terminals delivers measurable results. A 5-axis machining cell reduced wrong-tool scrap incidents by implementing digital tool callouts with barcode verification. The fix was not discipline or retraining—it was making the right action easier than the wrong action.

    Practical error-proofing approaches include:

    • Fixtures keyed to prevent part misorientation
    • Poka-yoke devices for connector installation sequences
    • Barcoded material ID checks for alloy and heat lot verification

    These approaches respect operator capability while removing opportunities for human error. They enhance product safety without adding inspection burden.

    Supplier and MRO Network Integration into Scrap Reduction

    Scrap and rework often materialize at your site but originate upstream—at a forge, machine house, special process shop, or in an MRO exchange pool. Aerospace organizations cannot control scrap without extending visibility and accountability into the supply chain.

    Extending scrap strategy beyond internal walls requires:

    • Shared NC, SCAR, and concession data: Replace email and spreadsheet exchanges with a common platform that provides seamless integration between customer and supplier quality systems.
    • Early-warning signals: Detect when multiple sites experience similar quality issues with the same supplier or part family before the pattern becomes a program crisis.
    • Joint root cause sessions: Include supplier process owners in root cause analysis, not just sales or quality representatives who lack technical depth.

    Common supplier-originated scrap patterns include:

    • Heat-treat vendors driving hardness variability that manifests as machining scrap downstream
    • Coating houses causing adhesion issues on aluminum structural parts that fail inspection at final assembly
    • Forge suppliers with dimensional variation that consumes tolerance budget before machining begins

    MRO operations face specific challenges: scrap of high-value rotable assets triggers immediate cost exposure. Understanding recurring damage patterns requires full repair and overhaul history across the exchange pool. Without this history, every teardown starts from zero.

    Connect981’s supplier workflow integration and shared data views synchronize POs, certs, FAI results, and NC history across a two to three tier chain. This creates the transparency required for supplier certifications and ongoing performance management without requiring suppliers to adopt enterprise-scale systems.

    From Firefighting to Prevention: Building a Sustainable Scrap Reduction Discipline

    Initial scrap reductions are achievable through focused attention and temporary task forces. Sustaining those reductions requires embedding prevention into the operating system. Without institutionalization, gains erode within 12–18 months as attention shifts to the next crisis.

    Behaviors that must become permanent:

    • MRB and CAPA reviews prioritizing systemic fixes: Containment is necessary but insufficient. Every MRB disposition should include assessment of whether the root cause is isolated or systemic. Corrective actions must address system gaps, not just the specific instance.
    • Lessons learned applied to NPI: Scrap patterns from current programs must inform design and process decisions on new product introduction for 2026 and beyond. Organizations that repeat the same mistakes on successive programs are paying tuition without learning.
    • Incentives aligned with prevention: KPIs that reward process capability projects and scrap prevention as much as short-term throughput wins. If only output is measured, only output will be optimized.

    Continuous improvement frameworks must become structured rather than episodic. This includes annual scrap reduction roadmaps tied to capital planning, tooling upgrades, and supplier development plans. The roadmap creates accountability and resource allocation. Ad hoc events create temporary improvement followed by regression.

    An engineering team is gathered around a table in an aerospace manufacturing facility, reviewing technical documents to ensure compliance with stringent quality standards and regulatory requirements. The atmosphere reflects a focus on operational efficiency and continuous improvement within the aerospace industry.

    Digital infrastructure like Connect981 helps sustain discipline by making it easy to keep standardized processes, instructions, and data aligned as the organization changes. When a key engineer leaves, their knowledge about scrap drivers should not leave with them. When a new program starts, the scrap history from similar programs should inform planning automatically.

    How Connect981 Supports an Aerospace Scrap Reduction Strategy

    Connect981 serves as a unified operations layer built specifically for aerospace manufacturing and MRO. It is not a replacement for ERP or QMS. It is the execution and visibility layer that connects those systems to shopfloor reality.

    Capabilities that directly support scrap reduction:

    Capability

    Scrap Reduction Impact

    Centralized defect logging and NC management

    Single source of truth across factories and suppliers

    Digital work instructions with version control

    Current configuration always available, reducing misbuilds

    Real-time dashboards

    Scrap, rework, and first-pass yield visible by program, part family, and supplier

    AI-assisted root cause pattern detection

    Identifies recurring patterns across historical NC data and production context

    Supplier workflow integration

    Shared visibility into NC, SCAR, and certification status

    Practical example: A plant using Connect981 identified that composite part scrap concentrated at a specific layup station during a specific shift pattern. The root cause was environmental variation (humidity) interacting with cure parameters. Updating work instructions to include humidity checks and adjusting cure windows reduced scrap by 30% on that part family within two months.

    Connect981 overlays existing ERP, MES, and quality management systems rather than requiring disruptive replacement. This is critical in highly regulated aerospace environments where system changes require validation and customer approval. The platform achieves audit readiness and real time data visibility without the risk and timeline of enterprise system replacement.

    For operations and program leaders responsible for margin protection, Connect981 offers a direct path to the visibility and execution discipline that scrap reduction requires. Request a demo focused specifically on scrap and rework reduction use cases to assess fit for your environment.

    Conclusion: Scrap Reduction as a Leadership Discipline

    Aerospace scrap reduction is not a quality department initiative. It is a cross-functional leadership discipline that touches engineering, supply chain, operations, and quality governance simultaneously. Organizations that achieve sustainable reduction treat scrap as an economic and strategic risk indicator, not just a line in the quality report.

    Inspection-heavy approaches cannot address scrap that originates in engineering decisions, supplier variation, or process instability. Isolated quality projects cannot succeed when engineering, supply chain, and operations continue practices that generate scrap. Prevention requires leadership that aligns incentives, invests in process capability, and holds cross-functional teams accountable for outcomes.

    Modern digital platforms like Connect981 are enablers of this discipline. They provide the visibility, traceability, and execution infrastructure that governance requires. But technology alone cannot substitute for ownership, accountability, and a prevention mindset. Customer satisfaction and operational excellence depend on leaders who understand that scrap is a systemic signal, not an isolated defect.

    The 2025–2030 period will intensify pressure on aerospace organizations. Capacity ramps demand operational efficiency at scale. Sustainability requirements add environmental responsibility to operational priorities. Regulatory standards continue to tighten. Supply chain volatility persists. Organizations that have embedded scrap reduction into their operating system will meet stringent safety and delivery requirements while protecting margin. Those still treating scrap as a quality metric will find themselves absorbing losses they cannot recover.

    The reframing is straightforward: scrap reduction is not a department. It is a discipline. It is not a metric. It is a capability. And it is not optional for aerospace organizations that intend to remain competitive through the next decade.