Tag: scrap reduction

  • Aerospace Scrap Reduction Strategy

    Aerospace Scrap Reduction Strategy

    Scrap in aerospace manufacturing is not a quality problem. It is a margin stability problem. This distinction matters because it determines how organizations respond. Quality problems get assigned to the quality department. Margin stability problems get executive attention.

    In fixed-price and risk-sharing contract structures that have dominated aerospace programs since 2015, every scrapped titanium fitting, every rejected composite panel, and every rework cycle on an engine component comes directly out of program margin. There is no recovery mechanism. The economics are unforgiving: high-value materials, long cycle times, and multi-year build programs like the A320neo, 737 MAX, and F-35 mean that scrap accumulates into substantial financial exposure before leadership recognizes the pattern.

    This article is written from the perspective of someone who has owned scrap numbers at the cell, value stream, and site level. It is not a software pitch. Connect981 appears in this discussion because it serves as an enabling layer for execution and traceability, but the strategy itself is primarily about leadership discipline and systemic prevention. Technology cannot fix governance failures. It can only make good governance faster and more visible.

    The aerospace industry in 2024–2030 faces unprecedented challenges: capacity ramps, supply chain complexity, workforce transitions, and regulatory scrutiny. Organizations that treat scrap reduction as a strategic discipline will protect margin and schedule. Those that treat it as a quality metric will continue to absorb losses they cannot recover.

    Why Scrap Reduction in Aerospace Is Different from Other Industries

    A 1–2% scrap rate in consumer goods manufacturing is a rounding error. In aerospace, that same rate can destroy the economics of a fixed-price contract. A single scrapped part—a machined titanium bulkhead worth $120,000, or a composite wing skin layup after 20+ hours of touch labor—represents capital that cannot be recovered under most contract structures.

    The aerospace sector operates under constraints that make scrap economically devastating in ways other industries do not experience. Regulatory compliance is mandatory, not optional. ITAR and EAR controls govern material handling and documentation. AS9100D and NADCAP accreditation set baseline quality standards for processes like heat treating, chemical processing, and non destructive testing. Federal Aviation Administration and EASA oversight adds another layer. Customer DCMA representatives and prime audits verify adherence. Every scrapped part generates documentation burden in addition to material cost.

    The differentiators that separate aerospace from automotive or consumer goods manufacturing include:

    • Part value: Aerospace components use exotic materials—titanium alloys, Inconel, advanced composite materials—where raw materials alone can exceed $10,000–$50,000 per part before any machining or processing labor.
    • Low volume, high mix: Production runs are measured in hundreds or low thousands, not millions. Learning curve benefits are limited, and every scrapped unit matters.
    • Long qualification cycles: Requalifying a process or supplier after a change can take 12–24 months, making rapid corrections impossible.
    • Configuration-driven builds: Every aircraft and engine has serialized part histories and traceability requirements that mandate precise configuration management.
    • Schedule compounding: A scrapped part does not just cost material. It costs schedule. Missed delivery slots to Boeing or Airbus cascade into line stoppages and contractual penalties across multi-tier suppliers.

    In MRO operations, the stakes are equally high. Engine module rework during a 30–45 day TAT commitment leaves no room for unplanned scrap. Scrapping a high-value rotable asset—a fan blade, a gear, an actuator—during teardown inspection triggers immediate cost exposure and potential AOG situations for the customer.

    Mapping the Economic Impact of Scrap and Rework Across the Value Stream

    The first step in any aerospace scrap reduction strategy is to quantify scrap and rework as economic leakage, not just as PPM or percentage of pieces. Traditional quality metrics obscure the true impact. A part family with 2% scrap looks acceptable until leadership learns that 2% represents $1.8 million in annual material cost plus another $600,000 in touch labor and MRB processing.

    Building a scrap heat map requires pulling 12–24 months of historical data from ERP, MES, and manual logs. The goal is visibility by cell, part family, program, and supplier. Most aerospace organizations discover that 60–70% of their scrap cost concentrates in 15–20% of part numbers. This concentration creates leverage for targeted intervention.
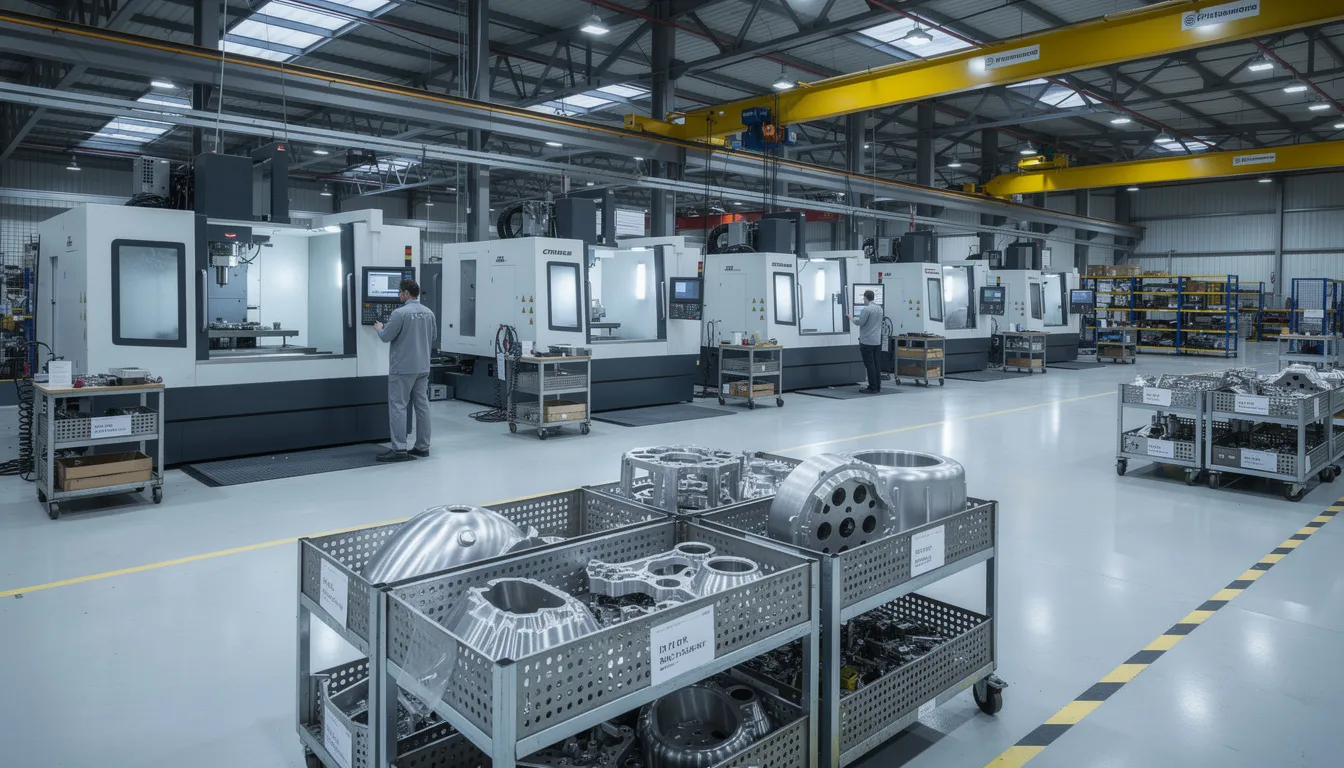
    The image depicts an aerospace manufacturing factory floor featuring multiple CNC machining centers surrounded by organized parts bins, illustrating the operational efficiency and advanced quality management systems essential in the aerospace industry. This setting highlights the importance of standardized processes and regulatory compliance in producing high-quality aerospace components.

    The cost components that must be captured include:

    • Material cost: The value of scrapped raw materials and semi-finished goods, including any special processing already completed.
    • Touch labor: Direct labor hours invested in the scrapped part, valued at fully-burdened rates.
    • Indirect support: MRB hours, engineering disposition time, and quality documentation labor.
    • Expedite and replacement costs: Freight premiums, expedited supplier processing, and overtime to recover schedule.
    • Customer penalties: Contractual damages for late delivery or concession processing fees.

    Connect981 can centralize nonconformance data, rework routing, and cost tags from multiple plants and suppliers into a single view without replacing ERP or existing MES infrastructure. This creates the visibility foundation that governance requires.

    One aerospace supplier manufacturing composite spoilers reduced scrap cost by 25% over 18 months by mapping economic impact at this level of detail. The reduction did not require new capital equipment. It required understanding which operations, which shifts, and which material lots drove the highest-value scrap events—then addressing those specific sources.

    Root Causes of Aerospace Scrap: Systemic Patterns, Not Operator Mistakes

    Aerospace scrap rarely originates in dramatic single events. It accumulates through systemic patterns: engineering ambiguity, late design changes, tolerance stacking, uncontrolled process drift, supplier inconsistency, and weak configuration management. The operator who produces the defect is usually the last person in a chain of decisions that made the defect inevitable.

    Concrete sources of variation that drive scrap include:

    • Model-based definition interpretation errors: PMI and GD&T on complex parts can be misread or inconsistently applied across stations and shifts.
    • Out-of-date work instructions: Engineering changes release but work instructions lag by days or weeks, creating misbuilds.
    • Tribal knowledge on setups: Critical setup parameters live in experienced operators’ heads, not in controlled documents.
    • Missing special process parameters: Routed operations reference NADCAP-controlled processes but omit the specific parameters required for the part configuration.
    • Tolerance stacking: Individual features are in-spec but the assembly fails because tolerance stack-ups were not analyzed at design.

    The cultural normalization of rework has become embedded in aerospace manufacturing since the 1990s. The phrase “we’ll fix it in MRB” signals a system that tolerates chronic instability. MRB becomes a permanent fixture rather than an exception. Rework becomes budgeted rather than reduced. This masks the underlying process capability gaps that continue generating scrap.

    Tangible examples from operating facilities:

    • Recurring hole location issues on 5-axis titanium brackets: The same hole pattern drifts out of position on the same part family, traced to fixture wear that inspection catches late in the routing.
    • Porosity-related scrap in NADCAP-approved weld cells: Shielding gas flow rates drift within acceptable ranges but interact with humidity variations to produce borderline porosity.
    • MRO teardown inspection findings: Certain engine module configurations repeatedly trigger the same unplanned repairs, but the pattern is invisible because teardown data lives in disconnected systems.

    Fragmented systems—paper packets, spreadsheets, disconnected quality tools—make true root cause analysis slow, inconsistent, and heavily dependent on individual expertise. Connect981 addresses this through standardized defect taxonomies, AI-assisted pattern detection across NC records, and shared visibility between plant and supplier engineering teams. The platform does not replace engineering judgment. It makes patterns visible faster so that judgment can be applied.

    Designing a Cross-Functional Aerospace Scrap Reduction Strategy

    Functional silos kill scrap reduction initiatives. Quality-led projects that ignore engineering release schedules fail. Plant initiatives isolated from Tier-1 and Tier-2 suppliers hit walls. Engineering changes that do not flow to the shopfloor in real time generate misbuilds. Effective scrap reduction requires a cross-functional strategy that aligns engineering, supply chain management, operations, quality, and program management around shared objectives.

    The following strategic pillars form the backbone of a sustainable aerospace scrap reduction strategy:

    Governance and ownership: Appoint a scrap reduction leader at the site or program level with clear authority and accountability. Establish a cross-functional steering team that meets monthly with quarterly targets tied to program economics. Without named ownership, scrap reduction becomes everyone’s second priority.

    Data and visibility: Define one source of truth for scrap events, rework, and associated cost. Standardize defect codes and traceability fields across 2024+ programs. Most aerospace organizations have three to five systems that each hold partial scrap data. Consolidation is mandatory for pattern detection.

    Engineering and configuration control: Mandate change management discipline. Require design-for-manufacturability reviews using historical NC and scrap data. Ensure digital work instructions update with every ECN/ECR. The connection between PLM and shopfloor execution must be real-time, not weekly batch updates.

    Supplier integration: Embed suppliers into the same NC, SCAR, and scrap visibility flow. Share dashboards. Conduct quarterly performance reviews that include supplier process owners, not just sales representatives. Scrap often materializes at your site but originates upstream.

    Process capability and stability: Focus on Cp/Cpk, process windows, and special process control instead of adding inspection steps. Statistical process control is not a 1990s relic—it is the foundation of stable aerospace manufacturing processes.

    Cultural shift: Move from “MRB will fix it” to “design and process prevent it.” Leadership messaging must align with incentives. If throughput is rewarded and prevention is ignored, operators and engineers will optimize for throughput.

    Governance, Metrics, and Target Setting for Scrap Reduction

    Leadership discipline separates organizations that achieve sustained scrap reduction from those that run temporary Kaizens. Without clear governance, scrap programs devolve into PowerPoint updates that do not change operations.

    Governance elements that must be defined:

    Element

    Description

    Steering cadence

    Monthly plant review, quarterly executive review

    Roles

    Ops VP, Quality Director, Chief Engineer, Supply Chain Lead

    Decision rights

    Who approves investments, who owns root cause closure, who escalates

    Escalation criteria

    Thresholds that trigger immediate leadership attention

    Metrics must move beyond traditional scrap percentage to capture economic impact:

    • Scrap cost as % of sales by program: This ties scrap directly to margin, making it visible at executive level.
    • Rework hours per airframe or engine: Normalizes rework burden across production volumes.
    • First-pass yield by key operation: Identifies where process instability concentrates.
    • MRB cycle time in days: Long MRB cycles compound schedule impact.

    Target-setting example: A wide-body nacelle program targeting reduction from 3.8% scrap cost to 2.2% of revenue over 12 months (2025), with leading indicators tracked weekly. Weekly tracking allows same-week reaction instead of quarter-end surprises.

    Connect981 provides real-time dashboards tied to work orders, serialized components, and supplier POs. This enables performance monitoring at the cadence governance requires. When a steering team meets monthly, they need data from yesterday, not from the last quarter close.

    Upstream Levers: Engineering, Configuration, and Design-for-Manufacture

    Most scrap originates in decisions made months or years before the part hits the machine. Tolerance decisions, GD&T selections, stack-up assumptions, and manufacturing process selections create the conditions for downstream scrap. By the time a part reaches final assembly, the probability of scrap is largely determined.

    Engineering practices that reduce scrap upstream include:

    • Design reviews using historical scrap data: For complex aerospace products like blisks, structural fittings, and composite spars, review historical NC and scrap records from similar part families before releasing design.
    • PLM-to-shopfloor alignment: Tight integration between PLM systems (CATIA, Teamcenter, 3DEXPERIENCE) and downstream work instructions ensures the latest configuration reaches operators. Configuration drift between released design and floor documentation is a primary scrap driver.
    • Elimination of unapproved shop drawings: Digital work instructions become the controlled, versioned reference. Handwritten notes and informal drawings are eliminated from production.

    A titanium engine mount bracket program experienced recurring dimensional issues traced to tolerance decisions that did not account for manufacturing sequence. Tolerance relaxation on non-critical features and process sequencing changes reduced scrap by 40% without compromising safety margins or product safety requirements.

    Connect981 can trigger mandatory engineering review workflows when NC patterns cross defined thresholds—for example, three similar events in 30 days on the same part family. This closes the loop between production data and engineering action, enabling corrective actions before scrap accumulates.

    Shopfloor Execution: Standardization, Digital Work Instructions, and Error-Proofing

    Scrap reduction on the shopfloor is about a stable system, not about pressuring operators to work harder. Operators who have clear instructions, current revisions, and usable tools produce fewer defects. Operators working from outdated paper packets, tribal knowledge, and ambiguous specifications will generate scrap regardless of effort.

    An aerospace technician is focused on a tablet device at their workstation, which is equipped with various tools and components essential for aerospace manufacturing. This scene highlights the importance of quality management systems and operational efficiency in the aerospace industry.

    Concrete execution levers that minimize defects:

    • Digital work instructions with embedded parameters: Step-by-step visuals, torque values, process parameters, and inspection checkpoints for complex assemblies like flight control surfaces and landing gear subassemblies.
    • Real-time revision access: Automated alerts when a new revision goes live for an active work order. No operator should work from yesterday’s instruction when engineering released a change this morning.
    • In-process quality checks: Embedded signoffs for hole size gauges, ply orientation checks, and dimensional verifications logged directly against the serialized part.

    Replacing paper routers and tribal notes with Connect981 on tablets and terminals delivers measurable results. A 5-axis machining cell reduced wrong-tool scrap incidents by implementing digital tool callouts with barcode verification. The fix was not discipline or retraining—it was making the right action easier than the wrong action.

    Practical error-proofing approaches include:

    • Fixtures keyed to prevent part misorientation
    • Poka-yoke devices for connector installation sequences
    • Barcoded material ID checks for alloy and heat lot verification

    These approaches respect operator capability while removing opportunities for human error. They enhance product safety without adding inspection burden.

    Supplier and MRO Network Integration into Scrap Reduction

    Scrap and rework often materialize at your site but originate upstream—at a forge, machine house, special process shop, or in an MRO exchange pool. Aerospace organizations cannot control scrap without extending visibility and accountability into the supply chain.

    Extending scrap strategy beyond internal walls requires:

    • Shared NC, SCAR, and concession data: Replace email and spreadsheet exchanges with a common platform that provides seamless integration between customer and supplier quality systems.
    • Early-warning signals: Detect when multiple sites experience similar quality issues with the same supplier or part family before the pattern becomes a program crisis.
    • Joint root cause sessions: Include supplier process owners in root cause analysis, not just sales or quality representatives who lack technical depth.

    Common supplier-originated scrap patterns include:

    • Heat-treat vendors driving hardness variability that manifests as machining scrap downstream
    • Coating houses causing adhesion issues on aluminum structural parts that fail inspection at final assembly
    • Forge suppliers with dimensional variation that consumes tolerance budget before machining begins

    MRO operations face specific challenges: scrap of high-value rotable assets triggers immediate cost exposure. Understanding recurring damage patterns requires full repair and overhaul history across the exchange pool. Without this history, every teardown starts from zero.

    Connect981’s supplier workflow integration and shared data views synchronize POs, certs, FAI results, and NC history across a two to three tier chain. This creates the transparency required for supplier certifications and ongoing performance management without requiring suppliers to adopt enterprise-scale systems.

    From Firefighting to Prevention: Building a Sustainable Scrap Reduction Discipline

    Initial scrap reductions are achievable through focused attention and temporary task forces. Sustaining those reductions requires embedding prevention into the operating system. Without institutionalization, gains erode within 12–18 months as attention shifts to the next crisis.

    Behaviors that must become permanent:

    • MRB and CAPA reviews prioritizing systemic fixes: Containment is necessary but insufficient. Every MRB disposition should include assessment of whether the root cause is isolated or systemic. Corrective actions must address system gaps, not just the specific instance.
    • Lessons learned applied to NPI: Scrap patterns from current programs must inform design and process decisions on new product introduction for 2026 and beyond. Organizations that repeat the same mistakes on successive programs are paying tuition without learning.
    • Incentives aligned with prevention: KPIs that reward process capability projects and scrap prevention as much as short-term throughput wins. If only output is measured, only output will be optimized.

    Continuous improvement frameworks must become structured rather than episodic. This includes annual scrap reduction roadmaps tied to capital planning, tooling upgrades, and supplier development plans. The roadmap creates accountability and resource allocation. Ad hoc events create temporary improvement followed by regression.

    An engineering team is gathered around a table in an aerospace manufacturing facility, reviewing technical documents to ensure compliance with stringent quality standards and regulatory requirements. The atmosphere reflects a focus on operational efficiency and continuous improvement within the aerospace industry.

    Digital infrastructure like Connect981 helps sustain discipline by making it easy to keep standardized processes, instructions, and data aligned as the organization changes. When a key engineer leaves, their knowledge about scrap drivers should not leave with them. When a new program starts, the scrap history from similar programs should inform planning automatically.

    How Connect981 Supports an Aerospace Scrap Reduction Strategy

    Connect981 serves as a unified operations layer built specifically for aerospace manufacturing and MRO. It is not a replacement for ERP or QMS. It is the execution and visibility layer that connects those systems to shopfloor reality.

    Capabilities that directly support scrap reduction:

    Capability

    Scrap Reduction Impact

    Centralized defect logging and NC management

    Single source of truth across factories and suppliers

    Digital work instructions with version control

    Current configuration always available, reducing misbuilds

    Real-time dashboards

    Scrap, rework, and first-pass yield visible by program, part family, and supplier

    AI-assisted root cause pattern detection

    Identifies recurring patterns across historical NC data and production context

    Supplier workflow integration

    Shared visibility into NC, SCAR, and certification status

    Practical example: A plant using Connect981 identified that composite part scrap concentrated at a specific layup station during a specific shift pattern. The root cause was environmental variation (humidity) interacting with cure parameters. Updating work instructions to include humidity checks and adjusting cure windows reduced scrap by 30% on that part family within two months.

    Connect981 overlays existing ERP, MES, and quality management systems rather than requiring disruptive replacement. This is critical in highly regulated aerospace environments where system changes require validation and customer approval. The platform achieves audit readiness and real time data visibility without the risk and timeline of enterprise system replacement.

    For operations and program leaders responsible for margin protection, Connect981 offers a direct path to the visibility and execution discipline that scrap reduction requires. Request a demo focused specifically on scrap and rework reduction use cases to assess fit for your environment.

    Conclusion: Scrap Reduction as a Leadership Discipline

    Aerospace scrap reduction is not a quality department initiative. It is a cross-functional leadership discipline that touches engineering, supply chain, operations, and quality governance simultaneously. Organizations that achieve sustainable reduction treat scrap as an economic and strategic risk indicator, not just a line in the quality report.

    Inspection-heavy approaches cannot address scrap that originates in engineering decisions, supplier variation, or process instability. Isolated quality projects cannot succeed when engineering, supply chain, and operations continue practices that generate scrap. Prevention requires leadership that aligns incentives, invests in process capability, and holds cross-functional teams accountable for outcomes.

    Modern digital platforms like Connect981 are enablers of this discipline. They provide the visibility, traceability, and execution infrastructure that governance requires. But technology alone cannot substitute for ownership, accountability, and a prevention mindset. Customer satisfaction and operational excellence depend on leaders who understand that scrap is a systemic signal, not an isolated defect.

    The 2025–2030 period will intensify pressure on aerospace organizations. Capacity ramps demand operational efficiency at scale. Sustainability requirements add environmental responsibility to operational priorities. Regulatory standards continue to tighten. Supply chain volatility persists. Organizations that have embedded scrap reduction into their operating system will meet stringent safety and delivery requirements while protecting margin. Those still treating scrap as a quality metric will find themselves absorbing losses they cannot recover.

    The reframing is straightforward: scrap reduction is not a department. It is a discipline. It is not a metric. It is a capability. And it is not optional for aerospace organizations that intend to remain competitive through the next decade.
  • Implementing MES in Aerospace with a Waste-Reduction First Mindset

    Implementing MES in Aerospace with a Waste-Reduction First Mindset

    Implementing MES in Aerospace with a Waste-Reduction First Mindset

    In aerospace manufacturing, scrap and rework are not just quality issues—they are financial events. Every scrapped titanium forging or long-cycle composite part erodes margin, consumes scarce capacity, and jeopardizes delivery commitments. Yet most waste doesn’t come from dramatic failures. It comes from small process deviations that go unnoticed until final inspection.

    Manufacturing Execution Systems (MES) can change that equation, but only if they are implemented with a clear focus on waste reduction from day one. This article explains how to plan and execute an aerospace MES implementation that targets scrap, rework, and material waste as its primary outcomes, while respecting regulatory, validation, and compliance requirements.

    For teams putting this topic into daily operation, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, scrap and rework reduction, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on quality management workflows, a connected execution platform, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    We will walk through how to define the business case, assess current waste, design MES use cases, plan a phased rollout, manage change with operators and engineers, and measure impact in a way that wins continued support.

    Why Tie MES Implementation to Waste Reduction Goals

    Many MES programs start as broad “digital transformation” initiatives and struggle to demonstrate tangible value quickly. Anchoring MES implementation to clear, quantifiable waste-reduction goals keeps the effort focused and fundable.

    Creating a clear business case and ROI story

    To justify MES investment in an aerospace environment, the business case should be specific about where value will come from and how it will be measured. Instead of generic benefits like “more visibility,” highlight concrete targets such as:

    • Reducing scrap rate on critical components by a defined percentage range
    • Lowering rework hours per unit on key product families
    • Cutting excess material consumption versus planned usage
    • Reducing disruptions to schedule caused by late-found defects

    Scrap in aerospace often involves high-value alloys, complex assemblies, or long lead-time components. Connecting MES use cases directly to reduced scrap and rework on these items creates a compelling Return on Investment (ROI) narrative. Rather than promising a specific payback period, describe a range and the factors that influence it, such as product mix, baseline process stability, and regulatory constraints on process changes.

    Aligning plant, quality, and finance priorities

    Waste reduction touches multiple stakeholders, and MES success depends on aligning their priorities:

    • Operations/Plant leadership cares about throughput, schedule adherence, and labor efficiency.
    • Quality and regulatory focus on conformance, traceability, and compliance with aerospace standards and customer requirements.
    • Finance tracks margin, cost of poor quality, and performance on long-term or fixed-price contracts.

    When presenting the MES program, frame waste reduction in terms that matter to each group:

    • For operations: fewer disruptive quality holds, smoother flow, less rework blocking bottleneck resources.
    • For quality: earlier detection of process drift, better evidence for root cause analysis, improved audit readiness.
    • For finance: lower scrap write-offs, improved cost predictability, better protection of margins on fixed-price programs.

    This alignment helps prevent MES from being seen as a “IT tool” and positions it as a shared capability for controlling waste and risk.

    Focusing on high-impact scrap and rework issues

    Not all waste is equal. In aerospace, some scrap events are so costly or schedule-critical that even small improvements matter. To ensure MES is focused on the most impactful problems:

    • Identify parts and assemblies with high material cost, long cycle times, or stringent rework limitations.
    • Review historical data to find frequent non-conformances, recurring deviations, and costly rework loops.
    • Engage cross-functional teams to select a handful of priority issues where MES can provide earlier detection, better execution control, or improved traceability.

    These high-impact issues become the backbone of your initial MES use-case roadmap and help ensure early phases of implementation demonstrate visible, measurable value.

    Assessing Current Scrap, Rework, and Material Waste

    Before defining MES requirements, you need an honest baseline of how much waste exists today, where it occurs, and how well it is currently measured.

    Gathering baseline data from existing systems

    Most aerospace manufacturers already have some level of data in ERP, QMS, PLM, and perhaps legacy shop-floor systems. To build a baseline:

    • Pull historical scrap and rework records by part number, work center, and defect type.
    • Review non-conformance reports (NCRs) and corrective action reports (CARs) for recurring issues and systemic causes.
    • Analyze material variance reports: actual vs. planned consumption, particularly for expensive materials and consumables.
    • Document the typical detection point for defects—in-process checks, final inspection, or even post-delivery.

    The goal is not perfection but a pragmatic understanding of where waste happens today and how visible it is in current systems.

    Identifying data gaps MES can fill

    As you review existing data, you will likely uncover gaps, such as:

    • Limited or inconsistent linking between process parameters and resulting defects.
    • Inadequate visibility into which operations most often introduce errors.
    • Fragmented or manual records of rework steps, making it hard to quantify true cost.
    • Poor tracking of partial scrappage (e.g., only part of an assembly is scrapped).

    These gaps inform the MES data model and configuration. For example, you might prioritize:

    • Capturing key process parameters at critical operations.
    • Standardizing reason codes for scrap and rework.
    • Linking material lot information and genealogy to each work order.

    By being explicit about today’s blind spots, you can design MES to make waste visible and traceable, rather than simply replicating current limitations in a new system.

    Prioritizing critical parts and processes

    Not every operation needs the same level of MES control from day one. To prioritize:

    • Rank parts or assemblies by scrap cost and rework frequency.
    • Identify special processes (e.g., heat treatment, welding, bonding, coating) that have tight validation and high risk.
    • Flag operations where rework is limited or prohibited by design or regulatory requirements.

    These priorities help you select where to implement detailed MES tracking, real-time monitoring, and strict standard work enforcement first. They also guide which cells or lines are the best candidates for your initial MES pilot.

    Defining MES Use Cases Around Waste Reduction

    With a baseline established, the next step is to translate waste-reduction goals into specific MES use cases. Each use case should clearly articulate who uses it, what data is captured, and how it prevents or reduces scrap, rework, or material waste.

    Real-time monitoring and holds

    One of the most powerful ways MES reduces waste is by detecting problems earlier than traditional sampling-based quality checks. Effective use cases include:

    • Parameter monitoring: Capture critical process parameters (temperature, torque, pressure, time-in-process) in real time and compare them to approved limits.
    • Automated alerts: Notify operators, supervisors, or quality when parameters deviate or when inspection results trend toward limits.
    • Automatic holds: Place affected work orders or serial numbers on hold when a serious deviation is detected, preventing further value-add until disposition.

    By intervening early, MES can stop defects before they multiply. Instead of discovering issues at final inspection—when multiple parts may already be affected—you can initiate corrective actions while only a small number of parts are at risk.

    Standard work enforcement and error-proofing

    Rework often stems from missed steps, incorrect settings, or inconsistent execution. MES can enforce standard work to reduce this variability:

    • Operation checklists that must be completed in sequence before moving to the next step.
    • Verification of tooling, fixtures, and programs (e.g., CNC program version, calibrated tool ID) before work starts.
    • In-process signoffs by operators and inspectors with clear accountability.
    • Embedded work instructions with visuals, parameters, and notes tailored to the specific configuration or revision.

    These capabilities do not replace training or certification, but they make it harder for common errors to slip through, especially when dealing with complex routings or multiple product variants on the same line.

    Material tracking and yield analytics

    Material waste in aerospace is often hidden. Offcuts, over-issues, and non-visible losses rarely show up in headline metrics. MES can help you understand and control this waste through:

    • Lot and serial tracking for high-value materials, linking each lot to specific work orders and operations.
    • Actual vs. planned material usage at the operation or work-order level, not just net at the end of the job.
    • Yield reporting that shows how much input material results in conforming output across operations.

    With better data, engineering and operations can refine nesting strategies, cutting patterns, and process parameters. Over time, this moves decisions from rough assumptions to evidence-based optimization.

    Phased MES Rollout Strategy for Aerospace Plants

    Given aerospace regulatory and validation requirements, a “big bang” MES rollout is risky. A phased approach allows you to learn, adjust, and demonstrate value while maintaining control.

    Starting with a pilot line or product family

    Choose a pilot that is meaningful but manageable. Good candidates include:

    • A product family with significant scrap or rework issues.
    • A cell with relatively stable staffing and leadership support.
    • A value stream where both engineering and quality are engaged and available.

    In the pilot, focus on a limited set of high-impact MES use cases rather than attempting full functionality at once. For example, prioritize real-time monitoring at one special process, standardized work instructions for a critical assembly, and basic material tracking for expensive materials.

    Balancing speed with validation and compliance needs

    Aerospace environments must comply with customer, regulatory, and internal standards (for example, regarding software validation, configuration management, and data integrity). When planning your pilot:

    • Define which MES functions require formal validation before use in production.
    • Document configurations, workflows, and change controls from the start.
    • Use a test environment for training, configuration testing, and scenario validation before migrating to production.

    It is important not to underestimate the effort here. Validation and documentation add time, but they also build trust with quality and regulatory teams, which in turn helps smooth the path for broader adoption.

    Scaling to additional cells, plants, and suppliers

    Once the pilot demonstrates measurable waste reduction and stable operations, build a scale-out plan:

    • Standardize core templates for routes, work instructions, and data collection that can be reused across cells.
    • Capture lessons learned on change management, training, and configuration so future rollouts go faster.
    • Consider extending MES capabilities to key suppliers or integrating supplier data where appropriate to gain better visibility into upstream waste drivers.

    As you scale, maintain a clear priority on waste-reduction use cases so new deployments continue to deliver recognizable, quantifiable improvements.

    Change Management and Operator Adoption

    Even the best-designed MES will fail to reduce waste if people see it as extra work or surveillance rather than a tool that helps them succeed. Effective change management is essential.

    Communicating the purpose and benefits

    Frontline operators, inspectors, and technicians are closest to the process and will use MES every day. To gain their support:

    • Explain that the goal is preventing problems earlier, not blaming individuals for defects discovered late.
    • Highlight how MES can reduce rework loops, urgent expedites, and last-minute firefighting.
    • Show that better data will support more realistic process capability assessments and help justify needed investments in tooling, training, or equipment.

    Include operators and inspectors in design workshops and pilot reviews. Their insights often reveal practical ways to capture the right data with minimal disruption.

    Designing intuitive UIs and workflows

    To encourage adoption:

    • Keep screens simple and focused on the current task, avoiding unnecessary fields.
    • Use terminology and sequences that match how the work is actually performed on the floor.
    • Minimize manual entry where possible, using barcodes, RFID, or machine integration.
    • Provide clear visual indicators when something is out of tolerance or requires action.

    A small number of well-designed screens that accurately reflect real work will be more effective than a complex UI that attempts to handle every scenario from day one.

    Using early wins to build momentum

    After the pilot goes live, actively look for early signs that MES is helping reduce scrap, rework, or material waste. Examples include:

    • A parameter alert catches tool wear before it causes a run of non-conforming parts.
    • Standardized work instructions reduce rework on a complex assembly step.
    • Better material tracking reveals and corrects a recurring over-issue practice.

    Share these stories widely, backed by data. Recognize teams and individuals who contributed. Early success stories build credibility and help others see MES as a practical tool for improvement rather than a corporate mandate.

    Measuring and Communicating Impact

    To sustain support and funding, you must translate MES-enabled waste reductions into meaningful metrics and narratives for multiple audiences.

    Tracking scrap, rework, and material usage trends

    Define a small set of core metrics before go-live and measure them consistently over time. Typical examples include:

    • Scrap rate by part family, work center, and defect type.
    • Rework hours per unit or per month, by operation.
    • Material yield for key materials, comparing input mass or area to conforming output.
    • Time to detect critical defects (from introduction to detection).

    MES should make these metrics easier and faster to produce by providing consistent, structured data from the shop floor.

    Translating improvements into financial terms

    To communicate with executives and finance, connect operational improvements to financial impact. Examples include:

    • Annualized reduction in scrap write-offs for specific part families.
    • Reduced rework labor hours, expressed as capacity freed for value-add work.
    • Improved predictability of material usage, supporting more accurate costing and quoting.

    Be clear about assumptions and influencing factors. Instead of claiming a guaranteed payback period, present reasoned estimates and sensitivity to variables like volume, product mix, and future process changes.

    Sharing results with executives and customers

    Use dashboards, periodic reports, and simple before/after comparisons to show how MES contributes to performance. For customers and auditors, MES can demonstrate:

    • Enhanced traceability and control of special processes.
    • Systematic, data-driven approaches to reducing defects.
    • Evidence that corrective actions are effective and sustained.

    These capabilities can strengthen your position in bids, customer audits, and long-term partnership discussions, especially on programs where waste directly affects fixed-price margins.

    Sustaining Waste Reduction as a Continuous Improvement Program

    MES implementation is not a one-time project. To keep scrap, rework, and material waste trending down, you need an ongoing governance and improvement framework.

    Establishing governance and ownership

    Clarify who owns which aspects of MES and waste reduction:

    • Business process owners (operations, quality, engineering) define rules, workflows, and priorities.
    • IT or digital teams maintain the platform, integrations, and technical configuration.
    • Continuous improvement or Lean/Six Sigma teams use MES data to identify and close performance gaps.

    Set up a cross-functional steering group that regularly reviews MES performance, waste trends, and proposed changes.

    Regularly reviewing MES rules and configurations

    As processes change and new products are introduced, static MES configurations can become outdated. To prevent this:

    • Schedule periodic reviews of key alerts, holds, and data collection points.
    • Use MES data to refine control limits, inspection frequencies, and standard work steps.
    • Retire or simplify features that are not adding value or are causing unnecessary complexity.

    This ongoing tuning helps ensure MES continues to support waste reduction rather than becoming a rigid constraint.

    Integrating with Lean, Six Sigma, and quality programs

    MES and traditional improvement methodologies are complementary. MES provides the real-time, granular data that Lean and Six Sigma teams need to identify variation, validate improvements, and sustain gains. To integrate effectively:

    • Use MES data to populate value-stream maps, capability analyses, and control charts.
    • Build standard problem-solving workflows that reference MES data for root cause analysis.
    • Incorporate MES training into broader continuous improvement education for leaders and frontline staff.

    By treating MES as a core enabler of waste reduction as continuous improvement with MES in aerospace, you turn it from an IT project into a long-term competitive advantage.

    Conclusion

    Implementing MES in aerospace with a waste-reduction first mindset means starting from the real problems: costly scrap, limited rework options, hidden material losses, and schedule risk. By building a targeted business case, prioritizing high-impact use cases, rolling out in phases, and investing in change management, you can turn MES into a practical tool for preventing defects and protecting margins.

    With clear ownership and ongoing integration into continuous improvement programs, MES becomes a sustained capability for controlling waste in an environment where every gram of material and every minute of capacity matters.

  • Protecting Margins on Fixed-Price Aerospace Contracts with MES

    Protecting Margins on Fixed-Price Aerospace Contracts with MES

    Protecting Margins on Fixed-Price Aerospace Contracts with MES

    In aerospace manufacturing, scrap is not just a quality problem. It is a financial event. Under fixed-price and long-term contracts, every lost part, extra hour of rework, and unplanned material withdrawal directly erodes program margin. A well-implemented Manufacturing Execution System (MES) gives aerospace manufacturers the visibility and control needed to keep waste from silently eating into profitability.

    This article explains how MES-driven scrap, rework, and material waste reduction supports margin protection in fixed-price aerospace contracts. It also shows how plant-floor data can feed program-level financial decisions, improve risk management, and strengthen contract negotiations.

    For a broader view of waste reduction strategies, see how MES supports reducing scrap, rework, and material waste in aerospace manufacturing as a foundation for margin protection.

    Why Waste is So Dangerous in Fixed-Price Aerospace Programs

    Fixed-price and long-duration aerospace contracts lock in revenue while leaving most cost risk with the supplier. That structure amplifies the impact of scrap, rework, and material waste.

    Limited Ability to Pass Costs to Customers

    In many aerospace programs, contracts are structured as firm fixed-price, fixed-price with incentive, or long-term pricing agreements. Once the price per unit or per block of deliveries is agreed, your room to recover unplanned costs is limited.

    • Unplanned scrap of high-value materials (e.g., nickel alloys, titanium, composites) must usually be absorbed internally.
    • Extra rework hours consume capacity and increase overtime without a corresponding price increase.
    • Expedited materials and logistics to protect delivery dates often hit your P&L, not the customer’s.

    Without detailed, timely waste data, these costs accumulate gradually and only become visible when program margins are already compromised.

    Tight Margins and Long Production Horizons

    Aerospace programs often run for years or even decades, with cost curves expected to improve over time. In this environment:

    • Initial learning curve assumptions are built into bid models.
    • Planned rate increases depend on predictable cycle times and yields.
    • Suppliers commit to price reductions or productivity targets over the life of the contract.

    If scrap and rework rates stay higher than planned—even by a few percentage points—the impact on lifetime program margin can be substantial. MES helps teams detect when real-world waste performance diverges from the cost model early enough to intervene.

    Forecasting Challenges for Emerging Programs

    On new or ramping programs, forecasts are inherently uncertain. Engineering changes, immature processes, and supplier variability all introduce risk. Traditional quality systems that rely on sampling and end-of-line checks often miss small process deviations until multiple parts are affected.

    MES addresses this by:

    • Capturing real-time process data (machine parameters, operator inputs, environmental conditions).
    • Flagging out-of-tolerance trends before they produce large batches of non-conforming parts.
    • Enforcing standardized work instructions so new processes are executed consistently.

    The result is a faster feedback loop between the shop floor and program finance teams, reducing the gap between estimated and actual costs.

    Linking MES Waste Data to Program Financials

    To protect margins, waste metrics must be connected directly to program and contract financials. MES is the system of record for what actually happened during manufacturing; when integrated properly with ERP and program controls, it becomes a powerful financial lens.

    Attributing Scrap and Rework Costs to Specific Contracts

    Under fixed-price arrangements, the critical question is not just how much scrap or rework occurred, but which contract or customer it affected. MES enables this by:

    • Tracking every unit and lot by work order, contract number, and customer.
    • Recording scrap events with coded reasons (e.g., process deviation, supplier defect, programming error).
    • Logging rework operations, including additional labor, machine time, and consumables.

    When MES data is linked to cost rates from ERP, you can calculate:

    • Scrap cost per contract, part number, and configuration.
    • Rework labor and overhead by program.
    • Trends in waste by customer or major assembly group.

    This enables more accurate program margin analysis and targeted corrective actions.

    Understanding Cost per Good Piece by Configuration

    Aerospace products often have multiple configurations, options, or block points. The real cost per good piece can vary significantly depending on:

    • Configuration-specific processing sequences.
    • Different inspection requirements or special processes.
    • Distinct yield profiles for early versus mature designs.

    MES provides the necessary granularity by:

    • Tying each operation and inspection to a specific configuration or effectivity.
    • Capturing actual cycle times, scrap, and rework at the operation level.
    • Supporting traceability across serial numbers and lots.

    When combined with cost data, this gives program managers a clear view of cost per good piece by configuration, helping them understand where margin is being gained or lost.

    Supporting Earned Value and Program Reporting

    Many aerospace programs use Earned Value Management (EVM) or similar frameworks. MES can feed more accurate actuals into these models by providing:

    • Real-time actual hours consumed versus planned.
    • Visibility into rework hours that might not be obvious in high-level reports.
    • Accurate counts of accepted units versus scrapped or reworked quantities.

    With this data, cost performance index (CPI) and schedule performance index (SPI) reflect true execution performance rather than optimistic assumptions. Program teams can course-correct earlier and defend their forecasts with objective evidence.

    Reducing Cost Volatility with MES-Controlled Processes

    Margin protection on fixed-price contracts is not only about lowering average cost; it is about reducing cost volatility. MES-controlled processes make outcomes more predictable.

    Stabilizing Scrap and Rework Rates Over Time

    Most waste does not come from dramatic failures. It comes from small process deviations—a worn tool, a drifting fixture, a subtle setup mistake—that accumulate over time. MES helps stabilize performance by:

    • Monitoring key process parameters continuously instead of relying on periodic checks.
    • Issuing immediate alerts when parameters exceed tolerance.
    • Automatically placing holds on affected work orders to prevent further nonconforming production.

    By catching issues early, MES reduces the number of parts involved in each incident, smoothing waste rates and avoiding spikes that can wipe out a period’s margin.

    Reducing Schedule Risk from Unexpected Rework

    Rework can sometimes save expensive hardware, but it also:

    • Consumes finite capacity on critical machines and skilled labor.
    • Introduces additional risk of further nonconformances.
    • Threatens on-time delivery when discovered late in the process.

    MES mitigates these risks by:

    • Enforcing correct execution the first time with validated data entry and digital work instructions.
    • Routing nonconforming parts through controlled disposition and rework workflows.
    • Providing visibility into rework queues and cycle times for scheduling and capacity planning.

    Reduced surprise rework directly supports schedule adherence and avoids the expensive expediting often required to protect customer commitments.

    Improving Confidence in Rate Readiness

    As aerospace programs ramp from development to rate production, customers scrutinize suppliers’ ability to meet volume and quality targets. MES strengthens your case by providing:

    • Historical trends on scrap and rework rates by process and part family.
    • Evidence of process stability under increasing load.
    • Data-supported projections of first-pass yield at higher rates.

    This gives both your internal leadership and your customers greater confidence that quoted rates and costs are achievable, reducing the risk of margin-damaging surprises during ramp-up.

    Using MES Insights in Contract Negotiations and Change Management

    While MES cannot change the basic commercial structure of a fixed-price contract, it can materially improve your negotiating position and change management outcomes by supplying objective, detailed data. This data does not guarantee customer acceptance, but it provides a credible foundation for discussions.

    Providing Data-Backed Justification for Pricing and Surcharges

    When new proposals or re-pricing events arise, MES helps build more accurate cost models by:

    • Supplying actual cycle times by operation and configuration.
    • Quantifying scrap and rework rates for similar parts or processes.
    • Highlighting special process steps or inspections that drive cost.

    This allows commercial teams to justify pricing with concrete operational evidence rather than historical averages alone. In some cases, MES data may support discussions about surcharges or price adjustments when customer-driven changes clearly increase cost.

    Demonstrating Process Capability to Customers

    Aerospace OEMs and Tier 1s increasingly expect suppliers to demonstrate capability, not just quote a price. MES can support this by providing:

    • Capability summaries (e.g., yield, defect rates, process stability) for key operations.
    • Evidence of closed-loop corrective actions and sustained improvements.
    • Traceable histories showing how the plant responded to prior disruptions.

    These insights can improve your position in competitive bids and support conversations about risk-sharing and scheduling flexibility.

    Managing the Impact of Design and Scope Changes

    Design changes, new customer requirements, and scope expansions are facts of life in aerospace programs. MES helps quantify their impact by:

    • Simulating revised routing and operation sequences.
    • Estimating incremental cycle time and inspection effort based on similar past changes.
    • Tracking post-change scrap and rework trends to validate cost assumptions.

    This supports structured change management, helping both sides understand how new requirements affect cost and schedule. While MES data alone does not guarantee contractual relief, it makes your case more transparent and defensible.

    Metrics for Executives: From Plant Data to Program Health

    Executives need a concise set of metrics that connect MES data to program performance. The goal is to translate detailed shop-floor information into indicators that signal margin risk early.

    Scrap Cost as a Percentage of Contract Value

    One powerful metric is scrap cost as a percentage of contract or program value. To compute it, combine MES scrap quantities with material and processing costs from finance, and compare the result to total revenue on the contract.

    This view helps executives:

    • Identify programs where waste is reaching materiality thresholds.
    • Prioritize improvement projects where margin is most at risk.
    • Track the return on MES and process improvement investments.

    Rework Hours vs Planned Labor

    Another key indicator is the ratio of rework hours to planned production labor. MES can distinguish between planned operations and rework steps, allowing for:

    • Visibility into how much capacity is absorbed by non-value-added recovery work.
    • Comparison of actual rework effort to what was assumed in bids or budgets.
    • Trend analysis to see whether corrective actions are sustainable.

    High or rising rework ratios are early warning signs that program margins may be under pressure even if shipments and revenue appear on track.

    On-Time Delivery Performance Under Waste Control

    Fixed-price contracts often include delivery penalties or incentives. Waste and rework can quietly jeopardize on-time performance. MES supports more reliable delivery by:

    • Flagging potential schedule slips when scrap or rework events affect critical path components.
    • Providing accurate work-in-progress (WIP) status and queue times.
    • Helping planners and program managers re-sequence work to protect contractual dates.

    Tracking on-time delivery alongside waste metrics lets executives see whether improvements in scrap and rework are translating into reliable customer performance and preserved margin.

    Implementing MES for Financial Visibility

    To realize the margin-protection potential of MES, implementation must be designed with financial and contractual outcomes in mind—not just manufacturing efficiency.

    Aligning Finance, Operations, and IT Requirements

    Successful MES programs in aerospace bring together finance, operations, and IT to define:

    • Which waste categories matter most for margin (scrap, rework, consumables, overtime triggers).
    • How contracts and programs will be identified within MES and related systems.
    • What reporting granularity is required for program reviews and customer discussions.

    This alignment ensures that MES data structures support both operational control and program-level financial analysis from day one.

    Ensuring Accurate Cost Allocation in MES and ERP

    MES captures what happened; ERP and finance determine how costs are allocated. To link them effectively:

    • Use common keys and identifiers (work orders, WBS elements, contract numbers) across systems.
    • Define clear rules for how scrap and rework costs flow to programs and cost centers.
    • Regularly reconcile MES quantities with inventory and financial records.

    The tighter the integration, the more reliably you can translate execution data into meaningful financial insight without manual workarounds.

    Phasing Deployment by Highest-Risk Programs

    Not every program needs the same level of MES sophistication immediately. A pragmatic approach is to:

    • Identify high-value or low-margin contracts where waste poses the greatest financial risk.
    • Prioritize complex parts and special processes with historically higher scrap and rework.
    • Roll out MES capabilities in phases, starting with traceability, scrap capture, and rework control, then extending to advanced analytics.

    This sequencing accelerates financial impact and builds internal support using results from the most exposed programs.

    Communicating Value to Internal and External Stakeholders

    MES only protects margins if people understand and use the information it provides. Communicating value clearly is essential for sustaining investment and adoption.

    Framing MES Investments as Margin Protection

    Internally, MES is often viewed as an operations or IT project. To gain executive sponsorship, frame it as a margin protection initiative for fixed-price programs:

    • Quantify current scrap and rework cost exposures using available data.
    • Estimate potential savings from even modest yield improvements.
    • Highlight the role of MES in supporting accurate bids and avoiding surprises after contract award.

    This shifts the conversation from system features to financial outcomes.

    Reporting Improvements to OEMs and Regulators

    Aerospace customers and regulators care deeply about process control and traceability. MES can strengthen your external position by enabling:

    • Structured reports on defect reduction and process capability.
    • Transparent documentation of corrective and preventive actions.
    • Evidence of consistent compliance with approved processes.

    While this may not directly change pricing, it builds trust, supports supplier ratings, and can influence future sourcing decisions.

    Using Success Stories to Scale Across Programs

    Once MES has delivered measurable benefits on one or two programs, capture those results and use them to build momentum:

    • Document before-and-after metrics for scrap, rework, on-time delivery, and margin where possible.
    • Share case studies internally to show how data-driven decisions improved outcomes.
    • Incorporate lessons learned into standard deployment templates for new areas.

    Over time, this creates a culture where MES is viewed as an essential tool for managing the financial health of fixed-price aerospace contracts, not just a manufacturing system.

    By tightly linking MES waste data to program financials, aerospace manufacturers can move from reacting to margin erosion to proactively managing it—protecting profitability while delivering reliable performance to their customers.

  • Real-Time MES Monitoring and Alerts to Prevent Aerospace Scrap

    Real-Time MES Monitoring and Alerts to Prevent Aerospace Scrap

    Real-Time MES Monitoring and Alerts to Prevent Aerospace Scrap

    In aerospace manufacturing, scrap is not just a quality defect—it is a financial event that threatens margins, delivery performance, and customer confidence. Real-time monitoring and alerts in a Manufacturing Execution System (MES) give plants the ability to detect process drift and nonconformances early, before they cascade into large scrap events.

    This article explains which parameters to monitor, how to configure effective alerts, and how to balance sensitivity with alert fatigue so you can intervene early without slowing throughput.

    Most aerospace waste does not come from dramatic failures. It comes from subtle process deviations—tool wear, environmental changes, small setup errors—that go unnoticed until final inspection. By then, multiple high-value parts may already be affected. MES turns this reactive model into a proactive one by continuously capturing execution and quality data, comparing it to approved limits, and triggering alerts the moment risk appears.

    If you are also looking at the broader picture of waste reduction with MES in aerospace manufacturing, real-time monitoring and alerts are one of the most powerful levers you can deploy.

    The Cost of Late Detection in Aerospace Production

    In aerospace, late detection of defects amplifies both direct and indirect costs. The combination of expensive materials, complex routings, and strict regulatory requirements makes every scrap event disproportionately painful.

    High-value materials and long cycle times

    Aerospace components are often made from high-value alloys and composites and may require multiple specialized operations such as precision machining, heat treatment, surface treatment, and complex assembly. When a defect is discovered late, you do not just lose raw material—you lose all the value added at each prior operation.

    • Material loss: Titanium, nickel-based superalloys, and engineered composites are expensive and often subject to long lead times.
    • Value-add loss: Hours of machining, heat treatment cycles, and inspection effort are embedded in each part.
    • Limited rework options: Many aerospace specifications restrict or forbid rework, turning marginal parts into full scrap.

    Impact on delivery schedules and customer commitments

    Scrap discovered late in the route can break carefully planned production schedules.

    • Schedule slips: Replacing a scrapped part may require an entirely new build sequence, consuming capacity you did not plan for.
    • Knock-on effects: One late part can delay engine builds, aircraft assembly, or maintenance events downstream.
    • Customer impact: Missed delivery windows can trigger penalties or harm long-term relationships.

    Hidden rework and unplanned capacity consumption

    Not every late-detected defect is scrapped; some are reworked. But rework is often underestimated:

    • Capacity drain: Rework consumes machine time, fixtures, inspection, and engineering support that could have been used for first-pass yield.
    • Increased risk: Additional handling and processing introduce new opportunities for error.
    • Opaque cost: Without detailed execution data, true rework cost remains buried in overhead.

    Real-time MES monitoring does not eliminate scrap or rework altogether, but it significantly reduces their frequency and scale by surfacing problems earlier.

    Core MES Capabilities for Real-Time Monitoring

    To prevent scrap effectively, an MES needs more than simple data collection. It must connect execution data with rules and workflows that support fast, decisive action.

    Collecting process and quality data at the operation level

    Real-time monitoring starts with high-quality data collection close to the process:

    • Machine and sensor data: Temperatures, pressures, speeds, feeds, cycle times, torque, oven profiles, and more.
    • Inspection and measurement results: Dimensions, surface finish, hardness, and other quality checks captured through manual input or digital gaging.
    • Operator and setup inputs: Tool changes, fixture IDs, batch numbers for consumables, and special process parameters.

    MES ties this data to specific work orders, lots, and serial numbers, enabling precise traceability for aerospace audits and investigations.

    Defining control limits and tolerance bands

    Once data is available in real time, the next step is defining control limits. In an MES context, limits typically include:

    • Specification limits: The allowable range of a parameter on the part drawing or process specification.
    • Process control limits: Tighter internal limits that provide early warning before a parameter reaches the specification boundary.
    • Contextual limits: Conditions specific to a machine, tool, batch, or customer program.

    These limits should be derived collaboratively by quality, manufacturing engineering, and process specialists, using historical data where possible rather than guesswork.

    Event-driven alerts vs. periodic reports

    Periodic reports are useful for trend analysis, but they are too slow to prevent many scrap events. Real-time MES adds:

    • Event-driven alerts: Immediate notifications triggered when data crosses defined conditions (e.g., a temperature exceeds its upper limit for more than a set time).
    • Escalation logic: Rules that escalate to supervisors, quality, or engineering when critical events occur or when lower-priority alerts remain unresolved.
    • Actionable context: Alerts that include the affected lot, operation, machine, and recent history so responders can act quickly.

    This shift from after-the-fact reports to in-the-moment alerts is what enables early intervention.

    Choosing What to Monitor in Aerospace Processes

    Monitoring every available signal with equal priority is neither practical nor desirable. An effective strategy focuses on parameters that meaningfully affect airworthiness, compliance, and cost.

    Critical-to-quality (CTQ) characteristics

    Start with characteristics that are directly critical to performance and safety:

    • Structural dimensions: Features affecting fit, load paths, or clearance.
    • Material properties: Hardness, tensile strength, or grain structure after heat treatment.
    • Functional surfaces: Seal faces, bearing journals, aerodynamic surfaces, or interfaces with mating components.

    For CTQs, consider early-warning limits stricter than drawing requirements so that subtle shifts are detected before nonconformance occurs.

    Environment, tool, and setup variables

    Many aerospace defects originate not in the part itself, but in the process conditions around it:

    • Environment: Temperature, humidity, and contamination levels in areas like composite layup, bonding, or painting.
    • Tooling and fixtures: Tool age, wear indicators, calibration status, and correct fixture or program selection.
    • Setup parameters: Correct NC program version, work offset selection, clamping sequence, and verified tool lists.

    MES can monitor these variables by integrating with machines and sensors, enforcing checklists, and validating scanned IDs or barcodes at each operation.

    Inspection results and operator inputs

    In many aerospace shops, critical knowledge still lives in operators’ heads or on paper. Real-time MES monitoring brings this into the digital workflow:

    • In-process inspection data: Periodic measurements during long runs or complex setups.
    • Visual defect logging: Operator-recorded defects, anomalies, or unusual sounds/vibrations.
    • Process confirmations: Sign-offs that specific steps, holds, or special process requirements were followed.

    Clarify the operational risk

    When the work behind Real-Time MES Monitoring and Alerts affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in Real-Time MES Monitoring and Alerts

    When this information is captured at the point of execution, MES can apply rules and trigger alerts based on patterns that would otherwise be invisible.

    Designing Effective MES Alerts

    Well-designed alerts help teams stop defects before they multiply. Poorly designed alerts create noise, slow production, and erode trust in the system. The goal is targeted sensitivity: enough to catch meaningful risk, but not so much that operators feel overwhelmed.

    Thresholds, trends, and rule-based logic

    Effective alerting uses a mix of simple thresholds and more advanced logic:

    • Threshold-based alerts: Triggered when a single value falls outside a defined band (e.g., pressure below a minimum limit).
    • Trend-based alerts: Triggered when a parameter is drifting toward a limit over time, even if still within spec.
    • Rule-based alerts: Triggered by combinations such as a specific CTQ deviation plus a particular machine, tool, or batch of material.

    In aerospace environments, trend and rule-based alerts are especially useful for catching subtle process drift before it crosses formal specification limits.

    Prioritizing alerts by risk and cost of failure

    Not all alerts deserve the same urgency. Prioritization should reflect both safety and cost:

    • Safety and airworthiness: Parameters tied directly to flight safety or regulatory compliance should generate high-priority alerts with clear escalation paths.
    • High scrap cost: Operations that consume expensive material or long cycle times merit stricter monitoring and faster response.
    • Containment complexity: Processes where defects are hard to detect later (e.g., embedded features) should be monitored more closely.

    Defining clear alert levels (for example, informational, warning, critical) helps operators and supervisors decide when immediate intervention is required.

    Avoiding alert fatigue among operators and engineers

    Alert fatigue—when users stop paying attention due to excessive or low-value notifications—is a real risk. To avoid it:

    • Limit alerts to actionable conditions: Every alert should imply a clear action or decision.
    • Minimize duplicates: Suppress repeated alerts for the same condition once acknowledged, and group related events.
    • Use meaningful messages: Include the affected operation, part or lot ID, parameter, current value, and recommended next steps.
    • Review usage data: Periodically analyze which alerts are acknowledged, ignored, or overridden to refine the rules.

    The objective is quality attention, not constant attention. A smaller number of well-targeted alerts will prevent more scrap than a flood of low-importance messages.

    Workflow After an Alert: From Response to Resolution

    Real-time alerts only deliver value when they trigger the right actions. MES should embed a consistent, auditable workflow from the moment an alert fires through to resolution.

    Automatic holds on work orders and lots

    For high-risk situations, MES can automatically place holds on affected work orders, lots, or serial numbers:

    • Immediate containment: Prevents suspect parts from moving to the next operation or shipping stage.
    • Targeted scope: Uses traceability data to identify which parts, tools, batches, or time windows are impacted.
    • Controlled release: Requires documented review and approval, often by quality or engineering, before holds are lifted.

    Guided troubleshooting steps in MES

    To support fast and consistent response, alerts should be tied to standard troubleshooting guidance:

    • Checklists: Step-by-step validation of machine status, tooling, programs, and setup conditions.
    • Decision trees: Logic that guides users based on what they find (e.g., different actions if tool wear is detected versus a fixture issue).
    • Integration with NCR and CAPA workflows: Automatic creation of nonconformance records or corrective action requests when certain thresholds are met.

    Embedding this guidance in MES helps ensure that different shifts and sites respond consistently to the same signals.

    Documentation and learning from each event

    Every alert is an opportunity to learn about process behavior:

    • Root cause capture: Documented conclusions on what actually caused the deviation.
    • Effectiveness checks: Follow-up to confirm that corrective actions prevented recurrence.
    • Feedback into rules: Adjusting alert thresholds, logic, or workflows based on what the team learned.

    Over time, this closed-loop approach sharpens both the process and the alerting strategy, reducing the number of significant events while maintaining protection against scrap.

    Case Examples: Catching Scrap Before It Scales

    The following examples illustrate how real-time MES monitoring and alerts can catch problems early. These are representative scenarios; each facility should tailor its approach based on its own processes, data, and risk profile.

    Detecting thermal profile drift in heat treatment

    Heat treatment is critical for achieving required material properties in aerospace components. Small deviations in temperature or soak time can render entire loads suspect.

    • Monitoring: MES collects furnace data—zone temperatures, ramp rates, soak times, and quench delays—in real time.
    • Alerting: Rules trigger warnings when temperatures trend toward control limits and critical alerts when they exceed them for more than a defined duration.
    • Outcome: Operators are prompted to intervene or adjust the load setup before parts are fully processed, reducing the risk of scrapping costly parts or entire loads.

    Catching mis-loaded programs in machining cells

    In a multi-part machining cell, loading the wrong NC program or an outdated revision can quickly generate multiple nonconforming parts.

    • Monitoring: MES validates that the active NC program ID and revision match the work order, part number, and operation.
    • Alerting: If a mismatch is detected, MES issues an immediate alert, stops the operation, and places a hold on the suspect parts.
    • Outcome: Only a small number of parts (or none) are affected, avoiding a broader scrap or rework event.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for Real-Time MES Monitoring and Alerts

    Identifying out-of-spec surface treatment conditions

    Surface treatments such as plating, coating, and anodizing often have tight process windows for bath chemistry, temperature, and current density.

    • Monitoring: MES ingests sensor and lab data for bath composition, pH, temperature, and current parameters, linked to each load.
    • Alerting: Deviations from configured control limits generate alerts; if persistent, the system can automatically quarantine affected loads for review.
    • Outcome: Potential nonconformances are contained before treated parts move to downstream operations or customers, reducing the scale and cost of any necessary rework or scrap.

    Governance and Continuous Improvement of Alert Rules

    Real-time monitoring is not a one-time configuration exercise. As processes, products, and data maturity evolve, alert rules should evolve as well.

    Tuning limits based on historical data

    Historical MES data is a powerful resource for improving alert performance:

    • Baseline behavior: Understand normal process variation before setting tight limits.
    • Correlation analysis: Identify which parameters and patterns actually correlate with nonconformances or rework.
    • Refinement: Gradually adjust control bands and logic to reduce false positives without sacrificing protection.

    Because aerospace processes and equipment differ widely, generic limit values are rarely appropriate; tuning should be done using your own data and expertise.

    Involving quality and manufacturing engineering

    Effective alert governance is cross-functional:

    • Quality: Ensures alerts align with specifications, risk assessments, and audit expectations.
    • Manufacturing engineering: Brings deep understanding of process capability and practical constraints.
    • Operations leadership: Balances responsiveness with throughput and resource availability.

    Define clear ownership for individual alert rules, along with a process for proposing, reviewing, approving, and retiring them.

    Aligning alerts with customer and regulatory requirements

    Aerospace programs often have customer-specific and regulatory requirements that influence monitoring and alerting:

    • Customer specifications: Some programs mandate particular process controls, inspection frequencies, or data retention practices.
    • Regulatory standards: Requirements from authorities and industry standards bodies affect traceability, documentation, and process validation.
    • Audit readiness: Well-governed alerts, with documented rationale and change history, support smoother audits and customer reviews.

    By embedding these requirements into MES alert rules and workflows, aerospace manufacturers can reduce risk proactively rather than reacting during audits or after-field events.

    Putting It All Together

    Real-time MES monitoring and alerts will not guarantee zero scrap, but they are among the most effective tools available to reduce the frequency and scale of waste in aerospace manufacturing. By focusing on critical parameters, designing actionable and prioritized alerts, and continuously refining rules based on real data, plants can catch issues early—often when only a handful of parts are at risk.

    Combined with strong containment workflows, guided troubleshooting, and disciplined governance, this approach protects margins, supports on-time delivery, and builds confidence with aerospace customers that your processes are under control.

    For teams putting this topic into daily operation, work orders and digital travelers, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    This article is for aerospace operations, quality, and compliance teams who need to understand Real-Time MES Monitoring and Alerts to Prevent Aerospace Scrap. It explains the practical question this topic answers in a manufacturing execution context.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

  • How Real-Time MES Monitoring and Alerts Reduce Scrap in Aerospace Manufacturing

    How Real-Time MES Monitoring and Alerts Reduce Scrap in Aerospace Manufacturing

    Scrap in aerospace manufacturing is more than a quality problem—it is a financial event. Losing a single high-value forging, composite layup, or machined structure can erase the margin on an entire order and ripple through delivery schedules and customer commitments.

    Most of that waste does not come from dramatic failures. It comes from small process deviations that quietly accumulate between inspections. Real-time monitoring and alerts in a Manufacturing Execution System (MES) give aerospace plants a way to detect those deviations early, intervene before scrap multiplies, and protect throughput and on-time delivery.

    This article explains which parameters to monitor, how to design effective alerts, and how to respond when MES detects a problem—all with a focus on real time MES monitoring in aerospace environments.

    For a broader view of how MES cuts scrap and waste across the value stream, see our guide on waste reduction with MES in aerospace manufacturing.

    The Cost of Late Detection in Aerospace Production

    High-value materials and long cycle times

    Aerospace parts often combine expensive materials, complex routings, and long cycle times. When a defect is found late—for example, at final inspection—you are not just scrapping material. You are discarding:

    • Machine time and labor across multiple operations
    • Consumables, tooling life, and utilities
    • Occupied capacity that could have produced good parts

    In some programs, rework is tightly controlled or prohibited entirely. A nonconformance discovered late can mean a total loss, plus the cost of expediting a replacement.

    Impact on delivery schedules and customer commitments

    When defects are found only at end-of-line inspection, the recovery path usually involves:

    • Re-planning production to squeeze in replacement parts
    • Premium freight for materials or finished goods
    • Negotiations around missed milestones or penalty clauses

    Because cycle times are long, there may be no quick way to replace scrapped parts without displacing other work. This erodes customer confidence and increases program risk.

    Hidden rework and unplanned capacity consumption

    Even when parts can be saved, rework often hides the real cost of late detection. Rework consumes:

    • Engineering time to evaluate dispositions and concessions
    • Quality resources for additional inspections and documentation
    • Production capacity that should be producing conforming parts

    Without good traceability and real-time visibility, these costs can be buried in overhead. MES exposes this waste and, more importantly, helps prevent it by catching deviations as soon as they appear.

    Core MES Capabilities for Real-Time Monitoring

    Collecting process and quality data at the operation level

    Real-time MES monitoring in aerospace starts with data collection at the point of execution. This typically includes:

    • Process parameters (temperatures, pressures, speeds, feeds, flows, times)
    • Machine and cell status (run, idle, fault, setup, changeover)
    • In-process inspection results (dimensional checks, NDT results, visual inspections)
    • Operator inputs (checklists, confirmations, defect codes, comments)

    The MES associates this data with specific work orders, serial numbers, and operations. That traceability is crucial in aerospace, where requirements from customers and regulators demand clear evidence of how each part was produced.

    Defining control limits and tolerance bands

    To enable real-time monitoring, the MES needs to know what “good” looks like. This usually involves:

    • Nominal values for process parameters (e.g., target temperature or torque)
    • Specification limits from engineering drawings or process sheets
    • Control limits or tighter warning bands based on historical performance

    In many aerospace operations, especially special processes like heat treatment, coating, or bonding, the acceptable window may be narrow. The MES compares incoming data against these configured limits in real time and generates events when something drifts or crosses a boundary.

    Event-driven alerts vs. periodic reports

    Traditional quality systems often rely on daily or weekly reports, or batch uploads from machines. By the time someone analyzes the data, defects may already have multiplied.

    With real-time MES monitoring:

    • Event-driven alerts fire immediately when a rule is violated (e.g., a temperature exceeds its upper limit).
    • Trend-based notifications can indicate drift before a parameter leaves its tolerance band.
    • Dashboards show current status at the line, cell, or plant level for supervisors and engineers.

    Periodic reports still have value for analysis and improvement, but the primary protection against scrap comes from event-driven, in-the-moment feedback.

    Choosing What to Monitor in Aerospace Processes

    Critical-to-quality (CTQ) characteristics

    Not every parameter warrants a real-time alert. In aerospace, a practical starting point is to focus on critical-to-quality (CTQ) characteristics—those with the highest impact on safety, performance, and compliance. Examples include:

    • Key dimensions on flight-critical or rotating components
    • Bond-line thickness in composite assembly
    • Heat treatment profiles for structural alloys
    • Coating thickness and cure profiles on corrosion-critical surfaces

    By mapping CTQs to process steps in the MES, you can ensure that critical characteristics are measured, recorded, and monitored continuously where it matters most.

    Environment, tool, and setup variables

    Many defects originate not from the part itself but from its environment and setup. Real-time MES monitoring can track:

    • Ambient conditions (temperature, humidity) for processes where they affect cure, adhesion, or dimensional stability
    • Tooling and fixture status (tool life, calibration dates, fixture ID and verification)
    • Setup verification (correct program loaded, correct tooling loaded, correct material and revision)

    By alerting on these factors, the MES can catch problems like out-of-calibration tools, incorrect fixtures, or misconfigured programs before they impact multiple parts.

    Inspection results and operator inputs

    Inspection and operator feedback are often early indicators of problems. An effective MES will:

    • Capture in-process inspection results directly at the station
    • Compare those values to drawing tolerances or control limits
    • Allow operators to flag suspected issues or enter defect codes

    When an operator reports a recurring defect or borderline measurement, the MES can trigger alerts to quality and engineering, initiating investigation before the issue spreads.

    Designing Effective MES Alerts

    Thresholds, trends, and rule-based logic

    Effective alerts in aerospace MES implementations are rarely based on a single hard threshold. Common patterns include:

    • Limit violations: A parameter crosses a high or low limit.
    • Trend detection: A sequence of measurements shows consistent drift in one direction.
    • Rule-based logic: Combinations of conditions (e.g., “IF temperature is high AND dwell time is short THEN alert”).

    Clarify the operational risk

    When the work behind How Real-Time MES Monitoring and affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in How Real-Time MES Monitoring and

    Trend and rule-based alerts are especially useful for catching issues early, when parameters are still technically in tolerance but migrating toward an out-of-spec condition.

    Prioritizing alerts by risk and cost of failure

    Not all alerts are equal. To keep focus on what matters most, aerospace plants typically tier alerts, such as:

    • Critical: Potential impact on safety-of-flight or regulatory compliance; requires immediate action and often an automatic hold.
    • High: Likely to result in scrap or major rework if not addressed promptly.
    • Medium/Low: Early warnings, trends, or minor deviations that can be addressed in routine reviews.

    Prioritization helps ensure that the most serious issues are impossible to ignore while less urgent signals are still visible but not disruptive.

    Avoiding alert fatigue among operators and engineers

    Alert fatigue occurs when personnel receive so many notifications that they begin to ignore or routinely dismiss them. To avoid this in real time MES monitoring for aerospace:

    • Limit alerts on non-critical parameters; use dashboards or periodic summaries instead.
    • Consolidate related conditions into a single alert event when possible.
    • Set sensible deadbands or timers so alerts do not repeatedly fire for minor oscillations.
    • Review alert volumes regularly; disable or tune rules that generate frequent but low-value notifications.

    Well-designed alerts should be meaningful, actionable, and rare enough that operators treat them as important signals, not background noise.

    Workflow After an Alert: From Response to Resolution

    Automatic holds on work orders and lots

    When an alert indicates a potential nonconformance, speed matters. MES can automatically:

    • Place the affected lot, serial number, or work order on hold
    • Prevent further processing or shipment until evaluation is complete
    • Flag related parts that went through the same operation or setup window

    This containment limits exposure while engineers and quality teams investigate. Automatic holds are especially important when the suspected issue involves flight-critical components or special processes.

    Guided troubleshooting steps in MES

    To avoid ad-hoc responses, aerospace MES workflows often provide:

    • Standard response plans linked to specific alert types
    • Checklists for operators and technicians (e.g., verify tooling, confirm program version, inspect fixture)
    • Data capture forms for documenting findings, measurements, and interim actions

    By embedding troubleshooting guidance directly in the MES, plants can shorten response times and ensure that corrective actions are consistent and well documented.

    Documentation and learning from each event

    Every alert is an opportunity to strengthen the process. MES can support continuous improvement by:

    • Capturing the root cause analysis and final disposition
    • Linking alerts to corrective and preventive actions (CAPA)
    • Tracking how often specific alerts occur and how they are resolved

    Over time, this history helps engineers refine limits, update work instructions, and improve equipment maintenance plans—gradually reducing both scrap and the frequency of serious alerts.

    Case Examples: Catching Scrap Before It Scales

    Detecting thermal profile drift in heat treatment

    Consider a heat treatment furnace used for structural alloy components. The MES continuously records:

    • Zone temperatures at defined intervals
    • Soak times and ramp rates
    • Load details (part numbers, quantities, locations)

    Alert rules watch for trends where one zone begins to underperform relative to others. Before any run actually violates specification limits, the MES detects a pattern of slow drift and notifies engineering. The result:

    • Maintenance can investigate the heating elements and controls.
    • Potential nonconformances are caught before multiple loads are affected.
    • Scrap risk is reduced without stopping the furnace unnecessarily.

    Catching mis-loaded programs in machining cells

    In a flexible machining cell, each part number requires a specific NC program and tooling setup. The MES integrates with the machine controllers to verify:

    • Correct program revision is loaded for the scheduled part
    • Tool list matches the approved setup for that operation
    • Offsets and work coordinates are within expected ranges

    If an operator attempts to start a cycle with a mismatched program, the MES generates an alert and prevents machining from starting. This avoids the scenario where dozens of high-value parts are machined with an incorrect revision before anyone notices at inspection.

    Identifying out-of-spec surface treatment conditions

    Surface treatments such as anodizing, coating, or plating are common special processes in aerospace. MES can monitor:

    • Bath chemistry (concentration, pH, conductivity)
    • Temperature and agitation parameters
    • Exposure times for each rack or part

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for How Real-Time MES Monitoring and

    When any parameter trends toward the edge of its allowable range, the MES issues alerts to operators and process engineers, who can perform corrective actions such as adjusting chemistry or scheduling tank maintenance. This reduces the chance that large batches of parts will require stripping and reprocessing or, in the worst case, scrapping.

    Governance and Continuous Improvement of Alert Rules

    Tuning limits based on historical data

    Initial MES alert limits are often set conservatively based on specifications and engineering judgment. Over time, historical data from real-time monitoring allows teams to:

    • Identify normal process variation and tighten or widen warning bands accordingly
    • Spot parameters that rarely move and may not need real-time alerts
    • Recognize patterns that precede failures and design better trend rules

    This tuning process helps balance early detection with operational stability, ensuring alerts are both sensitive and meaningful.

    Involving quality and manufacturing engineering

    Effective governance of MES alerts requires cross-functional collaboration. Common practices include:

    • Defining an alert ownership model (who maintains which rules, who responds)
    • Reviewing alert performance metrics (volume, response time, outcomes)
    • Formal change control for modifying alert logic on critical CTQs

    Quality, manufacturing engineering, maintenance, and operations should all have a voice in how alerts are configured and maintained, especially in aerospace programs with demanding customer and regulatory oversight.

    Aligning alerts with customer and regulatory requirements

    Many aerospace customers and authorities require evidence that processes are controlled and that special processes are monitored. Real-time MES monitoring and alerting can support this by:

    • Providing audit-ready records of process parameters and alert responses
    • Demonstrating that CTQ characteristics and special processes are actively controlled
    • Linking nonconformance events to traceable alert histories and actions

    While no monitoring system can guarantee zero scrap, a well-governed MES alert framework shows due diligence in risk reduction and process control—key points in customer and regulatory reviews.

    Using Real-Time MES Monitoring to Reduce Scrap Without Slowing Throughput

    Real-time MES monitoring and alerts are most valuable when they prevent problems, not when they repeatedly stop production. By focusing on high-risk CTQs, tuning thresholds over time, and designing clear response workflows, aerospace manufacturers can:

    • Detect process drift before it creates large scrap events
    • Contain and analyze potential nonconformances quickly
    • Reduce unplanned rework and protect limited capacity
    • Provide stronger evidence of process control to customers and regulators

    Real-time alerts do not eliminate scrap, but they are powerful risk-reduction tools. When implemented thoughtfully as part of a broader MES strategy for waste reduction with MES in aerospace manufacturing, they help protect margins, schedules, and reputation in a highly demanding industry.

    For teams putting this topic into daily operation, work orders and digital travelers, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    This article is for aerospace operations, quality, and compliance teams who need to understand How Real-Time MES Monitoring and Alerts Reduce Scrap in Aerospace Manufacturing. It explains the practical question this topic answers in a manufacturing execution context.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.