Blog

  • Aerospace Manufacturing Operations: Executive Guide for Modern Programs

    Aerospace Manufacturing Operations: Executive Guide for Modern Programs

    The aerospace industry in 2025 and 2026 faces a straightforward reality: backlogs are growing, fleets are aging, and the operational approaches that worked a decade ago cannot deliver the throughput required today. COOs and plant leaders must answer a practical question over the next 12 to 24 months. What should we actually do differently in our operations?

    Aerospace manufacturing operations represent the integrated system where precision engineering meets rigorous production standards. This encompasses concept design through industrialization, sourcing raw materials like titanium alloys and ceramic matrix composites, high-volume production via CNC machining and additive manufacturing, final assembly with automated systems, extensive testing, certification under AS9100 and FAA frameworks, delivery to OEMs, and ongoing aftermarket MRO involving disassembly, inspection, repair, and recertification.

    This executive guide connects ERP, MES, quality systems, workforce management, and digital execution strategies into a coherent operational framework. The perspective comes from Connect981, a B2B SaaS platform built specifically for aerospace manufacturing and MRO realities rather than generic discrete manufacturing.
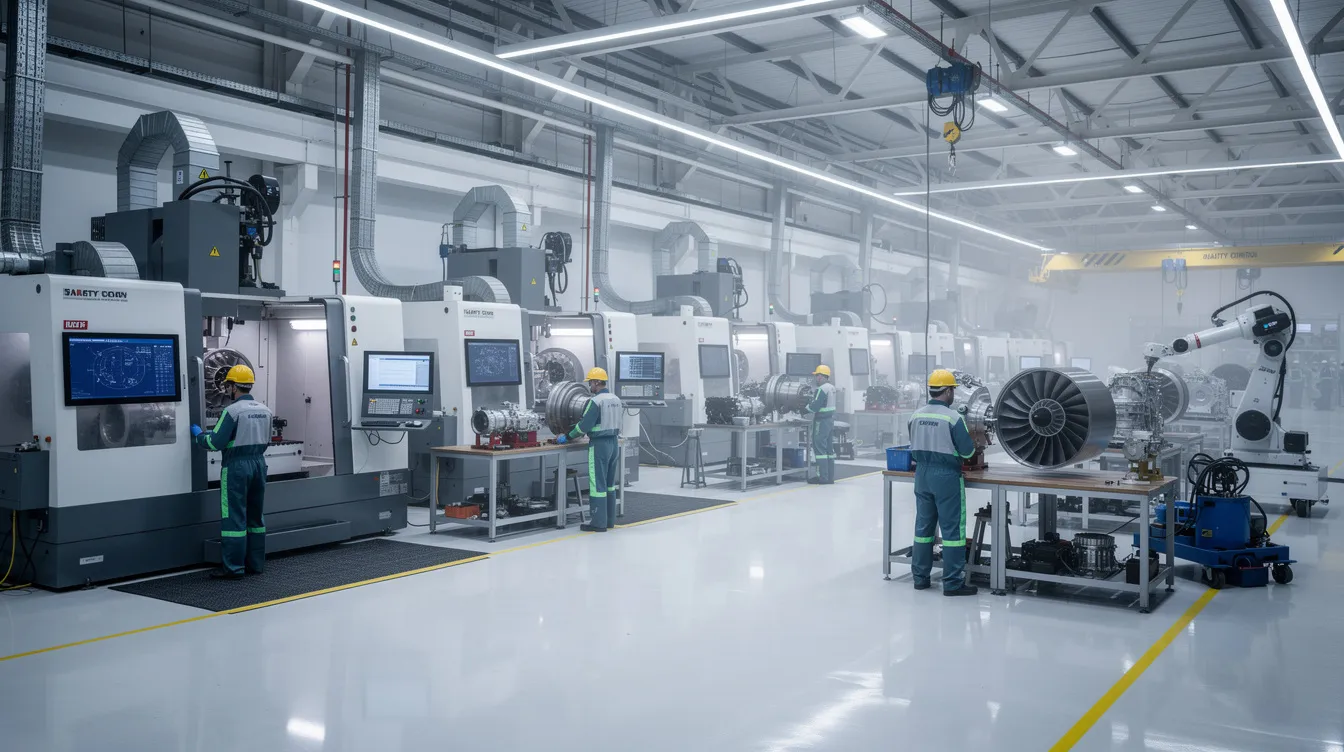
    The image depicts a busy aerospace factory floor, showcasing precision machinery and workers engaged in the aerospace manufacturing process within a controlled environment. This setting highlights advanced manufacturing technologies and emphasizes the importance of safety and performance standards in the aerospace industry.

    The State of Aerospace Manufacturing and MRO in 2025–2026

    The global aerospace parts manufacturing market stood at approximately $930 billion in 2024, projected to reach $1.2 trillion by 2034 with a CAGR of 3.8%. North America continues to dominate due to its mature ecosystem, defense contracts, and leadership in advanced manufacturing technologies including digital twins and AI-powered quality control.

    Key demand drivers shaping aerospace operations include:

    • Commercial aviation recovery with Airbus holding 8,617 outstanding orders and Boeing at 6,528 as of May 2025, translating to roughly 5,000 undelivered aircraft
    • Defense modernization accelerating hypersonics, UAVs, and autonomous systems requiring high production rates
    • Commercial space expansion via reusable launch vehicles and satellite constellations
    • Fleet aging to 11.3 years from 9.7 in 2018, with airlines extending leases 11% more in 2024 versus 2018

    Operational realities include chronic supply chain instability with 12 to 24 month lead times for titanium alloys, semiconductor shortages, and labor constraints with over 60% of aerospace manufacturers citing workforce issues. Certification timelines stretch 6 to 12 months for simple parts and up to 7 years for complex systems such as engines or airframes.

    MRO growth has become a strategic focus area. Engine scarcity crises are reshaping aftermarket economics, with new capacity expansions emerging in Middle East and Asia hubs to address turnaround time pressures.

    Core Building Blocks of Aerospace Manufacturing Operations

    The aerospace manufacturing process follows an end-to-end value chain:

    • Concept design in PLM systems managing configurations and BOMs
    • Industrialization creating build books and route cards
    • Sourcing with approved vendor lists tracking heat lots and batches
    • Production via shopfloor execution with travelers and digital work instructions
    • Final assembly and test incorporating NDT signoffs and torque verifications
    • Certification via AS9102 FAIs and AS9145/APQP processes
    • Delivery and ongoing aftermarket MRO

    The main operational domains include:

    Domain

    Key Activities

    Artifacts

    Engineering and Industrialization

    ECO management, configuration control

    Build books, route cards

    Shopfloor Execution

    WIP tracking, operation sequencing

    Travelers, work instructions

    Quality and Compliance

    CAPA workflows, audit trails

    FAIRs, nonconformance records

    Supply Chain Management

    Supplier OTD, PPM monitoring

    Approved vendor lists, POs

    MRO Operations

    Dynamic routing, findings management

    Task cards, SB/AD compliance logs

    The typical system landscape features ERP for finance and inventory, PLM for design revisions, MES for machine scheduling and OEE, and QMS for nonconformance and audits. Gaps persist in operator guidance, rich routing logic, and cross-system unification. A digital operations layer like Connect981 emerges as the connective tissue, aggregating data without replacing core systems.

    Operational Visibility for Aerospace Leaders

    COOs and plant managers need real-time visibility across programs, sites, and suppliers to monitor WIP status, bottlenecks, quality escapes, and MRO turnaround times. Current visibility gaps typically manifest as weekly slide decks, manual status spreadsheets, email updates from suppliers, and poor cross-site comparability.

    Modern operational visibility means unified dashboards pulling from ERP, MES, QMS, and execution systems into a single pane of glass. Role-based views allow plant managers to see site performance while program leaders track cross-factory progress.

    KPIs aerospace executives should see at a glance:

    • OTD by program targeting 95%+ for tier-1 suppliers
    • First-pass yield typically 85-95% in precision machining
    • Rework rate ideally under 5%
    • Hours per unit by operation
    • TAT by MRO routing with 30-60 day targets for engine shops
    • AS9100 and FAA audit findings trends
    • Supplier delivery and quality performance metrics

    Connect981 acts as that visibility layer by aggregating work order execution data, digital work instructions status, and supplier workflow milestones into live reports. Site comparison views allow leaders to identify which facilities execute similar operations faster and why.
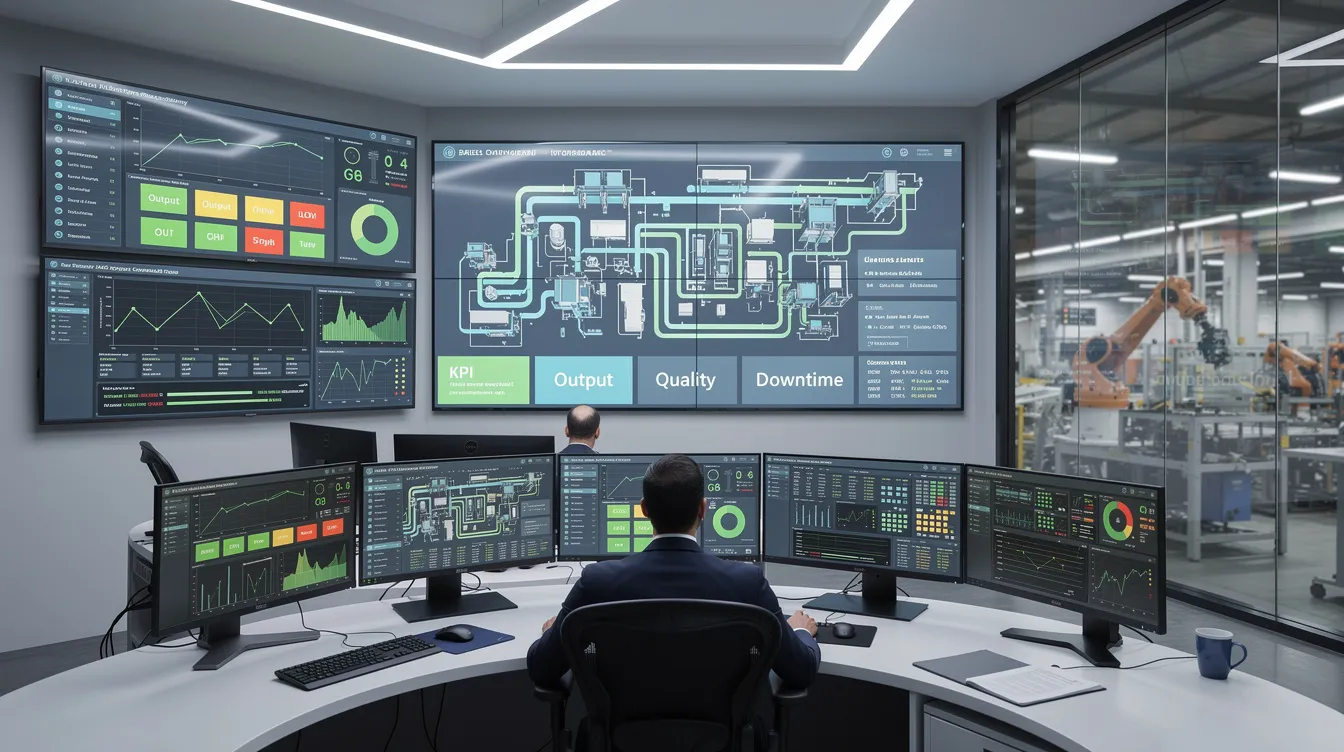
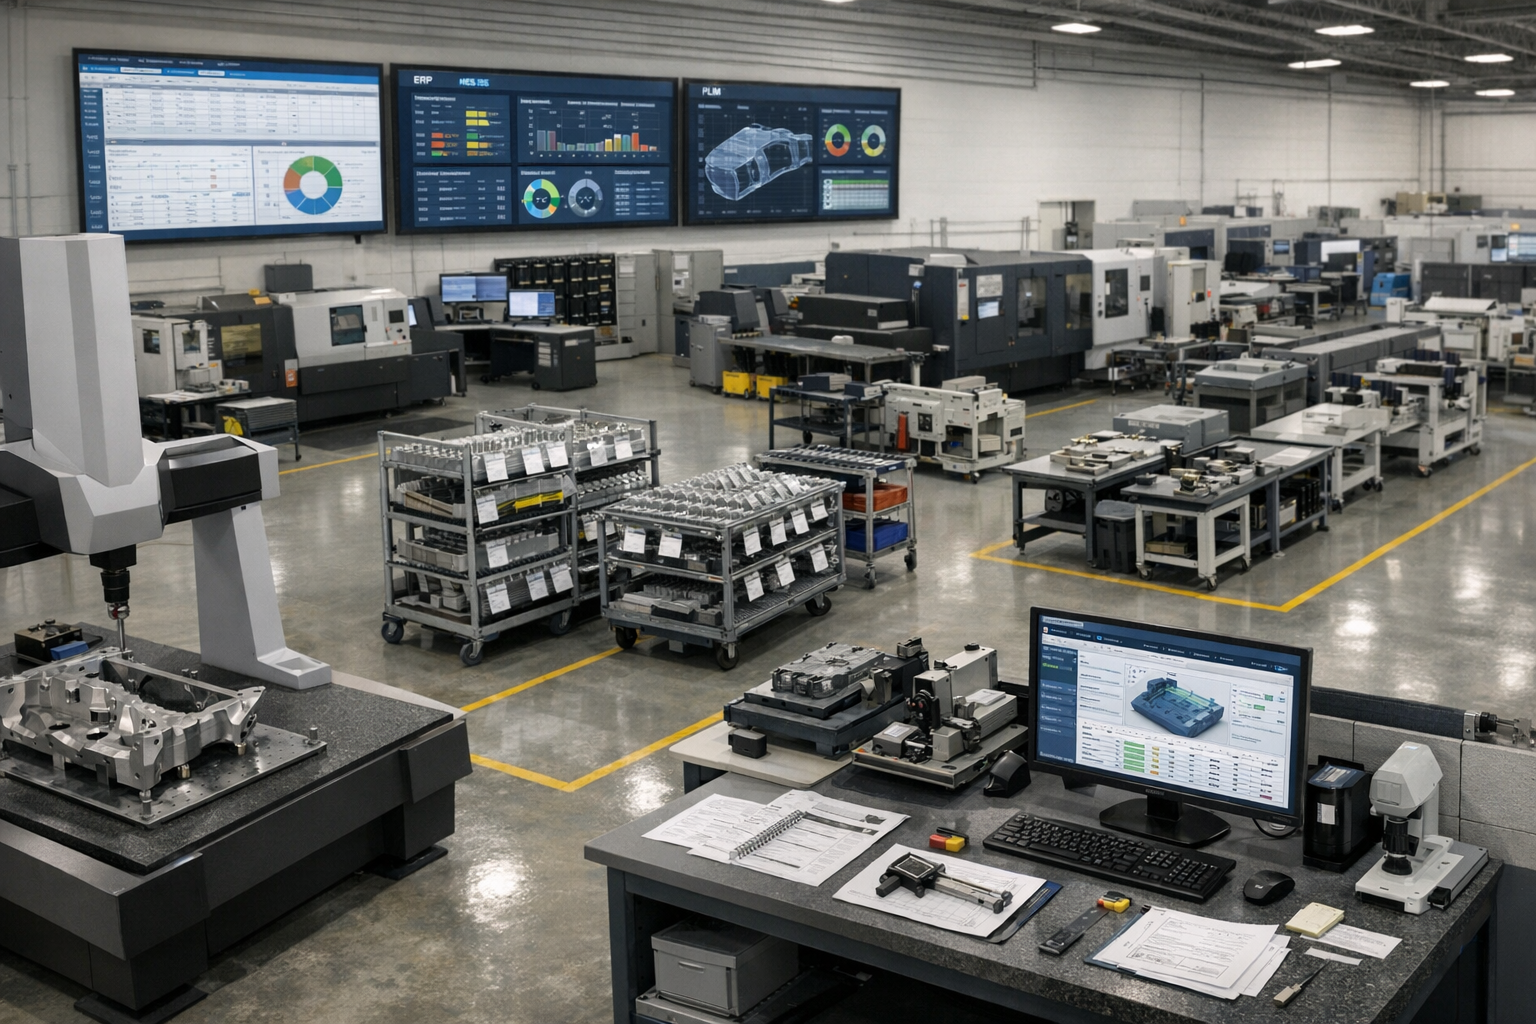
    The image depicts a modern manufacturing control room featuring multiple digital dashboards that showcase real-time production data essential for optimizing aerospace manufacturing processes. This high-tech environment highlights the integration of advanced manufacturing technologies to enhance operational efficiency and ensure compliance with safety and performance standards.

    Scaling Aerospace Programs Without Losing Control

    Ramping a new aircraft, engine, or subsystem program from prototype to LRIP and then to full-rate production presents specific challenges between 2025 and 2030. Commercial aerospace sector OEM ambitions frequently outpace supply chain capacity, while defense industry rapid capability deployment demands accelerated timelines.

    Pain points during scale-up include:

    • Configuration proliferation from engineering change orders
    • Late-breaking engineering changes disrupting production schedules
    • Incomplete build documentation causing rework
    • Inconsistent processes across plants and suppliers amid backlogs

    Standardized digital work packages address these challenges. Routing, work instructions, inspection plans, torque charts, and test steps can synchronize multiple lines via template-based workflows and controlled revision releases. Automated alerts flag when work starts on superseded revisions.

    Scalable operations require governance around AS9100, AS9102 FAI, AS9145/APQP, and NADCAP processes built into daily execution rather than living only in manuals. Complex geometries requiring hybrid additive-traditional manufacturing methods demand consistent documentation across facilities.

    A digital execution layer like Connect981 supports consistent rollouts across multiple factories and suppliers without forcing a full MES overhaul. Templates propagate instantly, and revision control ensures every site works from current documentation.

    Workforce Productivity and the Aerospace Skills Gap

    The aerospace sector faces a skills challenge with high retirement rates among experienced mechanics and machinists combined with difficulty attracting younger talent into complex, regulated environments. Over 60% of aerospace manufacturers cite workforce issues as a primary constraint, with UK manufacturers reshoring over 50% of production to mitigate risks.

    Typical productivity drains include:

    • Searching for the correct revision of work instructions
    • Walking to paper binders for reference documents
    • Re-entering data from travelers into systems
    • Manual article inspection documentation for FAIRs

    Digital work instructions with embedded photos, 3D models, torque charts, and checklists shorten onboarding time by 30-50% and reduce dependency on tribal knowledge. A technician drilling composite panels or assembling wiring harnesses can follow visual guidance rather than interpreting text-heavy procedures.

    AI assistance in platforms like Connect981 guides technicians through root cause analysis, suggests likely causes of recurring defects, and flags missing quality steps. Before digitization, paper-based operations typically take 20-30% longer per unit than digitized flows that capture timestamps and parameters automatically.

    An aerospace technician is focused on a tablet device while working on an aircraft component, highlighting the integration of digital tools in the aerospace manufacturing process. This scene emphasizes the importance of technology in optimizing production processes and ensuring quality control in the aerospace industry.

    Digital Execution Layers vs. Traditional MES and ERP

    Understanding the difference between core transaction systems, heavy MES layers, and modern lightweight digital execution platforms clarifies where gaps exist.

    ERPs handle orders, finance, and inventory well but fall short on operator guidance, in-process quality checks, and detailed traceability at the operation level. Traditional MES manages machine scheduling, OEE, and automation interfaces but gaps appear in documentation control, rich routing logic, supplier collaboration, and MRO workflows.

    A digital operations layer sits above and between ERP, MES, PLM, and QMS. It coordinates work instructions, checklists, approvals, and contextual data for each task without requiring system replacement.

    Concrete integration patterns include:

    • Pulling work order and BOM data from SAP or Oracle
    • Associating production tasks with CAD/PLM revisions
    • Pushing completion data and nonconformance records back into ERP/QMS
    • Faster ECN propagation across connected systems

    Executives do not need to rip-and-replace existing systems to achieve modern execution capabilities. Connect981 extends the existing landscape rather than competing with established infrastructure investments.

    Quality, Traceability, and Compliance by Design

    Aerospace and MRO operations require designing in quality and traceability from day one to satisfy safety and performance standards under AS9100, AS9102, NADCAP, ITAR, FAA, EASA, and OEM customer certification requirements.

    Concrete practices include:

    • Serial and batch number traceability throughout production processes
    • Heat lot control for specialty alloys and key components
    • Digital FAIRs replacing paper-based first article inspection
    • CAPA workflows with immutable audit trails
    • Sign-off records for every process change and rework event

    Digital work instructions embed mandatory quality checkpoints that must be completed before advancing operations. Torque verification, NDT signoff, and visual inspections gate progression automatically rather than relying on technician memory.

    The value during audits becomes clear: instant access to routing, parameters, technicians, calibrated tools, and rework history for any serial number. Regulatory bodies and OEM quality representatives can verify compliance without manual document retrieval.

    Connect981 captures these elements automatically as technicians execute work, reducing reliance on manual forms and scanned PDFs. Quality escapes drop 20-40% in certified environments using embedded checkpoint enforcement.

    Connected Factory: Integrating ERP, MES, PLM, QMS, and Supplier Systems

    The typical aerospace IT landscape in 2025 includes multiple ERPs across regions, legacy MES installations, PLM for design, standalone QMS, and supplier portals. These systems remain only partially integrated.

    Data silos create issues:

    • Mismatched revisions between PLM and shopfloor instructions
    • Delayed quality feedback to engineering teams
    • Limited supplier visibility into engineering or routing changes
    • Configuration drift between production sites

    A unified operations layer reads and writes to these complex systems, ensuring technicians, engineers, and supplier partners all see the same current configuration. Technology integration patterns include API-based connections for modern systems and file-based exchanges where legacy infrastructure requires it.

    Role-based data sharing respects international traffic in arms regulations and export controls while enabling necessary collaboration. Connect981 bridges OEM and tier-1 systems with tier-2 and tier-3 suppliers, enabling shared workflows for build packages, FAIR approvals, and deviation management.

    Business outcomes include fewer build holds, faster engineering change implementation, and reduced rework from revision mismatches.

    Managing Complex Aerospace Supply Chains

    Aerospace supply chains remain fragile due to long lead times for titanium and specialty alloys spanning 12 to 24 months, semiconductor constraints, complex electronics, and thousands of tier-2 and tier-3 suppliers per program. Supply chain resilience has become a board-level priority.

    Geopolitical events, export controls under ITAR and EAR, and evolving cybersecurity requirements under CMMC add layers of operational risk. The defense systems segment faces particularly stringent requirements affecting prime contractors and their supplier networks.

    Operational impacts include:

    • Line-stopping shortages requiring production schedule changes
    • Out-of-sequence work creating downstream complications
    • Expedited freight costs eroding margins
    • Last-minute engineering deviations to accommodate substitute parts

    Digital supply chain coordination addresses these challenges through shared build packages, real-time PO and routing visibility, and supplier progress updates integrated directly into factory execution views. Aerospace customers gain transparency into supplier status without manual status calls.

    Connect981 supports supplier collaboration by giving external partners controlled access to relevant work instructions, quality requirements, and documentation checklists. Coordinating FAIRs, managing approved vendor lists, and monitoring supplier on-time delivery and PPM become streamlined activities rather than administrative burdens.

    Aerospace MRO Operations and Turnaround Time Optimization

    Aerospace MRO differs fundamentally from new production through variable work scopes, discovery-driven routing, and heavy dependence on historic maintenance records. Predictive maintenance strategies intersect with traditional scheduled overhaul requirements.

    Key MRO metrics include:

    Metric

    Target

    Impact

    Turnaround time (TAT)

    30-60 days for engine shops

    Customer satisfaction, lease costs

    On-time release

    95%+

    Contract compliance

    Findings-per-visit

    Trending analysis

    Process optimization

    Rework rate

    Under 5%

    Cost control

    Repeat visits within 18-24 months

    Minimized

    Quality verification

    Digital routing and task cards adapt dynamically during disassembly and inspection, updating work content as findings are logged. An engine module strip reveals conditions that modify the repair scope in real time rather than requiring separate paper processes.

    Integrated parts traceability and maintenance history improve decisions on repair versus replace and help prove compliance to regulatory requirements and lessors. Connect981 unifies MRO planning, routing execution, parts kitting, quality checks, and customer approvals in one view, reducing TAT by 15-25% and eliminating paperwork cycles.
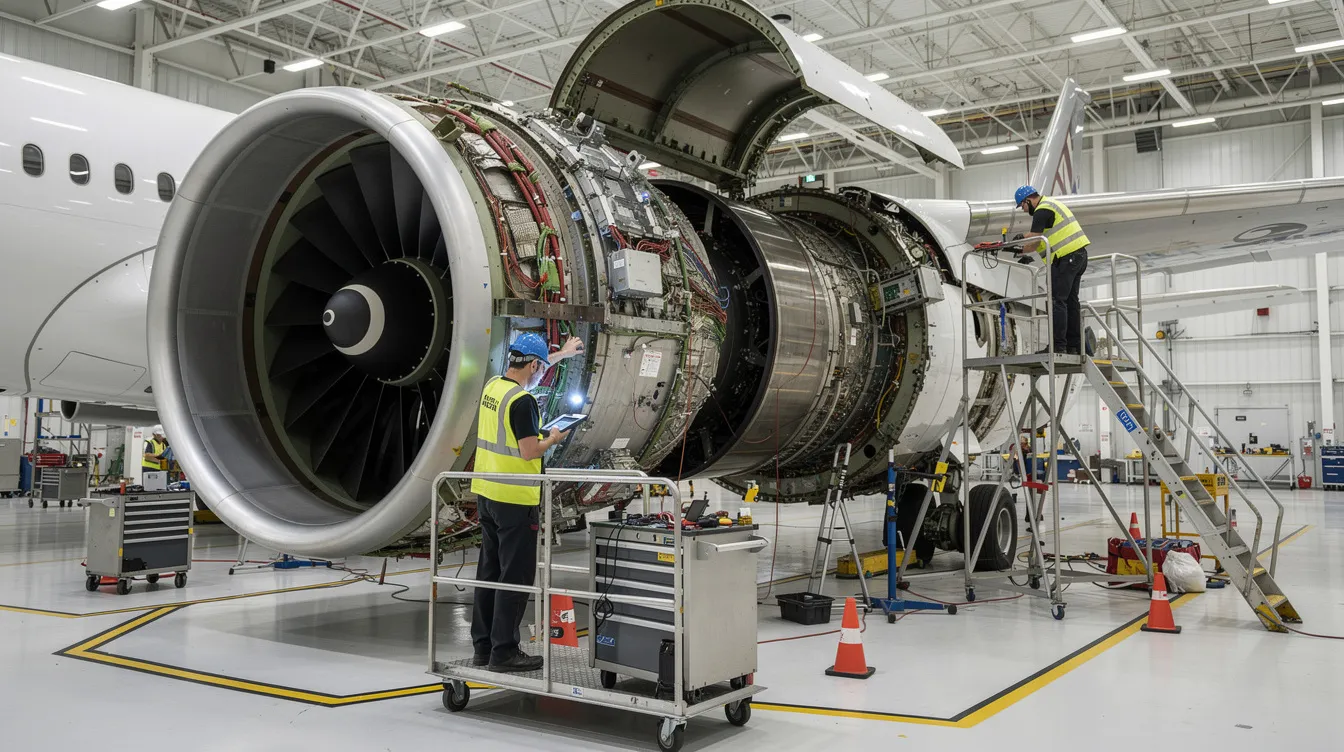
    The image depicts an aircraft engine being meticulously inspected during maintenance at a modern MRO facility, highlighting the critical aerospace manufacturing processes that ensure safety and performance standards in the aerospace industry. Skilled technicians are seen utilizing advanced manufacturing technologies and quality control measures to optimize production processes and maintain the reliability of aerospace components.

    Leveraging AI and Analytics in Aerospace Manufacturing Operations

    Realistic AI and data analytics use cases achievable on the factory floor before 2028 focus on operational improvement rather than speculative autonomous systems. Machine learning applications must meet aerospace constraints around certification requirements and model validation expectations.

    Specific opportunities include:

    • Predictive quality flagging likely nonconforming operations before completion
    • Anomaly detection in process control data
    • Intelligent routing suggestions based on historical performance
    • AI-assisted root cause analysis for CAPA workflows
    • Real time feedback on process deviations

    Operational data collected in Connect981 including timestamps, user actions, defect types, and process parameters feeds these models to deliver program-specific insights. Advanced analytics reveal patterns invisible in manual review.

    Constraints unique to aerospace demand explainable AI for regulators and internal quality authorities. Aerospace companies must govern AI adoption through phased pilots on selected lines or MRO cells, human-in-the-loop decision making, and clear boundaries between advisory and automated actions.

    Examples include reducing scrap on composite layup by 10-20% or improving FAI pass rates on complex machined specialized components through pattern recognition.

    Implementation Roadmap: From Paper and Spreadsheets to a Connected Operations Layer

    A pragmatic 12 to 24 month transformation roadmap for aerospace plants reliant on paper travelers, spreadsheets, and shared drives follows a phased approach to optimize production processes.

    Months 1-6: Foundation

    • Select one value stream or MRO cell for initial digitization
    • Digitize work instructions and quality checklists for repetitive tasks
    • Establish baseline metrics for comparison
    • Train core team on platform capabilities

    Months 6-12: Expansion

    • Expand to quality workflows and parts traceability
    • Connect supplier collaboration for selected programs
    • Integrate with ERP for work order data synchronization
    • Measure first-pass yield improvements and reduce waste

    Months 12-24: Enterprise Scale

    • Roll out across additional production lines and sites
    • Standardize workflows based on lessons learned
    • Enable cross-site visibility and benchmarking
    • Extend to MRO operations and additional supplier tiers

    Cross-functional governance requires operations, manufacturing engineering, quality, IT, and supply chain jointly defining standard workflows and data structures. Aviation management leadership must champion adoption.

    Connect981’s zero and low-code platform shortens deployment using aerospace-specific templates for FAI, inspection, routing, and concessions. Early wins like reducing missing paperwork by 50% or shortening signoff cycles build organizational momentum and support continuous improvement.

    How Connect981 Supports Modern Aerospace Manufacturing Operations

    Connect981 serves as a unified aerospace operations platform connecting ERP, MES, PLM, QMS, and supplier systems into one digital execution layer. The platform addresses aerospace and defense industry requirements rather than generic industrial manufacturing needs.

    Core capabilities mapped to operational priorities:

    • Digital work instructions with embedded media and version control
    • Shopfloor execution tracking with real-time WIP visibility
    • Serial and lot traceability throughout production cycles
    • Integrated quality workflows with checkpoint enforcement
    • Supplier collaboration with controlled access and shared documentation
    • MRO routing management with dynamic task adaptation

    Scenario examples:

    • Ramping a new program across multiple sites with consistent work packages and synchronized documentation releases
    • Stabilizing a critical supplier through shared FAI workflows and deviation management
    • Reducing TAT in an engine MRO shop by 20% through unified planning and execution views

    Connect981 differentiates from general MES and low-code platforms through aerospace-first data models, templates for AS9100 and FAA workflows, and fast time-to-value without requiring system replacement. Digital tools deploy in weeks rather than months.

    Conclusion: Next Steps for Aerospace Operations Leaders

    Modern aerospace manufacturing operations require integrated visibility, scalable processes, empowered workforces, and a digital execution layer bridging legacy systems. The aerospace projects demanding attention in 2026 cannot wait for multi-year transformation programs.

    Executive priorities for the next 18 to 24 months:

    1. Unify operational data across ERP, MES, and shopfloor systems
    2. Digitize work instructions and quality flows to reduce cost and development cycles
    3. Standardize processes across sites using template-based workflows
    4. Connect suppliers and MRO operations into shared visibility frameworks

    Leaders can assess current maturity by inventorying paper-based workflows, counting manual spreadsheets used for production control, and reviewing audit findings related to documentation and traceability. The biggest challenges often hide in plain sight.

    A pilot with Connect981 on a targeted program or MRO cell provides a low-risk path to validate benefits and balance innovation with operational continuity. Strategic partnerships between operations leadership and digital platforms enable aerospace companies to stay competitive. Educational institutions and leadership programs increasingly emphasize digital manufacturing competencies for future workforce development.

    The next 18 to 24 months will separate organizations that digitize execution from those still managing paper trails. Operational efficiency gains compound across programs when the foundation is right. Request a Demo to see how Connect981 extends your existing ERP and MES landscape to meet aerospace production demands and ensure safety across other industries and beyond.
  • AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C tightens expectations on how aerospace manufacturers plan, execute, and document First Article Inspection (FAI). For quality and manufacturing teams already under pressure, the update raises an important question: what exactly changed, and how do we comply in a practical, digital way without slowing programs down?

    This guide explains the AS9102 Rev C requirements, highlights key differences from Rev B, and shows how modern digital AS9102 software capabilities make day‑to‑day compliance manageable for OEMs and suppliers.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Overview of AS9102 Rev C and Its Purpose

    AS9102 is the international aerospace standard that defines how organizations plan, perform, and document first article inspections. It sits alongside AS9100 and IAQG guidance as the primary reference for verifying that production processes can reliably manufacture conforming parts.

    Why AS9102 Was Created and How It Supports AS9100 and Regulatory Expectations

    AS9102 was created to solve a persistent industry problem: inconsistent and incomplete first article inspection practices across the aerospace supply chain. Before AS9102, each customer tended to define its own FAI rules and templates, creating confusion and rework for suppliers.

    The standard provides:

    • Common definitions for FAI scope, terminology, and documentation.
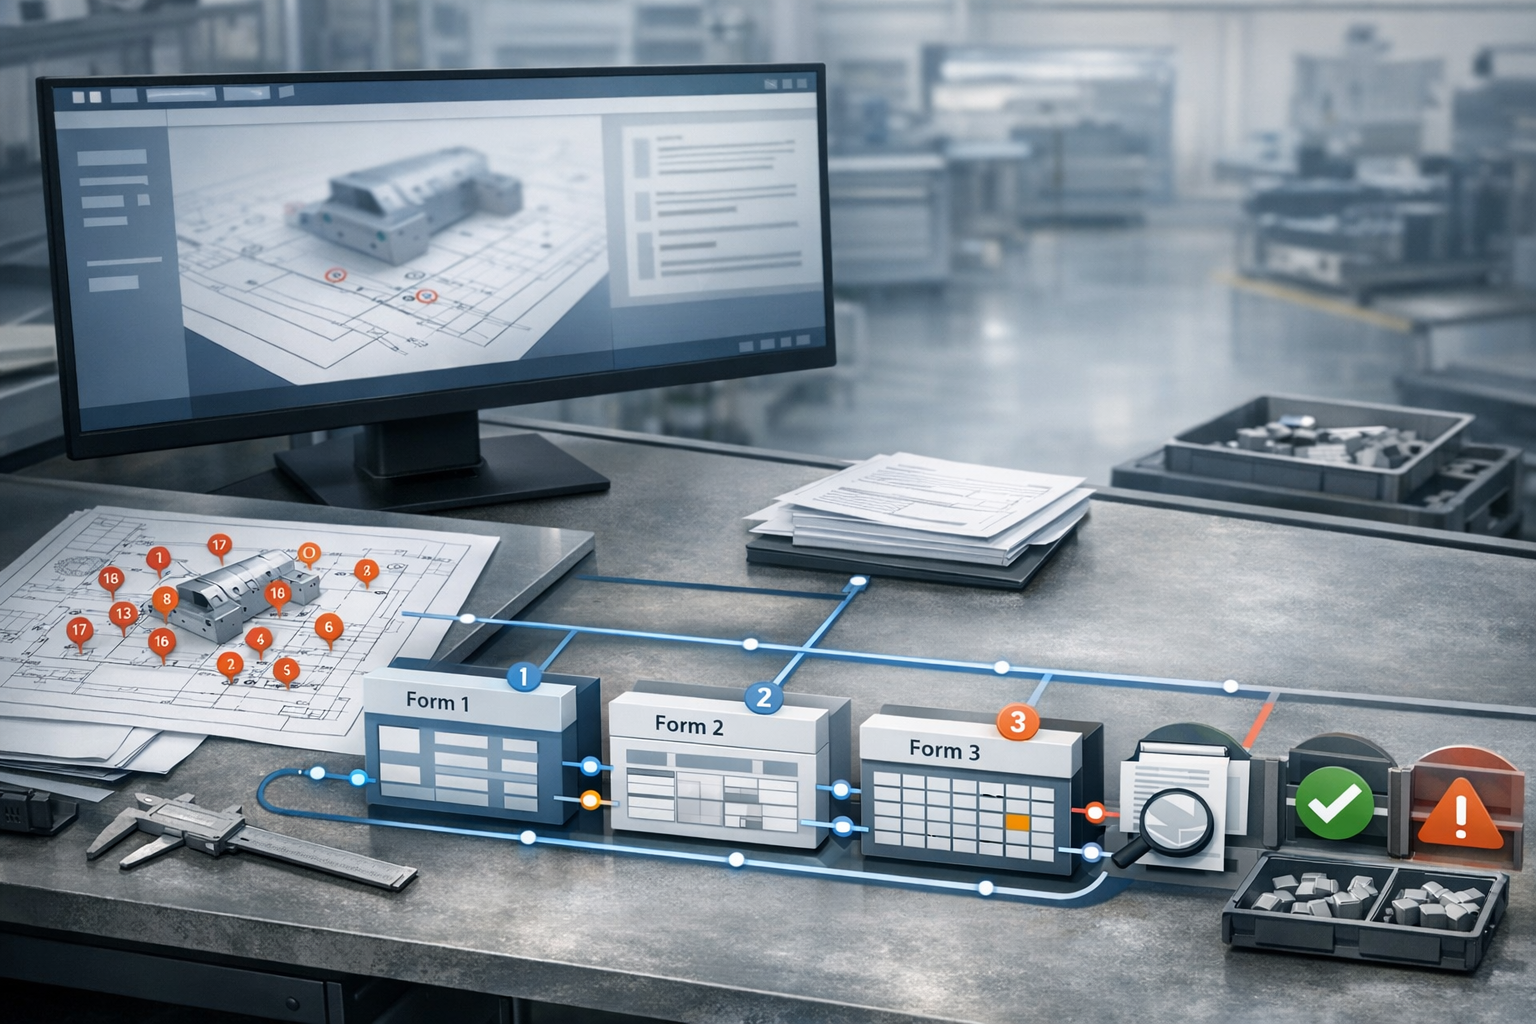
    • Standardized forms (Forms 1, 2, and 3) to document part accountability, material and process verification, and characteristic results.
    • Minimum expectations for traceability from design data (drawings, models, specifications) to inspection evidence.

    AS9102 supports AS9100 by providing objective evidence that the production process has been validated. It also aligns with FAA, EASA, and other airworthiness regulators by demonstrating that initial and changed configurations are thoroughly verified before rate production.

    Timeline of Revisions From Original Release to Rev C

    AS9102 has evolved as follows:

    • AS9102 (original release, 2004-era): Established the core concepts of FAI and the three standard forms.
    • AS9102B (around 2009–2014 adoption window): Emphasized FAI planning and clarified expectations around documentation and re-accomplishment.
    • AS9102C (Rev C, most recent): Focuses heavily on clarity for digital implementations, improved handling of partial and delta FAI, and better alignment with modern aerospace configuration and data-management practices.

    For many organizations, Rev C has been the catalyst to move away from manual, spreadsheet-driven FAIRs and invest in digital solutions that can consistently interpret and enforce the updated requirements.

    Who AS9102 Rev C Applies To in the Aerospace Supply Chain

    AS9102 Rev C applies when it is invoked by contract, purchase order, or quality clause. Typically, it affects:

    • OEMs and airframe manufacturers who must demonstrate configuration and process validation for new and changed parts.
    • Tier 1 and Tier 2 suppliers who deliver flight-critical structures, engine components, avionics hardware, interiors, and other aerospace products requiring FAI.
    • Special process providers whose outputs (heat treatment, NDT, plating, coatings) are essential to meeting drawing requirements documented on Form 2 and Form 3.

    AS9102 itself is not a regulation; it is a standard. However, once a customer or prime specifies AS9102 Rev C, compliance becomes a contractual requirement and is often sampled during AS9100 and customer audits.

    Core Requirements of AS9102 Rev C

    AS9102 Rev C defines when an FAI is required, how to categorize it (full, partial, delta), and what information must be present on Forms 1, 2, and 3 to show complete characteristic accountability and traceability.

    Full, Partial, and Delta FAI Definitions and Applicability

    Under Rev C, FAI categories are more explicitly defined to match real-world change scenarios:

    • Full FAI
      • Required for a new part number or when otherwise specified by the customer.
      • Covers all design characteristics and requirements shown on the applicable drawing or model, including notes, GD&T, and special requirements.
      • Generates a complete FAIR package (Forms 1–3 plus supporting evidence).
    • Partial FAI
      • Used when only a subset of characteristics or operations need to be re-verified.
      • Often triggered by a change in manufacturing process, location, tooling, or equipment where design data is unchanged.
      • Documented clearly as a partial FAI on Form 1, with traceability to the baseline full FAI.
    • Delta FAI
      • Used when an engineering or design change affects only certain characteristics.
      • Focuses on characteristics impacted by the design change, while referencing the baseline FAI for unchanged features.
      • Requires clear identification of revised design data and affected characteristics.

    Rev C expects organizations to classify FAI correctly and to maintain traceable linkage between full, partial, and delta FAI so that the product’s verification history is transparent.

    Mandatory Data Elements for Forms 1, 2, and 3

    AS9102 Rev C retains the three-form structure but clarifies what must be captured on each form. While the standard’s exact field layout is copyrighted, you must ensure the following types of information are present and complete.

    Form 1 – Part Number Accountability typically includes:

    • Part number, name, and configuration (revision, issue, or version).
    • FAI status (full, partial, delta) with cross-reference to the baseline FAIR when applicable.
    • Serial number(s) or lot/batch identification for the first article units.
    • Customer and internal references (PO, job/traveler, work order, etc.).
    • Signatures, dates, and organization information for those who prepared and approved the FAIR.

    Form 2 – Product Accountability focuses on:

    • Materials used, including specification, type, and lot or heat numbers.
    • Special processes such as heat treatment, NDT, welding, plating, coating, and surface treatments.
    • Functional tests and performance verifications where results are pass/fail rather than dimensional.
    • References to certifications, test reports, and process records (e.g., certificates of conformity, NADCAP approvals).

    Form 3 – Characteristic Accountability, Verification Results, and Compatibility Evaluation documents:

    • Each ballooned characteristic with a unique identifier/sequence number.
    • Design requirement (nominal, tolerance, GD&T callout, or note description).
    • Actual measured results or verification outcome.
    • Acceptance status and compatibility evaluation where applicable.
    • Links to the measurement method, inspection equipment, or CMM program as needed.

    Rev C emphasizes that all applicable characteristics—including dimensions, notes, and special requirements—must appear on Form 3 so there is no ambiguity about what has been verified.

    Requirements for Characteristic Accountability and Traceability

    Characteristic accountability is the backbone of AS9102. Rev C expects you to demonstrate that every requirement in the design data has been identified, numbered, and verified with a clear record.

    Practically, this means:

    • Each drawing or model requirement is assigned a unique balloon number or similar identifier.
    • That identifier is used as the sequence number on Form 3, creating one-to-one mapping between the drawing and FAIR.
    • Measurement results, pass/fail decisions, and notes are recorded under the same identifier so anyone can trace from drawing to data and back.
    • Special processes and materials that support a given characteristic are traceable via Form 2 and attached certifications.

    Rev C strengthens the expectation that traceability must include configuration control. FAIRs must be tied to a specific drawing or model revision, and later delta/partial FAIs must clearly reference prior FAIRs and the changes that triggered them.

    AS9102 Rev B vs Rev C: Key Changes

    Organizations moving from Rev B to Rev C often underestimate the impact of the new revision. Much of the terminology is familiar, but Rev C clarifies intent, tightens definitions, and explicitly anticipates digital execution.

    Clarifications Introduced for Digital Implementations

    Rev C was written against the backdrop of widespread digital FAI tools rather than paper and spreadsheets. Some key clarifications include:

    • Improved guidance on linking digital drawings/models to Forms 1–3, ensuring the configuration of the data source is clear.
    • Recognition that digital signatures and electronic approvals can meet the standard as long as they are controlled and traceable.
    • Expectations for consistent handling of multi-sheet drawings and multi-configuration parts in digital systems.
    • Clearer distinction between the FAI process and the FAIR (report), which is important when using automated data flows.

    These clarifications are not optional; they drive how digital solutions must behave to be considered aligned with Rev C.

    Changes to Partial and Delta FAI Handling

    Under Rev B, organizations frequently struggled with when and how to perform partial or delta FAI. Rev C addresses this by:

    • More explicitly defining triggers for partial vs delta (manufacturing/process vs design/engineering driven).
    • Reinforcing that partial and delta FAI must still maintain traceable linkage to the baseline full FAI.
    • Emphasizing that only affected characteristics are re-verified, but documentation must clearly state what changed and why.

    Done correctly, Rev C’s structure reduces unnecessary rework while still satisfying customer and regulatory expectations.

    New or Reworded Fields and Expectations on the Forms

    Rev C introduces reworded field descriptions and some additional expectations on how certain information is captured, for example:

    • More precise language around FAI status (full, partial, delta) and its indication on Form 1.
    • Clearer guidance on recording design data references (drawing/model numbers, revisions, specification references).
    • More consistent terminology for compatibility evaluations and special characteristics.

    Digital tools should be configured to reflect these Rev C expectations in field labels, required fields, and validation rules, even if the underlying data model is similar to what you used under Rev B.

    Practical Triggers for AS9102 FAI Under Rev C

    Knowing the theory is only half the story. Day-to-day, teams need a clear understanding of when Rev C expects a new FAI activity.

    Design and Engineering Change Scenarios

    Engineering changes that typically trigger full or delta FAI under Rev C include:

    • New part introduction (new part number or first time build at your site).
    • Changes that affect form, fit, function, reliability, or safety.
    • Drawing or model revision that adds, deletes, or significantly changes key features.
    • Tightening or relaxing tolerances on critical dimensions.
    • New material specifications or design notes that drive new verification activities.

    Most of these are handled via delta FAI, provided you can show clear traceability to prior FAIRs and focus only on affected characteristics.

    Process, Material, and Supplier Changes

    Process-oriented changes typically trigger partial FAI. Common examples include:

    • Moving production to a new machine, cell, or facility.
    • Changing the manufacturing route (e.g., switching from one machining sequence to another).
    • Introducing new tooling or fixtures that could affect dimensions.
    • Changing a sub-tier supplier for raw material, castings/forgings, or critical processes.
    • Modifying process parameters for special processes (e.g., new heat treat cycle, new NDT technique).

    Rev C expects organizations to have documented criteria—often in their QMS—for when such changes trigger partial FAI, and to demonstrate that the partial scope correctly corresponds to the impacted characteristics.

    Lapse in Production and Customer-Specific Triggers

    Another key trigger is lapse in production. If a part has not been produced for an extended period (commonly two years, but some customers specify different thresholds), Rev C expects you to reassess whether FAI is required. Many organizations treat this as a partial FAI unless design or process changes require more.

    Customer-specific triggers may include:

    • FAI required for every lot or every nth lot for high-risk parts.
    • FAI required when internal yield or defect trends exceed thresholds.
    • FAI mandated when a supplier changes certain sub-tiers, even if design and process remain stable.

    AS9102 Rev C sets the baseline; purchase orders and customer quality clauses can add stricter conditions, and these must be interpreted alongside the standard.

    How Digital AS9102 Software Supports Rev C Compliance

    Trying to meet Rev C requirements with manual ballooning and spreadsheets is possible for simple parts, but it becomes risky and inefficient at aerospace scale. Modern AS9102 software is designed specifically to satisfy Rev C expectations while reducing cycle time and error rates.

    Configuring Templates and Fields to Match the Rev C Standard

    A robust digital solution lets you:

    • Configure Form 1, 2, and 3 templates to align with Rev C’s required data elements and field definitions.
    • Define mandatory fields and validation rules (e.g., FAI type required, drawing revision cannot be blank, serial numbers must match work orders).
    • Standardize customer-specific layouts on top of a single, controlled data model.

    This configuration step is critical to applying Rev C consistently across sites and suppliers.

    Automated Checks to Prevent Common Nonconformances

    AS9102 software can embed rule-based and automated checks such as:

    • Verifying that every ballooned characteristic on the drawing has a corresponding entry on Form 3.
    • Ensuring that FAI type (full/partial/delta) and baseline references are populated correctly on Form 1.
    • Blocking approval if there are missing certificates for materials and processes referenced on Form 2.
    • Highlighting inconsistencies between drawing revision, work order, and FAIR configuration.

    These checks greatly reduce the risk of FAIR rejection by customers or findings during audits.

    Managing Revisions, Partial, and Delta FAI in Software

    Effective digital tools provide structured support for Rev C’s FAI types:

    • Full FAI: Create a baseline FAIR that captures all characteristics and associated evidence.
    • Partial FAI: Clone the baseline FAIR, restrict the scope to impacted operations/characteristics, and record the partial status on Form 1.
    • Delta FAI: Compare new and prior design data to identify affected characteristics, generate a focused Form 3 subset, and clearly reference prior FAIRs.

    Advanced systems can even visualize FAI lineage as a tree, showing which FAIRs are related to which design or process changes. This directly supports Rev C’s intent for transparent traceability.

    Implementation Checklist for AS9102 Rev C

    Moving to Rev C is not just a documentation update. It touches procedures, training, systems, and supplier expectations. The following checklist can guide implementation.

    Gap Analysis From Current Practices to Rev C Requirements

    Start by assessing your current state:

    • Review quality procedures and work instructions against Rev C clauses.
    • Audit sample FAIRs to check for complete characteristic accountability and clear FAI type identification.
    • Evaluate whether partial/delta FAI usage matches Rev C definitions and triggers.
    • Identify where manual workarounds (e.g., untracked spreadsheet columns) are substituting for systematic controls.

    Document gaps and prioritize remediation based on risk, customer expectations, and audit feedback.

    Training, Work Instructions, and System Updates

    Next, update the human and procedural side:

    • Revise FAI procedures to reference AS9102 Rev C explicitly, including FAI triggers and FAI type definitions.
    • Update work instructions for quality engineers, inspectors, and manufacturing engineers, including clear guidance on how to classify and document FAI.
    • Deliver role-specific training that focuses on practical scenarios rather than just standard text.
    • Adjust your AS9102 software configuration (forms, validations, workflows) to reflect Rev C requirements and any customer-specific overlays.

    The goal is that anyone involved in FAI can recognize when Rev C applies and how to execute it consistently in your chosen digital environment.

    Ongoing Monitoring and Audit Readiness Under Rev C

    Once Rev C is in place, you need continuous assurance that it is being followed:

    • Periodically sample FAIRs for completeness, characteristic coverage, and alignment with design changes.
    • Track FAIR rejection rates by customer and cause to identify systemic issues.
    • Prepare for audits by ensuring FAIRs, supporting documents, and change histories are searchable and retrievable within minutes.
    • Leverage digital dashboards, where available, to monitor open FAIRs, overdue approvals, and FAI bottlenecks.

    Rev C does not require perfection, but it does expect a controlled, repeatable process with objective evidence to back it up.

    Where AS9102 Rev C Fits in a Digital FAI Strategy

    FAI should not be handled as a stand-alone, tactical task. Under Rev C, it is increasingly viewed as part of a broader digital aerospace operations strategy—one that connects design, planning, execution, and quality.

    For a deeper look at how ballooning, Forms 1–3, workflows, and supplier collaboration come together in software, see the hub guide on AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

    By aligning your procedures, training, and AS9102 software with Rev C requirements, you reduce FAIR rejections, protect program schedules, and strengthen your position with OEMs and regulators—while turning FAI data into a reusable asset rather than a one-time deliverable.

  • Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    For most aerospace manufacturers, the slowest and most error-prone part of AS9102 first article inspection (FAI) is not the measurements themselves. It is turning complex drawings into ballooned characteristics and then mapping every requirement into Forms 1, 2, and 3. Digital FAIR forms and automated ballooned drawings target this exact bottleneck, replacing hand-marked prints and Excel templates with a structured, reviewable, and reusable data model.

    This article explains how modern tools automate ballooned drawings, populate AS9102 forms, and maintain one-to-one traceability between every drawing requirement and every Form 3 line. It also shows how digital FAIRs support partial and delta FAI, integrate measurement data, and create a foundation for long-term traceability.

    For teams putting this topic into daily operation, Connect 981’s aerospace execution solutions, real aerospace execution examples, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you need a broader overview of how these capabilities fit into a full platform, see our AS9102 software overview.

    Why Ballooned Drawings and FAIR Forms Are Central to AS9102

    AS9102 revolves around a simple idea: every requirement in the design must be clearly identified, measured, and documented. Ballooned drawings and FAIR forms are how that happens in practice.

    The role of ballooned drawings in capturing every requirement

    A ballooned drawing is a drawing where every verifiable requirement is given a unique identifier (a “balloon” number). This typically includes:

    • Dimensions and tolerances (linear, angular, diameters, radii, etc.)
    • GD&T callouts (position, flatness, perpendicularity, profile, and others)
    • Surface finish requirements
    • Drawing notes that imply verification (e.g., “NO SHARP EDGES”, “DEBURR ALL EDGES”)
    • Material specifications and heat-treat conditions
    • Coatings and other special processes that must be verified

    Each balloon creates a discrete, traceable “characteristic” that should appear on Form 3. When ballooning is incomplete or inconsistent, characteristic accountability breaks down and AS9102 expectations are not met.

    How Forms 1, 2, and 3 relate to the drawing

    AS9102 Rev C structures the FAIR into three core forms:

    • Form 1 – Part Number Accountability: Identifies the part, configuration, and whether the FAIR is full, partial, or delta.
    • Form 2 – Product Accountability: Lists materials, special processes, and functional tests with traceable documentation.
    • Form 3 – Characteristic Accountability: Maps every ballooned characteristic to measured or verified results and compatibility evaluations.

    The ballooned drawing drives Form 3. Each balloon ID should correspond to exactly one Form 3 line, which then references the same part and revision context defined in Form 1 and the associated materials and processes summarized in Form 2.

    Common failure modes in manual FAIR creation

    Manual FAI processes typically involve printing drawings, marking balloons with a pen, and populating Excel-based forms. This approach is familiar but fragile. Common problems include:

    • Missed or duplicated balloons: Critical dimensions can be skipped entirely or numbered twice, resulting in gaps or conflicts in Form 3.
    • Mismatch between drawing and forms: Balloon numbering on paper does not match line numbering in Excel, making reviews and audits difficult.
    • Incorrect tolerance or unit interpretation: Values are re-typed manually, increasing the chance of misreading, rounding, or unit mix-ups.
    • Weak revision control: FAIRs are completed against one drawing revision while a newer revision is already in effect, but there is no systematic link.
    • Heavy reliance on tribal knowledge: Only a few experts know how to balloon in the “right way” or which Excel template applies to which customer.

    Digital FAIR tools focus on eliminating these failure modes by treating ballooning and forms as connected, governed data rather than as disconnected documents.

    How Digital Tools Automate Ballooned Drawings

    Digital ballooning is the starting point for any modern AS9102 workflow. Instead of manually adding balloons on paper, engineers work with digital drawings and software that recognizes and structures characteristics.

    Importing PDF and CAD-derived drawings

    Most FAI scenarios still rely on 2D drawings, even when the design originates from a 3D CAD model. Effective digital ballooning starts with robust import:

    • PDF drawing import: The system ingests released PDF drawings directly from PLM or document control, preserving scaling and clarity.
    • CAD-derived drawings: For organizations using model-based workflows, tools may import 2D drawings generated from the 3D model or access published views that carry product manufacturing information (PMI).
    • Config-controlled access: The ballooning tool should clearly display the drawing revision and ensure the FAIR is always linked to the correct configuration.

    By anchoring ballooning to controlled source files, the risk of using outdated prints is dramatically reduced.

    Automated detection of dimensions, GD&T, and notes

    Once drawings are imported, modern tools use OCR and pattern recognition to identify potential characteristics:

    • Dimension values and tolerances are recognized and tagged as measurement-required characteristics.
    • GD&T frames are captured as separate, structured items with their respective datum references.
    • Notes that imply verification — such as specific finishing, cleanliness, or edge conditions — can be flagged for inclusion.

    Engineers can then review a first-pass extraction rather than ballooning everything from scratch. It is important to view this as assisted extraction, not guaranteed perfection: the software accelerates identification, but quality engineers still verify and adjust the characteristic set before release.

    Managing multi-sheet aerospace drawings and numbering

    Aerospace parts frequently require multi-sheet drawings with multiple views, detail callouts, and separate notes pages. Digital tools must handle this complexity while preserving clarity:

    • Consistent numbering across sheets: Balloon numbers remain unique across all sheets, even when a characteristic is referenced on multiple views.
    • Clear sheet and view references: Each characteristic record includes sheet number, view, and zone (if used) to make later reviews straightforward.
    • Filters for visibility: Users can filter characteristics by sheet, view, or type (dimension, note, GD&T) to simplify large FAIs.

    The outcome is a digital ballooned package where every requirement is visible, numbered, and traceable without the clutter and ambiguity of paper markups.

    Designing Effective Digital FAIR Forms

    Ballooned drawings create the characteristic structure. Digital FAIR forms turn that structure into an AS9102-compliant report that can be submitted, revised, and audited.

    Structuring Forms 1, 2, and 3 for AS9102 Rev C

    Digital FAIR tools should mirror the intent and fields of AS9102 Rev C while still being flexible enough to support customer-specific needs. Good practice includes:

    • Form 1: Controlled fields for part/assembly number, name, revision, FAIR type (full, partial, delta), and reference documents.
    • Form 2: Structured rows for materials, special processes, and functional tests, with clear linkage to certificates, NADCAP scopes, or lab reports.
    • Form 3: One row per characteristic with reference to drawing location, requirement, measured result, units, tolerance, and acceptance status.

    The software should treat these as data-backed forms rather than static templates, enabling calculated fields, consistent formatting, and robust reporting.

    Validation rules that prevent missing or inconsistent data

    One of the central advantages of digital FAIRs over spreadsheets is the ability to enforce rules that catch issues before submission. Examples include:

    • Mandatory completion of key Form 1 fields (part number, revision, FAIR type, FAI status).
    • Automatic warnings if a ballooned characteristic does not have a corresponding Form 3 entry.
    • Checks for unit consistency (e.g., preventing inches and millimeters from being mixed for the same characteristic without explicit conversion).
    • Flags when measurement results appear outside the declared tolerance range, prompting review.

    Instead of discovering issues during customer review, engineers see them while the FAIR is still in preparation.

    Prime-specific formats vs a unified data model

    Many aerospace suppliers must support different AS9102 formats or overlays requested by primes such as Boeing or Airbus. Manually maintaining separate Excel templates quickly becomes unmanageable. Digital FAIR tools should:

    • Maintain a single underlying data model that captures all required AS9102 fields.
    • Allow configurable output layouts — for example, one export tailored to a specific customer’s format and another using a standard AS9102 Rev C layout.
    • Ensure that regardless of the output style, the same governed data set underpins every FAIR.

    This approach avoids having multiple “sources of truth” while still meeting customer-specific presentation requirements.

    Ensuring One-to-One Characteristic Accountability

    Characteristic accountability is the core of AS9102: for each requirement, there is a clear, auditable link from drawing to measured result. Digital tooling makes this explicit and enforceable.

    Mapping each balloon to a unique Form 3 row

    In a well-designed system, the characteristic list created during ballooning is the same list used to populate Form 3. Key behaviors include:

    • Each balloon ID is represented once and only once on Form 3.
    • Characteristics cannot be deleted from Form 3 without equivalent change in the ballooned set, maintaining alignment.
    • Renumbering or re-grouping balloons (for example, after engineering review) automatically updates the associated Form 3 lines.

    This eliminates the common manual error of mismatched numbering between drawings and forms.

    Flagging key and critical characteristics in the data model

    Key characteristics (KCs) and critical characteristics (CCs) drive additional scrutiny and may require enhanced sampling or control plans. Digital FAIRs should support:

    • Flags on each characteristic indicating whether it is a KC, CC, or other special category as defined by the prime or internal procedures.
    • Rules that require additional documentation (e.g., process capability studies) or approvals before a FAIR with CCs can be fully released.
    • The ability to report and trend KCs and CCs across multiple FAIRs, lots, or suppliers.

    When these flags live in a structured data model instead of free-text notes, quality teams can reliably filter, monitor, and report on safety-critical items.

    Bidirectional navigation between drawing and form

    One of the most tangible usability benefits of digital FAIRs is the ability to navigate between the ballooned drawing and Form 3:

    • Clicking on a Form 3 row highlights the associated balloon on the drawing and brings it into view.
    • Selecting a balloon on the drawing jumps directly to the corresponding Form 3 line.
    • Filters and search on either side stay in sync, making internal reviews and customer discussions much faster.

    This bidirectional link reduces ambiguity and helps reviewers focus on the real question: whether the product meets requirements, not whether the documentation can be interpreted.

    Integrating Measurement Data into Digital FAIRs

    Once the characteristic structure is in place, the next challenge is getting accurate measurement and verification data into Form 3 efficiently and correctly.

    Capturing manual measurements accurately

    Many FAIs still involve manual measurements taken with calipers, micrometers, height gages, or simple gauges. Digital FAIR tools should support:

    • Guided data entry forms that show the requirement, nominal, and tolerance alongside an input field for the actual result.
    • On-the-spot validation to catch obvious mis-keys (e.g., a value an order of magnitude off expected nominal).
    • Direct association of who measured, when, and with which instrument, if required by internal or customer procedures.

    The goal is to eliminate re-keying from handwritten sheets into Excel and instead have measurement data recorded once, in the system of record.

    Importing CMM and other automated inspection data

    For complex components, automated inspection systems (CMMs, vision systems, laser scanners) often generate result files in standardized formats. A mature digital FAIR workflow:

    • Maps result file feature IDs to Form 3 characteristic IDs, ensuring that data flows to the correct line.
    • Handles multiple runs or samples, summarizing results as required by the AS9102 form while retaining detailed data behind the scenes.
    • Allows selective review, so engineers can quickly focus on out-of-tolerance or near-limit conditions.

    This tight linkage between inspection systems and FAIRs removes transcription errors and accelerates report completion.

    Handling units, tolerances, and compatibility evaluations

    AS9102 Form 3 requires more than just recording numbers. It also demands a clear compatibility evaluation that confirms whether the characteristic is acceptable. Digital FAIR tools help by:

    • Standardizing units and enforcing conversions where needed, so a drawing in inches and a CMM report in millimeters remain consistent.
    • Structuring tolerance formats (e.g., bilateral, unilateral, limit) so calculations can be automated and consistently interpreted.
    • Providing explicit fields where engineers record compatibility or attach supporting notes for borderline cases.

    Instead of interpreting free-text comments during an audit, reviewers see structured results together with a clear pass/fail or compatible/not compatible conclusion.

    Reuse and Change Management with Digital FAIR Structures

    AS9102 Rev C recognizes that not every event requires a completely new, full FAIR. Digital FAIR structures make it practical to reuse characteristic sets and manage partial or delta FAI without losing traceability.

    Reusing balloon and characteristic structures across builds

    Once a part number has been fully ballooned and its characteristics validated, that structure becomes a reusable asset:

    • New FAIRs for repeat builds can leverage the same ballooning, avoiding repeated engineering effort.
    • Suppliers or additional plants can inherit an approved characteristic set, reducing variation in interpretation.
    • Updates to the drawing trigger incremental reviews instead of new ballooning from scratch.

    This reuse is only safe if revision control is handled carefully, which is where digital tooling excels compared to file-based workflows.

    Supporting partial and delta FAI without recreating forms

    Partial and delta FAIs are often the most confusing for teams using spreadsheets. Digital FAIR tools can make them routine by:

    • Allowing Form 1 to explicitly flag FAIR type (full, partial, delta) as required by AS9102 Rev C.
    • Duplicating the baseline FAIR structure and then highlighting only those characteristics that must be re-verified.
    • Maintaining a link back to the original FAIR so reviewers see the complete history at a glance.

    Instead of building a new spreadsheet for every change, teams extend a controlled data set and capture exactly what has changed and why.

    Maintaining traceability across revisions and submissions

    Traceability in digital FAI spans more than just drawing revisions:

    • Each FAIR is linked to the drawing revision, associated change notices, and the specific production lot or serial numbers inspected.
    • Subsequent FAIRs (for example, after a process move or design modification) explicitly reference the earlier baseline FAIR.
    • Systems can provide a “family tree” of FAIRs showing how the part has evolved and when verification was repeated.

    This level of traceability is extremely difficult to maintain using independent Excel files stored on shared drives. Digital FAIR tools make it a natural byproduct of everyday work.

    How Digital FAIRs Fit into a Broader AS9102 Software Strategy

    Digital FAIR forms and ballooned drawings are the engine of AS9102 documentation, but they rarely live in isolation. When they are integrated into a broader AS9102 software approach, organizations gain:

    • Automatic population of part, revision, and purchase order data from ERP or PLM.
    • Alignment of FAIRs with shop-floor execution, work instructions, and quality checks.
    • Centralized storage and search for all FAIRs, measurement results, and supporting documents.

    To understand how these elements span planning, execution, and audit readiness, it is useful to step back and review an AS9102 software overview that covers workflow orchestration, integration, and analytics on top of the digital FAIR foundation.

    Practical Steps to Implement Digital FAIR Forms and Ballooned Drawings

    Organizations moving from manual to digital FAI can take a phased approach focused on risk reduction and quick wins.

    1. Start with high-impact parts: Select parts with complex drawings, high characteristic counts, or a history of FAIR rework.
    2. Digitize ballooning: Implement automated ballooning for those parts, validating extraction rules and review practices.
    3. Standardize AS9102 forms: Configure Forms 1, 2, and 3 templates aligned with Rev C and major customer overlays.
    4. Integrate measurement data: Pilot CMM and manual data capture flows for a subset of characteristics.
    5. Introduce partial/delta FAI logic: Once the baseline FAIR is stable, use the same structure to manage engineering changes.

    By proving value on a manageable scope first, teams build confidence and templates that can scale across programs, sites, and suppliers.

    Conclusion

    Digital FAIR forms and automated ballooned drawings transform AS9102 FAI from a manual document-creation activity into a governed, reusable data process. By automating characteristic extraction, enforcing one-to-one mapping between balloons and Form 3, and integrating measurement data, quality and manufacturing teams can reduce cycle time, lower error rates, and strengthen traceability.

    When these capabilities are connected to broader AS9102 software workflows, they become a foundation for aerospace compliance, audit readiness, and continuous improvement. The practical next step is to identify where manual ballooning and spreadsheet-based FAIRs are causing the most pain, and then pilot a digital FAIR approach that directly addresses those bottlenecks.

  • Partial vs Delta FAI in AS9102 Software: Practical Digital Strategies

    Partial vs Delta FAI in AS9102 Software: Practical Digital Strategies

    Under AS9102 Rev C, you no longer have to choose between re-doing an entire first article inspection or risking gaps in coverage when designs or processes change. Partial and delta FAI give aerospace manufacturers a structured way to verify only what has actually changed—provided you can manage the details correctly.

    This article explains how full, partial, and delta FAI relate to each other, where organizations struggle when managing them manually, and how modern AS9102 software can automate reuse, lineage, and impact analysis. The perspective here reflects common industry practice, not a legal interpretation of the standard, and final scope decisions must always follow customer and regulatory requirements.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you need a broader overview of digital AS9102 and FAIR workflows before diving into change scenarios, see our guide on AS9102 and digital FAI fundamentals.

    Definitions: Full, Partial, and Delta FAI Under AS9102 Rev C

    AS9102 Rev C clarifies terminology so suppliers and customers can distinguish between a brand-new verification and targeted re-verification when things change.

    When a full FAI is mandatory

    In practice, organizations treat a full FAI as the baseline reference FAIR for a given part configuration. Typical triggers include:

    • New part introduction – First production run of a new part number for a site or supplier.
    • Major design changes impacting form, fit, or function – For example, a new rib structure on a wing component or a significant geometry change on a turbine blade.
    • New manufacturing source – Moving production to a different supplier or facility when the customer requires full re-validation.
    • Extended production lapse – When no parts have been produced for an extended period (often around two years, but this can be customer-specific).

    Under a full FAI, every characteristic on the drawing and applicable specifications must be ballooned and accounted for on Form 3, with supporting material and process evidence on Forms 1 and 2.

    Typical triggers for partial FAI

    Partial FAI is used when only selected characteristics require re-verification, usually because the manufacturing process has changed while the design itself has not. Common triggers include:

    • Process or operation changes – A drilling or milling operation is moved to a different machine, cell, or facility.
    • Tooling or fixture changes – New cutting tools, workholding, or gaging that could affect particular dimensions.
    • Supplier or sub-tier changes for specific operations – For example, moving a plating step to a new special process supplier while the base part remains unchanged.
    • Documented process issues – A corrective action drives re-validation of a specific subset of characteristics.

    The scope of a partial FAI is defined by which characteristics are affected by the process change. You still rely on the existing baseline FAIR for unchanged items.

    Typical triggers for delta FAI

    Delta FAI applies when there is a design or specification change, and you must verify only the impacted characteristics against the new configuration while referencing the prior full FAI.

    • Drawing revision changes – A revision adds, removes, or modifies dimensions, tolerances, GD&T callouts, or notes.
    • Specification updates – A new material spec is called out, a test requirement changes, or a surface treatment is updated.
    • Additional features – New holes, cutouts, stiffeners, or bosses are added to an existing part.
    • Tolerance changes – A previously generous tolerance is tightened on high-risk features.

    The delta FAIR documents only changed and newly added characteristics, but it must clearly reference the baseline FAIR for everything else. This is where digital lineage and linking are especially valuable.

    Common Challenges with Manual Partial and Delta FAI

    On paper and spreadsheets, partial and delta FAI often create more confusion than efficiency. The standard allows targeted verification, but without structured tools, teams struggle to manage scope correctly.

    Over-documentation and unnecessary re-inspection

    To be “safe,” some organizations treat every change as a reason to redo a near-full FAI:

    • Re-ballooning entire drawings instead of only the affected areas.
    • Copy-pasting a prior Form 3 and re-entering measurements for most characteristics.
    • Running duplicate inspections on features that are demonstrably unaffected by the change.

    This wastes engineering capacity, clogs CMM queues, and delays deliveries. It also undermines the original purpose of partial and delta FAI: focusing effort where risk actually changed.

    Under-documentation and missed linked features

    The opposite problem is just as common: teams underestimate scope.

    • A tooling change that affects multiple related features is treated as affecting only one dimension.
    • A GD&T callout is revised, but only one characteristic is updated instead of the entire feature pattern.
    • Downstream processes or mating parts impacted by a tolerance change are not considered.

    Without structured impact analysis, it is easy to miss derived or associated characteristics, exposing you to customer rejections or findings during AS9102 or AS9100 audits.

    Traceability gaps between baseline and follow-on FAIRs

    Manual systems often handle follow-on FAIRs as isolated files:

    • Baseline and delta FAIRs live in different network folders with inconsistent naming.
    • Form 1 status (full, partial, delta) is not used consistently, so reviewers cannot tell what they are looking at.
    • There is no simple way to see how many FAIRs exist for a part and what changed each time.

    These gaps make it hard to prove configuration history and FAIR lineage when customers or auditors ask for evidence.

    Designing Software Workflows for Partial FAI

    Modern AS9102 software can codify partial FAI logic so engineers execute consistent, risk-based scopes instead of reinventing the process each time.

    Tagging FAIRs with status (full, partial, delta)

    Start with explicit status tagging:

    • Every FAIR record uses the Form 1 field to mark full, partial, or delta.
    • Workflows and dashboards filter and report based on that status.
    • Search tools allow users to quickly find the most recent full FAI for a part and all associated partial or delta FAIRs.

    In a software system, status tagging can also drive automated routing and required approvals—for example, forcing quality or customer approval when a partial FAI is used to qualify a new facility.

    Reusing baseline characteristic data safely

    The biggest efficiency gain from digital FAI comes from treating the baseline FAIR as a structured data set rather than a static PDF.

    • Characteristics extracted and ballooned once are stored as reusable digital objects.
    • When a partial FAI is created, the software clones the baseline FAIR metadata, but flags only selected characteristics as “in scope” for re-verification.
    • Unchanged characteristics remain present for context but carry a clear indication that they are not being re-inspected as part of this partial FAI.

    This approach preserves one source of truth for the part while avoiding duplicated Form 3 lines and repeated manual entry.

    Controlling scope when process changes occur

    Well-designed workflows guide engineers through scope decisions instead of leaving everything to memory:

    • Partial FAI templates prompt users to identify the operation, machine, or facility that changed.
    • Characteristics in the baseline FAIR are linked to process steps and work centers.
    • The system proposes a list of characteristics likely affected by the changed operation.

    Engineers can then review, expand, or narrow that list, but they are no longer starting from a blank spreadsheet. This reduces the chance of missing characteristics that should logically be within partial FAI scope.

    Managing Delta FAI for Engineering Changes

    Delta FAI sits at the intersection of engineering change control and production verification. Software can bridge PLM, drawings, and FAIRs so the right characteristics are re-verified every time a revision is released.

    Linking ECNs and drawing revisions to affected balloons

    An effective digital workflow starts with change artifacts—Engineering Change Notices (ECNs), Engineering Change Orders (ECOs), or PLM change objects.

    • Each ECN or drawing revision is associated with the relevant part numbers in the FAI system.
    • The system compares old and new drawings, highlighting changed callouts, dimensions, notes, or specifications.
    • These differences are mapped directly to balloon numbers on the digital drawing and their corresponding Form 3 rows.

    With this linkage in place, the delta FAIR can be generated from a concrete list of changed characteristics instead of relying on manual visual comparison.

    Impact analysis to identify which characteristics must be re-verified

    The next layer of capability is impact analysis—looking beyond the explicitly edited dimension to understand what else should be considered in scope.

    • A tighter positional tolerance on a hole pattern may also bring associated datum features, countersinks, or threads into scope.
    • A surface finish requirement might impact both the machining operation and subsequent coating steps.
    • Changes to a material specification could trigger new or repeated material tests and special process verifications.

    Software can use rules and relationships embedded in the data model to suggest affected characteristic groups. Engineers then review and finalize the scope rather than building it from scratch.

    Building FAIR family trees and lineage views

    Over the life of a part, you may have one full FAI plus multiple partial and delta FAIRs. Without tools, keeping track of this family is difficult.

    • Digital systems construct a FAIR family tree that shows the baseline full FAI and every associated partial or delta FAIR, in chronological order.
    • Each child FAIR contains explicit links back to its parent FAIR and drawing revision.
    • Users can click into a characteristic and see a history of all times it was re-verified and why.

    This lineage not only supports audits; it also helps engineers quickly understand what has already been proven when planning further changes.

    Examples: Partial and Delta FAI Scenarios in Aerospace

    Concrete scenarios help clarify when to consider partial versus delta FAI and how software can handle each case. The exact decision in your organization should always follow customer and internal requirements, but these patterns are common.

    Machine or facility relocation of a machining operation

    Scenario: A supplier moves a 5-axis machining operation for a structural bracket from Plant A to Plant B. The drawing and spec do not change.

    • FAI type: Typically a partial FAI focused on characteristics produced by the relocated operation.
    • Manual challenge: Determining which dimensions are affected by the moved operation and which remain untouched.
    • Software approach: Link each characteristic in the baseline FAIR to its operation routing. When the routing changes, the system suggests the affected characteristics and generates a partial FAIR pre-populated with those characteristics only.

    Tolerance changes on critical hole patterns

    Scenario: Engineering tightens the positional tolerance and surface finish requirement on a critical hole pattern in a landing gear component.

    • FAI type: A delta FAI covering the modified pattern and any associated datums or related features deemed impacted.
    • Manual challenge: Ensuring all holes in the pattern, and not just one edited dimension, are included in the delta scope.
    • Software approach: The system compares drawing revisions, identifies the updated tolerance and finish, and maps those edits to all ballooned features in the pattern. Engineers validate the automatically generated list for the delta FAIR.

    Material substitution for specific callouts

    Scenario: A casting alloy spec is updated, or a substitute material is permitted for specific callouts on a structural part.

    • FAI type: Often a delta FAI covering characteristics and tests influenced by the new material, plus a new record of material certifications on Form 2.
    • Manual challenge: Understanding which tests or special processes need to be repeated and which geometric characteristics need closer scrutiny.
    • Software approach: Characteristics and Form 2 entries linked to the original material spec are flagged; the system prompts for updated certs, test results, and any newly required verifications.

    Measuring the Impact of Digital Partial and Delta FAI

    Organizations often adopt digital FAI tools to solve immediate pain, but you should also measure the impact of better handling of partial and delta FAI over time.

    Cycle time reductions and engineering capacity gains

    Key metrics for partial and delta FAI include:

    • Average time to complete a full FAI vs. partial/delta – With robust reuse and impact analysis, delta FAIRs should routinely take 50–80% less time than a full FAI.
    • Number of FAIRs completed per quality engineer – Automation should increase throughput without extending work hours.
    • Queue time at CMM and inspection resources – Reduced scope directly shortens queues when only affected characteristics are re-measured.

    Effect on audit findings and customer rejections

    Digitizing partial and delta FAI should also improve compliance outcomes:

    • Fewer documentation-related FAIR rejections – Clear status tagging and lineage reduce confusion about what has been verified when.
    • Reduced AS9100/AS9102 audit findings related to configuration control and traceability.
    • Better responsiveness in customer reviews – FAIR family trees and instant retrieval of supporting evidence shorten review cycles.

    Best practices for standardizing partial/delta policies

    To get consistent value from your software, codify your decision logic:

    • Create a partial vs. delta decision matrix aligned with the AS9102 standard and major customer requirements.
    • Embed that matrix into workflow rules and templates so engineers see guidance in context.
    • Review edge cases regularly and adjust rules to reflect lessons learned from audits and customer feedback.

    Over time, your partial and delta FAI process becomes repeatable, auditable, and scalable across sites and suppliers rather than dependent on a few experts.

    Using Partial and Delta FAI as a Strategic Lever

    Done well, partial and delta FAI strategies turn engineering change from a recurring scramble into a controlled, data-driven process. Modern AS9102 software helps you:

    • Reuse baseline FAIR data with confidence instead of rebuilding every time.
    • Focus verification on clearly defined, risk-based scopes.
    • Maintain transparent lineage across full, partial, and delta FAIRs for each part number.
    • Demonstrate robust configuration control during customer and certification audits.

    As your organization advances its digital FAI capabilities, consider how partial and delta FAI workflows align with broader goals like standardizing processes across plants, integrating with PLM and MES, and supporting a connected aerospace operations platform.

    For a deeper foundation on digital FAI tools, templates, and integrations, review the cluster hub on AS9102 and digital FAI fundamentals and then map your current partial and delta FAI workflows against the capabilities described there.

  • Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    In modern aerospace manufacturing, AS9102 first article inspection (FAI) cannot be treated as a stand-alone activity. To keep programs on schedule and pass audits reliably, your FAI process and first article inspection reports (FAIRs) must be tightly connected to ERP, MES, PLM, and QMS systems. True AS9102 software integration removes manual data re-entry, strengthens configuration control, and makes FAIRs part of the broader digital thread.

    This article explains how AS9102 tools should integrate with core enterprise systems, the typical data flows you should expect, and example workflows that embed FAI into day-to-day production. It is a spoke in a larger guide on AS9102 software and a unified aerospace operations platform.

    For teams putting this topic into daily operation, digital AS9102 FAI, shop floor execution control, ERP, MES, and PLM integration paths help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Why AS9102 FAI Cannot Live in a Silo

    The risks of stand-alone spreadsheets and local tools

    Many aerospace OEMs and suppliers still run FAI using Excel templates, local ballooning tools, and network drive folders. Even when these tools generate AS9102-compliant forms, they usually sit outside the enterprise stack. The result is a set of disconnected artifacts that must be reconciled manually with ERP, MES, PLM, and QMS data.

    Common risks of siloed FAI tools include:

    • Re-keying errors: Part numbers, revisions, purchase orders, and lot data are typed multiple times across systems.
    • Configuration mismatches: FAIRs are created to one drawing revision while ERP or PLM have already advanced to another.
    • Limited reuse: Data from one FAI event cannot easily be reused for partial or delta FAI, change management, or trend analysis.
    • Local workarounds: Each plant or engineer maintains their own templates and conventions, undermining standardization.

    How disconnected FAI impacts schedule, quality, and audits

    When FAI is disconnected from core systems, the impact shows up quickly on programs and audits:

    • Schedule delays: FAIRs are started late because nobody realizes a new part or major change has reached production until after work orders are released.
    • Rejections and rework: Customers reject FAIRs due to wrong part numbers, incorrect revision levels, or missing traceability back to material and special processes.
    • Audit exposure: During AS9100 or customer audits, teams scramble across email, shared drives, and local PCs to reconstruct the full FAI picture.
    • Lost lessons learned: Nonconformances identified during FAI do not feed back into design or process improvement because they are trapped in separate spreadsheets or PDFs.

    Benefits of connected FAI data across the value stream

    By contrast, integrating AS9102 software into your enterprise architecture produces tangible benefits:

    • Single source of truth: Part, revision, and order data flow directly from ERP and PLM into FAIRs, eliminating conflicting records.
    • Automatic triggering: New part introductions, engineering changes, or process transfers can automatically trigger FAI requirements.
    • Closed-loop quality: FAIRs connect to nonconformance reports (NCRs), corrective actions (CAPAs), and process controls in the QMS.
    • Digital thread: FAI becomes a key node linking design, planning, production, quality, and in-service data.

    Key Integration Points for AS9102 Software

    Effective AS9102 software touches multiple systems. The integrations do not need to be implemented all at once, but the data model should anticipate each of these connections.

    ERP: part numbers, revisions, orders, and routings

    The ERP system is typically your commercial and planning source of truth. AS9102 software should at minimum:

    • Import item master data: Part numbers, descriptions, and key attributes such as make/buy status or commodity type.
    • Sync revisions: Current engineering or manufacturing revision, ideally cross-referenced to PLM identifiers.
    • Link to orders: Work orders, purchase orders, and sales orders that require FAIR submission.
    • Reference routings: Major operations or work centers associated with the part, enabling routing-based FAI rules.

    Typical workflows include:

    • FAI software periodically receives new or updated item data from ERP so Form 1 can be populated reliably.
    • When an order meets FAI criteria (e.g., first production lot, new part, or re-start after a lapse), ERP flags it, and an FAI record is automatically created.

    MES: work orders, operations, machines, and operators

    MES or shopfloor systems hold execution context. Integrating AS9102 software with MES enables:

    • Work order linkage: FAIRs tied to specific work orders or lots.
    • Operation-level traceability: Measurement results mapped to the operation, machine, and operator that produced the feature.
    • In-process data reuse: Dimensional or process checks collected during production can automatically populate Form 3.

    Common patterns include:

    • Launching FAI-specific inspection plans or electronic checklists when an FAI-designated work order reaches certain operations.
    • Pulling measurement data from automated equipment or operator tablets directly into the FAIR database.

    PLM: drawings, models, and engineering change data

    PLM or PDM systems manage design authority. They are essential for ensuring that FAIRs reflect the correct design configuration:

    • Drawing and model access: AS9102 software imports the released PDF drawings or model-based definition (MBD) for ballooning.
    • Revision control: FAIRs are tagged to specific design revisions; when a change is released, impacted characteristics are identified for delta FAI.
    • Change notice linkage: Engineering change orders (ECOs) or equivalent are associated with affected FAIRs for traceability.

    In a mature setup, PLM becomes the source of balloonable artifacts, while the FAI system manages characteristic extraction, accountability, and measurement results.

    Data Flows Between FAI and Quality Systems

    Beyond ERP, MES, and PLM, AS9102 workflows must connect to the organization’s QMS to support AS9100 and customer requirements.

    Connecting FAIRs to nonconformance and corrective actions

    FAI is often where early nonconformances are discovered. Integration with the QMS should support:

    • Linked NCRs: Each out-of-tolerance characteristic on Form 3 can initiate or link to an NCR.
    • Corrective action traceability: CAPAs reference the exact part, revision, and FAIR where the problem was found.
    • Closed-loop verification: Follow-up FAIRs or delta FAI events demonstrate that corrective actions were effective.

    Reusing FAI data in AS9100 documentation

    The structured data created during FAI can power broader quality documentation:

    • Evidence for process validation and production approval under AS9100.
    • Inputs to risk management and FMEA, particularly for key characteristics that show high variation.
    • Support for control plan updates and sampling strategy adjustments informed by FAI results.

    Without integration, teams must copy data from FAIRs into separate QMS records. With integration, FAI becomes a structured data source that feeds other processes automatically.

    Aligning calibration and measurement system data

    For FAIRs to stand up during audits, measurement results must tie back to calibrated instruments and qualified gages. Integration between AS9102 software and calibration/asset management systems should allow:

    • Recording which gage or CMM program was used for each measurement.
    • Verifying that instruments were within calibration at the time of use.
    • Flagging FAIRs if a later calibration failure suggests results may be suspect.

    This alignment simplifies responses when auditors ask for “evidence that gages used during this FAI were calibrated.”

    Example End-to-End AS9102 Workflow with Integrations

    To illustrate how these integrations work in practice, consider an end-to-end workflow for a new aerospace part.

    Triggering FAI from new work orders or part introductions

    1. Design release in PLM: Engineering releases a new part and associated drawing or model. PLM notifies downstream systems.
    2. ERP item creation: The part is added or updated in ERP, including revision and primary routing. A rule marks this part as requiring FAI for the first production lot.
    3. Automatic FAI record creation: When the first qualifying work order is created in ERP or MES, the AS9102 system automatically creates a corresponding FAIR record and Form 1 header using imported part/order data.

    Collecting inspection data on the shopfloor

    1. Ballooning and planning: The quality or manufacturing engineer imports the released drawing or model into the AS9102 tool, auto-balloons characteristics, and defines which operations or work centers will generate which measurements.
    2. Shopfloor execution: Operators or inspectors receive digital checklists or inspection plans via MES-integrated terminals or tablets. As they record measurements, results flow back to the FAI database, filling Form 3 rows linked to balloon numbers.
    3. Nonconformance handling: Any out-of-tolerance result automatically opens an NCR in the QMS, with a reference to the specific characteristic and FAIR.

    Approving and submitting FAIRs with linked evidence

    1. Quality review: Quality engineers review Form 1–3 inside the AS9102 system, verify that all characteristics are accounted for, and confirm that required material and special process certificates are attached.
    2. Electronic approval: FAIRs move through defined approval workflows with electronic signatures and time stamps.
    3. Submission and archiving: A customer-ready FAIR package (PDF plus structured data if required) is generated and submitted. The system stores the FAIR in a centralized repository, indexed by part, revision, order, and supplier.
    4. Future reuse: When a design or process changes, the baseline FAIR is reused to create partial or delta FAIRs rather than starting from scratch.

    Multi-Site and Supplier Integration Considerations

    Most aerospace programs involve multiple plants and a complex supplier network. AS9102 integration must account for this distributed reality.

    Standardizing FAIR templates across sites and suppliers

    Without standardization, each site or supplier tends to customize FAIR formats and naming conventions. A connected platform enables you to:

    • Define global AS9102 templates that enforce common fields and rules.
    • Allow limited configuration for customer-specific layouts while keeping a consistent underlying data model.
    • Report across FAIRs from different locations because they share the same structure.

    Supplier portals and shared data models

    For purchased parts, suppliers often own the FAI execution, but the OEM is still responsible for overall airworthiness. A supplier-facing portal or shared AS9102 platform can:

    • Provide guided FAIR templates aligned with your standards and customer requirements.
    • Enable suppliers to upload ballooned drawings, Forms 1–3, and certifications directly into your system.
    • Support automated validation checks on incoming FAIRs before they are accepted.

    This approach reduces variation in FAIR quality and accelerates review cycles, especially for high-volume or global supplier bases.

    Managing customer-specific requirements globally

    Major primes and engine manufacturers often apply their own FAIR formats, field requirements, and submission methods. An integrated platform should handle:

    • Configuration by customer: Mapping a single internal data model to different outward-facing FAIR templates.
    • Rule-based triggers: Customer and program-specific criteria for when FAI, partial FAI, or delta FAI is required.
    • Central visibility: Dashboards showing FAI status across customers, plants, and suppliers.

    Architecture Patterns for AS9102 Integration

    There is no one-size-fits-all approach to integrating AS9102 software. The right architecture depends on your existing systems, IT strategy, and digital maturity.

    Point-to-point vs platform-centric integrations

    Two broad patterns are common:

    • Point-to-point: The FAI system connects directly to ERP, MES, PLM, and QMS with separate integrations for each. This can be fast to implement for a small footprint but may become complex to maintain as scope grows.
    • Platform-centric: AS9102 capabilities are part of a broader aerospace operations platform that already integrates with ERP/MES/PLM/QMS. FAI reuses existing data models and services.

    Organizations starting with light integrations might choose point-to-point initially and then consolidate into a platform approach as volume and complexity increase.

    APIs, data lakes, and middleware approaches

    From a technical standpoint, integrations usually rely on one or more of the following:

    • REST or SOAP APIs: Near-real-time synchronization of parts, orders, and status updates.
    • Message queues or integration buses: Event-driven flows (e.g., a new ECO triggers delta FAI creation).
    • Data lakes or warehouses: Consolidated reporting and analytics across FAIRs, production data, and nonconformances.
    • File-based exchange: CSV, XML, or JSON batches for legacy environments where APIs are limited.

    Regardless of the technical mechanism, governance is critical: clear ownership of master data, change management, and validation of integrations before they are used for production decisions.

    Roadmap planning for digital thread and future scalability

    AS9102 integration should be planned as part of a broader digital thread roadmap rather than as an isolated IT project. Key roadmap considerations include:

    • Sequencing integrations (e.g., start with ERP/PLM, then add MES and QMS).
    • Defining standard identifiers for parts, revisions, orders, and characteristics across systems.
    • Ensuring that FAI data structures can support future capabilities such as MBD, AI-assisted sampling, and advanced analytics.

    For many organizations, moving from stand-alone ballooning tools to a unified aerospace operations platform is the key step that defines long-term scalability.

    Conclusion

    Integrating AS9102 software with ERP, MES, PLM, and QMS transforms FAI from a manual compliance burden into a strategic source of configuration control and process insight. By designing data flows carefully, standardizing templates across sites and suppliers, and choosing an architecture that fits your digital thread roadmap, you can reduce FAIR cycle times, cut rework, and strengthen audit readiness.

    The most successful aerospace organizations treat FAI as a connected process embedded in everyday manufacturing workflows. Start by identifying your highest-friction handoffs—typically between design, planning, and quality—and design integrations that eliminate re-keying while preserving rigorous validation and security review.

  • AS9102 Audit Readiness: Building Digital Traceability for FAI

    AS9102 Audit Readiness: Building Digital Traceability for FAI

    AS9102 Audit Readiness: Building Digital Traceability for FAI

    For aerospace manufacturers and suppliers, AS9102 first article inspection reports (FAIRs) are among the most scrutinized records in any audit. AS9100 surveillance audits, customer process reviews, and regulatory oversight all use AS9102 data as evidence of process capability, configuration control, and traceability.

    When FAIRs are scattered across spreadsheets, email threads, and shared drives, audit preparation can consume days of engineering time and still produce gaps. By contrast, digital AS9102 workflows give you structured data, clear traceability links, and rapid retrieval of evidence that can turn a high-stress audit into a routine review.

    For teams putting this topic into daily operation, digital AS9102 FAI, part traceability and as-built evidence, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains how auditors actually use AS9102 FAIRs, what they look for in your records, and which digital traceability capabilities matter most. It builds on the broader AS9102 software: digital first article inspection for aerospace manufacturing hub by focusing specifically on audit readiness.

    How AS9102 FAIRs Are Used in Audits

    FAIRs are more than part-specific documents; they are a window into how effectively your quality management system operates. Different types of audits use AS9102 evidence in slightly different ways.

    AS9100 surveillance and certification audits

    Certification and surveillance auditors use FAIRs to confirm that your organization:

    • Plans and executes first article inspection when required (new parts, design changes, process changes, lapses in production, and other triggers defined in AS9102).
    • Maintains configuration control so FAIRs match the correct drawing and specification revisions.
    • Demonstrates traceability from design requirements to inspection results, material certifications, and special processes.
    • Controls documents and records, including templates, approvals, and revisions.

    Typically, auditors will:

    • Sample a subset of part numbers and request the associated full, partial, or delta FAIRs.
    • Trace from the FAIR to the underlying drawing, work order, and material or process records.
    • Follow the trail into related procedures, work instructions, and training records.

    Gaps here often translate directly into nonconformances against AS9100 requirements for configuration management, monitoring and measurement, and documented information.

    Customer source inspections and process audits

    Customer auditors are usually more part- and program-focused. They use FAIRs to answer questions such as:

    • Did this supplier prove the process before we accepted production parts?
    • Are key characteristics (KCs) and critical characteristics (CCs) consistently controlled?
    • Are customer-specific clauses or purchase order requirements visible in the FAIR and supporting records?

    In many cases, the FAIR becomes the primary reference when customers evaluate supplier performance, approve new sources, or investigate recurring escapes. If FAIRs are incomplete, inconsistent, or hard to retrieve, confidence in your overall system immediately drops.

    Regulatory oversight and airworthiness evidence

    Regulators and delegated organizations (for example, through Designated Engineering Representatives or similar roles) rarely review every FAIR, but they expect to see that:

    • FAI is integrated into your production system as a standard practice, not a one-off activity.
    • Traceability exists from serial- and lot-level hardware back to the FAIR and its supporting evidence.
    • Special processes, materials, and key safety characteristics are verified and documented.

    When a potential airworthiness concern emerges, FAIRs and their traceability chain become critical inputs to investigations and corrective actions.

    What Auditors Typically Look for in AS9102 Records

    While each auditor brings their own style, there is a consistent core of AS9102-related questions and checkpoints. Understanding these expectations allows you to design your digital workflows around them.

    Characteristic accountability and completeness

    Characteristic accountability is central to AS9102. Auditors want to confirm that:

    • Every applicable requirement on the drawing and specification set has been identified and ballooned.
    • Each ballooned characteristic maps to exactly one row on Form 3.
    • Results on Form 3 are complete, legible, and clearly indicate acceptance or nonconformance.
    • Key and critical characteristics are identified and handled per internal and customer procedures.

    Digital tools make this easier by:

    • Automating ballooning of dimensions, GD&T, notes, and other requirements.
    • Synchronizing balloons to Form 3 so there are no missing or duplicated characteristics.
    • Providing click-through navigation between the Form 3 row and the corresponding balloon on the drawing.

    Correct usage of Forms 1, 2, and 3

    Auditors will review how you populate and control the three primary AS9102 forms:

    • Form 1 – Part Number Accountability
      They check that the part number, revision, FAI type (full, partial, delta), and related part or assembly details are accurate and consistent with your engineering and planning systems.
    • Form 2 – Product Accountability
      Expect questions about how you capture and link materials, special processes, and functional tests. Auditors verify that each entry is backed by a material certification, special process record, lab report, or functional test evidence.
    • Form 3 – Characteristic Accountability, Verification and Compatibility Evaluation
      They confirm that measurements, test results, and compatibility checks are properly recorded, with clear acceptance status and reference to the correct drawing revision.

    Misuse of forms—such as putting material data on Form 3, omitting FAI type on Form 1, or mixing drawing revisions—often triggers findings.

    Evidence of proper approvals and document control

    AS9102 FAIRs must reflect your broader document control practices. Auditors typically ask:

    • Who prepared, reviewed, and approved each FAIR—and when?
    • How do you ensure that only the latest approved FAIR template is in use?
    • What happens when a form or template is revised? Can you still retrieve prior versions?

    Digital AS9102 systems streamline these checks by embedding electronic signatures, maintaining template versions, and recording a time-stamped audit trail of changes.

    Building End-to-End Digital Traceability

    Traceability is the connective tissue that lets auditors move from drawing to FAIR to physical hardware and supporting evidence without losing the thread. A robust digital implementation captures these links by design.

    Linking FAIRs to serials, lots, and work orders

    At a minimum, your system should allow anyone to start from a specific part and quickly find:

    • The relevant FAIR(s) for that part number and configuration.
    • The associated work orders or shop orders and their status.
    • Individual serial numbers or lot numbers covered by the FAIR.

    From an audit perspective, this enables scenarios such as:

    • Starting from a serial number in service and working backward to the FAIR.
    • Starting from a FAIR and working forward to identify which batches or serials it covers.
    • Verifying that subsequent builds reference the correct baseline, partial, or delta FAIR.

    Integrating AS9102 software with ERP or MES makes these connections much more reliable than relying on manual data entry in spreadsheets.

    Associating material certs and special process records

    Auditors frequently follow the FAIR trail into materials and processes. Effective digital traceability includes:

    • Direct links between Form 2 entries and stored material certifications (e.g., heat, lot, and mill certs).
    • Attachments or references for special process records such as heat treatment, plating, welding, or NDT, including NADCAP scope where applicable.
    • Ability to filter or search FAIRs based on specific material lots or process batches when investigating issues.

    Instead of searching network folders for a PDF with a similar name to the lot number, auditors can click from the Form 2 line item directly to the supporting cert. That level of organization and speed sends a strong signal of control.

    Capturing calibration and equipment traceability

    For measurement and test data, auditors also care about the instruments and equipment used. Strong digital traceability supports:

    • Identifying which measurement devices or gages were used for specific characteristics.
    • Linking those devices to calibration records and due dates.
    • Demonstrating that no out-of-calibration equipment was used for FAI.

    Some organizations capture gage IDs directly in Form 3 or in linked inspection records. Others maintain traceability via integrated QMS tooling. Either way, the goal is to answer, with evidence: “How do you know the measurements in this FAIR are trustworthy?”

    How AS9102 Software Simplifies Audit Preparation

    Digital AS9102 platforms are not a substitute for good processes, but they make those processes visible and repeatable. The biggest audit-readiness gains come from how software centralizes data, preserves history, and standardizes outputs.

    Centralized search and retrieval across programs and suppliers

    Instead of chasing files across email, laptops, and shared drives, a central AS9102 system allows you to:

    • Search FAIRs by part number, part family, revision, work order, serial number, supplier, or customer.
    • Filter by FAI type (full, partial, delta) and status (draft, in review, approved, rejected).
    • Retrieve all FAIRs associated with a particular program or platform in seconds.

    During an audit, this means you can respond to document requests in minutes instead of hours or days, while maintaining confidence that you have the complete and correct records.

    Audit logs and version control for FAIRs and templates

    Auditors often ask, implicitly or explicitly, “How do you know this record is accurate and has not been altered inappropriately?” Strong digital controls help you demonstrate that by design:

    • Every FAIR has a full audit trail: who created it, who edited each field, who approved it, and at what date and time.
    • Template versions are controlled, so you can show exactly which revision of the AS9102 form was used for a given FAIR.
    • Historical versions of FAIRs are preserved, not overwritten, which is especially important for delta FAIs and repeated builds.

    When an auditor questions an entry or a change, you can walk through the digital history instead of relying on memory and handwritten notes.

    Standardized exports for audit evidence packages

    Many audits require you to assemble “evidence packages” that include:

    • Completed AS9102 Forms 1, 2, and 3.
    • Ballooned drawings.
    • Material certifications, special process records, and lab reports.
    • Relevant procedures or work instructions.

    Modern AS9102 software can generate these packages in standardized formats (often PDF plus native data exports) with a few clicks. Some systems also support customer-specific layouts and naming conventions while keeping a single internal data model.

    The outcome is not just audit speed, but consistency: every auditor sees complete and similarly structured evidence, which reduces confusion and follow-up questions.

    Preventing Common FAI-Related Audit Findings

    Most AS9102-related nonconformances are predictable. Understanding the patterns allows you to design your digital workflows, training, and checks to avoid repeat issues.

    Incomplete or mismatched FAIRs

    Frequent findings include:

    • FAIRs that do not cover all characteristics on the released drawing set.
    • FAIRs referencing the wrong drawing revision or obsolete specifications.
    • Inconsistencies between the part revision on the FAIR and the ERP, PLM, or purchase order.

    Digital mitigations include:

    • Automatic drawing import and ballooning tied to a specific revision.
    • Integration with PLM or ERP to pre-populate part and revision fields.
    • Validation rules that prevent approval if required fields or attachments are missing.

    Poor change control for partial and delta FAI

    Another common source of findings is how organizations handle changes:

    • Re-performing full FAI when only a subset of characteristics changed, without clearly documenting why.
    • Performing limited measurements but failing to declare the FAIR type as partial or delta on Form 1.
    • Creating new FAIRs that do not clearly reference the baseline FAIR they build upon.

    Digital AS9102 tools reduce this risk by:

    • Explicitly tagging FAIRs as full, partial, or delta and enforcing required fields for each type.
    • Reusing baseline FAIR data and clearly identifying only those characteristics impacted by the change.
    • Maintaining family trees or lineage views showing the relationships between the original and subsequent FAIRs.

    Inconsistent use of templates across sites

    Multi-site organizations and global supply chains often struggle with inconsistent FAIR formats and processes, leading to:

    • Different spreadsheet templates with different required fields.
    • Site-specific shortcuts that omit data important to customers or regulators.
    • Confusion during audits when evidence from different plants looks and behaves differently.

    By deploying a common digital AS9102 platform, you can enforce:

    • Standard templates that still allow for controlled customer-specific variants.
    • Shared workflows for preparation, review, and approval.
    • Centralized reporting on FAIR status and issues across all sites and key suppliers.

    Using FAI Data for Continuous Improvement

    Audit readiness improves dramatically when FAIRs are not just compliance paperwork but also inputs to continuous improvement. Digital traceability turns FAI data into an analytical asset.

    Trend analysis across FAIRs for recurring issues

    With structured, centralized FAI data, you can:

    • Identify characteristics that routinely run close to tolerance limits.
    • Spot recurring nonconformances for specific features, processes, or materials.
    • Compare performance across plants or suppliers for the same part or family.

    These insights inform process capability work, supplier development, and risk-based planning for future FAIs.

    Feeding lessons learned into design and process controls

    Digital FAIRs make it easier to loop findings back into engineering and manufacturing:

    • Highlight design features that consistently cause manufacturing or inspection challenges.
    • Provide quantitative evidence for adjusting tolerances, GD&T schemes, or process parameters.
    • Support risk assessments and control plans for future parts with similar features or processes.

    When auditors ask how you use data to drive improvement—not just compliance—you can point to structured analyses of FAIR results and resulting changes in design or process documentation.

    Aligning FAI improvements with AS9100 objectives

    AS9100 emphasizes risk-based thinking, process performance, and continual improvement. Digital AS9102 implementations support these objectives by:

    • Reducing the time and cost of FAI, freeing engineering capacity for proactive work.
    • Lowering FAIR rejection and rework rates through standardized, validated workflows.
    • Providing fact-based metrics on FAI cycle times, defects, and bottlenecks.

    This alignment is attractive to auditors: they see that your investment in digital FAI is part of a broader quality strategy rather than a narrow compliance response.

    Putting It All Together: A Practical Path to AS9102 Audit Readiness

    Preparing for AS9102-focused audits is not about building a separate checklist; it is about embedding audit-ready practices into your daily workflows:

    1. Standardize on clear procedures for full, partial, and delta FAI that reflect AS9102 Rev C expectations.
    2. Digitize ballooned drawings and FAIR forms so characteristic accountability and traceability are built into your tools.
    3. Connect your AS9102 system to ERP, MES, PLM, and QMS where practical to eliminate duplicate entry and mismatch risks.
    4. Control templates, approvals, and audit logs so you can demonstrate who did what, when, and under which revision.
    5. Analyze FAI data periodically to identify trends, recurring issues, and improvement opportunities.

    These steps will not guarantee a finding-free audit—no tool can—but they significantly reduce avoidable risk and show auditors that your organization manages AS9102 in a systematic, data-driven way.

    For a broader view of how digital FAI supports aerospace programs, including ballooning automation, workflow integration, and supplier collaboration, see the digital FAI and AS9102 software overview hub article.

  • AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    In aerospace manufacturing, one of the most common quality questions is not what AS9102 first article inspection is, but when it is actually required. Teams know first article inspection matters. They know customers expect a compliant FAIR. What causes real friction is deciding whether a situation calls for a full FAI, a partial FAI, or no new FAI at all.

    That decision matters because unnecessary first article work slows production, ties up quality resources, and adds documentation overhead. On the other hand, missing a valid trigger can create customer escapes, audit findings, approval delays, and serious traceability problems. In aerospace, where configuration control and product conformity carry real operational and regulatory weight, getting this right is not optional.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains the most important AS9102 FAI triggers, including new part introduction, engineering changes, process changes, production lapses, and the circumstances that justify a partial or delta FAI rather than a full reset. It also looks at how aerospace manufacturers can manage these triggers more consistently using connected digital workflows.

    If you want the broader foundation first, review AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

    What AS9102 FAI Is Designed to Prove

    AS9102 first article inspection is a structured method for verifying that a production process can manufacture a part or assembly that fully conforms to engineering, specification, and purchase order requirements at the released configuration. It is not just a sample inspection. It is not a one-time paperwork exercise. It is a formal record that shows the part definition was interpreted correctly, the process was executed properly, and the evidence of conformity is complete and traceable.

    In practice, an FAI helps answer a straightforward but high-stakes question:

    Can this exact aerospace production process, at this exact released configuration, produce conforming hardware with full documented accountability?

    That is why FAI sits so close to configuration control, traceability, launch readiness, supplier quality, and customer approval. It creates a documented baseline that can later support change management, resubmissions, investigations, and audits.

    Why Knowing the Right Trigger Matters

    Plenty of aerospace organizations understand how to complete Form 1, Form 2, and Form 3. Fewer have a disciplined internal method for deciding when a new or updated FAI is required. That is where problems begin.

    If the trigger logic is weak, teams end up doing one of two things. They either over-trigger, which creates waste and slows down manufacturing, or they under-trigger, which creates risk. Neither outcome is good. The first hurts efficiency. The second hurts compliance, customer trust, and sometimes product integrity.

    A clear trigger model helps quality and manufacturing teams:

    • Apply AS9102 consistently across programs and part families
    • Reduce unnecessary full FAIR rebuilds
    • Identify when partial or delta FAI is appropriate
    • Align change control with customer and contract expectations
    • Protect traceability when production conditions shift

    Here’s the thing. The cost of poor trigger discipline is rarely visible all at once. It shows up as late package corrections, missing evidence, confused resubmissions, duplicated work, and uncomfortable customer conversations.

    New Part Introduction Is the Most Obvious FAI Trigger

    The clearest AS9102 trigger is the first production run of a new part number or assembly. When an aerospace organization introduces a part into production for the first time, it needs objective evidence that the released design can be built and verified correctly using the intended production process.

    This usually calls for a full FAI because there is no prior approved baseline to rely on.

    What counts as a new part introduction

    New part introduction typically includes:

    • A newly released part number entering production for the first time
    • A new assembly requiring first-time product accountability
    • A part transferred from development or prototype status into controlled production
    • A customer program launch where the released configuration has not yet been formally validated

    In these cases, the FAIR establishes the first documented baseline for the product. That baseline matters later when changes occur, because it gives the organization something traceable to compare against.

    Why aerospace treats this carefully

    In aerospace, new part introduction is not just about proving that one part measured correctly on one day. It is about proving that the released configuration, manufacturing route, inspection method, material traceability, and special process chain all support conformity. That is why the first baseline FAIR often becomes an anchor record for the life of the part.

    Design Changes Often Trigger Full or Partial FAI Activity

    Engineering changes are one of the most common reasons organizations revisit FAI. Not every revision change means the entire FAIR must be rebuilt, but changes that affect requirements, form, fit, function, interfaces, or inspection criteria often require at least a partial or delta FAI.

    Examples of design changes that may trigger FAI

    • Dimensional changes to a feature on the drawing
    • Tolerance changes on an existing characteristic
    • Material specification changes
    • Updated notes affecting finish, marking, or identification
    • Changes to critical, key, or safety-related characteristics
    • Revision changes affecting mating or installation conditions

    The real question is not simply whether the drawing revision changed. The better question is whether the released product definition changed in a way that affects conformity or verification. If it did, the FAI baseline likely needs to be updated.

    When a design change justifies a partial or delta FAI

    If the change affects only certain characteristics rather than the entire part, a partial or delta FAI is often the right choice. That allows the organization to revalidate only the impacted features while preserving the unaffected baseline from the original FAIR.

    This approach is especially valuable in aerospace because programs often evolve slowly through controlled revisions, and rebuilding a full FAIR every time can become needlessly expensive. Still, that efficiency only works if the company has strong revision control and can clearly identify which characteristics were affected.

    Process Changes Can Trigger FAI Even When the Drawing Stays the Same

    One of the biggest mistakes organizations make is assuming that if the drawing did not change, the FAIR does not need attention. In aerospace manufacturing, process changes matter because the product may be the same on paper while the route used to build it has changed in a meaningful way.

    If the process changes in a way that could affect part conformity, a new or updated FAI may be required.

    Common process-related FAI triggers

    • New manufacturing equipment or machine replacement
    • New tooling, fixtures, or program changes
    • Method changes in machining, forming, assembly, or inspection
    • Changes to sequence of operations that affect product outcome
    • Transfer of work between facilities or production cells
    • Changes in outside processing sources for controlled operations

    What this really means is that aerospace FAI is not only about the part definition. It is also about the process definition behind that part. If the way the part is made changes enough to alter risk, the FAIR logic needs to catch up.

    Why process changes matter so much in aerospace

    Aerospace production often involves tight tolerances, special processes, controlled materials, complex routings, and customer-specific source requirements. A machine swap, tooling update, supplier change, or move to a different facility can alter process behavior even if the part number and drawing revision remain identical. That is why smart trigger discipline looks at more than engineering release history.

    Material and Special Process Changes Require Careful Review

    In aerospace, traceability to material and special process evidence is central to FAI integrity. Form 2 exists for a reason. If the source or nature of the controlled inputs changes, organizations need to evaluate whether a new or updated FAI is required.

    Typical material and source changes that may trigger FAI

    • A new supplier for a controlled alloy or raw material
    • A change in material specification or condition
    • A new special process source for plating, heat treatment, NDT, coating, or similar operations
    • A change in approval status or scope of a special process provider
    • A change in process parameters that affects product characteristics

    Some of these may require only partial FAI activity. Others may justify a broader review, depending on the criticality of the change and the customer’s expectations. Either way, they should never be treated as invisible background changes. In aerospace, they are often part of the conformity story.

    Production Lapses Are a Real Aerospace Trigger

    Aerospace manufacturing does not always run at a steady cadence. Many parts are made intermittently. Some programs have long pauses. Some part numbers may go quiet for months or years before restarting. That makes production lapse one of the most important and most overlooked FAI triggers.

    If production has been dormant long enough, organizations may need to review whether the baseline process can still be trusted without refreshed validation.

    Why lapse-based triggers exist

    A long production gap can introduce risk even when the part and process documentation appear unchanged. During the lapse, a lot may have shifted:

    • Operators may have changed
    • Tooling may have worn or been replaced
    • Programs may have been updated
    • Equipment may have been serviced or relocated
    • Suppliers may have changed
    • Inspection methods may have evolved

    That is why production lapse should be treated as a process risk issue, not just a scheduling detail.

    How lapse thresholds are handled

    Many organizations use internal thresholds, customer requirements, or contract-specific rules to define what counts as a significant lapse. A common reference point is two years, but the right answer always depends on the customer, the product, and the organization’s quality system. The main point is that lapse-based trigger logic should be defined clearly and applied consistently.

    Full FAI vs Partial FAI vs Delta FAI

    One reason AS9102 remains practical in real aerospace operations is that it does not force a full restart every time something changes. Instead, it allows manufacturers to scale the response to the actual scope of impact.

    When a full FAI is usually appropriate

    • First production of a new part number or assembly
    • Major design change affecting broad portions of the part definition
    • Major process change with wide conformity impact
    • No reliable baseline FAIR exists
    • Customer or contract explicitly requires a complete new FAIR

    When a partial or delta FAI is often the better choice

    • Only selected characteristics changed
    • A limited process change affected a defined subset of features
    • Material or source changes affected traceability but not the full configuration
    • The baseline FAIR remains valid for unaffected requirements

    The discipline here is simple to say but harder to execute: revalidate what changed, preserve what did not, and document the logic clearly.

    Why organizations struggle with delta FAI

    Delta FAI sounds efficient, and it is, but only when the underlying data is structured well enough to support it. If characteristics are trapped in static spreadsheets, traceability is fragmented, or revision history is unclear, teams often end up redoing far more than necessary. In those environments, delta FAI becomes confusing because nobody can cleanly separate affected from unaffected requirements.

    Customer-Specific Requirements Still Matter

    AS9102 gives aerospace manufacturers a standard framework, but it does not erase customer-specific expectations. Many primes and upper-tier suppliers apply additional rules around when FAI is required, what counts as a significant change, how lapse thresholds are handled, and what submission format is acceptable.

    That means the right internal question is never only:

    What does the standard allow?

    It also needs to be:

    What did the customer contract, purchase order, or program requirement actually ask for?

    This matters because a technically defensible partial FAI may still be rejected if the customer expects a full resubmission package, specific portal workflow, or extra supporting documentation.

    Common Mistakes Aerospace Teams Make with FAI Triggers

    Most FAI trigger failures come from poor process visibility rather than bad intent. Teams are busy, systems are disconnected, and changes are sometimes managed in silos.

    Typical mistakes include

    • Treating revision changes as administrative without checking affected characteristics
    • Ignoring process changes because the drawing stayed the same
    • Missing lapse-based triggers on low-volume or intermittent parts
    • Failing to assess source changes for material or special processes
    • Overusing full FAI because delta logic is too hard to manage manually
    • Assuming one customer’s interpretation applies to every program

    The result is usually one of two ugly outcomes. Either the organization creates a lot of unnecessary quality work, or it ships with weaker evidence than the customer expects. Neither is a good place to be.

    How Digital Systems Make FAI Trigger Decisions Easier

    Digital FAI platforms are at their best when they do more than produce forms. They should help aerospace manufacturers manage trigger logic as part of a connected quality and manufacturing workflow.

    What a strong digital workflow can do

    • Maintain a traceable baseline FAIR by part number and revision
    • Track changes to characteristics, materials, and process routes
    • Highlight which features were affected by a revision or process update
    • Support partial or delta FAI generation without recreating everything
    • Connect Form 1, Form 2, Form 3, ballooned drawings, and certifications in one record set
    • Preserve audit history around why a given trigger decision was made

    That last point matters more than people think. In aerospace, it is not enough to make the right trigger decision. You often need to show later why that decision was reasonable.

    Why this matters for Connect 981-style operations

    Connected platforms are especially useful in regulated manufacturing because they reduce the gap between engineering changes, manufacturing process shifts, and quality documentation. Instead of waiting for someone to notice a trigger manually, the system can support earlier visibility into what changed and what evidence may need to be refreshed.

    That does not replace engineering judgment. It makes that judgment more consistent, more traceable, and less dependent on memory.

    How to Build a Better Internal FAI Trigger Policy

    Every aerospace manufacturer should define a practical internal trigger policy that aligns with AS9102, customer requirements, and real production conditions. The best policies are not vague. They are specific enough that quality, manufacturing, and engineering teams can use them without guesswork.

    A strong internal policy should define

    • What counts as a new part or first production run
    • What kinds of design changes trigger full, partial, or delta FAI
    • What kinds of process changes require review
    • How material and special process source changes are evaluated
    • What lapse threshold applies by default
    • How customer-specific rules override standard internal logic
    • Who has authority to approve the trigger decision
    • How that decision is documented for future audit or customer review

    Without this, organizations tend to rely too heavily on tribal knowledge. That works until the key person is out, the program changes hands, or the customer starts asking harder questions.

    Final Takeaway

    AS9102 FAI triggers are not just a compliance detail. They are part of how aerospace manufacturers control change, preserve traceability, and protect confidence in the production process. New parts, engineering changes, process shifts, material source changes, and production lapses can all justify a new or updated FAIR. The real challenge is knowing when a full FAI is necessary and when a partial or delta FAI is the smarter, defensible path.

    The organizations that handle this well do not treat FAI as a last-minute quality document. They treat it as part of a connected operational system that links engineering, production, inspection, and customer requirements. That is where the real efficiency shows up, and it is also where the strongest compliance posture comes from.

    To go deeper into digital workflows, FAIR structure, and connected aerospace quality execution, read AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

  • Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Building the Business Case and Measuring ROI for Digital AS9102 FAI

    Aerospace manufacturers and suppliers rarely question whether they must comply with AS9102. The real question is whether they can continue to absorb the time, risk, and opportunity cost of manual first article inspection (FAI) processes.

    Digital AS9102 software promises shorter cycle times, fewer errors, and cleaner audits. To win budget and executive support, those promises must be translated into a clear, defensible business case with tangible financial impact.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This guide provides a structured way to quantify the return on investment (ROI) of AS9102 software. You will learn which metrics to track, how to model savings, and how to align your case with quality, operations, and IT stakeholders. For a broader view of capabilities and architecture, see our unified AS9102 and digital FAI platform overview.

    Why AS9102 FAI Is a High-Leverage Improvement Area

    FAI sits at the intersection of engineering, quality, operations, and customer delivery. That makes it one of the highest-leverage processes to digitize: small improvements compound across programs, plants, and suppliers.

    Engineering time consumed by manual FAIRs

    In many aerospace organizations, quality and manufacturing engineers spend a surprising portion of their time on manual first article inspection reports (FAIRs):

    • Hand-ballooning multi-sheet drawings with hundreds of characteristics
    • Copying data into spreadsheet-based Forms 1, 2, and 3
    • Chasing material certs, special process documentation, and signatures
    • Reworking rejected FAIRs from customers or internal approvers

    For complex parts, a single full FAIR frequently consumes 8–24 hours of engineering time. If you produce dozens or hundreds of FAIRs per year, the labor cost and capacity impact become substantial.

    Impact of FAI delays on deliveries and cash flow

    FAI is often on the critical path for first deliveries and engineering changes. When FAIRs run late or are rejected, the impact includes:

    • Delayed shipment of first production lots
    • Slippage in new program milestones and entry into service
    • Deferred revenue recognition and slower cash collection
    • Premium freight or overtime to recover schedule

    Even if the direct cost of an engineer’s time appears modest, the downstream schedule risk can be far more expensive. A credible business case should connect FAI performance to late deliveries and the cost of schedule recovery.

    Hidden costs of rejections and audit findings

    Manual FAIRs are error-prone. Common issues include missed or duplicated balloons, mismatched drawing revisions, incomplete Form 2 documentation, and incorrect tolerance interpretation. These lead to:

    • Customer rejections and resubmissions
    • Internal quality holds while documentation is corrected
    • AS9100 or customer audit findings tied to FAI and traceability
    • Reduced customer confidence and increased oversight

    Digital AS9102 software cannot eliminate all issues, but it can dramatically reduce documentation-related nonconformances. That reduction is a core component of AS9102 software ROI.

    Key Metrics for Evaluating AS9102 Performance

    Before you model ROI, you need a baseline. The following metrics create a clear, quantifiable picture of current performance and provide a way to measure improvement after implementing digital FAI.

    Average time to complete full and delta FAIRs

    Track both engineering and overall calendar time:

    • Engineering effort per FAIR (hours of quality/manufacturing engineering)
    • Elapsed cycle time from trigger to approved FAIR (days)
    • Separate values for full vs. delta FAI

    Suggested approach:

    1. Select a representative sample (e.g., last 20–50 FAIRs across key programs).
    2. Capture effort from time sheets, issue trackers, or quick engineer estimates.
    3. Record dates for FAI trigger, initial submission, rejection (if any), and final approval.

    This baseline is essential for modeling time savings from automated ballooning, form population, and streamlined approvals.

    FAIR rejection and rework rates

    Next, examine quality and completeness of your FAIRs:

    • Percentage of FAIRs rejected by customers or internal approvers
    • Average number of resubmission cycles per FAIR
    • Primary reasons for rejection (documentation vs. product nonconformance)

    Digital FAI primarily affects documentation-related rejections: missed characteristics, mismatched revisions, missing certs, or inconsistent use of AS9102 Forms 1, 2, and 3. Categorizing issues lets you estimate how much rework digital tools can realistically reduce.

    Late deliveries attributable to FAI

    Where possible, identify how often FAI is a direct or contributing cause of late delivery:

    • Number of shipments delayed due to incomplete or rejected FAIRs
    • Average days of delay when FAI is the primary cause
    • Estimated cost of delay (expedite costs, penalties, or internal recovery spend)

    This data is often spread across ERP notes, program reviews, and customer complaints. Even directional estimates (e.g., 5–10 orders per year delayed primarily due to FAIRs) can materially strengthen your business case.

    Estimating the ROI of AS9102 Software

    Once you have baseline metrics, you can model ROI using a combination of time savings, quality risk reduction, and audit efficiency. Avoid promising a single precise number; instead, build a conservative, realistic range.

    Modeling time savings per FAIR and annual volume

    A practical way to estimate time savings is to compare current effort with benchmark reductions from digital FAI:

    • Manual baseline: 8–24 engineering hours per full FAIR is common for complex aerospace parts.
    • Digital target range: Many organizations see full FAIR effort drop to 2–6 hours once ballooning and form population are automated.

    Define variables for your model, for example:

    • H_manual_full = average manual hours per full FAIR
    • H_digital_full = expected digital hours per full FAIR
    • H_manual_delta = average manual hours per delta FAIR
    • H_digital_delta = expected digital hours per delta FAIR
    • N_full = number of full FAIRs per year
    • N_delta = number of delta FAIRs per year
    • Blended_rate = loaded hourly cost for engineers (salary + benefits + overhead)

    Then compute annual labor savings:

    Labor_savings = ((H_manual_full - H_digital_full) × N_full
                     + (H_manual_delta - H_digital_delta) × N_delta)
                     × Blended_rate
    

    For example, if you save 6 hours on 150 FAIRs per year at a blended rate of $80/hour, labor savings alone is roughly $72,000 annually.

    Quantifying reduction in customer escapes and audit issues

    Digital AS9102 software helps enforce complete characteristic accountability, correct use of Rev C forms, and traceability to materials and special processes. The impact shows up as:

    • Fewer documentation-related customer rejections
    • Reduced nonconformance costs linked to incorrect or missing FAIRs
    • Lower likelihood of audit findings tied to FAI records

    To model this conservatively:

    1. Estimate your current annual cost of documentation-related FAI issues (extra engineering time, expedited shipments, minor concessions, or penalties).
    2. Apply an improvement factor based on target rejection reduction (e.g., 20–40% reduction in documentation-related rejections).
    3. Include the value of avoided audit findings (e.g., time for root cause analysis, corrective actions, follow-up audits).

    The formula can be framed as:

    Quality_savings = (Baseline_FAIR_issue_cost × Expected_reduction_percentage)
    

    Because these numbers can be sensitive, use ranges and anonymized examples rather than suggesting guaranteed outcomes.

    Factoring in training and implementation costs

    To present a credible ROI, you must subtract real implementation costs:

    • Software license and subscription: annual or multi-year
    • Implementation services: configuration, integrations, data migration
    • Training time: hours spent by engineers and inspectors learning the system
    • Change management: internal project management and process updates

    Define total annualized cost:

    Total_cost = Software_fees + (Implementation_services / Amortization_years)
                 + Training_cost + Internal_project_cost
    

    Then calculate ROI over a chosen period (often 3 years):

    Annual_benefit = Labor_savings + Quality_savings + Audit_savings + Schedule_risk_impact
    ROI = (Annual_benefit - Total_cost) / Total_cost
    Payback_period = Total_cost / Annual_benefit
    

    Present ROI as a range (e.g., 40–120% over three years) to reflect uncertainty in assumptions and acknowledge that actual results depend on baseline maturity and implementation quality.

    Example Before-and-After Scenarios

    Different organizations start from different levels of digital maturity. The business case for AS9102 software looks a bit different if you are transitioning from paper and spreadsheets versus upgrading from a stand-alone ballooning tool.

    Manual spreadsheets vs. stand-alone ballooning tools

    For teams working primarily with paper drawings and Excel forms, moving to a stand-alone FAI tool typically delivers:

    • Time savings: Auto-ballooning and automatic Form 3 population can cut FAIR creation time by more than half.
    • Error reduction: Fewer missed characteristics and better revision control.
    • Documentation consistency: Standard templates aligned with AS9102 Rev C.

    A high-level scenario:

    • Baseline: 10 hours per full FAIR; 100 FAIRs/year.
    • After stand-alone tool: 4–5 hours per full FAIR.
    • Labor savings: 5–6 hours × 100 FAIRs × blended rate.

    This is often the first step for single-site suppliers with limited integration needs.

    Stand-alone tools vs. integrated operations platforms

    Organizations already using point tools may still struggle with disconnected data and duplicate work across ERP, MES, PLM, and QMS. Moving to an integrated aerospace operations platform that embeds AS9102 FAI alongside work instructions and in-process inspections can add:

    • Reduced re-keying of part, revision, and routing data
    • Direct import of CMM and measurement data into Form 3
    • Unified workflows for FAIR approvals, nonconformance management, and change control
    • Analytics spanning FAI, in-process, and final inspection data

    Here, savings come not just from FAI creation time, but also from fewer discrepancies between systems, faster approvals, and better reuse of data for audits and continuous improvement.

    Multi-site standardization and supplier collaboration gains

    For OEMs and large Tier 1 suppliers, the largest ROI often appears when standardizing AS9102 processes across plants and suppliers:

    • Common FAIR templates and workflows across internal sites
    • Supplier portals for submitting FAIRs in a consistent structure
    • Global visibility into FAI status across programs and tiers
    • Centralized management of prime- or customer-specific AS9102 requirements

    Benefits include:

    • Higher throughput per engineer because tools, templates, and expectations are standardized.
    • Lower training overhead for transfers and new hires.
    • Better supplier performance through clear expectations and shared data.
    • Improved audit readiness at both central and site levels.

    While this level of deployment takes more upfront investment, multi-site standardization typically yields compounding benefits over time.

    Aligning the Business Case with Stakeholder Priorities

    A strong AS9102 software business case speaks different languages to different stakeholders. The core ROI model may be the same, but emphasis and messaging should vary.

    Quality and compliance leadership perspectives

    Quality leaders and compliance managers focus on:

    • AS9102 Rev C conformity and correct use of Forms 1, 2, and 3
    • Reduction in customer rejections and concessions due to FAIR issues
    • Audit readiness for AS9100, customer, and regulatory reviews
    • Traceability from ballooned drawing to measurement, material, and process records

    For this audience, highlight:

    • Lower documentation-related nonconformance rates
    • Faster and more confident responses during audits
    • Reusable FAI data for trend analysis and corrective actions

    Operations and program management concerns

    Operations, plant managers, and program leaders care about:

    • On-time delivery and schedule adherence
    • Engineering capacity to support new product introduction and changes
    • Impact of FAI bottlenecks on throughput and WIP
    • Cost of recovery when FAI issues delay shipments

    For them, emphasize:

    • Reduced cycle time for FAIR approvals
    • Fewer late deliveries attributable to FAI
    • More engineering hours available for process improvement and problem-solving
    • Clear dashboards showing FAI status across programs

    IT and digital transformation alignment

    IT and digital transformation teams look for:

    • Alignment with the broader digital thread and data strategy
    • Integration with ERP, MES, PLM, and QMS
    • Security, access control, and audit logging
    • Scalability across sites and suppliers

    Key talking points include:

    • Standards-based data structures for AS9102 FAIRs
    • Available APIs or connectors to existing systems
    • Cloud and on-premises deployment options, as applicable
    • Support for future capabilities like model-based definition and AI-assisted analytics

    Position digital FAI as a building block in a broader smart manufacturing roadmap, not an isolated point solution.

    Practical Steps to Pilot and Scale Digital FAI

    Even with a compelling ROI model, many organizations benefit from a pilot to validate assumptions, build internal champions, and refine processes before full rollout.

    Selecting candidate parts and suppliers

    A good pilot scope is big enough to be meaningful but small enough to manage. Consider:

    • Parts with medium-to-high complexity (100–300 characteristics) where time savings will be visible
    • Programs with active customer engagement and upcoming engineering changes
    • Sites or suppliers that experience repeated FAIR rejections or long cycle times
    • Internal teams that are open to change and willing to provide detailed feedback

    Include both full and delta FAI cases so you can evaluate how the software handles engineering change scenarios.

    Defining success criteria and measurement plans

    Before the pilot starts, agree on success metrics and how they will be measured. Common criteria include:

    • Reduction in average engineering hours per FAIR
    • Reduction in FAIR cycle time from trigger to approval
    • Decrease in documentation-related rejections
    • User adoption and satisfaction (surveys or interviews)

    Set realistic targets (e.g., 30–50% time reduction in the first phase, improving further as teams gain proficiency) rather than assuming best-case numbers from day one.

    Planning phased rollout across plants and programs

    After a successful pilot, expand in phases:

    1. Stabilize the pilot: Address lessons learned, refine templates, and finalize integrations for the initial site.
    2. Extend to similar parts and programs: Roll out to adjacent product families where requirements and workflows are similar.
    3. Expand to additional sites: Standardize governance, training, and configuration management so each new site ramps faster.
    4. Onboard key suppliers: Provide training and support for tiered suppliers to submit FAIRs using your preferred digital process.

    Each phase should have clear objectives, timelines, and owners. Use early phases to build internal case studies and testimonials that support broader adoption.

    Using a Unified Digital FAI Platform as a Strategic Lever

    While any move away from manual spreadsheets will improve FAI efficiency, a unified operations platform that embeds AS9102 within broader aerospace workflows can unlock additional strategic benefits:

    • Consistent application of AS9102 Rev C across programs, plants, and suppliers
    • Centralized control over templates, customer-specific requirements, and change histories
    • Integrated nonconformance and corrective action management tied to specific FAIRs and characteristics
    • Real-time dashboards for FAI throughput, bottlenecks, and audit readiness

    As described in the AS9102 software: digital first article inspection for aerospace manufacturing overview, platforms like Connect 981 treat FAI as one element of a connected aerospace operations environment. That broader context can strengthen your business case, especially for multi-site and prime-level stakeholders.

    Building a Credible, Actionable Business Case

    To summarize, a strong business case for AS9102 software should include:

    • Current-state baseline for FAIR time, rejection rates, and FAI-driven delays
    • Projected time savings based on realistic efficiency ranges
    • Quality and audit impacts framed as risk and cost reductions, not guarantees
    • Implementation and operating costs with transparent assumptions
    • ROI range and payback period, ideally under 18–24 months
    • Stakeholder-specific benefits for quality, operations, and IT
    • Pilot plan with clear success criteria and a phased rollout strategy

    By grounding your proposal in concrete metrics and openly acknowledging assumptions, you can move AS9102 software from a “nice to have” tool to a strategic investment in capacity, compliance, and customer performance.

    The next step is to gather your baseline data, model a conservative ROI scenario, and design a pilot that tests both the technology and the process changes needed for sustainable improvement.

  • From Stand-Alone FAI Tools to Connected Aerospace Operations Platforms

    From Stand-Alone FAI Tools to Connected Aerospace Operations Platforms

    From Stand-Alone FAI Tools to Connected Aerospace Operations Platforms

    Digital AS9102 software platforms now sit at the center of how aerospace organizations manage first article inspection (FAI), new part introduction, and regulatory compliance. But not every company is ready to jump straight from spreadsheets to a fully integrated operations platform. Many teams start with stand-alone ballooning and FAIR tools before they connect FAI to the broader digital thread.

    This article explains the digital maturity journey from paper-based FAI to point solutions and, ultimately, to connected aerospace operations platforms. It outlines the trade-offs at each stage and helps you decide which approach aligns with your programs, customer mix, and long-term digital strategy.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you need a broader grounding in AS9102 and digital FAI before diving into architecture choices, see our AS9102 software and digital FAI overview.

    The Three Maturity Levels of FAI Digitalization

    Most aerospace organizations follow a recognizable path in how they manage AS9102 FAI:

    Paper and spreadsheets

    At the earliest stage, FAI is executed with manual tools:

    • Printed drawings ballooned by hand
    • Excel-based FAIR templates managed on shared drives
    • Certificates and special process records collected via email
    • Approvals captured through signatures on paper or static PDFs

    This approach can work for low volumes, but it tends to break down when any of the following factors appear:

    • Hundreds of characteristics per drawing
    • Frequent engineering changes (delta FAI)
    • Multiple customer-specific FAIR formats
    • Multi-site operations or complex supply chains

    Cycle times stretch to days or weeks, and error rates (missed balloons, wrong revisions, duplicated data entry) create repeated FAIR rejections and audit pain.

    Stand-alone FAI tools

    The next step is adopting dedicated point solutions that automate ballooning and FAIR creation:

    • Import drawings and generate balloon numbers digitally
    • Auto-populate Form 3 rows from extracted characteristics
    • Standardize AS9102 Forms 1, 2, and 3 templates
    • Store FAIRs in a local or cloud repository

    This sharply reduces the time spent on manual ballooning and basic data entry. For single plants or small quality teams, it can be a high-ROI improvement, often cutting a typical full FAIR from 8–24 hours to a few hours or less.

    The limitation: these tools often remain disconnected from ERP, MES, PLM, and broader quality workflows. FAI becomes more efficient locally but still operates as an island.

    Integrated digital operations platforms

    At the highest maturity level, FAI lives inside a connected aerospace operations platform, where:

    • Work instructions, in-process inspections, nonconformances, and FAIRs share a unified data model
    • FAI requirements are triggered automatically by part configuration, routing, and change events
    • Measurement data can flow directly from CMMs or shopfloor inspection tools into Form 3
    • Multi-site and supplier FAIRs are governed via common templates and workflows

    The step up from stand-alone tools to platforms is about connecting FAI to everything around it: design, planning, execution, and compliance. It typically requires more upfront design and change management, but delivers compounding benefits as programs and sites scale.

    Pros and Cons of Stand-Alone FAI Tools

    Before committing to a full platform, many organizations evaluate or adopt stand-alone AS9102 point solutions. Understanding their strengths and constraints helps you decide whether they are a long-term answer or a stepping stone.

    Speed of adoption and localized benefits

    Stand-alone FAI tools are attractive because they:

    • Can often be deployed by a single plant or even a single quality engineer
    • Require relatively limited IT involvement compared to platform projects
    • Provide quick wins in ballooning speed and standard form generation
    • Are familiar to users who already work with desktop or office tools

    For organizations that:

    • Run a few FAIs per month
    • Have predominantly single-site production
    • Face moderate rather than extreme audit pressure

    these tools can represent a practical and cost-effective solution.

    Data silos and manual bridges to other systems

    The main drawback of stand-alone FAI tools is that they often operate as a data silo. Typical pain points include:

    • Double data entry: Part numbers, revisions, and order data manually copied from ERP or MES into the FAI tool
    • Attachment hunting: Material certs, process records, and approvals scattered across emails and file shares
    • Limited traceability: Difficult to navigate from a nonconformance or audit finding back to the originating FAIR and related shopfloor context
    • Isolated analytics: FAI measurements not easily aggregated with in-process or final inspection data

    Teams compensate with manual bridges—spreadsheets, copy-paste, and ad hoc reports. These workarounds tend to reintroduce errors and drag down the efficiency gains achieved by the tool itself.

    Suitability for specific plant sizes and part portfolios

    Stand-alone tools are usually best suited to environments with:

    • One or a few manufacturing sites
    • Lower volumes of FAI events
    • Relatively simple customer requirements
    • Limited need for cross-site reporting or standardized global governance

    If your portfolio is dominated by build-to-print work with stable designs and predictable FAI demand, a point solution may remain viable for years. As soon as you face frequent design changes, multi-site collaboration, or tighter digital thread expectations from primes, the limitations become more visible.

    What Connected Operations Platforms Add

    Connected aerospace operations platforms treat AS9102 FAI as one component of a coordinated production and quality system. This changes both the scope and the impact of your digital FAI investment.

    Unified data model for work instructions, FAI, and inspections

    A platform creates a shared context for all execution and quality activities. For example:

    • Each operation in a routing has linked work instructions and inspection steps
    • FAI characteristics are tied to the same features and operations used for in-process checks and final inspections
    • Nonconformances reference specific characteristics, work orders, serials, and suppliers

    This unified data model enables:

    • Automatic population of FAIR fields from existing master data
    • Direct reuse of FAI characteristics for ongoing inspection plans
    • Elimination of inconsistencies between what was planned, what was built, and what was inspected

    Cross-site standardization and governance

    For OEMs and multi-site suppliers, consistency is as important as efficiency. With a connected platform, you can:

    • Define standard AS9102 templates and workflows once and roll them out globally
    • Enforce common rules for full, partial, and delta FAI, including how change notices are interpreted
    • Support customer-specific formats while retaining a single underlying data structure
    • Govern permissions, approvals, and electronic signatures centrally

    This reduces variability between plants and suppliers, which is particularly valuable when primes or regulators review FAIRs across your network.

    Analytics and continuous improvement across processes

    Because platforms integrate FAI with in-process inspections, NCRs, and corrective actions, you can analyze patterns that are invisible in stand-alone tools, such as:

    • Characteristics that repeatedly appear in both FAI and production nonconformances
    • Operations, machines, or suppliers associated with clusters of FAI issues
    • Programs where delta FAI volume indicates design instability or process risk

    Over time, this supports targeted improvements in design-for-manufacturability, process capability, and supplier development—turning FAI data into a strategic asset instead of a one-time compliance artifact.

    Decision Factors: Which Approach Fits Your Organization?

    Choosing between stand-alone FAI tools and integrated AS9102 software platforms is not only a technology decision. It is a question of timing, priorities, and organizational capacity.

    Volume, complexity, and customer mix

    Consider your current and future workload:

    • FAI volume: How many full and delta FAIRs do you execute per month and per site?
    • Part complexity: How many characteristics per drawing, and how many special processes and certs per part?
    • Customer mix: Do you serve multiple primes with different FAIR formats and quality clauses?
    • Supply chain structure: Are you coordinating FAIs across multiple internal plants and tiered suppliers?

    Low volumes and simple programs can be well served by stand-alone tools. Complex, high-volume environments usually benefit from a platform approach that avoids duplicated work and fragmented records.

    IT strategy and digital thread roadmaps

    Your company’s broader digital strategy should also guide the choice:

    • If you are standardizing on a digital thread connecting PLM, ERP, MES, and quality, it is usually more effective to select an AS9102 solution that can integrate natively into that architecture.
    • If your IT roadmap is still emerging and budgets are tight, a stand-alone tool can function as an interim step while you design the longer-term ecosystem.

    Either way, it is wise to evaluate how easily today’s choice can evolve—whether data can be migrated, and whether the vendor’s roadmap aligns with your future integration needs.

    Change management capacity and timeline

    Implementing a connected operations platform requires more than software installation:

    • Process harmonization across plants and teams
    • Training engineers, inspectors, and supervisors on new workflows
    • Aligning quality, manufacturing, and IT stakeholders

    If you need relief immediately for a single site under intense FAI pressure, a focused tool can stabilize the situation while you build support for a broader platform. If you already have sponsorship for digital transformation and cross-functional governance, going directly to a platform can help you avoid rework and tool sprawl.

    Transitioning from Tools to Platforms Without Disruption

    Many organizations will not choose between stand-alone FAI tools and platforms in a single step; they will move through a transition where both coexist. Managing that transition thoughtfully reduces risk and protects ongoing production.

    Migrating historical FAIRs and templates

    Historical AS9102 data has real value for audits, change analysis, and future delta FAIs. When moving to a platform, consider:

    • Which FAIRs must be migrated (e.g., active programs, key customers, recent serials)
    • How to convert existing Forms 1–3 into structured records that maintain characteristic accountability
    • How to map old template variations into a standardized platform model without losing required customer fields

    Not every legacy FAIR needs full conversion. Many teams choose a risk-based approach—migrating high-criticality programs and leaving older or low-risk FAIRs in an archived, read-only state.

    Training and process harmonization

    Platform rollouts are an opportunity to clean up inconsistent practices:

    • Agree on standard rules for when full, partial, and delta FAI are required
    • Define naming conventions for parts, revisions, and FAIR identifiers
    • Align how key characteristics, critical characteristics, and special process indicators are flagged

    Training should focus not only on button clicks, but on why these rules matter for auditability and traceability. This helps teams see FAI as part of an integrated quality system rather than another compliance burden.

    Hybrid approaches during the transition phase

    During migration, it is common to run a hybrid model:

    • Some legacy programs continue using the stand-alone tool until completion
    • New programs and high-visibility customers start in the platform from day one
    • Bridges (e.g., CSV imports or APIs) transfer essential data between systems

    Clear scoping and communication are key. Define which parts and customers are in which system, how approvals work in each, and when a given program will transition fully to the platform.

    Future-Proofing Your AS9102 Digital Strategy

    Choosing between stand-alone FAI tools and connected operations platforms is ultimately about future-proofing. Aerospace compliance and digital expectations will continue to evolve; your AS9102 software platforms need to keep pace.

    Preparing for MBD, AI, and advanced analytics

    Over the coming years, leading aerospace organizations are likely to expand:

    • Model-based definition (MBD) and 3D PMI as primary design authorities
    • AI-assisted inspection planning, suggesting which characteristics warrant tighter controls
    • Advanced analytics correlating FAI data with process capability and field performance

    A future-ready AS9102 solution should be able to:

    • Handle both 2D drawings and 3D model inputs
    • Expose FAI data in a way that analytics tools and data scientists can easily consume
    • Support incremental automation, such as automatic anomaly detection in measurement results

    Ensuring scalability for new programs and suppliers

    As you win new programs or expand globally, your FAI system will need to scale without multiplying manual work. Consider:

    • How quickly new sites, suppliers, and customers can be onboarded
    • Whether FAIR templates and workflows are configurable without custom code
    • How licensing and infrastructure models support growth across regions

    Platforms are generally better positioned for this kind of scaling because they centralize governance while allowing local teams to operate within defined frameworks.

    Governance and ownership of FAI data long term

    Finally, clarify who owns and stewards FAI data as a strategic asset:

    • Which roles are accountable for data quality and template changes?
    • How are customer-specific requirements and revisions controlled?
    • How is data retained for long-term regulatory and contractual obligations?

    Whether you remain on a stand-alone tool or move to a connected platform, explicit governance prevents FAI from slipping back into ad hoc practices as organizations and programs evolve.

    Putting It All Together

    The path from manual FAI to connected operations is not one-size-fits-all. A practical way to plan your AS9102 digitalization journey is to:

    1. Map your current maturity: Paper, stand-alone tool, or partially integrated platform.
    2. Quantify the pain: Cycle time, rejection rates, audit findings, and late deliveries tied to FAI.
    3. Align with strategy: Ensure your FAI approach fits your company’s digital thread and smart factory roadmap.
    4. Design a staged plan: Stabilize urgent bottlenecks quickly, then move toward platform-level integration as capacity and sponsorship grow.

    AS9102 software platforms that embed FAI into a unified operations environment offer the strongest long-term leverage—especially for organizations managing complex programs, multi-site networks, and demanding prime customers. Stand-alone tools can still play a useful role, particularly as transitional solutions or for focused use cases.

    By viewing FAI not just as a compliance requirement but as a core node in your digital operations strategy, you can unlock better schedule performance, lower quality costs, and stronger customer confidence across your aerospace programs.

  • The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    The Future of Digital FAI: MBD, AI, and the Aerospace Digital Thread

    First article inspection (FAI) is no longer just a stack of AS9102 forms checked before releasing a new aerospace part to production. Over the next few years, FAI will sit at the intersection of model-based definition (MBD), AI-assisted analytics, and the broader aerospace digital thread that connects design, planning, execution, and in-service data. Teams that still treat FAI as an isolated paperwork exercise will struggle to keep pace with program complexity and customer expectations.

    This article explores how digital FAI is evolving, and what quality, manufacturing, and engineering leaders should expect from the next generation of AS9102 software. It builds on foundational concepts from AS9102 software for digital first article inspection, and looks ahead to how MBD, AI, and connected factory systems will reshape day-to-day workflows.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    From 2D Drawings to Model-Based Definition (MBD)

    Most aerospace organizations still anchor FAI on 2D drawings and PDF packages, even when design authority already maintains a full 3D model. That gap creates redundant work: engineers translate 3D intent back into 2D, then FAI teams balloon the drawing and re-enter characteristic data into AS9102 forms.

    What MBD and PMI Mean for FAI

    Model-based definition (MBD) moves the authoritative product definition into the 3D model itself. Dimensions, geometric tolerancing (GD&T), surface finishes, and notes are captured as product manufacturing information (PMI) attached directly to model features. For FAI, that means:

    • The 3D model becomes the primary source for characteristic extraction, not a downstream 2D derivative.
    • Balloon numbers and Form 3 rows can be generated from PMI tags rather than from optical character recognition on a PDF.
    • Design changes propagate through PLM-managed models in a controlled way, reducing the risk of using the wrong revision during FAI.

    In a mature digital thread, AS9102 software consumes PMI-rich models via PLM or CAD integrations, creating structured characteristic records without manual re-interpretation of 2D views.

    Extracting Characteristics Directly from 3D Models

    As MBD adoption increases, the logical next step is for FAI tools to extract measurable requirements directly from 3D geometry and PMI. In practice, this looks like:

    • Loading a native CAD or neutral MBD format, then parsing PMI to identify all verifiable dimensions, GD&T frames, and notes.
    • Assigning unique characteristic IDs that map one-to-one to Form 3 rows and can be reused across builds, delta FAI, and future programs.
    • Providing 3D navigation from each characteristic to its associated feature, making it easier for inspectors and CMM programmers to understand intent.

    Compared with PDF-based ballooning, 3D extraction improves consistency and reduces interpretation errors, especially for complex structures and tight GD&T schemes. It also aligns FAI more closely with how CMM and metrology software already operate in many aerospace factories.

    Challenges in Transitioning from 2D-Centric Processes

    Moving FAI workflows from 2D drawings to MBD is not just a tooling change; it is an organizational shift. Common challenges include:

    • Mixed-revision environments: Some parts are fully MBD, others remain drawing-centric, and FAI teams must support both simultaneously.
    • Standards and customer expectations: Customers may still specify 2D drawing deliverables or have not formally approved model-based FAIRs as a primary reference.
    • Skills and training: Inspectors and quality engineers may be less comfortable navigating 3D PMI than reading traditional blueprints.

    A pragmatic approach is to run hybrid pilots: use MBD-derived characteristics as the internal source of truth but still generate AS9102-compliant forms and, where needed, drawing-based views for customer submission. Over time, as standards and customer practices evolve, organizations can phase out redundant 2D work.

    AI and Automation in FAI Data Analysis

    AI is often oversold as a push-button solution that will replace engineering judgment. In regulated aerospace manufacturing environments, that is neither realistic nor desirable. The more practical direction is AI and analytics augmenting human decision-making: guiding where to focus attention, checking FAIRs for inconsistencies, and surfacing patterns that would be hard to see manually.

    AI-Assisted Risk-Based Sampling Approaches

    Risk-based inspection is already established in aerospace quality systems; what changes is the data and tooling that inform those decisions. Emerging AS9102 software capabilities include:

    • Using historical FAIRs and in-process inspection results to estimate process capability for families of parts and operations.
    • Suggesting when 100% measurement is warranted (e.g., new suppliers, unstable processes, safety-critical characteristics) versus when statistically justified sampling is appropriate.
    • Highlighting characteristics with marginal capability or frequent near-miss conditions so engineers can tighten sampling or adjust control plans.

    Importantly, these AI-assisted recommendations should be transparent and overrideable. Quality leaders remain responsible for approving inspection strategies; the system provides context, not commands.

    Anomaly Detection in Measurement Data

    FAI results often sit in a repository until an audit or customer issue forces a review. Anomaly detection changes that by scanning results as they are recorded. Typical use cases include:

    • Flagging unusual distributions, such as one dimension consistently trending toward a tolerance limit across multiple builds.
    • Identifying inconsistent units, extreme outliers, or patterns that suggest transcription errors.
    • Surfacing systematic offsets that hint at fixture, probe, or program issues, before they propagate across a fleet of parts.

    Because AI models can misinterpret rare yet valid data, anomaly alerts should be reviewed by engineers who can confirm whether the pattern reflects a true process issue or expected variation. The value lies in earlier visibility, not automatic disposition.

    Automated Validation of FAIR Completeness and Consistency

    One of the most immediate AI-adjacent wins is rule-based and statistical validation of FAIRs before submission. Advanced AS9102 tools can:

    • Check that every ballooned or PMI-derived characteristic appears exactly once on Form 3.
    • Verify that material certs and special process records are attached for all relevant Form 2 entries.
    • Confirm unit consistency, tolerance format, and revision alignment across Forms 1, 2, and 3.

    Much of this can be implemented today with deterministic rules, complemented by AI models that learn typical patterns for a program or supplier and highlight deviations. The result is fewer customer rejections and less manual rework on incomplete FAIRs.

    FAI as a Node in the Aerospace Digital Thread

    Historically, FAI data stayed within the quality function. In a digital thread architecture, first article inspection becomes a key node linking design, process planning, production execution, and in-service performance. That shift turns FAIRs from static evidence into a rich source of engineering, sourcing, and operations intelligence.

    Connecting Design, Planning, Production, and In-Service Data

    In a connected aerospace manufacturing environment, AS9102 software does not operate alone. It exchanges data with PLM, MES, ERP, and maintenance information systems:

    • Design: PLM supplies the authoritative model or drawing, change history, and configuration rules.
    • Planning: Process plans and operation sequences flow from manufacturing engineering tools into the FAI context.
    • Production: MES links FAIRs to specific work orders, machines, tools, and operators.
    • In service: Maintenance and reliability systems can reference original FAI data when investigating recurring issues.

    When these connections are in place, the FAIR becomes a snapshot of how a particular configuration was realized at a moment in time, fully traceable back to design intent and forward to field performance.

    Using FAI Results to Refine Tolerances and Manufacturability

    First article results often reveal whether a design is realistically manufacturable with the intended processes and suppliers. By aggregating FAI data across parts and programs, engineering teams can:

    • Identify features that repeatedly push process capability limits or require excessive rework.
    • Highlight tolerances that are unnecessarily tight relative to functional needs.
    • Feed evidence-based feedback into design for manufacturability (DFM) guidelines and design standards.

    This turns FAI from a compliance gate into a feedback loop: design decisions are informed by past production reality, reducing ramp-up friction on future programs.

    Linking Certifications and Process Data to Maintenance Records

    For long-life aerospace platforms, the ability to trace from an in-service serial number back to its initial FAI and associated certifications is increasingly important. In a robust digital thread:

    • Each FAIR is indexed by part number, serial, lot, and configuration.
    • Material and special process records attached to Forms 1 and 2 are stored as structured data, not just PDFs on a shared drive.
    • Maintenance events in fleet management systems can link back to the original FAIR to investigate whether initial variability correlates with field performance.

    This level of linkage requires disciplined configuration management and common identifiers across systems, but it pays off in faster root-cause analysis and more targeted corrective actions.

    Supplier Collaboration and Real-Time Portals

    Aerospace primes are increasingly pushing digital requirements into their supply base: structured FAIRs, standard templates, and near-real-time visibility into inspection status. The future of digital FAI will depend as much on supplier collaboration as on internal factory systems.

    Shared FAIR Templates and Live Status Visibility

    Instead of each supplier maintaining its own spreadsheet templates, modern platforms provide shared, controlled AS9102 formats via secure portals. Capabilities typically include:

    • Prime-defined templates that enforce mandatory fields, revision usage, and customer-specific clauses.
    • Real-time visibility into FAIR status across suppliers: not started, in progress, submitted, under review, or approved.
    • Standardized data structures that make downstream analytics (e.g., across suppliers or commodity groups) feasible.

    This reduces interpretation errors and ensures that when data reaches the OEM, it is already compatible with their systems and reporting needs.

    Reducing Rework and Clarification Cycles with Primes

    Much of the delay and friction around FAI comes from back-and-forth clarification: missing attachments, ambiguous dimension coverage, or questions about process changes. Digital collaboration environments help by:

    • Embedding validation rules and checklists that suppliers must pass before submission.
    • Providing structured comment threads tied to specific characteristics or documents.
    • Maintaining a single source of truth for each FAIR, rather than multiple email chains and file versions.

    The outcome is fewer rejected FAIRs, more predictable lead times, and better use of both supplier and OEM engineering capacity.

    Security, IP Protection, and Access Control Considerations

    As more design and inspection data flows through shared portals, protecting intellectual property and regulated information becomes critical. Future-ready FAI platforms must support:

    • Granular access control down to part families, programs, or specific FAIRs.
    • Encryption in transit and at rest, with clear segregation between customers and suppliers.
    • Audit trails showing who accessed or modified data, when, and from where.

    Aerospace organizations should evaluate not only functional capabilities but also how FAI tools align with IT security policies, export control requirements, and customer data handling clauses.

    Preparing Your Organization for the Next Generation of FAI

    Transitioning to AI-enabled, MBD-driven FAI will not happen overnight. Organizations need to understand their current maturity, set realistic priorities, and align technology decisions with standards evolution and customer roadmaps.

    Assessing Current Digital Readiness

    A practical first step is a structured assessment of how FAI is executed today:

    • What proportion of FAIRs are created manually in spreadsheets versus via dedicated AS9102 software?
    • How frequently are 3D models with PMI available, and how are they used today?
    • Which systems hold critical FAI-related data (PLM, MES, ERP, QMS), and how well are they integrated?

    Documenting this baseline helps identify where digital upgrades will have the most immediate impact: reducing rework, shortening lead time, or improving audit readiness.

    Prioritizing Capabilities to Invest in First

    Not every organization needs cutting-edge AI on day one. For many aerospace manufacturers, the highest-value early investments are:

    • Reliable digital ballooning and characteristic extraction from drawings or models.
    • Structured AS9102 forms with built-in validation and revision control.
    • Centralized storage and search for FAIRs, certs, and supporting documents.

    Once those foundations are in place, teams can layer on analytics, anomaly detection, and deeper integration with MES and PLM. Attempting advanced capabilities without a stable data foundation usually leads to frustration.

    Building a Roadmap That Aligns with Standards Evolution

    AS9102, AS9100, and customer-specific requirements will continue to evolve as digital practices mature. A useful roadmap:

    • Maps target capabilities (e.g., MBD-based FAI, supplier portals, AI-assisted checks) against planned system upgrades and program milestones.
    • Identifies standards or customer guidance that may affect when certain practices are accepted (for example, model-based submissions).
    • Includes governance for how FAI processes are updated as standards or internal procedures change.

    The goal is to avoid one-off tool deployments and instead build a coherent, long-term path toward connected, data-centric FAI.

    Practical Steps to Experiment with Advanced FAI Capabilities

    Many aerospace teams want to explore advanced digital FAI but are constrained by active programs, existing contracts, and limited engineering bandwidth. Small, well-scoped pilots can prove value without disrupting ongoing delivery.

    Pilot Projects Using MBD-Derived Characteristics

    For programs where the design authority already maintains MBD, consider a pilot that:

    • Uses a limited set of parts to trial PMI-based characteristic extraction into the FAI system.
    • Compares time and error rates against traditional 2D ballooning.
    • Engages both design and quality teams to refine how PMI is structured for inspection use.

    Lessons from this pilot can inform modeling practices, internal standards, and supplier training before rolling out model-based FAI more broadly.

    Using Analytics on Existing FAIR Data

    Even without new measurement equipment or AI models, most organizations have years of FAIRs that are underutilized. A straightforward analytics initiative might:

    • Normalize existing FAIR data into a common structure, even if it began as spreadsheets.
    • Visualize where FAI rejections, late approvals, or near-miss dimensions cluster by part family, supplier, or process.
    • Feed those insights into process improvement projects or design guidelines.

    This kind of work builds the data literacy and governance needed before deploying more advanced anomaly detection or risk-based sampling algorithms.

    Partnering with Software Providers on Roadmap Features

    Given the pace of change around the digital thread and AI, no single vendor will have every capability fully mature today. Aerospace manufacturers can shape solutions by:

    • Participating in customer advisory boards focused on MBD, AS9102 Rev C interpretation, and supplier collaboration.
    • Co-designing pilot features such as AI-assisted FAIR checks or new integration points with PLM and MES.
    • Aligning contracts and deployment plans with clear milestones for advanced capabilities rather than generic promises.

    For platforms like Connect 981 that already embed FAI within a broader aerospace operations environment, this collaboration ensures that future enhancements match real engineering and production needs, not abstract technology trends.

    The trajectory is clear: FAI is moving from static documentation toward an integrated, data-rich capability that supports faster new part introduction, tighter process control, and more effective collaboration across the aerospace supply chain. Organizations that invest now in solid digital foundations—structured AS9102 data, integration with core systems, and disciplined configuration management—will be best positioned to take advantage of MBD and AI as they mature.