Category: Uncategorized

  • Designing an AS9102 Workflow: Best Practices from Planning to Submission

    Designing an AS9102 Workflow: Best Practices from Planning to Submission

    Designing an AS9102 Workflow: Best Practices from Planning to Submission

    Aerospace manufacturers, defense programs, and space hardware suppliers all depend on reliable first article inspection (FAI) to prove that new or changed production processes can consistently deliver conforming hardware. AS9102 defines the minimum requirements, but it does not tell your organization how to design the day-to-day workflow across engineering, quality, operations, and suppliers. That design choice determines whether FAIs move smoothly or become a recurring bottleneck.

    This article describes a practical end-to-end AS9102 workflow from planning through execution, review, and submission, and then shows how to standardize it across plants and suppliers using digital tools. It complements the broader perspective on digital article inspection in AS9102 software for digital first article inspection, focusing specifically on workflow design, roles, and governance.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Planning the AS9102 FAI

    A robust AS9102 workflow starts before any balloons are placed on a drawing. Planning clarifies when FAI is required, what will be inspected, and how responsibilities are divided across teams and organizations.

    Determining when FAI is required

    AS9102 specifies common triggers for FAI, but each aerospace organization must translate these into clear rules embedded in its quality management system (QMS) and production planning processes. Typical triggers include:

    • New part introduction to production or to a particular site or supplier.
    • Engineering changes that affect form, fit, or function.
    • Process changes such as new equipment, tooling, or manufacturing location.
    • Changes in material, source, or software that affect product characteristics.
    • Production lapses exceeding the time limit defined in your QMS or customer requirements.

    In a mature workflow, FAI triggers are not left to memory or tribal knowledge. Instead, they are encoded in planning rules inside ERP, MES, or an integrated quality platform so that a work order or configuration automatically indicates whether a full, partial, or delta FAI is required. That automation avoids missed FAIs and late discovery of requirements at shipment.

    Defining scope and classification of characteristics

    For each FAI event, the planning step must define the technical scope. This includes identifying the applicable configuration and deciding how to classify characteristics, such as:

    • Standard characteristics inspected according to drawing tolerances.
    • Key characteristics (KCs) that significantly affect performance, reliability, or manufacturability.
    • Critical characteristics (CCs) that relate directly to safety of flight or regulatory requirements.

    Classification drives the depth of evidence expected on Form 3, sampling plans, and the level of process capability analysis that may accompany the FAIR. In a digital workflow, these classifications should be stored as structured data, not handwritten notes, so that downstream inspection plans and dashboards can easily distinguish KCs and CCs across part families and programs.

    Coordinating with customers on expectations and formats

    Many primes and Tier 1 customers add program-specific requirements on top of AS9102, such as unique FAIR templates, additional traceability fields, or naming conventions. Effective FAI planning therefore includes explicit customer coordination:

    • Confirm whether the customer requires its own template or will accept your standard AS9102-compliant format.
    • Check if any additional evidence—such as capability studies, special process logs, or test data—must be bundled with the FAIR.
    • Align on submission method (portal upload, EDI, email) and review timelines.

    Digital systems can codify these expectations into customer-specific profiles so that each FAIR inherits the correct template and export format based on customer, part family, or contract.

    Preparing Drawings, Data, and Inputs

    Once an FAI is triggered and scoped, the next step is to ensure all technical inputs, documents, and digital structures are in place. Preparation quality strongly influences the cycle time and accuracy of the final FAIR.

    Ensuring correct drawing revision and configuration

    Configuration management is a critical risk area in aerospace production. Before ballooning or inspection planning begins, the team must verify that:

    • The drawing or model being used matches the configuration defined on the contract and work order.
    • All associated specifications and notes are at the correct revision level.
    • Digital systems consistently reference the same revision across PLM, ERP, MES, and FAI tools.

    In connected factories, this is handled by linking FAIRs directly to controlled configuration objects (e.g., engineering change orders or released models). The FAI workflow should prevent creation of a FAIR against an obsolete revision and should preserve traceability when a delta FAI is required after a design change.

    Gathering material, process, and certification requirements

    Beyond the drawing, AS9102 requires evidence that materials and special processes comply with design requirements. During preparation, the responsible engineer or planner should:

    • Identify all material specifications and associated certificates that must be captured on Form 2.
    • List all special processes (e.g., heat treatment, surface treatment, welding, NDT) and correlate them with internal or supplier process approvals.
    • Clarify which process outcomes (hardness, coating thickness, conductivity, etc.) must be recorded as results versus simply documented through certificates.

    Digital FAI tools can help by enforcing required attachments, linking process records and material lots to the FAIR, and flagging missing certifications before approval.

    Setting up digital templates and checklists

    Standardization begins at the template level. Rather than letting each engineer build FAIRs from blank forms or ad hoc spreadsheets, leading aerospace organizations maintain controlled digital templates and checklists that define:

    • Fields and structure of Forms 1, 2, and 3 in alignment with AS9102 Rev C.
    • Additional internal fields required by the QMS (e.g., internal routing numbers, process owner codes).
    • Checklist items for planning, including trigger confirmation, rev checks, and customer-specific expectations.

    Workflow-oriented platforms can automatically instantiate these templates based on part type, risk category, or customer. This reduces variability and accelerates training for new engineers or supplier quality teams.

    Executing the FAI

    Execution is where most effort and error risk concentrates: ballooning the drawing or model, capturing actual results, and managing issues discovered during inspection. A disciplined, digital-first workflow minimizes manual transcription and enforces characteristic accountability.

    Ballooning drawings and extracting characteristics

    The first visible step in execution is creating the ballooned drawing or model view. In a modern workflow, this should be done using software rather than manual markup.

    • Drawings (or 3D models with PMI) are imported into FAI software that identifies dimensions, GD&T, notes, and other inspection-relevant requirements.
    • Each requirement receives a unique balloon number, which becomes a persistent identifier for that characteristic.
    • Engineers review and validate detected characteristics, adding any overlooked notes or process-related requirements.

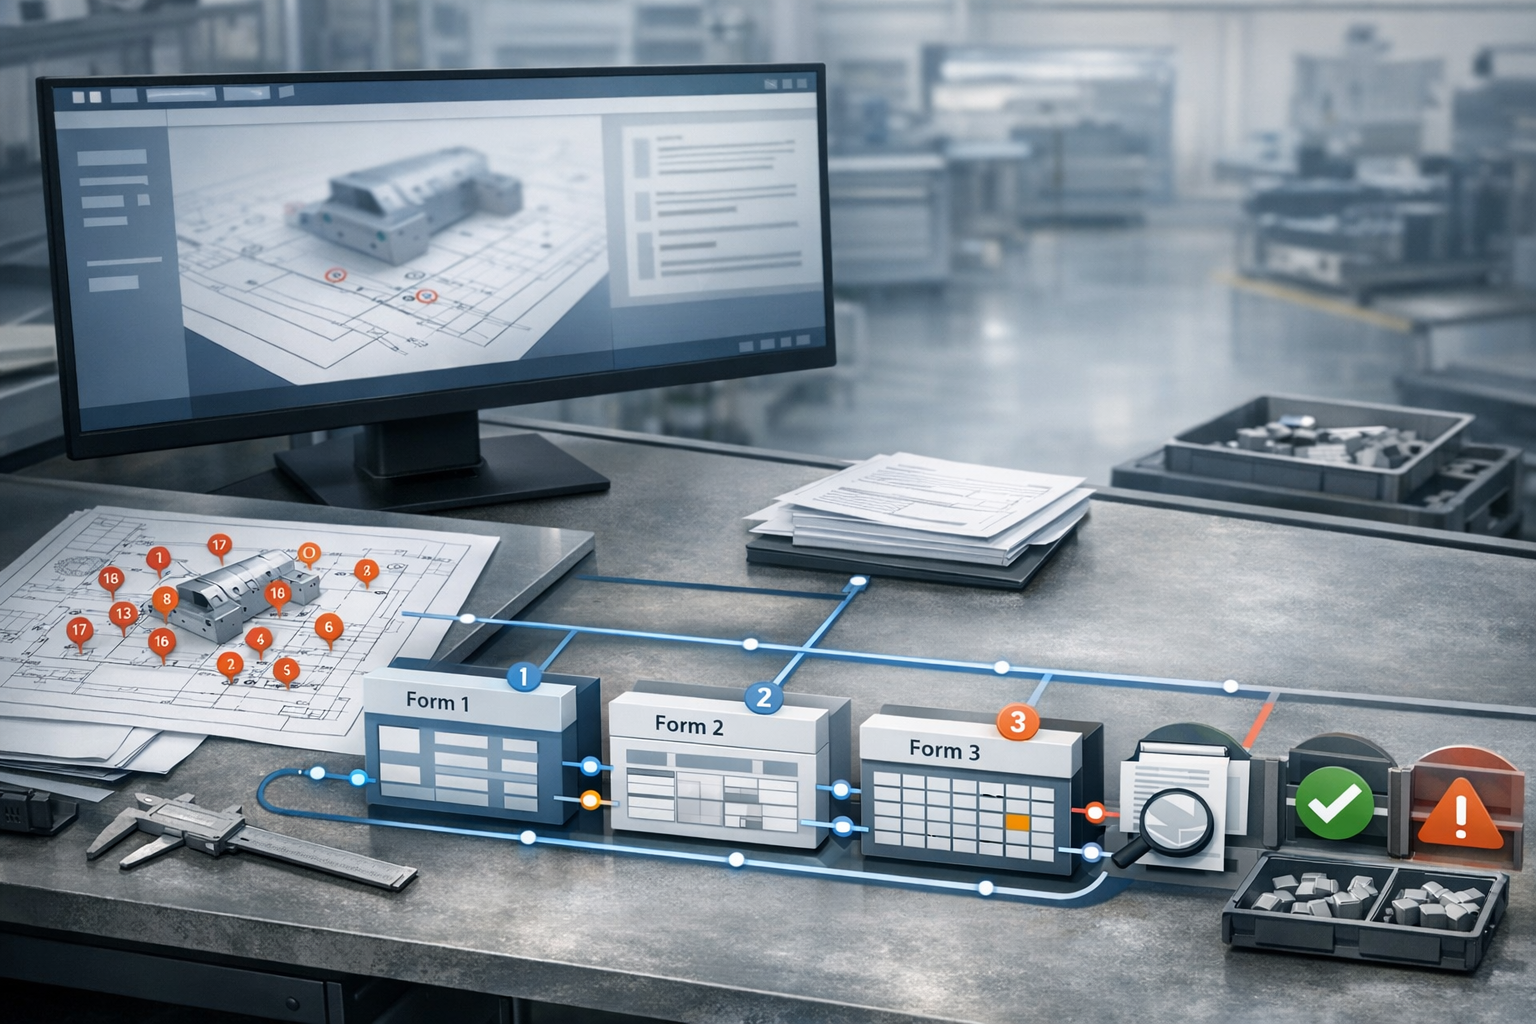
    The crucial principle is one characteristic, one balloon, one Form 3 line. This mapping is the backbone of traceability. Once balloons are confirmed, the system should auto-generate the Form 3 characteristic list and maintain a reliable link back to the visual representation.

    Collecting measurement and test data

    Next, inspection and test results are gathered for each characteristic. In an optimized AS9102 workflow, manual entry into spreadsheets is avoided wherever possible. Instead, organizations integrate multiple data sources:

    • CMM programs and other metrology systems that push results directly into the characteristic fields on Form 3.
    • Digital checklists or MES terminals used by operators to record in-process inspection measurements.
    • Laboratory test results (e.g., hardness, conductivity, tensile) imported as structured data and linked to the relevant balloons.

    Validation rules in the digital FAIR form help catch issues such as missing units, out-of-range values, or inconsistent decimal precision. When nonconformances are found, they should trigger formal nonconformance records, not just notes in the FAIR.

    Managing rework and nonconformances during FAI

    Inevitably, some FAIs uncover discrepancies. The workflow must define how to respond without losing traceability or compromising compliance.

    • Nonconformances are logged in the QMS with a clear link back to the specific characteristic and FAIR.
    • Rework is planned and executed through controlled work instructions, with repeat measurements recorded against the same balloon numbers.
    • If disposition decisions (e.g., use-as-is, repair, deviation) are required, these are documented in the QMS, while the FAIR records the final accepted result.

    The FAIR itself should not become a substitute for nonconformance or deviation processes. Instead, it acts as a structured summary of final, accepted results, with references to the supporting quality records.

    Review, Approval, and Submission

    Even well-executed inspections can fail if review and approval are inconsistent or poorly documented. AS9102 workflows should make these steps explicit, role-based, and digitally controlled.

    Internal review and quality signoff

    Before any FAIR is sent to a customer, an internal review ensures completeness and accuracy. Typical checks include:

    • Verification that all applicable characteristics are accounted for and correctly mapped.
    • Confirmation that Forms 1, 2, and 3 are coherent (e.g., part numbers, revisions, and serials match across forms).
    • Checks that required supporting documents—material certs, process logs, test reports—are attached and legible.

    Digital workflows can formalize these reviews using checklists, role-based tasks, and dashboards that highlight missing or inconsistent data. This reduces reliance on individual reviewer experience and improves consistency across sites.

    Electronic signatures and controlled approvals

    Many aerospace organizations operate in environments that require secure, auditable electronic signatures. A best-practice FAI workflow therefore includes:

    • Role-based approval routing (e.g., manufacturing engineering, quality engineering, quality manager).
    • Electronic signatures that are tied to individual user identities and time-stamped, with clear indication of which form or revision was approved.
    • Immutable audit logs that show who changed what and when between draft and approved FAIRs.

    This approach supports both AS9100 expectations and regulatory requirements, and it makes responding to customer or registrar questions significantly easier during audits.

    Submitting FAIRs and responding to customer feedback

    Submission is more than just sending a PDF. The workflow should clarify:

    • Submission channels (customer portal, secure file transfer, or integrated interfaces).
    • Required file formats (native digital format, PDF, data exchange formats) per customer or program.
    • Responsibilities for tracking status, recording customer approvals, and managing rejections or clarification requests.

    Digital platforms can track FAIR status across the supply chain—draft, submitted, under review, accepted, or rejected—giving program and quality leaders visibility into where FAI-related delays might affect deliveries.

    Standardizing Workflows Across Sites and Suppliers

    Designing a single robust AS9102 workflow is only the first step. The real challenge for aerospace companies is ensuring that the same principles are applied consistently across internal plants and external suppliers, without ignoring local constraints or customer-specific clauses.

    Common templates and process maps

    Standardization starts with a documented reference workflow and shared templates. Organizations often define:

    • A core process map that outlines planning, preparation, execution, review, and submission steps.
    • Standard digital templates for Forms 1–3 and for supporting checklists.
    • Risk-based variants of the workflow (e.g., enhanced review for critical parts or programs).

    These artifacts should be centrally controlled but configurable so that sites and suppliers can tailor fields or steps to satisfy local regulatory requirements or customer demands while still staying aligned with the corporate standard.

    Training and competency development

    Even the best-designed AS9102 workflow fails if engineers and inspectors do not fully understand the intent behind each step. Organizations should treat FAI as a core competency, not an occasional paperwork task, by:

    • Providing structured onboarding for new engineers and supplier quality staff on AS9102 concepts and internal workflow expectations.
    • Using real FAIR examples—including both strong and weak submissions—to illustrate acceptable practice.
    • Leveraging digital tools to embed guidance into forms themselves (tooltips, in-form examples, links to procedures).

    Competency assessment can be supported with periodic FAIR reviews, peer audits, or spot checks that focus on systemic understanding, not just form completion.

    Governance for changes to FAI procedures

    As AS9102 evolves and customers update their requirements, FAI workflows must adapt while preserving traceability. Governance mechanisms should include:

    • Formal change control for FAI procedures, templates, and digital workflows.
    • Impact assessment to determine which programs, sites, or suppliers are affected by a change.
    • Versioning of FAIR templates and associated instructions so that past FAIRs remain linked to the procedures in effect at the time.

    Digital workflow engines make it easier to implement these changes consistently and to document which FAIRs were built under each procedural version—critical evidence during audits or investigations.

    Embedding Continuous Improvement into the AS9102 Workflow

    FAI is often viewed as a compliance burden, but it also produces rich data about product design, process capability, and supplier performance. Organizations that treat FAI data as an improvement asset can reduce future defects and streamline new product introduction.

    Capturing lessons learned from each FAIR

    Each completed FAIR should feed a structured lessons-learned process. Typical topics include:

    • Characteristics that were consistently close to tolerance limits, indicating potential process capability concerns.
    • Design features that were difficult to inspect or that required complex setups.
    • Recurring issues with particular suppliers, processes, or materials.

    Digital platforms can capture these insights in a standardized way—through tags, structured comments, or dedicated review steps—and make them discoverable for future programs and engineering change assessments.

    Using metrics to refine workflows and training

    To understand the effectiveness of the AS9102 workflow, aerospace leaders should track quantitative metrics, such as:

    • Average cycle time from FAI trigger to customer-accepted FAIR.
    • Percentage of FAIRs rejected due to documentation or traceability issues.
    • Number of late deliveries where FAI delays were a contributing factor.
    • Frequency and impact of FAI-related audit findings.

    By analyzing these metrics across programs, sites, and suppliers, organizations can identify where training, template refinement, or additional automation will produce the highest return.

    Integrating FAI feedback with design and process engineering

    Finally, the AS9102 workflow should connect back into the broader digital thread of aerospace product development and manufacturing. Examples include:

    • Using FAI measurement data to inform design-for-manufacturability reviews and tolerance optimization.
    • Feeding recurring FAI issues into formal corrective action and process improvement projects.
    • Linking FAIRs to configuration-managed design and planning objects so engineering can see exactly how changes affected process capability.

    Platforms like Connect 981 position FAI as one node in a connected aerospace operations environment, rather than an isolated document. This perspective enables better decisions across engineering, production, and supplier management, while still respecting that each organization must tailor workflows to its own QMS and customer expectations.

    When designing or refining your AS9102 workflow, treat this reference model as a guide, not a rigid prescription. Align each step with your existing QMS, regulatory context, and contractual requirements, and use digital tools to enforce consistency, improve visibility, and capture the data needed for continuous improvement across your aerospace manufacturing network.
  • AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C Requirements: A Practical Guide for Aerospace Manufacturers

    AS9102 Rev C tightens expectations on how aerospace manufacturers plan, execute, and document First Article Inspection (FAI). For quality and manufacturing teams already under pressure, the update raises an important question: what exactly changed, and how do we comply in a practical, digital way without slowing programs down?

    This guide explains the AS9102 Rev C requirements, highlights key differences from Rev B, and shows how modern digital AS9102 software capabilities make day‑to‑day compliance manageable for OEMs and suppliers.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Overview of AS9102 Rev C and Its Purpose

    AS9102 is the international aerospace standard that defines how organizations plan, perform, and document first article inspections. It sits alongside AS9100 and IAQG guidance as the primary reference for verifying that production processes can reliably manufacture conforming parts.

    Why AS9102 Was Created and How It Supports AS9100 and Regulatory Expectations

    AS9102 was created to solve a persistent industry problem: inconsistent and incomplete first article inspection practices across the aerospace supply chain. Before AS9102, each customer tended to define its own FAI rules and templates, creating confusion and rework for suppliers.

    The standard provides:

    • Common definitions for FAI scope, terminology, and documentation.
    • Standardized forms (Forms 1, 2, and 3) to document part accountability, material and process verification, and characteristic results.
    • Minimum expectations for traceability from design data (drawings, models, specifications) to inspection evidence.

    AS9102 supports AS9100 by providing objective evidence that the production process has been validated. It also aligns with FAA, EASA, and other airworthiness regulators by demonstrating that initial and changed configurations are thoroughly verified before rate production.

    Timeline of Revisions From Original Release to Rev C

    AS9102 has evolved as follows:

    • AS9102 (original release, 2004-era): Established the core concepts of FAI and the three standard forms.
    • AS9102B (around 2009–2014 adoption window): Emphasized FAI planning and clarified expectations around documentation and re-accomplishment.
    • AS9102C (Rev C, most recent): Focuses heavily on clarity for digital implementations, improved handling of partial and delta FAI, and better alignment with modern aerospace configuration and data-management practices.

    For many organizations, Rev C has been the catalyst to move away from manual, spreadsheet-driven FAIRs and invest in digital solutions that can consistently interpret and enforce the updated requirements.

    Who AS9102 Rev C Applies To in the Aerospace Supply Chain

    AS9102 Rev C applies when it is invoked by contract, purchase order, or quality clause. Typically, it affects:

    • OEMs and airframe manufacturers who must demonstrate configuration and process validation for new and changed parts.
    • Tier 1 and Tier 2 suppliers who deliver flight-critical structures, engine components, avionics hardware, interiors, and other aerospace products requiring FAI.
    • Special process providers whose outputs (heat treatment, NDT, plating, coatings) are essential to meeting drawing requirements documented on Form 2 and Form 3.

    AS9102 itself is not a regulation; it is a standard. However, once a customer or prime specifies AS9102 Rev C, compliance becomes a contractual requirement and is often sampled during AS9100 and customer audits.

    Core Requirements of AS9102 Rev C

    AS9102 Rev C defines when an FAI is required, how to categorize it (full, partial, delta), and what information must be present on Forms 1, 2, and 3 to show complete characteristic accountability and traceability.

    Full, Partial, and Delta FAI Definitions and Applicability

    Under Rev C, FAI categories are more explicitly defined to match real-world change scenarios:

    • Full FAI
      • Required for a new part number or when otherwise specified by the customer.
      • Covers all design characteristics and requirements shown on the applicable drawing or model, including notes, GD&T, and special requirements.
      • Generates a complete FAIR package (Forms 1–3 plus supporting evidence).
    • Partial FAI
      • Used when only a subset of characteristics or operations need to be re-verified.
      • Often triggered by a change in manufacturing process, location, tooling, or equipment where design data is unchanged.
      • Documented clearly as a partial FAI on Form 1, with traceability to the baseline full FAI.
    • Delta FAI
      • Used when an engineering or design change affects only certain characteristics.
      • Focuses on characteristics impacted by the design change, while referencing the baseline FAI for unchanged features.
      • Requires clear identification of revised design data and affected characteristics.

    Rev C expects organizations to classify FAI correctly and to maintain traceable linkage between full, partial, and delta FAI so that the product’s verification history is transparent.

    Mandatory Data Elements for Forms 1, 2, and 3

    AS9102 Rev C retains the three-form structure but clarifies what must be captured on each form. While the standard’s exact field layout is copyrighted, you must ensure the following types of information are present and complete.

    Form 1 – Part Number Accountability typically includes:

    • Part number, name, and configuration (revision, issue, or version).
    • FAI status (full, partial, delta) with cross-reference to the baseline FAIR when applicable.
    • Serial number(s) or lot/batch identification for the first article units.
    • Customer and internal references (PO, job/traveler, work order, etc.).
    • Signatures, dates, and organization information for those who prepared and approved the FAIR.

    Form 2 – Product Accountability focuses on:

    • Materials used, including specification, type, and lot or heat numbers.
    • Special processes such as heat treatment, NDT, welding, plating, coating, and surface treatments.
    • Functional tests and performance verifications where results are pass/fail rather than dimensional.
    • References to certifications, test reports, and process records (e.g., certificates of conformity, NADCAP approvals).

    Form 3 – Characteristic Accountability, Verification Results, and Compatibility Evaluation documents:

    • Each ballooned characteristic with a unique identifier/sequence number.
    • Design requirement (nominal, tolerance, GD&T callout, or note description).
    • Actual measured results or verification outcome.
    • Acceptance status and compatibility evaluation where applicable.
    • Links to the measurement method, inspection equipment, or CMM program as needed.

    Rev C emphasizes that all applicable characteristics—including dimensions, notes, and special requirements—must appear on Form 3 so there is no ambiguity about what has been verified.

    Requirements for Characteristic Accountability and Traceability

    Characteristic accountability is the backbone of AS9102. Rev C expects you to demonstrate that every requirement in the design data has been identified, numbered, and verified with a clear record.

    Practically, this means:

    • Each drawing or model requirement is assigned a unique balloon number or similar identifier.
    • That identifier is used as the sequence number on Form 3, creating one-to-one mapping between the drawing and FAIR.
    • Measurement results, pass/fail decisions, and notes are recorded under the same identifier so anyone can trace from drawing to data and back.
    • Special processes and materials that support a given characteristic are traceable via Form 2 and attached certifications.

    Rev C strengthens the expectation that traceability must include configuration control. FAIRs must be tied to a specific drawing or model revision, and later delta/partial FAIs must clearly reference prior FAIRs and the changes that triggered them.

    AS9102 Rev B vs Rev C: Key Changes

    Organizations moving from Rev B to Rev C often underestimate the impact of the new revision. Much of the terminology is familiar, but Rev C clarifies intent, tightens definitions, and explicitly anticipates digital execution.

    Clarifications Introduced for Digital Implementations

    Rev C was written against the backdrop of widespread digital FAI tools rather than paper and spreadsheets. Some key clarifications include:

    • Improved guidance on linking digital drawings/models to Forms 1–3, ensuring the configuration of the data source is clear.
    • Recognition that digital signatures and electronic approvals can meet the standard as long as they are controlled and traceable.
    • Expectations for consistent handling of multi-sheet drawings and multi-configuration parts in digital systems.
    • Clearer distinction between the FAI process and the FAIR (report), which is important when using automated data flows.

    These clarifications are not optional; they drive how digital solutions must behave to be considered aligned with Rev C.

    Changes to Partial and Delta FAI Handling

    Under Rev B, organizations frequently struggled with when and how to perform partial or delta FAI. Rev C addresses this by:

    • More explicitly defining triggers for partial vs delta (manufacturing/process vs design/engineering driven).
    • Reinforcing that partial and delta FAI must still maintain traceable linkage to the baseline full FAI.
    • Emphasizing that only affected characteristics are re-verified, but documentation must clearly state what changed and why.

    Done correctly, Rev C’s structure reduces unnecessary rework while still satisfying customer and regulatory expectations.

    New or Reworded Fields and Expectations on the Forms

    Rev C introduces reworded field descriptions and some additional expectations on how certain information is captured, for example:

    • More precise language around FAI status (full, partial, delta) and its indication on Form 1.
    • Clearer guidance on recording design data references (drawing/model numbers, revisions, specification references).
    • More consistent terminology for compatibility evaluations and special characteristics.

    Digital tools should be configured to reflect these Rev C expectations in field labels, required fields, and validation rules, even if the underlying data model is similar to what you used under Rev B.

    Practical Triggers for AS9102 FAI Under Rev C

    Knowing the theory is only half the story. Day-to-day, teams need a clear understanding of when Rev C expects a new FAI activity.

    Design and Engineering Change Scenarios

    Engineering changes that typically trigger full or delta FAI under Rev C include:

    • New part introduction (new part number or first time build at your site).
    • Changes that affect form, fit, function, reliability, or safety.
    • Drawing or model revision that adds, deletes, or significantly changes key features.
    • Tightening or relaxing tolerances on critical dimensions.
    • New material specifications or design notes that drive new verification activities.

    Most of these are handled via delta FAI, provided you can show clear traceability to prior FAIRs and focus only on affected characteristics.

    Process, Material, and Supplier Changes

    Process-oriented changes typically trigger partial FAI. Common examples include:

    • Moving production to a new machine, cell, or facility.
    • Changing the manufacturing route (e.g., switching from one machining sequence to another).
    • Introducing new tooling or fixtures that could affect dimensions.
    • Changing a sub-tier supplier for raw material, castings/forgings, or critical processes.
    • Modifying process parameters for special processes (e.g., new heat treat cycle, new NDT technique).

    Rev C expects organizations to have documented criteria—often in their QMS—for when such changes trigger partial FAI, and to demonstrate that the partial scope correctly corresponds to the impacted characteristics.

    Lapse in Production and Customer-Specific Triggers

    Another key trigger is lapse in production. If a part has not been produced for an extended period (commonly two years, but some customers specify different thresholds), Rev C expects you to reassess whether FAI is required. Many organizations treat this as a partial FAI unless design or process changes require more.

    Customer-specific triggers may include:

    • FAI required for every lot or every nth lot for high-risk parts.
    • FAI required when internal yield or defect trends exceed thresholds.
    • FAI mandated when a supplier changes certain sub-tiers, even if design and process remain stable.

    AS9102 Rev C sets the baseline; purchase orders and customer quality clauses can add stricter conditions, and these must be interpreted alongside the standard.

    How Digital AS9102 Software Supports Rev C Compliance

    Trying to meet Rev C requirements with manual ballooning and spreadsheets is possible for simple parts, but it becomes risky and inefficient at aerospace scale. Modern AS9102 software is designed specifically to satisfy Rev C expectations while reducing cycle time and error rates.

    Configuring Templates and Fields to Match the Rev C Standard

    A robust digital solution lets you:

    • Configure Form 1, 2, and 3 templates to align with Rev C’s required data elements and field definitions.
    • Define mandatory fields and validation rules (e.g., FAI type required, drawing revision cannot be blank, serial numbers must match work orders).
    • Standardize customer-specific layouts on top of a single, controlled data model.

    This configuration step is critical to applying Rev C consistently across sites and suppliers.

    Automated Checks to Prevent Common Nonconformances

    AS9102 software can embed rule-based and automated checks such as:

    • Verifying that every ballooned characteristic on the drawing has a corresponding entry on Form 3.
    • Ensuring that FAI type (full/partial/delta) and baseline references are populated correctly on Form 1.
    • Blocking approval if there are missing certificates for materials and processes referenced on Form 2.
    • Highlighting inconsistencies between drawing revision, work order, and FAIR configuration.

    These checks greatly reduce the risk of FAIR rejection by customers or findings during audits.

    Managing Revisions, Partial, and Delta FAI in Software

    Effective digital tools provide structured support for Rev C’s FAI types:

    • Full FAI: Create a baseline FAIR that captures all characteristics and associated evidence.
    • Partial FAI: Clone the baseline FAIR, restrict the scope to impacted operations/characteristics, and record the partial status on Form 1.
    • Delta FAI: Compare new and prior design data to identify affected characteristics, generate a focused Form 3 subset, and clearly reference prior FAIRs.

    Advanced systems can even visualize FAI lineage as a tree, showing which FAIRs are related to which design or process changes. This directly supports Rev C’s intent for transparent traceability.

    Implementation Checklist for AS9102 Rev C

    Moving to Rev C is not just a documentation update. It touches procedures, training, systems, and supplier expectations. The following checklist can guide implementation.

    Gap Analysis From Current Practices to Rev C Requirements

    Start by assessing your current state:

    • Review quality procedures and work instructions against Rev C clauses.
    • Audit sample FAIRs to check for complete characteristic accountability and clear FAI type identification.
    • Evaluate whether partial/delta FAI usage matches Rev C definitions and triggers.
    • Identify where manual workarounds (e.g., untracked spreadsheet columns) are substituting for systematic controls.

    Document gaps and prioritize remediation based on risk, customer expectations, and audit feedback.

    Training, Work Instructions, and System Updates

    Next, update the human and procedural side:

    • Revise FAI procedures to reference AS9102 Rev C explicitly, including FAI triggers and FAI type definitions.
    • Update work instructions for quality engineers, inspectors, and manufacturing engineers, including clear guidance on how to classify and document FAI.
    • Deliver role-specific training that focuses on practical scenarios rather than just standard text.
    • Adjust your AS9102 software configuration (forms, validations, workflows) to reflect Rev C requirements and any customer-specific overlays.

    The goal is that anyone involved in FAI can recognize when Rev C applies and how to execute it consistently in your chosen digital environment.

    Ongoing Monitoring and Audit Readiness Under Rev C

    Once Rev C is in place, you need continuous assurance that it is being followed:

    • Periodically sample FAIRs for completeness, characteristic coverage, and alignment with design changes.
    • Track FAIR rejection rates by customer and cause to identify systemic issues.
    • Prepare for audits by ensuring FAIRs, supporting documents, and change histories are searchable and retrievable within minutes.
    • Leverage digital dashboards, where available, to monitor open FAIRs, overdue approvals, and FAI bottlenecks.

    Rev C does not require perfection, but it does expect a controlled, repeatable process with objective evidence to back it up.

    Where AS9102 Rev C Fits in a Digital FAI Strategy

    FAI should not be handled as a stand-alone, tactical task. Under Rev C, it is increasingly viewed as part of a broader digital aerospace operations strategy—one that connects design, planning, execution, and quality.

    For a deeper look at how ballooning, Forms 1–3, workflows, and supplier collaboration come together in software, see the hub guide on AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

    By aligning your procedures, training, and AS9102 software with Rev C requirements, you reduce FAIR rejections, protect program schedules, and strengthen your position with OEMs and regulators—while turning FAI data into a reusable asset rather than a one-time deliverable.

  • Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    Digital FAIR Forms and Ballooned Drawings: Automating AS9102 FAI

    For most aerospace manufacturers, the slowest and most error-prone part of AS9102 first article inspection (FAI) is not the measurements themselves. It is turning complex drawings into ballooned characteristics and then mapping every requirement into Forms 1, 2, and 3. Digital FAIR forms and automated ballooned drawings target this exact bottleneck, replacing hand-marked prints and Excel templates with a structured, reviewable, and reusable data model.

    This article explains how modern tools automate ballooned drawings, populate AS9102 forms, and maintain one-to-one traceability between every drawing requirement and every Form 3 line. It also shows how digital FAIRs support partial and delta FAI, integrate measurement data, and create a foundation for long-term traceability.

    For teams putting this topic into daily operation, Connect 981’s aerospace execution solutions, real aerospace execution examples, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you need a broader overview of how these capabilities fit into a full platform, see our AS9102 software overview.

    Why Ballooned Drawings and FAIR Forms Are Central to AS9102

    AS9102 revolves around a simple idea: every requirement in the design must be clearly identified, measured, and documented. Ballooned drawings and FAIR forms are how that happens in practice.

    The role of ballooned drawings in capturing every requirement

    A ballooned drawing is a drawing where every verifiable requirement is given a unique identifier (a “balloon” number). This typically includes:

    • Dimensions and tolerances (linear, angular, diameters, radii, etc.)
    • GD&T callouts (position, flatness, perpendicularity, profile, and others)
    • Surface finish requirements
    • Drawing notes that imply verification (e.g., “NO SHARP EDGES”, “DEBURR ALL EDGES”)
    • Material specifications and heat-treat conditions
    • Coatings and other special processes that must be verified

    Each balloon creates a discrete, traceable “characteristic” that should appear on Form 3. When ballooning is incomplete or inconsistent, characteristic accountability breaks down and AS9102 expectations are not met.

    How Forms 1, 2, and 3 relate to the drawing

    AS9102 Rev C structures the FAIR into three core forms:

    • Form 1 – Part Number Accountability: Identifies the part, configuration, and whether the FAIR is full, partial, or delta.
    • Form 2 – Product Accountability: Lists materials, special processes, and functional tests with traceable documentation.
    • Form 3 – Characteristic Accountability: Maps every ballooned characteristic to measured or verified results and compatibility evaluations.

    The ballooned drawing drives Form 3. Each balloon ID should correspond to exactly one Form 3 line, which then references the same part and revision context defined in Form 1 and the associated materials and processes summarized in Form 2.

    Common failure modes in manual FAIR creation

    Manual FAI processes typically involve printing drawings, marking balloons with a pen, and populating Excel-based forms. This approach is familiar but fragile. Common problems include:

    • Missed or duplicated balloons: Critical dimensions can be skipped entirely or numbered twice, resulting in gaps or conflicts in Form 3.
    • Mismatch between drawing and forms: Balloon numbering on paper does not match line numbering in Excel, making reviews and audits difficult.
    • Incorrect tolerance or unit interpretation: Values are re-typed manually, increasing the chance of misreading, rounding, or unit mix-ups.
    • Weak revision control: FAIRs are completed against one drawing revision while a newer revision is already in effect, but there is no systematic link.
    • Heavy reliance on tribal knowledge: Only a few experts know how to balloon in the “right way” or which Excel template applies to which customer.

    Digital FAIR tools focus on eliminating these failure modes by treating ballooning and forms as connected, governed data rather than as disconnected documents.

    How Digital Tools Automate Ballooned Drawings

    Digital ballooning is the starting point for any modern AS9102 workflow. Instead of manually adding balloons on paper, engineers work with digital drawings and software that recognizes and structures characteristics.

    Importing PDF and CAD-derived drawings

    Most FAI scenarios still rely on 2D drawings, even when the design originates from a 3D CAD model. Effective digital ballooning starts with robust import:

    • PDF drawing import: The system ingests released PDF drawings directly from PLM or document control, preserving scaling and clarity.
    • CAD-derived drawings: For organizations using model-based workflows, tools may import 2D drawings generated from the 3D model or access published views that carry product manufacturing information (PMI).
    • Config-controlled access: The ballooning tool should clearly display the drawing revision and ensure the FAIR is always linked to the correct configuration.

    By anchoring ballooning to controlled source files, the risk of using outdated prints is dramatically reduced.

    Automated detection of dimensions, GD&T, and notes

    Once drawings are imported, modern tools use OCR and pattern recognition to identify potential characteristics:

    • Dimension values and tolerances are recognized and tagged as measurement-required characteristics.
    • GD&T frames are captured as separate, structured items with their respective datum references.
    • Notes that imply verification — such as specific finishing, cleanliness, or edge conditions — can be flagged for inclusion.

    Engineers can then review a first-pass extraction rather than ballooning everything from scratch. It is important to view this as assisted extraction, not guaranteed perfection: the software accelerates identification, but quality engineers still verify and adjust the characteristic set before release.

    Managing multi-sheet aerospace drawings and numbering

    Aerospace parts frequently require multi-sheet drawings with multiple views, detail callouts, and separate notes pages. Digital tools must handle this complexity while preserving clarity:

    • Consistent numbering across sheets: Balloon numbers remain unique across all sheets, even when a characteristic is referenced on multiple views.
    • Clear sheet and view references: Each characteristic record includes sheet number, view, and zone (if used) to make later reviews straightforward.
    • Filters for visibility: Users can filter characteristics by sheet, view, or type (dimension, note, GD&T) to simplify large FAIs.

    The outcome is a digital ballooned package where every requirement is visible, numbered, and traceable without the clutter and ambiguity of paper markups.

    Designing Effective Digital FAIR Forms

    Ballooned drawings create the characteristic structure. Digital FAIR forms turn that structure into an AS9102-compliant report that can be submitted, revised, and audited.

    Structuring Forms 1, 2, and 3 for AS9102 Rev C

    Digital FAIR tools should mirror the intent and fields of AS9102 Rev C while still being flexible enough to support customer-specific needs. Good practice includes:

    • Form 1: Controlled fields for part/assembly number, name, revision, FAIR type (full, partial, delta), and reference documents.
    • Form 2: Structured rows for materials, special processes, and functional tests, with clear linkage to certificates, NADCAP scopes, or lab reports.
    • Form 3: One row per characteristic with reference to drawing location, requirement, measured result, units, tolerance, and acceptance status.

    The software should treat these as data-backed forms rather than static templates, enabling calculated fields, consistent formatting, and robust reporting.

    Validation rules that prevent missing or inconsistent data

    One of the central advantages of digital FAIRs over spreadsheets is the ability to enforce rules that catch issues before submission. Examples include:

    • Mandatory completion of key Form 1 fields (part number, revision, FAIR type, FAI status).
    • Automatic warnings if a ballooned characteristic does not have a corresponding Form 3 entry.
    • Checks for unit consistency (e.g., preventing inches and millimeters from being mixed for the same characteristic without explicit conversion).
    • Flags when measurement results appear outside the declared tolerance range, prompting review.

    Instead of discovering issues during customer review, engineers see them while the FAIR is still in preparation.

    Prime-specific formats vs a unified data model

    Many aerospace suppliers must support different AS9102 formats or overlays requested by primes such as Boeing or Airbus. Manually maintaining separate Excel templates quickly becomes unmanageable. Digital FAIR tools should:

    • Maintain a single underlying data model that captures all required AS9102 fields.
    • Allow configurable output layouts — for example, one export tailored to a specific customer’s format and another using a standard AS9102 Rev C layout.
    • Ensure that regardless of the output style, the same governed data set underpins every FAIR.

    This approach avoids having multiple “sources of truth” while still meeting customer-specific presentation requirements.

    Ensuring One-to-One Characteristic Accountability

    Characteristic accountability is the core of AS9102: for each requirement, there is a clear, auditable link from drawing to measured result. Digital tooling makes this explicit and enforceable.

    Mapping each balloon to a unique Form 3 row

    In a well-designed system, the characteristic list created during ballooning is the same list used to populate Form 3. Key behaviors include:

    • Each balloon ID is represented once and only once on Form 3.
    • Characteristics cannot be deleted from Form 3 without equivalent change in the ballooned set, maintaining alignment.
    • Renumbering or re-grouping balloons (for example, after engineering review) automatically updates the associated Form 3 lines.

    This eliminates the common manual error of mismatched numbering between drawings and forms.

    Flagging key and critical characteristics in the data model

    Key characteristics (KCs) and critical characteristics (CCs) drive additional scrutiny and may require enhanced sampling or control plans. Digital FAIRs should support:

    • Flags on each characteristic indicating whether it is a KC, CC, or other special category as defined by the prime or internal procedures.
    • Rules that require additional documentation (e.g., process capability studies) or approvals before a FAIR with CCs can be fully released.
    • The ability to report and trend KCs and CCs across multiple FAIRs, lots, or suppliers.

    When these flags live in a structured data model instead of free-text notes, quality teams can reliably filter, monitor, and report on safety-critical items.

    Bidirectional navigation between drawing and form

    One of the most tangible usability benefits of digital FAIRs is the ability to navigate between the ballooned drawing and Form 3:

    • Clicking on a Form 3 row highlights the associated balloon on the drawing and brings it into view.
    • Selecting a balloon on the drawing jumps directly to the corresponding Form 3 line.
    • Filters and search on either side stay in sync, making internal reviews and customer discussions much faster.

    This bidirectional link reduces ambiguity and helps reviewers focus on the real question: whether the product meets requirements, not whether the documentation can be interpreted.

    Integrating Measurement Data into Digital FAIRs

    Once the characteristic structure is in place, the next challenge is getting accurate measurement and verification data into Form 3 efficiently and correctly.

    Capturing manual measurements accurately

    Many FAIs still involve manual measurements taken with calipers, micrometers, height gages, or simple gauges. Digital FAIR tools should support:

    • Guided data entry forms that show the requirement, nominal, and tolerance alongside an input field for the actual result.
    • On-the-spot validation to catch obvious mis-keys (e.g., a value an order of magnitude off expected nominal).
    • Direct association of who measured, when, and with which instrument, if required by internal or customer procedures.

    The goal is to eliminate re-keying from handwritten sheets into Excel and instead have measurement data recorded once, in the system of record.

    Importing CMM and other automated inspection data

    For complex components, automated inspection systems (CMMs, vision systems, laser scanners) often generate result files in standardized formats. A mature digital FAIR workflow:

    • Maps result file feature IDs to Form 3 characteristic IDs, ensuring that data flows to the correct line.
    • Handles multiple runs or samples, summarizing results as required by the AS9102 form while retaining detailed data behind the scenes.
    • Allows selective review, so engineers can quickly focus on out-of-tolerance or near-limit conditions.

    This tight linkage between inspection systems and FAIRs removes transcription errors and accelerates report completion.

    Handling units, tolerances, and compatibility evaluations

    AS9102 Form 3 requires more than just recording numbers. It also demands a clear compatibility evaluation that confirms whether the characteristic is acceptable. Digital FAIR tools help by:

    • Standardizing units and enforcing conversions where needed, so a drawing in inches and a CMM report in millimeters remain consistent.
    • Structuring tolerance formats (e.g., bilateral, unilateral, limit) so calculations can be automated and consistently interpreted.
    • Providing explicit fields where engineers record compatibility or attach supporting notes for borderline cases.

    Instead of interpreting free-text comments during an audit, reviewers see structured results together with a clear pass/fail or compatible/not compatible conclusion.

    Reuse and Change Management with Digital FAIR Structures

    AS9102 Rev C recognizes that not every event requires a completely new, full FAIR. Digital FAIR structures make it practical to reuse characteristic sets and manage partial or delta FAI without losing traceability.

    Reusing balloon and characteristic structures across builds

    Once a part number has been fully ballooned and its characteristics validated, that structure becomes a reusable asset:

    • New FAIRs for repeat builds can leverage the same ballooning, avoiding repeated engineering effort.
    • Suppliers or additional plants can inherit an approved characteristic set, reducing variation in interpretation.
    • Updates to the drawing trigger incremental reviews instead of new ballooning from scratch.

    This reuse is only safe if revision control is handled carefully, which is where digital tooling excels compared to file-based workflows.

    Supporting partial and delta FAI without recreating forms

    Partial and delta FAIs are often the most confusing for teams using spreadsheets. Digital FAIR tools can make them routine by:

    • Allowing Form 1 to explicitly flag FAIR type (full, partial, delta) as required by AS9102 Rev C.
    • Duplicating the baseline FAIR structure and then highlighting only those characteristics that must be re-verified.
    • Maintaining a link back to the original FAIR so reviewers see the complete history at a glance.

    Instead of building a new spreadsheet for every change, teams extend a controlled data set and capture exactly what has changed and why.

    Maintaining traceability across revisions and submissions

    Traceability in digital FAI spans more than just drawing revisions:

    • Each FAIR is linked to the drawing revision, associated change notices, and the specific production lot or serial numbers inspected.
    • Subsequent FAIRs (for example, after a process move or design modification) explicitly reference the earlier baseline FAIR.
    • Systems can provide a “family tree” of FAIRs showing how the part has evolved and when verification was repeated.

    This level of traceability is extremely difficult to maintain using independent Excel files stored on shared drives. Digital FAIR tools make it a natural byproduct of everyday work.

    How Digital FAIRs Fit into a Broader AS9102 Software Strategy

    Digital FAIR forms and ballooned drawings are the engine of AS9102 documentation, but they rarely live in isolation. When they are integrated into a broader AS9102 software approach, organizations gain:

    • Automatic population of part, revision, and purchase order data from ERP or PLM.
    • Alignment of FAIRs with shop-floor execution, work instructions, and quality checks.
    • Centralized storage and search for all FAIRs, measurement results, and supporting documents.

    To understand how these elements span planning, execution, and audit readiness, it is useful to step back and review an AS9102 software overview that covers workflow orchestration, integration, and analytics on top of the digital FAIR foundation.

    Practical Steps to Implement Digital FAIR Forms and Ballooned Drawings

    Organizations moving from manual to digital FAI can take a phased approach focused on risk reduction and quick wins.

    1. Start with high-impact parts: Select parts with complex drawings, high characteristic counts, or a history of FAIR rework.
    2. Digitize ballooning: Implement automated ballooning for those parts, validating extraction rules and review practices.
    3. Standardize AS9102 forms: Configure Forms 1, 2, and 3 templates aligned with Rev C and major customer overlays.
    4. Integrate measurement data: Pilot CMM and manual data capture flows for a subset of characteristics.
    5. Introduce partial/delta FAI logic: Once the baseline FAIR is stable, use the same structure to manage engineering changes.

    By proving value on a manageable scope first, teams build confidence and templates that can scale across programs, sites, and suppliers.

    Conclusion

    Digital FAIR forms and automated ballooned drawings transform AS9102 FAI from a manual document-creation activity into a governed, reusable data process. By automating characteristic extraction, enforcing one-to-one mapping between balloons and Form 3, and integrating measurement data, quality and manufacturing teams can reduce cycle time, lower error rates, and strengthen traceability.

    When these capabilities are connected to broader AS9102 software workflows, they become a foundation for aerospace compliance, audit readiness, and continuous improvement. The practical next step is to identify where manual ballooning and spreadsheet-based FAIRs are causing the most pain, and then pilot a digital FAIR approach that directly addresses those bottlenecks.

  • Partial vs Delta FAI in AS9102 Software: Practical Digital Strategies

    Partial vs Delta FAI in AS9102 Software: Practical Digital Strategies

    Under AS9102 Rev C, you no longer have to choose between re-doing an entire first article inspection or risking gaps in coverage when designs or processes change. Partial and delta FAI give aerospace manufacturers a structured way to verify only what has actually changed—provided you can manage the details correctly.

    This article explains how full, partial, and delta FAI relate to each other, where organizations struggle when managing them manually, and how modern AS9102 software can automate reuse, lineage, and impact analysis. The perspective here reflects common industry practice, not a legal interpretation of the standard, and final scope decisions must always follow customer and regulatory requirements.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you need a broader overview of digital AS9102 and FAIR workflows before diving into change scenarios, see our guide on AS9102 and digital FAI fundamentals.

    Definitions: Full, Partial, and Delta FAI Under AS9102 Rev C

    AS9102 Rev C clarifies terminology so suppliers and customers can distinguish between a brand-new verification and targeted re-verification when things change.

    When a full FAI is mandatory

    In practice, organizations treat a full FAI as the baseline reference FAIR for a given part configuration. Typical triggers include:

    • New part introduction – First production run of a new part number for a site or supplier.
    • Major design changes impacting form, fit, or function – For example, a new rib structure on a wing component or a significant geometry change on a turbine blade.
    • New manufacturing source – Moving production to a different supplier or facility when the customer requires full re-validation.
    • Extended production lapse – When no parts have been produced for an extended period (often around two years, but this can be customer-specific).

    Under a full FAI, every characteristic on the drawing and applicable specifications must be ballooned and accounted for on Form 3, with supporting material and process evidence on Forms 1 and 2.

    Typical triggers for partial FAI

    Partial FAI is used when only selected characteristics require re-verification, usually because the manufacturing process has changed while the design itself has not. Common triggers include:

    • Process or operation changes – A drilling or milling operation is moved to a different machine, cell, or facility.
    • Tooling or fixture changes – New cutting tools, workholding, or gaging that could affect particular dimensions.
    • Supplier or sub-tier changes for specific operations – For example, moving a plating step to a new special process supplier while the base part remains unchanged.
    • Documented process issues – A corrective action drives re-validation of a specific subset of characteristics.

    The scope of a partial FAI is defined by which characteristics are affected by the process change. You still rely on the existing baseline FAIR for unchanged items.

    Typical triggers for delta FAI

    Delta FAI applies when there is a design or specification change, and you must verify only the impacted characteristics against the new configuration while referencing the prior full FAI.

    • Drawing revision changes – A revision adds, removes, or modifies dimensions, tolerances, GD&T callouts, or notes.
    • Specification updates – A new material spec is called out, a test requirement changes, or a surface treatment is updated.
    • Additional features – New holes, cutouts, stiffeners, or bosses are added to an existing part.
    • Tolerance changes – A previously generous tolerance is tightened on high-risk features.

    The delta FAIR documents only changed and newly added characteristics, but it must clearly reference the baseline FAIR for everything else. This is where digital lineage and linking are especially valuable.

    Common Challenges with Manual Partial and Delta FAI

    On paper and spreadsheets, partial and delta FAI often create more confusion than efficiency. The standard allows targeted verification, but without structured tools, teams struggle to manage scope correctly.

    Over-documentation and unnecessary re-inspection

    To be “safe,” some organizations treat every change as a reason to redo a near-full FAI:

    • Re-ballooning entire drawings instead of only the affected areas.
    • Copy-pasting a prior Form 3 and re-entering measurements for most characteristics.
    • Running duplicate inspections on features that are demonstrably unaffected by the change.

    This wastes engineering capacity, clogs CMM queues, and delays deliveries. It also undermines the original purpose of partial and delta FAI: focusing effort where risk actually changed.

    Under-documentation and missed linked features

    The opposite problem is just as common: teams underestimate scope.

    • A tooling change that affects multiple related features is treated as affecting only one dimension.
    • A GD&T callout is revised, but only one characteristic is updated instead of the entire feature pattern.
    • Downstream processes or mating parts impacted by a tolerance change are not considered.

    Without structured impact analysis, it is easy to miss derived or associated characteristics, exposing you to customer rejections or findings during AS9102 or AS9100 audits.

    Traceability gaps between baseline and follow-on FAIRs

    Manual systems often handle follow-on FAIRs as isolated files:

    • Baseline and delta FAIRs live in different network folders with inconsistent naming.
    • Form 1 status (full, partial, delta) is not used consistently, so reviewers cannot tell what they are looking at.
    • There is no simple way to see how many FAIRs exist for a part and what changed each time.

    These gaps make it hard to prove configuration history and FAIR lineage when customers or auditors ask for evidence.

    Designing Software Workflows for Partial FAI

    Modern AS9102 software can codify partial FAI logic so engineers execute consistent, risk-based scopes instead of reinventing the process each time.

    Tagging FAIRs with status (full, partial, delta)

    Start with explicit status tagging:

    • Every FAIR record uses the Form 1 field to mark full, partial, or delta.
    • Workflows and dashboards filter and report based on that status.
    • Search tools allow users to quickly find the most recent full FAI for a part and all associated partial or delta FAIRs.

    In a software system, status tagging can also drive automated routing and required approvals—for example, forcing quality or customer approval when a partial FAI is used to qualify a new facility.

    Reusing baseline characteristic data safely

    The biggest efficiency gain from digital FAI comes from treating the baseline FAIR as a structured data set rather than a static PDF.

    • Characteristics extracted and ballooned once are stored as reusable digital objects.
    • When a partial FAI is created, the software clones the baseline FAIR metadata, but flags only selected characteristics as “in scope” for re-verification.
    • Unchanged characteristics remain present for context but carry a clear indication that they are not being re-inspected as part of this partial FAI.

    This approach preserves one source of truth for the part while avoiding duplicated Form 3 lines and repeated manual entry.

    Controlling scope when process changes occur

    Well-designed workflows guide engineers through scope decisions instead of leaving everything to memory:

    • Partial FAI templates prompt users to identify the operation, machine, or facility that changed.
    • Characteristics in the baseline FAIR are linked to process steps and work centers.
    • The system proposes a list of characteristics likely affected by the changed operation.

    Engineers can then review, expand, or narrow that list, but they are no longer starting from a blank spreadsheet. This reduces the chance of missing characteristics that should logically be within partial FAI scope.

    Managing Delta FAI for Engineering Changes

    Delta FAI sits at the intersection of engineering change control and production verification. Software can bridge PLM, drawings, and FAIRs so the right characteristics are re-verified every time a revision is released.

    Linking ECNs and drawing revisions to affected balloons

    An effective digital workflow starts with change artifacts—Engineering Change Notices (ECNs), Engineering Change Orders (ECOs), or PLM change objects.

    • Each ECN or drawing revision is associated with the relevant part numbers in the FAI system.
    • The system compares old and new drawings, highlighting changed callouts, dimensions, notes, or specifications.
    • These differences are mapped directly to balloon numbers on the digital drawing and their corresponding Form 3 rows.

    With this linkage in place, the delta FAIR can be generated from a concrete list of changed characteristics instead of relying on manual visual comparison.

    Impact analysis to identify which characteristics must be re-verified

    The next layer of capability is impact analysis—looking beyond the explicitly edited dimension to understand what else should be considered in scope.

    • A tighter positional tolerance on a hole pattern may also bring associated datum features, countersinks, or threads into scope.
    • A surface finish requirement might impact both the machining operation and subsequent coating steps.
    • Changes to a material specification could trigger new or repeated material tests and special process verifications.

    Software can use rules and relationships embedded in the data model to suggest affected characteristic groups. Engineers then review and finalize the scope rather than building it from scratch.

    Building FAIR family trees and lineage views

    Over the life of a part, you may have one full FAI plus multiple partial and delta FAIRs. Without tools, keeping track of this family is difficult.

    • Digital systems construct a FAIR family tree that shows the baseline full FAI and every associated partial or delta FAIR, in chronological order.
    • Each child FAIR contains explicit links back to its parent FAIR and drawing revision.
    • Users can click into a characteristic and see a history of all times it was re-verified and why.

    This lineage not only supports audits; it also helps engineers quickly understand what has already been proven when planning further changes.

    Examples: Partial and Delta FAI Scenarios in Aerospace

    Concrete scenarios help clarify when to consider partial versus delta FAI and how software can handle each case. The exact decision in your organization should always follow customer and internal requirements, but these patterns are common.

    Machine or facility relocation of a machining operation

    Scenario: A supplier moves a 5-axis machining operation for a structural bracket from Plant A to Plant B. The drawing and spec do not change.

    • FAI type: Typically a partial FAI focused on characteristics produced by the relocated operation.
    • Manual challenge: Determining which dimensions are affected by the moved operation and which remain untouched.
    • Software approach: Link each characteristic in the baseline FAIR to its operation routing. When the routing changes, the system suggests the affected characteristics and generates a partial FAIR pre-populated with those characteristics only.

    Tolerance changes on critical hole patterns

    Scenario: Engineering tightens the positional tolerance and surface finish requirement on a critical hole pattern in a landing gear component.

    • FAI type: A delta FAI covering the modified pattern and any associated datums or related features deemed impacted.
    • Manual challenge: Ensuring all holes in the pattern, and not just one edited dimension, are included in the delta scope.
    • Software approach: The system compares drawing revisions, identifies the updated tolerance and finish, and maps those edits to all ballooned features in the pattern. Engineers validate the automatically generated list for the delta FAIR.

    Material substitution for specific callouts

    Scenario: A casting alloy spec is updated, or a substitute material is permitted for specific callouts on a structural part.

    • FAI type: Often a delta FAI covering characteristics and tests influenced by the new material, plus a new record of material certifications on Form 2.
    • Manual challenge: Understanding which tests or special processes need to be repeated and which geometric characteristics need closer scrutiny.
    • Software approach: Characteristics and Form 2 entries linked to the original material spec are flagged; the system prompts for updated certs, test results, and any newly required verifications.

    Measuring the Impact of Digital Partial and Delta FAI

    Organizations often adopt digital FAI tools to solve immediate pain, but you should also measure the impact of better handling of partial and delta FAI over time.

    Cycle time reductions and engineering capacity gains

    Key metrics for partial and delta FAI include:

    • Average time to complete a full FAI vs. partial/delta – With robust reuse and impact analysis, delta FAIRs should routinely take 50–80% less time than a full FAI.
    • Number of FAIRs completed per quality engineer – Automation should increase throughput without extending work hours.
    • Queue time at CMM and inspection resources – Reduced scope directly shortens queues when only affected characteristics are re-measured.

    Effect on audit findings and customer rejections

    Digitizing partial and delta FAI should also improve compliance outcomes:

    • Fewer documentation-related FAIR rejections – Clear status tagging and lineage reduce confusion about what has been verified when.
    • Reduced AS9100/AS9102 audit findings related to configuration control and traceability.
    • Better responsiveness in customer reviews – FAIR family trees and instant retrieval of supporting evidence shorten review cycles.

    Best practices for standardizing partial/delta policies

    To get consistent value from your software, codify your decision logic:

    • Create a partial vs. delta decision matrix aligned with the AS9102 standard and major customer requirements.
    • Embed that matrix into workflow rules and templates so engineers see guidance in context.
    • Review edge cases regularly and adjust rules to reflect lessons learned from audits and customer feedback.

    Over time, your partial and delta FAI process becomes repeatable, auditable, and scalable across sites and suppliers rather than dependent on a few experts.

    Using Partial and Delta FAI as a Strategic Lever

    Done well, partial and delta FAI strategies turn engineering change from a recurring scramble into a controlled, data-driven process. Modern AS9102 software helps you:

    • Reuse baseline FAIR data with confidence instead of rebuilding every time.
    • Focus verification on clearly defined, risk-based scopes.
    • Maintain transparent lineage across full, partial, and delta FAIRs for each part number.
    • Demonstrate robust configuration control during customer and certification audits.

    As your organization advances its digital FAI capabilities, consider how partial and delta FAI workflows align with broader goals like standardizing processes across plants, integrating with PLM and MES, and supporting a connected aerospace operations platform.

    For a deeper foundation on digital FAI tools, templates, and integrations, review the cluster hub on AS9102 and digital FAI fundamentals and then map your current partial and delta FAI workflows against the capabilities described there.

  • Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    Integrating AS9102 Software with ERP, MES, PLM, and QMS in Aerospace

    In modern aerospace manufacturing, AS9102 first article inspection (FAI) cannot be treated as a stand-alone activity. To keep programs on schedule and pass audits reliably, your FAI process and first article inspection reports (FAIRs) must be tightly connected to ERP, MES, PLM, and QMS systems. True AS9102 software integration removes manual data re-entry, strengthens configuration control, and makes FAIRs part of the broader digital thread.

    This article explains how AS9102 tools should integrate with core enterprise systems, the typical data flows you should expect, and example workflows that embed FAI into day-to-day production. It is a spoke in a larger guide on AS9102 software and a unified aerospace operations platform.

    For teams putting this topic into daily operation, digital AS9102 FAI, shop floor execution control, ERP, MES, and PLM integration paths help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Why AS9102 FAI Cannot Live in a Silo

    The risks of stand-alone spreadsheets and local tools

    Many aerospace OEMs and suppliers still run FAI using Excel templates, local ballooning tools, and network drive folders. Even when these tools generate AS9102-compliant forms, they usually sit outside the enterprise stack. The result is a set of disconnected artifacts that must be reconciled manually with ERP, MES, PLM, and QMS data.

    Common risks of siloed FAI tools include:

    • Re-keying errors: Part numbers, revisions, purchase orders, and lot data are typed multiple times across systems.
    • Configuration mismatches: FAIRs are created to one drawing revision while ERP or PLM have already advanced to another.
    • Limited reuse: Data from one FAI event cannot easily be reused for partial or delta FAI, change management, or trend analysis.
    • Local workarounds: Each plant or engineer maintains their own templates and conventions, undermining standardization.

    How disconnected FAI impacts schedule, quality, and audits

    When FAI is disconnected from core systems, the impact shows up quickly on programs and audits:

    • Schedule delays: FAIRs are started late because nobody realizes a new part or major change has reached production until after work orders are released.
    • Rejections and rework: Customers reject FAIRs due to wrong part numbers, incorrect revision levels, or missing traceability back to material and special processes.
    • Audit exposure: During AS9100 or customer audits, teams scramble across email, shared drives, and local PCs to reconstruct the full FAI picture.
    • Lost lessons learned: Nonconformances identified during FAI do not feed back into design or process improvement because they are trapped in separate spreadsheets or PDFs.

    Benefits of connected FAI data across the value stream

    By contrast, integrating AS9102 software into your enterprise architecture produces tangible benefits:

    • Single source of truth: Part, revision, and order data flow directly from ERP and PLM into FAIRs, eliminating conflicting records.
    • Automatic triggering: New part introductions, engineering changes, or process transfers can automatically trigger FAI requirements.
    • Closed-loop quality: FAIRs connect to nonconformance reports (NCRs), corrective actions (CAPAs), and process controls in the QMS.
    • Digital thread: FAI becomes a key node linking design, planning, production, quality, and in-service data.

    Key Integration Points for AS9102 Software

    Effective AS9102 software touches multiple systems. The integrations do not need to be implemented all at once, but the data model should anticipate each of these connections.

    ERP: part numbers, revisions, orders, and routings

    The ERP system is typically your commercial and planning source of truth. AS9102 software should at minimum:

    • Import item master data: Part numbers, descriptions, and key attributes such as make/buy status or commodity type.
    • Sync revisions: Current engineering or manufacturing revision, ideally cross-referenced to PLM identifiers.
    • Link to orders: Work orders, purchase orders, and sales orders that require FAIR submission.
    • Reference routings: Major operations or work centers associated with the part, enabling routing-based FAI rules.

    Typical workflows include:

    • FAI software periodically receives new or updated item data from ERP so Form 1 can be populated reliably.
    • When an order meets FAI criteria (e.g., first production lot, new part, or re-start after a lapse), ERP flags it, and an FAI record is automatically created.

    MES: work orders, operations, machines, and operators

    MES or shopfloor systems hold execution context. Integrating AS9102 software with MES enables:

    • Work order linkage: FAIRs tied to specific work orders or lots.
    • Operation-level traceability: Measurement results mapped to the operation, machine, and operator that produced the feature.
    • In-process data reuse: Dimensional or process checks collected during production can automatically populate Form 3.

    Common patterns include:

    • Launching FAI-specific inspection plans or electronic checklists when an FAI-designated work order reaches certain operations.
    • Pulling measurement data from automated equipment or operator tablets directly into the FAIR database.

    PLM: drawings, models, and engineering change data

    PLM or PDM systems manage design authority. They are essential for ensuring that FAIRs reflect the correct design configuration:

    • Drawing and model access: AS9102 software imports the released PDF drawings or model-based definition (MBD) for ballooning.
    • Revision control: FAIRs are tagged to specific design revisions; when a change is released, impacted characteristics are identified for delta FAI.
    • Change notice linkage: Engineering change orders (ECOs) or equivalent are associated with affected FAIRs for traceability.

    In a mature setup, PLM becomes the source of balloonable artifacts, while the FAI system manages characteristic extraction, accountability, and measurement results.

    Data Flows Between FAI and Quality Systems

    Beyond ERP, MES, and PLM, AS9102 workflows must connect to the organization’s QMS to support AS9100 and customer requirements.

    Connecting FAIRs to nonconformance and corrective actions

    FAI is often where early nonconformances are discovered. Integration with the QMS should support:

    • Linked NCRs: Each out-of-tolerance characteristic on Form 3 can initiate or link to an NCR.
    • Corrective action traceability: CAPAs reference the exact part, revision, and FAIR where the problem was found.
    • Closed-loop verification: Follow-up FAIRs or delta FAI events demonstrate that corrective actions were effective.

    Reusing FAI data in AS9100 documentation

    The structured data created during FAI can power broader quality documentation:

    • Evidence for process validation and production approval under AS9100.
    • Inputs to risk management and FMEA, particularly for key characteristics that show high variation.
    • Support for control plan updates and sampling strategy adjustments informed by FAI results.

    Without integration, teams must copy data from FAIRs into separate QMS records. With integration, FAI becomes a structured data source that feeds other processes automatically.

    Aligning calibration and measurement system data

    For FAIRs to stand up during audits, measurement results must tie back to calibrated instruments and qualified gages. Integration between AS9102 software and calibration/asset management systems should allow:

    • Recording which gage or CMM program was used for each measurement.
    • Verifying that instruments were within calibration at the time of use.
    • Flagging FAIRs if a later calibration failure suggests results may be suspect.

    This alignment simplifies responses when auditors ask for “evidence that gages used during this FAI were calibrated.”

    Example End-to-End AS9102 Workflow with Integrations

    To illustrate how these integrations work in practice, consider an end-to-end workflow for a new aerospace part.

    Triggering FAI from new work orders or part introductions

    1. Design release in PLM: Engineering releases a new part and associated drawing or model. PLM notifies downstream systems.
    2. ERP item creation: The part is added or updated in ERP, including revision and primary routing. A rule marks this part as requiring FAI for the first production lot.
    3. Automatic FAI record creation: When the first qualifying work order is created in ERP or MES, the AS9102 system automatically creates a corresponding FAIR record and Form 1 header using imported part/order data.

    Collecting inspection data on the shopfloor

    1. Ballooning and planning: The quality or manufacturing engineer imports the released drawing or model into the AS9102 tool, auto-balloons characteristics, and defines which operations or work centers will generate which measurements.
    2. Shopfloor execution: Operators or inspectors receive digital checklists or inspection plans via MES-integrated terminals or tablets. As they record measurements, results flow back to the FAI database, filling Form 3 rows linked to balloon numbers.
    3. Nonconformance handling: Any out-of-tolerance result automatically opens an NCR in the QMS, with a reference to the specific characteristic and FAIR.

    Approving and submitting FAIRs with linked evidence

    1. Quality review: Quality engineers review Form 1–3 inside the AS9102 system, verify that all characteristics are accounted for, and confirm that required material and special process certificates are attached.
    2. Electronic approval: FAIRs move through defined approval workflows with electronic signatures and time stamps.
    3. Submission and archiving: A customer-ready FAIR package (PDF plus structured data if required) is generated and submitted. The system stores the FAIR in a centralized repository, indexed by part, revision, order, and supplier.
    4. Future reuse: When a design or process changes, the baseline FAIR is reused to create partial or delta FAIRs rather than starting from scratch.

    Multi-Site and Supplier Integration Considerations

    Most aerospace programs involve multiple plants and a complex supplier network. AS9102 integration must account for this distributed reality.

    Standardizing FAIR templates across sites and suppliers

    Without standardization, each site or supplier tends to customize FAIR formats and naming conventions. A connected platform enables you to:

    • Define global AS9102 templates that enforce common fields and rules.
    • Allow limited configuration for customer-specific layouts while keeping a consistent underlying data model.
    • Report across FAIRs from different locations because they share the same structure.

    Supplier portals and shared data models

    For purchased parts, suppliers often own the FAI execution, but the OEM is still responsible for overall airworthiness. A supplier-facing portal or shared AS9102 platform can:

    • Provide guided FAIR templates aligned with your standards and customer requirements.
    • Enable suppliers to upload ballooned drawings, Forms 1–3, and certifications directly into your system.
    • Support automated validation checks on incoming FAIRs before they are accepted.

    This approach reduces variation in FAIR quality and accelerates review cycles, especially for high-volume or global supplier bases.

    Managing customer-specific requirements globally

    Major primes and engine manufacturers often apply their own FAIR formats, field requirements, and submission methods. An integrated platform should handle:

    • Configuration by customer: Mapping a single internal data model to different outward-facing FAIR templates.
    • Rule-based triggers: Customer and program-specific criteria for when FAI, partial FAI, or delta FAI is required.
    • Central visibility: Dashboards showing FAI status across customers, plants, and suppliers.

    Architecture Patterns for AS9102 Integration

    There is no one-size-fits-all approach to integrating AS9102 software. The right architecture depends on your existing systems, IT strategy, and digital maturity.

    Point-to-point vs platform-centric integrations

    Two broad patterns are common:

    • Point-to-point: The FAI system connects directly to ERP, MES, PLM, and QMS with separate integrations for each. This can be fast to implement for a small footprint but may become complex to maintain as scope grows.
    • Platform-centric: AS9102 capabilities are part of a broader aerospace operations platform that already integrates with ERP/MES/PLM/QMS. FAI reuses existing data models and services.

    Organizations starting with light integrations might choose point-to-point initially and then consolidate into a platform approach as volume and complexity increase.

    APIs, data lakes, and middleware approaches

    From a technical standpoint, integrations usually rely on one or more of the following:

    • REST or SOAP APIs: Near-real-time synchronization of parts, orders, and status updates.
    • Message queues or integration buses: Event-driven flows (e.g., a new ECO triggers delta FAI creation).
    • Data lakes or warehouses: Consolidated reporting and analytics across FAIRs, production data, and nonconformances.
    • File-based exchange: CSV, XML, or JSON batches for legacy environments where APIs are limited.

    Regardless of the technical mechanism, governance is critical: clear ownership of master data, change management, and validation of integrations before they are used for production decisions.

    Roadmap planning for digital thread and future scalability

    AS9102 integration should be planned as part of a broader digital thread roadmap rather than as an isolated IT project. Key roadmap considerations include:

    • Sequencing integrations (e.g., start with ERP/PLM, then add MES and QMS).
    • Defining standard identifiers for parts, revisions, orders, and characteristics across systems.
    • Ensuring that FAI data structures can support future capabilities such as MBD, AI-assisted sampling, and advanced analytics.

    For many organizations, moving from stand-alone ballooning tools to a unified aerospace operations platform is the key step that defines long-term scalability.

    Conclusion

    Integrating AS9102 software with ERP, MES, PLM, and QMS transforms FAI from a manual compliance burden into a strategic source of configuration control and process insight. By designing data flows carefully, standardizing templates across sites and suppliers, and choosing an architecture that fits your digital thread roadmap, you can reduce FAIR cycle times, cut rework, and strengthen audit readiness.

    The most successful aerospace organizations treat FAI as a connected process embedded in everyday manufacturing workflows. Start by identifying your highest-friction handoffs—typically between design, planning, and quality—and design integrations that eliminate re-keying while preserving rigorous validation and security review.

  • AS9102 Audit Readiness: Building Digital Traceability for FAI

    AS9102 Audit Readiness: Building Digital Traceability for FAI

    AS9102 Audit Readiness: Building Digital Traceability for FAI

    For aerospace manufacturers and suppliers, AS9102 first article inspection reports (FAIRs) are among the most scrutinized records in any audit. AS9100 surveillance audits, customer process reviews, and regulatory oversight all use AS9102 data as evidence of process capability, configuration control, and traceability.

    When FAIRs are scattered across spreadsheets, email threads, and shared drives, audit preparation can consume days of engineering time and still produce gaps. By contrast, digital AS9102 workflows give you structured data, clear traceability links, and rapid retrieval of evidence that can turn a high-stress audit into a routine review.

    For teams putting this topic into daily operation, digital AS9102 FAI, part traceability and as-built evidence, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains how auditors actually use AS9102 FAIRs, what they look for in your records, and which digital traceability capabilities matter most. It builds on the broader AS9102 software: digital first article inspection for aerospace manufacturing hub by focusing specifically on audit readiness.

    How AS9102 FAIRs Are Used in Audits

    FAIRs are more than part-specific documents; they are a window into how effectively your quality management system operates. Different types of audits use AS9102 evidence in slightly different ways.

    AS9100 surveillance and certification audits

    Certification and surveillance auditors use FAIRs to confirm that your organization:

    • Plans and executes first article inspection when required (new parts, design changes, process changes, lapses in production, and other triggers defined in AS9102).
    • Maintains configuration control so FAIRs match the correct drawing and specification revisions.
    • Demonstrates traceability from design requirements to inspection results, material certifications, and special processes.
    • Controls documents and records, including templates, approvals, and revisions.

    Typically, auditors will:

    • Sample a subset of part numbers and request the associated full, partial, or delta FAIRs.
    • Trace from the FAIR to the underlying drawing, work order, and material or process records.
    • Follow the trail into related procedures, work instructions, and training records.

    Gaps here often translate directly into nonconformances against AS9100 requirements for configuration management, monitoring and measurement, and documented information.

    Customer source inspections and process audits

    Customer auditors are usually more part- and program-focused. They use FAIRs to answer questions such as:

    • Did this supplier prove the process before we accepted production parts?
    • Are key characteristics (KCs) and critical characteristics (CCs) consistently controlled?
    • Are customer-specific clauses or purchase order requirements visible in the FAIR and supporting records?

    In many cases, the FAIR becomes the primary reference when customers evaluate supplier performance, approve new sources, or investigate recurring escapes. If FAIRs are incomplete, inconsistent, or hard to retrieve, confidence in your overall system immediately drops.

    Regulatory oversight and airworthiness evidence

    Regulators and delegated organizations (for example, through Designated Engineering Representatives or similar roles) rarely review every FAIR, but they expect to see that:

    • FAI is integrated into your production system as a standard practice, not a one-off activity.
    • Traceability exists from serial- and lot-level hardware back to the FAIR and its supporting evidence.
    • Special processes, materials, and key safety characteristics are verified and documented.

    When a potential airworthiness concern emerges, FAIRs and their traceability chain become critical inputs to investigations and corrective actions.

    What Auditors Typically Look for in AS9102 Records

    While each auditor brings their own style, there is a consistent core of AS9102-related questions and checkpoints. Understanding these expectations allows you to design your digital workflows around them.

    Characteristic accountability and completeness

    Characteristic accountability is central to AS9102. Auditors want to confirm that:

    • Every applicable requirement on the drawing and specification set has been identified and ballooned.
    • Each ballooned characteristic maps to exactly one row on Form 3.
    • Results on Form 3 are complete, legible, and clearly indicate acceptance or nonconformance.
    • Key and critical characteristics are identified and handled per internal and customer procedures.

    Digital tools make this easier by:

    • Automating ballooning of dimensions, GD&T, notes, and other requirements.
    • Synchronizing balloons to Form 3 so there are no missing or duplicated characteristics.
    • Providing click-through navigation between the Form 3 row and the corresponding balloon on the drawing.

    Correct usage of Forms 1, 2, and 3

    Auditors will review how you populate and control the three primary AS9102 forms:

    • Form 1 – Part Number Accountability
      They check that the part number, revision, FAI type (full, partial, delta), and related part or assembly details are accurate and consistent with your engineering and planning systems.
    • Form 2 – Product Accountability
      Expect questions about how you capture and link materials, special processes, and functional tests. Auditors verify that each entry is backed by a material certification, special process record, lab report, or functional test evidence.
    • Form 3 – Characteristic Accountability, Verification and Compatibility Evaluation
      They confirm that measurements, test results, and compatibility checks are properly recorded, with clear acceptance status and reference to the correct drawing revision.

    Misuse of forms—such as putting material data on Form 3, omitting FAI type on Form 1, or mixing drawing revisions—often triggers findings.

    Evidence of proper approvals and document control

    AS9102 FAIRs must reflect your broader document control practices. Auditors typically ask:

    • Who prepared, reviewed, and approved each FAIR—and when?
    • How do you ensure that only the latest approved FAIR template is in use?
    • What happens when a form or template is revised? Can you still retrieve prior versions?

    Digital AS9102 systems streamline these checks by embedding electronic signatures, maintaining template versions, and recording a time-stamped audit trail of changes.

    Building End-to-End Digital Traceability

    Traceability is the connective tissue that lets auditors move from drawing to FAIR to physical hardware and supporting evidence without losing the thread. A robust digital implementation captures these links by design.

    Linking FAIRs to serials, lots, and work orders

    At a minimum, your system should allow anyone to start from a specific part and quickly find:

    • The relevant FAIR(s) for that part number and configuration.
    • The associated work orders or shop orders and their status.
    • Individual serial numbers or lot numbers covered by the FAIR.

    From an audit perspective, this enables scenarios such as:

    • Starting from a serial number in service and working backward to the FAIR.
    • Starting from a FAIR and working forward to identify which batches or serials it covers.
    • Verifying that subsequent builds reference the correct baseline, partial, or delta FAIR.

    Integrating AS9102 software with ERP or MES makes these connections much more reliable than relying on manual data entry in spreadsheets.

    Associating material certs and special process records

    Auditors frequently follow the FAIR trail into materials and processes. Effective digital traceability includes:

    • Direct links between Form 2 entries and stored material certifications (e.g., heat, lot, and mill certs).
    • Attachments or references for special process records such as heat treatment, plating, welding, or NDT, including NADCAP scope where applicable.
    • Ability to filter or search FAIRs based on specific material lots or process batches when investigating issues.

    Instead of searching network folders for a PDF with a similar name to the lot number, auditors can click from the Form 2 line item directly to the supporting cert. That level of organization and speed sends a strong signal of control.

    Capturing calibration and equipment traceability

    For measurement and test data, auditors also care about the instruments and equipment used. Strong digital traceability supports:

    • Identifying which measurement devices or gages were used for specific characteristics.
    • Linking those devices to calibration records and due dates.
    • Demonstrating that no out-of-calibration equipment was used for FAI.

    Some organizations capture gage IDs directly in Form 3 or in linked inspection records. Others maintain traceability via integrated QMS tooling. Either way, the goal is to answer, with evidence: “How do you know the measurements in this FAIR are trustworthy?”

    How AS9102 Software Simplifies Audit Preparation

    Digital AS9102 platforms are not a substitute for good processes, but they make those processes visible and repeatable. The biggest audit-readiness gains come from how software centralizes data, preserves history, and standardizes outputs.

    Centralized search and retrieval across programs and suppliers

    Instead of chasing files across email, laptops, and shared drives, a central AS9102 system allows you to:

    • Search FAIRs by part number, part family, revision, work order, serial number, supplier, or customer.
    • Filter by FAI type (full, partial, delta) and status (draft, in review, approved, rejected).
    • Retrieve all FAIRs associated with a particular program or platform in seconds.

    During an audit, this means you can respond to document requests in minutes instead of hours or days, while maintaining confidence that you have the complete and correct records.

    Audit logs and version control for FAIRs and templates

    Auditors often ask, implicitly or explicitly, “How do you know this record is accurate and has not been altered inappropriately?” Strong digital controls help you demonstrate that by design:

    • Every FAIR has a full audit trail: who created it, who edited each field, who approved it, and at what date and time.
    • Template versions are controlled, so you can show exactly which revision of the AS9102 form was used for a given FAIR.
    • Historical versions of FAIRs are preserved, not overwritten, which is especially important for delta FAIs and repeated builds.

    When an auditor questions an entry or a change, you can walk through the digital history instead of relying on memory and handwritten notes.

    Standardized exports for audit evidence packages

    Many audits require you to assemble “evidence packages” that include:

    • Completed AS9102 Forms 1, 2, and 3.
    • Ballooned drawings.
    • Material certifications, special process records, and lab reports.
    • Relevant procedures or work instructions.

    Modern AS9102 software can generate these packages in standardized formats (often PDF plus native data exports) with a few clicks. Some systems also support customer-specific layouts and naming conventions while keeping a single internal data model.

    The outcome is not just audit speed, but consistency: every auditor sees complete and similarly structured evidence, which reduces confusion and follow-up questions.

    Preventing Common FAI-Related Audit Findings

    Most AS9102-related nonconformances are predictable. Understanding the patterns allows you to design your digital workflows, training, and checks to avoid repeat issues.

    Incomplete or mismatched FAIRs

    Frequent findings include:

    • FAIRs that do not cover all characteristics on the released drawing set.
    • FAIRs referencing the wrong drawing revision or obsolete specifications.
    • Inconsistencies between the part revision on the FAIR and the ERP, PLM, or purchase order.

    Digital mitigations include:

    • Automatic drawing import and ballooning tied to a specific revision.
    • Integration with PLM or ERP to pre-populate part and revision fields.
    • Validation rules that prevent approval if required fields or attachments are missing.

    Poor change control for partial and delta FAI

    Another common source of findings is how organizations handle changes:

    • Re-performing full FAI when only a subset of characteristics changed, without clearly documenting why.
    • Performing limited measurements but failing to declare the FAIR type as partial or delta on Form 1.
    • Creating new FAIRs that do not clearly reference the baseline FAIR they build upon.

    Digital AS9102 tools reduce this risk by:

    • Explicitly tagging FAIRs as full, partial, or delta and enforcing required fields for each type.
    • Reusing baseline FAIR data and clearly identifying only those characteristics impacted by the change.
    • Maintaining family trees or lineage views showing the relationships between the original and subsequent FAIRs.

    Inconsistent use of templates across sites

    Multi-site organizations and global supply chains often struggle with inconsistent FAIR formats and processes, leading to:

    • Different spreadsheet templates with different required fields.
    • Site-specific shortcuts that omit data important to customers or regulators.
    • Confusion during audits when evidence from different plants looks and behaves differently.

    By deploying a common digital AS9102 platform, you can enforce:

    • Standard templates that still allow for controlled customer-specific variants.
    • Shared workflows for preparation, review, and approval.
    • Centralized reporting on FAIR status and issues across all sites and key suppliers.

    Using FAI Data for Continuous Improvement

    Audit readiness improves dramatically when FAIRs are not just compliance paperwork but also inputs to continuous improvement. Digital traceability turns FAI data into an analytical asset.

    Trend analysis across FAIRs for recurring issues

    With structured, centralized FAI data, you can:

    • Identify characteristics that routinely run close to tolerance limits.
    • Spot recurring nonconformances for specific features, processes, or materials.
    • Compare performance across plants or suppliers for the same part or family.

    These insights inform process capability work, supplier development, and risk-based planning for future FAIs.

    Feeding lessons learned into design and process controls

    Digital FAIRs make it easier to loop findings back into engineering and manufacturing:

    • Highlight design features that consistently cause manufacturing or inspection challenges.
    • Provide quantitative evidence for adjusting tolerances, GD&T schemes, or process parameters.
    • Support risk assessments and control plans for future parts with similar features or processes.

    When auditors ask how you use data to drive improvement—not just compliance—you can point to structured analyses of FAIR results and resulting changes in design or process documentation.

    Aligning FAI improvements with AS9100 objectives

    AS9100 emphasizes risk-based thinking, process performance, and continual improvement. Digital AS9102 implementations support these objectives by:

    • Reducing the time and cost of FAI, freeing engineering capacity for proactive work.
    • Lowering FAIR rejection and rework rates through standardized, validated workflows.
    • Providing fact-based metrics on FAI cycle times, defects, and bottlenecks.

    This alignment is attractive to auditors: they see that your investment in digital FAI is part of a broader quality strategy rather than a narrow compliance response.

    Putting It All Together: A Practical Path to AS9102 Audit Readiness

    Preparing for AS9102-focused audits is not about building a separate checklist; it is about embedding audit-ready practices into your daily workflows:

    1. Standardize on clear procedures for full, partial, and delta FAI that reflect AS9102 Rev C expectations.
    2. Digitize ballooned drawings and FAIR forms so characteristic accountability and traceability are built into your tools.
    3. Connect your AS9102 system to ERP, MES, PLM, and QMS where practical to eliminate duplicate entry and mismatch risks.
    4. Control templates, approvals, and audit logs so you can demonstrate who did what, when, and under which revision.
    5. Analyze FAI data periodically to identify trends, recurring issues, and improvement opportunities.

    These steps will not guarantee a finding-free audit—no tool can—but they significantly reduce avoidable risk and show auditors that your organization manages AS9102 in a systematic, data-driven way.

    For a broader view of how digital FAI supports aerospace programs, including ballooning automation, workflow integration, and supplier collaboration, see the digital FAI and AS9102 software overview hub article.

  • AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    AS9102 FAI Triggers: New Parts, Changes, Lapses, and Delta Requirements

    In aerospace manufacturing, one of the most common quality questions is not what AS9102 first article inspection is, but when it is actually required. Teams know first article inspection matters. They know customers expect a compliant FAIR. What causes real friction is deciding whether a situation calls for a full FAI, a partial FAI, or no new FAI at all.

    That decision matters because unnecessary first article work slows production, ties up quality resources, and adds documentation overhead. On the other hand, missing a valid trigger can create customer escapes, audit findings, approval delays, and serious traceability problems. In aerospace, where configuration control and product conformity carry real operational and regulatory weight, getting this right is not optional.

    For teams putting this topic into daily operation, digital AS9102 FAI help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, digital AS9102 FAI, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains the most important AS9102 FAI triggers, including new part introduction, engineering changes, process changes, production lapses, and the circumstances that justify a partial or delta FAI rather than a full reset. It also looks at how aerospace manufacturers can manage these triggers more consistently using connected digital workflows.

    If you want the broader foundation first, review AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

    What AS9102 FAI Is Designed to Prove

    AS9102 first article inspection is a structured method for verifying that a production process can manufacture a part or assembly that fully conforms to engineering, specification, and purchase order requirements at the released configuration. It is not just a sample inspection. It is not a one-time paperwork exercise. It is a formal record that shows the part definition was interpreted correctly, the process was executed properly, and the evidence of conformity is complete and traceable.

    In practice, an FAI helps answer a straightforward but high-stakes question:

    Can this exact aerospace production process, at this exact released configuration, produce conforming hardware with full documented accountability?

    That is why FAI sits so close to configuration control, traceability, launch readiness, supplier quality, and customer approval. It creates a documented baseline that can later support change management, resubmissions, investigations, and audits.

    Why Knowing the Right Trigger Matters

    Plenty of aerospace organizations understand how to complete Form 1, Form 2, and Form 3. Fewer have a disciplined internal method for deciding when a new or updated FAI is required. That is where problems begin.

    If the trigger logic is weak, teams end up doing one of two things. They either over-trigger, which creates waste and slows down manufacturing, or they under-trigger, which creates risk. Neither outcome is good. The first hurts efficiency. The second hurts compliance, customer trust, and sometimes product integrity.

    A clear trigger model helps quality and manufacturing teams:

    • Apply AS9102 consistently across programs and part families
    • Reduce unnecessary full FAIR rebuilds
    • Identify when partial or delta FAI is appropriate
    • Align change control with customer and contract expectations
    • Protect traceability when production conditions shift

    Here’s the thing. The cost of poor trigger discipline is rarely visible all at once. It shows up as late package corrections, missing evidence, confused resubmissions, duplicated work, and uncomfortable customer conversations.

    New Part Introduction Is the Most Obvious FAI Trigger

    The clearest AS9102 trigger is the first production run of a new part number or assembly. When an aerospace organization introduces a part into production for the first time, it needs objective evidence that the released design can be built and verified correctly using the intended production process.

    This usually calls for a full FAI because there is no prior approved baseline to rely on.

    What counts as a new part introduction

    New part introduction typically includes:

    • A newly released part number entering production for the first time
    • A new assembly requiring first-time product accountability
    • A part transferred from development or prototype status into controlled production
    • A customer program launch where the released configuration has not yet been formally validated

    In these cases, the FAIR establishes the first documented baseline for the product. That baseline matters later when changes occur, because it gives the organization something traceable to compare against.

    Why aerospace treats this carefully

    In aerospace, new part introduction is not just about proving that one part measured correctly on one day. It is about proving that the released configuration, manufacturing route, inspection method, material traceability, and special process chain all support conformity. That is why the first baseline FAIR often becomes an anchor record for the life of the part.

    Design Changes Often Trigger Full or Partial FAI Activity

    Engineering changes are one of the most common reasons organizations revisit FAI. Not every revision change means the entire FAIR must be rebuilt, but changes that affect requirements, form, fit, function, interfaces, or inspection criteria often require at least a partial or delta FAI.

    Examples of design changes that may trigger FAI

    • Dimensional changes to a feature on the drawing
    • Tolerance changes on an existing characteristic
    • Material specification changes
    • Updated notes affecting finish, marking, or identification
    • Changes to critical, key, or safety-related characteristics
    • Revision changes affecting mating or installation conditions

    The real question is not simply whether the drawing revision changed. The better question is whether the released product definition changed in a way that affects conformity or verification. If it did, the FAI baseline likely needs to be updated.

    When a design change justifies a partial or delta FAI

    If the change affects only certain characteristics rather than the entire part, a partial or delta FAI is often the right choice. That allows the organization to revalidate only the impacted features while preserving the unaffected baseline from the original FAIR.

    This approach is especially valuable in aerospace because programs often evolve slowly through controlled revisions, and rebuilding a full FAIR every time can become needlessly expensive. Still, that efficiency only works if the company has strong revision control and can clearly identify which characteristics were affected.

    Process Changes Can Trigger FAI Even When the Drawing Stays the Same

    One of the biggest mistakes organizations make is assuming that if the drawing did not change, the FAIR does not need attention. In aerospace manufacturing, process changes matter because the product may be the same on paper while the route used to build it has changed in a meaningful way.

    If the process changes in a way that could affect part conformity, a new or updated FAI may be required.

    Common process-related FAI triggers

    • New manufacturing equipment or machine replacement
    • New tooling, fixtures, or program changes
    • Method changes in machining, forming, assembly, or inspection
    • Changes to sequence of operations that affect product outcome
    • Transfer of work between facilities or production cells
    • Changes in outside processing sources for controlled operations

    What this really means is that aerospace FAI is not only about the part definition. It is also about the process definition behind that part. If the way the part is made changes enough to alter risk, the FAIR logic needs to catch up.

    Why process changes matter so much in aerospace

    Aerospace production often involves tight tolerances, special processes, controlled materials, complex routings, and customer-specific source requirements. A machine swap, tooling update, supplier change, or move to a different facility can alter process behavior even if the part number and drawing revision remain identical. That is why smart trigger discipline looks at more than engineering release history.

    Material and Special Process Changes Require Careful Review

    In aerospace, traceability to material and special process evidence is central to FAI integrity. Form 2 exists for a reason. If the source or nature of the controlled inputs changes, organizations need to evaluate whether a new or updated FAI is required.

    Typical material and source changes that may trigger FAI

    • A new supplier for a controlled alloy or raw material
    • A change in material specification or condition
    • A new special process source for plating, heat treatment, NDT, coating, or similar operations
    • A change in approval status or scope of a special process provider
    • A change in process parameters that affects product characteristics

    Some of these may require only partial FAI activity. Others may justify a broader review, depending on the criticality of the change and the customer’s expectations. Either way, they should never be treated as invisible background changes. In aerospace, they are often part of the conformity story.

    Production Lapses Are a Real Aerospace Trigger

    Aerospace manufacturing does not always run at a steady cadence. Many parts are made intermittently. Some programs have long pauses. Some part numbers may go quiet for months or years before restarting. That makes production lapse one of the most important and most overlooked FAI triggers.

    If production has been dormant long enough, organizations may need to review whether the baseline process can still be trusted without refreshed validation.

    Why lapse-based triggers exist

    A long production gap can introduce risk even when the part and process documentation appear unchanged. During the lapse, a lot may have shifted:

    • Operators may have changed
    • Tooling may have worn or been replaced
    • Programs may have been updated
    • Equipment may have been serviced or relocated
    • Suppliers may have changed
    • Inspection methods may have evolved

    That is why production lapse should be treated as a process risk issue, not just a scheduling detail.

    How lapse thresholds are handled

    Many organizations use internal thresholds, customer requirements, or contract-specific rules to define what counts as a significant lapse. A common reference point is two years, but the right answer always depends on the customer, the product, and the organization’s quality system. The main point is that lapse-based trigger logic should be defined clearly and applied consistently.

    Full FAI vs Partial FAI vs Delta FAI

    One reason AS9102 remains practical in real aerospace operations is that it does not force a full restart every time something changes. Instead, it allows manufacturers to scale the response to the actual scope of impact.

    When a full FAI is usually appropriate

    • First production of a new part number or assembly
    • Major design change affecting broad portions of the part definition
    • Major process change with wide conformity impact
    • No reliable baseline FAIR exists
    • Customer or contract explicitly requires a complete new FAIR

    When a partial or delta FAI is often the better choice

    • Only selected characteristics changed
    • A limited process change affected a defined subset of features
    • Material or source changes affected traceability but not the full configuration
    • The baseline FAIR remains valid for unaffected requirements

    The discipline here is simple to say but harder to execute: revalidate what changed, preserve what did not, and document the logic clearly.

    Why organizations struggle with delta FAI

    Delta FAI sounds efficient, and it is, but only when the underlying data is structured well enough to support it. If characteristics are trapped in static spreadsheets, traceability is fragmented, or revision history is unclear, teams often end up redoing far more than necessary. In those environments, delta FAI becomes confusing because nobody can cleanly separate affected from unaffected requirements.

    Customer-Specific Requirements Still Matter

    AS9102 gives aerospace manufacturers a standard framework, but it does not erase customer-specific expectations. Many primes and upper-tier suppliers apply additional rules around when FAI is required, what counts as a significant change, how lapse thresholds are handled, and what submission format is acceptable.

    That means the right internal question is never only:

    What does the standard allow?

    It also needs to be:

    What did the customer contract, purchase order, or program requirement actually ask for?

    This matters because a technically defensible partial FAI may still be rejected if the customer expects a full resubmission package, specific portal workflow, or extra supporting documentation.

    Common Mistakes Aerospace Teams Make with FAI Triggers

    Most FAI trigger failures come from poor process visibility rather than bad intent. Teams are busy, systems are disconnected, and changes are sometimes managed in silos.

    Typical mistakes include

    • Treating revision changes as administrative without checking affected characteristics
    • Ignoring process changes because the drawing stayed the same
    • Missing lapse-based triggers on low-volume or intermittent parts
    • Failing to assess source changes for material or special processes
    • Overusing full FAI because delta logic is too hard to manage manually
    • Assuming one customer’s interpretation applies to every program

    The result is usually one of two ugly outcomes. Either the organization creates a lot of unnecessary quality work, or it ships with weaker evidence than the customer expects. Neither is a good place to be.

    How Digital Systems Make FAI Trigger Decisions Easier

    Digital FAI platforms are at their best when they do more than produce forms. They should help aerospace manufacturers manage trigger logic as part of a connected quality and manufacturing workflow.

    What a strong digital workflow can do

    • Maintain a traceable baseline FAIR by part number and revision
    • Track changes to characteristics, materials, and process routes
    • Highlight which features were affected by a revision or process update
    • Support partial or delta FAI generation without recreating everything
    • Connect Form 1, Form 2, Form 3, ballooned drawings, and certifications in one record set
    • Preserve audit history around why a given trigger decision was made

    That last point matters more than people think. In aerospace, it is not enough to make the right trigger decision. You often need to show later why that decision was reasonable.

    Why this matters for Connect 981-style operations

    Connected platforms are especially useful in regulated manufacturing because they reduce the gap between engineering changes, manufacturing process shifts, and quality documentation. Instead of waiting for someone to notice a trigger manually, the system can support earlier visibility into what changed and what evidence may need to be refreshed.

    That does not replace engineering judgment. It makes that judgment more consistent, more traceable, and less dependent on memory.

    How to Build a Better Internal FAI Trigger Policy

    Every aerospace manufacturer should define a practical internal trigger policy that aligns with AS9102, customer requirements, and real production conditions. The best policies are not vague. They are specific enough that quality, manufacturing, and engineering teams can use them without guesswork.

    A strong internal policy should define

    • What counts as a new part or first production run
    • What kinds of design changes trigger full, partial, or delta FAI
    • What kinds of process changes require review
    • How material and special process source changes are evaluated
    • What lapse threshold applies by default
    • How customer-specific rules override standard internal logic
    • Who has authority to approve the trigger decision
    • How that decision is documented for future audit or customer review

    Without this, organizations tend to rely too heavily on tribal knowledge. That works until the key person is out, the program changes hands, or the customer starts asking harder questions.

    Final Takeaway

    AS9102 FAI triggers are not just a compliance detail. They are part of how aerospace manufacturers control change, preserve traceability, and protect confidence in the production process. New parts, engineering changes, process shifts, material source changes, and production lapses can all justify a new or updated FAIR. The real challenge is knowing when a full FAI is necessary and when a partial or delta FAI is the smarter, defensible path.

    The organizations that handle this well do not treat FAI as a last-minute quality document. They treat it as part of a connected operational system that links engineering, production, inspection, and customer requirements. That is where the real efficiency shows up, and it is also where the strongest compliance posture comes from.

    To go deeper into digital workflows, FAIR structure, and connected aerospace quality execution, read AS9102 Software: Digital First Article Inspection for Aerospace Manufacturing.

  • Modeling Manufacturing KPIs with ISO 22400: Time, States, and Quantities

    Modeling Manufacturing KPIs with ISO 22400: Time, States, and Quantities

    Modeling Manufacturing KPIs with ISO 22400: Time, States, and Quantities

    ISO 22400 gives aerospace manufacturers a precise vocabulary for how key performance indicators (KPIs) are structured, not just what they are called. For production, MRO, and space hardware lines that must coordinate across multiple plants, suppliers, and digital systems, this structure is what keeps “utilization” or “availability” comparable from one site to another. This article explains how ISO 22400 models KPIs from raw signals through indicators to aggregated KPIs, and how time categories, equipment states, and quantity relationships shape data models used in aerospace manufacturing platforms such as ISO 22400 manufacturing KPI frameworks.

    The focus here is conceptual: how to design a KPI model that is faithful to ISO 22400, while leaving room for aerospace-specific metrics, regulatory constraints, and digital thread requirements.

    For teams putting this topic into daily operation, Connect 981’s aerospace execution solutions, real aerospace execution examples, ISO 22400 KPI governance help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, ISO 22400 KPI governance, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    From Raw Data to Standardized KPIs in ISO 22400

    ISO 22400 distinguishes clearly between what happens on the factory floor, how it is captured, and how it is eventually represented as KPIs. For aerospace engineering and manufacturing teams, understanding these layers is crucial for building traceable, auditable performance data across complex, multi-part assemblies and long product lifecycles.

    Raw signals: events, counters, and timestamps

    At the lowest level, production systems emit raw signals. These are direct outputs from control systems, machine controllers, test rigs, automated fastening cells, and inspection stations. Typical examples include:

    • Binary equipment status (ON/OFF, RUN/STOP bits)
    • Cycle counters (number of fastening cycles, pressure tests, or cure cycles completed)
    • Timestamps for state transitions (start of test, end of cure, pause/resume events)
    • Piece count pulses (part passed a sensor, panel left a station)
    • Alarm and interlock events (door open, vacuum loss, E-stop)

    These signals are typically stored in historians, SCADA archives, or MES event logs. On their own they are not KPIs; they are facts about what equipment did and when. ISO 22400 treats them as the foundation from which more meaningful indicators are derived.

    Derived indicators built from raw signals

    Derived indicators are intermediate measures created by processing raw signals. Common examples in aerospace environments include:

    • Time spent in a given equipment state (e.g., minutes in RUN vs. IDLE for a drilling cell)
    • Duration of a production order, operation, or test sequence
    • Total quantity produced, accepted, rejected, or reworked for a work order
    • Number of changeovers or configuration switches for a test stand

    These indicators are often calculated in MES or a manufacturing data platform by grouping raw events by order, work center, or resource and applying rules aligned with ISO 22400 definitions. The critical point is that indicators are still not KPIs; they are standardized building blocks from which KPIs are constructed.

    Aggregated KPIs as standardized conceptual objects

    KPIs in ISO 22400 are selected, aggregated indicators that have a specific meaning in manufacturing operations management. Examples include equipment utilization, order execution effectiveness, and quality-related performance indicators. They are characterized by:

    • Clear definitions: what they measure and which indicators they depend on
    • Time behavior: whether they apply to a shift, day, campaign, or order lifecycle
    • Scope: work unit, line, area, plant, or enterprise
    • Intended users: operator, supervisor, engineering, or management

    An ISO 22400-aligned aerospace data model therefore needs explicit objects (or tables) for raw events, derived indicators, and KPIs, with traceable relationships among them. This traceability is especially important in regulated environments (e.g., AS9100-compliant plants) where performance numbers must be auditable back to their underlying production evidence.

    Time-Based Foundations of ISO 22400 KPIs

    Time is the backbone of many ISO 22400 KPIs. For aerospace and defense manufacturing—where long takt times, complex assemblies, and certification-critical tests are common—time structure must be modeled carefully to avoid misleading utilization or turnaround metrics.

    Planned time vs. actual time

    ISO 22400 draws a strong distinction between planned time and actual time:

    • Planned time represents the scheduled availability of a resource or work unit—for example, a composite layup cell planned to run from 06:00 to 14:00 with a specific crew and product mix.
    • Actual time captures what really happened during that horizon—when the cell was running parts, in setup, in scheduled maintenance, blocked by missing material, or waiting for quality signoff.

    In a compliant data model, planned time and actual time should be represented as separate but related concepts, often linked by production order, resource, and calendar. KPIs such as utilization or schedule adherence draw on both, making it essential that the model preserves their differences.

    Busy, operating, and downtime categories

    ISO 22400 defines multiple time categories, including concepts such as busy time, operating time, and various forms of downtime. While the exact categorization is specified in the standard and supporting literature, the typical aerospace interpretation includes:

    • Operating-related time: intervals when the resource is technically able to operate, regardless of whether it is currently producing.
    • Busy time: sub-intervals of operating-related time where the equipment is actively performing its intended operation (e.g., machining, curing, testing).
    • Planned downtime: scheduled maintenance, calibration, or qualification runs that intentionally take the resource out of normal production.
    • Unplanned downtime: failures, quality holds, missing parts, and other disruptions.

    In KPI modeling, these categories are usually computed from sequences of equipment states and calendar rules. For example, a test stand in state RUN during planned production hours contributes to busy time, while the same RUN state during an off-shift period might be treated differently depending on the organization’s definition of planned operating time.

    Mapping time categories to performance concepts

    Many ISO 22400 KPIs can be understood as relationships among these time buckets. For instance, indicators related to utilization, availability, or schedule fulfillment can be conceptually defined as ratios involving busy time, operating-related time, and planned time. ISO 22400 does not mandate specific formulas; instead, it describes which time concepts are relevant to a given KPI.

    For aerospace plants, this mapping has practical implications:

    • Long-duration processes like autoclave curing must clearly distinguish between active process time and waiting or setup intervals.
    • Shared resources (e.g., metrology labs) require unambiguous rules for how time is allocated to different orders and programs.
    • MRO lines may need different time categorizations for turnaround commitments versus deep-dive inspections.

    A data model aligned with ISO 22400 therefore needs explicit structures for time segments, their categories, and their relationships to equipment, orders, and shifts.

    Equipment States and Their Role in KPI Calculation

    Time categories are derived from equipment states, which act as the bridge between automation signals and management-level KPIs. For aerospace and space hardware production, properly modeling these states is critical when multiple systems (test cells, tooling, handling robots) must report performance in a consistent way.

    RUN, STOP, IDLE, SLOW and other state concepts

    ISO 22400 uses conceptual states such as RUN, STOP, IDLE, and SLOW to characterize what equipment is doing. In practice, an aerospace facility might map detailed PLC codes or machine-status words into these generalized states:

    • RUN: machine is executing its defined operation on a work order (e.g., drilling a fuselage panel, performing a structural load test).
    • STOP: equipment is halted and not available to produce; cause codes may include fault, safety stop, or interlock.
    • IDLE: equipment is technically available but not currently processing—waiting for material, schedule, or operator.
    • SLOW: equipment is operating below its defined nominal rate, potentially due to conservative process settings, rework, or part complexity.

    These conceptual states do not replace detailed fault codes or process statuses; they sit above them as standard categories that can be interpreted consistently across sites and vendors.

    How states map to standardized time buckets

    To compute ISO 22400-aligned indicators, each interval in which a resource is in a given state is mapped to one or more time categories. For example:

    • RUN during planned production is usually part of busy time.
    • STOP during planned production may fall under unplanned downtime.
    • IDLE within planned operating hours might correspond to waiting or micro-downtime categories.
    • RUN during calibration may be counted as planned downtime or a specialized category depending on policy.

    The mapping logic is where MES, SCADA, and integration platforms implement business rules. ISO 22400 describes which combinations of time and state concepts a KPI depends on, but it leaves organizations free to tailor detailed mapping as long as the conceptual meaning is preserved.

    Consistency across automation and MES systems

    In aerospace manufacturing, it is common to operate mixed equipment fleets—legacy test stands, new digital workstations, and custom rigs from different suppliers. Without a clear state model, each system may use its own vocabulary, making multi-site KPIs impossible to compare.

    By adopting ISO 22400 state concepts as a common abstraction, manufacturers can:

    • Map heterogeneous PLC and controller states into a unified state set.
    • Ensure that utilization or downtime KPIs mean the same thing for a composite cell and a final assembly line.
    • Provide auditors and customers with a transparent explanation of how performance metrics are constructed.

    Platforms that integrate MES, historians, and supervisory control—such as a digital infrastructure used in aerospace plants—benefit from keeping this state model explicit and configuration-driven, rather than hard-coding vendor-specific semantics.

    Quantity-Based Elements: Good Units, Scrap, and Rework

    While time is central to many KPIs, ISO 22400 also structures quantity-based elements—produced units, scrap, and rework—especially important in aerospace where traceability, serial-number control, and configuration management are mandatory.

    Material-related quantities in ISO 22400

    ISO 22400 introduces standardized notions of material-related quantities such as:

    • Input quantity: material or units entering an operation or work center.
    • Output quantity: material or units leaving the operation, which may be further categorized.
    • Good quantity: output that meets defined quality requirements and is accepted into the next step or inventory.
    • Scrap quantity: output that cannot be used and is discarded or downgraded.
    • Rework quantity: output that requires additional processing before acceptance.

    In aerospace, these quantities must often be tracked at the level of serialized components, build positions, or configuration-controlled assemblies, not just bulk counts. An ISO 22400-aligned model should therefore link quantities to orders, product definitions, and serial numbers while preserving the standard’s conceptual roles.

    Relating quantity measures to time categories

    Many performance indicators relate quantities to time: for example, output per hour, accepted units per shift, or rework load relative to busy time. ISO 22400 encourages expressing these relationships using time categories and material-related quantities that have consistent definitions.

    In an aerospace setting, such relationships are crucial when comparing:

    • Different programs with varying levels of complexity and inspection intensity.
    • Prototype phases with high rework levels against stabilized series production.
    • MRO lines handling different fleet ages and modification packages.

    By modeling time categories and material quantities explicitly, engineers can construct KPIs that distinguish between true performance shifts and changes driven by mix or configuration.

    Conceptual links to quality and throughput KPIs

    Quality-related KPIs—such as first-pass yield or defect ratios—are conceptually built from good, scrap, and rework quantities. Throughput indicators combine these quantity measures with time segments to highlight the pace at which acceptable units flow through the system.

    ISO 22400 does not prescribe how aerospace organizations should act on these KPIs, but it ensures that the meaning of “good quantity” or “rework” is unambiguous. When a prime contractor and a tiered supplier both reference ISO 22400-aligned definitions, their reported quality and throughput figures can be compared or combined without semantic confusion.

    Designing a Data Model Aligned with ISO 22400

    For architects and data engineers building aerospace manufacturing platforms, the key challenge is turning ISO 22400 concepts into a coherent data model that remains stable over time and flexible enough for program-specific extensions.

    Representing indicators, KPIs, and relationships

    A practical ISO 22400-aligned model typically introduces distinct structures for:

    • Events and states: raw signals, state transitions, and alarms, linked to equipment, order, and timestamp.
    • Time segments: contiguous intervals of a given state and category (busy, planned downtime, etc.).
    • Quantity records: material movements and quantity outcomes per order, operation, and resource.
    • Indicators: computed aggregates (e.g., total busy time, scrap quantity) with clear derivation rules.
    • KPIs: structured objects that reference indicators, define their scope, and capture metadata such as unit of measure and trend direction.

    Keeping indicators and KPIs separate is important. It allows aerospace plants to introduce new KPIs—such as program-specific readiness metrics—without disrupting the underlying event or indicator structures that support other standards and reports.

    Dealing with multiple levels: work unit to plant

    ISO 22400 is consistent with hierarchical models used in manufacturing integration standards. KPIs can be defined at multiple levels: work unit, work center, area, site, or enterprise. Aerospace operations often add another set of slices: by program, platform, major assembly, or aircraft tail number.

    To reconcile these views, a robust data model should:

    • Maintain clear relationships between equipment and organizational units (lines, cells, areas, plants).
    • Support aggregations by physical hierarchy (e.g., test stands in a lab) and by logical groupings (e.g., all resources supporting a specific program).
    • Allow KPIs to be defined at one level and rolled up or drilled down without redefining their meaning.

    This multi-level design is especially important for OEM–supplier networks, where each organization may report ISO 22400-based KPIs at different granularities while still needing a consistent structure for contract performance reporting.

    Supporting future extensions without breaking the model

    ISO 22400 intentionally does not cover every aerospace-specific metric. Plants may need indicators tied to regulatory audits, customer-specific milestones, or advanced digital thread use cases. A well-structured data model should therefore:

    • Store KPI definitions as configurable metadata rather than hard-coded columns.
    • Allow additional attributes (e.g., safety relevance, certification impact) to be attached to KPIs.
    • Keep clear lineage from KPIs back to raw events, enabling review when definitions change.

    This approach lets organizations extend their KPI portfolios—adding, for example, metrics focused on engineering change-cycle time or test re-run rates—while maintaining alignment with the ISO 22400 concepts already in use.

    Using an ISO 22400-Aligned Model in Connected Environments

    Aerospace manufacturing operates as an interconnected network of systems: ERP for orders and contracts, PLM for product definition, MES for execution, QMS for nonconformance and corrective action, and specialized tools for test, inspection, and configuration management. ISO 22400 provides the shared KPI vocabulary these systems can use when exchanging performance data.

    Interfacing with ERP, MES, SCADA, and historians

    In a connected environment, each system contributes part of the data needed to construct ISO 22400 KPIs:

    • ERP supplies production orders, planned quantities, due dates, and sometimes planned calendars.
    • MES orchestrates operations, tracks execution, and records completion quantities and statuses.
    • SCADA and historians capture real-time equipment states, alarms, and process variables.
    • QMS manages inspection results, nonconformances, and dispositions that influence good/scrap/rework quantities.

    An ISO 22400-aligned manufacturing data infrastructure must consolidate these sources, align identifiers (orders, resources, serial numbers), and then compute indicators and KPIs according to the standard’s conceptual model. The goal is that a utilization figure or quality KPI computed from this integrated dataset carries the same meaning regardless of which plant, supplier, or system contributed the inputs.

    How platforms like an aerospace digital operations layer consume and expose KPI structures

    A digital manufacturing platform used in aerospace environments typically implements ISO 22400 concepts in its data layer while providing domain-specific experiences on top. It may:

    • Ingest state and quantity data from existing MES and test systems.
    • Normalize time, state, and quantity semantics to align with ISO 22400.
    • Expose KPIs through dashboards, APIs, and reports that can be filtered by program, tail number, or supplier.

    Because the KPIs are grounded in the standard’s structure, engineering and operations teams can compare performance more reliably across programs, plants, and external partners, even if their underlying automation landscapes differ.

    Maintaining conceptual purity when adding custom KPIs

    Aerospace organizations nearly always need KPIs beyond the 34 defined in ISO 22400-2—examples include metrics for airworthiness signoff cycle time, configuration-change backlog, or digital thread completeness. When adding such KPIs, it is important to maintain a clear separation:

    • Label ISO 22400-conformant KPIs explicitly, including references to the relevant parts of the standard where appropriate.
    • Mark organization-specific KPIs as custom while still building them on the same indicator and state/quantity structures.
    • Document how any custom KPIs relate to, or differ from, standard KPIs to avoid confusion in supplier and customer reporting.

    This approach preserves the integrity of ISO 22400 semantics while still giving aerospace plants the flexibility they need for regulatory, contractual, and engineering-driven performance measures.

    Conclusion: ISO 22400 as a Structural Guide for Aerospace KPI Modeling

    ISO 22400 does not tell aerospace manufacturers which KPIs they must use or how to run their factories. Instead, it defines how KPIs should be structured—how time categories, equipment states, and quantity concepts relate to each other and to the underlying raw data. By modeling these elements explicitly, aerospace organizations can build performance reporting that is consistent, auditable, and interoperable across plants, programs, and suppliers.

    For data architects and engineering teams, the value of ISO 22400 lies in treating KPIs as well-defined conceptual objects rather than ad hoc formulas. That discipline makes it possible to align digital thread initiatives, supplier scorecards, and internal improvement programs around a shared, standards-based understanding of manufacturing performance.

  • ISO 22400 KPI Categories: How the Standard Structures Manufacturing Metrics

    ISO 22400 KPI Categories: How the Standard Structures Manufacturing Metrics

    ISO 22400 KPI Categories: How the Standard Structures Manufacturing Metrics

    ISO 22400 gives aerospace and defense manufacturers a common language for describing manufacturing KPIs, but its real power shows up in how it categorizes those KPIs. The standard defines families and structures that cut across production, maintenance, quality, logistics, and energy, and it organizes indicators by object of measurement, organizational level, time horizon, and data type. For a digital aerospace factory, aligning to these categories makes it far easier to build interoperable MES dashboards, multi-site reports, and supplier KPIs that actually compare. This article explains how those ISO 22400 KPI categories work and how to apply them to aerospace operations, in conjunction with the broader ISO 22400 manufacturing KPI framework.

    Why KPI Categorization Matters in ISO 22400

    ISO 22400 is not just a list of 34 KPIs; it is a conceptual model for how performance indicators fit together. That structure is critical in regulated aerospace environments where programs, sites, and suppliers must align on definitions without being forced into one rigid dashboard template.

    For teams putting this topic into daily operation, ISO 22400 KPI governance help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, ISO 22400 KPI governance, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Linking KPI families to decision-making levels

    Within ISO 22400, KPI families are implicitly tied to different decision-making levels, from shift supervision to site leadership. For example, equipment-oriented indicators such as utilization and state-based time structure sit close to Level 3 (manufacturing operations management) in the IEC 62264 hierarchy, where production supervisors and manufacturing engineers work. Order-related KPIs—such as adherence between planned and executed order times—are more relevant to planning teams and program managers who need to reconcile capacity, delivery dates, and contract performance.

    In an aerospace plant, this means:

    • Cell leads and work-center supervisors focus on work-unit and line-level KPIs: machine availability, changeover behavior, and state distributions that explain why a composite layup cell or machining center is not meeting expected output.
    • Manufacturing engineering and industrialization teams focus on KPI families that compare planned versus actual routing times, NC program execution efficiency, and yield along the route.
    • Site leadership and program management rely on aggregated, ISO 22400-aligned KPIs (for example, site-level equipment utilization or order execution reliability) for capacity reviews and program health checks.

    Because KPI families are defined against the same conceptual structure, a site director can drill from a site-level scorecard down to a specific line or work unit without changing definitions along the way.

    Avoiding duplication and metric overload

    Aerospace factories frequently suffer from metric overload: multiple versions of “availability,” “efficiency,” or “on-time completion,” each defined differently by functions or programs. ISO 22400 reduces this risk by describing consistent categories and relationships among KPIs rather than letting each team invent their own vocabulary.

    By mapping plant-level metrics into ISO 22400 families, organizations can:

    • Recognize when two KPIs are actually the same concept with different names, and standardize on one.
    • Differentiate truly distinct indicators—such as a state-based availability measure versus an order-based schedule adherence KPI—so they are not conflated in reviews.
    • Limit dashboards to a curated subset of indicators that cover each needed category, instead of adding every variant of a similar measure.

    The result is leaner KPI sets that still cover production, quality, logistics, maintenance, and energy performance without redundant metrics that confuse operators and leadership.

    Functional Domains: Production, Maintenance, Quality, Logistics, Energy

    ISO 22400 groups KPIs by functional domain, recognizing that production, maintenance, quality, logistics, and energy each view the same manufacturing reality from different angles. This is especially important in aerospace, where a single nonconforming part can block production, disrupt logistics, and trigger additional inspection and rework.

    Production-oriented KPI families

    Production-oriented KPI families focus on how effectively a plant converts planned production time and capacity into conforming output. In aerospace environments, these families are typically applied to:

    • Machining cells and special processes (e.g., heat treatment, shot peening, composite curing), where time in RUN, STOP, and IDLE states directly affects backlog.
    • Assembly lines for fuselage sections, engine modules, or avionics racks, where takt adherence and order progression must align with program schedules.
    • Test cells for engines or components, where utilization, test cycle duration, and retest rates influence delivery performance.

    Within these families, ISO 22400 distinguishes between:

    • Equipment-focused indicators based on how a work unit spends its time.
    • Order-focused indicators based on how production orders progress versus plan.
    • Quantity-focused indicators summarizing produced, accepted, and rejected quantities over a period.

    Digital manufacturing systems can use these definitions to consistently classify data, regardless of whether the underlying process is machining a titanium bracket or assembling a guidance module.

    Maintenance, quality, and logistics-oriented KPI families

    Beyond pure production, ISO 22400 addresses KPI families that reflect other MOM functions:

    • Maintenance-oriented KPIs focus on the effect of planned and unplanned maintenance on equipment availability and capacity. In aerospace, this includes indicators such as the proportion of equipment time blocked for scheduled calibration, the impact of unscheduled downtime on critical path operations, and readiness of special-process equipment.
    • Quality-oriented KPIs measure how often output meets acceptance criteria, where nonconformances occur, and how rework affects flow. Typical examples include yield at a specific operation, rework ratio at a special process, or defect occurrence along a route. These indicators are particularly important in AS9100 environments where escape risk and recurring defects must be tightly controlled.
    • Logistics-oriented KPIs track material availability, work-in-progress location, and buffer behavior. For aerospace, this may cover kit completeness at line-side, staging accuracy for high-value components, and the effect of material shortages on order delays.
    • Energy-oriented KPIs relate energy consumption to production output or time in particular states. For example, a test cell’s energy use per test hour or a heat-treat furnace’s energy consumption per conforming batch.

    Each domain can own its specific indicators while still using a shared ISO 22400 vocabulary. A maintenance engineer and a quality engineer may discuss very different KPIs, but both can interpret how those KPIs relate to equipment states, orders, and time structures defined by the standard.

    Objects of Measurement and Organizational Levels

    Another ISO 22400 categorization dimension is the object of measurement—what the KPI actually describes—and the organizational level at which the KPI is applied. For aerospace operations, this is crucial for aligning cell-level realities with program-level commitments.

    From work unit to plant: where KPIs apply

    ISO 22400 recognizes different physical and logical objects of measurement, such as work units, work centers, areas, and whole plants. In an aerospace context, these might correspond to:

    • Work unit: A single machine (e.g., 5-axis mill, autoclave, coordinate measuring machine) or test stand.
    • Work center: A machining cell, composite layup area, or electrical harness assembly cell.
    • Area: A major section of the plant such as structural assembly, engine module build, or space payload integration.
    • Plant: The full manufacturing site manufacturing for multiple programs and customers.

    The same KPI family can be rolled up or down across these levels. For example, equipment utilization may be calculated for a single autoclave, aggregated across all autoclaves in the composite area, and further aggregated into a single composite-area capacity utilization metric for site-level planning.

    Aligning KPIs with enterprise/site/area/work center levels

    ISO 22400 uses a hierarchy consistent with IEC 62264, including enterprise, site, area, work center, and work unit. In aerospace, program management often spans multiple sites and suppliers, so the same conceptual KPI must be interpretable at each level:

    • Enterprise/program level: KPIs provide a cross-site view for a given aircraft, engine, or spacecraft program—for example, average order execution reliability across all plants producing a specific module.
    • Site level: Indicators highlight how a single plant performs overall, merging MOM data from machining, assembly, and test areas.
    • Area/work center level: KPIs show whether specific operations—like avionics integration or engine final assembly—are constraining throughput or generating disproportionate quality issues.
    • Work unit level: Detailed, state-based KPIs drive troubleshooting of particular machines or cells.

    Standards-aligned MES and reporting systems can map the same ISO 22400 KPI definitions up and down this hierarchy, simplifying multi-site benchmarking. A digital thread architecture can then tie those KPIs back to product definitions, routings, and configuration baselines.

    Time Horizons and Data Types in ISO 22400 KPIs

    ISO 22400 also categorizes KPIs by time horizon and data type. This is essential for aerospace manufacturing, where near-real-time decisions (such as reacting to a delayed material kit) must coexist with long-horizon metrics used in capacity and capital planning.

    Real-time vs. aggregated KPIs

    The standard distinguishes KPIs that are meaningful in near real time from those that require aggregation. For instance:

    • Real-time, state-based views: Dashboards showing the current status of critical machines (RUN, IDLE, STOP) for a hot engine-build or spacecraft integration area.
    • Shift- or day-level aggregations: Utilization and yield indicators over a shift, supporting crew debriefs and daily tier meetings.
    • Week- and month-level trends: Longer-term capacity and reliability behaviors used for staffing, capital planning, and program performance reviews.
    • Order-lifecycle metrics: KPIs computed per production order or lot, from release to completion, such as order execution reliability or overall order lead-time breakdown.

    A standards-based MES can label each KPI with its intended time behavior, making it clear which indicators are suitable for live shop-floor management versus retrospective analysis.

    State-based vs. quantity-based indicators

    ISO 22400 differentiates indicators driven primarily by states (time spent in defined equipment or order states) from those driven by quantities (produced, accepted, rejected units). Aerospace plants use both:

    • State-based indicators might capture the proportion of time an autoclave spends in RUN versus WAIT_FOR_LOAD, or how often a test cell is STOP due to missing instrumentation or ground support equipment.
    • Quantity-based indicators describe the number of conforming parts produced, scrap and rework volumes, or the ratio of accepted to total tested units during a given horizon.

    Many ISO 22400 KPIs combine both elements—for example, relating produced quantity to operating time. Aerospace manufacturers can use these distinctions to structure historians and data models: one layer describing states and times, another capturing quantities and results, and ISO 22400 KPIs defined on top of that foundation.

    Interdependencies Among the 34 ISO 22400-2 KPIs

    The 34 KPIs in ISO 22400-2 are not stand-alone; they share common time and quantity structures. This interdependency is especially important when analyzing complex aerospace production systems, where multiple indicators can shift together when a constraint or quality issue emerges.

    How changes in one KPI affect others

    Because ISO 22400 KPIs often share time categories or quantities, changing one part of the system can shift many indicators simultaneously. For example:

    • Improved maintenance planning that converts unplanned stops into scheduled downtime may improve equipment availability while slightly reducing nominal production time.
    • Reducing rework by addressing a recurring nonconformance at a machining operation may improve both yield and overall order execution reliability, since fewer orders are delayed for additional processing.
    • Simplifying changeovers in a cell may reduce setup time, improving utilization and throughput without changing total scheduled hours.

    From a standards viewpoint, these moves reallocate time among well-defined categories or change the ratio of accepted to total output. The interdependencies encoded in ISO 22400 make those trade-offs transparent.

    Practical implications for root cause analysis

    For root cause analysis, using ISO 22400 categories means that engineering and operations teams can rely on consistent relationships when drilling into issues. If aircraft wing assembly is behind schedule, analysts can reference:

    • State-based KPIs for the key work centers to see whether availability or planned stoppages are driving lost time.
    • Order-related KPIs to see whether delays are concentrated at specific operations or spread across the route.
    • Quality-oriented KPIs to see whether rework or nonconformances are consuming unexpected capacity.

    Because these KPIs are defined on shared time and quantity structures, conclusions drawn from one plant can more readily be compared to another site or supplier using the same ISO 22400 concepts, reinforcing both internal and external benchmarking efforts.

    Designing Dashboards Aligned with ISO 22400 Categories

    ISO 22400 does not prescribe one dashboard design, but its categories make it easier to build coherent views. For aerospace digital factories implementing an MES or a broader digital thread platform, these categories become the backbone of KPI visualization strategies.

    Grouping KPIs by function and object of measurement

    A practical way to design dashboards is to use ISO 22400 dimensions explicitly:

    • By functional domain: Separate views for production, maintenance, quality, logistics, and energy so each function sees indicators relevant to its responsibilities while still sharing a consistent vocabulary.
    • By object of measurement: Dashboards aimed at work-unit, work-center, area, or plant level, each using the same definitions but different aggregation scopes.
    • By time horizon: Live status displays for control rooms and cells, shift/24-hour summaries for supervisors, and weekly/monthly analytics for managers and continuous improvement teams.
    • By data type: Distinct panels for state-based time structure, quantity and yield metrics, and order-level execution indicators.

    For example, a composite manufacturing area might have:

    • A cell operator view showing current state of each autoclave, queue length, and imminent order completions.
    • A supervisor view with shift-level utilization, scrap/rework rates by work center, and schedule adherence by order family.
    • An engineering view focused on process capability and chronic downtime causes, using the same ISO 22400 categories but with more diagnostic detail.

    Examples of cross-functional KPI views

    Cross-functional dashboards are where ISO 22400 categories deliver the most value. Consider a site-level aerospace production visibility system that provides:

    • Production KPIs at area and plant level (e.g., equipment utilization, order execution reliability).
    • Quality KPIs linked to the same orders and work centers (e.g., yield, rework ratios, nonconformance density at special processes).
    • Logistics KPIs describing kit completeness and on-time availability of critical materials for those same orders.
    • Energy KPIs for high-consumption equipment such as autoclaves or test cells, tied back to output volume.

    Because all KPIs use ISO 22400-compliant definitions, a program manager reviewing a late aircraft structure can see, in one place, whether the constraint is equipment availability, quality escapes, missing material, or a combination of the three. When that manager then looks across multiple sites or key suppliers, indicators are directly comparable without negotiating new definitions each time.

    Platforms such as Connect 981 can implement these concepts as part of a standards-aligned digital manufacturing infrastructure, while allowing each aerospace organization to choose which ISO 22400 KPI families matter most for their operations and how they should be combined in reports and analyses.

  • Manufacturing Operations Management Standards in Aerospace: ISA-95, IEC 62264, and ISO 22400

    Manufacturing Operations Management Standards in Aerospace: ISA-95, IEC 62264, and ISO 22400

    Manufacturing operations management, usually shortened to MOM, sits in the layer between enterprise planning and machine-level control. It is the operational space where production orders become real work, quality checks happen in context, materials are tracked through execution, maintenance activities are coordinated, and actual performance data is captured for review.

    That middle layer matters in every manufacturing sector, but it matters especially in aerospace. Aerospace operations do not just need efficiency. They need traceability, configuration control, documented execution, supplier visibility, and audit-ready records. That makes MOM more than a scheduling concept. In a regulated environment, it becomes part of the control structure that connects engineering intent, shopfloor execution, and quality evidence.

    For aerospace manufacturers and MRO teams, MOM standards provide a shared way to define how this layer should work. Standards such as ISA-95, IEC 62264, and ISO 22400 help organizations describe the operational model, clarify how information should move between business systems and the floor, and measure whether execution is actually performing as intended.

    Connect 981 sits directly in this layer. It helps aerospace organizations connect work instructions, quality evidence, traceability records, supplier context, and execution visibility so the operational system is not split across disconnected tools. That is where MOM standards become practical. They are not just reference models. They describe the structure that modern aerospace operations need in order to run cleanly and prove control.

    What Manufacturing Operations Management Means in Aerospace

    At a high level, manufacturing operations management covers the activities used to manage, coordinate, monitor, and improve operations between planning and control. It is where high-level business intent gets translated into executable work and where execution results get pushed upward as usable operational data.

    In aerospace, that includes more than production dispatching. MOM typically touches four operational domains:

    • Production operations such as work order execution, sequencing, dispatching, and status tracking
    • Quality operations such as inspections, holds, nonconformance logging, acceptance evidence, and in-process verification
    • Maintenance operations such as equipment reliability, repair coordination, and service planning
    • Inventory operations such as raw material movement, WIP control, serialized parts tracking, and floor-level inventory visibility

    In aerospace manufacturing, these domains are tightly tied to compliance and product integrity. A work order is not just a job ticket. It may carry configuration requirements, revision-controlled instructions, part traceability, tooling requirements, inspection gates, and signoff expectations. That is one reason generic factory coordination language is usually not enough in aerospace. Teams need models that define these functions with much more precision.

    Where MOM Sits in the Manufacturing Stack

    The most widely used conceptual model for this comes from ISA-95, later aligned internationally as IEC 62264 and ISO 62264. These standards place MOM at Level 3 in the manufacturing hierarchy.

    Level Role Typical Scope
    Level 4 Business planning and logistics ERP, forecasting, master scheduling, enterprise resource allocation, planning
    Level 3 Manufacturing operations management Scheduling, dispatching, quality operations, maintenance coordination, inventory execution, work instructions, production visibility
    Level 2 Supervisory control SCADA, HMI, supervisory logic, machine status visibility
    Level 1 Direct control PLCs, controllers, equipment logic, feedback loops
    Level 0 Physical process Machines, tooling, materials, operators, physical production activity

    This model is useful because it makes the boundary clear. MOM is not long-range planning, and it is not direct machine control. It is the execution coordination layer in between.

    In aerospace, that is often the most operationally painful layer because it is where planning meets the reality of revision changes, shortages, supplier delays, inspection failures, operator signoffs, serialized components, and controlled deviations. It is also where most organizations feel the cost of fragmented systems most sharply.

    ISA-95 and IEC 62264 as the Core MOM Reference Model

    ISA-95 is the foundational standard family for defining manufacturing operations management functions and enterprise-control integration. It gives organizations a shared language for how manufacturing activities are structured, what kinds of information objects are exchanged, and where the operational layer begins and ends.

    Its international counterpart, IEC 62264, carries the same core conceptual role. In practice, many teams refer to ISA-95 and IEC 62264 together because they describe the same underlying model.

    What these standards define

    ISA-95 and IEC 62264 help define:

    • functional hierarchies across Levels 0 through 4
    • activity models for production, quality, maintenance, and inventory operations
    • information models for exchanging data between business systems and operational systems
    • clear boundaries between planning, operations coordination, and control

    That may sound abstract, but it matters in practice. If an aerospace organization cannot clearly describe what the operations layer is responsible for, it usually ends up with overlap, gaps, or disconnected systems. Work instructions may live in one place, inspection results in another, serialized material data somewhere else, and supplier visibility nowhere useful at all.

    The four MOM domains from ISA-95

    ISA-95 breaks manufacturing operations management into four main domains:

    1. Production operations management
      Covers scheduling, dispatching, work execution, resource allocation, and production status tracking.
    2. Maintenance operations management
      Covers maintenance planning, maintenance execution, equipment reliability, and upkeep coordination.
    3. Quality operations management
      Covers inspections, process verification, holds, nonconformance control, and quality reporting.
    4. Inventory operations management
      Covers material tracking, WIP control, movement visibility, and execution-level inventory status.

    Those categories map directly to aerospace pain points. A production team may be trying to dispatch work in sequence while quality is holding a serialized subassembly, maintenance is working around a machine issue, and inventory is waiting on controlled material release. That is not four separate realities. It is one operational system, and ISA-95 gives it structure.

    Why MOM Standards Matter More in Aerospace

    Many factories can tolerate operational ambiguity for a while. Aerospace usually cannot. The moment you add configuration control, special process traceability, regulated documentation, supplier flowdown, and audit expectations, the Level 3 operating layer becomes much more important.

    In aerospace, MOM-aligned operations help coordinate things like:

    • revision-controlled work instructions
    • serialized part installation records
    • inspection gates tied to product definition
    • nonconformance handling in production context
    • material traceability through execution
    • production and maintenance data needed for compliance evidence

    This is where Connect 981 becomes especially relevant. It supports the operational layer where those controls actually live. Instead of leaving quality evidence, execution records, supplier inputs, and floor-level status scattered across multiple tools, Connect 981 helps bring them into one connected operating view.

    ISO 22400 and the Measurement Side of MOM

    If ISA-95 and IEC 62264 tell you what the operational layer is, ISO 22400 tells you how to measure its performance more consistently.

    ISO 22400 focuses on key performance indicators for manufacturing operations management. The goal is to standardize how organizations define and calculate operational metrics so results can be interpreted more clearly across teams, sites, and time periods.

    What ISO 22400 contributes

    • standardized MOM-related terminology
    • defined KPI concepts and formulas
    • measurement logic tied to operational activities
    • more consistent interpretation of production performance

    This matters in aerospace because organizations often operate across multiple plants, suppliers, and programs. If one site calculates throughput one way and another site uses a different logic, leadership gets noise instead of insight.

    Common KPI categories linked to MOM

    Category Example Metrics
    Production and time Cycle time, throughput rate, schedule adherence, execution time
    Quality First-pass yield, defect rate, scrap ratio, rework rate
    Equipment and utilization Availability, performance rate, overall equipment effectiveness
    Maintenance Mean time between failures, mean time to repair, planned vs unplanned maintenance
    Inventory Inventory accuracy, stock turns, WIP visibility, material availability

    In aerospace, some of these metrics need nuance. OEE may still be useful, but it rarely tells the whole story in a low-volume, high-complexity, high-documentation environment. First-pass yield, schedule adherence on constrained programs, inspection queue time, hold duration, and traceability-related delays may matter just as much.

    Connect 981 helps make these metrics more meaningful because it ties them to the execution context behind them. A performance number becomes much more useful when teams can see which work order, part family, station, supplier input, or quality event shaped it.

    How ISO 22400 Relates Back to ISA-95

    The relationship is straightforward. ISA-95 and IEC 62264 describe the functional operating model. ISO 22400 describes how to quantify the performance of that operating model.

    • ISA-95 / IEC 62264 define the structure of production, quality, maintenance, and inventory operations
    • ISO 22400 defines how to measure those operations consistently

    That pairing is useful because it gives aerospace organizations both the language for the workflow and the language for the scorecard. One defines how the operational system is structured. The other defines how its performance can be evaluated in a more consistent, comparable way.

    Other Standards That Shape the MOM Layer

    Manufacturing operations management does not live in isolation. In aerospace, the MOM layer is shaped by other standards and regulatory expectations even when those standards are not MOM frameworks themselves.

    AS9100

    AS9100 is the aerospace quality management system standard. It does not define MOM architecture, but it strongly shapes what the operations layer must support. If the quality system requires traceability, documented process control, nonconformance management, and audit-ready evidence, the MOM environment has to help deliver that.

    AS9102

    First article inspection workflows often sit at or near the MOM layer because they connect production execution, inspection activity, drawing accountability, and evidence generation. A disconnected FAI process usually creates friction because it is detached from the operational execution model around it.

    NADCAP and special process oversight

    Special process traceability and supplier approvals also push requirements into the operations layer. The shopfloor or execution system needs to know not just what job is being run, but what approved source, process route, or certification scope applies.

    ISA-88

    ISA-88 is more closely tied to batch control, so it is not the primary MOM standard for most aerospace discrete manufacturing environments. Still, the concept matters in operations where structured procedural execution, recipe-like controls, or tightly sequenced process logic are relevant.

    Planning, MOM, and Control: The Practical Boundary

    One of the most useful things MOM standards do is force clarity about where one layer ends and another begins.

    Planning layer

    The planning layer decides what should be made, in what quantity, and in what overall timeframe. This is where ERP, demand planning, financial planning, master scheduling, and aggregate resource logic usually live.

    MOM layer

    The MOM layer translates that intent into executable work. It handles detailed scheduling, order dispatching, operator-facing instructions, execution visibility, floor-level quality coordination, maintenance coordination, and actual-versus-plan feedback.

    Control layer

    The control layer runs the machines and equipment. It is responsible for setpoints, sequencing, machine logic, supervisory control, and physical process execution.

    Why does this boundary matter? Because in aerospace operations, confusion at the boundaries creates real pain:

    • ERP tries to own details it cannot see in real time
    • machine systems expose data with no operational context
    • quality records sit outside production execution
    • operators get instructions that are current in one system and outdated in another

    A MOM-aligned operating model helps keep those responsibilities clearer. Connect 981 supports that model by sitting in the execution and coordination layer rather than trying to replace planning systems or machine controls. It helps bridge the gap between what the business planned and what the floor can actually prove happened.

    How MOM Standards Apply in Aerospace Manufacturing

    For aerospace manufacturers, MOM standards become valuable when translated into practical workflows.

    Production operations

    • controlled release of work instructions
    • routing visibility tied to revision status
    • sequencing and dispatching around constrained equipment or approvals
    • as-built execution data connected to the production order

    Quality operations

    • in-process inspection capture
    • hold points before critical operations continue
    • defect logging with production context
    • FAI, verification, and acceptance evidence connected to execution history

    Inventory operations

    • lot and serial traceability through the floor
    • WIP visibility by job, operation, or configuration state
    • controlled material issue and consumption records
    • supplier-linked material status where approvals matter

    Maintenance operations

    • equipment readiness visibility
    • maintenance coordination that affects execution schedules
    • machine reliability metrics that matter for constrained processes
    • better distinction between planned and disruptive downtime

    These are not just smart factory nice-to-haves. In aerospace, they support schedule integrity, compliance confidence, and product traceability. Connect 981 supports these workflows by helping organizations connect execution status, instructions, quality records, supplier context, and evidence in one environment.

    How MOM Standards Apply in Aerospace MRO

    MRO environments introduce a different version of the same problem. In maintenance operations, the execution layer must coordinate inspections, findings, repair routing, serialized component history, replacement decisions, and airworthiness-related documentation. That makes MOM concepts just as useful, even if the environment looks different from new production.

    In MRO, MOM-aligned thinking helps structure:

    • task execution against controlled maintenance instructions
    • findings capture with traceable evidence
    • component and serialized asset history
    • repair cycle coordination across stations or vendors
    • maintenance KPIs such as turnaround time, repeat findings, and reliability trends

    That is especially relevant because aerospace operations often span both production and support environments. Connect 981 supports both by helping teams keep instructions, findings, records, and coordination activity linked instead of split across departmental tools.

    What a Connected MOM Layer Looks Like in Practice

    In older environments, ISA-95 might map cleanly to a classic MES that sat between ERP and shopfloor control. In modern aerospace operations, the reality is often much more fragmented. One tool may handle instructions, another inspections, another defects, another supplier coordination, and another production status. The result is not a coherent MOM layer. It is a patchwork.

    A connected platform approach restores that missing operational layer by unifying:

    • digital work instructions
    • execution status tracking
    • quality checks and evidence capture
    • nonconformance workflows
    • supplier and material context
    • traceability across the job lifecycle

    That is where Connect 981 fits. It strengthens the operational zone that MOM standards describe. It helps aerospace organizations make the Level 3 layer more real, more connected, and more useful by tying execution, quality, supplier input, and traceability together in ways that support both compliance and day-to-day control.

    Final Takeaway

    ISA-95 and IEC 62264 define the operational structure. ISO 22400 defines how performance is measured. Aerospace standards such as AS9100 shape what that operating layer must support. Together, they form a practical framework for understanding how aerospace manufacturing and MRO operations should connect planning, execution, quality, maintenance, and measurement.

    For aerospace organizations, MOM is not an abstract standards topic. It is the structure behind cleaner execution, stronger traceability, better evidence, and more disciplined control across the operational layer. Connect 981 supports that structure by helping manufacturers and MRO teams bring work instructions, quality events, traceability, supplier context, and execution visibility into one connected operating model.

    For teams putting data mapping and system interoperability into daily operation, data mapping and system interoperability, ERP, MES, and PLM integration paths, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.