Author: garethshaw

  • Reducing AOG Risk With Faster Aerospace Non-Conformance Resolution

    Reducing AOG Risk With Faster Aerospace Non-Conformance Resolution

    Reducing AOG Risk With Faster Aerospace Non-Conformance Resolution

    In aerospace manufacturing and MRO, a single non-conformance can strand an aircraft on the ground, push a major delivery milestone to the right, or trigger an intensive regulatory review. Non-conformance management is not back-office paperwork; it is one of the main levers that determines how often quality issues turn into Aircraft-on-Ground (AOG) events and missed customer commitments. When organizations connect non-conformance workflows into an integrated aerospace non-conformance management workflow, they materially reduce operational disruption and protect key contracts.

    This article is for aerospace operations, quality, and compliance teams who need to understand Reducing AOG Risk With Faster Aerospace Non-Conformance Resolution. It explains the practical question this topic answers in a manufacturing execution context.

    This article links day-to-day non-conformance report (NCR) performance to AOG exposure, schedule risk, and customer trust. It focuses on practical levers: improving containment discipline, shortening engineering disposition time, and creating a data-driven view of risk across an AS9100-regulated manufacturing environment.

    For teams putting this topic into daily operation, non-conformance management, quality management workflows, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    AOG and Delivery Commitments in the Aerospace Context

    AOG situations and late deliveries are rarely the result of a single catastrophic failure. More often, they arise from ordinary non-conformances that are detected late, investigated slowly, or poorly communicated. Understanding how NCRs intersect with operations is the first step to reducing that risk.

    Why Even Single Non-Conformances Can Ground Aircraft

    In aerospace, non-conformances are tied to specific serial numbers, build records, and aircraft tail numbers. When a discrepancy is found on a safety-critical component—such as a flight control actuator, engine mount, or pressure vessel—regulations and internal airworthiness policies typically require immediate containment. That may include grounding an aircraft until engineering has issued a formal disposition.

    Even seemingly minor deviations (for example, out-of-tolerance fastener torques, undocumented process deviations, or missing inspection sign-offs) can become AOG drivers if they affect a configuration-critical zone or a system that is already on the aircraft. The technical risk may be small, but until a qualified engineer analyzes the condition against design and certification basis, the default position is to protect safety and hold the asset.

    The Cost and Reputation Impact of AOG Situations

    AOG events tied to non-conformances have measurable cost drivers: unplanned maintenance labor, expedited replacement parts, repositioning crews, and penalties under power-by-the-hour or availability contracts. For defense and space programs, AOG-like readiness impacts may drive liquidated damages or contractual performance deductions.

    Beyond direct cost, repeat AOG incidents attributable to slow or inconsistent NCR handling erode customer confidence. Airlines, operators, and government customers track how quickly suppliers can assess and resolve quality issues. When engineering dispositions routinely take days instead of hours, customers start to question the maturity of the supplier’s quality system and its ability to support long-term fleet operations.

    How NCR Processes Intersect With Maintenance and Delivery

    Non-conformance workflows are woven through production, modification, and maintenance operations:

    • Final assembly and delivery: An NCR on a late-stage component can immediately threaten the delivery date, especially if it involves a serialized part with long lead time or a customer-specific configuration.
    • MRO and heavy checks: When maintenance discovers a deviation that is not covered by the approved data set, work often stops while engineering issues a repair or concession. The aircraft stays in the hangar, regardless of slot pressure.
    • Field incidents and service bulletins: Non-conformances discovered in service can trigger fleet-wide inspections and additional NCRs on the production line, tying together manufacturing, in-service engineering, and customer support.

    The more fragmented the NCR process, the more these interactions create surprises: parts on hold that production planners don’t see, pending dispositions that line maintenance is unaware of, or inspection findings that never reach the team managing delivery milestones.

    Where Non-Conformance Processes Slow Down Operations

    Most aerospace organizations understand the technical rigor required for non-conformance evaluation. The bottlenecks usually arise from process and systems: who is notified, how information moves, and how decisions are documented across a distributed factory and supply chain.

    Waiting for Engineering Dispositions

    Engineering disposition time is often the longest single contributor to NCR cycle time, especially for complex assemblies and safety-critical hardware. Common delay patterns include:

    • NCRs arriving as unstructured email attachments or scanned PDFs, requiring engineers to search for essential data such as drawing revisions, process history, and serial numbers.
    • Ambiguous or incomplete discrepancy descriptions that force multiple clarification loops between quality and engineering.
    • Limited visibility into operational impact, so engineers are unaware that a pending disposition is blocking a customer delivery or an AOG return-to-service.

    In an integrated digital environment, engineers should see, at a glance, which open NCRs are tied to aircraft already in service, near-term deliveries, or critical schedule paths—and prioritize accordingly.

    Unclear Ownership of Containment Actions

    Containment is the first line of defense against AOG and schedule impact, yet responsibility is often diffuse. A non-conforming lot may be partially in stock, partially on the line, and partially at an external processor. Without clear ownership and system-driven tasks, containment becomes inconsistent:

    • Material is quarantined in one store but allowed to continue into assembly at another site.
    • Work instructions are updated on one shift but not communicated effectively to the next.
    • Maintenance finds an issue on-wing but the related parts in production are not flagged, creating future risk.

    When containment is slow or incomplete, the eventual disposition often affects a much larger population of parts or aircraft, increasing the likelihood of AOG-level actions.

    Fragmented Tracking Across Sites and Shifts

    Aerospace programs typically span multiple facilities, time zones, and partner organizations. If NCRs are tracked in local spreadsheets, email folders, or non-integrated MES and QMS tools, no one has a single, reliable view of risk and status. This fragmentation introduces several AOG drivers:

    • Open NCRs on safety-critical components that are invisible to the teams planning maintenance or delivery slots.
    • Duplicate investigations into the same underlying condition at different sites, wasting engineering capacity and delaying real root cause analysis.
    • Missed escalation thresholds because there is no consolidated dashboard of aging, high-risk NCRs.

    Connect 981 and similar digital manufacturing infrastructures address this by creating a unified, cross-site picture where each NCR has a clear owner, status, and operational linkage.

    Key Levers to Reduce NCR-Related AOG Risk

    Preventing AOG and delivery slips is less about eliminating non-conformances altogether and more about managing them intelligently. Three levers consistently show impact: risk-based prioritization, automated communication, and standardization for high-risk items.

    Clarify the operational risk

    When the work behind Reducing AOG Risk With Faster affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in Reducing AOG Risk With Faster

    Risk-Based Prioritization and Routing

    Not all NCRs merit the same urgency. A structured risk model helps route and prioritize work so that scarce engineering and quality resources focus where they protect availability and safety most:

    • Technical criticality: Link NCRs to part criticality (for example, flight safety, mission-critical, maintenance-significant) and to the systems they affect.
    • Operational impact: Flag NCRs associated with assets in service, in heavy check, or within a defined delivery horizon.
    • Regulatory sensitivity: Identify non-conformances that touch certification basis, airworthiness limitations, or mandated inspections.

    An NCR with moderate technical severity but direct impact on an AOG recovery may deserve higher priority than a more severe issue on a part still weeks away from use. Digital workflows can codify these rules and push high-risk NCRs to specialized engineering teams with appropriate response-time targets.

    Automated Notifications and Escalations

    Manual follow-ups—phone calls, reminder emails, spreadsheet extracts—are unreliable mechanisms for managing hundreds or thousands of open NCRs. Automated notification logic reduces latency between events (detection, containment, disposition) and decisions:

    • Immediate alerts to responsible engineers when an NCR is raised on a safety-critical serialized component.
    • Escalations to functional and program management when high-risk NCRs approach or exceed defined cycle time thresholds.
    • Notifications to planning and logistics when a disposition decision changes part availability assumptions.

    These mechanisms should be integrated with existing MES, ERP, and engineering tools so that status changes in one system are reflected in others. The goal is to ensure that an NCR never languishes simply because the next actor didn’t see it.

    Standardized Templates for High-Risk Parts and Systems

    For certain parts—landing gear components, hydraulic actuators, structural joints, propulsion hardware—non-conformances recur in recognizable patterns. Creating standardized NCR templates and investigation checklists for these areas shortens engineering response and improves consistency:

    • Pre-defined data fields for loads, environment, material batch, and inspection method relevant to the specific part family.
    • Embedded guidance on acceptable deviations, applicable design allowables, and previous dispositions.
    • Standard repair schemes or concession criteria that can be rapidly tailored rather than created from scratch.

    This standardization works best when supported by a central, searchable knowledge base linked directly to the NCR system, rather than scattered engineering reports on shared drives.

    Using Data to Predict and Prevent Disruptions

    Non-conformance data is often underused. When integrated into a broader digital thread, it becomes a forward-looking indicator of AOG and schedule risk rather than a static archive for audits.

    Identifying Patterns Tied to AOG Events

    By correlating historical AOG incidents and major delivery slips with NCR records, organizations can identify specific signatures that signal elevated risk. Examples include:

    • Repeated late-stage NCRs on the same subassembly or work center.
    • Clusters of non-conformances on parts from specific suppliers or special processes.
    • Frequent concessions on the same dimension or feature, indicating design or tolerance issues.

    These patterns guide where to focus engineering support, process improvement, or design changes. More importantly, they can feed alerting logic: when similar NCR patterns reappear on current programs, operations teams can proactively protect schedule and fleet availability.

    Monitoring Cycle Time for Safety-Critical NCRs

    Overall mean time to close NCRs is useful, but safety-critical and AOG-linked NCRs require more granular monitoring. Typical metrics include:

    • Average and 90th-percentile disposition time for safety-critical components.
    • Time from detection to effective containment on serialized, in-service hardware.
    • Number of open high-risk NCRs older than agreed thresholds.

    When these indicators degrade, it often signals capacity issues in engineering, process bottlenecks, or insufficient data in initial NCRs. Addressing those upstream problems directly reduces the chance that a future aircraft will remain on the ground while decisions are made.

    Proactive Maintenance and Design Improvements

    Non-conformance trends also inform reliability engineering and maintenance planning. If NCRs repeatedly surface on the same component in both production and MRO, that may justify:

    • More targeted inspection intervals or condition-based monitoring thresholds.
    • Design changes that increase manufacturability or reduce sensitivity to process variation.
    • Supplier process changes or additional process controls for high-variation steps.

    These actions will not eliminate AOG events entirely—operational and environmental factors also play significant roles—but they reduce one of the key controllable contributors: quality-driven disruptions.

    Collaborating With Customers on Critical Non-Conformances

    For major operators and government customers, how an organization communicates about critical non-conformances during an AOG or high-visibility delivery issue is almost as important as the technical fix.

    Communication Protocols During AOG-Related Issues

    Structured communication protocols help avoid both under- and over-communication. Typical elements include:

    • Pre-defined trigger conditions for customer notification (for example, NCRs affecting in-service fleet, airworthiness limitations, or delivery-critical items).
    • Named technical and commercial points of contact on both sides.
    • Agreed update cadence during active AOG investigations.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for Reducing AOG Risk With Faster

    These protocols should be linked to the NCR system so that when an issue is flagged as customer-notifiable, the corresponding communication workflow starts automatically, with consistent content and traceability.

    Sharing Status and Documentation Securely

    Customers increasingly expect near-real-time visibility into NCRs that affect their assets or delivery lines, but this has to be balanced with intellectual property and export control constraints. A modern platform approach enables:

    • Role-based access to NCR summaries, dispositions, and supporting evidence.
    • Time-bound sharing of specific records for joint investigations or regulatory reporting.
    • Audit trails of what was shared, with whom, and when.

    This transparency builds trust while maintaining control over proprietary design and process data, and simplifies joint root cause analysis during multi-party investigations.

    Balancing Transparency With Data Protection

    Aerospace programs often involve export-controlled information, classified work, or sensitive defense capabilities. Non-conformance records naturally contain technical detail, so uncontrolled sharing is not acceptable. Effective collaboration therefore relies on:

    • Data segregation and tagging (for example, ITAR, EAR, program-restricted) within the NCR system.
    • Configurable redaction or abstraction of sensitive details in externally shared reports.
    • Alignment between engineering, export control, and legal teams on what can be disclosed under which circumstances.

    These controls should be embedded into the digital workflow so that engineers and quality teams can collaborate with customers efficiently without manually managing classification rules each time.

    Embedding Lessons Learned Back Into Operations

    Reducing AOG and delivery risk is not a one-time project. The value of each closed NCR lies in how well its lessons are captured and reused across the production system and supply chain.

    Updating Procedures and Training

    When repeat non-conformances drive AOGs or delivery slides, the root causes often point to unclear procedures or inconsistent training. Effective organizations link NCR closure to concrete updates:

    • Revision of work instructions, inspection plans, or special process parameters.
    • Targeted refresher training for specific roles or certifications.
    • Job aids or checklists embedded at the point of use in MES or digital work instructions.

    The NCR system should track which procedural changes were triggered by which investigations, making it easier to verify that corrective actions are fully deployed.

    Adjusting Inspection Points and Sampling Plans

    Non-conformance data is a powerful input to risk-based inspection planning. When particular features or operations are systematically implicated in AOG-related NCRs, organizations can:

    • Introduce additional in-process inspections earlier in the routing.
    • Increase sampling rates or move from sampling to 100% inspection for selected characteristics.
    • Deploy automated inspection technologies where human error is a significant contributor.

    Conversely, areas with stable performance and a long history of conforming results can sometimes justify reduced inspection intensity, freeing up quality capacity to focus on higher-risk work.

    Tracking Whether Improvements Reduce Future AOG Incidents

    Closing the loop requires measuring whether process changes actually reduce operational disruption. Useful indicators include:

    • Trend in AOG events where non-conformance was a primary or contributing factor.
    • Reduction in repeat NCRs for the same cause, part, or work center.
    • Improved adherence to delivery milestones on assemblies historically affected by quality-driven delays.

    By linking these outcomes back to specific NCR-driven improvements, organizations build a quantitative case for continued investment in integrated quality systems and digital infrastructure.

    Non-conformances will always exist in complex aerospace manufacturing and maintenance environments. The differentiator is how effectively they are detected, contained, investigated, and translated into enduring improvements. When non-conformance management is treated as a core element of the aerospace production system—supported by integrated data, risk-based workflows, and disciplined collaboration—it becomes one of the most powerful tools for controlling AOG risk and protecting delivery performance.
  • MES for Aerospace MRO: Managing Tail-Number-Specific Maintenance Execution

    Manufacturing execution in maintenance, repair, and overhaul looks very different from execution in a production line. In an aerospace MRO environment, the work scope is driven by aircraft condition, operator requirements, service bulletins, airworthiness directives, and the exact configuration of the tail number or serialized assembly in the shop. That means an MES for aerospace MRO must do more than route work through standard steps. It must coordinate changing workscopes, maintain serial-level history, and preserve the evidence needed for compliant release documentation.

    This article is for aerospace operations, quality, and compliance teams who need to understand MES for Aerospace MRO: Managing Tail-Number-Specific Maintenance Execution. It explains the practical question this topic answers in a manufacturing execution context.

    For repair stations and airline maintenance organizations, the execution layer is where inspections, findings, repair decisions, parts replacements, and approvals become a controlled digital record. This is also where teams connect planning systems, shop activity, quality checks, and technical publications into a single operational flow. For a broader view of connected MES for aerospace MRO operations, it helps to start with the role of execution in regulated aerospace environments.

    For teams putting this topic into daily operation, MES execution control, MRO execution workflows, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Connect981 can serve as that execution layer for Part 145 organizations by orchestrating digital workflows across inspection, repair, subassembly routing, traceability, and release readiness without forcing maintenance teams into a rigid high-volume production model.

    Regulatory Context for MRO and Repair Stations

    FAA Part 145, EASA Part-145, and customer requirements

    Repair stations operate under a different compliance profile than production organizations. The governing framework typically includes FAA Part 145 or EASA Part-145 requirements, plus air carrier procedures, OEM maintenance data, lessor conditions, and customer-specific contractual controls. In practice, execution software has to help enforce the approved maintenance data and the organization’s own procedures, while still allowing authorized personnel to document findings and disposition paths as work evolves.

    An MRO MES should therefore support controlled routing, role-based approvals, revision-aware work instructions, and evidence capture tied to the actual maintenance event. It should not attempt to replace the regulatory framework or interpret approvals on behalf of the repair station. Its value is in making the approved process executable, traceable, and reviewable.

    Differences between production and maintenance records

    Production records focus on how a part was built. Maintenance records focus on the condition of an in-service article, what was found, what action was taken, what parts were removed or installed, and who approved each step. The record must often connect installed configuration, operational limits, prior maintenance history, and the maintenance data used during the event.

    That distinction matters because MRO execution often starts with uncertainty. A shop may receive an engine module, flight control component, or avionics assembly with a planned scope, then expand that scope after teardown and inspection. An MES designed for repetitive manufacturing can struggle here unless it supports conditional branching, ad hoc findings capture, and controlled routing additions.

    Audit expectations for digital maintenance histories

    Auditors and customers generally expect a maintenance history that can be followed from intake through release. That includes timestamps, technician actions, inspection outcomes, material or component changes, and evidence that required approvals occurred. Digital systems are valuable when they preserve an attributable, legible, and reviewable history rather than scattered paper packages and disconnected spreadsheets.

    For aerospace organizations, this history also needs to survive customer review, internal quality investigations, and long retention periods. An execution system should make it easy to retrieve the complete trail for a tail number, serialized subassembly, or repair event without reconstructing the story manually.

    Execution Challenges Unique to Aerospace MRO

    Unplanned work scope and findings during teardown

    One of the defining MRO problems is that the true workload often appears only after disassembly. Corrosion, wear, out-of-tolerance dimensions, coating loss, impact damage, contamination, or undocumented prior repairs can all change the route. A usable MRO MES must let teams decompose a high-level work order into emerging tasks without losing control of approvals or traceability.

    For example, a landing gear component may arrive for scheduled shop visit work. During teardown, inspectors identify bushing wear and a damaged bore that triggers additional inspection, engineering review, special process routing, and part replacement. The execution layer should be able to add those steps, assign holds, collect measurements, and document the approved path to reassembly.

    Managing service bulletins and airworthiness directives

    MRO execution is also shaped by mandatory and recommended actions from OEMs and regulators. Service bulletins and airworthiness directives can alter inspection criteria, replacement thresholds, or required modifications. The challenge is not just storing those references; it is ensuring the right maintenance data and task content are applied to the affected tail number or serialized assembly.

    An effective MES can associate the current workscope with applicable maintenance requirements, flag open actions, and route tasks based on model, configuration, or operator program. This helps teams avoid missed compliance steps when different fleets, engine variants, or customer maintenance programs are processed in the same facility.

    Clarify the operational risk

    When the work behind MES for Aerospace MRO: Managing affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in MES for Aerospace MRO: Managing

    Handling life-limited and time-controlled parts

    Life-limited parts and time-controlled components are central to many overhaul environments, especially in engines, rotating assemblies, and safety-critical systems. The execution system must track part identity, status, installed position where relevant, accumulated usage data if provided, and the maintenance action taken during the event.

    This is not simply inventory control. The maintenance record has to show that the correct serialized component was removed, evaluated, replaced or reinstalled under the approved criteria, and reflected in the final configuration. When these controls are weak, release documentation becomes slower and the risk of traceability gaps rises sharply.

    MES Functions for MRO Workscopes and Routing Control

    Work order decomposition by assembly and subassembly

    In MRO, the top-level visit or repair order is rarely enough to control execution. Teams need to break work down by module, assembly, subassembly, and component so each item can move through inspection, repair, outside processing, and reassembly with its own status. An MRO-capable MES should support this hierarchy natively.

    That means a single engine overhaul event can be decomposed into fan module, compressor, combustor, turbine, accessory gearbox, and serialized piece-part activity. Each level can carry findings, routing steps, required approvals, and material transactions while remaining connected to the overall shop visit record.

    Disassembly, inspection, repair, and reassembly sequences

    Unlike repetitive manufacturing routes, MRO sequences often begin with controlled disassembly and condition assessment. The system should be able to record when a serialized article was disassembled, what was removed, what condition was observed, and what downstream steps were triggered. After inspection, approved repairs and reassembly tasks must be sequenced so nothing advances past required checks.

    Practical controls include operation gating, hold points, mandatory data fields, attachment of images or measurement records, and inspector sign-off before the next task can begin. These controls reduce the chance of components bypassing required evaluation or reassembly proceeding with unresolved discrepancies.

    Variant management for different aircraft and engine models

    Repair stations frequently support multiple aircraft, engine, and component variants in the same shop. Even where the hardware appears similar, maintenance limits, manuals, tooling requirements, and approvals can differ. A strong MES architecture supports variant-specific routings and task logic rather than one generic process.

    This matters for both compliance and throughput. If technicians have to manually determine which version of a route applies every time, errors increase. If the system can present the correct tasks, forms, references, and sign-off chain based on model and configuration, execution becomes more consistent and easier to audit.

    Tracking Parts, Findings, and Approvals at Tail-Number Level

    Serial tracking from installed configuration to shop and back

    Tail-number-level maintenance execution depends on serial traceability across removal, induction, shop processing, and reinstallation or return to stock. The MES should connect the installed configuration of the aircraft or engine to the serialized article entering the shop, then maintain that identity through every work step.

    For line replaceable units, modules, and piece-parts, the level of granularity may vary by process, but the principle is the same: the maintenance history should show where the item came from, what happened to it, and what its resulting status became. This is especially important when parts move between internal cells and external suppliers before coming back into the repair chain.

    Recording findings, repairs, and replaced components

    Findings are the operational heartbeat of MRO. The MES should let inspectors and technicians record defect types, locations, measurements, reference criteria, and disposition pathways in a structured way. It should also capture what repair was performed, what replacement component was installed, and whether additional inspections were required as a result.

    Structured findings data is valuable beyond the individual work order. It supports trend analysis across fleets, operators, component families, and repair events. Over time, this can help quality and reliability teams identify recurring defects, refine maintenance planning assumptions, and adjust stocking or subcontractor strategies.

    Capturing digital signatures for return-to-service

    Return-to-service and release-related approvals require disciplined control. While the exact approval process depends on the organization and applicable rules, the execution system should support role-based electronic signatures, review of open discrepancies, verification of completed tasks, and confirmation that required records are attached before release documentation is finalized.

    The goal is not to automate airworthiness judgment. The goal is to ensure that authorized personnel have a complete digital package to review and approve, with clear evidence of who performed the work, who inspected it, and whether all required steps were completed before release.

    Connect981 as an MRO Execution and Coordination Layer

    Integrating airline systems, ERP, and shop tooling

    Most repair stations do not operate from a single system. Planning may live in ERP or airline maintenance software, technical data may come from OEM portals, calibration and quality records may sit elsewhere, and shop equipment may generate its own files. Connect981 can act as the coordination layer that brings these inputs into a controlled execution workflow.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for MES for Aerospace MRO: Managing

    That makes it possible to manage work packages, route inspections, capture technician activity, record findings, and return completion data to upstream systems without depending on paper travelers. In practical terms, the platform can support the handoff between planning, execution, quality, and documentation rather than forcing each function to maintain separate manual logs.

    Example: engine overhaul shop with multiple OEM manuals

    Consider an engine overhaul environment servicing multiple models with different manual sets, inspection thresholds, and subcontracted special processes. A conventional one-size-fits-all route often leads to side spreadsheets and exception handling outside the system. Connect981 can instead organize the workscope by module and serial, present the applicable workflow path, and capture findings and approvals at each stage.

    When a component moves out for coating, machining, or NDT, the execution record can remain open and visible. When it returns, the system can verify receipt, attach the supplier documentation, and release the next operation only after required review. That improves continuity across the full repair chain.

    Supplier and subcontractor visibility across repair chains

    MRO execution often depends on subcontractors for specialized repair or processing. Without a connected execution layer, components disappear into email threads until they come back. By treating supplier handoffs as part of the controlled workflow, organizations can track shipment status, expected return, received documentation, and downstream readiness.

    This matters operationally because turnaround time is frequently constrained by waiting, not wrench time. Better visibility into external processing helps planners identify bottlenecks earlier and gives quality teams a cleaner chain of evidence for outside work incorporated into the final release package.

    KPIs and Continuous Improvement for MRO MES

    Turnaround time, findings rate, and rework rate

    The best MRO metrics start with execution reality, not only schedule promises. Turnaround time should be measured at meaningful levels such as overall visit, module, and major process segment. Findings rate helps reveal whether induction assumptions are realistic. Rework rate indicates whether repairs, inspections, or documentation controls are breaking down and causing loops.

    Because the MES records work progression step by step, these KPIs can be based on actual event timestamps and status changes rather than manual estimates. That gives operations leaders a more reliable basis for capacity planning and workflow redesign.

    Trend analysis on recurring defects by fleet or operator

    Tail-number and operator-linked data become especially valuable when aggregated. If a repair station sees recurring damage modes on a specific fleet type, route region, or operator maintenance program, that pattern can inform spares planning, inspection readiness, and engineering feedback. The same applies to recurring supplier escapes or subcontractor-related returns.

    Structured MES data turns isolated repair records into a usable reliability dataset. Even when the system is not the formal reliability platform, it can provide the execution evidence needed to support those analyses.

    Using MES data to refine maintenance programs

    Over time, digital execution data can help organizations improve how they plan and perform maintenance. Shops may adjust standard work packages, improve teardown sequencing, pre-stage likely replacement parts, or tighten routing controls around known problem areas. The value is practical: fewer surprises, faster release preparation, and better alignment between planned and actual work.

    For aerospace MRO, that is the real promise of MES. It is not just digitizing shop paperwork. It is creating a controlled execution environment where tail-number-specific maintenance, findings-driven repairs, part traceability, and release readiness can be managed in one connected workflow.

  • KPI Governance with ISO 22400: Roles, Rules, and Routines

    KPI Governance with ISO 22400: Roles, Rules, and Routines

    ISO 22400 gives manufacturers a shared vocabulary for key performance indicators (KPIs). KPI governance decides how that vocabulary is used, who can change it, and how definitions stay consistent across plants, business units, and systems.

    This article explains how to build an ISO 22400–aligned KPI governance framework that is practical, lightweight, and transparent. The focus is on organizational practices (roles, processes, and documentation), not on any specific technology or software stack.

    Why KPI Governance Matters in Multi-Site Manufacturing

    As plants digitize and more stakeholders gain access to performance dashboards, the number of metrics can explode. Without governance, the same label may mean different things in different places, and seemingly similar metrics may be calculated differently.

    The risks of uncontrolled KPI proliferation

    • Inconsistent definitions: One site measures “availability” including setup time; another excludes it. Both report a single percentage under the same name.
    • Duplicated metrics: Slightly different formulas are introduced for similar KPIs, multiplying dashboards without improving insight.
    • Hidden assumptions: Local spreadsheets and reports embed undocumented business rules that nobody else can see or audit.
    • Integration overhead: IT teams must constantly translate between plant-specific definitions when building group reports or integrating new systems.

    Impact on decision quality and trust in numbers

    When people discover that two plants use different definitions for supposedly identical KPIs, trust erodes quickly. Common symptoms include:

    • Management running parallel analyses to “verify” reported performance.
    • Endless debates over which numbers are correct instead of what actions to take.
    • Plants resisting corporate dashboards because they do not recognize the definitions.

    A governance framework does not automatically improve performance, but it does make performance information reliable enough to support decisions.

    How ISO 22400 provides a stable vocabulary

    ISO 22400 offers a neutral, standardized language for manufacturing operations KPIs. It defines concepts such as availability, utilization, equipment states, time categories, and order-related performance in a technology-agnostic way.

    By aligning governance with the ISO 22400 manufacturing KPI definition framework, organizations can:

    • Start from published, consensus-based definitions instead of inventing everything from scratch.
    • Make data integration easier between MES, ERP, historians, and reporting tools.
    • Clarify which KPIs are standardized and which are organization-specific.

    Defining Governance Roles and Responsibilities

    Clear ownership is the foundation of KPI governance. Every KPI should have someone who is accountable for its definition, and a defined group that can propose changes.

    Central KPI owners vs. local process experts

    A practical pattern for multi-site manufacturers is to separate central ownership from local stewardship:

    • Central KPI owners (often in an operations excellence, manufacturing engineering, or business analytics function) are accountable for:
      • Maintaining the canonical definition aligned with ISO 22400 where applicable.
      • Approving or rejecting change requests.
      • Ensuring documentation stays complete and up to date.
      • Coordinating across sites when a definition change has broad impact.
    • Local process experts (plant engineers, production supervisors, maintenance leads) act as stewards who:
      • Validate whether the KPI is meaningful and applicable locally.
      • Identify issues with data availability or interpretation on the shop floor.
      • Propose refinements or additional indicators to capture local realities.

    This split keeps definitions coherent at the group level while still grounding them in operational reality.

    Involving IT, operations, and finance

    ISO 22400 KPIs touch multiple functions. A robust governance model usually involves three perspectives:

    • Operations: Ensure that the KPI reflects how production, maintenance, and quality are actually managed day to day.
    • IT / data engineering: Confirm that required data exists, can be collected reliably, and can be processed at the needed latency and granularity.
    • Finance / controlling: Align operational KPI definitions with how performance is reported at higher levels without confusing operational indicators with financial results.

    Many organizations formalize this collaboration in a cross-functional KPI steering group or data governance council that meets regularly to review requests and issues.

    Decision rights for adding or changing KPIs

    To avoid ad-hoc changes, define explicit decision rights:

    • Who can propose: Typically any plant or function can raise a request for a new KPI or a change in definition.
    • Who can recommend: A working group of subject-matter experts assesses the proposal, its ISO 22400 alignment, and technical feasibility.
    • Who can decide: Central KPI owners or a governance board approve, defer, or reject changes, considering network-wide impact.

    Documenting these rights reduces friction and ensures that no single site can unilaterally redefine a shared KPI.

    Documenting KPIs Using ISO 22400 Concepts

    Without structured documentation, governance becomes informal and dependent on tribal knowledge. ISO 22400 suggests a rich set of attributes that can be reused in your internal KPI catalog.

    Using standardized attributes and terminology

    For each KPI, capture a minimum set of attributes, reusing ISO 22400 concepts where they apply:

    • Name: A unique label, ideally reflecting ISO 22400 terminology.
    • Conceptual definition: A plain-language explanation of what the KPI measures, not just its formula.
    • Scope / object of measurement: Work unit, line, area, plant, or order, aligned with the standard’s hierarchy.
    • Domain: Production, quality, maintenance, inventory, or energy.
    • Time behavior: Whether it is real-time, per shift, daily, weekly, etc.
    • Underlying states and quantities: Which equipment states, time buckets, and material quantities feed into the KPI.
    • Unit of measure and direction: Percentage, hours, units produced, with a clear statement of whether “more is better” or “less is better.”
    • ISO 22400 linkage: References to the standardized concept (for example, “Aligned with ISO 22400 availability indicator”).
    • Data source: Systems or sensors that provide the input data.
    • Owner and stakeholders: Who is accountable for the definition and who uses it.

    Clarify the operational risk

    When the work behind KPI Governance with ISO 22400 affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in KPI Governance with ISO 22400

    Creating a centralized KPI catalog or dictionary

    A centralized KPI catalog (sometimes called a KPI dictionary or data catalog entry for KPIs) makes these definitions discoverable and auditable. It may be implemented as:

    • A specialized data catalog tool.
    • An internal web portal with search and filters.
    • A governed spreadsheet or database with controlled access.

    Key success factors include:

    • Assigning responsibility to keep entries current whenever dashboards or data models change.
    • Ensuring that business users can easily navigate by plant, domain, or role.
    • Linking catalog entries to report and dashboard metadata so that users can jump from a chart to its definition.

    Marking which KPIs are ISO 22400-based

    Not every KPI will or should be ISO 22400-based. To avoid confusion:

    • Tag ISO 22400-aligned KPIs explicitly in the catalog (for example, a boolean flag or a specific category).
    • Record any deviations from the standard definition, such as additional filters or modified scope.
    • Use consistent naming conventions so that standardized KPIs are easy to recognize in reports.

    This clarity helps teams distinguish between standardized, comparable KPIs and locally defined indicators designed for specialized needs.

    Change Management for KPI Definitions

    Once KPIs become embedded in reports, incentives, and supplier contracts, changing a definition can have significant consequences. ISO 22400 provides a stable foundation, but your own definitions will still evolve as operations change.

    Assessing impact of KPI changes

    Before modifying a KPI definition, governance should consider:

    • Systems affected: Which dashboards, reports, alerts, and integrations consume this KPI?
    • Stakeholders impacted: Which plants, teams, and external partners use it in their decision-making?
    • Historical comparability: Will the change break trend analysis or contractual baselines?
    • Standard alignment: Does the proposed change move the KPI closer to or further from ISO 22400 concepts?

    Simple change templates or checklists make this assessment repeatable and auditable.

    Versioning and communication practices

    To keep trust in KPIs, treat definition changes like software releases:

    • Version numbers: Assign a version to each KPI definition; increment it whenever the meaning changes, not just the visualization.
    • Effective dates: Record when the new version takes effect, so data can be interpreted correctly over time.
    • Change logs: Maintain a concise history explaining why each change was made and who approved it.
    • Communication plans: Inform affected users in advance, including what will change, why, and how to interpret trends across the change.

    Managing coexistence during transitions

    In some cases, the old and new definitions must coexist for a period. Common strategies include:

    • Dual reporting: Show both the legacy KPI and the new one on the same dashboard, clearly labeled, for a defined transition period.
    • Back-calculation where feasible: If raw data allows, compute the new definition for past periods to maintain continuous trend lines, while documenting that the series was recalculated.
    • Cutover points in reports: Mark the date when the definition changed on historical charts.

    The goal is transparency: users should never be surprised by unexplained jumps in KPI values.

    Embedding Governance into Tools and Workflows

    Governance works best when it is built into everyday tools and processes instead of relying on manual policing. While ISO 22400 is technology-agnostic, its concepts can be enforced through configuration and automation.

    Using platforms like an ISO 22400 KPI definition framework to enforce definitions

    If you use a centralized platform for manufacturing performance reporting or a dedicated KPI management tool, you can configure it around ISO 22400 concepts:

    • Define canonical formulas and scopes aligned with ISO 22400 in a single place.
    • Expose standardized KPIs as reusable building blocks for dashboards and plants.
    • Integrate the platform with your KPI catalog so that users can click through from a chart to its official definition.

    Roles-based access to KPI configuration

    Roles and permissions in reporting and analytics tools should reflect governance rules:

    • Configuration roles: Only designated owners or administrators can edit standardized KPI definitions.
    • Local extension roles: Sites can create plant-specific indicators, but must label them clearly and cannot overwrite global definitions.
    • Viewer roles: Most users consume KPIs but cannot change underlying definitions.

    This division enables local flexibility without sacrificing global consistency.

    Automated checks to prevent duplicate or conflicting KPIs

    Tools can support governance by detecting issues early:

    • Name uniqueness checks: Prevent new KPIs from using names already assigned to existing indicators.
    • Similarity checks: Flag definitions that are nearly identical to existing KPIs, prompting consolidation.
    • Metadata completeness rules: Require key attributes (unit, owner, ISO 22400 alignment flag) before a KPI can be published.
    • Approval workflows: Route new or changed KPI definitions for review before they appear in production dashboards.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for KPI Governance with ISO 22400

    Measuring the Success of KPI Governance

    Governance itself should be monitored. While ISO 22400 defines operational KPIs, you can create a small set of governance health indicators to see whether your KPI management practices are working.

    Indicators of improved comparability and trust

    Signs that governance is effective include:

    • Reduction in ad-hoc metrics: Fewer locally defined KPIs that duplicate or conflict with group standards.
    • Stable definitions: Core KPIs change infrequently and, when they do, changes are properly documented.
    • Fewer disputes over numbers: Less time spent reconciling reports across sites and more time spent on root-cause analysis and improvement ideas.
    • Simpler system integration: New plants or systems can be onboarded using existing KPI definitions with minimal translation work.

    Feedback loops from plant teams and management

    Governance should be a living process, not a one-time project. To keep it relevant:

    • Solicit regular feedback from plants on whether KPI definitions fit real-world operations.
    • Schedule periodic reviews of the KPI catalog to retire unused indicators and refine ambiguous ones.
    • Track issues raised through support channels or data-quality tickets that relate to KPI meaning or interpretation.

    When feedback results in visible improvements, engagement with governance processes tends to increase.

    Continuously evolving governance as operations change

    As manufacturing strategies, products, and technologies evolve, so will your KPIs. ISO 22400 provides a durable backbone, but your governance model should accommodate:

    • New domains (for example, energy efficiency or advanced traceability) that require additional indicators beyond the standard.
    • New data sources such as IoT sensors or advanced analytics models that enrich existing KPIs.
    • Organizational changes such as plant acquisitions or divestments that affect the set of shared KPIs.

    The aim is not to freeze KPI definitions forever, but to manage change deliberately and transparently.

    Putting It All Together

    ISO 22400 does not prescribe how to govern KPIs, but it offers a clear conceptual foundation. By combining that foundation with practical governance practices — ownership, documentation, change control, and tool support — manufacturers can create a KPI environment that is both comparable across sites and adaptable to local realities.

    A well-run governance framework will not, by itself, improve performance. What it does is ensure that leaders, engineers, and operators share a common understanding of the numbers they use to steer the business. That shared understanding is a prerequisite for meaningful, data-informed improvement across modern manufacturing networks.

    For teams putting this topic into daily operation, ISO 22400 KPI governance, a connected execution platform, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    This article is for aerospace operations, quality, and compliance teams who need to understand KPI Governance with ISO 22400: Roles, Rules, and Routines. It explains the practical question this topic answers in a manufacturing execution context.

    The same operating model also depends on real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    For teams putting this topic into daily operation, ISO 22400 KPI governance help connect the concept to traceability, work-order reality, and audit-ready evidence.

  • ISO 22400 Scope and Limits: Where Strategy Begins and the Standard Ends

    ISO 22400 Scope and Limits: Where Strategy Begins and the Standard Ends

    ISO 22400 gives aerospace manufacturers a shared vocabulary for key performance indicators (KPIs) in manufacturing operations, but it does not decide what “good” looks like in your plant. The standard defines concepts, structures, and naming conventions so that manufacturing data is comparable across systems and sites. Strategy, KPI selection, target-setting, and improvement methods remain the responsibility of each organization.

    This article is for aerospace operations, quality, and compliance teams who need to understand ISO 22400 Scope and Limits: Where Strategy Begins and the Standard Ends. It explains the practical question this topic answers in a manufacturing execution context.

    For aerospace and defense programs operating under AS9100, stringent configuration control, and multi-tier supplier networks, this boundary matters. You can align your data model and KPI semantics with the ISO 22400 manufacturing KPI framework while still tailoring metrics to specific aircraft platforms, engine programs, or space hardware contracts.

    For teams putting this topic into daily operation, scrap and rework reduction, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    The Purposefully Narrow Scope of ISO 22400

    ISO 22400 sits in the automation and integration family of standards. It is designed to let systems exchange performance information consistently, not to act as a performance management handbook. In practice, that means it emphasizes conceptual definitions over management practices.

    Definitions and structures vs. business strategy

    At its core, ISO 22400 defines what a KPI means in the context of manufacturing operations. It clarifies terms such as availability, utilization, work unit, production order, and equipment state. It also describes how KPIs relate to time, quantity, and event data, and where in the enterprise hierarchy they typically apply (work unit, line, area, site).

    For an aerospace factory, this definitional layer becomes part of the digital thread. When a manufacturing execution system (MES), an ERP, and a quality system all use the same ISO 22400 definition of "equipment utilization" or "order execution reliability," KPI values remain comparable from a composite layup cell to a final assembly line, and across prime-supplier boundaries.

    What ISO 22400 does not do is define your business strategy. It does not state that utilization is more important than schedule adherence for a given engine program, or that quality-related KPIs must carry more weight than throughput in a space hardware test facility. Those priorities are driven by contract risk, safety, regulatory expectations, and portfolio strategy.

    Why the standard avoids prescriptive KPI sets

    The standard includes a set of KPIs that are common across manufacturing, but it characterizes them as examples and reference concepts, not as a mandatory list. This is deliberate. A rigid KPI catalog would fit poorly across the diversity of aerospace operations—from composite fabrication and avionics assembly to engine overhaul and satellite integration.

    By remaining neutral, ISO 22400 lets a single platform support:

    • High-mix, low-volume prototype lines for new flight hardware.
    • Rate-driven production of mature aircraft components.
    • Maintenance, repair, and overhaul (MRO) shops with turn-time constraints and stringent traceability.
    • Space system integration facilities with long-duration test campaigns.

    The standard ensures shared meaning where concepts overlap, but expects each organization to extend or specialize the KPI set to reflect its aerospace-specific realities.

    What ISO 22400 Does Not Standardize

    The clearest way to understand ISO 22400 is to list what it intentionally leaves out. These omissions are not gaps; they are boundaries.

    KPI selection, thresholds, and targets

    ISO 22400 helps you define KPIs correctly, but it does not tell you which KPIs you must track. Selecting metrics is a strategic exercise that depends on product risk, customer contracts, and regulatory context. For example:

    • A flight-control electronics line may prioritize first-pass yield, defect density per configuration item, and rework cycle time.
    • A composite wing box cell may elevate cure cycle utilization, autoclave availability, and nonconformance rate per panel.
    • An engine MRO line may center on turnaround time, work scope stability, and findings per shop visit.

    Similarly, ISO 22400 does not define target values or alert thresholds. What counts as acceptable equipment utilization, schedule adherence, or scrap rate differs dramatically between prototyping and rate production, and between structural components and non-flight ground equipment.

    Targets are shaped by:

    • Contractual obligations and service levels.
    • Certification and airworthiness considerations.
    • Risk appetite and safety margins.
    • Capital allocation and capacity plans.

    The standard provides the KPI structure that you monitor against, but the "green/yellow/red" bands and escalation logic are defined by your own governance processes.

    Improvement methodologies and incentive systems

    ISO 22400 is not a continuous improvement framework. It does not describe how to interpret a declining OEE trend, how often to hold performance reviews, or how to design your daily management system. It stays neutral on whether you use lean, Six Sigma, theory of constraints, or internal methodologies.

    Clarify the operational risk

    When the work behind ISO 22400 Scope and Limits affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in ISO 22400 Scope and Limits

    It also does not specify how KPIs should feed into incentive programs. For aerospace manufacturers, that boundary is important: tying bonuses directly to high-level KPIs without careful design can push teams toward behaviors that conflict with safety or compliance—for example, prioritizing throughput at the expense of rigorous configuration control. ISO 22400 leaves these choices to your leadership and HR policies; it only ensures that the data you base them on is consistently defined.

    Handling Context-Dependent KPI Choices

    Within aerospace and defense, context shifts quickly across programs and facilities. ISO 22400 acknowledges this by avoiding context-specific prescriptions. You must map its neutral definitions into your particular operating environment.

    Discrete vs. process industries in aerospace

    Many aerospace factories blend discrete and process characteristics. A composites facility may run autoclave cures (process-like), then trim and drill individual parts (discrete). ISO 22400 supports both kinds of behavior at the conceptual level: time states, order-related time structures, and quantity-based indicators can all apply.

    However, you choose where to emphasize which KPIs. In a resin transfer molding line, cure time conformance and equipment state distribution may dominate. In avionics box assembly, order cycle time, WIP aging, and test yield may be more informative. The standard does not rank these for you; it simply gives you consistent language to capture them.

    Regulated domains like aerospace and pharma

    Highly regulated sectors such as aerospace, defense, and pharmaceuticals share concerns about traceability, documentation, and validation, yet ISO 22400 remains industry-neutral. It does not encode AS9100 requirements, FAA/EASA expectations, or export control constraints.

    For an AS9100-compliant organization, that means you overlay regulatory and customer requirements onto the ISO 22400 framework. For example:

    • You might extend order execution KPIs with metrics for inspection coverage, quality escape rate, or the proportion of operations executed under approved digital work instructions.
    • You may track the latency between a detected nonconformance and containment actions, or between engineering change release and production adoption.

    These are critical performance dimensions in aerospace, but they sit on top of, not inside, the ISO 22400 core concepts.

    Granularity, Aggregation, and Reporting Decisions

    ISO 22400 describes how KPIs can exist at multiple levels of the manufacturing hierarchy. It does not dictate which level is appropriate for which audience or decision.

    Selecting levels (work unit, line, plant) per decision-maker

    The standard aligns with hierarchy notions similar to enterprise, site, area, work center, and work unit. In aerospace operations, these are often mapped to:

    • Work unit: a specific CNC machine, autoclave, test stand, or build station.
    • Work center or line: a composite cell, harness assembly line, or engine module line.
    • Area or site: a building, program-focused hall, or entire plant.

    ISO 22400 allows KPIs to be defined at any of these levels but does not specify which level a given role must use. In practice:

    • Cell leads may need work-unit-level availability and short-interval control metrics.
    • Program managers may prefer line- or area-level schedule adherence and capacity utilization.
    • Executive leadership often uses site-level productivity, on-time delivery, and quality indicators.

    Your reporting design decisions—what detail to expose to whom—are outside the standard’s scope, even though it underpins the metrics themselves.

    Choosing time buckets and aggregation rules

    ISO 22400 is explicit about time-related behavior (e.g., whether a KPI is point-in-time, shift-based, or period-aggregated), but it doesn’t tell you which time buckets to use for managing your aerospace plant. You decide whether to aggregate by shift, day, week, or program milestone, and how to roll up across shifts that span calendar days.

    Similarly, the standard does not prescribe how to aggregate across heterogeneous resources. For instance, combining utilization for a bank of test stands with different capabilities and maintenance regimes is a modeling choice. You might weight by criticality, capacity, or program relevance; ISO 22400 simply ensures that the underlying utilization concept is consistently defined before aggregation.

    Combining ISO 22400 with Domain-Specific Metrics

    Aerospace manufacturers cannot operate solely on generic production metrics. They need KPIs that reflect traceability, configuration control, and safety-critical quality performance. ISO 22400 is designed to coexist with these domain-specific metrics rather than replace them.

    Aerospace traceability and MRO turnaround KPIs

    Traceability metrics are central in aerospace but not explicitly modeled in ISO 22400. Examples include:

    • Coverage of part genealogy data for serialized components and assemblies.
    • Time to achieve full digital sign-off across all required operations on a work order.
    • Percentage of parts with complete material, process, and inspection provenance attached to the digital thread.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for ISO 22400 Scope and Limits

    For MRO operations, turnaround-time KPIs may break down total elapsed time into waiting-for-parts, waiting-for-engineering, teardown, inspection, repair, test, and paperwork segments. These draw on ISO 22400 time-structure ideas but are tuned to MRO realities and contract penalties.

    In both cases, ISO 22400 provides reusable building blocks such as order states and time categories, while specialized KPIs capture the aerospace-specific concerns.

    Energy, sustainability, and ESG-related metrics

    Space and defense programs increasingly track energy use, emissions, and resource efficiency, whether for internal commitments or customer reporting. ISO 22400 includes generic energy-related indicators, but it does not define a complete ESG reporting model. You may need to extend your KPI framework to cover:

    • Energy per test hour on thermal vacuum chambers or engine test stands.
    • Scrap and rework rates expressed as material mass or embodied carbon per flight-critical assembly.
    • Resource utilization for specialized, high-energy processes such as large autoclave cycles.

    These metrics often combine ISO 22400 production indicators with sustainability data in your data warehouse. The standard remains a definitional anchor, not the full solution.

    Using ISO 22400 as a Foundation for Custom KPI Frameworks

    The most effective use of ISO 22400 in aerospace manufacturing is as a stable foundation for a tailored KPI framework rather than as the framework itself. This involves careful use of standardized terminology and transparent documentation of what is, and is not, ISO 22400-aligned.

    Building on standardized terminology

    When designing KPI catalogs for an aerospace plant or multi-site network, using ISO 22400 terms where possible reduces ambiguity. For example:

    • Base equipment utilization, availability, and performance KPIs on ISO 22400 definitions for time states and operating time.
    • Align order-related KPIs with the standard’s view of planned vs. actual time structures for production orders.
    • Reuse standard attributes (units of measure, trend direction, applicability) in KPI specifications.

    On top of these, define aerospace-specific KPIs such as "nonconformances per 1,000 flight-critical operations," "digital work instruction adherence," or "configuration change adoption lag." These draw from ISO 22400 concepts but extend them to cover your AS9100 and program needs.

    Documenting what is and is not ISO 22400-aligned

    As the KPI set grows, it becomes important—especially in a connected ecosystem of OEMs and suppliers—to distinguish between metrics that directly follow ISO 22400 and those that are custom. Practical steps include:

    • Tag each KPI in your catalog with an attribute that indicates whether it is fully, partially, or not aligned with ISO 22400.
    • Provide traceability from custom KPIs back to the underlying standard concepts they reuse (e.g., based on ISO 22400 equipment busy time).
    • Clarify definitions in data dictionaries and interface specifications so that suppliers and partners know which metrics can be interpreted via the standard.

    Platforms like Connect 981 can help enforce this discipline: the data model can encode ISO 22400 semantics for core KPIs while allowing program-specific measures to coexist, clearly labeled as extensions. This approach maintains comparability where it matters—such as equipment effectiveness across multiple plants—without constraining the nuanced performance views required by aerospace engineering and quality teams.

    Implications for Digital Manufacturing Infrastructure

    In a modern aerospace production environment, ISO 22400 acts as a semantic layer across MES, ERP, PLM, QMS, historian, and analytics systems. It standardizes the language, but the architecture and workflows are designed by you.

    When building or evolving a digital manufacturing infrastructure, understanding ISO 22400’s limits helps avoid two risks: expecting the standard to answer strategic questions it was never meant to address, and designing bespoke KPI definitions where standard ones already exist.

    By treating ISO 22400 as a foundational reference, aerospace organizations can integrate heterogeneous systems, maintain consistent KPI semantics across a global supply chain, and still exercise full control over strategy, KPI selection, targets, and improvement practices.

  • Integrating Non-Conformance Management With ERP and MES in Aerospace

    Integrating Non-Conformance Management With ERP and MES in Aerospace

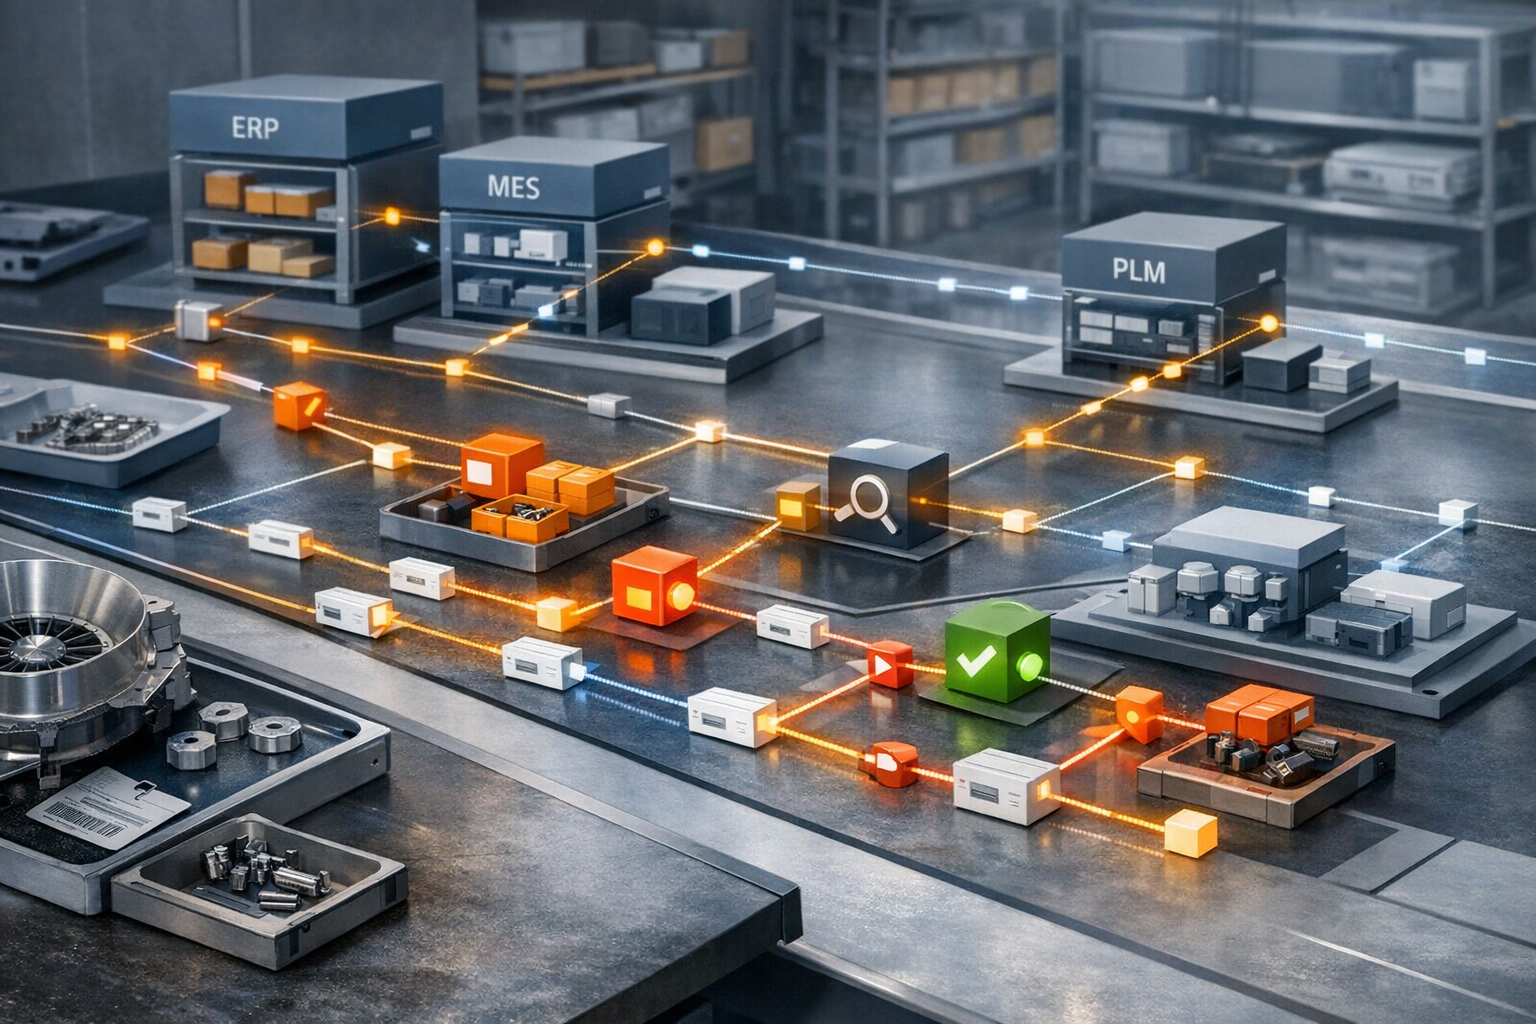
    In aerospace manufacturing and MRO, non-conformance reports (NCRs) do not live in a vacuum. Every quality decision affects production schedules, inventory availability, cost accounting, and—ultimately—flight safety. When NCR workflows are disconnected from enterprise resource planning (ERP) and manufacturing execution systems (MES), organizations end up with blind spots, double entry, and conflicting data that erode both efficiency and compliance.

    Integrating non-conformance management with ERP and MES creates a single coherent story across work orders, inventory, and quality records. Done well, it lets teams see—within minutes—what material is affected, which operations are blocked, what the cost impact is, and when a line can restart. Done poorly, it introduces new failure modes, data inconsistencies, and audit risks.

    For teams putting erp / mes / plm interoperability into daily operation, data mapping and system interoperability, MES execution control, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on ERP, MES, and PLM integration paths, quality management workflows, a connected execution platform, Connect 981’s aerospace execution solutions, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains how to integrate non-conformance management with ERP and MES in aerospace environments. It focuses on key data flows, typical integration scenarios, and design considerations that support reliability, traceability, and regulatory compliance.

    For a broader view of process design before you tackle integration, see our guide on integrated aerospace quality workflows.

    Why NCR Integration With ERP and MES Matters

    Aerospace organizations often start with quality-managed NCRs in a standalone system or spreadsheet. Over time, they discover that almost every disposition decision requires data held elsewhere: work order status in MES, inventory balances in ERP, contract requirements in a customer portal, and so on. Integration closes these gaps.

    Linking quality events to work orders and routings

    When an inspector raises an NCR, they usually do it in the context of a specific job: a work order, operation, or task. If your NCR system is not tied to ERP and MES, you immediately face problems:

    • Ambiguous context: NCRs reference work orders or operations via free-text fields, increasing the risk of mis-typed IDs and mislinked records.
    • Lost history: Planners and engineers viewing work orders in ERP or MES cannot see associated NCRs without separate searches.
    • Inconsistent status: A work order may look released and executable in MES even though a critical NCR is still open in the quality system.

    Integration solves this by ensuring each NCR is anchored to authoritative production data:

    • The NCR record references the exact work order, operation, operation sequence, and resource from MES/ERP.
    • Work order screens show links or badges indicating open NCRs and their dispositions.
    • Routings and travelers reflect holds or additional steps (e.g., rework operations) derived from NCR decisions.

    Accurate inventory, WIP, and cost accounting

    Every NCR disposition—rework, scrap, or use-as-is—affects quantities and costs. Without integration, these updates depend on manual re-keying into ERP, which is slow and error-prone.

    Key impacts that should be automated via integration include:

    • Inventory balances: Moving parts to quality hold, returning them to stock, scrapping them, or issuing replacements.
    • WIP (work in process): Adjusting WIP quantities when assemblies are partially scrapped or reworked.
    • Cost allocation: Capturing labor, material, and overhead associated with rework or scrap to the right cost centers, work orders, or projects.
    • Customer or contract impacts: Flagging costs that must be charged to a specific program, contract line item, or warranty account.

    With integrated systems, an approved disposition in the NCR workflow can automatically trigger the right ERP transactions—such as inventory adjustments, additional operations, or cost postings—removing the need for duplicate data entry.

    Real-time impact assessment for production planning

    Production planners, schedulers, and program managers need to answer questions such as:

    • How many assemblies are blocked by quality holds?
    • Which lines are at risk if this NCR leads to scrap instead of rework?
    • Do we have enough conforming material to meet this week’s ship dates?

    When NCR, ERP, and MES data are synchronized, planning tools can show the impact of quality events in real time:

    • Work orders and operations affected by open NCRs are clearly visible in planning boards.
    • Inventory availability calculations reflect parts under quality hold.
    • Scenario planning can incorporate potential scrap rates or extended lead times driven by rework.

    Core Data Elements Shared Across Systems

    Successful integration starts with a precise understanding of which data elements are owned by which system—and how they should be referenced in NCR workflows.

    Parts, serial numbers, and configuration baselines

    Aerospace quality decisions hinge on precise identification of parts and configurations. Typical shared elements include:

    • Part and assembly identifiers: Part numbers, revisions, and descriptions managed in ERP/PLM.
    • Serial/lot/batch numbers: Unique identifiers needed for traceability to specific aircraft, engines, or line-replaceable units.
    • Configuration baselines: Which drawing revision, bill of material (BOM), and process specification applied when the unit was built or serviced.

    From an integration standpoint, your NCR system should never maintain its own “shadow” master list of parts or serials. Instead, it should reference authoritative master data from ERP and, where applicable, PLM or configuration management systems.

    Work orders, operations, and resources

    Most NCRs relate to an execution context, which lives primarily in MES and/or ERP:

    • Work orders / shop orders: Job identifiers, quantities, due dates, and related projects or contracts.
    • Operations / tasks: Routing steps, standard work instructions, and inspection operations.
    • Resources: Machines, tools, and cells, plus the operators or technicians executing the work.

    Integrating non-conformance management with ERP and MES means NCR records can:

    • Automatically pull in the correct work order and operation when raised from an MES screen.
    • Associate resource usage (machine, fixture, tool) with the deviation to support root cause analysis.
    • Feed back rework operations or additional inspections into routings as part of approved dispositions.

    Suppliers, customers, and contracts

    External stakeholders are a critical part of aerospace non-conformance management:

    • Suppliers: Vendor IDs, purchase orders, delivery notes, and certificates of conformity.
    • Customers: Contract references, customer-specific quality clauses, and deviation permit processes.
    • Regulatory and contractual constraints: Requirements for notification, approval workflows, and retention periods.

    Quality systems must use supplier and customer master data from ERP/CRM to ensure that notifications, charge-backs, and reporting align with commercial agreements. For example, an NCR against incoming material should be directly linked to the originating PO and supplier record, not just recorded via free text.

    Typical Integration Scenarios

    Most aerospace organizations converge on a handful of common NCR–ERP–MES integration patterns. The specifics vary, but the underlying scenarios are remarkably consistent.

    Creating NCRs from ERP/MES context

    The most visible integration requirement is the ability to launch an NCR from within ERP or MES while preserving context:

    • Inspector in MES identifies a defect during an in-process check and raises an NCR against the current operation.
    • Receiver in ERP identifies a discrepancy at incoming inspection and triggers an NCR from the purchase order or receipt line.
    • Planner finds a documentation error on a work order and opens an NCR tied to that job.

    Key design choices include:

    • Single sign-on and deep links: Users click a button in MES/ERP and are taken directly to a pre-populated NCR form.
    • Pre-filled data: Work order IDs, part numbers, operations, and supplier/customer data are automatically copied from ERP/MES into the NCR.
    • Bidirectional references: The NCR stores the originating ERP/MES keys, and the ERP/MES record stores a link or reference back to the NCR.

    Applying holds and releases in inventory and WIP

    Once an NCR is raised, the organization must prevent suspect material from advancing. Integration enables this without manual phone calls or emails:

    • Inventory holds: An NCR on incoming material automatically sets the relevant lots or serials to a quality-hold status in ERP.
    • WIP holds: Open NCRs against certain work orders or operations can block movement to the next operation in MES.
    • Release logic: When an NCR is dispositioned and containment is verified, the integration can remove holds or redirect units to rework operations.

    Design considerations:

    • Define which system is the system of record for hold/release status (often ERP for stock, MES for WIP).
    • Ensure that NCR workflows cannot close without confirming that physical inventory/WIP status has been updated.
    • Provide clear visibility in ERP/MES screens when a part or job is on hold because of an NCR.

    Posting rework, scrap, and use-as-is decisions

    Disposition drives financial and operational outcomes. Integration should translate quality decisions into concrete ERP and MES transactions:

    • Rework: Create or modify operations in MES, issue additional materials, and capture labor hours against rework tasks.
    • Scrap: Post scrap transactions in ERP to remove inventory/WIP and book the cost to the appropriate account or project.
    • Use as-is / deviation: Record engineering approvals in the NCR system and, where required, update configuration or as-built records in ERP/MES.

    These postings should be as automated as practical, based on pre-defined mapping between disposition codes and ERP/MES transactions. At the same time, aerospace organizations must ensure that IT and compliance teams review any automation to verify it meets internal control requirements.

    Technical Integration Approaches

    No single integration pattern is universally correct. The right design depends on your existing architecture, vendor capabilities, regulatory expectations, and internal IT standards. Most aerospace companies mix several of the approaches below.

    APIs, middleware, and event-driven workflows

    Modern NCR, ERP, and MES platforms often expose REST or SOAP APIs and can publish or consume events. Typical choices include:

    • Direct API integrations: NCR application calls ERP/MES APIs (or vice versa) to retrieve master data and post transactions.
    • Middleware / ESB: An integration layer orchestrates data flows, transforms payloads, and centralizes error handling.
    • Event-driven architecture: Systems publish business events (e.g., “NCRCreated”, “NCRDispositioned”) to a message bus, and subscribers react by updating their own data stores.

    Event-driven designs can reduce coupling and improve scalability but require robust monitoring and governance to avoid silent failures.

    Data mapping and master data management

    Technical plumbing alone is not enough. You must define consistent semantics across systems:

    • Standardized codes for dispositions, defect types, causes, and corrective actions.
    • Common identifiers for parts, customers, suppliers, and resources.
    • Clear ownership rules for who can create or change master data and how those changes propagate.

    Master data management (MDM) practices help here. Whether you use a dedicated MDM tool or governance processes around ERP, the goal is to ensure that all systems refer to the same business objects in the same way.

    Handling offline and multi-site environments

    Aerospace operations often span multiple plants, test facilities, and field locations—some with intermittent connectivity. Integration designs should account for:

    • Local capture: Ability to record NCRs offline on tablets or local systems, then synchronize when connectivity is restored.
    • Latency-aware behavior: Clear rules about what actions can proceed without immediate confirmation from ERP/MES (e.g., temporary local holds vs. enterprise-wide stock status changes).
    • Site-specific variations: Different ERPs or MES instances at different plants, with a central quality system or vice versa.

    For multi-site environments, consider patterns such as hub-and-spoke integration, regional middleware instances, or phased rollouts that allow each site to stabilize before expanding the footprint.

    Designing for Reliability and Traceability

    In aerospace, an integration that “usually” works is not good enough. Systems must support rigorous traceability, predictable behavior under failure, and clear audit trails.

    Error handling and reconciliation

    Integration errors will occur: network timeouts, data validation failures, or mismatched identifiers. Designing for reliability means:

    • Idempotent operations: Replaying integration messages without creating duplicate transactions.
    • Queued retries: Automatic retries for transient failures with backoff policies.
    • Dead-letter handling: A controlled queue or worklist for messages that cannot be processed automatically.
    • Reconciliation reports: Periodic checks comparing key fields (e.g., hold statuses, scrap quantities) across systems to detect drifts.

    Audit trails across system boundaries

    Regulators and customers expect you to prove not only what decisions were made, but also how those decisions flowed through your systems. Practical measures include:

    • Storing correlation IDs that link NCR records to ERP/MES transactions.
    • Logging which integration process invoked which API, with timestamps and outcomes.
    • Ensuring that any automated changes (e.g., inventory status updates from an NCR decision) are traceable to the originating NCR and user.

    These capabilities simplify audits by showing a clear, end-to-end chain from defect discovery through disposition, execution, and financial posting.

    Change management and regression testing

    As processes, systems, and regulations evolve, integrations must change. Before deploying modifications:

    • Use representative test data that includes critical cases (serialized parts, safety-critical items, customer-specific rules).
    • Run end-to-end regression tests that validate not just data movement but also business outcomes (e.g., holds applied, costs posted correctly).
    • Involve quality, production, finance, and compliance stakeholders in sign-off.

    IT and compliance teams should jointly agree on the level of validation required for each type of integration change, especially where it may impact regulatory evidence or financial postings.

    Governance and Continuous Improvement

    NCR–ERP–MES integration is not a one-time project. As product lines, suppliers, customers, and regulations change, so do integration requirements. Governance keeps the solution aligned with the business.

    Defining ownership for integrated processes

    Clarify who owns what:

    • Process ownership: Quality leaders define how NCR workflows should behave and what data they require.
    • System ownership: IT or application owners manage the configuration and technical integrity of ERP, MES, and quality systems.
    • Integration ownership: An integration architect or team maintains the contracts, data mappings, and monitoring around cross-system flows.

    Having named owners makes it easier to resolve issues, prioritize enhancement requests, and manage change.

    Monitoring data quality and integration KPIs

    Beyond technical uptime, monitor indicators that reveal whether integrated processes actually work for the business. Examples include:

    • Percentage of NCRs created from ERP/MES context versus manual entry.
    • Frequency of mismatches between NCR dispositions and ERP inventory or cost data.
    • Number of integration-related incidents discovered during audits.
    • Mean time to apply holds in ERP/MES after NCR creation.

    These metrics help you identify where integrations need refinement or additional training.

    Iterating integration as business needs evolve

    As you mature, you may:

    • Extend integration to new plants or maintenance depots.
    • Incorporate additional systems (e.g., PLM, supplier portals, or field service tools).
    • Automate more of the NCR lifecycle where risk and internal controls allow.

    Approach this as a continuous improvement program, not a one-time rollout. Regularly revisit your integration design in light of new customer requirements, regulatory interpretations, and internal lessons learned.

    Putting It All Together

    Integrating non-conformance management with ERP and MES is a cornerstone of modern aerospace quality operations. By anchoring NCRs to production, inventory, and financial data, organizations can:

    • Reduce manual data entry and associated errors.
    • Provide real-time visibility into the impact of quality issues.
    • Strengthen traceability from defect detection through disposition and execution.
    • Improve readiness for regulatory and customer audits.

    There is no single blueprint that fits every aerospace organization. The right integration architecture depends on your current systems, regulatory posture, and risk tolerance. What matters most is that IT, quality, production, and finance jointly define how data should flow, validate the design against compliance requirements, and treat integration as a living capability that evolves with the business.

  • Supplier Work Order Coordination in the Aerospace Supply Chain

    Supplier Work Order Coordination in the Aerospace Supply Chain

    When supplier work orders are invisible, on-time delivery becomes guesswork

    Aerospace manufacturers depend on a wide network of suppliers and sub-tiers. Critical components, special processes, and repair activities often happen outside your own walls. Yet in many organizations, supplier work orders become effectively invisible once a purchase order is issued. That is not just a visibility problem. It is an on-time delivery problem.

    This article is for aerospace operations, quality, and compliance teams who need to understand Supplier Work Order Coordination in the Aerospace Supply Chain. It explains the practical question this topic answers in a manufacturing execution context.

    Supplier OTD and Client OTD are two of the most important KPIs in aerospace. Supplier OTD determines whether parts arrive when planned. Client OTD determines whether you deliver aircraft, assemblies, or serviceable assets on schedule. The hard reality is that these KPIs are linked across tiers. When a supplier loses days acknowledging an order, clarifying requirements, or resolving documentation gaps, that delay flows downstream. Your internal schedule compresses, expedites increase, and delivery risk rises.

    For teams putting this topic into daily operation, supplier and supply chain coordination, supply chain and supplier execution, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you manage supplier execution by PDF and email, you are managing OTD by feel rather than by evidence.

    The typical pattern looks like this. ERP issues a PO. A PDF of requirements or a drawing set is attached. The supplier converts those requirements into their own internal work orders and instructions. Weeks later, parts arrive with a packet of certificates and inspection records. If something is late, incomplete, or out of tolerance, you discover it at the receiving dock or later in the build. By then, the schedule impact is already real.

    This disconnect affects more than delivery dates. It weakens traceability. It complicates non-conformance investigation. It leaves program managers guessing how supplier issues will affect complex builds. The internal work order management discipline you may have built does not extend to the external work that your products depend on.

    Clarify the operational risk

    When the work behind Supplier Work Order Coordination in affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in Supplier Work Order Coordination in

    Why supplier portals matter for OTD, not just documentation

    Many people hear “supplier portal” and think of a place to upload documents. That is part of it, but the real operational value is faster acknowledgement, clearer execution alignment, and tighter exception handling. Those three directly improve Supplier OTD, and when Supplier OTD improves, Client OTD becomes easier to protect.

    A supplier portal supports OTD in practical ways:

    • Faster order acknowledgement: suppliers can confirm receipt, accept or reject dates, and flag constraints immediately, instead of waiting on email chains.
    • Reduced clarification cycles: requirements, drawings, and inspection expectations are shared in a controlled way, which reduces back and forth and rework.
    • Earlier exception detection: if a supplier hits a hold, material delay, or capacity issue, it becomes visible while recovery options still exist.
    • Shorter administrative latency: certificates, inspection results, and required evidence are submitted in the right context, reducing receiving delays and MRB churn.

    In practice, this means fewer surprises and fewer compressed schedules. It also means more predictable lead times. Predictable lead times are what allow manufacturers to take on more work, commit to tighter delivery windows, and win additional contracts.

    Why traditional supplier portals still fall short

    Basic supplier portals help with communication, but many do not touch how the supplier actually executes the work. Suppliers log in to acknowledge orders, provide promised dates, and upload documentation. That helps, but it is still shallow if the portal cannot represent execution status and quality evidence in a way that connects to your internal workflows.

    Common limitations include:

    • No visibility into the supplier’s routing, work instructions, or inspection points for critical work.
    • No way to see partial completion or in-process holds, only final delivery status.
    • Documentation uploads that do not tie directly to specific operations, serial numbers, or traceability requirements.
    • Separate systems for quality complaints and non-conformances, disconnected from the original work order context.

    In this setup, the supplier sees the PO and high-level requirements. You see promised dates and final documents. The shared understanding of how the work is progressing remains limited, which makes it harder to improve Supplier OTD in a durable way.

    Increase Supplier OTD by connecting orders to execution and exceptions

    On-time delivery is not only about date promises. It is about what happens between order release and shipment. The biggest OTD losses often come from slow acknowledgement, unclear requirements, and late discovery of exceptions.

    1) Acknowledgement speed is the first controllable lever

    Order acknowledgement sounds administrative, but it has real schedule impact. If a supplier takes days to confirm receipt, confirm feasibility, or request clarification, you lose schedule before work even starts. A supplier portal that supports rapid acknowledgement and structured questions reduces that latency. It also gives you early signals when dates need to move, which allows program teams to plan rather than react.

    2) In-process visibility prevents late surprises

    Most suppliers do not miss dates because they are careless. They miss dates because exceptions occur, and those exceptions are discovered late by the customer. A controlled supplier portal can surface in-process holds and blockers, including material shortages, tooling constraints, special process queue delays, and inspection failures. That creates recovery options. You can resequence internal work, expedite where it matters, or rebalance load across suppliers.

    3) Documentation readiness affects receiving timelines and downstream OTD

    Even when parts arrive “on time,” they can still miss the real schedule if certificates or inspection evidence are incomplete. Receiving delays, MRB holds, and document chases create hidden lead time. A portal that ties documentation submission to the correct part, operation, and traceability requirement reduces this friction.

    Traceability and non-conformance are not separate from OTD

    Traceability issues and non-conformance issues are schedule issues. When the evidence chain is incomplete, work stops. When inspection data is missing, acceptance is delayed. When a defect is discovered late, the impact expands. Supplier collaboration improves when the portal supports both delivery coordination and quality control alignment.

    That includes:

    • Submitting certificates and inspection results in context, tied to serial numbers and required characteristics.
    • Flagging potential issues early, before shipment, instead of letting the customer discover them at receiving.
    • Coordinating non-conformance workflows so containment and corrective action are visible across organizations.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for Supplier Work Order Coordination in

    This is where supplier portal workflows connect directly to quality control and the NCR process. If an issue is found, it should be handled with a closed loop that ties back to the execution record, as described in non-conformance management.

    Extend work order concepts across organizational boundaries

    The alternative to email and PDFs is to treat external work with the same discipline you expect internally. A component or process performed by a supplier should be referenced by a specific work order in your system, not just by a purchase order line. That is what allows you to connect progress, exceptions, and evidence to the schedule you are accountable for.

    In practice, that means:

    • Creating external work orders in your operations layer for supplier activities, with routing, quality requirements, and traceability rules defined.
    • Allowing suppliers to see and interact with these work orders through a controlled interface, instead of sending static packets.
    • Receiving in-process status, inspection results, and documentation against those work orders, not as disconnected uploads.

    This approach does not require imposing your entire internal system on suppliers. It requires providing a structured way for them to align execution with the work order level expectations that drive compliance, quality, and on-time delivery.

    Supplier portal workflows in Connect 981

    Connect 981 supports supplier collaboration through a portal model that extends its unified operations layer to selected suppliers and sub-tiers. Internal teams manage external work using the same structural concepts as internal routing and controlled instructions, adapted to the level of detail appropriate for each supplier. The goal is shared visibility and faster coordination, not forcing a heavy MES deployment on partners.

    Capabilities include:

    • External work orders that link POs, parts, and processing steps: visible to both parties, reducing ambiguity and clarification cycles.
    • Faster acknowledgement and structured communication: suppliers can confirm dates, flag constraints, and request clarifications early.
    • In-process status updates: supplier progress and holds feed into your internal scheduling and planning workflows.
    • Structured capture of inspection data and certificates: tied to operations and serial numbers, improving traceability and reducing receiving delays.
    • Coordinated exception handling: issues are surfaced early, so recovery actions can protect Supplier OTD and Client OTD.

    Connect 981 can also bridge the system boundaries that usually slow this down, especially when ERP and MES do not share consistent execution data. That integration path is covered in integrating work orders with ERP and MES.

    Traceability that spans the full supply chain

    For regulators and prime customers, traceability does not stop at your receiving dock. They expect to see how critical characteristics were controlled across the value chain. When external work orders are coordinated through a supplier portal workflow, that traceability becomes easier to provide and easier to trust.

    For a given aircraft structure or system, you can show:

    • Which internal and external work orders contributed to each serialized component.
    • Which suppliers and sub-tiers performed special processes or repairs.
    • Which inspection results and certificates are tied to each operation, not just to the shipment.
    • How non-conformances were identified, contained, and corrected across organizations.

    This level of transparency reduces time spent on audits and investigations. It also improves day to day decision making. When a supplier issue emerges, you can quickly identify the internal work orders and assemblies that may be affected, then act with precision instead of broad, costly holds.

    Supporting suppliers rather than policing them

    Supplier performance is shaped by the clarity and practicality of the requirements they receive. A supplier portal model based on shared work order visibility is not about surveillance. It is about reducing ambiguity and rework for both sides, which improves both Supplier OTD and Client OTD.

    Suppliers benefit from:

    • Clear visibility into required checkpoints and documentation before work starts.
    • Fewer last-minute changes sent by email, since configuration control is handled through the same platform.
    • Faster feedback on submitted documentation and inspection evidence.
    • Less friction during audits, since records are organized by work order and operation.

    Manufacturers benefit from fewer surprises, better alignment on lead times, and fewer cycles spent reconciling documentation gaps. Over time, this reliability is what creates capacity to take on more contracts and deliver more consistently.

    Taking the next step in Supplier OTD and Client OTD performance

    Many aerospace organizations have strengthened internal execution and quality control, but still run supplier coordination through email, PDFs, and late status updates. Extending work order discipline to the supply chain is the next logical step. It closes visibility gaps and accelerates decision making across tiers.

    Connect 981 was built with this in mind. By using Connect 981 as a supplier portal and shared operations layer for selected suppliers, you can align routing, quality expectations, and status updates without forcing a heavy system on partners. The outcome is a supply chain that operates on shared evidence rather than assumptions, which is exactly what OTD improvement requires.

    If you want to see how supplier portal workflows can improve Supplier OTD and Client OTD in your environment, request a demo of Connect 981 and explore how a unified operations layer can accelerate execution across your aerospace supply chain.

  • Digital Travelers in Aerospace Manufacturing: Routing, Traceability, and Execution Control

    In aerospace manufacturing and MRO, the traveler is more than a routing record. It is the operational thread that ties a work order to a specific part number, serial number, configuration, and approved process sequence. When travelers stay on paper or in disconnected spreadsheets, traceability becomes fragile, rework loops are hard to control, and audit preparation turns into document hunting.

    A well-designed digital traveler creates a live execution record for each unit moving through production or maintenance. It connects routing, operator actions, inspection results, nonconformance events, and revision-controlled instructions into one history. As part of a broader digital work instructions in aerospace strategy, digital travelers help ensure that the right work is performed in the right sequence against the correct configuration baseline.

    For teams putting this topic into daily operation, digital work instructions and operator guidance, part traceability and as-built evidence, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    For airframe assembly, engine and APU overhaul, avionics production, structures fabrication, and supplier operations, the value is practical: clearer routing control, stronger serial number genealogy, better WIP visibility, and faster evidence collection for AS9100 and FAA or EASA reviews. The key is not simply replacing paper with a screen. The key is designing a traveler model that reflects real aerospace workflows, exceptions, and compliance needs.

    Role of Digital Travelers in Aerospace Manufacturing and MRO

    From paper travelers to digital routing records

    Traditional travelers followed jobs physically from one work center to the next. They carried operation numbers, sign-off blocks, and sometimes handwritten notes about deviations or missing material. That model provided a basic chain of custody, but it depended on manual updates and often separated execution evidence from the source instructions, inspection records, and engineering data.

    A digital traveler replaces that fragmented record with a controlled transaction history. Each operation can be opened, paused, placed on hold, completed, or sent to rework within a system that timestamps actions and associates them with the operator, inspector, or supervisor involved. Instead of relying on an annotated paper packet, the organization has a structured record of what happened and why.

    Why travelers matter more in long-life aerospace programs

    Aerospace programs may remain in production or sustainment for decades. Over that lifespan, routings change, suppliers change, approved processes change, and configuration effectivity becomes more complicated. A traveler therefore cannot be treated as a disposable shop-floor form. It must preserve the execution context for a unit long after build or maintenance is complete.

    That matters when an operator question from years ago becomes relevant to a field issue investigation, a service bulletin review, or a customer request for objective evidence. A digital traveler makes it possible to reconstruct the path of a serial number through the factory or repair station with far less ambiguity.

    How travelers support AS9100 and FAA/EASA traceability

    AS9100 environments require controlled execution and objective evidence. FAA and EASA oversight adds pressure around maintenance release records, task sign-offs, part identity, and compliance to approved data. A digital traveler supports these requirements by linking who performed a task, when it was completed, what revision-controlled instruction was in force, and what result was captured.

    The traveler does not replace every quality or engineering record. It acts as the orchestration layer that references and binds them together. That distinction is important: traceability improves most when the traveler is designed as the indexed path through execution data, not as an isolated form trying to duplicate every system around it.

    Core Data Model for an Aerospace Digital Traveler

    Linking work orders, part numbers, and serial numbers

    The minimum data model for a digital traveler should associate a work order or maintenance order with the affected part number and, where applicable, a unique serial number. In many aerospace settings, the traveler must also support lot or batch references for consumables and lower-level components, especially when genealogy is required for critical assemblies.

    For serialized production, each traveler instance should represent one controlled execution context. If ten units are on the same order but each carries a distinct serial number, the system should preserve serial-level state and evidence even if planning groups them operationally. This prevents sign-off ambiguity and allows downstream issues to be traced to the exact unit affected.

    Capturing configurations, options, and effectivity

    Not every unit follows the same path. Option content, customer-specific requirements, service bulletins, engineering changes, and line-replaceable unit variants can all alter the traveler. The traveler model therefore needs fields for configuration identifiers, effectivity ranges, revision references, and conditional operations.

    In practice, this means a routing is not just a fixed list of steps. It may contain optional branches, inspection points triggered by configuration, or alternate work centers qualified for a special process. The digital traveler should make these conditions explicit so operators and supervisors do not need to infer applicability from separate documents.

    Traveler states, holds, and exceptions

    Aerospace execution rarely proceeds in a perfectly linear way. Material shortages, missing tooling, engineering questions, inspection failures, and customer holds interrupt normal progress. A robust traveler needs clear states such as released, in work, waiting inspection, hold, rework, complete, and closed. It should also preserve the reason for each state change.

    Holds and exceptions deserve special attention. If a traveler is paused because a dimension is out of tolerance, that event should link to the nonconformance record, the disposition, and any resulting rework operation. Without this connection, the routing history may show that work resumed, but not whether it resumed under approved conditions.

    Integrating Digital Travelers with ERP, MES, PLM, and QMS

    Pulling work orders and routing from ERP/MES

    In many organizations, ERP remains the system of record for work orders, material planning, and high-level routings. MES may manage dispatching, labor reporting, and machine or station-level execution. A digital traveler should synchronize with those systems rather than duplicate them blindly.

    Common patterns include importing released work orders from ERP, inheriting the approved routing structure, and then extending execution detail at the operation and step level inside the traveler environment. This keeps planning authority where it belongs while allowing the traveler to enforce shop-floor control and richer traceability.

    Referencing BOMs and technical data from PLM

    PLM typically owns engineering structures, drawing references, effectivity, and controlled product definitions. A digital traveler should reference this data so each operation points to the applicable technical baseline. That does not mean dumping full engineering packages into the traveler. It means the traveler should resolve the correct revision and expose the exact data needed for execution.

    This approach reduces the risk of operators accessing outdated local copies or separate file shares. It also helps investigators answer a critical question later: what approved technical data was in force when this serial number passed through the operation?

    Connecting nonconformance and inspection data from QMS

    Inspection results and quality events often live in a QMS or adjacent quality application. Digital travelers become more valuable when they can trigger inspection holds, record pass-fail outcomes, and link to NCRs, concessions, or deviation approvals. That creates a unified execution history without forcing quality teams to abandon specialized workflows.

    For example, if an engine module teardown reveals damage outside standard limits, the traveler can route the job into a hold state, launch the quality review, and then release the next approved operation only after disposition is complete. The traveler becomes the control point for execution while quality remains the authority for the decision.

    Design Patterns for Digital Travelers in Key Aerospace Use Cases

    Final assembly lines and moving production

    On final assembly or large structures programs, work often moves physically while responsibility shifts across stations. Travelers in this environment need operation sequencing, zone or station assignment, and the ability to handle partial completions. A fuselage section may require confirmation of multiple inspection points before it can advance, even though supporting tasks are completed by different teams.

    Digital travelers help by showing exact status by unit and station, not just by order. Supervisors can see which serial numbers are waiting on buy-off, which are blocked by material, and which have open rework loops. That visibility is difficult to maintain with paper packets moving alongside large assemblies.

    Engine and APU MRO cells

    MRO travelers must handle recursive findings. A unit arrives with a baseline scope, but teardown inspection may add work, split components into different repair streams, or trigger engineering review. A rigid linear traveler often fails here. The better pattern is a core traveler with controlled branching for inspection findings, piece-part routing, repair approvals, and reassembly gates.

    This is especially important when serialized modules and subcomponents must maintain individual histories. The traveler should support parent-child relationships so the overhaul record reflects both the top-level engine event and the routed activity on the affected serialized parts.

    Component shops and special processes (NADCAP)

    In component machining, composites, heat treat, coating, and other special process environments, the traveler should capture not only completion status but also process evidence such as equipment identity, parameter ranges, lot references, and qualified personnel sign-off. The goal is to connect the routing event to the evidence required for release and audit.

    Where special process control is critical, traveler steps may need mandatory data capture before completion is allowed. This prevents operators from closing an operation without recording the objective evidence that quality and customers will later expect.

    Tier 1 and Tier 2 supplier manufacturing

    Suppliers often face the added challenge of working across multiple customer requirements. A configurable digital traveler lets them standardize the platform while varying routing content, approval gates, and record retention rules by program or customer. That is far more sustainable than maintaining separate paper practices for each OEM or prime relationship.

    For supplier traceability, the traveler should also preserve incoming material identity, subcontracted process references, and shipment linkage. This supports downstream genealogy requests without forcing manual reconstruction months later.

    Execution Control and Data Capture at Each Operation

    Binding travelers to digital work instructions

    A traveler should not be confused with a work instruction. The traveler controls the route and status of work. The instruction explains how to perform the task. In a mature implementation, the traveler presents or references the exact instruction revision required for the operation and configuration in scope.

    This linkage is what turns routing control into execution control. If an operation cannot start until the current instruction is acknowledged and the prerequisite conditions are met, the traveler becomes a practical compliance mechanism rather than a passive record.

    Recording step-level results, signatures, and measurements

    Some operations require only completion confirmation; others require measurements, torque values, test results, tool identifiers, or dual sign-off. The traveler design should support data collection at the right level of granularity. Too little detail creates audit gaps. Too much detail slows execution and encourages bypass behavior.

    The best pattern is risk-based capture. Critical operations should require the exact values and signatures needed to prove conformance. Lower-risk steps may only need completion evidence. This keeps the traveler useful on the shop floor while still preserving serial-level accountability.

    Handling deviations, concessions, and rework loops

    Deviation handling should be built into the traveler model from the start. Aerospace teams routinely encounter approved departures, concession dispositions, and controlled rework. If the traveler cannot represent these events cleanly, users will work around the system with side documents and emails.

    A better design creates a formal path: nonconformance detected, work held, quality disposition issued, rework or use-as-is decision recorded, and next operations released only under approved conditions. That structure protects traceability and reduces confusion during investigations or customer review.

    How Connect981 Implements Digital Travelers

    Traveler templates and configuration management

    Connect981 supports digital traveler templates that can be aligned to part families, programs, maintenance scopes, and supplier workflows. Instead of one fixed traveler design, teams can configure routing structures, data capture points, approval gates, and instruction links to fit different aerospace environments.

    This configurability is important because an avionics assembly traveler, a composite repair traveler, and a turbine module overhaul traveler do not carry the same execution logic. Templates provide standardization without pretending every operation follows the same pattern.

    Real-time traveler status and WIP visibility

    By digitizing traveler states and operation progress, Connect981 gives production and quality teams a current view of work in process. They can identify units waiting on inspection, jobs stalled in hold status, and serial numbers approaching key completion milestones. That visibility supports schedule recovery, escalation, and more accurate status communication across functions.

    For regulated production, real-time visibility also reduces the lag between an issue occurring and the organization reacting to it. A blocked traveler can immediately signal that execution should not continue until the required review is complete.

    Using traveler history for audits and investigations

    One of the strongest advantages of digital travelers is the ability to retrieve execution history quickly. Connect981 preserves traveler events, linked records, and status changes so teams can reconstruct who did what, when it happened, and what supporting evidence was recorded. That is useful during internal audits, customer audits, root cause investigations, and service history reviews.

    Instead of pulling paper packets from multiple archives, teams can navigate the traveler history for a serial number and follow the chain into instructions, inspections, and quality events. In aerospace, that speed matters because questions often arrive long after the original work was performed.

    Implementation Considerations and Common Pitfalls

    Overcomplicating traveler structures

    A common mistake is trying to encode every possible scenario into a single master traveler. The result is a cluttered execution experience that confuses operators and creates maintenance problems for engineering. It is usually better to build modular templates with conditional logic and clear applicability rules.

    The traveler should expose what the user needs now, not every possible branch for every program. Simplicity on the screen often produces better compliance than completeness in theory.

    Managing legacy work orders during migration

    Migration from paper or hybrid processes needs a deliberate cutover plan. Some organizations attempt to convert every open order midstream, which can create mismatches between historical packets and digital records. A staged approach is usually safer: define which jobs stay in the legacy method, which new releases start digitally, and how cross-reference will be maintained.

    This is especially important for long-cycle aerospace orders where a traveler may remain active for extended periods. The historical chain must remain coherent even during system transition.

    Ensuring user adoption on the shop floor

    No traveler architecture succeeds if technicians, inspectors, and supervisors view it as administrative overhead. Adoption depends on practical usability: clear operation status, minimal unnecessary fields, fast access to the right instruction, and obvious handling for exceptions. Training should focus on how the traveler helps control work, not just how to click through screens.

    Strong implementations also involve production and quality users early in design. They know where routing handoffs fail, where signatures are often missed, and where paper notes are hiding critical context. Digital travelers work best when they reflect those realities instead of imposing an abstract process model.

    For aerospace manufacturers and MRO organizations, digital travelers are the backbone of serialized execution. They connect work orders, routings, configuration, instructions, and quality records into a controlled history for each unit. When integrated thoughtfully with ERP, MES, PLM, and QMS, they improve both daily execution control and long-term traceability across the product lifecycle.

  • Applying ISO 22400 in Aerospace and MRO: KPI Use Cases and Patterns

    Applying ISO 22400 in Aerospace and MRO: KPI Use Cases and Patterns

    ISO 22400 defines a common language for manufacturing KPIs. Aerospace manufacturing and Maintenance, Repair, and Overhaul (MRO) environments operate under intense regulatory, safety, and traceability pressures, but they still benefit from standardized KPI terminology. Applying ISO 22400 here is less about inventing new aerospace metrics and more about mapping existing practices to clearly defined concepts that work across plants, partners, and digital systems.

    This article explains where ISO 22400 fits in aerospace and MRO, shows practical KPI use cases, and highlights how to combine standard definitions with sector-specific indicators such as turnaround time and traceability. It focuses on patterns and examples, not on prescribing a single KPI set or giving performance-improvement advice.

    For teams putting traceability and genealogy into daily operation, MES execution control, part genealogy and traceability, part traceability and as-built evidence help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on MRO execution workflows, shop floor execution control, a connected execution platform, Connect 981’s aerospace execution solutions, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    For a broader view of the standard itself and how it structures manufacturing KPIs across industries, see our overview of ISO 22400-aligned aerospace and MRO reporting.

    Aerospace and MRO KPI Challenges

    Aerospace and MRO organizations already report on utilization, schedule adherence, quality, and resource consumption. The difficulty is ensuring that metrics mean the same thing across facilities, programs, and suppliers, and that they remain auditable over long time horizons.

    High stakes for safety, traceability, and compliance

    In aerospace and MRO, metrics underpin decisions that affect airworthiness and regulatory compliance. Authorities and customers expect clear evidence for how aircraft, components, and maintenance activities were planned, executed, and released.

    • Safety and airworthiness: KPIs around maintenance execution, inspection findings, rework, and release status must be tightly linked to configuration and documentation baselines.
    • Traceability: Every part, task, and sign-off may need to be traced across multiple systems (PLM, ERP, MES/MRO, QMS). KPIs built on ambiguous definitions of time or quantity risk undermining that traceability.
    • Compliance: Regulators focus on whether records are complete, consistent, and understandable. KPI definitions that change from site to site can create gaps during audits.

    ISO 22400 does not define aerospace regulations. Instead, it offers standardized KPI concepts (for example, equipment utilization or order execution reliability) that can be aligned with regulated processes and record sets.

    Complex routings, configurations, and rework

    Aerospace manufacturing and MRO environments handle complex assemblies, long routings, and frequent engineering changes. Maintenance events, in particular, often deviate from plan as findings drive additional scope.

    • Non-linear work: Jobs may move backward in the routing because of rework, waiting for parts, or additional inspections, complicating lead time and utilization calculation.
    • Configuration variation: The same work center may handle multiple aircraft types, modification standards, or customer-specific configurations.
    • Extended dwell times: Aircraft or large assemblies may spend days or weeks at a given station while multiple work packages proceed in parallel.

    ISO 22400’s neutral definitions of time categories, equipment states, and order-related KPIs help bring structure to this complexity without prescribing aerospace-specific routing logic.

    Multi-party collaboration across OEMs, MROs, and suppliers

    Programs typically involve OEMs, tiered suppliers, independent MROs, and airline or operator maintenance teams. Each organization may use different systems, but they must still align on what reported metrics mean.

    • Supplier performance reporting: Contracts often reference utilization, turnaround, or defect-related indicators. Unclear definitions can create disputes.
    • Shared assets: Test cells, ground support equipment, and specialized tooling may be used by multiple organizations or sites.
    • Joint improvement initiatives: Cross-company projects need comparable KPIs to identify bottlenecks or validate improvements.

    Using ISO 22400 as a reference vocabulary helps align KPIs across organizations, even when each party uses its own software stack and industry-specific metrics.

    Where ISO 22400 Fits in Aerospace and MRO

    ISO 22400 is an industry-neutral standard for manufacturing operations KPIs. Aerospace and MRO organizations can adopt its concepts selectively, focusing on the KPIs that best match their production and maintenance workflows.

    Aligning core production and maintenance KPIs

    Many aerospace and MRO metrics correspond directly to ISO 22400 KPI families, even if they currently use different names. Examples include:

    • Equipment-oriented KPIs: Utilization of test cells, paint booths, autoclaves, and ground support equipment.
    • Order-related KPIs: Adherence of maintenance events, work orders, or modification campaigns to planned time structures.
    • Resource-related KPIs: Labor hours consumed versus planned, or material usage tied to specific operations.

    Mapping these to ISO 22400 terminology improves clarity. For instance, a site that reports the percentage of planned time that a test cell is actually operating can align that metric with the standard’s definitions of equipment utilization rather than inventing a facility-specific term.

    Using standardized definitions in supplier agreements

    Supplier and MRO contracts often specify KPI-based service levels. ISO 22400 can provide unambiguous KPI descriptions in these agreements:

    • Referencing an ISO 22400-aligned definition of a utilization or availability indicator when discussing asset access or readiness.
    • Using order execution-related KPIs for agreed reporting on maintenance event adherence to plan.
    • Defining units of measure, trend directions, and time behaviors consistently, so monthly dashboards reflect the same logic at every site.

    This approach does not turn ISO 22400 into a regulatory requirement; it simply reduces interpretation risk when multiple parties reference the same concept.

    Supporting cross-site performance comparisons

    Large aerospace OEMs and MRO networks often operate multiple facilities globally. Even when each site follows local regulations and customer requirements, leadership still wants to compare performance.

    • Consistent KPI semantics: Sites can continue using local dashboards, but the underlying KPI definitions are harmonized with ISO 22400 where possible.
    • Comparable time categories: Planned, unplanned, and idle time categories follow consistent meaning, so utilization and order execution reliability can be aggregated.
    • Neutral layer across verticals: Organizations that serve aerospace plus other sectors (for example, industrial gas turbine service) can use ISO 22400 as a common baseline while layering sector-specific metrics on top.

    Example Use Cases of ISO 22400-Aligned KPIs

    The following examples illustrate how ISO 22400 concepts can be applied to aerospace and MRO scenarios. They are patterns, not prescriptions, and they do not expand the standard’s formal KPI list.

    Equipment utilization for critical ground support assets

    Ground support equipment (GSE) such as engine test cells, jacks, docking systems, hoists, and specialized tooling are high-value, capacity-limiting assets. Under- or over-utilization affects both cost and schedule.

    ISO 22400 defines equipment-related KPIs based on time categories and equipment states. When applied to GSE:

    • State definition: RUN, IDLE, STOP, or other states can be mapped to the real behavior of test stands and docking systems.
    • Time allocation: Planned versus unplanned downtime, setup time, and active operation periods are clarified.
    • Utilization indicator: A utilization KPI can be defined as the ratio of actual productive time to a defined planned time window, aligned with ISO 22400 terminology.

    This yields a consistent measure of how intensively GSE is used across shops and sites, even if their schedules and aircraft mixes differ.

    Order execution reliability for maintenance events

    Maintenance events—such as C-checks, heavy checks, or modification campaigns—can be viewed as production orders in ISO 22400 terms. The standard’s order-related KPIs provide a structured way to describe how these events progress versus plan.

    • Planned time structure: The event has a planned start, planned finish, and possibly intermediate milestones.
    • Actual execution: Actual times are captured from MRO execution systems, including delays due to findings, parts, or engineering clarifications.
    • Order execution reliability: ISO 22400-aligned KPIs can describe how closely execution followed the planned time structure or quantity profile.

    These indicators do not replace aerospace-specific turnaround or on-time-release metrics. Instead, they provide neutral, comparable views of schedule adherence and execution variability that can be used for internal analysis or supplier reporting.

    Resource-related KPIs for labor and parts usage

    Labor hours and parts consumption are central to aerospace and MRO economics. ISO 22400’s resource-related KPI concepts allow these to be linked consistently to orders, equipment, and time periods.

    • Labor indicators: Personnel-related KPIs can express, for example, total maintenance labor hours associated with a work order or area over a given shift.
    • Material indicators: Material consumption KPIs can associate parts usage with specific operations or events, supporting cost and reliability analysis.
    • Energy indicators: Energy usage for large assets (such as engine test cells or autoclaves) can be treated as a resource KPI aligned to specific orders.

    Aligning resource-related KPIs with ISO 22400 terms helps ensure that, when labor or material intensities are compared between facilities, they rest on a shared conceptual basis.

    Combining ISO 22400 with Aerospace-Specific Metrics

    Aerospace and MRO teams need KPIs that go beyond the neutral scope of ISO 22400. The goal is not to force all metrics into the standard, but to clearly distinguish which indicators are ISO 22400-based and which are aerospace-specific.

    Turnaround time breakdowns and on-time release

    Turnaround time (TAT) and on-time release are central to MRO performance. These KPIs typically combine:

    • Total elapsed time between arrival and release.
    • Breakdowns by phase (induction, disassembly, inspection, repair, reassembly, test, closing).
    • Customer- or contract-specific commitments for on-time delivery.

    These composite metrics are not defined in ISO 22400. However, many of their building blocks—such as time in particular states or adherence to planned time structures—map well to ISO 22400 time and order-related concepts. Organizations can:

    • Use ISO 22400-aligned KPIs at the level of work centers, operations, and equipment.
    • Construct TAT and on-time-release metrics on top, labeled clearly as aerospace-specific.

    Regulatory auditability and record linkage

    Regulators and customers focus on whether maintenance and manufacturing records are complete and coherent. KPI design must support this auditability.

    • Transparent definitions: ISO 22400 encourages specifying units, applicable time behaviors, and trend directions. This documentation is useful during audits, even when the KPI itself is not required by regulation.
    • Stable semantics: Once a KPI definition is agreed, changes are versioned and recorded, so historic reports remain interpretable.
    • Linkages to records: KPIs reference underlying events, logs, and approvals stored in PLM, ERP, MES/MRO, and QMS systems.

    By grounding KPIs in ISO 22400 concepts, teams can more easily show how high-level indicators relate to the detailed records that auditors and airworthiness authorities examine.

    Integrating traceability indicators with standardized KPIs

    Aerospace traceability indicators—such as the percentage of parts with complete back-to-birth records or the number of tasks with missing sign-offs—are typically sector-specific. They sit alongside standard KPIs rather than inside ISO 22400’s formal list.

    One effective pattern is:

    • Use ISO 22400-aligned KPIs for time, quantity, and resource aspects of operations.
    • Define separate traceability indicators that reference the same orders, equipment, and time periods.
    • Ensure dashboards show clearly which indicators are ISO 22400-based and which are internal, aerospace-specific constructs.

    Digital Platforms and Integration in Aerospace and MRO

    Aerospace and MRO operations rely on multiple tightly integrated systems. ISO 22400 offers a conceptual model that digital platforms can use to keep KPI definitions consistent across this ecosystem.

    How platforms like the ISO 22400 manufacturing KPIs hub map ISO 22400 concepts

    Digital operations platforms that support ISO 22400 concepts typically:

    • Model equipment, work centers, and work units using definitions compatible with IEC 62264 and ISO 22400.
    • Translate raw events (for example, equipment state changes) into standardized time categories.
    • Provide libraries of ISO 22400-aligned KPIs that customers can adopt or extend.

    Aerospace and MRO users can then layer domain-specific workflows—such as digital work instructions, airworthiness releases, and findings management—on top of a shared KPI foundation.

    Connecting PLM, ERP, MES, and QMS in regulated environments

    In a regulated aerospace environment, systems are often validated and tightly controlled. ISO 22400 does not impose a particular architecture, but it helps with integration design:

    • PLM: Defines product structures, configurations, and approved repairs or modifications that may influence how KPIs are segmented.
    • ERP: Manages orders, contracts, and financial views that align with order-related KPI hierarchies.
    • MES/MRO systems: Track execution states at work centers and operations, providing the raw events and quantities underlying KPIs.
    • QMS: Holds nonconformance, concession, and corrective action data that can be correlated with performance metrics.

    By agreeing on ISO 22400-based KPI semantics, integration interfaces can exchange performance information without redefining basic concepts every time a new connection is built.

    Ensuring KPI definitions remain transparent and auditable

    Given the long service life of many aerospace platforms, KPIs must remain interpretable for years. Digital platforms can support this by:

    • Storing KPI definitions, including mappings to ISO 22400 concepts, as configuration items with version history.
    • Documenting any extensions or sector-specific metrics separately from the standard-aligned set.
    • Providing drill-down from aggregated KPI values to underlying events, orders, and records.

    This level of transparency is useful for internal reviews and external audits alike.

    Practical Adoption Tips for Aerospace and MRO Teams

    Adopting ISO 22400 in aerospace and MRO is a matter of careful alignment and communication rather than wholesale replacement of existing KPIs.

    Engaging quality and regulatory stakeholders early

    Because KPIs feed into audit trails and, in some cases, into regulated reports, quality and regulatory teams should participate from the beginning.

    • Review ISO 22400 concepts jointly with operations and IT, focusing on how they map to current metrics.
    • Identify any constraints arising from regulations, customer contracts, or approvals that affect KPI changes.
    • Agree on how KPI definitions will be documented, controlled, and communicated to auditors and customers.

    Documenting which KPIs are ISO 22400-based and which are not

    Clarity about scope is essential. A straightforward approach is to classify indicators into two groups:

    • ISO 22400-aligned KPIs: Indicators whose names, meanings, time behaviors, and measurement objects match the standard’s conceptual definitions.
    • Aerospace-specific metrics: Composite indicators such as TAT breakdowns, traceability scores, or customer-specific service-level metrics that extend beyond the standard.

    Labeling dashboards and reports accordingly prevents confusion and avoids implying that all aerospace metrics are part of ISO 22400.

    Building a roadmap for harmonized KPI reporting

    Most organizations will evolve toward ISO 22400 adoption rather than switching everything at once. A practical roadmap often includes:

    1. Inventory: Catalog existing KPIs used in manufacturing and MRO operations.
    2. Mapping: Identify which existing metrics correspond closely to ISO 22400 concepts and where gaps or differences exist.
    3. Pilots: Harmonize a small set of high-value KPIs across two or three facilities.
    4. Governance: Establish a change-control process for KPI definitions, including representation from operations, IT, quality, and regulatory teams.
    5. Rollout: Extend harmonized definitions to more sites, suppliers, and dashboards as systems and contracts are updated.

    Throughout this journey, the objective is not to eliminate aerospace-specific metrics but to ensure that, where ISO 22400 concepts apply, they are used consistently.

    Conclusion

    ISO 22400 does not tell aerospace and MRO organizations which KPIs to use or how to meet regulatory requirements. Its value lies in establishing a shared vocabulary and structure for core manufacturing and maintenance indicators. By aligning equipment, order, and resource-related KPIs with ISO 22400, aerospace manufacturers and MRO providers can make their reporting more comparable, auditable, and integration-friendly—while continuing to use sector-specific metrics such as turnaround time, traceability indicators, and on-time release.

    Using ISO 22400 as a neutral foundation, organizations can connect PLM, ERP, MES/MRO, and QMS data into coherent performance views that serve both operational decision-makers and external stakeholders, without constraining their strategic choices or domain-specific KPI designs.

  • Building ISO 22400-Aligned Data Models for Connected Manufacturing

    Building ISO 22400-Aligned Data Models for Connected Manufacturing

    Building ISO 22400-Aligned Data Models for Connected Manufacturing

    For aerospace and defense manufacturers, ISO 22400 is most powerful when it is implemented in the data model, not just referenced in a specification. The standard defines how manufacturing KPIs should be structured conceptually, but engineering teams still must decide how to represent those concepts in databases, event streams, and integrations across ERP, MES, SCADA, historians, PLM, and QMS. When this is done well, a multi-plant aerospace operation can compare KPIs with confidence, and a platform such as Connect 981 can present standardized manufacturing KPI views without forcing a single vendor stack.

    This article explains how ISO 22400 influences data modeling and system integration across typical aerospace digital infrastructure. It focuses on representing equipment states, orders, and time categories in a coherent KPI layer, while remaining vendor- and technology-agnostic. The goal is to give architects and data engineers a clear blueprint for aligning heterogeneous systems with ISO 22400 semantics.

    For teams putting this topic into daily operation, ISO 22400 KPI governance, ERP, MES, and PLM integration paths, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    Why ISO 22400 Needs a Thoughtful Data Model

    From conceptual definitions to database structures

    ISO 22400 is intentionally conceptual. It defines KPIs, time categories, and objects such as work units and production orders, but it does not dictate how these elements should be stored in tables, topics, or data lakes. In an aerospace environment, however, KPIs must be auditable, traceable to underlying events, and reproducible across program lifecycles. That requires explicit data modeling decisions.

    At minimum, an ISO 22400-aware model needs to capture three layers:

    • Raw signals and events from equipment, test stands, and assembly stations (e.g., PLC tags, NC program events, manual inspection start/stop).
    • Derived states and time segments, where each contiguous period is labeled with an ISO 22400-relevant state such as RUN, STOP, IDLE, or SLOW.
    • Aggregated indicators and KPIs that combine time segments and quantities into ISO 22400-defined concepts such as availability or equipment utilization.

    These layers can live in different systems: SCADA for signals, MES for high-level events, a historian for dense time-series data, and a cloud data platform for aggregation. The data model is the glue that ensures a KPI such as “availability” has the same meaning no matter where it is queried.

    Ensuring consistency across heterogeneous systems

    Aerospace production and MRO facilities frequently operate with a heterogeneous stack: a legacy MES on the shop floor, a modern PLM system defining configurations, ERP managing orders, plus multiple historians and test data repositories. Without a shared semantic model, every integration becomes a custom mapping exercise, and KPI definitions drift over time.

    ISO 22400 provides a reference vocabulary, but the implementation must resolve several practical questions:

    • How do we map proprietary equipment states from different machine vendors to a common RUN/STOP/IDLE/SLOW model?
    • How do we consistently connect production orders from ERP to work centers and work units in MES and SCADA?
    • How do we represent planned vs. unplanned downtime in a way that supports audit-friendly reporting in AS9100 environments?

    The answer is a shared, ISO 22400-aligned data model—often implemented as a semantic layer or KPI store—that sits above plant-specific systems. Connect 981 and similar platforms can then consume this layer to power cross-site aerospace KPI reporting, while respecting the constraints of each site’s local systems.

    Representing Equipment States and Time Categories

    Capturing RUN, STOP, IDLE, SLOW in event data

    ISO 22400 treats equipment states as the foundation for many equipment-related KPIs. For aerospace machining centers, autoclaves, composite layup machines, test cells, and assembly stations, these states are typically derived from a combination of:

    • Control system tags (e.g., cycle active, alarm active, manual mode).
    • Operator input (e.g., downtime reason codes captured at the MES terminal).
    • Schedule context (e.g., whether the current time is within planned production time for that resource).

    A robust event model represents state transitions explicitly. A common pattern is an equipment_state_event structure with fields such as:

    • equipment_id (work unit identifier, aligned with IEC 62264 levels).
    • state_code (normalized to RUN, STOP, IDLE, SLOW, or other ISO 22400-related states).
    • reason_code (plant-specific detail, e.g., TOOL_CHANGE, PROGRAM_LOAD, QUALITY_HOLD).
    • start_time and end_time (or start time plus duration).
    • source_system (SCADA, MES, manual entry, etc.).

    The raw machine or SCADA events can be noisy, with rapid transitions and transient conditions. A normalization pipeline should consolidate these into clean, non-overlapping time segments associated with a single state. This is where an ISO 22400 mapping table is valuable: it expresses how vendor-specific signals map to a standard state_code.

    Aggregating state data into indicator-friendly structures

    Once states are modeled as time segments, KPI-oriented aggregation becomes straightforward. ISO 22400 relies heavily on time categories—such as operating time, busy time, planned downtime, and unplanned downtime—that are built from these state segments.

    For aerospace plants, a daily or shift-level equipment_time_summary structure is useful. It can include:

    • equipment_id and time_bucket (e.g., day, shift, or custom period).
    • Durations by normalized state (RUN, STOP, IDLE, SLOW).
    • Durations by downtime category (planned vs. unplanned, safety-related, quality-related, maintenance).
    • Flags for special conditions (e.g., new program introduction, first article inspection periods).

    These summaries serve two purposes. First, they support ISO 22400-aligned KPIs such as utilization and availability. Second, they provide traceability: when a program-level performance review questions an equipment KPI, engineers can drill back from a KPI to a time summary and then to the underlying state events and SCADA signals.

    Modeling Orders, Lots, and Production Events

    Linking production orders to equipment and time

    In aerospace manufacturing, performance is often evaluated by program, configuration, or serialized asset rather than only by equipment. ISO 22400 addresses this by defining objects like production orders and lots that can be associated with work units and time periods. To align with this, the data model should represent the relationship among:

    • ERP orders (e.g., production orders, shop orders, repair orders).
    • MES operations (routing steps, work instructions, NC programs).
    • Work units and work centers (machines, cells, bays, test stands).

    A typical pattern uses a production_operation_execution entity with:

    • order_id and operation_id (from ERP/MES).
    • equipment_id and optionally work_center_id.
    • start_time, end_time, and scheduled_time.
    • good_quantity, rework_quantity, scrap_quantity, with units.
    • configuration_id or effectivity link for configuration-controlled parts.

    This entity provides the bridge between time-based equipment behavior and order-level KPIs. It allows ISO 22400 concepts such as production time structure and order execution reliability to be computed consistently, even when the underlying orders originate from multiple ERP instances or legacy planning tools.

    Handling batch, continuous, and discrete processes

    Aerospace workflows span multiple process types: discrete assembly of airframe structures, batch processes in special processing and coatings, and quasi-continuous operation in test facilities. ISO 22400 is designed to cover batch, continuous, and discrete industries; the data model should therefore avoid assuming a single process type.

    Practical strategies include:

    • Using a common lot_or_batch_id attribute to represent material groupings, whether they are heat lots, composite layup kits, or engine modules.
    • Capturing start/stop events for material independently from equipment state events, so that KPIs can distinguish equipment availability from material availability.
    • Allowing overlapping operations on the same order (e.g., parallel test cycles, multiple stations working on different sections of the same fuselage).

    This flexibility ensures that ISO 22400 KPIs retain their meaning across the breadth of aerospace operations—from precision machining to environmental testing—without requiring separate definitions per process family.

    Integrating ERP, MES, SCADA, and Historians

    Common integration patterns and interfaces

    ISO 22400 does not prescribe any transport protocols or message formats, but certain integration patterns appear repeatedly in aerospace digital environments:

    • Order and master data from ERP to MES, where order hierarchies, routings, and work centers are synchronized, providing the structural context for ISO 22400 KPIs.
    • Event and state data from SCADA and equipment controllers into a historian or event hub, which is then normalized to ISO 22400-like states for KPI computation.
    • Quality results from QMS and inspection systems feeding into the same semantic layer so that scrap, rework, and nonconformance time are consistently categorized.

    Interfaces may be implemented via OPC UA, file-based transfers, REST APIs, or message queues, but the key is that each system provides sufficient identifiers to be bound to the ISO 22400 objects in the semantic model (equipment IDs, order IDs, lot IDs, time stamps, and reason codes).

    Using ISO 22400 as a semantic layer for data exchange

    Instead of directly wiring every system to every other system, many aerospace organizations adopt a semantic layer that mediates integrations. ISO 22400 concepts become the vocabulary of that layer. For example:

    • Rather than sending raw tag names, SCADA publishes normalized equipment_state_event messages with ISO 22400-style state codes.
    • MES publishes operation_execution events using consistent order and equipment identifiers that match the semantic model.
    • QMS publishes quality_event messages that refer to the same operations and lots, allowing scrap-related time to be tied to downtime and performance KPIs.

    Platforms like Connect 981 can then subscribe to these normalized feeds and provide cross-plant KPI dashboards and analytics without having to interpret plant-specific codes each time. This approach is especially valuable when working with a distributed aerospace supply base, where primary OEM sites and tiered suppliers need to exchange KPI information in a comparable way.

    Designing an ISO 22400-Aligned KPI Store or Data Lake

    Schema considerations for KPI queries

    An ISO 22400-aware KPI store or data lake is typically organized around a small set of core dimensions and fact-like structures. For aerospace manufacturing, those dimension tables often include:

    • Equipment and work units, including mappings to physical assets, locations, and responsibility centers.
    • Orders and operations, aligned with ERP and MES, with attributes such as program, platform, and customer contract.
    • Time, including calendar, shifts, and production calendars with holidays and planned shutdowns.
    • Material and configurations, tying KPIs back to part numbers, revisions, and configuration baselines.

    The fact structures then contain normalized event-level and aggregated data:

    • fact_equipment_state for state segments.
    • fact_operation_execution for order-related production events.
    • fact_quality_outcome for inspection and test results.
    • fact_kpi_snapshot for pre-computed ISO 22400 KPI values by period and level (equipment, line, plant, program).

    By keeping the schema technology-agnostic (star schema, wide tables, or lakehouse-style parquet datasets), organizations retain freedom in their storage and query engines while still honoring the ISO 22400 semantic structure.

    Managing metadata, units, and logical ranges

    ISO 22400 emphasizes metadata such as units of measure, applicable logical ranges, and expected trend directions. Aerospace programs often require this information for documentation, internal standards, and customer reporting. In the KPI store, this suggests explicit metadata structures:

    • A kpi_definition table that lists each KPI, its ISO 22400 reference, unit, typical consumers (operator, supervisor, management), and whether higher values are considered good or bad.
    • Optional kpi_threshold or kpi_target tables that capture plant- or program-specific goals without conflating them with the standardized KPI definition.
    • Unit conversion logic that aligns energy, throughput, and time units across sites (e.g., standardizing on hours even if some systems report minutes or seconds).

    This metadata makes it easier to build dashboards, automated checks, and alerts in aerospace environments where KPI interpretation must be consistent across programs and subject to audit or regulatory review. It also prevents accidental redefinition of KPIs when sites introduce new visualization tools or reports.

    Examples of ISO 22400-Ready Data Pipelines

    Event ingestion and transformation flows

    Consider a composite manufacturing cell producing critical flight structures. SCADA systems capture autoclave cycle data and layup station states; MES manages work instructions and order status; ERP owns the overall production order and schedule. An ISO 22400-ready pipeline might look like this:

    1. Ingest raw events from SCADA (cycle start/stop, alarm events), MES (operation start/complete), and QMS (nonconformance creation) into a central event hub or streaming platform.
    2. Normalize equipment states by applying mapping rules to SCADA tags to derive RUN/STOP/IDLE/SLOW segments with clean start/end times.
    3. Enrich events with order and configuration context by joining to ERP and PLM data, ensuring each event is associated with the correct order, configuration, and program.
    4. Compute time categories and indicators such as operating time, planned downtime, and unplanned downtime at shift and daily levels.
    5. Persist aggregates and KPIs in the KPI store, including availability, utilization, and order-related indicators as defined by ISO 22400.

    The result is an auditable pipeline from raw sensor data to standardized KPIs, suitable for cross-plant comparison and customer-facing performance reports when needed.

    Feeding dashboards and analytics tools consistently

    On the consumption side, aerospace organizations may use a mix of tools: in-house portals, commercial BI platforms, engineering analytics notebooks, and specialized dashboards for program reviews. By exposing KPIs through a common ISO 2240-aligned semantic layer, these tools all draw from the same source of truth.

    Key practices include:

    • Providing a stable, documented API or SQL interface for KPI access, with KPIs described in terms of ISO 22400 concepts rather than tool-specific naming conventions.
    • Ensuring that drill-down paths from KPI to underlying events are preserved, supporting root-cause analysis of availability or performance issues in high-value assets such as engine test cells or structural assembly jigs.
    • Allowing program-specific slices (e.g., by platform or customer) without redefining the KPIs themselves, only the filters applied.

    In this model, Connect 981 or a similar digital manufacturing platform can coordinate KPI reporting across the aerospace enterprise, while the ISO 22400-aligned data model ensures that every plant, supplier, and program interprets those KPIs the same way.

    Putting ISO 22400 Data Modeling into Practice in Aerospace

    ISO 22400 does not dictate how to architect your MES, historian, or data lake. It does, however, define a shared language of states, time categories, orders, and KPIs that can guide architecture decisions. In regulated aerospace environments, where traceability, configuration control, and cross-site comparability matter, implementing that language in the data model provides tangible benefits.

    By representing equipment states as normalized events, linking orders and operations across ERP and MES, and consolidating heterogeneous system data into an ISO 22400-aligned KPI store, aerospace manufacturers can achieve consistent, audit-ready performance reporting. Platforms like Connect 981 can then leverage this foundation to support digital thread initiatives, supplier visibility, and standards-aligned KPI frameworks without forcing a single technology stack. The standard provides the semantics; the data model turns those semantics into operational reality.

  • Managing Supplier Non-Conformances in Aerospace: From SCARs to Scorecards

    Managing Supplier Non-Conformances in Aerospace: From SCARs to Scorecards

    Managing Supplier Non-Conformances in Aerospace: From SCARs to Scorecards

    In aerospace, a single defective lot from a supplier can halt production, trigger aircraft-on-ground (AOG) situations, or invite intense regulatory scrutiny. That is why aerospace supplier non conformance management is not just a purchasing or quality activity—it is a core risk-control and business performance process.

    This article focuses specifically on non conformances originating from suppliers: how they are detected, communicated, corrected, and ultimately used to drive long-term performance improvement. When done well, supplier NCR (non-conformance report) data becomes a strategic asset for managing risk and making sourcing decisions. When done poorly, it leads to recurring problems, strained relationships, and cost overruns.

    For teams putting non-conformance and capa into daily operation, non-conformance management, supply chain and supplier execution, quality management workflows help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on a connected execution platform, Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    If you are looking for a broader, end-to-end view of non-conformance handling across your operation, including in-house manufacturing and MRO, see our guide on enterprise-wide non conformance visibility.

    Why Supplier Non-Conformances Are Critical in Aerospace

    Impact on production schedules and AOG risk

    Purchased material typically represents a large portion of cost and risk in aerospace programs. When supplier parts arrive out of specification:

    • Production lines stall while engineering determines disposition and buyers scramble for replacement parts.
    • Aircraft-on-ground (AOG) situations may occur if replacement parts are not available to support final assembly or maintenance.
    • Buffers and safety stock are consumed more quickly, driving up inventory requirements and working capital if supplier quality is unstable.

    Because many aerospace parts have long lead times and tight qualification requirements, switching suppliers or re-sourcing is rarely a quick option. Effective supplier non-conformance management is therefore a critical lever for protecting delivery schedules.

    Regulatory and customer traceability expectations

    Regulators and aerospace customers expect full traceability for supplier-related non conformances:

    • Which lots, serial numbers, and work orders are affected?
    • What containment was applied and when?
    • What root cause was identified at the supplier and at your own facility?
    • What corrective and preventive actions (CAPA) were implemented, and how was effectiveness verified?

    Standards like AS9100, along with customer clauses, require documented, auditable processes for handling supplier-caused non conformances. Incomplete or inconsistent records can surface during audits, customer reviews, or incident investigations, with significant reputational and commercial consequences.

    Cost and relationship implications of poor supplier quality

    Supplier non conformances carry direct and indirect costs:

    • Direct costs: additional inspection, rework, scrap, expedited freight, and premium overtime.
    • Indirect costs: missed delivery commitments, line downtime, engineering support, and customer penalties.

    At the same time, suppliers are long-term partners. Overly punitive responses can damage relationships and limit collaboration, while overly lenient responses encourage recurrence. The goal is a fair, documented, and consistent process that:

    • Protects safety and compliance.
    • Allocates costs appropriately when justified by facts.
    • Supports genuine joint improvement with strategic suppliers.

    Typical Supplier Non-Conformance Workflow

    Although every organization has its own terminology and systems, most aerospace supplier non-conformance workflows follow a similar pattern.

    Detection at incoming inspection or in-process

    Supplier issues can be detected at multiple points:

    • Incoming inspection – dimensional checks, functional tests, documentation review, and visual inspection.
    • In-process – machining, assembly, or test operations reveal defects traceable back to supplier material.
    • Final inspection or test – failures linked to upstream supplier deviations.
    • Field or MRO feedback – service issues ultimately traced to a supplier component or process.

    When a deviation is found, the inspector or operator should immediately:

    1. Quarantine the suspect material (physical segregation and clear identification).
    2. Document the non conformance in the QMS or NCR system, including part numbers, lot/serials, supplier details, and defect description.
    3. Flag potential impact on work-in-process and delivered products using the same lot or configuration.

    Documentation and issuing supplier corrective action requests (SCARs)

    Not every minor defect warrants a formal Supplier Corrective Action Request (SCAR). Many organizations use thresholds based on:

    • Severity (safety or flight-critical impacts).
    • Frequency (repeat issues over a defined period).
    • Volume (defect rate across a lot or program).

    For issues that cross those thresholds, the quality or supplier management team issues a SCAR that typically includes:

    • Clear description of the non conformance and supporting evidence (photos, test results, measurements).
    • Traceability information (purchase order, lot, serial, manufacturing date, applicable specs and revisions).
    • Required containment actions at the supplier and your site.
    • Timelines for initial response, root cause analysis, and corrective action completion.

    Well-structured SCARs set expectations up front and avoid rework cycles where suppliers ask for missing information or clarification.

    Joint root cause analysis and corrective action planning

    Effective supplier non-conformance management is collaborative. After the SCAR is issued:

    • The supplier performs an initial assessment and confirms or updates containment scope.
    • Both parties may participate in a structured problem-solving method such as 8D or 5 Whys.
    • Root causes are identified not only at the supplier but also, if applicable, in your own processes (e.g., inadequate incoming inspection, unclear specifications).
    • Corrective and preventive actions are defined, including process changes, training, documentation updates, and verification plans.

    The aim is not merely to close the SCAR, but to implement actions that demonstrably prevent recurrence.

    Defining Clear Expectations for Suppliers

    Clarity upfront reduces friction and delays during non-conformance handling. Expectations should be documented in supplier quality requirements, purchase order terms, and, where appropriate, contracts.

    Response time targets and containment requirements

    Many aerospace organizations define tiered response expectations, such as:

    • Immediate (within 24 hours): Acknowledgement of the SCAR and confirmation of short-term containment actions and affected scope.
    • Interim report (3–5 business days): Initial root cause hypotheses, risk assessment, and additional containment if needed.
    • Final 8D / root cause and corrective action (10–30 days): Verified root cause, implemented corrective actions, and effectiveness plan.

    Containment expectations should specify:

    • How the supplier will identify and segregate potentially affected material (on-site and at your facility).
    • How they will prevent shipment of suspect product until risk is understood.
    • When and how they will perform 100% inspection or additional testing, if required.

    Data and evidence required with supplier responses

    To avoid low-quality responses, define minimum requirements for SCAR closure, such as:

    • Documented root cause analysis method used and why the cause is believed to be valid.
    • Objective evidence of process changes (updated work instructions, control plans, training records, equipment maintenance or calibration records).
    • Verification data, such as capability studies, inspection results, or pilot runs showing the issue is resolved.
    • Assessment of similar products, processes, and customers potentially affected by the same cause.

    Making these expectations visible to suppliers upfront improves the quality and consistency of their responses.

    Alignment with AS9100 and customer clauses

    Supplier expectations should be aligned with:

    • AS9100 requirements for control of externally provided processes, products, and services.
    • Specific customer quality requirements (e.g., mandatory notification timelines, approval of concessions, mandated use of particular 8D templates).
    • Any applicable design authority or regulatory requirements for concessions or deviations.

    Providing suppliers with a concise summary of these expectations—rather than assuming they will interpret long standards documents—reduces ambiguity and audit risk.

    Using Digital Tools to Manage Supplier Non Conformances

    Managing supplier SCARs through email, spreadsheets, and ad hoc trackers quickly becomes unmanageable, especially across multiple sites and high part counts. Digital solutions make the process more reliable and transparent.

    Supplier portals and shared NCR visibility

    A secure supplier portal within your quality management or non-conformance system allows suppliers to:

    • View all open and historical non conformances assigned to them.
    • Access relevant documentation (NCR forms, photos, drawings where authorized).
    • Submit SCAR responses, attach evidence, and update status directly.

    This eliminates version confusion from multiple spreadsheets and enables a single, auditable record for each issue. Suppliers see precisely what is expected and by when, and your teams see responses as soon as they are posted.

    Automated notifications and reminders

    Digital workflows can automatically:

    • Notify the appropriate supplier contacts when a new SCAR is issued or updated.
    • Send reminders ahead of due dates for containment, interim reports, and final actions.
    • Escalate overdue responses to supplier management or your internal supplier quality leaders.

    This reduces administrative follow-up burden and prevents SCARs from silently aging in inboxes.

    Integrating supplier data into scorecards and dashboards

    When supplier-related NCR and SCAR data is stored in structured, centralized systems, it becomes straightforward to:

    • Calculate defect rates by part family, program, or supplier.
    • Monitor response time and closure time performance.
    • Track repeat issues by root cause category.
    • Feed this information into supplier scorecards and executive dashboards.

    This connection between day-to-day non-conformance handling and periodic business reviews is a key element of mature supplier management.

    Building Supplier Scorecards From Non-Conformance Data

    Supplier scorecards are most effective when they combine objective defect data with a balanced view of responsiveness and collaboration.

    Key metrics: defect rates, response times, effectiveness

    Common quality and non-conformance related metrics include:

    • Defect rate: parts per million (PPM), percentage of lots rejected, or NCRs per million dollars of spend.
    • SCAR response time: average days from issuance to initial containment, interim report, and final closure.
    • Corrective action effectiveness: percentage of SCARs with no recurrence within a defined monitoring window.
    • Documentation quality: completeness and clarity of responses, frequency of returns for rework.

    These metrics should be trended over time to identify improvement or deterioration rather than viewed as one-off snapshots.

    Combining qualitative and quantitative assessments

    Numbers alone do not tell the full story. Leading organizations also consider qualitative factors, such as:

    • Collaboration: willingness to share data, engage in joint problem-solving, and attend technical reviews.
    • Engineering support: ability to respond to technical questions, support qualification, and manage changes.
    • Process maturity: evidence of robust internal quality systems (e.g., AS9100 certification, robust FMEA/control plans).

    Scorecards that mix hard data with structured qualitative input support better sourcing and development decisions.

    Using scorecards in reviews and sourcing decisions

    Supplier scorecards should not be a once-a-year exercise with little follow-through. They can be used to:

    • Guide quarterly business reviews (QBRs) with key suppliers.
    • Identify candidates for development plans or additional oversight.
    • Support sourcing decisions when awarding new business or consolidating volumes.
    • Recognize and reinforce high performers through preferred status or longer-term agreements.

    The key is consistency: suppliers should know how their performance is assessed and how scorecard results influence future opportunities.

    Collaborative Improvement With Strategic Suppliers

    Not all suppliers are equal. For strategic, high-impact suppliers, non-conformance management should feed a broader, collaborative improvement agenda.

    Sharing trends and lessons learned

    Instead of addressing each SCAR in isolation, analyze and share:

    • Trends in defect types (e.g., surface defects, documentation errors, process escapes).
    • Common root cause categories (e.g., operator training, programming errors, supplier sub-tier issues).
    • Lessons learned that could apply across part families or programs.

    Regularly reviewing this information with strategic suppliers helps both sides prioritize improvement projects that deliver the greatest risk reduction.

    Joint improvement projects and training

    Where recurring or high-risk issues are identified, consider:

    • Joint Kaizen or problem-solving events at the supplier facility.
    • Technical training on print interpretation, special process controls, or regulatory requirements.
    • Support for the supplier to improve their own NCR and CAPA systems, including how they manage their sub-tiers.

    These collaboration efforts should be targeted based on data from your non-conformance and scorecard systems, ensuring resources go where they have the most impact.

    Recognizing and rewarding strong performance

    Non-conformance data can also be used positively. For suppliers that consistently demonstrate:

    • Low defect rates,
    • Fast and effective SCAR responses,
    • Strong support during audits and customer visits,

    you can consider:

    • Reduced incoming inspection levels in accordance with risk and regulation.
    • Preferred-supplier status or opportunities for new programs.
    • Public recognition in supplier conferences or awards.

    Positive reinforcement, anchored in objective non-conformance data, helps build durable, high-performance supplier partnerships.

    Bringing It All Together

    Supplier non-conformance management in aerospace is about more than closing NCRs and SCARs. It is a structured way to protect safety, maintain regulatory compliance, safeguard production schedules, and strengthen your supply base.

    Organizations that move from fragmented spreadsheets and email to integrated, digital workflows gain:

    • Faster, more reliable detection and containment across sites.
    • Traceable, auditable records that stand up to regulatory and customer scrutiny.
    • Rich data to power supplier scorecards, risk assessments, and improvement plans.
    • Stronger collaboration with strategic suppliers built on clear expectations and shared visibility.

    By treating supplier non conformances as a high-value feedback loop rather than a necessary administrative burden, aerospace organizations can turn everyday quality problems into a driver of long-term performance and strategic advantage.