Tag: MES

  • MES vs SCADA: Understanding Two Complementary Manufacturing Systems

    MES and SCADA are not the same system. SCADA focuses on real-time equipment monitoring, data acquisition, supervisory control, alarms, and process control. MES focuses on production execution, work coordination, quality control, traceability, production performance, and operational reporting.

    Comparing MES and SCADA systems reveals they serve different purposes in manufacturing operations. SCADA focuses on real-time equipment monitoring and control, while MES manages production execution, work coordination, quality, and traceability. Understanding these differences helps manufacturing teams choose the right systems without common implementation mistakes.

    Below is a practical comparison of MES vs SCADA capabilities and applications.

    MES vs SCADA: Key Differences

    The primary difference between MES and SCADA systems is that SCADA focuses on real-time data acquisition and process control, whereas MES manages and optimizes the entire production process.

    When integrated, SCADA provides real-time operational data while MES adds structure, context, and business logic, enabling a comprehensive view of manufacturing processes. While SCADA provides immediate insight into equipment performance and operational status, MES translates that data into actionable insights for production management and quality assurance.

    Purpose and Primary Focus

    The fundamental purpose of each system determines where they fit in manufacturing operations.

    SCADA System Purpose

    SCADA, or Supervisory Control and Data Acquisition, systems are designed to monitor and control equipment across large industrial sites, providing real-time data from machines and processes to operators.

    A SCADA system is closest to the machine and process control layer. It supports monitoring equipment, controlling machinery, collecting data from sensors, and helping operators respond quickly when industrial processes drift outside expected limits. In modern manufacturing, SCADA reads raw sensor data from Programmable Logic Controllers (PLCs) and sends alarms if a machine malfunctions.

    SCADA systems focus on:

    SCADA systems detect abnormal conditions and generate alarms to alert operators, which helps teams respond quickly to issues and minimize downtime. This makes SCADA essential when the priority is to control equipment, stabilize process control, and maintain safe production line behavior.

    MES System Purpose

    A manufacturing execution system manages what happens during production. MES software connects production orders, work instructions, quality checks, raw materials, operators, routing, and reporting into a structured operating system for the shop floor.

    MES systems are focused on managing and optimizing production execution and workflows. MES handles transactional data like order numbers, part tracking, and worker schedules. Manufacturing Execution Systems (MES) provide real-time data collection, aggregating production data from machines, operators, and systems to create a complete record of manufacturing activity.

    MES systems focus on:

    MES supports quality assurance by enforcing process rules, collecting inspection data, and maintaining full genealogy and traceability records, which is critical for regulated industries. MES enables standardized workflows and automated decision rules that reduce manual intervention and improve consistency across shifts, lines, and sites.

    Data Types and Time Horizons

    SCADA and MES systems handle different data types and operate on different time scales.

    SCADA Data and Timing

    SCADA operates in real-time, milliseconds, and seconds. It is designed for real time data capture and real time control, especially where immediate action is required to protect equipment, quality, or safety.

    SCADA systems continuously collect data from field devices and display it through Human-Machine Interfaces (HMIs), dashboards, and trends, allowing operators to quickly understand current conditions and system status.

    Typical SCADA data includes:

    SCADA data collection is especially valuable for production monitoring, alarm handling, predictive maintenance inputs, and short-cycle decision making. Historians often store this real time data so engineering teams can review trends, investigate abnormal events, and improve processes.

    MES Data and Timing

    MES operates in shifts, hours, minutes, and days. It may collect real time data from machines, operators, and systems, but its main value is adding production context to all the data coming from the factory floor.

    Typical MES data includes:

    MES connects equipment activity to the production process. For example, SCADA may know that a machine stopped at 10:14. MES can show which order was running, which operator was assigned, what part number was being built, whether raw materials were correct, whether quality control was completed, and whether the downtime reason was a breakdown, changeover, inspection hold, or missing component.

    That context supports more informed decision making. It also helps production managers optimize production, compare performance across shifts, and identify where significant improvements are possible.

    Users and Interface Design

    Each system serves different roles with distinct interface requirements.

    SCADA User Interfaces

    The user base for SCADA includes automation engineers, machine operators, and maintenance technicians. These users need fast, clear visibility into control systems and equipment conditions.

    SCADA user interfaces usually include:

    A SCADA screen is designed for immediate response. Operators need to know whether a pump is running, a valve is open, a tank is filling, a line is stopped, or a process value is outside tolerance. SCADA focuses on the current state of equipment and supports quick control actions.

    MES User Interfaces

    The user base for MES includes plant managers, supervisors, schedulers, and quality assurance inspectors. MES interfaces are designed around production workflows, quality management, and production planning rather than direct control of machinery.

    MES user interfaces usually include:

    MES helps teams coordinate the entire manufacturing process. Operators use MES to follow work instructions, record inspection results, and confirm production steps. Supervisors use MES to see bottlenecks, labor status, and line performance. Quality teams use MES to review defects, audit trails, and traceability records.

    This is why MES and SCADA answer different questions. SCADA asks, “What is the machine doing right now?” MES asks, “What are we making, how well are we making it, and can we prove it was made correctly?”

    System Integration and Architecture Layer

    Understanding where each system fits in the ISA-95 automation pyramid helps clarify their roles.

    SCADA in the Automation Stack

    SCADA sits at Layer 2, Supervisory Control, in the ISA-95 Architecture Layer. In plain terms, this means SCADA is close to equipment supervision and control.

    SCADA integrates with:

    SCADA integration often depends on industrial protocols and connectors such as OPC UA, MQTT, REST APIs, tag bridges, or digital I/O. For brownfield production plants, older control devices may require gateways before they can support seamless data flow to modern systems.

    A historian usually stores high-frequency process values, alarms, and events from SCADA. A data lake can store raw and processed data from SCADA, MES, ERP, and other systems for analytics, predictive maintenance, and digital transformation initiatives.

    MES in the Automation Stack

    MES sits at Layer 3, Manufacturing Operations Management, in the ISA-95 Architecture Layer. In plain terms, MES sits between the plant floor and enterprise resource planning.

    MES integrates with:

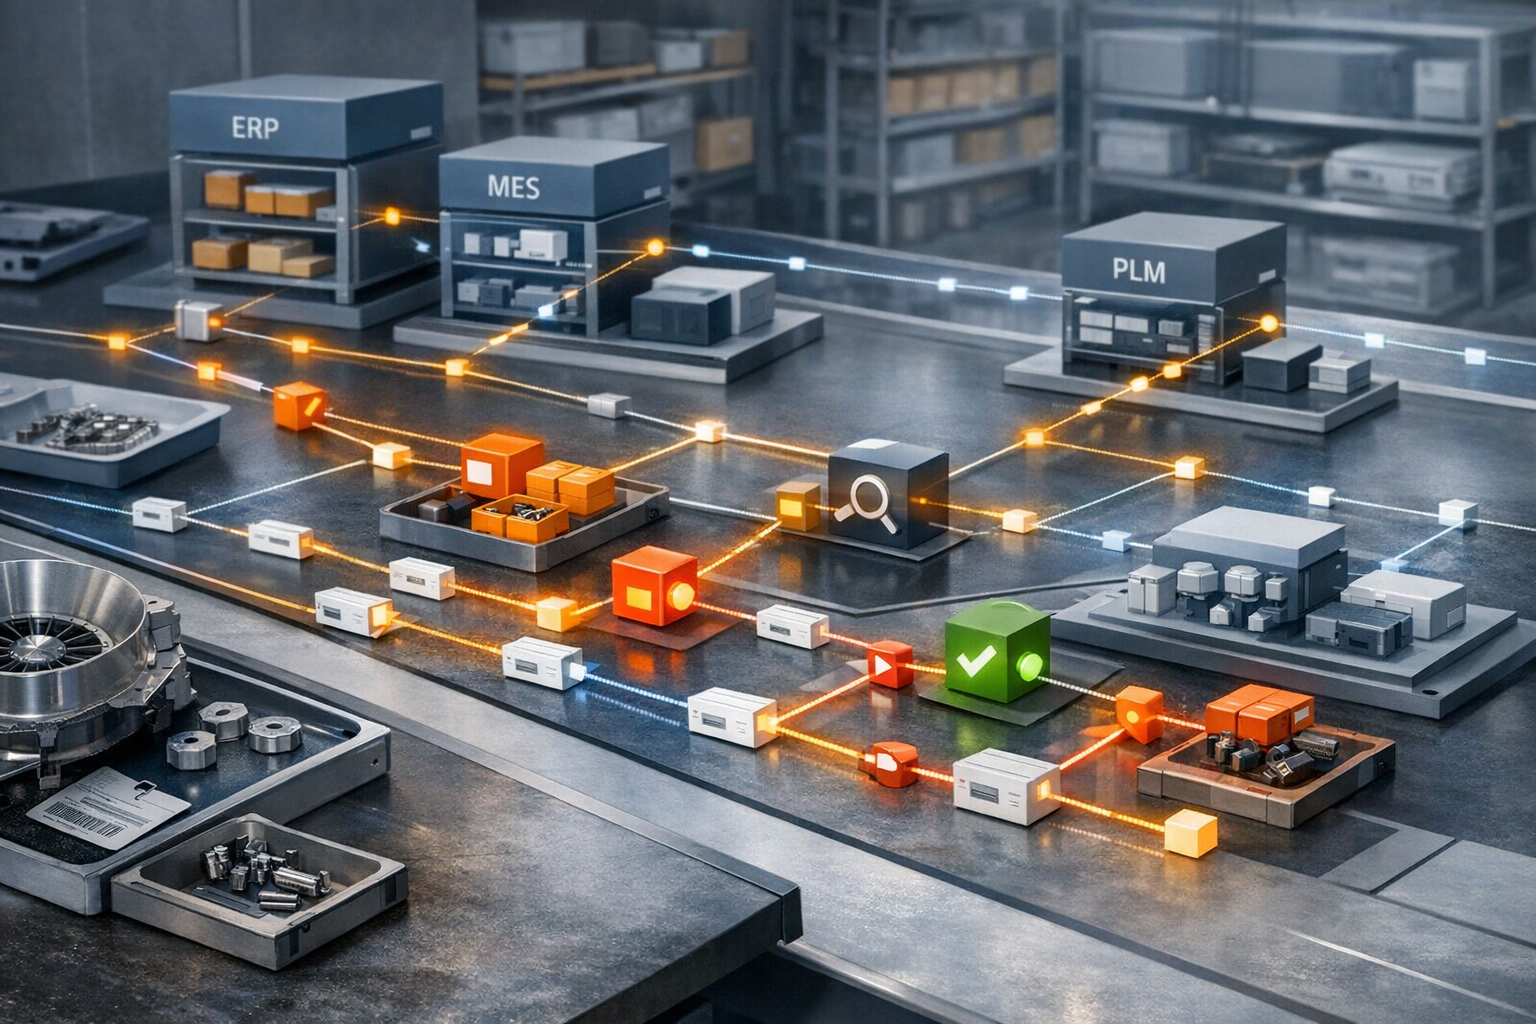
    ERP plans the business. MES executes the production plan. SCADA supervises equipment behavior. PLM defines the product. QMS governs quality rules. Historians and data lakes preserve data for analysis. These systems work best when they are connected without forcing every existing system to be replaced.

    Integrating MES and SCADA systems enhances operational efficiency by allowing for rapid detection of production problems and prompt decision-making, which simplifies procedures and fosters ongoing advancements within manufacturing processes. Integrating MES and SCADA systems also enhances operational efficiency by allowing for rapid detection of production problems and prompt decision-making, which supports more informed choices on the factory floor.

    The combination of SCADA and MES systems within manufacturing operations significantly improves the effectiveness of production processes, bolstering operational efficiency, diminishing wastage, and amplifying visibility throughout the stages of production. The combination of SCADA and MES systems significantly improves the effectiveness of production processes, enhancing operational efficiency, reducing waste, and amplifying visibility throughout the stages of production.

    Integrated MES and SCADA systems enable real-time surveillance and proficient control over production activities, resulting in refined plant functions with an increased capacity to adapt swiftly to modifications in production demands.

    When SCADA is Sufficient

    SCADA may be enough when the main requirement is equipment control, process visibility, and alarm response rather than production workflow coordination.

    SCADA is often sufficient for:

    For example, a utility, water treatment operation, pipeline, or stable continuous production process may prioritize process control, real time monitoring, and rapid alarm response. In these environments, the production process may not require complex routing, work instructions, serial tracking, batch traceability, or supplier documentation.

    SCADA systems can provide strong value in these cases because they support real time data acquisition, equipment visibility, remote control, and minimizing downtime. If the business does not need detailed production orders, quality records, operator task enforcement, or genealogy, a SCADA system and historian may cover most operational requirements.

    However, SCADA alone becomes limited when leaders need to connect equipment data to order context, production planning, quality management, and compliance records.

    When MES is Essential

    MES is essential when manufacturing operations need more than equipment-level visibility. If the business must coordinate people, materials, work instructions, quality checks, routing, and documentation, MES software becomes the execution layer.

    MES is usually needed for:

    This is common in aerospace, defense, medical device, electronics, automotive, and other regulated or high-mix manufacturing processes. In these environments, knowing that a machine ran is not enough. Teams need to know which part was produced, which serial number was installed, which operator completed the step, which inspection result passed, which revision of the work instruction was used, and whether the full record is audit-ready.

    MES supports consistent product quality by enforcing process rules and capturing production data as work happens. It also supports operational efficiency by reducing manual intervention, replacing paper travelers, improving data collection, and helping production managers identify scrap, rework, bottlenecks, and downtime causes.

    For regulated industries, MES is often the difference between having production data and having defensible production records.

    When Both Systems are Needed

    Many manufacturers need both SCADA and MES because the two systems solve different parts of the operational problem.

    Both are often needed in:

    In an integrated model, SCADA provides real time data from equipment and control systems. MES adds production context, quality rules, workflow logic, and traceability. Together, SCADA and MES create a seamless integration between the factory floor and higher level systems.

    For example, SCADA may detect that a production line has slowed. MES can connect that event to the production order, shift, operator, routing step, material lot, and quality status. ERP can then receive accurate updates about production progress, inventory movement, and delivery risk.

    This connected approach improves overall operational efficiency because leaders can move from production monitoring to action. Engineering teams can investigate equipment behavior. Quality teams can review inspection data. Production managers can make schedule decisions. Digital transformation teams can create a reliable data foundation for predictive maintenance, analytics, and continuous improvement.

    When a Lighter Operations Layer Makes Sense

    A full MES is not always the most practical first step. Some aerospace and MRO organizations need execution workflows, traceability, quality checks, supplier visibility, and reporting, but they cannot afford a heavy rip-and-replace implementation.

    A lighter operations layer makes sense for:

    This is where Connect 981 fits. Connect 981 should not be treated as a SCADA replacement. It does not replace real time control, supervisory control, or machine safety functions. It is also not a claim to replace every MES in every environment.

    Connect 981 is better understood as a practical operations layer for aerospace and MRO teams. It helps connect shop floor execution, work instructions, quality checks, traceability, supplier data, and reporting without forcing every existing system to be removed.

    For teams with ERP, PLM, QMS, SCADA, or legacy systems already in place, Connect 981 can support the missing execution layer: the place where operators complete work, inspectors capture quality data, suppliers share documentation, and leaders see production performance. This is especially useful when full MES deployment would be too slow, too costly, or too disruptive.

    Common Implementation Mistakes

    The biggest mistake is treating MES and SCADA as interchangeable systems. They are complementary, but they should not be forced into each other’s role.

    Common mistakes include:

    SCADA is not designed to manage operator workflows, quality forms, batch records, genealogy, or compliance documentation. Trying to make SCADA do those jobs often creates manual workarounds and weak traceability.

    MES is not designed to control machinery in milliseconds. Expecting MES to perform real time control or machine safety functions creates risk because process control belongs in PLCs, DCS, and SCADA systems.

    ERP disconnection is another common issue. If enterprise resource planning sends production orders to the plant but does not receive accurate updates from the shop floor, production planning becomes unreliable. Teams then build spreadsheet bridges, manual reports, and email-based status updates. Those workarounds are fragile, slow, and difficult to audit.

    A better approach is to define the role of each system clearly: SCADA for equipment supervision and control, MES for production execution and workflow management, ERP for enterprise planning, PLM for engineering data, QMS for quality governance, historians for process data, and data lakes for broader analytics.

    MES vs SCADA: Choosing the Right Approach

    Choose SCADA when equipment control, real time monitoring, process visualization, alarm response, and data acquisition are the primary needs.

    Choose MES when production execution, work instructions, quality tracking, traceability, production orders, downtime analysis, and workflow management are essential.

    Choose integrated MES and SCADA systems when manufacturing operations need both equipment-level visibility and production-level context. This is the right direction for comprehensive manufacturing operations, regulated production, complex production lines, and digital transformation programs that require complete operational visibility.

    Choose a lighter operations layer when a full MES is too heavy, but the business still needs structured execution workflows, quality checks, supplier visibility, batch traceability, and reporting. For aerospace and MRO teams, Connect 981 provides a practical way to connect shop floor execution, quality, supplier data, and compliance workflows without replacing every existing system.

    The best decision is rarely “MES vs SCADA” as competitors. The better question is: which layer is missing from your industrial automation stack?

    If your team needs to connect shopfloor execution, quality records, supplier workflows, and compliance reporting without ripping out SCADA, ERP, PLM, QMS, or other existing systems, request a demo to see how Connect 981 works in action.
  • Integrating Non-Conformance Management With ERP and MES in Aerospace

    Integrating Non-Conformance Management With ERP and MES in Aerospace

    In aerospace manufacturing and MRO, non-conformance reports (NCRs) do not live in a vacuum. Every quality decision affects production schedules, inventory availability, cost accounting, and—ultimately—flight safety. When NCR workflows are disconnected from enterprise resource planning (ERP) and manufacturing execution systems (MES), organizations end up with blind spots, double entry, and conflicting data that erode both efficiency and compliance.

    Integrating non-conformance management with ERP and MES creates a single coherent story across work orders, inventory, and quality records. Done well, it lets teams see—within minutes—what material is affected, which operations are blocked, what the cost impact is, and when a line can restart. Done poorly, it introduces new failure modes, data inconsistencies, and audit risks.

    For teams putting erp / mes / plm interoperability into daily operation, data mapping and system interoperability, MES execution control, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on ERP, MES, and PLM integration paths, quality management workflows, a connected execution platform, Connect 981’s aerospace execution solutions, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    This article explains how to integrate non-conformance management with ERP and MES in aerospace environments. It focuses on key data flows, typical integration scenarios, and design considerations that support reliability, traceability, and regulatory compliance.

    For a broader view of process design before you tackle integration, see our guide on integrated aerospace quality workflows.

    Why NCR Integration With ERP and MES Matters

    Aerospace organizations often start with quality-managed NCRs in a standalone system or spreadsheet. Over time, they discover that almost every disposition decision requires data held elsewhere: work order status in MES, inventory balances in ERP, contract requirements in a customer portal, and so on. Integration closes these gaps.

    Linking quality events to work orders and routings

    When an inspector raises an NCR, they usually do it in the context of a specific job: a work order, operation, or task. If your NCR system is not tied to ERP and MES, you immediately face problems:

    • Ambiguous context: NCRs reference work orders or operations via free-text fields, increasing the risk of mis-typed IDs and mislinked records.
    • Lost history: Planners and engineers viewing work orders in ERP or MES cannot see associated NCRs without separate searches.
    • Inconsistent status: A work order may look released and executable in MES even though a critical NCR is still open in the quality system.

    Integration solves this by ensuring each NCR is anchored to authoritative production data:

    • The NCR record references the exact work order, operation, operation sequence, and resource from MES/ERP.
    • Work order screens show links or badges indicating open NCRs and their dispositions.
    • Routings and travelers reflect holds or additional steps (e.g., rework operations) derived from NCR decisions.

    Accurate inventory, WIP, and cost accounting

    Every NCR disposition—rework, scrap, or use-as-is—affects quantities and costs. Without integration, these updates depend on manual re-keying into ERP, which is slow and error-prone.

    Key impacts that should be automated via integration include:

    • Inventory balances: Moving parts to quality hold, returning them to stock, scrapping them, or issuing replacements.
    • WIP (work in process): Adjusting WIP quantities when assemblies are partially scrapped or reworked.
    • Cost allocation: Capturing labor, material, and overhead associated with rework or scrap to the right cost centers, work orders, or projects.
    • Customer or contract impacts: Flagging costs that must be charged to a specific program, contract line item, or warranty account.

    With integrated systems, an approved disposition in the NCR workflow can automatically trigger the right ERP transactions—such as inventory adjustments, additional operations, or cost postings—removing the need for duplicate data entry.

    Real-time impact assessment for production planning

    Production planners, schedulers, and program managers need to answer questions such as:

    • How many assemblies are blocked by quality holds?
    • Which lines are at risk if this NCR leads to scrap instead of rework?
    • Do we have enough conforming material to meet this week’s ship dates?

    When NCR, ERP, and MES data are synchronized, planning tools can show the impact of quality events in real time:

    • Work orders and operations affected by open NCRs are clearly visible in planning boards.
    • Inventory availability calculations reflect parts under quality hold.
    • Scenario planning can incorporate potential scrap rates or extended lead times driven by rework.

    Core Data Elements Shared Across Systems

    Successful integration starts with a precise understanding of which data elements are owned by which system—and how they should be referenced in NCR workflows.

    Parts, serial numbers, and configuration baselines

    Aerospace quality decisions hinge on precise identification of parts and configurations. Typical shared elements include:

    • Part and assembly identifiers: Part numbers, revisions, and descriptions managed in ERP/PLM.
    • Serial/lot/batch numbers: Unique identifiers needed for traceability to specific aircraft, engines, or line-replaceable units.
    • Configuration baselines: Which drawing revision, bill of material (BOM), and process specification applied when the unit was built or serviced.

    From an integration standpoint, your NCR system should never maintain its own “shadow” master list of parts or serials. Instead, it should reference authoritative master data from ERP and, where applicable, PLM or configuration management systems.

    Work orders, operations, and resources

    Most NCRs relate to an execution context, which lives primarily in MES and/or ERP:

    • Work orders / shop orders: Job identifiers, quantities, due dates, and related projects or contracts.
    • Operations / tasks: Routing steps, standard work instructions, and inspection operations.
    • Resources: Machines, tools, and cells, plus the operators or technicians executing the work.

    Integrating non-conformance management with ERP and MES means NCR records can:

    • Automatically pull in the correct work order and operation when raised from an MES screen.
    • Associate resource usage (machine, fixture, tool) with the deviation to support root cause analysis.
    • Feed back rework operations or additional inspections into routings as part of approved dispositions.

    Suppliers, customers, and contracts

    External stakeholders are a critical part of aerospace non-conformance management:

    • Suppliers: Vendor IDs, purchase orders, delivery notes, and certificates of conformity.
    • Customers: Contract references, customer-specific quality clauses, and deviation permit processes.
    • Regulatory and contractual constraints: Requirements for notification, approval workflows, and retention periods.

    Quality systems must use supplier and customer master data from ERP/CRM to ensure that notifications, charge-backs, and reporting align with commercial agreements. For example, an NCR against incoming material should be directly linked to the originating PO and supplier record, not just recorded via free text.

    Typical Integration Scenarios

    Most aerospace organizations converge on a handful of common NCR–ERP–MES integration patterns. The specifics vary, but the underlying scenarios are remarkably consistent.

    Creating NCRs from ERP/MES context

    The most visible integration requirement is the ability to launch an NCR from within ERP or MES while preserving context:

    • Inspector in MES identifies a defect during an in-process check and raises an NCR against the current operation.
    • Receiver in ERP identifies a discrepancy at incoming inspection and triggers an NCR from the purchase order or receipt line.
    • Planner finds a documentation error on a work order and opens an NCR tied to that job.

    Key design choices include:

    • Single sign-on and deep links: Users click a button in MES/ERP and are taken directly to a pre-populated NCR form.
    • Pre-filled data: Work order IDs, part numbers, operations, and supplier/customer data are automatically copied from ERP/MES into the NCR.
    • Bidirectional references: The NCR stores the originating ERP/MES keys, and the ERP/MES record stores a link or reference back to the NCR.

    Applying holds and releases in inventory and WIP

    Once an NCR is raised, the organization must prevent suspect material from advancing. Integration enables this without manual phone calls or emails:

    • Inventory holds: An NCR on incoming material automatically sets the relevant lots or serials to a quality-hold status in ERP.
    • WIP holds: Open NCRs against certain work orders or operations can block movement to the next operation in MES.
    • Release logic: When an NCR is dispositioned and containment is verified, the integration can remove holds or redirect units to rework operations.

    Design considerations:

    • Define which system is the system of record for hold/release status (often ERP for stock, MES for WIP).
    • Ensure that NCR workflows cannot close without confirming that physical inventory/WIP status has been updated.
    • Provide clear visibility in ERP/MES screens when a part or job is on hold because of an NCR.

    Posting rework, scrap, and use-as-is decisions

    Disposition drives financial and operational outcomes. Integration should translate quality decisions into concrete ERP and MES transactions:

    • Rework: Create or modify operations in MES, issue additional materials, and capture labor hours against rework tasks.
    • Scrap: Post scrap transactions in ERP to remove inventory/WIP and book the cost to the appropriate account or project.
    • Use as-is / deviation: Record engineering approvals in the NCR system and, where required, update configuration or as-built records in ERP/MES.

    These postings should be as automated as practical, based on pre-defined mapping between disposition codes and ERP/MES transactions. At the same time, aerospace organizations must ensure that IT and compliance teams review any automation to verify it meets internal control requirements.

    Technical Integration Approaches

    No single integration pattern is universally correct. The right design depends on your existing architecture, vendor capabilities, regulatory expectations, and internal IT standards. Most aerospace companies mix several of the approaches below.

    APIs, middleware, and event-driven workflows

    Modern NCR, ERP, and MES platforms often expose REST or SOAP APIs and can publish or consume events. Typical choices include:

    • Direct API integrations: NCR application calls ERP/MES APIs (or vice versa) to retrieve master data and post transactions.
    • Middleware / ESB: An integration layer orchestrates data flows, transforms payloads, and centralizes error handling.
    • Event-driven architecture: Systems publish business events (e.g., “NCRCreated”, “NCRDispositioned”) to a message bus, and subscribers react by updating their own data stores.

    Event-driven designs can reduce coupling and improve scalability but require robust monitoring and governance to avoid silent failures.

    Data mapping and master data management

    Technical plumbing alone is not enough. You must define consistent semantics across systems:

    • Standardized codes for dispositions, defect types, causes, and corrective actions.
    • Common identifiers for parts, customers, suppliers, and resources.
    • Clear ownership rules for who can create or change master data and how those changes propagate.

    Master data management (MDM) practices help here. Whether you use a dedicated MDM tool or governance processes around ERP, the goal is to ensure that all systems refer to the same business objects in the same way.

    Handling offline and multi-site environments

    Aerospace operations often span multiple plants, test facilities, and field locations—some with intermittent connectivity. Integration designs should account for:

    • Local capture: Ability to record NCRs offline on tablets or local systems, then synchronize when connectivity is restored.
    • Latency-aware behavior: Clear rules about what actions can proceed without immediate confirmation from ERP/MES (e.g., temporary local holds vs. enterprise-wide stock status changes).
    • Site-specific variations: Different ERPs or MES instances at different plants, with a central quality system or vice versa.

    For multi-site environments, consider patterns such as hub-and-spoke integration, regional middleware instances, or phased rollouts that allow each site to stabilize before expanding the footprint.

    Designing for Reliability and Traceability

    In aerospace, an integration that “usually” works is not good enough. Systems must support rigorous traceability, predictable behavior under failure, and clear audit trails.

    Error handling and reconciliation

    Integration errors will occur: network timeouts, data validation failures, or mismatched identifiers. Designing for reliability means:

    • Idempotent operations: Replaying integration messages without creating duplicate transactions.
    • Queued retries: Automatic retries for transient failures with backoff policies.
    • Dead-letter handling: A controlled queue or worklist for messages that cannot be processed automatically.
    • Reconciliation reports: Periodic checks comparing key fields (e.g., hold statuses, scrap quantities) across systems to detect drifts.

    Audit trails across system boundaries

    Regulators and customers expect you to prove not only what decisions were made, but also how those decisions flowed through your systems. Practical measures include:

    • Storing correlation IDs that link NCR records to ERP/MES transactions.
    • Logging which integration process invoked which API, with timestamps and outcomes.
    • Ensuring that any automated changes (e.g., inventory status updates from an NCR decision) are traceable to the originating NCR and user.

    These capabilities simplify audits by showing a clear, end-to-end chain from defect discovery through disposition, execution, and financial posting.

    Change management and regression testing

    As processes, systems, and regulations evolve, integrations must change. Before deploying modifications:

    • Use representative test data that includes critical cases (serialized parts, safety-critical items, customer-specific rules).
    • Run end-to-end regression tests that validate not just data movement but also business outcomes (e.g., holds applied, costs posted correctly).
    • Involve quality, production, finance, and compliance stakeholders in sign-off.

    IT and compliance teams should jointly agree on the level of validation required for each type of integration change, especially where it may impact regulatory evidence or financial postings.

    Governance and Continuous Improvement

    NCR–ERP–MES integration is not a one-time project. As product lines, suppliers, customers, and regulations change, so do integration requirements. Governance keeps the solution aligned with the business.

    Defining ownership for integrated processes

    Clarify who owns what:

    • Process ownership: Quality leaders define how NCR workflows should behave and what data they require.
    • System ownership: IT or application owners manage the configuration and technical integrity of ERP, MES, and quality systems.
    • Integration ownership: An integration architect or team maintains the contracts, data mappings, and monitoring around cross-system flows.

    Having named owners makes it easier to resolve issues, prioritize enhancement requests, and manage change.

    Monitoring data quality and integration KPIs

    Beyond technical uptime, monitor indicators that reveal whether integrated processes actually work for the business. Examples include:

    • Percentage of NCRs created from ERP/MES context versus manual entry.
    • Frequency of mismatches between NCR dispositions and ERP inventory or cost data.
    • Number of integration-related incidents discovered during audits.
    • Mean time to apply holds in ERP/MES after NCR creation.

    These metrics help you identify where integrations need refinement or additional training.

    Iterating integration as business needs evolve

    As you mature, you may:

    • Extend integration to new plants or maintenance depots.
    • Incorporate additional systems (e.g., PLM, supplier portals, or field service tools).
    • Automate more of the NCR lifecycle where risk and internal controls allow.

    Approach this as a continuous improvement program, not a one-time rollout. Regularly revisit your integration design in light of new customer requirements, regulatory interpretations, and internal lessons learned.

    Putting It All Together

    Integrating non-conformance management with ERP and MES is a cornerstone of modern aerospace quality operations. By anchoring NCRs to production, inventory, and financial data, organizations can:

    • Reduce manual data entry and associated errors.
    • Provide real-time visibility into the impact of quality issues.
    • Strengthen traceability from defect detection through disposition and execution.
    • Improve readiness for regulatory and customer audits.

    There is no single blueprint that fits every aerospace organization. The right integration architecture depends on your current systems, regulatory posture, and risk tolerance. What matters most is that IT, quality, production, and finance jointly define how data should flow, validate the design against compliance requirements, and treat integration as a living capability that evolves with the business.

  • Applying ISO 22400 in Aerospace and MRO: KPI Use Cases and Patterns

    Applying ISO 22400 in Aerospace and MRO: KPI Use Cases and Patterns

    ISO 22400 defines a common language for manufacturing KPIs. Aerospace manufacturing and Maintenance, Repair, and Overhaul (MRO) environments operate under intense regulatory, safety, and traceability pressures, but they still benefit from standardized KPI terminology. Applying ISO 22400 here is less about inventing new aerospace metrics and more about mapping existing practices to clearly defined concepts that work across plants, partners, and digital systems.

    This article explains where ISO 22400 fits in aerospace and MRO, shows practical KPI use cases, and highlights how to combine standard definitions with sector-specific indicators such as turnaround time and traceability. It focuses on patterns and examples, not on prescribing a single KPI set or giving performance-improvement advice.

    For teams putting traceability and genealogy into daily operation, MES execution control, part genealogy and traceability, part traceability and as-built evidence help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on MRO execution workflows, shop floor execution control, a connected execution platform, Connect 981’s aerospace execution solutions, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    For a broader view of the standard itself and how it structures manufacturing KPIs across industries, see our overview of ISO 22400-aligned aerospace and MRO reporting.

    Aerospace and MRO KPI Challenges

    Aerospace and MRO organizations already report on utilization, schedule adherence, quality, and resource consumption. The difficulty is ensuring that metrics mean the same thing across facilities, programs, and suppliers, and that they remain auditable over long time horizons.

    High stakes for safety, traceability, and compliance

    In aerospace and MRO, metrics underpin decisions that affect airworthiness and regulatory compliance. Authorities and customers expect clear evidence for how aircraft, components, and maintenance activities were planned, executed, and released.

    • Safety and airworthiness: KPIs around maintenance execution, inspection findings, rework, and release status must be tightly linked to configuration and documentation baselines.
    • Traceability: Every part, task, and sign-off may need to be traced across multiple systems (PLM, ERP, MES/MRO, QMS). KPIs built on ambiguous definitions of time or quantity risk undermining that traceability.
    • Compliance: Regulators focus on whether records are complete, consistent, and understandable. KPI definitions that change from site to site can create gaps during audits.

    ISO 22400 does not define aerospace regulations. Instead, it offers standardized KPI concepts (for example, equipment utilization or order execution reliability) that can be aligned with regulated processes and record sets.

    Complex routings, configurations, and rework

    Aerospace manufacturing and MRO environments handle complex assemblies, long routings, and frequent engineering changes. Maintenance events, in particular, often deviate from plan as findings drive additional scope.

    • Non-linear work: Jobs may move backward in the routing because of rework, waiting for parts, or additional inspections, complicating lead time and utilization calculation.
    • Configuration variation: The same work center may handle multiple aircraft types, modification standards, or customer-specific configurations.
    • Extended dwell times: Aircraft or large assemblies may spend days or weeks at a given station while multiple work packages proceed in parallel.

    ISO 22400’s neutral definitions of time categories, equipment states, and order-related KPIs help bring structure to this complexity without prescribing aerospace-specific routing logic.

    Multi-party collaboration across OEMs, MROs, and suppliers

    Programs typically involve OEMs, tiered suppliers, independent MROs, and airline or operator maintenance teams. Each organization may use different systems, but they must still align on what reported metrics mean.

    • Supplier performance reporting: Contracts often reference utilization, turnaround, or defect-related indicators. Unclear definitions can create disputes.
    • Shared assets: Test cells, ground support equipment, and specialized tooling may be used by multiple organizations or sites.
    • Joint improvement initiatives: Cross-company projects need comparable KPIs to identify bottlenecks or validate improvements.

    Using ISO 22400 as a reference vocabulary helps align KPIs across organizations, even when each party uses its own software stack and industry-specific metrics.

    Where ISO 22400 Fits in Aerospace and MRO

    ISO 22400 is an industry-neutral standard for manufacturing operations KPIs. Aerospace and MRO organizations can adopt its concepts selectively, focusing on the KPIs that best match their production and maintenance workflows.

    Aligning core production and maintenance KPIs

    Many aerospace and MRO metrics correspond directly to ISO 22400 KPI families, even if they currently use different names. Examples include:

    • Equipment-oriented KPIs: Utilization of test cells, paint booths, autoclaves, and ground support equipment.
    • Order-related KPIs: Adherence of maintenance events, work orders, or modification campaigns to planned time structures.
    • Resource-related KPIs: Labor hours consumed versus planned, or material usage tied to specific operations.

    Mapping these to ISO 22400 terminology improves clarity. For instance, a site that reports the percentage of planned time that a test cell is actually operating can align that metric with the standard’s definitions of equipment utilization rather than inventing a facility-specific term.

    Using standardized definitions in supplier agreements

    Supplier and MRO contracts often specify KPI-based service levels. ISO 22400 can provide unambiguous KPI descriptions in these agreements:

    • Referencing an ISO 22400-aligned definition of a utilization or availability indicator when discussing asset access or readiness.
    • Using order execution-related KPIs for agreed reporting on maintenance event adherence to plan.
    • Defining units of measure, trend directions, and time behaviors consistently, so monthly dashboards reflect the same logic at every site.

    This approach does not turn ISO 22400 into a regulatory requirement; it simply reduces interpretation risk when multiple parties reference the same concept.

    Supporting cross-site performance comparisons

    Large aerospace OEMs and MRO networks often operate multiple facilities globally. Even when each site follows local regulations and customer requirements, leadership still wants to compare performance.

    • Consistent KPI semantics: Sites can continue using local dashboards, but the underlying KPI definitions are harmonized with ISO 22400 where possible.
    • Comparable time categories: Planned, unplanned, and idle time categories follow consistent meaning, so utilization and order execution reliability can be aggregated.
    • Neutral layer across verticals: Organizations that serve aerospace plus other sectors (for example, industrial gas turbine service) can use ISO 22400 as a common baseline while layering sector-specific metrics on top.

    Example Use Cases of ISO 22400-Aligned KPIs

    The following examples illustrate how ISO 22400 concepts can be applied to aerospace and MRO scenarios. They are patterns, not prescriptions, and they do not expand the standard’s formal KPI list.

    Equipment utilization for critical ground support assets

    Ground support equipment (GSE) such as engine test cells, jacks, docking systems, hoists, and specialized tooling are high-value, capacity-limiting assets. Under- or over-utilization affects both cost and schedule.

    ISO 22400 defines equipment-related KPIs based on time categories and equipment states. When applied to GSE:

    • State definition: RUN, IDLE, STOP, or other states can be mapped to the real behavior of test stands and docking systems.
    • Time allocation: Planned versus unplanned downtime, setup time, and active operation periods are clarified.
    • Utilization indicator: A utilization KPI can be defined as the ratio of actual productive time to a defined planned time window, aligned with ISO 22400 terminology.

    This yields a consistent measure of how intensively GSE is used across shops and sites, even if their schedules and aircraft mixes differ.

    Order execution reliability for maintenance events

    Maintenance events—such as C-checks, heavy checks, or modification campaigns—can be viewed as production orders in ISO 22400 terms. The standard’s order-related KPIs provide a structured way to describe how these events progress versus plan.

    • Planned time structure: The event has a planned start, planned finish, and possibly intermediate milestones.
    • Actual execution: Actual times are captured from MRO execution systems, including delays due to findings, parts, or engineering clarifications.
    • Order execution reliability: ISO 22400-aligned KPIs can describe how closely execution followed the planned time structure or quantity profile.

    These indicators do not replace aerospace-specific turnaround or on-time-release metrics. Instead, they provide neutral, comparable views of schedule adherence and execution variability that can be used for internal analysis or supplier reporting.

    Resource-related KPIs for labor and parts usage

    Labor hours and parts consumption are central to aerospace and MRO economics. ISO 22400’s resource-related KPI concepts allow these to be linked consistently to orders, equipment, and time periods.

    • Labor indicators: Personnel-related KPIs can express, for example, total maintenance labor hours associated with a work order or area over a given shift.
    • Material indicators: Material consumption KPIs can associate parts usage with specific operations or events, supporting cost and reliability analysis.
    • Energy indicators: Energy usage for large assets (such as engine test cells or autoclaves) can be treated as a resource KPI aligned to specific orders.

    Aligning resource-related KPIs with ISO 22400 terms helps ensure that, when labor or material intensities are compared between facilities, they rest on a shared conceptual basis.

    Combining ISO 22400 with Aerospace-Specific Metrics

    Aerospace and MRO teams need KPIs that go beyond the neutral scope of ISO 22400. The goal is not to force all metrics into the standard, but to clearly distinguish which indicators are ISO 22400-based and which are aerospace-specific.

    Turnaround time breakdowns and on-time release

    Turnaround time (TAT) and on-time release are central to MRO performance. These KPIs typically combine:

    • Total elapsed time between arrival and release.
    • Breakdowns by phase (induction, disassembly, inspection, repair, reassembly, test, closing).
    • Customer- or contract-specific commitments for on-time delivery.

    These composite metrics are not defined in ISO 22400. However, many of their building blocks—such as time in particular states or adherence to planned time structures—map well to ISO 22400 time and order-related concepts. Organizations can:

    • Use ISO 22400-aligned KPIs at the level of work centers, operations, and equipment.
    • Construct TAT and on-time-release metrics on top, labeled clearly as aerospace-specific.

    Regulatory auditability and record linkage

    Regulators and customers focus on whether maintenance and manufacturing records are complete and coherent. KPI design must support this auditability.

    • Transparent definitions: ISO 22400 encourages specifying units, applicable time behaviors, and trend directions. This documentation is useful during audits, even when the KPI itself is not required by regulation.
    • Stable semantics: Once a KPI definition is agreed, changes are versioned and recorded, so historic reports remain interpretable.
    • Linkages to records: KPIs reference underlying events, logs, and approvals stored in PLM, ERP, MES/MRO, and QMS systems.

    By grounding KPIs in ISO 22400 concepts, teams can more easily show how high-level indicators relate to the detailed records that auditors and airworthiness authorities examine.

    Integrating traceability indicators with standardized KPIs

    Aerospace traceability indicators—such as the percentage of parts with complete back-to-birth records or the number of tasks with missing sign-offs—are typically sector-specific. They sit alongside standard KPIs rather than inside ISO 22400’s formal list.

    One effective pattern is:

    • Use ISO 22400-aligned KPIs for time, quantity, and resource aspects of operations.
    • Define separate traceability indicators that reference the same orders, equipment, and time periods.
    • Ensure dashboards show clearly which indicators are ISO 22400-based and which are internal, aerospace-specific constructs.

    Digital Platforms and Integration in Aerospace and MRO

    Aerospace and MRO operations rely on multiple tightly integrated systems. ISO 22400 offers a conceptual model that digital platforms can use to keep KPI definitions consistent across this ecosystem.

    How platforms like the ISO 22400 manufacturing KPIs hub map ISO 22400 concepts

    Digital operations platforms that support ISO 22400 concepts typically:

    • Model equipment, work centers, and work units using definitions compatible with IEC 62264 and ISO 22400.
    • Translate raw events (for example, equipment state changes) into standardized time categories.
    • Provide libraries of ISO 22400-aligned KPIs that customers can adopt or extend.

    Aerospace and MRO users can then layer domain-specific workflows—such as digital work instructions, airworthiness releases, and findings management—on top of a shared KPI foundation.

    Connecting PLM, ERP, MES, and QMS in regulated environments

    In a regulated aerospace environment, systems are often validated and tightly controlled. ISO 22400 does not impose a particular architecture, but it helps with integration design:

    • PLM: Defines product structures, configurations, and approved repairs or modifications that may influence how KPIs are segmented.
    • ERP: Manages orders, contracts, and financial views that align with order-related KPI hierarchies.
    • MES/MRO systems: Track execution states at work centers and operations, providing the raw events and quantities underlying KPIs.
    • QMS: Holds nonconformance, concession, and corrective action data that can be correlated with performance metrics.

    By agreeing on ISO 22400-based KPI semantics, integration interfaces can exchange performance information without redefining basic concepts every time a new connection is built.

    Ensuring KPI definitions remain transparent and auditable

    Given the long service life of many aerospace platforms, KPIs must remain interpretable for years. Digital platforms can support this by:

    • Storing KPI definitions, including mappings to ISO 22400 concepts, as configuration items with version history.
    • Documenting any extensions or sector-specific metrics separately from the standard-aligned set.
    • Providing drill-down from aggregated KPI values to underlying events, orders, and records.

    This level of transparency is useful for internal reviews and external audits alike.

    Practical Adoption Tips for Aerospace and MRO Teams

    Adopting ISO 22400 in aerospace and MRO is a matter of careful alignment and communication rather than wholesale replacement of existing KPIs.

    Engaging quality and regulatory stakeholders early

    Because KPIs feed into audit trails and, in some cases, into regulated reports, quality and regulatory teams should participate from the beginning.

    • Review ISO 22400 concepts jointly with operations and IT, focusing on how they map to current metrics.
    • Identify any constraints arising from regulations, customer contracts, or approvals that affect KPI changes.
    • Agree on how KPI definitions will be documented, controlled, and communicated to auditors and customers.

    Documenting which KPIs are ISO 22400-based and which are not

    Clarity about scope is essential. A straightforward approach is to classify indicators into two groups:

    • ISO 22400-aligned KPIs: Indicators whose names, meanings, time behaviors, and measurement objects match the standard’s conceptual definitions.
    • Aerospace-specific metrics: Composite indicators such as TAT breakdowns, traceability scores, or customer-specific service-level metrics that extend beyond the standard.

    Labeling dashboards and reports accordingly prevents confusion and avoids implying that all aerospace metrics are part of ISO 22400.

    Building a roadmap for harmonized KPI reporting

    Most organizations will evolve toward ISO 22400 adoption rather than switching everything at once. A practical roadmap often includes:

    1. Inventory: Catalog existing KPIs used in manufacturing and MRO operations.
    2. Mapping: Identify which existing metrics correspond closely to ISO 22400 concepts and where gaps or differences exist.
    3. Pilots: Harmonize a small set of high-value KPIs across two or three facilities.
    4. Governance: Establish a change-control process for KPI definitions, including representation from operations, IT, quality, and regulatory teams.
    5. Rollout: Extend harmonized definitions to more sites, suppliers, and dashboards as systems and contracts are updated.

    Throughout this journey, the objective is not to eliminate aerospace-specific metrics but to ensure that, where ISO 22400 concepts apply, they are used consistently.

    Conclusion

    ISO 22400 does not tell aerospace and MRO organizations which KPIs to use or how to meet regulatory requirements. Its value lies in establishing a shared vocabulary and structure for core manufacturing and maintenance indicators. By aligning equipment, order, and resource-related KPIs with ISO 22400, aerospace manufacturers and MRO providers can make their reporting more comparable, auditable, and integration-friendly—while continuing to use sector-specific metrics such as turnaround time, traceability indicators, and on-time release.

    Using ISO 22400 as a neutral foundation, organizations can connect PLM, ERP, MES/MRO, and QMS data into coherent performance views that serve both operational decision-makers and external stakeholders, without constraining their strategic choices or domain-specific KPI designs.

  • Aerospace Manufacturing Operations: Executive Guide for Modern Programs

    Aerospace Manufacturing Operations: Executive Guide for Modern Programs

    The aerospace industry in 2025 and 2026 faces a straightforward reality: backlogs are growing, fleets are aging, and the operational approaches that worked a decade ago cannot deliver the throughput required today. COOs and plant leaders must answer a practical question over the next 12 to 24 months. What should we actually do differently in our operations?

    Aerospace manufacturing operations represent the integrated system where precision engineering meets rigorous production standards. This encompasses concept design through industrialization, sourcing raw materials like titanium alloys and ceramic matrix composites, high-volume production via CNC machining and additive manufacturing, final assembly with automated systems, extensive testing, certification under AS9100 and FAA frameworks, delivery to OEMs, and ongoing aftermarket MRO involving disassembly, inspection, repair, and recertification.

    This executive guide connects ERP, MES, quality systems, workforce management, and digital execution strategies into a coherent operational framework. The perspective comes from Connect981, a B2B SaaS platform built specifically for aerospace manufacturing and MRO realities rather than generic discrete manufacturing.

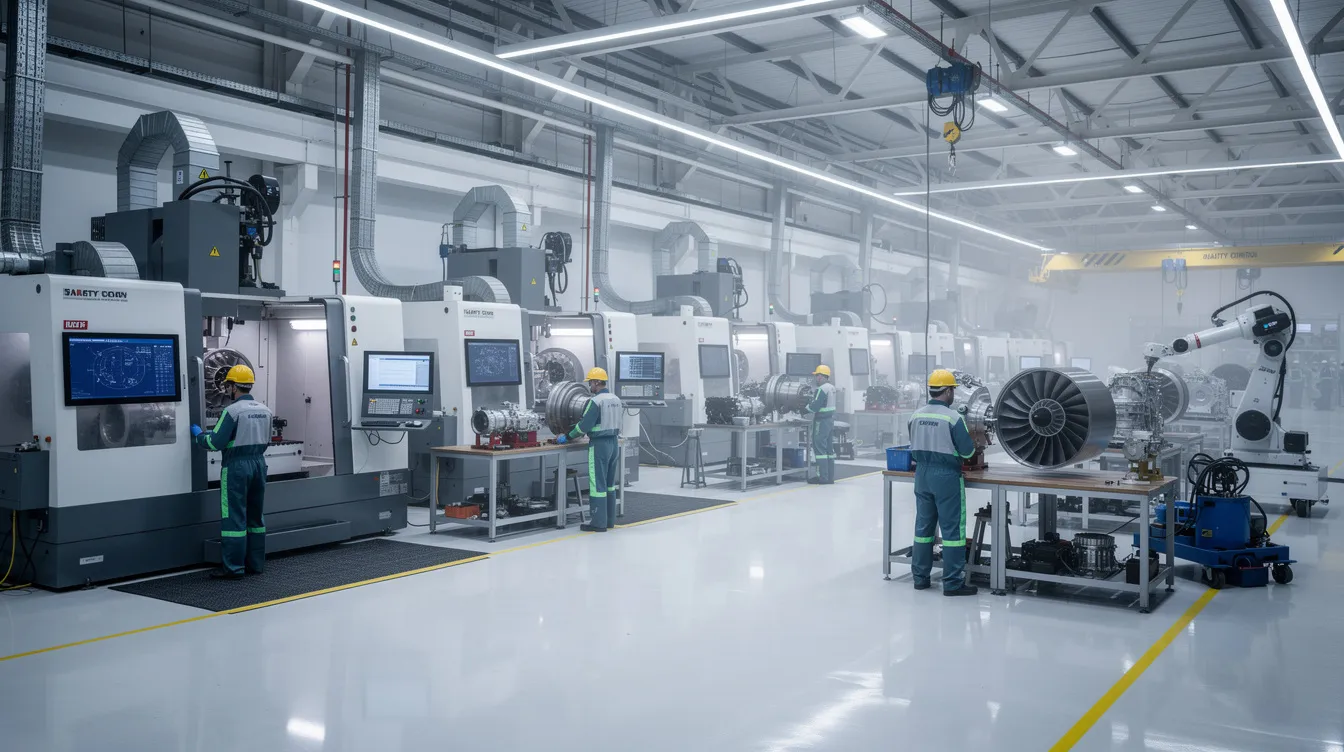
    The image depicts a busy aerospace factory floor, showcasing precision machinery and workers engaged in the aerospace manufacturing process within a controlled environment. This setting highlights advanced manufacturing technologies and emphasizes the importance of safety and performance standards in the aerospace industry.

    The State of Aerospace Manufacturing and MRO in 2025–2026

    The global aerospace parts manufacturing market stood at approximately $930 billion in 2024, projected to reach $1.2 trillion by 2034 with a CAGR of 3.8%. North America continues to dominate due to its mature ecosystem, defense contracts, and leadership in advanced manufacturing technologies including digital twins and AI-powered quality control.

    Key demand drivers shaping aerospace operations include:

    • Commercial aviation recovery with Airbus holding 8,617 outstanding orders and Boeing at 6,528 as of May 2025, translating to roughly 5,000 undelivered aircraft
    • Defense modernization accelerating hypersonics, UAVs, and autonomous systems requiring high production rates
    • Commercial space expansion via reusable launch vehicles and satellite constellations
    • Fleet aging to 11.3 years from 9.7 in 2018, with airlines extending leases 11% more in 2024 versus 2018

    Operational realities include chronic supply chain instability with 12 to 24 month lead times for titanium alloys, semiconductor shortages, and labor constraints with over 60% of aerospace manufacturers citing workforce issues. Certification timelines stretch 6 to 12 months for simple parts and up to 7 years for complex systems such as engines or airframes.

    MRO growth has become a strategic focus area. Engine scarcity crises are reshaping aftermarket economics, with new capacity expansions emerging in Middle East and Asia hubs to address turnaround time pressures.

    Core Building Blocks of Aerospace Manufacturing Operations

    The aerospace manufacturing process follows an end-to-end value chain:

    • Concept design in PLM systems managing configurations and BOMs
    • Industrialization creating build books and route cards
    • Sourcing with approved vendor lists tracking heat lots and batches
    • Production via shopfloor execution with travelers and digital work instructions
    • Final assembly and test incorporating NDT signoffs and torque verifications
    • Certification via AS9102 FAIs and AS9145/APQP processes
    • Delivery and ongoing aftermarket MRO

    The main operational domains include:

    Domain

    Key Activities

    Artifacts

    Engineering and Industrialization

    ECO management, configuration control

    Build books, route cards

    Shopfloor Execution

    WIP tracking, operation sequencing

    Travelers, work instructions

    Quality and Compliance

    CAPA workflows, audit trails

    FAIRs, nonconformance records

    Supply Chain Management

    Supplier OTD, PPM monitoring

    Approved vendor lists, POs

    MRO Operations

    Dynamic routing, findings management

    Task cards, SB/AD compliance logs

    The typical system landscape features ERP for finance and inventory, PLM for design revisions, MES for machine scheduling and OEE, and QMS for nonconformance and audits. Gaps persist in operator guidance, rich routing logic, and cross-system unification. A digital operations layer like Connect981 emerges as the connective tissue, aggregating data without replacing core systems.

    Operational Visibility for Aerospace Leaders

    COOs and plant managers need real-time visibility across programs, sites, and suppliers to monitor WIP status, bottlenecks, quality escapes, and MRO turnaround times. Current visibility gaps typically manifest as weekly slide decks, manual status spreadsheets, email updates from suppliers, and poor cross-site comparability.

    Modern operational visibility means unified dashboards pulling from ERP, MES, QMS, and execution systems into a single pane of glass. Role-based views allow plant managers to see site performance while program leaders track cross-factory progress.

    KPIs aerospace executives should see at a glance:

    • OTD by program targeting 95%+ for tier-1 suppliers
    • First-pass yield typically 85-95% in precision machining
    • Rework rate ideally under 5%
    • Hours per unit by operation
    • TAT by MRO routing with 30-60 day targets for engine shops
    • AS9100 and FAA audit findings trends
    • Supplier delivery and quality performance metrics

    Connect981 acts as that visibility layer by aggregating work order execution data, digital work instructions status, and supplier workflow milestones into live reports. Site comparison views allow leaders to identify which facilities execute similar operations faster and why.

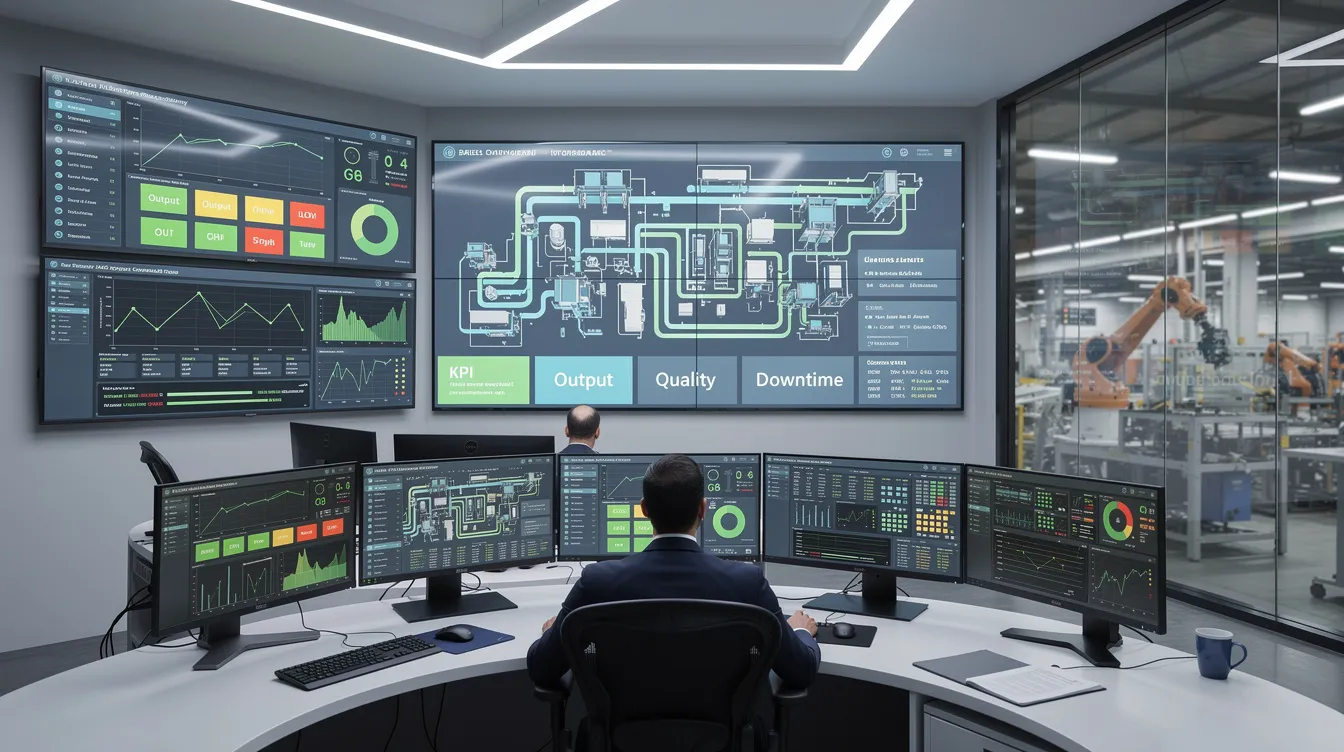
    The image depicts a modern manufacturing control room featuring multiple digital dashboards that showcase real-time production data essential for optimizing aerospace manufacturing processes. This high-tech environment highlights the integration of advanced manufacturing technologies to enhance operational efficiency and ensure compliance with safety and performance standards.

    Scaling Aerospace Programs Without Losing Control

    Ramping a new aircraft, engine, or subsystem program from prototype to LRIP and then to full-rate production presents specific challenges between 2025 and 2030. Commercial aerospace sector OEM ambitions frequently outpace supply chain capacity, while defense industry rapid capability deployment demands accelerated timelines.

    Pain points during scale-up include:

    • Configuration proliferation from engineering change orders
    • Late-breaking engineering changes disrupting production schedules
    • Incomplete build documentation causing rework
    • Inconsistent processes across plants and suppliers amid backlogs

    Standardized digital work packages address these challenges. Routing, work instructions, inspection plans, torque charts, and test steps can synchronize multiple lines via template-based workflows and controlled revision releases. Automated alerts flag when work starts on superseded revisions.

    Scalable operations require governance around AS9100, AS9102 FAI, AS9145/APQP, and NADCAP processes built into daily execution rather than living only in manuals. Complex geometries requiring hybrid additive-traditional manufacturing methods demand consistent documentation across facilities.

    A digital execution layer like Connect981 supports consistent rollouts across multiple factories and suppliers without forcing a full MES overhaul. Templates propagate instantly, and revision control ensures every site works from current documentation.

    Workforce Productivity and the Aerospace Skills Gap

    The aerospace sector faces a skills challenge with high retirement rates among experienced mechanics and machinists combined with difficulty attracting younger talent into complex, regulated environments. Over 60% of aerospace manufacturers cite workforce issues as a primary constraint, with UK manufacturers reshoring over 50% of production to mitigate risks.

    Typical productivity drains include:

    • Searching for the correct revision of work instructions
    • Walking to paper binders for reference documents
    • Re-entering data from travelers into systems
    • Manual article inspection documentation for FAIRs

    Digital work instructions with embedded photos, 3D models, torque charts, and checklists shorten onboarding time by 30-50% and reduce dependency on tribal knowledge. A technician drilling composite panels or assembling wiring harnesses can follow visual guidance rather than interpreting text-heavy procedures.

    AI assistance in platforms like Connect981 guides technicians through root cause analysis, suggests likely causes of recurring defects, and flags missing quality steps. Before digitization, paper-based operations typically take 20-30% longer per unit than digitized flows that capture timestamps and parameters automatically.

    An aerospace technician is focused on a tablet device while working on an aircraft component, highlighting the integration of digital tools in the aerospace manufacturing process. This scene emphasizes the importance of technology in optimizing production processes and ensuring quality control in the aerospace industry.

    Digital Execution Layers vs. Traditional MES and ERP

    Understanding the difference between core transaction systems, heavy MES layers, and modern lightweight digital execution platforms clarifies where gaps exist.

    ERPs handle orders, finance, and inventory well but fall short on operator guidance, in-process quality checks, and detailed traceability at the operation level. Traditional MES manages machine scheduling, OEE, and automation interfaces but gaps appear in documentation control, rich routing logic, supplier collaboration, and MRO workflows.

    A digital operations layer sits above and between ERP, MES, PLM, and QMS. It coordinates work instructions, checklists, approvals, and contextual data for each task without requiring system replacement.

    Concrete integration patterns include:

    • Pulling work order and BOM data from SAP or Oracle
    • Associating production tasks with CAD/PLM revisions
    • Pushing completion data and nonconformance records back into ERP/QMS
    • Faster ECN propagation across connected systems

    Executives do not need to rip-and-replace existing systems to achieve modern execution capabilities. Connect981 extends the existing landscape rather than competing with established infrastructure investments.

    Quality, Traceability, and Compliance by Design

    Aerospace and MRO operations require designing in quality and traceability from day one to satisfy safety and performance standards under AS9100, AS9102, NADCAP, ITAR, FAA, EASA, and OEM customer certification requirements.

    Concrete practices include:

    • Serial and batch number traceability throughout production processes
    • Heat lot control for specialty alloys and key components
    • Digital FAIRs replacing paper-based first article inspection
    • CAPA workflows with immutable audit trails
    • Sign-off records for every process change and rework event

    Digital work instructions embed mandatory quality checkpoints that must be completed before advancing operations. Torque verification, NDT signoff, and visual inspections gate progression automatically rather than relying on technician memory.

    The value during audits becomes clear: instant access to routing, parameters, technicians, calibrated tools, and rework history for any serial number. Regulatory bodies and OEM quality representatives can verify compliance without manual document retrieval.

    Connect981 captures these elements automatically as technicians execute work, reducing reliance on manual forms and scanned PDFs. Quality escapes drop 20-40% in certified environments using embedded checkpoint enforcement.

    Connected Factory: Integrating ERP, MES, PLM, QMS, and Supplier Systems

    The typical aerospace IT landscape in 2025 includes multiple ERPs across regions, legacy MES installations, PLM for design, standalone QMS, and supplier portals. These systems remain only partially integrated.

    Data silos create issues:

    • Mismatched revisions between PLM and shopfloor instructions
    • Delayed quality feedback to engineering teams
    • Limited supplier visibility into engineering or routing changes
    • Configuration drift between production sites

    A unified operations layer reads and writes to these complex systems, ensuring technicians, engineers, and supplier partners all see the same current configuration. Technology integration patterns include API-based connections for modern systems and file-based exchanges where legacy infrastructure requires it.

    Role-based data sharing respects international traffic in arms regulations and export controls while enabling necessary collaboration. Connect981 bridges OEM and tier-1 systems with tier-2 and tier-3 suppliers, enabling shared workflows for build packages, FAIR approvals, and deviation management.

    Business outcomes include fewer build holds, faster engineering change implementation, and reduced rework from revision mismatches.

    Managing Complex Aerospace Supply Chains

    Aerospace supply chains remain fragile due to long lead times for titanium and specialty alloys spanning 12 to 24 months, semiconductor constraints, complex electronics, and thousands of tier-2 and tier-3 suppliers per program. Supply chain resilience has become a board-level priority.

    Geopolitical events, export controls under ITAR and EAR, and evolving cybersecurity requirements under CMMC add layers of operational risk. The defense systems segment faces particularly stringent requirements affecting prime contractors and their supplier networks.

    Operational impacts include:

    • Line-stopping shortages requiring production schedule changes
    • Out-of-sequence work creating downstream complications
    • Expedited freight costs eroding margins
    • Last-minute engineering deviations to accommodate substitute parts

    Digital supply chain coordination addresses these challenges through shared build packages, real-time PO and routing visibility, and supplier progress updates integrated directly into factory execution views. Aerospace customers gain transparency into supplier status without manual status calls.

    Connect981 supports supplier collaboration by giving external partners controlled access to relevant work instructions, quality requirements, and documentation checklists. Coordinating FAIRs, managing approved vendor lists, and monitoring supplier on-time delivery and PPM become streamlined activities rather than administrative burdens.

    Aerospace MRO Operations and Turnaround Time Optimization

    Aerospace MRO differs fundamentally from new production through variable work scopes, discovery-driven routing, and heavy dependence on historic maintenance records. Predictive maintenance strategies intersect with traditional scheduled overhaul requirements.

    Key MRO metrics include:

    Metric

    Target

    Impact

    Turnaround time (TAT)

    30-60 days for engine shops

    Customer satisfaction, lease costs

    On-time release

    95%+

    Contract compliance

    Findings-per-visit

    Trending analysis

    Process optimization

    Rework rate

    Under 5%

    Cost control

    Repeat visits within 18-24 months

    Minimized

    Quality verification

    Digital routing and task cards adapt dynamically during disassembly and inspection, updating work content as findings are logged. An engine module strip reveals conditions that modify the repair scope in real time rather than requiring separate paper processes.

    Integrated parts traceability and maintenance history improve decisions on repair versus replace and help prove compliance to regulatory requirements and lessors. Connect981 unifies MRO planning, routing execution, parts kitting, quality checks, and customer approvals in one view, reducing TAT by 15-25% and eliminating paperwork cycles.

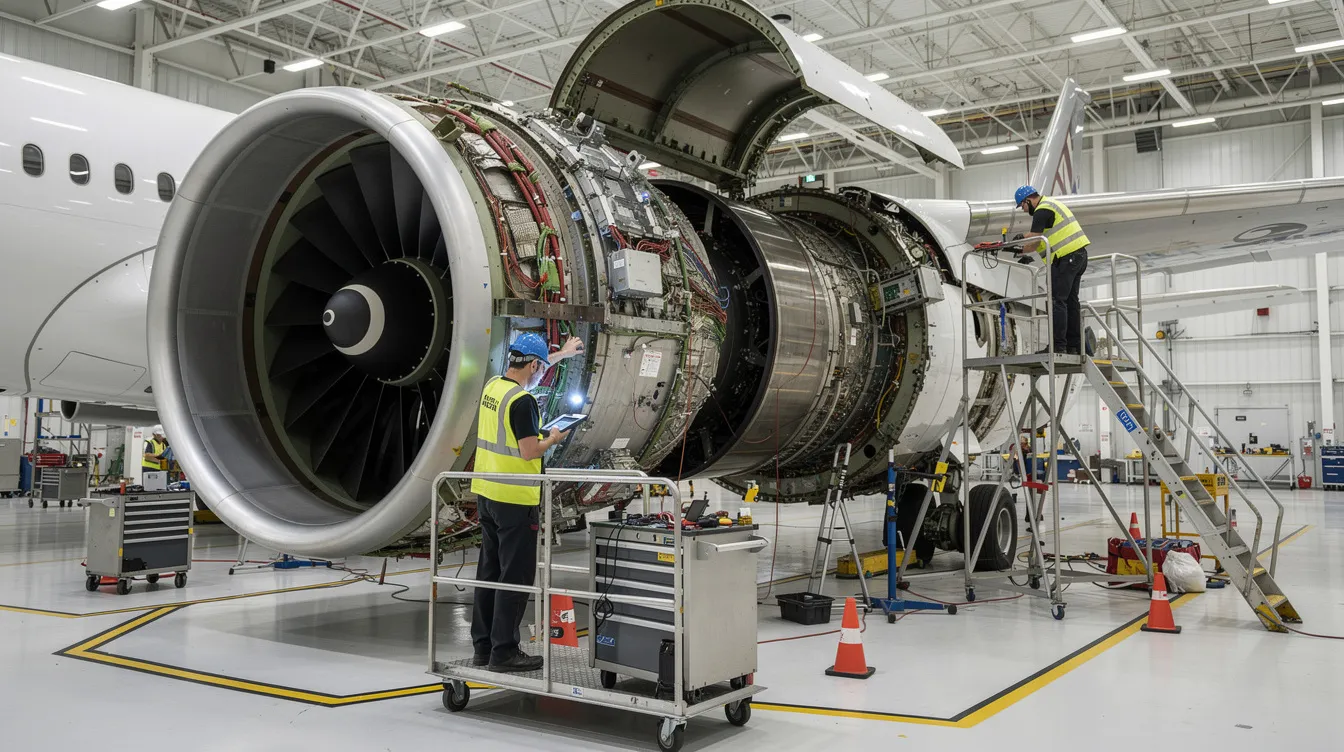
    The image depicts an aircraft engine being meticulously inspected during maintenance at a modern MRO facility, highlighting the critical aerospace manufacturing processes that ensure safety and performance standards in the aerospace industry. Skilled technicians are seen utilizing advanced manufacturing technologies and quality control measures to optimize production processes and maintain the reliability of aerospace components.

    Leveraging AI and Analytics in Aerospace Manufacturing Operations

    Realistic AI and data analytics use cases achievable on the factory floor before 2028 focus on operational improvement rather than speculative autonomous systems. Machine learning applications must meet aerospace constraints around certification requirements and model validation expectations.

    Specific opportunities include:

    • Predictive quality flagging likely nonconforming operations before completion
    • Anomaly detection in process control data
    • Intelligent routing suggestions based on historical performance
    • AI-assisted root cause analysis for CAPA workflows
    • Real time feedback on process deviations

    Operational data collected in Connect981 including timestamps, user actions, defect types, and process parameters feeds these models to deliver program-specific insights. Advanced analytics reveal patterns invisible in manual review.

    Constraints unique to aerospace demand explainable AI for regulators and internal quality authorities. Aerospace companies must govern AI adoption through phased pilots on selected lines or MRO cells, human-in-the-loop decision making, and clear boundaries between advisory and automated actions.

    Examples include reducing scrap on composite layup by 10-20% or improving FAI pass rates on complex machined specialized components through pattern recognition.

    Implementation Roadmap: From Paper and Spreadsheets to a Connected Operations Layer

    A pragmatic 12 to 24 month transformation roadmap for aerospace plants reliant on paper travelers, spreadsheets, and shared drives follows a phased approach to optimize production processes.

    Months 1-6: Foundation

    • Select one value stream or MRO cell for initial digitization
    • Digitize work instructions and quality checklists for repetitive tasks
    • Establish baseline metrics for comparison
    • Train core team on platform capabilities

    Months 6-12: Expansion

    • Expand to quality workflows and parts traceability
    • Connect supplier collaboration for selected programs
    • Integrate with ERP for work order data synchronization
    • Measure first-pass yield improvements and reduce waste

    Months 12-24: Enterprise Scale

    • Roll out across additional production lines and sites
    • Standardize workflows based on lessons learned
    • Enable cross-site visibility and benchmarking
    • Extend to MRO operations and additional supplier tiers

    Cross-functional governance requires operations, manufacturing engineering, quality, IT, and supply chain jointly defining standard workflows and data structures. Aviation management leadership must champion adoption.

    Connect981’s zero and low-code platform shortens deployment using aerospace-specific templates for FAI, inspection, routing, and concessions. Early wins like reducing missing paperwork by 50% or shortening signoff cycles build organizational momentum and support continuous improvement.

    How Connect981 Supports Modern Aerospace Manufacturing Operations

    Connect981 serves as a unified aerospace operations platform connecting ERP, MES, PLM, QMS, and supplier systems into one digital execution layer. The platform addresses aerospace and defense industry requirements rather than generic industrial manufacturing needs.

    Core capabilities mapped to operational priorities:

    • Digital work instructions with embedded media and version control
    • Shopfloor execution tracking with real-time WIP visibility
    • Serial and lot traceability throughout production cycles
    • Integrated quality workflows with checkpoint enforcement
    • Supplier collaboration with controlled access and shared documentation
    • MRO routing management with dynamic task adaptation

    Scenario examples:

    • Ramping a new program across multiple sites with consistent work packages and synchronized documentation releases
    • Stabilizing a critical supplier through shared FAI workflows and deviation management
    • Reducing TAT in an engine MRO shop by 20% through unified planning and execution views

    Connect981 differentiates from general MES and low-code platforms through aerospace-first data models, templates for AS9100 and FAA workflows, and fast time-to-value without requiring system replacement. Digital tools deploy in weeks rather than months.

    Conclusion: Next Steps for Aerospace Operations Leaders

    Modern aerospace manufacturing operations require integrated visibility, scalable processes, empowered workforces, and a digital execution layer bridging legacy systems. The aerospace projects demanding attention in 2026 cannot wait for multi-year transformation programs.

    Executive priorities for the next 18 to 24 months:

    1. Unify operational data across ERP, MES, and shopfloor systems
    2. Digitize work instructions and quality flows to reduce cost and development cycles
    3. Standardize processes across sites using template-based workflows
    4. Connect suppliers and MRO operations into shared visibility frameworks

    Leaders can assess current maturity by inventorying paper-based workflows, counting manual spreadsheets used for production control, and reviewing audit findings related to documentation and traceability. The biggest challenges often hide in plain sight.

    A pilot with Connect981 on a targeted program or MRO cell provides a low-risk path to validate benefits and balance innovation with operational continuity. Strategic partnerships between operations leadership and digital platforms enable aerospace companies to stay competitive. Educational institutions and leadership programs increasingly emphasize digital manufacturing competencies for future workforce development.

    The next 18 to 24 months will separate organizations that digitize execution from those still managing paper trails. Operational efficiency gains compound across programs when the foundation is right. Request a Demo to see how Connect981 extends your existing ERP and MES landscape to meet aerospace production demands and ensure safety across other industries and beyond.

  • Implementing MES in Aerospace with a Waste-Reduction First Mindset

    Implementing MES in Aerospace with a Waste-Reduction First Mindset

    Implementing MES in Aerospace with a Waste-Reduction First Mindset

    In aerospace manufacturing, scrap and rework are not just quality issues—they are financial events. Every scrapped titanium forging or long-cycle composite part erodes margin, consumes scarce capacity, and jeopardizes delivery commitments. Yet most waste doesn’t come from dramatic failures. It comes from small process deviations that go unnoticed until final inspection.

    Manufacturing Execution Systems (MES) can change that equation, but only if they are implemented with a clear focus on waste reduction from day one. This article explains how to plan and execute an aerospace MES implementation that targets scrap, rework, and material waste as its primary outcomes, while respecting regulatory, validation, and compliance requirements.

    For teams putting this topic into daily operation, Connect 981’s aerospace execution solutions help connect the concept to traceability, work-order reality, and audit-ready evidence.

    For teams putting this topic into daily operation, scrap and rework reduction, shop floor execution control help connect the concept to traceability, work-order reality, and audit-ready evidence.

    The same operating model also depends on quality management workflows, a connected execution platform, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

    We will walk through how to define the business case, assess current waste, design MES use cases, plan a phased rollout, manage change with operators and engineers, and measure impact in a way that wins continued support.

    Why Tie MES Implementation to Waste Reduction Goals

    Many MES programs start as broad “digital transformation” initiatives and struggle to demonstrate tangible value quickly. Anchoring MES implementation to clear, quantifiable waste-reduction goals keeps the effort focused and fundable.

    Creating a clear business case and ROI story

    To justify MES investment in an aerospace environment, the business case should be specific about where value will come from and how it will be measured. Instead of generic benefits like “more visibility,” highlight concrete targets such as:

    • Reducing scrap rate on critical components by a defined percentage range
    • Lowering rework hours per unit on key product families
    • Cutting excess material consumption versus planned usage
    • Reducing disruptions to schedule caused by late-found defects

    Scrap in aerospace often involves high-value alloys, complex assemblies, or long lead-time components. Connecting MES use cases directly to reduced scrap and rework on these items creates a compelling Return on Investment (ROI) narrative. Rather than promising a specific payback period, describe a range and the factors that influence it, such as product mix, baseline process stability, and regulatory constraints on process changes.

    Aligning plant, quality, and finance priorities

    Waste reduction touches multiple stakeholders, and MES success depends on aligning their priorities:

    • Operations/Plant leadership cares about throughput, schedule adherence, and labor efficiency.
    • Quality and regulatory focus on conformance, traceability, and compliance with aerospace standards and customer requirements.
    • Finance tracks margin, cost of poor quality, and performance on long-term or fixed-price contracts.

    When presenting the MES program, frame waste reduction in terms that matter to each group:

    • For operations: fewer disruptive quality holds, smoother flow, less rework blocking bottleneck resources.
    • For quality: earlier detection of process drift, better evidence for root cause analysis, improved audit readiness.
    • For finance: lower scrap write-offs, improved cost predictability, better protection of margins on fixed-price programs.

    This alignment helps prevent MES from being seen as a “IT tool” and positions it as a shared capability for controlling waste and risk.

    Focusing on high-impact scrap and rework issues

    Not all waste is equal. In aerospace, some scrap events are so costly or schedule-critical that even small improvements matter. To ensure MES is focused on the most impactful problems:

    • Identify parts and assemblies with high material cost, long cycle times, or stringent rework limitations.
    • Review historical data to find frequent non-conformances, recurring deviations, and costly rework loops.
    • Engage cross-functional teams to select a handful of priority issues where MES can provide earlier detection, better execution control, or improved traceability.

    These high-impact issues become the backbone of your initial MES use-case roadmap and help ensure early phases of implementation demonstrate visible, measurable value.

    Assessing Current Scrap, Rework, and Material Waste

    Before defining MES requirements, you need an honest baseline of how much waste exists today, where it occurs, and how well it is currently measured.

    Gathering baseline data from existing systems

    Most aerospace manufacturers already have some level of data in ERP, QMS, PLM, and perhaps legacy shop-floor systems. To build a baseline:

    • Pull historical scrap and rework records by part number, work center, and defect type.
    • Review non-conformance reports (NCRs) and corrective action reports (CARs) for recurring issues and systemic causes.
    • Analyze material variance reports: actual vs. planned consumption, particularly for expensive materials and consumables.
    • Document the typical detection point for defects—in-process checks, final inspection, or even post-delivery.

    The goal is not perfection but a pragmatic understanding of where waste happens today and how visible it is in current systems.

    Identifying data gaps MES can fill

    As you review existing data, you will likely uncover gaps, such as:

    • Limited or inconsistent linking between process parameters and resulting defects.
    • Inadequate visibility into which operations most often introduce errors.
    • Fragmented or manual records of rework steps, making it hard to quantify true cost.
    • Poor tracking of partial scrappage (e.g., only part of an assembly is scrapped).

    These gaps inform the MES data model and configuration. For example, you might prioritize:

    • Capturing key process parameters at critical operations.
    • Standardizing reason codes for scrap and rework.
    • Linking material lot information and genealogy to each work order.

    By being explicit about today’s blind spots, you can design MES to make waste visible and traceable, rather than simply replicating current limitations in a new system.

    Prioritizing critical parts and processes

    Not every operation needs the same level of MES control from day one. To prioritize:

    • Rank parts or assemblies by scrap cost and rework frequency.
    • Identify special processes (e.g., heat treatment, welding, bonding, coating) that have tight validation and high risk.
    • Flag operations where rework is limited or prohibited by design or regulatory requirements.

    These priorities help you select where to implement detailed MES tracking, real-time monitoring, and strict standard work enforcement first. They also guide which cells or lines are the best candidates for your initial MES pilot.

    Defining MES Use Cases Around Waste Reduction

    With a baseline established, the next step is to translate waste-reduction goals into specific MES use cases. Each use case should clearly articulate who uses it, what data is captured, and how it prevents or reduces scrap, rework, or material waste.

    Real-time monitoring and holds

    One of the most powerful ways MES reduces waste is by detecting problems earlier than traditional sampling-based quality checks. Effective use cases include:

    • Parameter monitoring: Capture critical process parameters (temperature, torque, pressure, time-in-process) in real time and compare them to approved limits.
    • Automated alerts: Notify operators, supervisors, or quality when parameters deviate or when inspection results trend toward limits.
    • Automatic holds: Place affected work orders or serial numbers on hold when a serious deviation is detected, preventing further value-add until disposition.

    By intervening early, MES can stop defects before they multiply. Instead of discovering issues at final inspection—when multiple parts may already be affected—you can initiate corrective actions while only a small number of parts are at risk.

    Standard work enforcement and error-proofing

    Rework often stems from missed steps, incorrect settings, or inconsistent execution. MES can enforce standard work to reduce this variability:

    • Operation checklists that must be completed in sequence before moving to the next step.
    • Verification of tooling, fixtures, and programs (e.g., CNC program version, calibrated tool ID) before work starts.
    • In-process signoffs by operators and inspectors with clear accountability.
    • Embedded work instructions with visuals, parameters, and notes tailored to the specific configuration or revision.

    These capabilities do not replace training or certification, but they make it harder for common errors to slip through, especially when dealing with complex routings or multiple product variants on the same line.

    Material tracking and yield analytics

    Material waste in aerospace is often hidden. Offcuts, over-issues, and non-visible losses rarely show up in headline metrics. MES can help you understand and control this waste through:

    • Lot and serial tracking for high-value materials, linking each lot to specific work orders and operations.
    • Actual vs. planned material usage at the operation or work-order level, not just net at the end of the job.
    • Yield reporting that shows how much input material results in conforming output across operations.

    With better data, engineering and operations can refine nesting strategies, cutting patterns, and process parameters. Over time, this moves decisions from rough assumptions to evidence-based optimization.

    Phased MES Rollout Strategy for Aerospace Plants

    Given aerospace regulatory and validation requirements, a “big bang” MES rollout is risky. A phased approach allows you to learn, adjust, and demonstrate value while maintaining control.

    Starting with a pilot line or product family

    Choose a pilot that is meaningful but manageable. Good candidates include:

    • A product family with significant scrap or rework issues.
    • A cell with relatively stable staffing and leadership support.
    • A value stream where both engineering and quality are engaged and available.

    In the pilot, focus on a limited set of high-impact MES use cases rather than attempting full functionality at once. For example, prioritize real-time monitoring at one special process, standardized work instructions for a critical assembly, and basic material tracking for expensive materials.

    Balancing speed with validation and compliance needs

    Aerospace environments must comply with customer, regulatory, and internal standards (for example, regarding software validation, configuration management, and data integrity). When planning your pilot:

    • Define which MES functions require formal validation before use in production.
    • Document configurations, workflows, and change controls from the start.
    • Use a test environment for training, configuration testing, and scenario validation before migrating to production.

    It is important not to underestimate the effort here. Validation and documentation add time, but they also build trust with quality and regulatory teams, which in turn helps smooth the path for broader adoption.

    Scaling to additional cells, plants, and suppliers

    Once the pilot demonstrates measurable waste reduction and stable operations, build a scale-out plan:

    • Standardize core templates for routes, work instructions, and data collection that can be reused across cells.
    • Capture lessons learned on change management, training, and configuration so future rollouts go faster.
    • Consider extending MES capabilities to key suppliers or integrating supplier data where appropriate to gain better visibility into upstream waste drivers.

    As you scale, maintain a clear priority on waste-reduction use cases so new deployments continue to deliver recognizable, quantifiable improvements.

    Change Management and Operator Adoption

    Even the best-designed MES will fail to reduce waste if people see it as extra work or surveillance rather than a tool that helps them succeed. Effective change management is essential.

    Communicating the purpose and benefits

    Frontline operators, inspectors, and technicians are closest to the process and will use MES every day. To gain their support:

    • Explain that the goal is preventing problems earlier, not blaming individuals for defects discovered late.
    • Highlight how MES can reduce rework loops, urgent expedites, and last-minute firefighting.
    • Show that better data will support more realistic process capability assessments and help justify needed investments in tooling, training, or equipment.

    Include operators and inspectors in design workshops and pilot reviews. Their insights often reveal practical ways to capture the right data with minimal disruption.

    Designing intuitive UIs and workflows

    To encourage adoption:

    • Keep screens simple and focused on the current task, avoiding unnecessary fields.
    • Use terminology and sequences that match how the work is actually performed on the floor.
    • Minimize manual entry where possible, using barcodes, RFID, or machine integration.
    • Provide clear visual indicators when something is out of tolerance or requires action.

    A small number of well-designed screens that accurately reflect real work will be more effective than a complex UI that attempts to handle every scenario from day one.

    Using early wins to build momentum

    After the pilot goes live, actively look for early signs that MES is helping reduce scrap, rework, or material waste. Examples include:

    • A parameter alert catches tool wear before it causes a run of non-conforming parts.
    • Standardized work instructions reduce rework on a complex assembly step.
    • Better material tracking reveals and corrects a recurring over-issue practice.

    Share these stories widely, backed by data. Recognize teams and individuals who contributed. Early success stories build credibility and help others see MES as a practical tool for improvement rather than a corporate mandate.

    Measuring and Communicating Impact

    To sustain support and funding, you must translate MES-enabled waste reductions into meaningful metrics and narratives for multiple audiences.

    Tracking scrap, rework, and material usage trends

    Define a small set of core metrics before go-live and measure them consistently over time. Typical examples include:

    • Scrap rate by part family, work center, and defect type.
    • Rework hours per unit or per month, by operation.
    • Material yield for key materials, comparing input mass or area to conforming output.
    • Time to detect critical defects (from introduction to detection).

    MES should make these metrics easier and faster to produce by providing consistent, structured data from the shop floor.

    Translating improvements into financial terms

    To communicate with executives and finance, connect operational improvements to financial impact. Examples include:

    • Annualized reduction in scrap write-offs for specific part families.
    • Reduced rework labor hours, expressed as capacity freed for value-add work.
    • Improved predictability of material usage, supporting more accurate costing and quoting.

    Be clear about assumptions and influencing factors. Instead of claiming a guaranteed payback period, present reasoned estimates and sensitivity to variables like volume, product mix, and future process changes.

    Sharing results with executives and customers

    Use dashboards, periodic reports, and simple before/after comparisons to show how MES contributes to performance. For customers and auditors, MES can demonstrate:

    • Enhanced traceability and control of special processes.
    • Systematic, data-driven approaches to reducing defects.
    • Evidence that corrective actions are effective and sustained.

    These capabilities can strengthen your position in bids, customer audits, and long-term partnership discussions, especially on programs where waste directly affects fixed-price margins.

    Sustaining Waste Reduction as a Continuous Improvement Program

    MES implementation is not a one-time project. To keep scrap, rework, and material waste trending down, you need an ongoing governance and improvement framework.

    Establishing governance and ownership

    Clarify who owns which aspects of MES and waste reduction:

    • Business process owners (operations, quality, engineering) define rules, workflows, and priorities.
    • IT or digital teams maintain the platform, integrations, and technical configuration.
    • Continuous improvement or Lean/Six Sigma teams use MES data to identify and close performance gaps.

    Set up a cross-functional steering group that regularly reviews MES performance, waste trends, and proposed changes.

    Regularly reviewing MES rules and configurations

    As processes change and new products are introduced, static MES configurations can become outdated. To prevent this:

    • Schedule periodic reviews of key alerts, holds, and data collection points.
    • Use MES data to refine control limits, inspection frequencies, and standard work steps.
    • Retire or simplify features that are not adding value or are causing unnecessary complexity.

    This ongoing tuning helps ensure MES continues to support waste reduction rather than becoming a rigid constraint.

    Integrating with Lean, Six Sigma, and quality programs

    MES and traditional improvement methodologies are complementary. MES provides the real-time, granular data that Lean and Six Sigma teams need to identify variation, validate improvements, and sustain gains. To integrate effectively:

    • Use MES data to populate value-stream maps, capability analyses, and control charts.
    • Build standard problem-solving workflows that reference MES data for root cause analysis.
    • Incorporate MES training into broader continuous improvement education for leaders and frontline staff.

    By treating MES as a core enabler of waste reduction as continuous improvement with MES in aerospace, you turn it from an IT project into a long-term competitive advantage.

    Conclusion

    Implementing MES in aerospace with a waste-reduction first mindset means starting from the real problems: costly scrap, limited rework options, hidden material losses, and schedule risk. By building a targeted business case, prioritizing high-impact use cases, rolling out in phases, and investing in change management, you can turn MES into a practical tool for preventing defects and protecting margins.

    With clear ownership and ongoing integration into continuous improvement programs, MES becomes a sustained capability for controlling waste in an environment where every gram of material and every minute of capacity matters.

  • Leveraging MES Traceability to Reduce Waste and Support Aerospace Compliance

    Leveraging MES Traceability to Reduce Waste and Support Aerospace Compliance

    Leveraging MES Traceability to Reduce Waste and Support Aerospace Compliance

    In aerospace manufacturing, scrap is not just a quality metric. It is a financial and contractual event. Losing a single high-value machined forging or composite structure can ripple through schedules, margins, and customer commitments. Robust traceability in a Manufacturing Execution System (MES) is one of the most effective ways to contain that impact when problems do occur.

    This article explains how aerospace MES traceability structures data so that, when defects are discovered, you can precisely identify affected parts, lots, and operations. That precision allows you to avoid over-scrapping, limit re-inspection, and respond to regulators and customers with confidence.

    For a broader discussion of waste reduction practices, see MES-supported waste reduction and traceability in aerospace.

    Regulatory and Customer Expectations for Aerospace Traceability

    Aerospace OEMs and regulatory bodies expect manufacturers to demonstrate where every critical part came from, how it was processed, and whether it met requirements at each key step. MES is a primary tool for capturing and organizing this information, but expectations vary by part criticality and contractual context.

    Typical traceability requirements by part criticality

    Traceability depth is closely tied to the risk posed by a part or assembly:

    • Flight-critical and safety-critical parts typically require full serial-level genealogy. You must be able to trace every individual item from incoming material, through each operation, to final assembly and test.
    • Mission-critical or performance-critical parts may require serial or small-lot traceability, including key process parameters and inspection results, but with some aggregation where risk is lower.
    • Standard or non-critical parts are often managed at lot or batch level, with enough traceability to support quality management and basic containment without excessive burden.

    OEM flow-downs, airworthiness authority guidance, and internal engineering risk assessments typically define which level applies. An MES should be configurable enough to reflect those distinctions without forcing a single model on all parts.

    Differences between lot, batch, and serial tracking

    The way you structure traceability strongly influences your exposure when a defect appears:

    • Lot tracking associates groups of items with a common identifier (e.g., a barstock heat lot or fastener lot). If a defect is traced to a lot, you may have to contain or scrap everything produced from that lot, across time and work orders.
    • Batch tracking is similar, but often tied to a manufacturing event (e.g., a batch of parts heat-treated together). A defect in the batch process generally drives containment of all batch members.
    • Serial tracking assigns a unique identity to each specific part or assembly. If a problem is linked to a particular process or material exposure, you can typically narrow the impact to just the serials that passed through that exact condition.

    An aerospace MES needs to manage all three simultaneously. The finer the traceability granularity, the more precisely you can limit the scope of scrap and rework, though this comes at a cost of data volume and operational discipline.

    Implications for scrap and rework decisions

    When a nonconformance is discovered—whether through inspection, in-service feedback, or supplier notification—the traceability model determines your options:

    • With coarse traceability (e.g., only lot-level), you may be forced to treat an entire lot as suspect, even if only a fraction of parts actually experienced the adverse condition.
    • With robust serial-level genealogy, you can identify exactly which part serials saw which tool, fixture, program version, operator, or material batch at the time of deviation.

    The result is a more defensible decision about what to scrap, what to re-inspect, and what can continue to ship, reducing both direct waste and schedule disruption.

    How MES Structures Traceability Data

    To achieve useful traceability, an aerospace MES must connect multiple dimensions of manufacturing data into a coherent genealogy: materials, processes, inspections, tooling, and people.

    Linking materials, processes, and inspections

    A mature traceability model in MES constructs a chain of evidence that ties together:

    • Incoming material: supplier lot, heat number, certificates of conformity, receiving inspections, and release status.
    • Process execution: which operation was run, on which machine or cell, using which work instructions and parameters at the time.
    • In-process and final inspections: measured values, pass/fail results, sampling plans, and any nonconformance reports raised.

    Each produced unit or lot carries these links throughout its lifecycle. When an anomaly emerges, engineers can quickly traverse this data from any direction: from part back to process, from process to tooling, or from material lot forward to all affected assemblies.

    As-built records and operation history

    An as-built record is essentially the factual history of how a given unit was manufactured, as opposed to how it was planned. In aerospace MES, this typically includes:

    • All operations actually executed, including deviations from the routing.
    • Start/finish timestamps and elapsed time per step.
    • Configuration identifiers (program revision, work instruction version, NC file version).
    • Key process parameters as recorded (temperatures, pressures, torque values, cure cycles, etc.).
    • Inspection points, measurements, and dispositions.

    This operation history turns investigations from guesswork into data-driven analysis. It is also crucial evidence for regulators and OEMs if a field issue triggers a broader fleet review.

    Tooling, program, and operator associations

    Many systemic defects are not about the part itself, but the conditions under which it was made. Effective aerospace MES traceability therefore links each produced item to:

    • Tools and fixtures: serial numbers, calibration status, and maintenance records.
    • NC programs and work instructions: which revision was used, and whether any temporary instructions or concessions were active.
    • Operators and inspectors: who performed which step, and what qualifications or certifications they held at the time.

    When a programming error, tool wear, or training gap is discovered, you can immediately map that condition to the exact set of affected parts or batches, rather than applying broad assumptions.

    Using Traceability to Contain Defects Efficiently

    Even in highly controlled environments, nonconformances will occur. The key is to prevent them from propagating into large quantities of scrap or widespread rework. MES-based traceability is a core enabler of fast, precise containment.

    Quickly bounding affected populations

    When an issue is flagged—by a failed inspection, supplier alert, or monitoring alarm—engineers need to answer two questions quickly: What exactly went wrong? and Which units were exposed?

    With a well-designed MES genealogy model, you can:

    • Query all parts produced on a specific machine, with a particular tool or program revision, during a defined time window.
    • Identify all assemblies containing material from a suspect lot or batch, across multiple levels of the bill of material.
    • Trace forward from a suspect subassembly to finished units already in stock, in shipment, or at the customer.

    This allows you to set precise holds and shipping stops, rather than blanket freezes that paralyze production.

    Avoiding unnecessary scrap and re-inspection

    When data is incomplete, organizations often err on the side of caution by scrapping broadly or re-inspecting large populations of parts. This is costly and, in many cases, avoidable.

    Robust aerospace MES traceability reduces this waste by providing evidence that:

    • Only parts processed within a defined timeframe or parameter window were at risk.
    • Specific serials did not pass through the suspect condition and can be safely released.
    • Previously executed inspections already verified the relevant characteristics, eliminating the need to repeat them.

    The combination of genealogy and recorded measurements supports risk-based decisions that stand up to internal and external scrutiny.

    Coordinating with customers on disposition

    When potential escapes or in-service findings occur, OEMs and regulators expect clear, data-backed responses. MES traceability enables you to:

    • Provide trace reports showing how many units are affected, where they are, and what their exact as-built configuration is.
    • Support engineering disposition (use-as-is, repair, or scrap) with detailed parameter histories and inspection evidence.
    • Collaborate on risk assessments by simulating worst-case combinations of variables based on actual production data.

    This often leads to more targeted repair or rework actions, rather than defaulting to scrapping complete batches or assemblies.

    Reducing Rework Risk with Better Genealogy

    Rework may appear to save scrap but can introduce new defects, consume capacity, and complicate traceability if not tightly controlled. A strong genealogy model reduces both the need for rework and the risk it introduces.

    Ensuring correct rework paths are followed

    When a nonconformance is found, MES can enforce approved rework routings and capture all steps taken. Proper genealogy ensures that:

    • Only parts with specific nonconformance codes are eligible for certain rework paths.
    • Rework steps are linked to engineering-authorized instructions and concessions.
    • Additional inspections or tests required after rework are completed before release.

    This prevents ad-hoc fixes that might resolve the immediate defect but violate design intent or introduce hidden risks.

    Tracking multiple rework cycles and concessions

    Some aerospace parts may legitimately go through multiple repair or rework cycles, especially on long-life assets. Without clear genealogy, it becomes difficult to understand the cumulative impact of concessions and deviations.

    An aerospace MES should record:

    • Each rework cycle as a distinct but linked set of operations.
    • All concessions, waivers, or deviations applied, with references to approvals.
    • Resulting configurations, especially if they differ from the nominal design.

    This history supports future maintenance decisions, fleet management, and life-limited part analysis, while also protecting against unapproved work that could invalidate airworthiness assumptions.

    Avoiding double-handling and undocumented fixes

    Undocumented touch labor is a hidden source of waste and risk. It consumes time, may invalidate prior inspections, and can break the traceability chain.

    By tightly integrating rework processes into MES:

    • All work, including unplanned fixes, must be logged against the part or lot.
    • Operators receive clear instructions on whether to rework, scrap, or route parts to MRB (Material Review Board).
    • Supervisors can see the total rework burden and target process improvements at the root cause.

    This reduces double-handling and ensures that every action performed on a part is captured in its genealogy.

    Traceability-Driven Continuous Improvement

    Traceability is not only about compliance and containment. When used effectively, MES genealogy becomes a continuous improvement engine that exposes systemic waste drivers and validates corrective actions.

    Identifying systemic issues across programs

    Aggregated genealogy data helps you spot patterns that individual nonconformance reports may not reveal, such as:

    • Higher defect rates associated with specific machines, tools, or shifts.
    • Increased rework on parts produced from certain material lots or suppliers.
    • Recurring issues tied to specific process windows (e.g., temperature, humidity, or cure times).

    By analyzing these patterns, quality and manufacturing engineers can prioritize improvement projects that deliver the greatest reduction in scrap and rework.

    Feeding genealogy insights into design and process changes

    When MES is integrated with engineering systems, genealogy data can inform both product and process design:

    • Feedback on which features or tolerances drive most defects can trigger design simplification or tolerance relaxation (subject to regulatory and performance constraints).
    • Evidence of robust performance under certain process ranges can be used to widen allowable windows, reducing false alarms and unnecessary rework.
    • Changes in tooling, fixtures, or methods can be evaluated by comparing before/after defect rates at a granular level.

    This closes the loop between production reality and engineering assumptions, making waste reduction an ongoing capability rather than a one-time initiative.

    Audit trails that support lessons learned

    Aerospace organizations are frequently audited by customers, regulators, and internal compliance teams. MES traceability provides an objective audit trail that:

    • Documents exactly how a process was run at a given point in time.
    • Shows how nonconformances were detected, contained, and corrected.
    • Records changes and their approvals, supporting robust configuration control.

    These audit trails not only reinforce compliance but also serve as a knowledge base for future programs, helping new projects avoid repeating past causes of scrap and rework.

    Designing a Traceability Model in MES

    Achieving the right level of traceability requires deliberate design. Overly coarse models drive excessive waste; overly detailed models can be costly to maintain and slow operations. The goal is a risk-based balance.

    Deciding what to track at serial vs lot level

    Key considerations when deciding traceability granularity include:

    • Risk and criticality: Flight-critical and safety-critical parts typically demand serial-level tracking, whereas standard hardware may be adequately managed at lot level.
    • Defect detection opportunities: If issues are likely to be caught at or near the point of origin, coarser traceability may be acceptable. If detection tends to occur late (e.g., final test, in service), finer granularity can dramatically reduce exposure.
    • Volume and handling: High-volume, low-risk parts may become impractical to track individually. In these cases, a hybrid approach (e.g., serial tracking only after a certain assembly stage) can be effective.

    The chosen model should be formally risk-assessed and aligned with engineering, quality, and customer requirements.

    Balancing detail with practicality and performance

    More data is not always better. Aerospace MES implementations must balance:

    • Data capture burden: Manual data entry slows operators and increases the risk of errors. Use automation (e.g., barcode/RFID scans, equipment integration) wherever feasible.
    • System performance: Excessive granularity can create large datasets that are hard to query quickly during investigations. Data architecture and indexing must support fast genealogy queries.
    • Human factors: Traceability processes should fit naturally into the workflow. If they are seen as overhead, workarounds and data gaps are likely to emerge.

    Continuous feedback from production teams helps refine the model over time, ensuring it stays both effective and usable.

    Integrating MES with PLM, ERP, and QMS

    Traceability does not live in MES alone. Its effectiveness depends on connections to surrounding systems:

    • PLM (Product Lifecycle Management) provides the authoritative design intent, bills of material, and approved processes that MES must execute and track against.
    • ERP (Enterprise Resource Planning) manages material purchasing, inventory, and financials; linking MES genealogy to ERP lots and orders closes the loop from cost to cause.
    • QMS (Quality Management System) handles nonconformance records, corrective actions, and audits; integrating MES data enriches investigations and supports more effective corrective actions.

    These integrations ensure that traceability is not an isolated data silo, but a shared resource for engineering, operations, quality, and supply chain teams.

    Case Examples: Limiting Scrap via Precise Traceability

    To illustrate how aerospace MES traceability limits waste, consider several typical scenarios. Details will vary by organization and program, and specific configurations must be tailored to applicable requirements.

    Narrowing a suspected material defect to a small batch

    A material supplier notifies your organization of a potential anomaly in a specific heat lot of alloy used for machined brackets. Without robust traceability, you might have to treat all brackets of that type as suspect.

    With MES genealogy in place, you can instead:

    • Identify exactly which internal lots and serials used that heat.
    • Trace forward to all assemblies containing those brackets.
    • Apply targeted holds and inspections to only the affected units.

    This can reduce the number of impacted parts from thousands to a much smaller, well-defined population, saving material and avoiding unnecessary line disruptions.

    Isolating parts exposed to out-of-spec process conditions

    Suppose a heat treatment furnace is later found to have operated slightly out of specification for a period of time. The question becomes: which parts were actually in the furnace during that window?

    An MES with detailed equipment and time-based genealogy can:

    • List all loads processed in that furnace while it was out of spec.
    • Identify every part serial or batch included in those loads.
    • Trace those parts into higher-level assemblies and current locations.

    Instead of scrapping every part ever processed in that furnace, you focus on a time-bounded subset. In many cases, additional testing or engineering analysis may clear some of these parts for use, based on the exact conditions experienced.

    Providing evidence for customer waivers or repairs

    In some situations, an OEM or regulator may consider a waiver, concession, or defined repair in lieu of scrapping suspect hardware. The decision depends heavily on confidence in the underlying data.

    MES traceability supports these discussions by:

    • Demonstrating that only certain features, loads, or parameters deviated, with all other conditions meeting requirements.
    • Providing detailed histories that support engineering analyses of structural or performance impact.
    • Documenting any rework or repair performed, tying it to approved instructions and validated results.

    This evidence can convert potential scrap into accepted, safe hardware, while maintaining trust with customers and oversight bodies.

    Making Traceability a Strategic Waste-Reduction Lever

    Traceability is often pursued first as a compliance obligation in aerospace, but its value goes far beyond regulatory checklists. With a well-designed genealogy model in MES, manufacturers can:

    • Respond faster and more precisely to defects and supplier alerts.
    • Limit the scope of scrap, rework, and re-inspection when issues arise.
    • Feed rich operational data into continuous improvement and design decisions.

    Requirements differ by program, customer, and jurisdiction, so no single MES configuration can guarantee compliance in all contexts. However, investing in thoughtful traceability design—and integrating it with broader MES-supported waste reduction and traceability in aerospace practices—consistently pays dividends in reduced waste, stronger margins, and more resilient customer relationships.

  • Protecting Margins on Fixed-Price Aerospace Contracts with MES

    Protecting Margins on Fixed-Price Aerospace Contracts with MES

    Protecting Margins on Fixed-Price Aerospace Contracts with MES

    In aerospace manufacturing, scrap is not just a quality problem. It is a financial event. Under fixed-price and long-term contracts, every lost part, extra hour of rework, and unplanned material withdrawal directly erodes program margin. A well-implemented Manufacturing Execution System (MES) gives aerospace manufacturers the visibility and control needed to keep waste from silently eating into profitability.

    This article explains how MES-driven scrap, rework, and material waste reduction supports margin protection in fixed-price aerospace contracts. It also shows how plant-floor data can feed program-level financial decisions, improve risk management, and strengthen contract negotiations.

    For a broader view of waste reduction strategies, see how MES supports reducing scrap, rework, and material waste in aerospace manufacturing as a foundation for margin protection.

    Why Waste is So Dangerous in Fixed-Price Aerospace Programs

    Fixed-price and long-duration aerospace contracts lock in revenue while leaving most cost risk with the supplier. That structure amplifies the impact of scrap, rework, and material waste.

    Limited Ability to Pass Costs to Customers

    In many aerospace programs, contracts are structured as firm fixed-price, fixed-price with incentive, or long-term pricing agreements. Once the price per unit or per block of deliveries is agreed, your room to recover unplanned costs is limited.

    • Unplanned scrap of high-value materials (e.g., nickel alloys, titanium, composites) must usually be absorbed internally.
    • Extra rework hours consume capacity and increase overtime without a corresponding price increase.
    • Expedited materials and logistics to protect delivery dates often hit your P&L, not the customer’s.

    Without detailed, timely waste data, these costs accumulate gradually and only become visible when program margins are already compromised.

    Tight Margins and Long Production Horizons

    Aerospace programs often run for years or even decades, with cost curves expected to improve over time. In this environment:

    • Initial learning curve assumptions are built into bid models.
    • Planned rate increases depend on predictable cycle times and yields.
    • Suppliers commit to price reductions or productivity targets over the life of the contract.

    If scrap and rework rates stay higher than planned—even by a few percentage points—the impact on lifetime program margin can be substantial. MES helps teams detect when real-world waste performance diverges from the cost model early enough to intervene.

    Forecasting Challenges for Emerging Programs

    On new or ramping programs, forecasts are inherently uncertain. Engineering changes, immature processes, and supplier variability all introduce risk. Traditional quality systems that rely on sampling and end-of-line checks often miss small process deviations until multiple parts are affected.

    MES addresses this by:

    • Capturing real-time process data (machine parameters, operator inputs, environmental conditions).
    • Flagging out-of-tolerance trends before they produce large batches of non-conforming parts.
    • Enforcing standardized work instructions so new processes are executed consistently.

    The result is a faster feedback loop between the shop floor and program finance teams, reducing the gap between estimated and actual costs.

    Linking MES Waste Data to Program Financials

    To protect margins, waste metrics must be connected directly to program and contract financials. MES is the system of record for what actually happened during manufacturing; when integrated properly with ERP and program controls, it becomes a powerful financial lens.

    Attributing Scrap and Rework Costs to Specific Contracts

    Under fixed-price arrangements, the critical question is not just how much scrap or rework occurred, but which contract or customer it affected. MES enables this by:

    • Tracking every unit and lot by work order, contract number, and customer.
    • Recording scrap events with coded reasons (e.g., process deviation, supplier defect, programming error).
    • Logging rework operations, including additional labor, machine time, and consumables.

    When MES data is linked to cost rates from ERP, you can calculate:

    • Scrap cost per contract, part number, and configuration.
    • Rework labor and overhead by program.
    • Trends in waste by customer or major assembly group.

    This enables more accurate program margin analysis and targeted corrective actions.

    Understanding Cost per Good Piece by Configuration

    Aerospace products often have multiple configurations, options, or block points. The real cost per good piece can vary significantly depending on:

    • Configuration-specific processing sequences.
    • Different inspection requirements or special processes.
    • Distinct yield profiles for early versus mature designs.

    MES provides the necessary granularity by:

    • Tying each operation and inspection to a specific configuration or effectivity.
    • Capturing actual cycle times, scrap, and rework at the operation level.
    • Supporting traceability across serial numbers and lots.

    When combined with cost data, this gives program managers a clear view of cost per good piece by configuration, helping them understand where margin is being gained or lost.

    Supporting Earned Value and Program Reporting

    Many aerospace programs use Earned Value Management (EVM) or similar frameworks. MES can feed more accurate actuals into these models by providing:

    • Real-time actual hours consumed versus planned.
    • Visibility into rework hours that might not be obvious in high-level reports.
    • Accurate counts of accepted units versus scrapped or reworked quantities.

    With this data, cost performance index (CPI) and schedule performance index (SPI) reflect true execution performance rather than optimistic assumptions. Program teams can course-correct earlier and defend their forecasts with objective evidence.

    Reducing Cost Volatility with MES-Controlled Processes

    Margin protection on fixed-price contracts is not only about lowering average cost; it is about reducing cost volatility. MES-controlled processes make outcomes more predictable.

    Stabilizing Scrap and Rework Rates Over Time

    Most waste does not come from dramatic failures. It comes from small process deviations—a worn tool, a drifting fixture, a subtle setup mistake—that accumulate over time. MES helps stabilize performance by:

    • Monitoring key process parameters continuously instead of relying on periodic checks.
    • Issuing immediate alerts when parameters exceed tolerance.
    • Automatically placing holds on affected work orders to prevent further nonconforming production.

    By catching issues early, MES reduces the number of parts involved in each incident, smoothing waste rates and avoiding spikes that can wipe out a period’s margin.

    Reducing Schedule Risk from Unexpected Rework

    Rework can sometimes save expensive hardware, but it also:

    • Consumes finite capacity on critical machines and skilled labor.
    • Introduces additional risk of further nonconformances.
    • Threatens on-time delivery when discovered late in the process.

    MES mitigates these risks by:

    • Enforcing correct execution the first time with validated data entry and digital work instructions.
    • Routing nonconforming parts through controlled disposition and rework workflows.
    • Providing visibility into rework queues and cycle times for scheduling and capacity planning.

    Reduced surprise rework directly supports schedule adherence and avoids the expensive expediting often required to protect customer commitments.

    Improving Confidence in Rate Readiness

    As aerospace programs ramp from development to rate production, customers scrutinize suppliers’ ability to meet volume and quality targets. MES strengthens your case by providing:

    • Historical trends on scrap and rework rates by process and part family.
    • Evidence of process stability under increasing load.
    • Data-supported projections of first-pass yield at higher rates.

    This gives both your internal leadership and your customers greater confidence that quoted rates and costs are achievable, reducing the risk of margin-damaging surprises during ramp-up.

    Using MES Insights in Contract Negotiations and Change Management

    While MES cannot change the basic commercial structure of a fixed-price contract, it can materially improve your negotiating position and change management outcomes by supplying objective, detailed data. This data does not guarantee customer acceptance, but it provides a credible foundation for discussions.

    Providing Data-Backed Justification for Pricing and Surcharges

    When new proposals or re-pricing events arise, MES helps build more accurate cost models by:

    • Supplying actual cycle times by operation and configuration.
    • Quantifying scrap and rework rates for similar parts or processes.
    • Highlighting special process steps or inspections that drive cost.

    This allows commercial teams to justify pricing with concrete operational evidence rather than historical averages alone. In some cases, MES data may support discussions about surcharges or price adjustments when customer-driven changes clearly increase cost.

    Demonstrating Process Capability to Customers

    Aerospace OEMs and Tier 1s increasingly expect suppliers to demonstrate capability, not just quote a price. MES can support this by providing:

    • Capability summaries (e.g., yield, defect rates, process stability) for key operations.
    • Evidence of closed-loop corrective actions and sustained improvements.
    • Traceable histories showing how the plant responded to prior disruptions.

    These insights can improve your position in competitive bids and support conversations about risk-sharing and scheduling flexibility.

    Managing the Impact of Design and Scope Changes

    Design changes, new customer requirements, and scope expansions are facts of life in aerospace programs. MES helps quantify their impact by:

    • Simulating revised routing and operation sequences.
    • Estimating incremental cycle time and inspection effort based on similar past changes.
    • Tracking post-change scrap and rework trends to validate cost assumptions.

    This supports structured change management, helping both sides understand how new requirements affect cost and schedule. While MES data alone does not guarantee contractual relief, it makes your case more transparent and defensible.

    Metrics for Executives: From Plant Data to Program Health

    Executives need a concise set of metrics that connect MES data to program performance. The goal is to translate detailed shop-floor information into indicators that signal margin risk early.

    Scrap Cost as a Percentage of Contract Value

    One powerful metric is scrap cost as a percentage of contract or program value. To compute it, combine MES scrap quantities with material and processing costs from finance, and compare the result to total revenue on the contract.

    This view helps executives:

    • Identify programs where waste is reaching materiality thresholds.
    • Prioritize improvement projects where margin is most at risk.
    • Track the return on MES and process improvement investments.

    Rework Hours vs Planned Labor

    Another key indicator is the ratio of rework hours to planned production labor. MES can distinguish between planned operations and rework steps, allowing for:

    • Visibility into how much capacity is absorbed by non-value-added recovery work.
    • Comparison of actual rework effort to what was assumed in bids or budgets.
    • Trend analysis to see whether corrective actions are sustainable.

    High or rising rework ratios are early warning signs that program margins may be under pressure even if shipments and revenue appear on track.

    On-Time Delivery Performance Under Waste Control

    Fixed-price contracts often include delivery penalties or incentives. Waste and rework can quietly jeopardize on-time performance. MES supports more reliable delivery by:

    • Flagging potential schedule slips when scrap or rework events affect critical path components.
    • Providing accurate work-in-progress (WIP) status and queue times.
    • Helping planners and program managers re-sequence work to protect contractual dates.

    Tracking on-time delivery alongside waste metrics lets executives see whether improvements in scrap and rework are translating into reliable customer performance and preserved margin.

    Implementing MES for Financial Visibility

    To realize the margin-protection potential of MES, implementation must be designed with financial and contractual outcomes in mind—not just manufacturing efficiency.

    Aligning Finance, Operations, and IT Requirements

    Successful MES programs in aerospace bring together finance, operations, and IT to define:

    • Which waste categories matter most for margin (scrap, rework, consumables, overtime triggers).
    • How contracts and programs will be identified within MES and related systems.
    • What reporting granularity is required for program reviews and customer discussions.

    This alignment ensures that MES data structures support both operational control and program-level financial analysis from day one.

    Ensuring Accurate Cost Allocation in MES and ERP

    MES captures what happened; ERP and finance determine how costs are allocated. To link them effectively:

    • Use common keys and identifiers (work orders, WBS elements, contract numbers) across systems.
    • Define clear rules for how scrap and rework costs flow to programs and cost centers.
    • Regularly reconcile MES quantities with inventory and financial records.

    The tighter the integration, the more reliably you can translate execution data into meaningful financial insight without manual workarounds.

    Phasing Deployment by Highest-Risk Programs

    Not every program needs the same level of MES sophistication immediately. A pragmatic approach is to:

    • Identify high-value or low-margin contracts where waste poses the greatest financial risk.
    • Prioritize complex parts and special processes with historically higher scrap and rework.
    • Roll out MES capabilities in phases, starting with traceability, scrap capture, and rework control, then extending to advanced analytics.

    This sequencing accelerates financial impact and builds internal support using results from the most exposed programs.

    Communicating Value to Internal and External Stakeholders

    MES only protects margins if people understand and use the information it provides. Communicating value clearly is essential for sustaining investment and adoption.

    Framing MES Investments as Margin Protection

    Internally, MES is often viewed as an operations or IT project. To gain executive sponsorship, frame it as a margin protection initiative for fixed-price programs:

    • Quantify current scrap and rework cost exposures using available data.
    • Estimate potential savings from even modest yield improvements.
    • Highlight the role of MES in supporting accurate bids and avoiding surprises after contract award.

    This shifts the conversation from system features to financial outcomes.

    Reporting Improvements to OEMs and Regulators

    Aerospace customers and regulators care deeply about process control and traceability. MES can strengthen your external position by enabling:

    • Structured reports on defect reduction and process capability.
    • Transparent documentation of corrective and preventive actions.
    • Evidence of consistent compliance with approved processes.

    While this may not directly change pricing, it builds trust, supports supplier ratings, and can influence future sourcing decisions.

    Using Success Stories to Scale Across Programs

    Once MES has delivered measurable benefits on one or two programs, capture those results and use them to build momentum:

    • Document before-and-after metrics for scrap, rework, on-time delivery, and margin where possible.
    • Share case studies internally to show how data-driven decisions improved outcomes.
    • Incorporate lessons learned into standard deployment templates for new areas.

    Over time, this creates a culture where MES is viewed as an essential tool for managing the financial health of fixed-price aerospace contracts, not just a manufacturing system.

    By tightly linking MES waste data to program financials, aerospace manufacturers can move from reacting to margin erosion to proactively managing it—protecting profitability while delivering reliable performance to their customers.

  • Faster Decision-Making in Aerospace Manufacturing Through MES Data Integration

    Faster Decision-Making in Aerospace Manufacturing Through MES Data Integration

    Aerospace manufacturing decisions often stall for one simple reason. The data needed to make them lives in too many places.

    Supervisors chase status updates. Planners reconcile reports. Quality teams wait for confirmation. By the time clarity arrives, the window to act has already closed.

    Why decision-making slows down in complex operations

    Traditional manufacturing environments rely on disconnected systems and delayed reporting. Production data arrives after the fact. Quality metrics lag behind execution. Resource availability is inferred rather than confirmed.

    Common decision delays include:

    • Waiting for manual status updates
    • Reconciling conflicting reports
    • Chasing missing information across teams
    • Making decisions based on yesterday’s data

    In aerospace, those delays translate directly into missed delivery commitments and reactive firefighting.

    How MES creates a single operational view

    Manufacturing Execution Systems integrate execution data at the point of work. Production status, quality holds, material availability, and equipment usage are captured in real time.

    Instead of assembling information manually, decision-makers access a unified, current view of operations.

    From reporting to situational awareness

    MES dashboards are not historical reports. They provide live situational awareness.

    This includes:

    • Which jobs are at risk right now
    • Where bottlenecks are forming
    • Which resources are constrained
    • What actions will have the greatest impact

    Decisions move from reactive to proactive.

    Responding to change without disruption

    Customer change requests, late material deliveries, and equipment issues are inevitable. MES allows teams to respond quickly because the consequences of each option are visible immediately.

    Schedules can be adjusted, priorities rebalanced, and customers informed before problems escalate.

    Decision speed as a competitive advantage

    In high-compliance industries, speed must coexist with control. MES delivers both by grounding decisions in verified execution data.

    Organizations that decide faster without sacrificing accuracy consistently outperform those still managing by spreadsheets and status meetings.

  • Using MES Analytics to Reduce Material Usage Variance in Aerospace

    Using MES Analytics to Reduce Material Usage Variance in Aerospace

    Using MES Analytics to Reduce Material Usage Variance in Aerospace

    In aerospace manufacturing, material waste is never just a scrap problem—it is a financial event. High-cost alloys, forgings, and composite materials turn into immediate margin erosion when usage drifts beyond plan. Yet most of this waste does not come from dramatic failures. It comes from small, repeated variances that traditional systems struggle to see.

    Manufacturing Execution Systems (MES) can close this visibility gap. By capturing actual material consumption, scrap, and yield at each operation, MES enables detailed analytics on material usage variance. The result is practical insight into where waste is occurring, why it is happening, and which actions will deliver the greatest financial impact.

    This article explains how aerospace manufacturers can use MES analytics to track material usage variance, refine cost models, and support continuous improvement—without replacing existing ERP financial controls. For a broader view of scrap and rework, see our guide on material waste and cost visibility with MES in aerospace.

    The Financial Impact of Material Waste in Aerospace

    Aerospace programs are uniquely sensitive to material waste. Parts are often made from expensive, specialty materials and produced in low volumes with long cycle times. That combination makes even modest usage variance highly consequential.

    High-cost alloys, forgings, and composites

    Aerospace structures and engine components rely on titanium, nickel-based superalloys, advanced aluminum, and sophisticated composite systems. These materials are expensive to purchase, difficult to process, and sometimes subject to long lead times and strict qualification requirements.

    Material usage variance in this context has a disproportionate cost impact:

    • High raw material cost per part means that a few percentage points of over-consumption can outweigh labor savings.
    • Buy-to-fly ratios for complex machined parts are already high; unplanned waste further reduces effective yield.
    • Special process coupons and test samples add legitimate consumption, but lack of visibility can make them look like unexplained variance.

    Effect on fixed-price and long-term contracts

    Many aerospace manufacturers operate under fixed-price contracts, long-term agreements (LTAs), or rate-based pricing. When material costs rise during the life of a program, recovering those costs can be difficult or impossible.

    Material usage variance directly affects:

    • Program margin, especially on mature programs where price is stable but costs are still drifting.
    • Make-or-buy decisions, where inaccurate internal usage data can distort comparisons to supplier pricing.
    • Negotiations for future blocks or lots, where historical variance should be understood and either eliminated or built into pricing.

    Without clear visibility to actual usage, finance and program management are left to explain unfavorable variances based on averages and assumptions rather than data.

    Why ERP alone can’t see true usage variance

    ERP systems are essential for planning, purchasing, and financial control. However, they are typically not designed to capture detailed, operation-level material usage:

    • Backflush at completion only: Many ERPs backflush material when an operation or order is completed, not when material is actually consumed.
    • Limited scrap categorization: ERP may record scrap quantities and value, but rarely captures enough context (operation, cause, shift) for root-cause analysis.
    • Coarse granularity: ERP tends to operate at the work-order or item level, not the individual serial number, lot, or operation-step level that aerospace traceability demands.

    Because of these limitations, ERP is excellent for valuing material but less effective at explaining where and why additional consumption occurs. MES fills this gap by capturing execution data as work happens.

    How MES Captures Actual Material Consumption

    MES connects people, machines, and materials at the point of execution. That makes it the ideal system to track real material usage and feed analytics on variance.

    Issuing and backflushing material to operations

    In a MES-enabled aerospace environment, material is typically associated with work as it moves through the routing:

    • Material issue at operation start: Operators scan barcodes or RFID tags to issue kits, panels, forgings, or raw stock to a specific operation.
    • Backflushing on consumption: For repetitive or predictable usage, MES can backflush material based on actual production quantities at that step, rather than only at order completion.
    • Partial usage: The system can record partial consumption of a panel, bar, or sheet and track the remaining remnant for reuse.

    This approach links specific material lots and quantities to operations and work centers, enabling much finer-grained variance analysis.

    Tracking scrap and yield at each step

    MES records what happens to material as parts move through the process:

    • Scrap events logged with reason codes (e.g., machining oversize, layup defect, cure failure).
    • Rework and repair recorded with additional material usage where allowed by engineering.
    • Yield calculation at each operation, not just at final inspection.

    The combination of issued material, good output, rework, and scrap enables MES to calculate actual yield by operation and by part, highlighting where material is being lost.

    Serial, lot, and heat-level traceability

    Aerospace programs often require traceability down to heat, lot, or individual serial numbers. MES supports this by:

    • Associating each part serial with the specific material lots and heats used in its manufacture.
    • Tracking consumables and process materials (e.g., adhesives, prepregs, fasteners) where they materially affect cost or quality.
    • Linking inspection results and process parameters to both part and material identifiers.

    This level of traceability not only supports regulatory and customer requirements, it also provides the dataset needed to analyze material usage variance across programs, lots, and suppliers.

    Reporting Actual vs Planned Usage by Part and Operation

    Once MES is reliably capturing material consumption and scrap, the next step is to compare it to the planned picture in your BOMs and routings.

    Comparing to standard routings and BOMs

    The core of material usage variance analysis is a comparison between:

    • Planned usage: Quantities defined in ERP or PLM bills of material, including scrap factors and allowances.
    • Actual usage: Quantities consumed and scrapped as recorded by MES at each operation.

    To enable this comparison, MES and ERP must share common item numbers, units of measure, and revision identifiers. With that alignment in place, MES analytics can produce reports such as:

    • Planned vs. actual material per part number and revision.
    • Variance per operation (e.g., rough machining vs. final machining vs. assembly).
    • Usage variance for specific materials across multiple part numbers.

    Identifying chronic over-consumption

    Not all variance is random. MES analytics can reveal chronic patterns of over-consumption, for example:

    • Certain work centers consistently consuming more composite material per panel.
    • Specific fixtures or tools associated with higher trim or machining scrap.
    • Programs where legacy allowances significantly underestimate actual material needs.

    By filtering data over weeks or months, you can distinguish between isolated incidents and systemic issues that warrant engineering or process changes.

    Understanding process-driven vs random variation

    MES data helps separate process-driven variance from genuine randomness by correlating usage with:

    • Operation and work center: Is variance localized to a step or spread across the route?
    • Shift and crew: Do certain shifts use more material due to experience levels or local workarounds?
    • Material batch or supplier: Does material source affect trim requirements, yield, or defect rates?

    Clarify the operational risk

    When the work behind Using MES Analytics to Reduce affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in Using MES Analytics to Reduce

    Patterns in this data indicate whether you should focus on process controls, training, supplier management, or BOM assumptions.

    Analyzing Scrap Drivers with MES Data

    Material usage variance often originates in scrap and rework. MES provides the depth of data needed to understand these drivers and prioritize corrective actions.

    Correlating scrap with work center, shift, and supplier

    Because MES ties scrap to specific operations, people, and materials, you can build analyses such as:

    • Scrap cost by work center, highlighting the most expensive points of failure.
    • Scrap rate by shift or crew, identifying training or staffing gaps.
    • Scrap by material lot or supplier, exposing quality or stability issues in the supply base.

    These insights go beyond simple scrap percentages, providing a basis for targeted improvement projects and supplier discussions.

    Spotting patterns in rework-driven material loss

    Rework often appears to save parts, but it can quietly increase material consumption through additional cutting, patching, or component replacement. MES can show:

    • How often rework leads to additional material usage (e.g., extra plies, shims, or hardware).
    • Which rework paths have the highest cost per saved part.
    • Operations where rework frequently fails, ultimately resulting in scrap.

    With this view, engineering and operations can determine when it is better to invest in first-pass yield improvements rather than relying on rework.

    Differentiating unavoidable trim from avoidable scrap

    Some material loss is inherent in aerospace manufacturing. Examples include:

    • Trim allowances for composite layups.
    • Starter stock for machining complex shapes.
    • Mandatory test coupons and process validation pieces.

    MES data helps differentiate this unavoidable trim from avoidable scrap by quantifying each type and mapping it to process steps. Over time, you can refine BOM scrap factors to reflect realistic, stable levels of unavoidable loss while targeting the remainder for reduction.

    Using Insights to Improve Processes and Cost Models

    Collecting data is only half the job. The real value of MES analytics is realized when insights drive concrete changes in processes and financial models.

    Refining allowances and scrap factors

    Legacy BOMs often contain conservative scrap factors or outdated assumptions. Using MES data, you can:

    • Update scrap factors by part family and operation based on recent, stable performance.
    • Right-size material allowances (e.g., panel size, bar length, ply count) to better match actual needs.
    • Separate regulatory-mandated scrap (e.g., coupons) from process-driven waste.

    This alignment improves standard costing, quoting accuracy, and program financial forecasts.

    Prioritizing continuous improvement projects

    Not every variance justifies an improvement project. MES analytics support rational prioritization by showing:

    • Scrap cost per operation and per work center.
    • Material usage variance per part number, ranked by annual spend.
    • Trend lines that distinguish worsening performance from stable, predictable variance.

    With this information, engineering and operations teams can focus limited resources on the few processes that drive most of the excess material cost.

    Collaborating with finance and program management

    Material usage variance is as much a financial topic as an engineering one. Effective MES usage supports collaboration by providing:

    • Common reports that tie together engineering scrap causes and financial impact.
    • Scenario analysis for “what if” questions (e.g., what happens to program margin if we improve yield by 2% at a specific operation?).
    • Evidence for price negotiations when unavoidable material costs differ significantly from original assumptions.

    Importantly, MES should be positioned as complementary to ERP—providing the operational detail needed to understand and influence the financial results that ERP records.

    Practical Dashboard and KPI Examples

    To turn MES data into action, aerospace manufacturers typically deploy focused dashboards and KPIs around material usage and scrap.

    Material yield by part family

    A useful starting view is material yield by part family or product line. A dashboard might show:

    • Planned vs. actual material per completed unit.
    • Yield trends by month or production lot.
    • Highlighting of families with the largest negative variance.

    This keeps attention on groups of parts where improvements will have significant aggregate impact.

    Scrap cost by process step

    Another powerful view is scrap cost by process step, not just by scrap quantity. This should include:

    • Material cost of scrapped parts and assemblies.
    • Additional material consumed in rework operations.
    • Drill-down capabilities from total cost to specific part numbers and work centers.

    By ranking process steps by scrap cost, organizations can quickly identify “hot spots” worth investigation.

    Top offenders by work center or program

    MES dashboards aimed at leaders often include “top offenders” lists, such as:

    • Work centers with the highest material usage variance this quarter.
    • Programs where actual usage significantly exceeds quoted assumptions.
    • Part numbers responsible for most of the variance in a given work cell.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for Using MES Analytics to Reduce

    These views promote accountability and support structured problem-solving, rather than relying on anecdotes or isolated incidents.

    Governance and Data Quality Considerations

    The value of MES analytics depends on data quality. Governance practices are essential to ensure the numbers can be trusted and used for decisions.

    Ensuring operators record scrap accurately

    Operator engagement is critical. To achieve reliable data without slowing production:

    • Design simple, quick scrap entry screens with clear reason codes.
    • Use mandatory fields only where they drive tangible value (e.g., operation, reason, quantity, disposition).
    • Provide feedback loops by sharing reports that show how the data is used to improve processes, not just monitor performance.

    Training should emphasize that accurate reporting protects programs and jobs by preventing unpleasant financial surprises later.

    Aligning MES and ERP material definitions

    For variance analytics to make sense, MES and ERP must speak the same language. Key alignment points include:

    • Item numbers and revisions used consistently in both systems.
    • Units of measure (e.g., kg vs. lb, sheet vs. m2) aligned or converted transparently.
    • Material groups and cost buckets mapped so MES reports can roll up to financial categories.

    Data integration should be designed so that planners and engineers do not need to maintain parallel structures in multiple systems.

    Handling rework, re-melt, and recovery flows

    Aerospace manufacturing often includes specialized material flows such as rework, re-melt, and recovery of scrap material. MES configurations should clarify:

    • When rework consumes additional material versus simply adding labor.
    • How recovered material (e.g., re-melted ingots, reclaimed test pieces) is credited back into inventory and reflected in variance calculations.
    • Which scrap streams are truly lost and should be fully burdened with material cost.

    Clear rules ensure that variance reporting fairly represents both waste and legitimate recovery activities.

    Bringing It All Together

    Reducing material usage variance in aerospace is a continuous effort, not a one-time project. MES analytics provide the factual foundation for that effort by:

    • Capturing actual material usage, scrap, and yield at each operation.
    • Comparing real performance to planned BOMs and routings.
    • Highlighting where waste is concentrated and where process improvements will protect margins.

    When combined with disciplined governance and close collaboration between operations, engineering, and finance, MES becomes a powerful enabler of margin protection and competitive pricing in demanding aerospace programs.

    To see how material variance fits into the broader picture of scrap and rework reduction, explore our hub article on reducing scrap, rework, and material waste in aerospace manufacturing with MES.

    For teams putting this topic into daily operation, work orders and digital travelers, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    This article is for aerospace operations, quality, and compliance teams who need to understand Using MES Analytics to Reduce Material Usage Variance in Aerospace. It explains the practical question this topic answers in a manufacturing execution context.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.

  • Using MES to Enforce Standard Work and Error-Proof Aerospace Operations

    Using MES to Enforce Standard Work and Error-Proof Aerospace Operations

    Using MES to Enforce Standard Work and Error-Proof Aerospace Operations

    In aerospace manufacturing, small deviations from standard work can have outsized consequences. A missed torque check, an out-of-date work instruction, or a skipped in-process inspection can mean scrapped high-value components, expensive rework, and potential escapes to the customer. Manufacturing Execution Systems (MES) give aerospace plants the tools to embed standard work directly into the workflow, so errors are prevented at the point of execution instead of discovered at final inspection.

    This article explains how MES can serve as the digital backbone for standard work in aerospace, how it enables practical error-proofing on the shop floor, and how it directly supports waste reduction, rework prevention, and regulatory compliance.

    Why Standard Work Breaks Down in Aerospace Shops

    Aerospace organizations typically invest heavily in procedures, work instructions, and training. Yet rework, scrap, and nonconformances still occur. The issue is rarely a lack of documented standard work, but rather breakdowns in how that standard work is delivered and followed in real time.

    Paper travelers and outdated instructions

    Many aerospace shops still rely on paper travelers, printed work instructions, and binders at workstations. This creates several problems:

    • Version confusion: Operators may unknowingly work from obsolete prints or instructions when new revisions are released after a traveler is printed.
    • Slow updates: Engineering changes can take days or weeks to propagate to all affected jobs, especially across multiple sites.
    • Limited context: Paper instructions often lack embedded visuals, 3D models, or video that would clarify complex steps.
    • Traceability gaps: Handwritten notes and check marks are hard to interpret later and may not meet customer or regulatory audit expectations.

    These issues increase the risk that an operator will follow an outdated or incomplete version of the standard work, creating variability and potential nonconformance.

    Complex routings and engineering changes

    Aerospace routings are complex. Parts may move through dozens or even hundreds of operations, often with special processes (e.g., heat treatment, NDT, coatings) and outsourced steps. Configuration changes and engineering revisions are frequent, especially on development programs and early production.

    In this environment, breakdowns occur when:

    • Route steps are added, removed, or reordered without clear guidance on when the new route applies.
    • Special-process parameters change (e.g., oven soak times, pressure limits) without synchronized updates to work instructions and data collection forms.
    • Different serial numbers within the same batch require different processing due to design changes or concessions, but the traveler does not clearly differentiate them.

    Without a digital system of record, operators and supervisors must rely on memory, printed emails, or ad-hoc workarounds that deviate from standard work.

    Training gaps and shift-to-shift variation

    Even with strong training programs, aerospace shops face:

    • Turnover and ramp-up: New hires and temporary workers may not internalize procedures quickly.
    • Informal shortcuts: Experienced operators may adopt their own methods over time, drifting away from documented standards.
    • Shift variation: Night and weekend shifts may follow different practices than dayshift if support and supervision differ.

    Training and competency management remain critical, but they are not enough on their own. MES complements training by embedding standard work into the workflow so that the correct steps are visible and enforced at the moment of execution.

    MES as the System of Record for Standard Work

    An MES can act as the single, controlled source of truth for how work should be performed on the shop floor. Instead of relying on static documents, standard work becomes a living, digital model executed through the system.

    Version-controlled electronic work instructions

    In a robust aerospace MES, electronic work instructions (eWIs) are maintained with formal revision control:

    • Each instruction set is tied to a specific part number, operation, and revision.
    • Approvals and release workflows ensure that only validated content reaches the shop.
    • Prior versions are archived for traceability but cannot be used on active jobs.

    On the floor, operators access eWIs from terminals or tablets. They see the correct version automatically, complete with photos, annotated drawings, and step-by-step guidance. When engineering updates an instruction, the MES can route it through review and release, then push it live without reprinting and redistributing paper.

    Linking routings to part numbers and revisions

    Standard work is more than instructions for a single operation; it is also the routing that defines the correct sequence of operations and resources. MES supports this by:

    • Associating routings with specific part numbers, configurations, and effectivity dates.
    • Aligning each operation step with the appropriate eWI, NC program, tooling list, and inspection plan.
    • Managing alternate routings (e.g., for rework, different machine groups, or subcontract operations) under controlled rules.

    This linkage ensures that when a work order is released, it automatically inherits the correct route and work instructions based on the part revision and configuration.

    Ensuring only approved processes are executed

    Because MES knows which instructions, routings, and process parameters are approved, it can actively prevent unapproved work:

    • Blocking the start of an operation if the instruction set is not released.
    • Restricting use of an NC program or recipe that is superseded or not qualified for the part.
    • Highlighting when a critical resource (e.g., calibrated gage, certified operator, qualified machine) is missing or not approved.

    This moves standard work from being a passive reference document to an enforced, system-driven behavior.

    Error-Proofing Techniques Enabled by MES

    Error-proofing in aerospace does not mean eliminating the need for skilled operators or training. Instead, it means designing processes and systems so that common mistakes are harder to make and easier to detect immediately. MES provides several capabilities that directly support error-proofing at the point of execution.

    Mandatory data fields and input validation

    Data collection is central to aerospace compliance and quality. MES can structure this data entry to reduce errors:

    • Required fields: Operators cannot complete an operation without entering mandatory values (e.g., torque, temperature, batch/lot numbers, inspector ID).
    • Range checks: Collected values are automatically checked against allowable limits; out-of-range entries trigger warnings or holds.
    • Format and logic validation: Serial numbers, lot codes, and other identifiers can be validated for correct format and checked against approved lists.
    • Context-based prompts: MES can display guidance when data trends indicate risk (e.g., trending toward upper tolerance), helping operators adjust before defects occur.

    By structuring data entry, MES reduces transcription errors and ensures that critical process parameters conform to standard work.

    Sequence enforcement and sign-offs

    In many aerospace operations, the order of steps is as important as the steps themselves. MES can enforce the correct sequence by:

    • Presenting steps in the required order and preventing skipping ahead.
    • Requiring electronic sign-off (with user credentials and timestamps) at key checkpoints.
    • Requiring dual sign-off or independent inspection for high-criticality steps.

    This helps ensure that operators do not bypass inspections, torque checks, or cleaning operations under time pressure. The system can prevent completion of an operation until all mandatory sign-offs are captured.

    In-line checks and conditional prompts

    Instead of relying solely on end-of-operation verification, MES enables in-line checks embedded within the workflow:

    • Prompting for measurements after specific sub-steps, not just at the end of the operation.
    • Triggering additional checks when certain conditions are met (e.g., a batch from a new supplier, a part with known risk features).
    • Integrating machine and test data automatically, reducing the chance of misrecording readings.

    Clarify the operational risk

    When the work behind Using MES to Enforce Standard affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.

    Map the risk in Using MES to Enforce Standard

    These embedded checks help detect deviations early, before additional value is added to the part, reducing both rework and scrap.

    Reducing Rework with First-Time-Right Execution

    Rework is especially costly in aerospace, due to high material value, long cycle times, and strict limitations on repair. MES-driven standard work and error-proofing aim to maximize first-time-right execution.

    Catching missing steps before moving to the next operation

    Traditional quality controls often detect issues only at final inspection or after several operations have been completed. MES changes this by:

    • Preventing the closure of an operation until all required steps, measurements, and sign-offs are complete.
    • Flagging missing or inconsistent data when an operator attempts to move a part forward.
    • Using visual dashboards to show supervisors which operations are blocked and why, enabling quick support.

    By stopping the part at the source of the issue, the plant avoids compounding the mistake across multiple downstream operations.

    Preventing unauthorized rework and deviations

    In time-pressured environments, informal rework or on-the-spot adjustments can creep in. MES helps control this by:

    • Defining approved rework routings and repair limits, including required inspections.
    • Requiring digital approval for deviations and concessions before rework can proceed.
    • Blocking ad-hoc changes to the standard route without proper authorization and documentation.

    This ensures that all rework is traceable, approved, and executed under controlled instructions, protecting both product integrity and compliance obligations.

    Ensuring proper material, tooling, and programs are used

    Many aerospace nonconformances stem from using the wrong material batch, tooling setup, or NC program. An integrated MES can mitigate these risks:

    • Linking each work order to specific material lots and enforcing lot selection rules at issue.
    • Checking that calibrated tools and gages are within date and appropriate for the required tolerance.
    • Verifying that the selected NC program and machine setup match the current part configuration and revision.

    These checks help ensure that operators have the right inputs to execute standard work correctly the first time, reducing both rework and the risk of scrap.

    Supporting Engineering Changes and Configuration Control

    Aerospace programs live under strict configuration control. Changes must be applied precisely to the correct parts, with full traceability. MES plays a central role in keeping standard work aligned with engineering intent as designs evolve.

    Propagating updated instructions to active orders

    When engineering releases a change, MES can:

    • Update routings and eWIs tied to the affected part numbers and revisions.
    • Identify active work orders impacted by the change and determine if they must be reworked, held, or allowed to proceed.
    • Push updated instructions to operators in real time, reducing lag between design decision and shop-floor execution.

    This minimizes the risk that parts are built to a superseded configuration and supports more agile engineering changes without uncontrolled variability.

    Handling grandfathered parts and mixed configurations

    Many aerospace lines run mixed configurations: some units built to the old standard, some to the new. MES can support this complexity by:

    • Associating each serial number with a specific configuration and effectivity date.
    • Automatically presenting the correct routing and instructions based on that configuration, even at the same workstation.
    • Flagging when an operator attempts to apply the wrong configuration or process to a part.

    This level of control is difficult to achieve with paper-based systems and is essential for preventing configuration-related rework and escapes.

    Auditability for customers and regulators

    Aerospace customers and regulators expect clear evidence that standard work was followed and that configuration control was maintained. MES strengthens audit readiness by:

    • Providing electronic records of every operation, sign-off, measurement, and deviation.
    • Linking data to specific parts, serial numbers, and configurations.
    • Enabling rapid retrieval of historical instruction versions and the dates they were in effect.

    These capabilities support certification activities, customer audits, and root-cause investigations while reducing the manual effort of assembling documentation.

    Change Management for Operators and Supervisors

    Digitizing standard work with MES is not just a technology project; it is a change in how people work. Success depends on involving end users and addressing concerns about pace, autonomy, and usability.

    Involving end users in instruction design

    The most effective eWIs are built with operator input:

    • Capturing tribal knowledge and proven best practices from experienced staff.
    • Piloting new instructions with a small group before widespread rollout.
    • Creating feedback loops so operators can suggest improvements based on real-world experience.

    This approach improves accuracy, buy-in, and the usability of digital standard work.

    Training on digital terminals and MES UIs

    Introducing MES often requires new skills:

    • Navigating digital instructions and entering data at terminals.
    • Understanding visual indicators, alerts, and workflows in the user interface.
    • Following electronic sign-off processes instead of paper signatures.

    Connect decisions to execution

    Connect 981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.

    Discuss the workflow for Using MES to Enforce Standard

    Structured training and coaching are essential; MES does not replace the need for formal training and competency management. Instead, it reinforces training by consistently presenting and enforcing the correct steps.

    Addressing concerns about pace and autonomy

    Some operators may worry that MES will slow them down or remove their judgment. Effective change management should:

    • Show how MES can reduce rework, re-inspections, and firefighting, making work more predictable.
    • Clarify where operator discretion is still vital, especially in problem-solving and continuous improvement.
    • Use metrics to demonstrate that, after initial adjustment, digital standard work can support stable or even improved throughput.

    By positioning MES as a support tool rather than a surveillance mechanism, organizations can foster adoption and sustained use.

    Measuring the Impact on Rework and Scrap

    To justify investment and guide continuous improvement, aerospace plants need to quantify how MES-driven standard work and error-proofing impact rework, scrap, and overall waste.

    Tracking rework rates by operation and work center

    MES provides granular visibility into where defects originate:

    • Capturing nonconformance and rework data at the specific operation where issues are found.
    • Aggregating rework rates by part family, work center, shift, and operator group.
    • Highlighting operations with recurring deviations from standard work.

    These insights allow quality and manufacturing engineering teams to prioritize improvements where they will have the greatest impact.

    Comparing defect profiles before and after MES rollout

    To evaluate the effectiveness of MES error-proofing, organizations can:

    • Establish baseline rework, scrap, and defect rates prior to MES deployment.
    • Track trends after digitizing standard work and introducing sequence controls, validations, and in-line checks.
    • Analyze how specific MES features (e.g., mandatory fields, routing enforcement) correlate with reductions in certain defect types.

    This data-driven approach helps tune both the MES configuration and the underlying standard work content.

    Highlighting high-impact standard work improvements

    MES makes it easier to test and validate changes to standard work:

    • Rolling out revised instructions to a pilot cell and monitoring quality and cycle time.
    • Comparing defect types and frequencies before and after instruction changes.
    • Scaling successful patterns across similar parts or lines.

    Over time, this capability supports a continuous-improvement loop that reduces waste and strengthens process capability across the plant.

    Connecting Standard Work to Broader Waste Reduction

    Digital standard work and error-proofing are core components of a broader MES strategy to reduce scrap, rework, and material waste across aerospace operations. When combined with real-time monitoring of process parameters and in-process quality checks, MES helps detect problems earlier and prevent defects from multiplying across batches and operations.

    To explore how these capabilities fit into a larger waste-reduction approach—including material usage tracking, trend analysis, and margin protection in fixed-price contracts—see our overview on reducing rework with MES in aerospace manufacturing.

    For teams putting this topic into daily operation, work orders and digital travelers, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.

    This article is for aerospace operations, quality, and compliance teams who need to understand Using MES to Enforce Standard Work and Error-Proof Aerospace Operations. It explains the practical question this topic answers in a manufacturing execution context.

    The same operating model also depends on Connect 981’s aerospace execution solutions, real aerospace execution examples, Connect 981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.